CN218619072U - Device is got to top tube clamp - Google Patents
Device is got to top tube clamp Download PDFInfo
- Publication number
- CN218619072U CN218619072U CN202223159274.4U CN202223159274U CN218619072U CN 218619072 U CN218619072 U CN 218619072U CN 202223159274 U CN202223159274 U CN 202223159274U CN 218619072 U CN218619072 U CN 218619072U
- Authority
- CN
- China
- Prior art keywords
- mandrel
- plate
- mounting seat
- splint
- upper pipe
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Shaping Of Tube Ends By Bending Or Straightening (AREA)
Abstract
本实用新型公开了一种上管夹取装置。该上管夹取装置包括安装座,安装座的底部至少设置有一排用于套接管料的芯棒,芯棒的外侧套接有推料板,安装座设置有第一往返机构,第一往返机构驱使推料板将管料推离芯棒,芯棒的外侧设置有与安装座滑动连接的夹板,安装座设置有第二往返机构,第二往返机构驱使夹板与芯棒配合夹持管料。本实用新型解决了现有技术生产效率低下的问题。
The utility model discloses an upper pipe clamping device. The upper pipe clamping device includes a mounting seat, at least one row of mandrels for socketing the pipe material is arranged at the bottom of the mounting seat, a pushing plate is sleeved on the outer side of the mandrels, and the mounting seat is provided with a first reciprocating mechanism, the first reciprocating The mechanism drives the pusher plate to push the pipe material away from the mandrel, and the outer side of the mandrel is provided with a splint slidingly connected with the mounting seat, and the mounting seat is provided with a second reciprocating mechanism, which drives the splint and the mandrel to clamp the pipe material . The utility model solves the problem of low production efficiency in the prior art.
Description
技术领域technical field
本实用新型涉及自动化设备技术领域,尤其是涉及一种上管夹取装置。The utility model relates to the technical field of automation equipment, in particular to an upper pipe clamping device.
背景技术Background technique
注肩软管自动化生产线中,常常为机械手配置上料机构,上料机构主要由两组夹板构成,将管料插入注塑模具中的芯棒上。众所周知,管料的初始形状都是圆柱状,当注塑模具中的芯棒为扁圆柱时,现有的上料机构则无法将圆柱状的软管插在扁圆柱状的芯棒上,因此,大都数厂家仍然选用手工插管,导致生产效率低下。In the automatic production line of injection shoulder hose, the manipulator is often equipped with a feeding mechanism. The feeding mechanism is mainly composed of two sets of splints, which insert the tube material into the mandrel in the injection mold. As we all know, the initial shape of the pipe material is cylindrical. When the mandrel in the injection mold is a flat cylinder, the existing feeding mechanism cannot insert the cylindrical hose on the flat cylindrical mandrel. Therefore, Most manufacturers still use manual intubation, resulting in low production efficiency.
实用新型内容Utility model content
本实用新型的目的是针对现有技术存在的不足,提供一种提高生产效率的上管夹取装置。The purpose of the utility model is to provide an upper pipe clamping device which can improve production efficiency in view of the deficiencies in the prior art.
为实现上述目的,本实用新型上管夹取装置采用的技术方案是:In order to achieve the above purpose, the technical solution adopted by the upper pipe clamping device of the utility model is:
一种上管夹取装置,包括安装座,安装座的底部至少设置有一排用于套接管料的芯棒,芯棒的外侧套接有推料板,安装座设置有第一往返机构,第一往返机构驱使推料板将管料推离芯棒,芯棒的外侧设置有与安装座滑动连接的夹板,安装座设置有第二往返机构,第二往返机构驱使夹板与芯棒配合夹持管料。An upper pipe clamping device, comprising a mounting seat, at least a row of mandrels for socketing pipe materials are arranged at the bottom of the mounting seat, a pushing plate is sleeved on the outer side of the mandrels, and a first reciprocating mechanism is provided on the mounting seat. A reciprocating mechanism drives the pushing plate to push the pipe material away from the mandrel. A splint is provided on the outside of the mandrel to slide and connect with the mounting seat. The mounting seat is provided with a second reciprocating mechanism, which drives the splint to cooperate with the mandrel for clamping. pipe material.
优选的,所述第一往返机构为与安装座固接的第一气缸,第一气缸的伸缩端与推料板固接。Preferably, the first reciprocating mechanism is a first air cylinder fixedly connected to the mounting seat, and the telescopic end of the first air cylinder is fixedly connected to the pushing plate.
优选的,所述第二往返机构为与安装座连接的第二气缸,第二气缸的伸缩端与夹板固接。Preferably, the second reciprocating mechanism is a second air cylinder connected to the mounting seat, and the telescopic end of the second air cylinder is fixedly connected to the splint.
优选的,所述安装座包括第一安装板,第一安装板的底面通过若干个立柱可拆卸连接有第二安装板,所述芯棒可拆卸安装于第二安装板的底面。Preferably, the mounting base includes a first mounting plate, the bottom surface of the first mounting plate is detachably connected to the second mounting plate through several uprights, and the mandrel is detachably mounted on the bottom surface of the second mounting plate.
优选的,所述第一安装板底面至少安装有一个导轨,导轨滑配有滑块,滑块通过连接板与夹板固接。Preferably, at least one guide rail is installed on the bottom surface of the first mounting plate, the guide rail is slidably equipped with a slider, and the slider is fixedly connected to the splint through the connecting plate.
优选的,所述夹板的内侧壁设置有胶条。Preferably, the inner side wall of the splint is provided with rubber strips.
优选的,所述芯棒的顶部设置有定位凸台,第二安装板的底面设置有与定位凸台配合定位凹陷。Preferably, the top of the mandrel is provided with a positioning boss, and the bottom surface of the second mounting plate is provided with a positioning recess that cooperates with the positioning boss.
优选的,所述芯棒的横截面为圆形、扁圆形、菱形、六边形中的一种。Preferably, the cross section of the mandrel is one of circular, oblate, rhombus and hexagonal.
本实用新型与现有技术相比,具有以下优点:Compared with the prior art, the utility model has the following advantages:
1、根据产品的形状,选择对应形状的芯棒,插入上一工序中的管料,使用夹板夹持,将在上一工序中完成预成型的管料送至注塑模具中,由推料板将管料推进套接注塑模具中芯棒上,从而实现自动化生产,提高了生产效率。1. According to the shape of the product, select the mandrel of the corresponding shape, insert the tube material in the previous process, clamp it with the splint, send the tube material preformed in the previous process to the injection mold, and push the material by the push plate The pipe material is pushed onto the mandrel in the sleeve injection mold, thereby realizing automatic production and improving production efficiency.
2、第二安装板与第一安装板之间、芯棒与第二安装板之间均为可拆连接,更换方便。2. The connections between the second mounting plate and the first mounting plate, and between the mandrel and the second mounting plate are all detachable and easy to replace.
附图说明Description of drawings
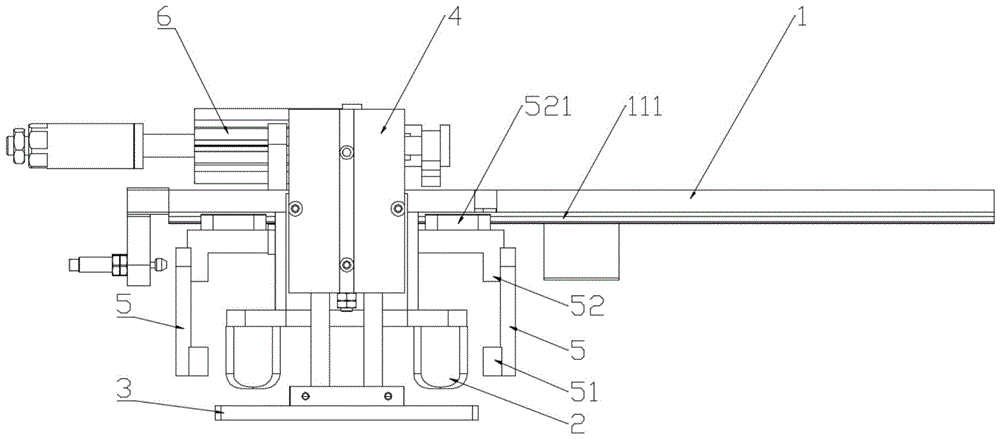
图1是本实用新型的上管夹取装置的结构示意图;Fig. 1 is a schematic structural view of the upper pipe clamping device of the present invention;
图2是安装座的结构示意图;Figure 2 is a schematic structural view of the mount;
图3是夹板的工作示意图;Fig. 3 is the working schematic diagram of splint;
图4是推料板的结构示意图。Fig. 4 is a structural schematic diagram of the pushing plate.
其中,1安装座,11第一安装板,111导轨,12立柱,13第二安装板,131定位凹陷,14第一连接板,2芯棒,21定位凸台,3推料板,31通孔,4第一往返机构,5夹板,51胶条,52第二连接板,521滑块,53第三安装板,54第一伸缩板,55连杆,56第二伸缩板,6第二往返机构。Among them, 1 mounting seat, 11 first mounting plate, 111 guide rail, 12 column, 13 second mounting plate, 131 positioning depression, 14 first connecting plate, 2 mandrel, 21 positioning boss, 3 pushing plate, 31 through Hole, 4 first reciprocating mechanism, 5 splint, 51 rubber strip, 52 second connecting plate, 521 slider, 53 third mounting plate, 54 first expansion plate, 55 connecting rod, 56 second expansion plate, 6 second to and from the agency.
具体实施方式Detailed ways
下面结合附图和具体实施方式,进一步阐明本实用新型,应理解这些实施方式仅用于说明本实用新型而不用于限制本实用新型的范围,在阅读了本实用新型之后,本领域技术人员对本实用新型的各种等价形式的修改均落于本申请所附权利要求所限定的范围。Below in conjunction with accompanying drawing and specific embodiment, further illustrate the utility model, it should be understood that these embodiments are only used to illustrate the utility model and are not intended to limit the scope of the utility model, after reading the utility model, those skilled in the art will understand this utility model The modifications of various equivalent forms of the utility model all fall within the scope defined by the appended claims of the present application.
如图1-4所示,一种上管夹取装置,包括安装座1,安装座包括第一安装板11,第一安装板的底面通过四个立柱12可拆卸连接第二安装板13,第二安装板的底部可拆卸安装两排,每排数量为四个的芯棒2,用于从上一工序中套接管料,以便单次能转运更多的管料,提高了生产效率,芯棒的横截面为扁圆形,芯棒的顶部一体成型定位凸台21,第二安装板的底面开设与定位凸台配合定位凹陷131,精确定位芯棒的位置,方便安装,芯棒的外侧套接推料板3,推料板开设与芯棒横截面匹配的通孔31,通孔与芯棒之间的间隙小于管料的壁厚,第二安装板的上方布置第一往返机构4,第一往返机构为第一气缸,考虑到受力平衡,第一气缸的数量为两个,分别处于第二安装板的前后两侧,第一气缸通过第一连接板14安装于第二安装板的顶部,第一气缸的伸缩端与推料板固接,第一气缸驱使推料板将管料推离芯棒,第二安装板的左右两侧布置与第一安装板滑动连接的夹板5,夹板的内侧壁安装胶条51,夹板的顶部两侧安装第二连接板52,第二连接板的顶部安装滑块521,滑块滑配导轨111,导轨安装于第一安装板的底面,第一安装板滑动连接第二往返机构6,第二往返机构为第二气缸,第二气缸固接第三安装板53,第三安装板的前后两侧与右侧的第二连接板固接,第二气缸的伸缩端固接第一伸缩板54,第一伸缩板通过连杆55固接第二伸缩板56,第二伸缩板的两侧与左侧的第二连接板固接,第二气缸驱使夹板与芯棒配合夹持管料。As shown in Figures 1-4, an upper pipe clamping device includes a mounting base 1, the mounting base includes a
一种上管夹取装置的具体工作过程与原理:初始时,第一、第二气缸的伸缩端均处于收缩状态,推料板套接在芯棒的外侧,夹板远离芯棒,机械手将芯棒带到上一工位,并驱使芯棒插入上一工位中的管料,启动第二气缸,第二气缸的伸缩端伸出,第一伸缩板带动左侧的夹板向右侧移动,在反作用力的影响下,第二气缸的缸体带动右侧的夹板向左侧移动,两侧的胶条将管料压紧在芯棒的侧壁,机械手将芯棒带到下一工位,先启动第二气缸松开管料,再启动第一气缸,第一气缸的伸缩端伸出,推料板将管料推进套接在注塑模具中的芯棒上,完成上料工作。本实用新型产品的形状,选择对应形状的芯棒,插入上一工序中的管料,使用夹板夹持,将在上一工序中完成预成型的管料送至注塑模具中,由推料板将管料推进套接注塑模具中芯棒上,从而实现自动化生产,提高了生产效率。The specific working process and principle of an upper pipe clamping device: Initially, the telescopic ends of the first and second cylinders are in a contracted state, the pusher plate is sleeved on the outside of the mandrel, the splint is far away from the mandrel, and the manipulator pulls the mandrel The rod is brought to the previous station, and the mandrel is driven to insert the pipe material in the previous station, the second cylinder is activated, the telescopic end of the second cylinder stretches out, and the first telescopic plate drives the splint on the left to move to the right. Under the influence of the reaction force, the cylinder body of the second cylinder drives the splint on the right to move to the left, and the rubber strips on both sides press the tube material against the side wall of the mandrel, and the manipulator takes the mandrel to the next station First start the second cylinder to loosen the pipe material, then start the first cylinder, the telescopic end of the first cylinder stretches out, and the pusher plate pushes the pipe material to be socketed on the mandrel in the injection mold to complete the feeding work. For the shape of the product of the utility model, select a mandrel of the corresponding shape, insert the pipe material in the previous process, and clamp it with a splint, and send the preformed pipe material in the previous process to the injection mold, and the material is pushed by the pushing plate The pipe material is pushed onto the mandrel in the sleeve injection mold, thereby realizing automatic production and improving production efficiency.
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223159274.4U CN218619072U (en) | 2022-11-28 | 2022-11-28 | Device is got to top tube clamp |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202223159274.4U CN218619072U (en) | 2022-11-28 | 2022-11-28 | Device is got to top tube clamp |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN218619072U true CN218619072U (en) | 2023-03-14 |
Family
ID=85450816
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202223159274.4U Expired - Fee Related CN218619072U (en) | 2022-11-28 | 2022-11-28 | Device is got to top tube clamp |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN218619072U (en) |
-
2022
- 2022-11-28 CN CN202223159274.4U patent/CN218619072U/en not_active Expired - Fee Related
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN211330942U (en) | Three-way punching die for round tubes | |
| CN106541268B (en) | A kind of O-ring automatic sheathing device for copper pipe assembling | |
| CN222153634U (en) | Stamping die with take off material mechanism | |
| CN101791655A (en) | Pipe fitting riveting machine | |
| CN201592223U (en) | A riveting machine for pipe fittings | |
| CN202070626U (en) | Multi-station pipe end forming device for manifold | |
| CN2459111Y (en) | End hole shrinking mechanism for pipe material | |
| CN205464004U (en) | Pipe fitting flaring processingequipment | |
| CN212310653U (en) | Tube End Flaring Device | |
| CN222873027U (en) | Drawing die for thin-wall rectangular pipe | |
| CN211161364U (en) | Bending device for U-shaped pipe of seat backrest framework | |
| CN210614938U (en) | A kind of reed switch bending device | |
| CN223960859U (en) | Magnetic type pressure riveting device convenient for replacing punch magnet | |
| CN201720664U (en) | Robot inlaying and picking apparatus | |
| CN221657770U (en) | Shell punching positioning device | |
| CN210586478U (en) | Ink jet device for stamping die | |
| CN222785627U (en) | Terminal spring plate assembling workbench | |
| CN222682078U (en) | A positioning mechanism for flatbed UV printing processing | |
| CN222767242U (en) | Motor casing riveting tools that can automatic positioning | |
| CN223338166U (en) | Square pipe punching device | |
| CN223354103U (en) | A fixture for producing faucets | |
| CN209813349U (en) | Cold press convenient to operate | |
| CN112108567A (en) | Arc panel beating work piece stamping die | |
| CN223617267U (en) | Locking clamp for sawing machine machining | |
| CN222805878U (en) | A high-strength guide pipe flanging tool |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20230314 |