CN218340923U - Forging die - Google Patents
Forging die Download PDFInfo
- Publication number
- CN218340923U CN218340923U CN202222778050.5U CN202222778050U CN218340923U CN 218340923 U CN218340923 U CN 218340923U CN 202222778050 U CN202222778050 U CN 202222778050U CN 218340923 U CN218340923 U CN 218340923U
- Authority
- CN
- China
- Prior art keywords
- spring
- seat
- block
- upsetting
- plate
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000005242 forging Methods 0.000 title claims abstract description 34
- 238000004080 punching Methods 0.000 claims abstract description 56
- 238000003825 pressing Methods 0.000 claims abstract description 23
- 230000007246 mechanism Effects 0.000 claims abstract description 17
- 238000012423 maintenance Methods 0.000 abstract description 3
- 238000004519 manufacturing process Methods 0.000 description 14
- 239000000463 material Substances 0.000 description 5
- 239000000654 additive Substances 0.000 description 2
- 230000000996 additive effect Effects 0.000 description 2
- 230000006835 compression Effects 0.000 description 2
- 238000007906 compression Methods 0.000 description 2
- 230000007547 defect Effects 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 238000005299 abrasion Methods 0.000 description 1
- 238000009825 accumulation Methods 0.000 description 1
- 230000003044 adaptive effect Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 230000002035 prolonged effect Effects 0.000 description 1
Images



Landscapes
- Forging (AREA)
Abstract
The utility model relates to a forging die, which comprises a bottom plate, a die holder, a clamping mechanism and an inclined punching module, wherein the die holder comprises a U-shaped block, a clamping block seat, a clamping block, a upsetting module, a circular pressing plate and a upsetting slider, a forming groove for forging parts is arranged in the upsetting module, a V-shaped groove is formed between the upsetting slider and the inner side wall of the U-shaped block, and the upsetting slider can slide between the clamping block seat and the side wall of the U-shaped block; the clamping mechanism is used for fastening the clamping block so as to clamp the workpiece; the inclined punching module comprises a first upper template, a first inclined punching plate, a first spring guide rod, a first spring and a spring pressing sleeve, wherein one end of the first spring guide rod penetrates through the U-shaped block to be connected with the upsetting slide block, the other end of the first spring guide rod is connected with the spring pressing sleeve, and the first spring is sleeved on the first spring guide rod and is positioned between the U-shaped block and the spring pressing sleeve; the first inclined punching plate is V-shaped in section, and the first upper die plate is used for being connected with a punch press or an oil press. The device has the advantages of high efficiency, simple and convenient use, easy maintenance and the like.
Description
Technical Field
The utility model relates to a forge the mould field, in particular to be applied to axle type part, need carry out the forging mould of vibration material disk.
Background
When some shaft parts are produced, two ends often need larger diameters to meet the requirements of the use performance of the parts, and the shaft parts often need to adopt additive manufacturing, namely a manufacturing method of material accumulation. The conventional manufacturing process is additive manufacturing using a forging machine or a swaging press. The special equipment has large volume and high cost, is not easy to purchase, is not suitable for small and medium-sized factory enterprises, has the defects of high price, long equipment input period, large one-time input, long return period and the like if the special equipment is purchased by the factories, and is not beneficial to the operation and maintenance of the factories and the production of products. If a punch press or an oil press with low cost and simple operation is used as power drive, the existing forging die is not adaptive enough, and is often realized by multiple sets of tools, so that the production and processing procedures are multiple, the production efficiency is low, and the production quality is difficult to guarantee.
SUMMERY OF THE UTILITY MODEL
The utility model aims to solve the technical problem that a forging die is provided, use equipment such as punch press or hydraulic press can replace forging machine or swager promptly and realize the vibration material disk, when saving equipment and dropping into, can also improve machining efficiency, reduce manufacturing cost.
The utility model adopts the following technical scheme to solve the technical problem.
A forging die comprises a bottom plate, a die holder, a clamping mechanism and an inclined punching module, wherein the die holder comprises a U-shaped block, a clamping block seat, a clamping block, a upsetting module, a circular pressing plate and an upsetting slider, the U-shaped block is fixed on the bottom plate, the clamping block seat, the upsetting module, the circular pressing plate and the upsetting slider are sequentially arranged in a U-shaped groove of the U-shaped block, the clamping block seat is tightly attached to the inner side edge of one end of the U-shaped block and fixed, the clamping block is arranged in the clamping block seat, a forming groove for forging parts is formed in the upsetting module, a flange is arranged at the end of one end of the upsetting module and fixed to one side of the upsetting slider through the circular pressing plate, the other side of the upsetting slider is obliquely arranged and forms a V-shaped groove with the inner side wall of the U-shaped block, and the upsetting slider can slide between the clamping block seat and the side wall of the U-shaped block;
the clamping mechanism comprises two groups of clamping components positioned on two sides of the die holder and used for fastening the clamping blocks so as to clamp the workpiece;
the inclined punching module comprises a first upper template, a first inclined punching plate, a first spring guide rod, a first spring and a spring pressing sleeve, wherein one end of the first spring guide rod penetrates through the U-shaped block to be connected with the upsetting slide block, the other end of the first spring guide rod is connected with the spring pressing sleeve, and the first spring is sleeved on the first spring guide rod and is positioned between the U-shaped block and the spring pressing sleeve; the first inclined punching plate is positioned below the first upper template and is perpendicular to the first upper template, one side of the first inclined punching plate is obliquely arranged, the inclination angle of the first inclined punching plate is the same as that of the sliding block, the section of the first inclined punching plate is V-shaped, and the first upper template is used for being connected with a punch press or an oil press.
Furthermore, a through groove capable of accommodating the first spring guide rod to penetrate is formed in the center of the first inclined punching plate.
Furthermore, the clamping mechanism comprises two groups of first sliding seats, second sliding seats, first roller seats, second rollers, disc springs, disc spring sliding blocks, first push rods, first push rod seats, first pin shafts, second pin shafts, third pin shafts, fourth pin shafts, second push rods, second upper templates and second inclined punching plates, wherein the two groups of first sliding seats, the second sliding seats, the first pin shafts, the second pin shafts, the third pin shafts, the fourth pin shafts, the second push rods, the second upper templates and the second inclined punching plates are positioned on two sides of the die holder, the first roller seats, the second roller seats, the first sliding seats and the second sliding seats are sequentially fixed on the bottom plate from right to left, a groove with a V-shaped bottom is formed between the first roller seats and the second roller seats, a sliding groove is horizontally arranged at the top of the second roller seats, the second rollers are embedded in the sliding groove and can horizontally displace along the sliding groove, the disc spring sliding blocks are positioned on one side, close to the second roller seats, of the second sliding seats, one end of a first push rod is sleeved with a disc-shaped spring sliding block, the disc-shaped spring is sleeved on the disc-shaped spring sliding block and is positioned between the first push rod and the disc-shaped spring sliding block, the other end of the first push rod is sleeved with a first push rod seat, the connecting positions of the first push rod and the first push rod seat are respectively provided with a first pin shaft hole, a first pin shaft is placed in the first pin shaft hole, the other end of the first push rod seat is provided with a second pin shaft hole, a second pin shaft is placed in the second pin shaft hole, one side of a second sliding seat, which is far away from a second roller seat, is provided with a movable push rod seat, a movable groove is formed in the movable push rod seat, the second pin shaft, a third pin shaft and a fourth pin shaft are all positioned in the movable groove, and the second pin shaft is positioned between the third pin shaft and the fourth pin shaft; the second push rod is perpendicular to the clamping block and can penetrate through the clamping block seat to be in contact with the clamping block; the second inclined punching plate is positioned below the second upper template and is perpendicular to the second upper template, the bottom of the second inclined punching plate is V-shaped, and the second upper template is used for being connected with a punch press or an oil press.
Furthermore, the clamping mechanism is also provided with a first roller which is rotatably connected to the top of the first roller seat through a first roller shaft.
Furthermore, the first upper template and the second upper template are positioned on the same horizontal line, and the length of the second inclined punching plate is greater than that of the first inclined punching plate, so that the clamping stroke is advanced than the upsetting stroke, namely, the workpiece is clamped by the clamping mechanism at the beginning of upsetting.
Further, the forging die further comprises a reset boosting module, the reset boosting module comprises a second spring support, a second spring guide rod, a second spring and a reset sliding block, the second spring support is arranged on the left side of the second sliding seat, the second spring support is L-shaped, a hollow groove is formed between the second spring support and the second sliding seat, the second spring guide rod penetrates through holes reserved in the second spring support and the second sliding seat and can slide in the holes, the second spring sleeve is arranged on the second spring guide rod and located between the second spring support and the second sliding seat, and the reset sliding block is located on the second sliding seat and connected with the end of the second spring guide rod.
Furthermore, the axes of the second spring guide rod, the reset sliding block, the first push rod and the disk spring sliding block are all located on the same straight line, and the axes of the clamping block seat, the upsetting module and the first spring guide rod are all located on the same straight line.
The utility model has the advantages that:
the utility model provides a stable tool mould for forging shaft parts, which uses a punch or an oil press to provide driving force and has the advantages of high efficiency, simple and convenient use, easy maintenance and the like; the material increase manufacturing device can replace a forging machine or a die forging machine to realize material increase manufacturing and reduce production cost, and can avoid the defects of long production period, large one-time investment, long return period and the like caused by the investment of new equipment.
The device simple structure, clamping mechanism and oblique towards module mutually support, have realized that automatic clamp is tight before forging, can realize the quick clamp of work piece and drawing of patterns through clamping mechanism and the boosting module that resets simultaneously, convenient operation has promoted production efficiency.
Drawings
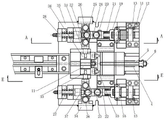
Fig. 1 is a schematic view of the overlooking structure of the forging die of the present invention.
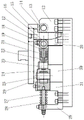
Fig. 2 is a cross-sectional view taken along section E-E in fig. 1.
Fig. 3 is a cross-sectional view taken along line a-a of fig. 1.
Fig. 4 is a schematic side view of the first inclined stamping plate of the forging die of the present invention.
Fig. 5 is an exploded view of some parts in the clamping mechanism of the forging die of the present invention.
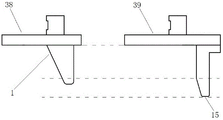
Fig. 6 is a comparison diagram of the first inclined punching plate and the second inclined punching plate of the forging die of the present invention.
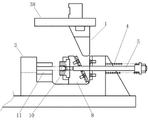
Fig. 7 is an opening state diagram of the oblique punching module of the forging mold of the present invention.
In the figure:
1-first inclined punch plate, 2-first friction plate, 3-U-shaped block, 4-first spring, 5-first spring guide rod, 6-spring press sleeve, 7-second friction plate, 8-upsetting slide block, 9-circular press plate, 10-upsetting module, 11-clamping block, 12-first roller seat, 13-first roller shaft, 14-first roller, 15-second inclined punch plate, 16-second roller, 17-second roller shaft, 18-cover plate, 19-disc spring slide block, 20-second roller seat, 21-disc spring, 22-first push rod, 23-first pin shaft, 24-first push rod seat, 25-second pin shaft, 26-third pin shaft, 27-second spring, 28-second spring guide rod, 29-second spring seat, 30-first slide seat, 31-second slide seat, 32-fourth push rod, 33-second pin shaft, 34-movable push rod seat, 35-bottom plate seat, 35-36-second spring guide rod, 37-second slide block seat, and upper die plate return block seat.
Detailed Description
In order to make the aforementioned objects, features and advantages of the present invention more clearly understood, the present invention will be described in further detail with reference to the accompanying drawings and detailed description. In the following description, numerous specific details are set forth in order to provide a thorough understanding of the present invention, however, the present invention may be practiced in other ways than those specifically described herein, and the present invention is not limited to the specific embodiments disclosed below.
As shown in 1~7, the forging die comprises a bottom plate 35, a die holder, a clamping mechanism and an inclined punching module, wherein the die holder comprises a U-shaped block 3, a clamping block seat 36, a clamping block 11, an upsetting module 10, a circular pressing plate 9 and an upsetting slider 8, the U-shaped block 3 is fixed on the bottom plate 35, the clamping block seat 36, the upsetting module 10, the circular pressing plate 9 and the upsetting slider 8 are sequentially arranged in a U-shaped groove of the U-shaped block 3, the clamping block seat 36 is fixed to the inner side edge of one end of the U-shaped block 3 in a clinging manner, the clamping block 11 is arranged in the clamping block seat 36, a forming groove for part forging is formed in the upsetting module 10, a flange is arranged at the end of one end of the upsetting module 10 and fixed to one side of the upsetting slider 8 through the circular pressing plate 9 and a bolt, the other side of the upsetting slider 8 is obliquely arranged and forms a V-shaped groove with the inner side wall of the U-shaped block 3, and the upsetting slider 8 can slide between the clamping block seat 36 and the side wall of the U-shaped block 3; and a first friction plate 2 and a second friction plate 7 are respectively arranged on the inner side wall of the U-shaped block 3 and the side wall of the upsetting slide block 8, so that the abrasion of the U-shaped block 3 and the upsetting slide block 8 is reduced, and the service life of the die is prolonged.
The clamping mechanism comprises two groups of first sliding seats 30, second sliding seats 31, first roller seats 12, second roller seats 20, first rollers 14, second rollers 16, disk springs 21, disk spring sliders 19, first push rods 22, first push rod seats 24, first pin shafts 23, second pin shafts 25, third pin shafts 26, fourth pin shafts 32, second push rods 33, second upper templates 39 and second inclined punching plates 15, the first roller seats 12, the second roller seats 20, the first sliding seats 30 and the second sliding seats 31 are sequentially fixed on a bottom plate 35 from right to left, and a groove with a V-shaped bottom is formed between the first roller seats 12 and the second roller seats 20; the first roller 14 is fixed on the top of the first roller seat 12 through a first roller shaft 13, and the first roller 14 can rotate around the first roller shaft 13 so as to reduce friction; a sliding groove is horizontally formed in the top of the second roller seat 20, the second roller 16 is embedded in the sliding groove through a second roller shaft 17, a cover plate 18 is arranged at the top of the second roller seat for fixing, the second roller 16 can horizontally move along the sliding groove, the disc spring slider 19 is arranged on one side, close to the second roller seat 20, of the second sliding seat 31, one end of the first push rod 22 is sleeved with the disc spring slider 19, the disc spring 21 is sleeved on the disc spring slider 19 and is positioned between the first push rod 22 and the disc spring slider 19, the other end of the first push rod 22 is sleeved with the first push rod seat 24, a first pin shaft 23 hole is formed in the connecting position of the first push rod 22 and the first push rod seat 24, the first pin shaft 23 is arranged in the first pin shaft 23 hole, a second pin shaft 25 hole is formed in the other end of the first push rod seat 24, the second pin shaft 25 is arranged in the second pin shaft 25 hole, a movable push rod seat 34 is arranged on one side, far away from the second roller seat 20, a movable groove is formed in the movable push rod seat 34, the second pin shaft 25, the third pin shaft 26 and the fourth pin shaft 32 are positioned between the second pin shaft 25 and the fourth pin shaft 32; wherein, the length of the movable groove is slightly less than the sum of the diameters of the second pin shaft 25, the third pin shaft 26 and the fourth pin shaft 32; the second push rod 33 is arranged perpendicular to the clamping block 11, and the second push rod 33 can penetrate through the clamping block seat 36 to be in contact with the clamping block 11 and is used for pushing the clamping block 11 tightly so as to clamp a workpiece; the second inclined punching plate 15 is positioned below the second upper die plate 39, the second inclined punching plate 15 and the second upper die plate 39 are vertically arranged, the bottom of the second inclined punching plate 15 is V-shaped, and the second upper die plate 39 is used for being connected with a punch press or an oil press and can drive the second inclined punching plate 15 to press downwards into a groove between the first roller seat 12 and the second roller seat 20.
The inclined punching module comprises a first upper template 38, a first inclined punching plate 1, a first spring guide rod 5, a first spring 4 and a spring pressing sleeve 6, wherein one end of the first spring guide rod 5 penetrates through the U-shaped block 3 to be connected with the upsetting slide block 8, the spring pressing sleeve 6 is arranged at the end part of the other end of the first spring guide rod 5, and the first spring 4 is sleeved on the first spring guide rod 5 and is positioned between the U-shaped block 3 and the spring pressing sleeve 6; the first inclined punching plate 1 is located below the first upper die plate 38, the first inclined punching plate 1 and the first upper die plate 38 are vertically arranged, one side of the first inclined punching plate 1 is obliquely arranged, the inclination angle of the first inclined punching plate is the same as that of the sliding block, the section of the first inclined punching plate is V-shaped, the first upper die plate 38 is used for being connected with a punch press or an oil press, and the first inclined punching plate 1 can be driven to be pressed downwards into a V-shaped groove between the upsetting sliding block 8 and the U-shaped block 3. The center of the first inclined punching plate 1 is provided with a through groove which can accommodate the first spring guide rod 5 to pass through and is vertically arranged, and through holes which can accommodate the first spring guide rod 5 to pass through are reserved on the first friction plate 2 and the second friction plate 7.
The forging die further comprises a resetting boosting module, the resetting boosting module comprises a second spring support 29, a second spring guide rod 28, a second spring 27 and a resetting sliding block 37, the second spring support 29 is arranged on the left side of a second sliding seat 31, the second spring support 29 is L-shaped, a hollow groove is formed between the second spring support 29 and the second sliding seat 31, the second spring guide rod 28 penetrates through holes reserved in the second spring support 29 and the second sliding seat 31 and can slide in the holes, the second spring 27 is sleeved on the second spring guide rod 28 and located between the second spring support 29 and the second sliding seat 31, and the resetting sliding block 37 is located on the second sliding seat 31 and connected with the end of the second spring guide rod 28.
The axes of the second spring guide rod 28, the reset slider 37, the first push rod 22 and the disk spring slider 19 are all located on the same straight line, and the axes of the clamping block seat 36, the upsetting module 10 and the first spring guide rod 5 are all located on the same straight line.
As shown in fig. 6, the first upper die plate 38 and the second upper die plate 39 are located on the same horizontal line, and the length of the second inclined punch plate 15 is greater than that of the first inclined punch plate 1, so that the clamping stroke is performed earlier than the upsetting stroke, that is, at the beginning of upsetting, the clamping mechanism has already finished clamping the workpiece.
The specific working process of the device is as follows: firstly, a workpiece penetrates through the U-shaped block 3 and the clamping block 11 and is placed into the upsetting module 10, then a punch press or a press machine is started to drive the first upper template 38 and the second upper template 39 to simultaneously press downwards, and therefore the first inclined punching plate 1 and the second inclined punching plate 15 are driven to simultaneously move downwards; at this time, since the length of the second inclined punching plate 15 is greater than that of the first inclined punching plate 1, the second inclined punching plate 15 firstly enters the groove between the first roller seat 12 and the second roller seat 20, the second roller 16 is pushed to move in the second roller seat 20 to the side of the disc spring slider 19, the disc spring slider 19 is pushed to move by extrusion, so that the first push rod 22, the first pin 23, the first push rod seat 24 and the second pin 25 are pushed to move simultaneously (at this time, the disc spring 21 compresses the accumulated force), the third pin 26 and the fourth pin 32 are pushed by the second pin 25, but the third pin 26 is limited by the movable push rod seat 34 and cannot move, so that the force acts on the fourth pin 32 to displace the fourth pin 32, the second push rod 33 is pushed to move inwards, a lateral clamping force is provided for the clamping block 11, and the clamping block 11 can clamp the workpiece to prevent the workpiece from moving backwards during forging; at this point the second spring 27 is compressed and the second spring guide 28 and the return slider 37 move backwards.
When a workpiece is clamped, the first inclined punching plate 1 moves downwards into a V-shaped groove between the upsetting slide block 8 and the U-shaped block 3 to push the upsetting slide block 8 to translate, the upsetting slide block 8 pushes the circular press plate 9 and the upsetting module 10 to move forwards to complete one-time forging and pressing, at the moment, the first spring guide rod 5 is driven by the upsetting slide block 8 to move forwards, and the first spring 4 is compressed.
Then the punch press or the press machine drives the first upper template 38 and the second upper template 39 to move upwards simultaneously, drives the first inclined punching plate 1 and the second inclined punching plate 15 to move upwards simultaneously, the first spring 4 releases the compression state to provide restoring force, pushes the first spring guide rod 5 to move backwards, and drives the upsetting slide block 8, the circular press plate 9 and the upsetting module 10 to move backwards, so that the workpiece is demoulded; similarly, the second spring 27 and the belleville spring 21 provide restoring force when the compression state is released, and respectively push the reset slider 37, the second spring guide 28, the second pin 25, the first push rod seat 24, the first pin 23, the first push rod 22, the belleville spring slider 19 and the second roller 16 to move, so that the component providing the lateral clamping force returns to the initial position, and the clamping state of the clamping block 11 is released. Waiting for the next job.
The above description is only a preferred embodiment of the present invention and is not intended to limit the present invention, and various modifications and changes may be made by those skilled in the art. Any modification, equivalent replacement, or improvement made within the spirit and principle of the present invention should be included in the protection scope of the present invention.
Claims (7)
1. A forging die comprises a bottom plate, a die holder, a clamping mechanism and an inclined punching module, and is characterized in that the die holder comprises a U-shaped block, a clamping block seat, a clamping block, an upsetting module, a circular pressing plate and an upsetting slider, the U-shaped block is fixed on the bottom plate, the clamping block seat, the upsetting module, the circular pressing plate and the upsetting slider are sequentially arranged in the U-shaped groove of the U-shaped block, the clamping block seat is tightly attached to the inner side edge of one end of the U-shaped block to be fixed, the clamping block is arranged in the clamping block seat, a forming groove for part forging is formed in the upsetting module, a flange is arranged at one end of the upsetting module and fixed on one side of the upsetting slider through the circular pressing plate, the other side of the upsetting slider is obliquely arranged and forms a V-shaped groove with the inner side wall of the U-shaped block, and the upsetting slider can slide between the clamping block seat and the side wall of the U-shaped block;
the clamping mechanism comprises two groups of clamping components positioned on two sides of the die holder and used for fastening the clamping blocks so as to clamp the workpiece;
the inclined punching module comprises a first upper template, a first inclined punching plate, a first spring guide rod, a first spring and a spring pressing sleeve, wherein one end of the first spring guide rod penetrates through the U-shaped block to be connected with the upsetting slide block, the other end of the first spring guide rod is connected with the spring pressing sleeve, and the first spring is sleeved on the first spring guide rod and is positioned between the U-shaped block and the spring pressing sleeve; the first inclined punching plate is positioned below the first upper template and is perpendicular to the first upper template, one side of the first inclined punching plate is obliquely arranged, the inclination angle of the first inclined punching plate is the same as that of the sliding block, the section of the first inclined punching plate is V-shaped, and the first upper template is used for being connected with a punch press or an oil press.
2. The forging die of claim 1, wherein a through slot capable of accommodating the first spring guide rod is formed in the center of the first inclined punching plate.
3. The forging die of claim 1, wherein the clamping mechanism includes two sets of first sliding seats, second sliding seats, first roller seats, second rollers, disk springs, disk spring sliders, first push rods, first push rod seats, first pin shafts, second pin shafts, third pin shafts, fourth pin shafts, second push rods, second upper die plates and second inclined punch plates, the first roller seats, the second roller seats, the first sliding seats and the second sliding seats are sequentially fixed on the bottom plate from right to left, a groove with a V-shaped bottom is formed between the first roller seats and the second roller seats, a sliding groove is horizontally formed at the top of the second roller seats, and the second rollers are embedded in the sliding groove and can horizontally move along the sliding groove, the disc spring sliding block is positioned on one side, close to the second roller seat, of the second sliding seat, one end of the first push rod is sleeved with the disc spring sliding block, the disc spring is sleeved on the disc spring sliding block and positioned between the first push rod and the disc spring sliding block, the other end of the first push rod is sleeved with the first push rod seat, a first pin hole is formed in the connecting position of the first push rod and the first push rod seat, the first pin shaft is placed in the first pin hole, a second pin hole is formed in the other end of the first push rod seat, the second pin shaft is placed in the second pin hole, a movable push rod seat is arranged on one side, away from the second roller seat, of the second sliding seat, a movable groove is formed in the movable push rod seat, the second pin shaft, the third pin shaft and the fourth pin shaft are all positioned in the movable groove, and the second pin shaft is positioned between the third pin shaft and the fourth pin shaft; the second push rod is perpendicular to the clamping block and can penetrate through the clamping block seat to be in contact with the clamping block; the second inclined punching plate is positioned below the second upper template and is perpendicular to the second upper template, the bottom of the second inclined punching plate is V-shaped, and the second upper template is used for being connected with a punch press or an oil press.
4. The forging die of claim 3, wherein the clamping mechanism further includes a first roller rotatably coupled to the top of the first roller mount by a first roller shaft.
5. The forging die of claim 3, wherein the first upper die plate and the second upper die plate are located on the same horizontal line, and the length of the second inclined punching plate is greater than that of the first inclined punching plate.
6. The forging die of claim 3, further comprising a resetting boosting module, wherein the resetting boosting module comprises a second spring support, a second spring guide rod, a second spring and a resetting slide block, the second spring support is arranged on the left side of the second slide seat, the second spring guide rod passes through holes reserved in the second spring support and the second slide seat and can slide in the holes, the second spring is sleeved on the second spring guide rod and located between the second spring support and the second slide seat, and the resetting slide block is located on the second slide seat and is connected with the end of the second spring guide rod.
7. The forging die as recited in claim 6, wherein axes of the second spring guide rod, the reset slider, the first push rod and the disc spring slider are all located on the same straight line, and axes of the clamping block seat, the upsetting module and the first spring guide rod are all located on the same straight line.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222778050.5U CN218340923U (en) | 2022-10-21 | 2022-10-21 | Forging die |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222778050.5U CN218340923U (en) | 2022-10-21 | 2022-10-21 | Forging die |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN218340923U true CN218340923U (en) | 2023-01-20 |
Family
ID=84897740
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202222778050.5U Active CN218340923U (en) | 2022-10-21 | 2022-10-21 | Forging die |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN218340923U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115592064A (en) * | 2022-10-21 | 2023-01-13 | 江西方大长力汽车零部件有限公司(Cn) | a forging mold |
-
2022
- 2022-10-21 CN CN202222778050.5U patent/CN218340923U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115592064A (en) * | 2022-10-21 | 2023-01-13 | 江西方大长力汽车零部件有限公司(Cn) | a forging mold |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN220127267U (en) | Quick bending structure and bending die suitable for symmetrical workpieces | |
| CN117282899B (en) | Forging and pressing device for flange machining | |
| CN211071651U (en) | Friction press | |
| CN221675491U (en) | A radiator mold for a car | |
| CN221754474U (en) | Deburring and punching device | |
| CN113634703A (en) | A rivet pressing fixture | |
| CN212944965U (en) | Inclined pushing mechanism for forming flanging | |
| CN113245458B (en) | Punching blanking machine for pipes, angle irons and channel steel | |
| CN118357333A (en) | Construction engineering stamping equipment for machining mechanical parts and application method | |
| CN214053273U (en) | A kind of iron sheet stamping equipment for industrial production | |
| CN210676541U (en) | Punching die capable of reversing punching direction | |
| CN210451360U (en) | Lower tray friction welding frock clamp | |
| CN222288463U (en) | A stamping equipment for steel production | |
| CN216542379U (en) | Side hole chamfering device | |
| CN115592064A (en) | a forging mold | |
| CN223718067U (en) | Metal pipe forming device | |
| CN221537785U (en) | A metal parts processing stamping machine tool | |
| CN219817679U (en) | Processing die capable of preventing automobile gasket from deforming | |
| CN220717367U (en) | Metal fitting multistation stamping device | |
| CN222242153U (en) | Stamping device is used in bearing roller production | |
| CN222902239U (en) | Workpiece bending and shaping device for stamping | |
| CN217369954U (en) | Accurate hardware component stamping equipment | |
| CN223981116U (en) | A relay splitting and riveting mold | |
| CN217412132U (en) | Automobile precision stamping die without pre-punching hole flanging structure | |
| CN219335665U (en) | Outer tube riveting die |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |