CN218274876U - Battery unit and battery module - Google Patents
Battery unit and battery module Download PDFInfo
- Publication number
- CN218274876U CN218274876U CN202221696051.9U CN202221696051U CN218274876U CN 218274876 U CN218274876 U CN 218274876U CN 202221696051 U CN202221696051 U CN 202221696051U CN 218274876 U CN218274876 U CN 218274876U
- Authority
- CN
- China
- Prior art keywords
- battery
- bracket
- battery unit
- positioning
- unit according
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Landscapes
- Connection Of Batteries Or Terminals (AREA)
Abstract
本实用新型涉及电池领域,公开了一种电池单元以及电池模组。所述电池单元包括具有容纳腔的散热板(1)、位于所述容纳腔内的电芯(2)以及连接于所述散热板(1)两端的支架(3),所述支架(3)上形成有安装槽(31),所述电芯(2)的极耳上连接有转接片(4),所述转接片(4)安装于所述安装槽(31)内。本实用新型中,通过在散热板两端设置支架构成电池框架,结构简单可靠,符合批量化、自动化的生产要求;将电芯的极耳通过转接片安装于支架的安装槽内,提高了电池单元的装配效率。并且多个电池单元之间可通过汇流排进行串并联连接,无需在汇流排上切出极耳穿过的位置,降低了汇流排的厚度,从而降低模组的重量以及生产成本。
The utility model relates to the field of batteries, and discloses a battery unit and a battery module. The battery unit includes a heat dissipation plate (1) having a housing chamber, an electric cell (2) located in the housing chamber, and brackets (3) connected to both ends of the heat dissipation plate (1), the bracket (3) An installation groove (31) is formed on the top, and an adapter piece (4) is connected to the tab of the battery core (2), and the adapter piece (4) is installed in the installation groove (31). In the utility model, the battery frame is formed by setting brackets at both ends of the cooling plate, the structure is simple and reliable, and meets the production requirements of mass production and automation; Assembly efficiency of battery cells. Moreover, multiple battery cells can be connected in series and parallel through the bus bar, without cutting out the position where the tabs pass through on the bus bar, reducing the thickness of the bus bar, thereby reducing the weight of the module and the production cost.
Description
技术领域technical field
本实用新型涉及电池技术领域,具体地涉及一种电池单元。在此基础之上,还涉及一种电池模组。The utility model relates to the technical field of batteries, in particular to a battery unit. On this basis, it also relates to a battery module.
背景技术Background technique
在新能源电池领域,由锂离子电池组成的大模组在提升系统能量密度和集成效率方面有很大优势,已经得到广泛的应用。软包锂离子电池大模组结构复杂,通常由于软包电芯自身不具备结构强度,需要较强的结构件,完成电芯的保护以及模组结构的实现,同时电芯之间的串并联需要良好的绝缘,汇流排通常需要载体承载,进一步增加了软包模组结构的复杂程度,并且零件种类的增加在工艺难度以及成本上都造成了增加。In the field of new energy batteries, large modules composed of lithium-ion batteries have great advantages in improving system energy density and integration efficiency, and have been widely used. The structure of the large module of soft-packed lithium-ion battery is complicated. Usually, because the soft-packed battery cell itself does not have structural strength, it needs strong structural parts to complete the protection of the battery cell and the realization of the module structure. At the same time, the series-parallel connection between the cells Good insulation is required, and the busbar usually needs to be carried by a carrier, which further increases the complexity of the soft package module structure, and the increase in the number of parts increases the process difficulty and cost.
此外,传统的软包锂离子电池模组电芯通常放置在框架内,电芯的极耳在模组两侧布置。电芯极耳折弯后,需要进行激光焊接,使得极耳与汇流排形成牢固连接;由于极耳穿插位置的铜排需要开孔避让,造成过流面积减小,故需要增厚铜排,进而增加了原材料成本。为了工艺可实现性以及绝缘保护等考虑,现有的软包模组的汇流排通常需要另外一个零件进行固定承载,汇流排的载体零件与框架上的注塑件效果有所重叠,进一步导致成本增加。并且,由于软包电芯极耳厚度较薄,在进行汇流焊接时,仅能将铜极耳焊接到铜排上,故汇流排的选材只能考虑铜排或者铜铝复合排。然而,铜排成本较高,重量较重,直接影响模组的成组效率以及原材料成本。为了解决传统的软包模组的成组过程中的问题,比如仅能采用铜排或者铜铝复合排进行汇流,而且传统的软包模组汇流排由于开口避让电芯极耳穿插位置,为了保证过流面积,只能增厚铜排,采用的铜排通常在2mm以上,以及传统软包电芯成组方案复杂,零件众多的问题。In addition, the cells of traditional soft-pack lithium-ion battery modules are usually placed in the frame, and the tabs of the cells are arranged on both sides of the module. After the battery tab is bent, laser welding is required to form a firm connection between the tab and the bus bar; since the copper bar at the insertion position of the tab needs to be opened to avoid, resulting in a reduction in the flow area, it is necessary to thicken the copper bar. This increases the cost of raw materials. For the sake of process feasibility and insulation protection, the busbar of the existing soft-pack module usually needs another part to carry the fixed load. The effect of the carrier part of the busbar and the injection molded part on the frame overlaps, which further leads to an increase in cost. . Moreover, due to the thin thickness of the lugs of the soft-packed cells, only the copper tabs can be welded to the copper bars during bus welding, so the selection of bus bars can only consider copper bars or copper-aluminum composite bars. However, the cost of copper bars is high and the weight is heavy, which directly affects the grouping efficiency of modules and the cost of raw materials. In order to solve the problems in the grouping process of traditional soft-pack modules, for example, only copper bars or copper-aluminum composite bars can be used for confluence, and the traditional soft-pack module bus bars avoid the insertion position of battery tabs due to openings. To ensure the overcurrent area, only thicken the copper bar, the copper bar used is usually more than 2mm, and the traditional soft-packed battery grouping scheme is complicated and there are many parts.
实用新型内容Utility model content
本实用新型的目的是为了克服现有技术存在的电池模组装配效率低下的问题,提供一种电池单元,该电池单元具有能够提高电池模组装配效率的优点。The purpose of the utility model is to overcome the problem of low assembly efficiency of the battery module in the prior art, and provide a battery unit which has the advantage of improving the assembly efficiency of the battery module.
为了实现上述目的,本实用新型第一方面提供一种电池单元,所述电池单元包括具有容纳腔的散热板、位于所述容纳腔内的电芯以及连接于所述散热板两端的支架,所述支架上形成有安装槽,所述电芯的极耳上连接有转接片,所述转接片安装于所述安装槽内。In order to achieve the above object, the first aspect of the utility model provides a battery unit, the battery unit includes a heat dissipation plate with an accommodation cavity, an electric cell located in the accommodation cavity, and brackets connected to both ends of the heat dissipation plate, the A mounting groove is formed on the bracket, and an adapter piece is connected to the tab of the battery cell, and the adapter piece is installed in the installation groove.
可选地,所述支架的背离所述容纳腔的一侧设置有卡扣,并且/或者,所述支架的沿所述电芯的层叠方向的两端设有定位销和/或定位孔。Optionally, buckles are provided on a side of the support away from the accommodating cavity, and/or positioning pins and/or positioning holes are provided at both ends of the support along the stacking direction of the battery cells.
可选地,所述支架的沿所述电芯的层叠方向的端部分别设置有所述定位销以及所述定位孔。Optionally, the positioning pins and the positioning holes are respectively provided at the ends of the support along the stacking direction of the electric cores.
可选地,所述支架包括位于沿所述电芯的层叠方向的两端的第一侧壁和第二侧壁,所述第一侧壁上设置有第一定位销和第一定位孔,所述第二侧壁上设有第二定位销和第二定位孔;其中,所述第一定位销与所述第二定位孔同轴,所述第二定位销与所述第一定位孔同轴。Optionally, the bracket includes a first side wall and a second side wall located at both ends along the stacking direction of the battery cells, the first side wall is provided with a first positioning pin and a first positioning hole, so The second side wall is provided with a second positioning pin and a second positioning hole; wherein, the first positioning pin is coaxial with the second positioning hole, and the second positioning pin is coaxial with the first positioning hole axis.
可选地,所述支架上设置有热熔点,所述散热板通过该热熔点热熔连接至所述支架。Optionally, a heat melting point is provided on the support, and the heat dissipation plate is thermally connected to the support through the heat melting point.
可选地,所述支架上形成有上下对称的两个所述安装槽。Optionally, two vertically symmetrical installation grooves are formed on the bracket.
可选地,所述支架为注塑件,并且/或者,所述支架上设置有与外部零件连接的安装孔。Optionally, the bracket is an injection molded part, and/or, the bracket is provided with mounting holes for connecting with external parts.
可选地,所述电池单元包括多个所述电芯,多个所述电芯的极耳通过预折弯而彼此贴合,并通过激光焊接连接至所述转接片。Optionally, the battery unit includes a plurality of battery cells, tabs of the battery cells are pre-bent to be attached to each other, and connected to the adapter piece by laser welding.
本实用新型第二方面提供一种电池模组,所述电池模组包括上述的电池单元以及连接于所述转接片的汇流排。The second aspect of the present invention provides a battery module, which includes the above-mentioned battery unit and a bus bar connected to the adapter piece.
本实用新型第三方面提供一种电池模组,所述电池模组包括至少两个根据上述的电池单元以及连接于至少两个所述转接片的汇流排,所述汇流排卡接于所述卡扣内,相邻的两个所述电池单元中的一者的所述定位销插接至另一者的所述定位孔内。The third aspect of the utility model provides a battery module, the battery module includes at least two battery units according to the above and bus bars connected to at least two of the adapter pieces, the bus bars are clamped to the In the buckle, the positioning pin of one of the two adjacent battery units is plugged into the positioning hole of the other.
通过上述技术方案,本实用新型中,通过在散热板两端设置支架构成电池框架,结构简单可靠,符合批量化、自动化的生产要求;将电芯的极耳通过转接片安装于支架的安装槽内,提高了电池单元的装配效率。多个电池单元之间可通过汇流排进行串并联连接,无需在汇流排上切出极耳穿过的位置,过流截面较大,大大降低汇流排的厚度,从而降低模组的重量以及生产成本。并且该电池单元的生产工艺具备统一性,满足各家客户需求,产线兼容难度降低。Through the above technical solution, in the utility model, the battery frame is formed by setting brackets at both ends of the heat dissipation plate, the structure is simple and reliable, and meets the requirements of mass production and automation; In the groove, the assembly efficiency of the battery unit is improved. Multiple battery cells can be connected in series and parallel through the bus bar, without cutting out the position where the tabs pass through on the bus bar, the cross-section is large, and the thickness of the bus bar is greatly reduced, thereby reducing the weight of the module and production cost. Moreover, the production process of the battery unit is unified to meet the needs of various customers, and the difficulty of production line compatibility is reduced.
附图说明Description of drawings
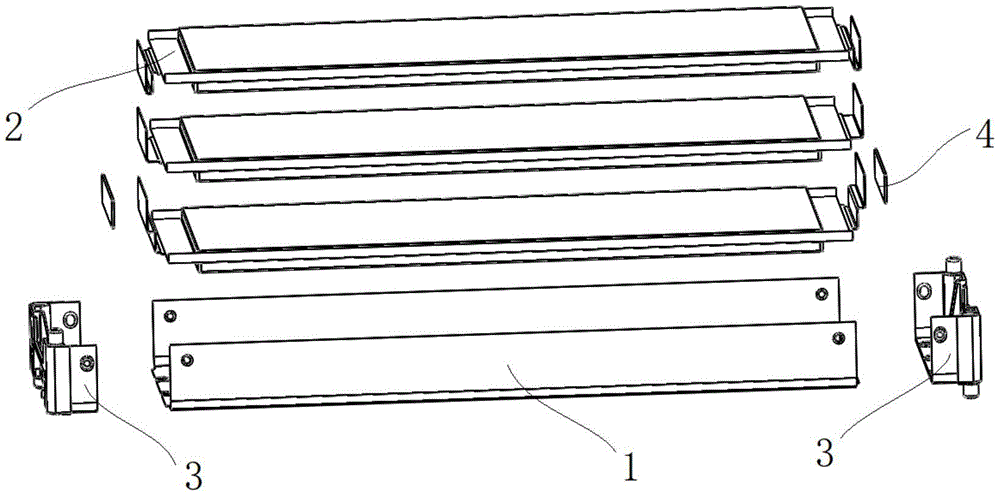
图1是本实用新型中电池单元的爆炸示意图;Fig. 1 is the explosion schematic diagram of battery cell in the utility model;
图2是本实用新型中电池单元的装配过程示意图;Fig. 2 is a schematic diagram of the assembly process of the battery unit in the utility model;
图3是图1和图2中支架的结构示意图;Fig. 3 is the structural representation of support in Fig. 1 and Fig. 2;
图4是图1和图2中散热板的结构示意图;Fig. 4 is a schematic structural view of the cooling plate in Fig. 1 and Fig. 2;
图5是本实用新型中散热板和支架装配后的示意图;Fig. 5 is the schematic diagram after assembling of radiator plate and support in the utility model;
图6是本实用新型中电池模组的结构示意图。Fig. 6 is a schematic structural view of the battery module in the present invention.
附图标记说明Explanation of reference signs
1-散热板;2-电芯;3-支架;31-安装槽;32-卡扣;33-第一侧壁;34-第一定位销;35-第一定位孔;37-第二定位销;39-热熔点;40-安装孔4-转接片;5-汇流排。1-radiating plate; 2-battery core; 3-bracket; 31-installation slot; 32-buckle; 33-first side wall; 34-first positioning pin; 35-first positioning hole; 37-second positioning Pin; 39-melting point; 40-installation hole 4-transfer piece; 5-bus.
具体实施方式detailed description
以下结合附图对本实用新型的具体实施方式进行详细说明。应当理解的是,此处所描述的具体实施方式仅用于说明和解释本实用新型,并不用于限制本实用新型。在本实用新型中,在未作相反说明的情况下,使用的方位词如“上、下、左、右”通常是指通常是指参照附图所示的方位,“内、外”是指相对于各部件本身轮廓的内、外。The specific embodiment of the utility model will be described in detail below in conjunction with the accompanying drawings. It should be understood that the specific embodiments described here are only used to illustrate and explain the utility model, and are not intended to limit the utility model. In the present utility model, unless otherwise stated, the used orientation words such as "up, down, left, right" usually refer to the orientation shown in the accompanying drawings, and "inside and outside" refer to Relative to the inside and outside of the contour of each part itself.
如图1和图2所示,本实用新型第一方面提供一种电池单元,该电池单元包括具有容纳腔的散热板1、位于所述容纳腔内的电芯2以及连接于所述散热板1两端的支架3,所述支架3上形成有安装槽31,所述电芯2的极耳上连接有转接片4,所述转接片4安装于所述安装槽31内。As shown in Figure 1 and Figure 2, the first aspect of the present invention provides a battery unit, the battery unit includes a
本实用新型中,通过在散热板1两端设置支架3构成如图5所示的电池框架,结构简单可靠,符合批量化、自动化的生产要求;将电芯2的极耳通过转接片4安装于支架3的安装槽31内,提高了电池单元的装配效率。并且多个电池单元之间可通过下述的汇流排5进行串并联连接,无需在汇流排5上切出极耳穿过的位置,过流截面较大,大大降低汇流排5的厚度,从而降低模组的重量以及生产成本。并且该电池单元的生产工艺具备统一性,满足各家客户需求,产线兼容难度降低。In the utility model, the battery frame shown in Fig. 5 is formed by setting
进一步地,如图3所示,所述支架3的背离所述容纳腔的一侧设置有卡扣32,并且/或者,所述支架3的沿所述电芯2的层叠方向的两端设有定位销和/或定位孔。可以理解的是,支架3上设置有上下对称的两个卡扣32。此外,支架3上下(该“上、下”参照图3所示的方位)颠倒地安装于散热板1的两侧,卡扣32用于在激光焊接下述的汇流排5时,起到固定汇流排5的作用,从而实现生产线的自动焊接。并且,支架3上设置有上下对称的两个安装槽31,转接片4可以同时插接于两个安装槽31内,也可以只插接于任意一个安装槽31内。转接片4安装于安装槽31内可以有效解决转接片4位置不固定,震动过程中撕扯极耳等问题。Further, as shown in FIG. 3 ,
更进一步地,所述支架3的沿所述电芯2的层叠方向的端部分别设置有所述定位销以及所述定位孔。优选地,所述支架3包括位于沿所述电芯2的层叠方向的两端的第一侧壁33和第二侧壁,所述第一侧壁33上设置有第一定位销34和第一定位孔35,所述第二侧壁上设有第二定位销37和第二定位孔;其中,所述第一定位销34与所述第二定位孔同轴,所述第二定位销37与所述第一定位孔35同轴。支架3上设置有对称的定位销与定位孔,可以满足两个动力电池之间的扣合安装,在软包电池成组过程中可以有效防止模组中间部分塌陷。在本实用新型的一种实施方式中,定位销上形成有通孔,可以在该通孔以及定位孔内穿设螺杆,进一步增加模组结构强度,提供多种模组固定方案。Furthermore, the positioning pins and the positioning holes are respectively provided at the ends of the
作为一种实施方式,所述支架3上设置有热熔点39,所述散热板1通过该热熔点39热熔连接至所述支架3。可以理解的是,支架3的上表面、下表面以及侧壁上分别设置有一个或多个热熔点39。并且,如图4所示,散热板1上形成有用于避让热熔点39的缺口。通过对热熔点39进行高温加热、融化使得支架3连接至散热板1的两端,组成如图5所示的电池框架。电池框架上可以集成电芯2的转接片4、汇流排5、低压采集固定点以及最外侧绝缘防护固定点等结构件。As an embodiment, the
此外,所述支架3可以为注塑件,并且/或者,所述支架3上设置有与外部零件连接的安装孔40。支架3上的特征,如安装槽31、定位销、定位孔、卡扣32、热熔点39、安装孔40等,均可以通过注塑的加工方式在支架3的制造过程中一体形成于支架3的本体上。其中,定位销也可以在支架3的注塑部分制作完成后,通过压入的方式安装于预留的孔中。安装孔40内可安装卡扣、塑料铆钉、扎带等零件,进一步固定模组所需的低压采集、外层保护盖等零件,极大的减少了模组零件种类和数量。In addition, the
进一步地,所述电池单元包括多个所述电芯2,多个所述电芯2的极耳通过预折弯而彼此贴合,并通过激光焊接连接至所述转接片4。在图1和图2所示的实施方式中,为三个电芯2并联。在其他实施方式中,也可以为单并、两并、四并等。将电芯2与转接片4焊接后的电芯单元整体放入电池框架内,将转接片4安装于安装槽31内。电芯2并联的时候可以通过极耳预折弯或者铝塑膜预折弯,完成电芯2极耳之间的贴合,转接片4可以为平板型式,也可为L型。Further, the battery unit includes a plurality of
本实用新型第二方面提供一种电池模组,所述电池模组包括上述的电池单元以及连接于所述转接片4的汇流排5。The second aspect of the present invention provides a battery module, which includes the above-mentioned battery unit and a
如图6所示,本实用新型第三方面提供一种电池模组,所述电池模组包括至少两个上述的电池单元以及连接于至少两个所述转接片4的汇流排5,所述汇流排5卡接于所述卡扣32内,相邻的两个所述电池单元中的一者的所述定位销插接至另一者的所述定位孔内。其中,如图6所示,相邻的两个电池单元为左右对称的结构。进一步地,本实用新型中,电芯2通过转接片4完成电芯极耳与汇流排5的焊接,使电芯极耳与汇流排5分别焊接位于转接片4的前后两侧,不需要汇流排5上切口,从而可以极大的减薄汇流排5的厚度。此外,转接片4可以为铜排或者铝排,汇流排5也可以为铜排或者铝排。可以理解的是,汇流排5连接于相邻的电池单元的相同极性的转接片4时,构成电池单元彼此并联的电池模块;汇流排5连接于相邻的电池单元的不同极性的转接片4时,构成电池单元彼此串联的电池模块。所述电池模组与上述电池单元相对于现有技术所具有的优势相同,在此不再赘述。As shown in Figure 6, the third aspect of the present invention provides a battery module, the battery module includes at least two of the above-mentioned battery cells and
以上结合附图详细描述了本实用新型的优选实施方式,但是,本实用新型并不限于此。在本实用新型的技术构思范围内,可以对本实用新型的技术方案进行多种简单变型,包括各个具体技术特征以任何合适的方式进行组合,为了避免不必要的重复,本实用新型对各种可能的组合方式不再另行说明。但这些简单变型和组合同样应当视为本实用新型所公开的内容,均属于本实用新型的保护范围。The preferred implementation of the present utility model has been described in detail above in conjunction with the accompanying drawings, however, the present utility model is not limited thereto. Within the scope of the technical concept of the present utility model, various simple modifications can be made to the technical solution of the present utility model, including the combination of each specific technical feature in any suitable manner. The combination method will not be explained separately. However, these simple modifications and combinations should also be regarded as the content disclosed by the utility model, and all belong to the protection scope of the utility model.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221696051.9U CN218274876U (en) | 2022-06-30 | 2022-06-30 | Battery unit and battery module |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221696051.9U CN218274876U (en) | 2022-06-30 | 2022-06-30 | Battery unit and battery module |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN218274876U true CN218274876U (en) | 2023-01-10 |
Family
ID=84760453
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202221696051.9U Active CN218274876U (en) | 2022-06-30 | 2022-06-30 | Battery unit and battery module |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN218274876U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116387761A (en) * | 2023-05-23 | 2023-07-04 | 中航锂电(洛阳)有限公司 | Conductive sheet, busbar bracket, busbar installation structure, battery module and battery |
| CN116387734A (en) * | 2023-05-23 | 2023-07-04 | 中航锂电(洛阳)有限公司 | Battery frame, battery unit, battery assembly, battery module and battery |
-
2022
- 2022-06-30 CN CN202221696051.9U patent/CN218274876U/en active Active
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116387761A (en) * | 2023-05-23 | 2023-07-04 | 中航锂电(洛阳)有限公司 | Conductive sheet, busbar bracket, busbar installation structure, battery module and battery |
| CN116387734A (en) * | 2023-05-23 | 2023-07-04 | 中航锂电(洛阳)有限公司 | Battery frame, battery unit, battery assembly, battery module and battery |
| CN116387734B (en) * | 2023-05-23 | 2025-09-23 | 中航锂电(洛阳)有限公司 | Battery frames, battery cells, battery assemblies, battery modules and batteries |
| CN116387761B (en) * | 2023-05-23 | 2026-02-06 | 中航锂电(洛阳)有限公司 | Busbar support, busbar mounting structure, battery module and battery |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111599955B (en) | A module-free aluminum shell battery module and aluminum shell battery | |
| CN110289379A (en) | A kind of soft-package battery mould group and its manufacturing method | |
| CN109904378B (en) | Lithium battery energy storage module and lithium battery energy storage module | |
| CN216793932U (en) | Busbar subassembly and battery module | |
| CN210576055U (en) | Laminate polymer battery module | |
| CN108155311A (en) | A kind of lithium-ion-power cell liquid chill group | |
| CN110233229A (en) | A kind of connection structure and battery modules of soft package battery module and busbar connector assembly | |
| CN211555995U (en) | A soft pack lithium battery assembly bracket | |
| CN207883786U (en) | A kind of power battery module and electric vehicle | |
| WO2024032641A1 (en) | Battery module and battery pack | |
| CN210805858U (en) | Large battery cell module unit integrally provided with water cooling plate and power battery pack thereof | |
| CN205452403U (en) | Laminate polymer battery module | |
| CN210576172U (en) | Busbar, electric core parallel structure, battery module and battery pack | |
| CN209447895U (en) | A kind of no mould group class aluminum-shell battery mould group | |
| CN209592169U (en) | A power battery soft pack module | |
| CN213583980U (en) | Battery cell module and battery box | |
| CN219393603U (en) | Battery module and battery pack | |
| CN208955068U (en) | Power battery module center and power battery module structure | |
| CN116014372B (en) | Power battery pack and integration method | |
| CN220138624U (en) | Busbar support and battery | |
| CN218677413U (en) | Spliced liquid-cooling energy storage device | |
| CN111490209A (en) | Laminate polymer battery module and new energy automobile | |
| CN218414944U (en) | CTP battery module | |
| CN116706411A (en) | Battery electrode output integrated part, battery module and battery pack | |
| CN213583935U (en) | A hybrid vehicle air-cooled battery module and battery pack |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address |
Address after: 108, 1st Floor, Building 4, No. 91 Pu'an Road, Doudian, Fangshan District, Beijing 102402 Patentee after: Beijing Weilan New Energy Technology Co.,Ltd. Country or region after: China Address before: No.1 Qihang West Street, Doudian Town, Fangshan District, Beijing Patentee before: BEIJING WELION NEW ENERGY TECHNOLOGY Co.,Ltd. Country or region before: China |
|
| CP03 | Change of name, title or address |