CN218225592U - Clamping mechanism simple in clamping - Google Patents
Clamping mechanism simple in clamping Download PDFInfo
- Publication number
- CN218225592U CN218225592U CN202222230458.9U CN202222230458U CN218225592U CN 218225592 U CN218225592 U CN 218225592U CN 202222230458 U CN202222230458 U CN 202222230458U CN 218225592 U CN218225592 U CN 218225592U
- Authority
- CN
- China
- Prior art keywords
- fixed
- clamping
- fixing
- positioning
- base
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Jigs For Machine Tools (AREA)
Abstract
本实用新型公开了一种装夹简单的装夹机构,包括底座组件和冶具组件,底座组件包括固定底座,冶具组件包括固定冶具,固定底座的顶部开设有第二螺孔,第二螺孔的内部设置有固定螺栓,固定冶具通过固定螺栓固定于固定底座的顶部,固定冶具的顶部两侧均开设有定位固定槽,定位固定槽的内侧设置有工件,装置采用卡接的的方式对工件进行定位,利用固定冶具上部的定位固定槽对工件进行卡接定位,在对较大工件进行固定时,相比已传统装夹机构装夹更加快速,可以方便工件的快速装夹,提高生产效率,而且固定位置仅位于工件的一侧,对加工的影响较小,不涉及到基准面相关尺寸,不会对刀具的加工造成影响,使材料得到最大的利用,可避免材料的浪费。
The utility model discloses a clamping mechanism with simple clamping, which comprises a base assembly and a jig assembly, the base assembly includes a fixed base, the jig assembly includes a fixed jig, the top of the fixed base is provided with a second screw hole, and the There are fixed bolts inside, and the fixed fixture is fixed on the top of the fixed base through the fixed bolts. There are positioning and fixing grooves on both sides of the top of the fixing fixture, and the inner side of the positioning and fixing groove is provided with workpieces. Positioning, use the positioning and fixing groove on the upper part of the fixed fixture to clamp and position the workpiece. When fixing a larger workpiece, it is faster than the traditional clamping mechanism, which can facilitate the rapid clamping of the workpiece and improve production efficiency. Moreover, the fixed position is only located on one side of the workpiece, which has little impact on the processing, does not involve the relevant dimensions of the reference plane, and will not affect the processing of the tool, so that the material can be used to the maximum and the waste of material can be avoided.
Description
技术领域technical field
本实用新型涉及装夹机构技术领域,具体为一种装夹简单的装夹机构。The utility model relates to the technical field of clamping mechanisms, in particular to a clamping mechanism with simple clamping.
背景技术Background technique
随着经济的发展,生产设备的自动化程度越来越高,数控切割机被广泛的应用于机械行业当中,数控切割机切割精度的不断提高,在机械零部件的加工过程中,如果要对零件进行其他的加工操作,需要配合装夹机构,在数控对工件进行加工时,需要装夹机构对工件进行装夹定位以方便加工,但在装夹时,由于部分零件的尺寸过大,不适合留夹持位进行装夹,装夹十分困难,如用常规的装夹机构进行装夹,由于装夹部位涉及到基准面相关尺寸,由于装夹会妨碍刀具的加工,会造成材料的浪费,现有的装夹机构无法满足此类工件的装夹固定。With the development of the economy, the degree of automation of production equipment is getting higher and higher. CNC cutting machines are widely used in the machinery industry. The cutting accuracy of CNC cutting machines continues to improve. For other processing operations, it is necessary to cooperate with the clamping mechanism. When the workpiece is processed by CNC, the clamping mechanism is required to clamp and position the workpiece to facilitate processing. However, due to the excessive size of some parts during clamping, it is not suitable for It is very difficult to hold the clamping position for clamping. If the conventional clamping mechanism is used for clamping, since the clamping position involves the relative size of the reference plane, the clamping will hinder the processing of the tool and cause waste of materials. The existing clamping mechanism cannot satisfy the clamping and fixing of such workpieces.
实用新型内容Utility model content
本实用新型的目的在于提供一种装夹简单的装夹机构,以解决上述背景技术中提出的问题。The purpose of this utility model is to provide a clamping mechanism with simple clamping, so as to solve the problems raised in the above-mentioned background technology.
为实现上述目的,本实用新型提供如下技术方案:一种装夹简单的装夹机构,包括底座组件和冶具组件,所述冶具组件设置于底座组件的顶部,所述底座组件包括固定底座,所述冶具组件包括固定冶具,所述固定冶具设置于固定底座的顶部;In order to achieve the above purpose, the utility model provides the following technical solutions: a clamping mechanism with simple clamping, including a base assembly and a jig assembly, the jig assembly is arranged on the top of the base assembly, the base assembly includes a fixed base, the The jig assembly includes a fixed jig, and the fixed jig is arranged on the top of the fixed base;
所述固定底座的顶部对称开设有数量为四个的第二螺孔,所述第二螺孔的内部设置有固定螺栓,所述固定螺栓螺纹连接于第二螺孔的内部,所述固定冶具的上部开设有与第二螺孔相适配的第五螺孔,所述固定冶具通过固定螺栓固定于固定底座的顶部,所述固定冶具的顶部两侧均开设有定位固定槽,所述定位固定槽的内侧设置有工件。The top of the fixed base is symmetrically provided with four second screw holes, the inside of the second screw holes is provided with fixing bolts, and the fixing bolts are threadedly connected to the inside of the second screw holes, and the fixing fixture The upper part of the upper part is provided with a fifth screw hole matching the second screw hole. The fixed jig is fixed on the top of the fixed base by fixing bolts. Both sides of the top of the fixed jig are provided with positioning and fixing grooves. The positioning and fixing grooves The inner side of is provided with a workpiece.
作为优选,上述定位固定槽的一侧对称开设有卡接槽孔,所述卡接槽孔的数量为两个,所述固定底座的顶部对称开设有数量为四个的第一螺孔。Preferably, one side of the positioning and fixing groove is symmetrically provided with snapping slots, and the number of the snapping slots is two, and the top of the fixing base is symmetrically provided with four first screw holes.
作为优选,上述所述固定底座的顶部开设有第一定位孔,所述第一定位孔的内部插入有定位销柱,所述固定冶具的底部开设有与定位销柱相适配的第二定位孔,所述定位销柱插入于第二定位孔的内部。As a preference, a first positioning hole is opened on the top of the above-mentioned fixed base, and a positioning pin is inserted into the inside of the first positioning hole, and a second positioning pin adapted to the positioning pin is opened on the bottom of the fixed fixture. The positioning pin is inserted into the second positioning hole.
作为优选,上述工件的底部设置有底部固定台,所述底部固定台的形状与定位固定槽相适配,所述底部固定台设置于定位固定槽的内侧。Preferably, the bottom of the workpiece is provided with a bottom fixing platform, the shape of the bottom fixing platform is adapted to the positioning and fixing groove, and the bottom fixing platform is arranged inside the positioning and fixing groove.
作为优选,上述底部固定台的底部两侧对称开设有第三螺孔,所述定位固定槽的内侧开设有与第三螺孔位置相对应的第四螺孔,所述第四螺孔内设置有紧固螺栓,所述紧固螺栓螺纹连接于第四螺孔的内侧,所述工件通过紧固螺栓固定于定位固定槽的内侧。As a preference, third screw holes are provided symmetrically on both sides of the bottom of the above-mentioned bottom fixing platform, and a fourth screw hole corresponding to the position of the third screw hole is opened on the inner side of the positioning and fixing groove, and a fourth screw hole is provided in the fourth screw hole. There are fastening bolts, and the fastening bolts are screwed to the inner side of the fourth screw hole, and the workpiece is fixed on the inner side of the positioning and fixing groove by the fastening bolts.
作为优选,上述底部固定台的中部开设有两个底部通孔,所述底部固定台的顶部设置有顶部凸台,所述顶部凸台的顶部开设有数量为两个的顶部通孔。Preferably, two bottom through holes are opened in the middle of the bottom fixing platform, and a top boss is provided on the top of the bottom fixing platform, and two top through holes are opened on the top of the top boss.
与现有技术相比,本实用新型的有益效果是:Compared with the prior art, the beneficial effects of the utility model are:
本装置采用卡接的的方式对工件进行定位,利用固定冶具上部的定位固定槽对工件进行卡接定位,并通过螺栓配合工件底部的螺孔对工件进行固定,在对较大工件进行固定时,相比已传统装夹机构装夹更加快速,可以方便工件的快速装夹,提高生产效率,而且固定位置仅位于工件的一侧,对加工的影响较小,不涉及到基准面相关尺寸,不会对刀具的加工造成影响,使材料得到最大的利用,可避免材料的浪费。This device adopts the clamping method to locate the workpiece, and uses the positioning and fixing groove on the upper part of the fixing tool to clamp and position the workpiece, and fixes the workpiece through the bolts matching the screw holes at the bottom of the workpiece. When fixing a larger workpiece Compared with the traditional clamping mechanism, the clamping is faster, which can facilitate the rapid clamping of the workpiece and improve the production efficiency, and the fixed position is only located on one side of the workpiece, which has little impact on the processing and does not involve the relevant dimensions of the reference plane. It will not affect the processing of the tool, so that the material can be used to the maximum and the waste of material can be avoided.
附图说明Description of drawings
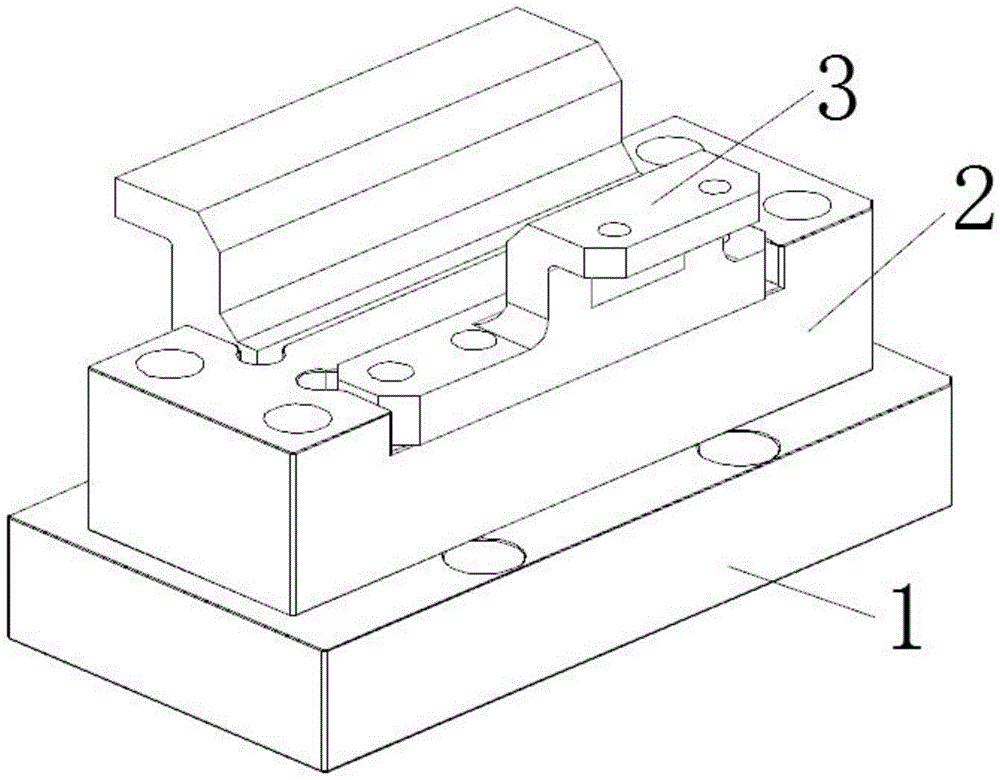
图1为本实用新型的整体立体结构示意图;Fig. 1 is the overall three-dimensional structure schematic diagram of the present utility model;
图2为本实用新型的底座组件结构示意图;Fig. 2 is a structural schematic diagram of the base assembly of the present invention;
图3为本实用新型的固定底座上部结构示意图;Fig. 3 is a schematic diagram of the upper structure of the fixed base of the utility model;
图4为本实用新型的冶具组件结构示意图;Fig. 4 is a structural schematic diagram of the tool assembly of the present utility model;
图5为本实用新型的固定冶具下侧结构示意图;Fig. 5 is a schematic diagram of the structure of the lower side of the fixed fixture of the present invention;
图6为本实用新型的工件加工前的结构示意图;Fig. 6 is the structural representation before the workpiece processing of the present utility model;
图7为本实用新型的工件加工后的结构示意图。Fig. 7 is a schematic structural view of the processed workpiece of the present invention.
图中:1、底座组件;2、冶具组件;3、工件;4、固定底座;5、第一螺孔;6、第二螺孔;7、第一定位孔;8、底部固定台;9、顶部凸台;10、底部通孔;11、第三螺孔;12、顶部通孔;13、固定冶具;14、定位固定槽;15、卡接槽孔;16、第四螺孔;17、第五螺孔;18、第二定位孔;19、固定螺栓;20、定位销柱。In the figure: 1. Base assembly; 2. Jig assembly; 3. Work piece; 4. Fixed base; 5. First screw hole; 6. Second screw hole; 7. First positioning hole; 8. Bottom fixed platform; 9 1. Top boss; 10. Bottom through hole; 11. Third screw hole; 12. Top through hole; 13. Fixing tool; 14. Positioning and fixing groove; 15. Clamping slot; 16. Fourth screw hole; , the fifth screw hole; 18, the second positioning hole; 19, the fixing bolt; 20, the positioning pin.
具体实施方式detailed description
下面将结合本实用新型实施例中的附图,对本实用新型实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本实用新型一部分实施例,而不是全部的实施例。基于本实用新型中的实施例,本领域普通技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本实用新型保护的范围。The technical solutions in the embodiments of the present invention will be clearly and completely described below in conjunction with the accompanying drawings in the embodiments of the present invention. Obviously, the described embodiments are only part of the embodiments of the present invention, not all of them. example. Based on the embodiments of the present utility model, all other embodiments obtained by persons of ordinary skill in the art without making creative efforts belong to the scope of protection of the present utility model.
实施例Example
请参阅图1-7,本实用新型提供一种技术方案:一种装夹简单的装夹机构,包括底座组件1和冶具组件2,固定底座4的顶部对称开设有数量为四个的第一螺孔5,通过第一螺孔5利用螺栓可将固定底座4,固定于机床中的加工平台的上部,实现对工件3的基准定位,冶具组件2设置于底座组件1的顶部,用于对工件3进行定位固定,底座组件1包括固定底座4,冶具组件2包括固定冶具13,固定底座4的顶部对称开设有数量为四个的第二螺孔6,第二螺孔6的内部设置有固定螺栓19,固定螺栓19螺纹连接于第二螺孔6的内部,固定冶具13的上部开设有与第二螺孔6相适配的第五螺孔17,固定冶具13通过固定螺栓19固定于固定底座4的顶部,采用螺栓连接可方便拆卸,固定冶具13的顶部两侧均开设有定位固定槽14,定位固定槽14的内侧设置有工件3,定位固定槽14的形状根据工件3的尺寸进行定制,在加工时可根据工件3的不同规格更换对应的冶具组件2,冶具组件2均可与固定底座4配合固定,适用于批量化的零件加工,定位固定槽14的一侧对称开设有卡接槽孔15,卡接槽孔15的数量为两个,卡接槽孔15可帮助对工件3进行卡接定位,同时还可为工件3的加工提供刀具运转的加工空间,利于工件3的加工。Please refer to Figures 1-7, the utility model provides a technical solution: a clamping mechanism with simple clamping, including a
固定底座4的顶部开设有第一定位孔7,第一定位孔7的内部插入有定位销柱20,固定冶具13的底部开设有与定位销柱20相适配的第二定位孔18,定位销柱20插入于第二定位孔18的内部,通过第一定位孔7、第二定位孔18与定位销柱20间的插入卡接,将固定冶具13精准安放于固定底座4的上部,工件3的底部设置有底部固定台8,底部固定台8的中部开设有两个底部通孔10,底部固定台8的顶部设置有顶部凸台9,顶部凸台9的顶部开设有数量为两个的顶部通孔12,底部固定台8的形状与定位固定槽14相适配,可便于工件3的精准定位与安装,底部固定台8的底部两侧对称开设有第三螺孔11,定位固定槽14的内侧开设有与第三螺孔11位置相对应的第四螺孔16,第四螺孔16内设置有紧固螺栓,紧固螺栓螺纹连接于第四螺孔16的内侧,工件3通过紧固螺栓固定于定位固定槽14的内侧,采用卡接的的方式对工件3进行定位安装,在对较大工件3进行固定时,相比已传统装夹机构装夹更加快速,而且固定位置仅位于工件3的一侧,对加工的影响较小,不涉及到基准面相关尺寸,不会对刀具的加工造成影响,使材料得到最大的利用,可避免材料的浪费。The top of the fixed
工作原理或者结构原理,使用时,通过固定底座4上部开设的第一螺孔5,利用螺栓将固定底座4固定于机床的加工平台的上部,通过第一定位孔7、第二定位孔18与定位销柱20间的插入卡接,将固定冶具13精准安放于固定底座4的上部,并通过固定螺栓19对固定冶具13进行固定,使固定冶具13被牢牢固定于固定底座4的上部,固定完成后,利用工件3底部设置的底部固定台8,通过底部固定台8与定位固定槽14间的形状配合,实现对工件3的卡接定位,并通过紧固螺栓将工件3固定于定位固定槽14的内侧,完成工件3的安装作业,相比已传统装夹机构装夹更加快速,可以方便工件3的快速装夹,提高生产效率,而且固定位置仅位于工件3的一侧,对加工的影响较小,不涉及到基准面相关尺寸,不会对刀具的加工造成影响,使材料得到最大的利用,可避免材料的浪费,其中定位固定槽14的形状根据工件3的尺寸进行定制,在加工时可根据工件3的不同规格更换对应的冶具组件2,冶具组件2均可与固定底座4配合固定,适用于批量化的零件加工。Working principle or structural principle, when in use, through the
尽管已经示出和描述了本实用新型的实施例,对于本领域的普通技术人员而言,可以理解在不脱离本实用新型的原理和精神的情况下可以对这些实施例进行多种变化、修改、替换和变型,本实用新型的范围由所附权利要求及其等同物限定。Although the embodiments of the present invention have been shown and described, those skilled in the art can understand that various changes and modifications can be made to these embodiments without departing from the principle and spirit of the present invention , replacements and modifications, the scope of the present utility model is defined by the appended claims and their equivalents.
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222230458.9U CN218225592U (en) | 2022-08-24 | 2022-08-24 | Clamping mechanism simple in clamping |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202222230458.9U CN218225592U (en) | 2022-08-24 | 2022-08-24 | Clamping mechanism simple in clamping |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN218225592U true CN218225592U (en) | 2023-01-06 |
Family
ID=84684520
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202222230458.9U Expired - Fee Related CN218225592U (en) | 2022-08-24 | 2022-08-24 | Clamping mechanism simple in clamping |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN218225592U (en) |
-
2022
- 2022-08-24 CN CN202222230458.9U patent/CN218225592U/en not_active Expired - Fee Related
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201143628Y (en) | An adjustable fixture for wire cutting | |
| CN112775686A (en) | Positioning device suitable for automatic lathe turning of inclined plane workpiece | |
| CN215316909U (en) | Special drilling and tapping machine for milling end face | |
| CN207746774U (en) | The universal fixturing in square shaped workpiece car hole | |
| CN219684626U (en) | Frock clamp that triaxial machining center processing inclined plane was used | |
| CN210147075U (en) | Universal adjustable drill clamp | |
| CN214264705U (en) | Positioning equipment suitable for automatic lathe turning of inclined plane work piece | |
| CN210967348U (en) | A frock clamp for high accuracy inner key groove line cutting process | |
| CN204122872U (en) | A kind of electrode holder assembly | |
| CN220533031U (en) | Frock clamp in counter sinking hole in dysmorphism part processing inclined plane | |
| CN209754590U (en) | multi-process composite milling clamp for bearing seat part | |
| CN114536036A (en) | Novel clamp for machining parts of precision machine tool | |
| CN217224547U (en) | Machining size positioning device on common lathe | |
| CN223300906U (en) | Clamp for horizontal clamping of numerical control lathe for machining round bars | |
| CN223544709U (en) | A rotatable, variable-position motor flange end cap processing device | |
| CN215393814U (en) | High-precision locking clamp | |
| CN213497772U (en) | Clamping jig with movable guide rod for cylindrical workpiece | |
| CN219379914U (en) | Magnetic type positioning and processing jig | |
| CN219704233U (en) | Double-station blade seat milling groove tool | |
| CN223455545U (en) | Special fixture for irregular part drilling and boring | |
| CN223325936U (en) | Flexible quick adjustment tray anchor clamps | |
| CN211991923U (en) | Clamp for finish machining of appearance of large body | |
| CN223210899U (en) | Anti-vibration fixture tool for numerical control machine tool | |
| CN203371078U (en) | Universal clamp for machining inclined hole | |
| CN222493149U (en) | Clamp mechanism of milling machine workbench |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20230106 |