CN217831810U - Casting system runner structure is used in production of thin wall structure spare - Google Patents
Casting system runner structure is used in production of thin wall structure spare Download PDFInfo
- Publication number
- CN217831810U CN217831810U CN202221960181.9U CN202221960181U CN217831810U CN 217831810 U CN217831810 U CN 217831810U CN 202221960181 U CN202221960181 U CN 202221960181U CN 217831810 U CN217831810 U CN 217831810U
- Authority
- CN
- China
- Prior art keywords
- branch
- gate
- cross
- pouring
- runner
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000005266 casting Methods 0.000 title claims abstract description 26
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 8
- 239000000463 material Substances 0.000 claims abstract description 24
- 229910052782 aluminium Inorganic materials 0.000 abstract description 11
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 abstract description 11
- 239000007788 liquid Substances 0.000 abstract description 8
- 239000004411 aluminium Substances 0.000 abstract description 6
- 230000003139 buffering effect Effects 0.000 abstract description 2
- 238000007493 shaping process Methods 0.000 abstract description 2
- 238000004512 die casting Methods 0.000 description 8
- 229910000838 Al alloy Inorganic materials 0.000 description 6
- 239000002893 slag Substances 0.000 description 4
- 230000007547 defect Effects 0.000 description 3
- 239000007789 gas Substances 0.000 description 3
- 239000012535 impurity Substances 0.000 description 3
- 239000002912 waste gas Substances 0.000 description 3
- 230000008901 benefit Effects 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 239000011148 porous material Substances 0.000 description 2
- 241000510097 Megalonaias nervosa Species 0.000 description 1
- 229910002065 alloy metal Inorganic materials 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 239000003818 cinder Substances 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 230000006872 improvement Effects 0.000 description 1
- 238000002844 melting Methods 0.000 description 1
- 230000008018 melting Effects 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 239000000203 mixture Substances 0.000 description 1
- 230000003014 reinforcing effect Effects 0.000 description 1
- 239000013049 sediment Substances 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
Images

Landscapes
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
Abstract
The utility model discloses a casting system flow channel structure for producing thin-wall structural members, wherein a material handle is arranged above a main flow channel, and the main flow channel is communicated with the material handle; a main runner straight gate and a cross gate; the cross pouring gate comprises a main pouring gate connected with the straight pouring gate, and two reverse branch pouring gates are arranged at one end of the main pouring gate, which is far away from the straight pouring gate; the two branch pouring channels are sequentially provided with a first branch, a second branch and a third branch; one end of each of the first branch, the second branch and the third branch, which is far away from the corresponding branch pouring gate, is provided with a first inner gate, a second inner gate and a third inner gate respectively. The utility model discloses a casting system runner structure for thin-walled structure spare production controls the flow direction of aluminium liquid in the cross gate, lets aluminium liquid fill the whole cross gate before, and then gets into the shaping of mould cavity, and aluminium liquid front end residue can be discharged into the inside of buffering package overflow launder; the ratio of the cross section areas of the inlet and the outlet of the cross gate is set between 1 and 1.5, so that the danger of pressure relief is prevented.
Description
Technical Field
The utility model relates to an alloy metal die-casting technical field especially relates to a casting system runner structure is used in production of thin wall structure spare.
Background
The aluminum alloy is cast under high pressure, and if the die expands in the die-casting production process, the product has flash; meanwhile, the tail end of the product and the thicker lug boss, reinforcing rib and the like of the product can generate internal quality defects of the product, such as air holes, shrinkage holes, pin holes, looseness and the like; the flash comes from the expansion die, and the mold clamping force of the expansion die is insufficient or the pressure of the molten aluminum is too large in the die to be normally and smoothly circulated. The casting system design of the casting ensures that the internal metal pressure of the product is uniform, and the internal metal interface pressure is mostly 50-60N/mm 2 Qualified parts can be produced by die casting; in the traditional horizontal pouring gate design, a part of cold charge is pushed and mixed due to unsmooth flow sequence of aluminum alloy, and the like, so that a plurality of part of curling gas is generated in the horizontal pouring gate at a low speed; gas residue in the product is caused due to unsmooth exhaust and slag discharge, and the product has more internal pores, impurities and looseness; finally causing surface pore defects and the like after the product is processed. The traditional cross pouring channel has pressure relief danger because the proportion of the cross section area of each inlet and outlet is unreasonable.
SUMMERY OF THE UTILITY MODEL
In view of the above-mentioned shortcomings or drawbacks of the prior art, it is desirable to provide a runner structure of a casting system for producing thin-walled structural members.
The utility model provides a casting system runner structure for producing thin-wall structural parts, which comprises a material handle and a main runner; wherein,
the material handle is arranged above the main flow channel, and the main flow channel is communicated with the material handle;
the main runner comprises a longitudinal sprue connected with the material handle, and a transverse sprue is arranged at one end of the sprue, which is far away from the material handle; the cross pouring gate comprises a main pouring gate connected with the straight pouring gate, two reverse branch pouring gates are arranged at one end of the main pouring gate, which is far away from the straight pouring gate, and the two branch pouring gates and the main pouring gate are arranged in a Y shape; the two branch pouring channels are sequentially provided with a first branch, a second branch and a third branch; and one ends of the first branch, the second branch and the third branch, which are far away from the corresponding branch pouring gates, are respectively provided with a first inner gate, a second inner gate and a third inner gate.
Preferably, the thickness of the main pouring channel is larger than the thickness of the two branch pouring channels, and the two branch pouring channels are arranged on the upper side of one end, far away from the straight pouring channel, of the main pouring channel.
Preferably, the tail end of the branch pouring channel is provided with a buffer ladle overflow groove.
Preferably, the cross-sectional area ratio of the inlet to the outlet of each branch of the runner is set to 1 to 1.5.
Preferably, the cross-sectional areas of the inlet and outlet of the first ingate are 137mm respectively 2 And 198mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the second inner gate are 196mm respectively 2 And 288mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the third inner gate are 71mm respectively 2 And 98.7mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the branch pouring channel close to the first branch are respectively 250mm 2 And 198mm 2 The cross-sectional areas of the inlet and outlet of the branch gate close to the third branch are 478mm 2 And 408mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the third branch are respectively 120mm 2 And 98.7mm 2 。
Preferably, the inlet cross-sectional area of the main pouring channel is 1561mm 2 The cross-sectional area of the outlet is 728mm 2 。
Compared with the prior art, the beneficial effects of the utility model are that:
the utility model discloses a casting system runner structure is used in production of thin wall structure spare, the flow direction of control aluminium liquid in the cross gate, let aluminium liquid fill up whole cross gate earlier through two branch runners and first reposition of redundant personnel branches, second reposition of redundant personnel branch and third reposition of redundant personnel branch, then get into the shaping of mould die cavity, aluminium liquid front end residue can discharge the inside of buffering package overflow launder, can guarantee that waste gas is smooth to be discharged to the end of exhaust passage along the exhaust passage direction, extrude the inside of collection cinder ladle with cold burden or impurity is smooth simultaneously, solve the row's of exhaust sediment unsmooth, thereby lead to the inside gaseous residue of product, the inside gas pocket of product, mix with, loose more and finally cause the problem of product processing back surface hole defect; the ratio of the cross-sectional areas of the inlet and outlet of each branch of the cross gate is set between 1-1.5, so as to prevent the danger of pressure relief.
It should be understood that what is described in this summary section is not intended to limit key or critical features of embodiments of the invention, nor is it intended to limit the scope of the invention.
Other features of the present invention will become apparent from the following description.
Drawings
Other features, objects and advantages of the invention will become more apparent upon reading of the detailed description of non-limiting embodiments made with reference to the following drawings:
fig. 1 is a schematic structural diagram illustrating an application of a casting system runner structure for producing a thin-wall structural member according to an embodiment of the present invention;
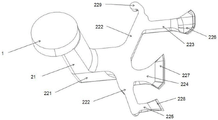
FIG. 2 is a schematic top view of a runner structure of the casting system;
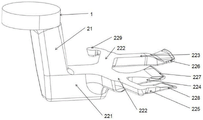
FIG. 3 is a schematic structural view in elevation of a runner structure of the casting system;
reference numbers in the figures: 1. a material handle; 2. a main flow channel; 21. a straight pouring channel; 22. a horizontal runner; 221. a main runner; 222. dividing a pouring channel; 223. a first branch; 224. a second branch; 225. a third branch; 226. a first inner gate; 227. a second ingate; 228. a third ingate; 229. a buffer bag overflow groove; 3. a product body; 4. an exhaust groove; 5. collecting a slag ladle; 6. and (4) an exhaust passage.
Detailed Description
The present invention will be described in further detail with reference to the accompanying drawings and examples. It is to be understood that the specific embodiments described herein are merely illustrative of the relevant invention and are not limiting of the invention. It should be noted that, for convenience of description, only the portions related to the present invention are shown in the drawings.
It should be noted that, in the present invention, the embodiments and features of the embodiments may be combined with each other without conflict. The present invention will be described in detail below with reference to the accompanying drawings in conjunction with embodiments.
Referring to fig. 1 to 3, an embodiment of the present invention provides a runner structure of a casting system for producing a thin-wall structural member, including a material handle 1 and a main runner 2; wherein,
the material handle 1 is arranged above the main runner 2, and the main runner 2 is communicated with the material handle 1;
the main runner 2 comprises a longitudinal sprue 21 connected with the material handle 1, and a transverse runner 22 is arranged at one end, away from the material handle 1, of the sprue 21; the horizontal pouring channel 22 comprises a main pouring channel 221 connected with the straight pouring channel 21, one end of the main pouring channel 221, far away from the straight pouring channel 21, is provided with two reverse branch pouring channels 222, and the two branch pouring channels 222 and the main pouring channel 221 are arranged in a Y shape; the two branch runners 222 are sequentially provided with a first branch 223, a second branch 224 and a third branch 225; the first branch 223, the second branch 224 and the third branch 225 are respectively provided with a first inner gate 226, a second inner gate 227 and a third inner gate 228 at the end far away from the corresponding branch gate 222.
In a preferred embodiment, the main runner 221 has a thickness greater than the thickness of the two sub-runners 222, and the two sub-runners 222 are disposed on an upper side of the end of the main runner 221 remote from the sprue 21.
In a preferred embodiment, the end of the branch gate 222 is provided with a buffer pack overflow slot 229.
In a preferred embodiment, the ratio of the inlet and outlet cross-sectional areas of the branches of the runner is set between 1 and 1.5, including the ratio of the inlet and outlet cross-sectional areas of the first ingate 226, the second ingate 227, the third ingate 228, the two branch runners 222 and the third branch 225.
In a preferred embodiment, the inlet and outlet cross-sectional areas of the first in-gate 226 are 137mm, respectively 2 And 198mm 2 (ii) a The second in-gate 227 is advancedThe cross-sectional area of the outlet is 196mm respectively 2 And 288mm 2 (ii) a The inlet and outlet cross-sectional areas of the third ingate 228 are 71mm each 2 And 98.7mm 2 (ii) a The inlet and outlet cross-sectional areas of the branch gate 222 adjacent to the first branch 223 are 250mm 2 And 198mm 2 The inlet and outlet cross-sectional areas of the branch gate 222 adjacent to the third branch 225 are 478mm 2 And 408mm 2 (ii) a The cross-sectional areas of the inlet and outlet of the third branch 225 are 120mm 2 And 98.7mm 2 。
The utility model relates to a casting system cross runner of bearing board aluminum alloy high pressure die casting in battery, this casting system has used the emerging "EN1706AC43500 trade mark aluminum alloy" material in new energy automobile field, can open up new way for the domestic new energy automobile field wide application in later stage; the bearing plate in the battery is made of aluminum alloy high-pressure die castings, the life cycle of ten years is 124 ten thousand pieces of aluminum alloy high-pressure die castings are planned to be needed every year, the value of each piece is about 90 yuan, and 1.1 million yuan of economic benefit can be generated; the temperature of the aluminum liquid is controlled to be 680 +/-10 ℃ during die casting production, and the internal aluminum liquid interface filling pressure designed by a product casting system is 55-60N/mm 2 And qualified products can be produced. The cross section area analysis is carried out according to the product performance, the cross section area of the inlet and the outlet of the cross runner is set to be 1-1.5 times, and the pressure relief danger is prevented.
Wherein, the ratio of the inlet and outlet cross-sectional areas of the first inner gate 226 is 198/137=1.45;
the ratio of the inlet and outlet cross-sectional areas of the second in-gate 227 is 288/196=1.47;
the ratio of the inlet and outlet cross-sectional areas of the third in-gate 228 is 98.7/71=1.39;
the ratio of the inlet and outlet cross-sectional areas of the branch gate 222 near the first branch 223 is 250/198=1.26;
the ratio of the inlet and outlet cross-sectional areas of the branch gate 222 close to the third branch 225 is 478/408=1.17
The ratio of the inlet and outlet cross-sectional areas of the third branch 225 is 120/98.7=1.22;
the ratio of the cross-sectional areas of the inlet and outlet of main runner 221 is 1561/(250 + 478) =2.14;
wherein the cross-sectional area of the inlet of the main runner 221 is 1561mm 2 The cross section area of the outlet is 478+250mm 2 Because the shape of the product is limited and inconvenient to change, the ratio of the cross section areas of the inlet and the outlet is more than 2 times, and as long as the ratio is close to 2, the design of the cross gate has good pressure relief and qualified product quality.
The utility model discloses an applied principle: the method comprises the steps that a punch of a die casting machine pushes molten aluminum to penetrate through a melting cup on a die, a sprue spreader on the die is contacted firstly, a material handle 1 is formed on the sprue spreader firstly, then the molten aluminum gradually enters a die cavity along a sprue 21 and a runner 22, a product body 3 is formed in the die cavity, waste gas enters a slag collecting bag 5 through an exhaust duct 4 according to the whole casting system, then enters an exhaust duct 6, the waste gas is discharged from a washboard type vacuum valve at the tail end of the exhaust duct 6, waste materials such as cold material impurities and the like are contained in the slag collecting bag 5, the whole casting system is formed instantly, then a movable die part is withdrawn, a movable die and a fixed die are separated, the casting system stays on one side of a movable die, a robot arm clamps the material handle from one side of the movable die, the whole casting system is taken down, then subsequent processing is carried out, and finished parts are finally manufactured in one step.
In the description of the present specification, the terms "connect", "mount", "fix", and the like are to be understood in a broad sense, for example, "connect" may be a fixed connection, a detachable connection, or an integral connection; may be directly connected or indirectly connected through an intermediate. The specific meaning of the above terms in the present application can be understood by those of ordinary skill in the art as appropriate.
In the description of the present application, the description of the terms "one embodiment," "some embodiments," or the like, means that a particular feature, structure, material, or characteristic described in connection with the embodiment or example is included in at least one embodiment or example of the application. In this specification, the schematic representations of the terms used above do not necessarily refer to the same embodiment or example. Furthermore, the particular features, structures, materials, or characteristics described may be combined in any suitable manner in any one or more embodiments or examples.
The above description is only a preferred embodiment of the present application and is not intended to limit the present application, and various modifications and changes may be made to the present application by those skilled in the art. Any modification, equivalent replacement, improvement and the like made within the spirit and principle of the present application shall be included in the protection scope of the present application.
Claims (6)
1. A casting system runner structure for producing a thin-wall structural member is characterized by comprising a material handle and a main runner; wherein,
the material handle is arranged above the main runner, and the main runner is communicated with the material handle;
the main runner comprises a longitudinal sprue connected with the material handle, and a transverse sprue is arranged at one end of the sprue, which is far away from the material handle; the cross pouring gate comprises a main pouring gate connected with the straight pouring gate, two reverse branch pouring gates are arranged at one end of the main pouring gate, which is far away from the straight pouring gate, and the two branch pouring gates and the main pouring gate are arranged in a Y shape; the two branch pouring channels are sequentially provided with a first branch, a second branch and a third branch; and one ends of the first branch, the second branch and the third branch, which are far away from the corresponding branch pouring gates, are respectively provided with a first inner gate, a second inner gate and a third inner gate.
2. The casting system runner structure for producing thin-walled structural members according to claim 1, wherein the main runner has a thickness greater than that of the two branch runners provided on an upper side of an end of the main runner remote from the sprue.
3. The casting system flow channel structure for producing the thin-walled structural member as claimed in claim 2, wherein the end of the branch runner is provided with a buffer ladle overflow groove.
4. The gating system channel structure for the production of thin-walled structural members as claimed in claim 3, wherein the ratio of the cross-sectional areas of the inlet and outlet of each branch of the runner is set to 1 to 1.5.
5. The casting system flow channel structure for producing thin-walled structural members as claimed in claim 4, wherein the first in-gate has an inlet cross-sectional area and an outlet cross-sectional area of 137mm, respectively 2 And 198mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the second inner gate are 196mm respectively 2 And 288mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the third inner sprue are 71mm respectively 2 And 98.7mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the branch pouring channel close to the first branch are respectively 250mm 2 And 198mm 2 The cross-sectional areas of the inlet and outlet of the branch gate close to the third branch are 478mm 2 And 408mm 2 (ii) a The cross-sectional areas of the inlet and the outlet of the third branch are respectively 120mm 2 And 98.7mm 2 。
6. The runner structure of a casting system for producing a thin-walled structural member as claimed in claim 5, wherein the main runner has an inlet cross-sectional area of 1561mm 2 The cross-sectional area of the outlet is 728mm 2 。
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221960181.9U CN217831810U (en) | 2022-07-28 | 2022-07-28 | Casting system runner structure is used in production of thin wall structure spare |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221960181.9U CN217831810U (en) | 2022-07-28 | 2022-07-28 | Casting system runner structure is used in production of thin wall structure spare |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN217831810U true CN217831810U (en) | 2022-11-18 |
Family
ID=84039701
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202221960181.9U Active CN217831810U (en) | 2022-07-28 | 2022-07-28 | Casting system runner structure is used in production of thin wall structure spare |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN217831810U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116851704A (en) * | 2023-07-27 | 2023-10-10 | 重庆东科模具制造有限公司 | A box pouring structure and its installation method |
| CN116900272A (en) * | 2023-06-16 | 2023-10-20 | 大连亚明汽车部件股份有限公司 | An oblique pouring system and vacuum die-casting process |
| CN117227847A (en) * | 2023-09-04 | 2023-12-15 | 重庆长安汽车股份有限公司 | A car body and vehicle |
| CN119973076A (en) * | 2025-01-09 | 2025-05-13 | 广州城市理工学院 | A die-casting mold for an aluminum alloy connecting bracket for new energy vehicles |
-
2022
- 2022-07-28 CN CN202221960181.9U patent/CN217831810U/en active Active
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116900272A (en) * | 2023-06-16 | 2023-10-20 | 大连亚明汽车部件股份有限公司 | An oblique pouring system and vacuum die-casting process |
| CN116851704A (en) * | 2023-07-27 | 2023-10-10 | 重庆东科模具制造有限公司 | A box pouring structure and its installation method |
| CN117227847A (en) * | 2023-09-04 | 2023-12-15 | 重庆长安汽车股份有限公司 | A car body and vehicle |
| CN117227847B (en) * | 2023-09-04 | 2026-02-27 | 重庆长安汽车股份有限公司 | A vehicle body and a vehicle |
| CN119973076A (en) * | 2025-01-09 | 2025-05-13 | 广州城市理工学院 | A die-casting mold for an aluminum alloy connecting bracket for new energy vehicles |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105945255B (en) | Thin-wall part die casting and die-cast formation equipment | |
| CN206382536U (en) | Thin-wall part die casting and die-cast formation equipment | |
| CN211661053U (en) | Aluminum alloy die-casting die | |
| CN113927017A (en) | Sub vehicle frame aluminium low pressure casting mould | |
| CN211564460U (en) | A mold gating system for die-casting engine bracket | |
| CN209736593U (en) | A liquid aluminum die-casting mold for new energy automobile parts | |
| CN210817409U (en) | Thin-wall gearbox body aluminum alloy low-pressure casting forming die | |
| CN219211574U (en) | Die casting die is used in production of engine intake pipe | |
| CN216607133U (en) | A universal mechanical cylinder gating system | |
| CN216096286U (en) | Cab front suspension lower support manufacturing equipment | |
| CN211516034U (en) | Magnesium alloy casting with arc-shaped structure | |
| CN223185523U (en) | Die casting molds | |
| CN113414370A (en) | Die casting die of heavy hydraulic automatic transmission printing oil circuit board | |
| CN223456790U (en) | Equipment for manufacturing engine suspension bracket | |
| CN223803525U (en) | A flow channel plate for a new energy electric vehicle and its manufacturing equipment | |
| CN209424519U (en) | Front-end module bracket pouring device | |
| CN224254199U (en) | Manufacturing equipment for a front suspension under bracket of a driver's cab | |
| CN223997290U (en) | Double-cavity die-casting die structure | |
| CN222856699U (en) | Center advances three board die casting die | |
| CN222519909U (en) | Die U-shaped cooling device for precision casting | |
| CN223371046U (en) | Frame assistant pipe of healthy sport skateboard and manufacturing device thereof | |
| CN223131801U (en) | A powertrain rear suspension bracket assembly and manufacturing equipment thereof | |
| CN209424520U (en) | Front-end module bracket pouring device | |
| CN217666322U (en) | Casting system | |
| CN211489525U (en) | Die for producing bending products of arc-shaped parts |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |