CN217668357U - Circulating grinding wheel dressing structure of vertical double-end-face grinding machine - Google Patents
Circulating grinding wheel dressing structure of vertical double-end-face grinding machine Download PDFInfo
- Publication number
- CN217668357U CN217668357U CN202221376353.8U CN202221376353U CN217668357U CN 217668357 U CN217668357 U CN 217668357U CN 202221376353 U CN202221376353 U CN 202221376353U CN 217668357 U CN217668357 U CN 217668357U
- Authority
- CN
- China
- Prior art keywords
- oilstone
- emery wheel
- repaiies
- grinding wheel
- trimming
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 229910001651 emery Inorganic materials 0.000 claims abstract description 28
- 238000009966 trimming Methods 0.000 claims description 26
- 230000008439 repair process Effects 0.000 abstract 7
- 230000006698 induction Effects 0.000 description 2
- 238000012423 maintenance Methods 0.000 description 2
- 238000000034 method Methods 0.000 description 2
- 230000006978 adaptation Effects 0.000 description 1
- 229910003460 diamond Inorganic materials 0.000 description 1
- 239000010432 diamond Substances 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
Images


Landscapes
- Grinding-Machine Dressing And Accessory Apparatuses (AREA)
Abstract
The utility model relates to a circulating emery wheel of vertical double-ended grinding machine repaiies structure comprises last emery wheel, lower emery wheel, oilstone piece, oilstone dish, repaiies the seat, repaiies the axle, repaiies band pulley, response piece, proximity switch, wedge, switch support, its characterized in that: the rotary control through finishing the band pulley repairs axle circulation and rotates to it is rotatory to drive the oilstone dish, and the oilstone dish drives the oilstone piece and repairs the emery wheel terminal surface, confirms through response piece and proximity switch and repairs position and repair the number of times, accomplishes the high accuracy of repairing the emery wheel terminal surface and repairs, and this structure has the characteristics that the design is simple reasonable, and it is effectual to repair, repair efficient.
Description
Technical Field
The utility model belongs to the technical field of the abrasive wheel is maintained and specifically relates to a circulating abrasive wheel of vertical double-ended grinding machine is maintained structure.
Background
At present, the grinding wheel dressing of a vertical double-end-face grinding machine is generally that a single dressing arm drives a diamond pen or an oilstone to carry out dressing, in the dressing process, the dressing arm reciprocates to realize repeated dressing of the end face of the grinding wheel, and because CBN grinding wheel dressing time is long, the dressing requirement of high efficiency cannot be met by adopting single-contact dressing, a quick dressing structure of the vertical double-end-face grinding machine which can adapt to high-speed dressing needs to be designed.
Disclosure of Invention
The utility model provides a technical scheme that above-mentioned problem was taken is: the utility model provides a circulating emery wheel of vertical double-ended grinding machine repaiies structure, by last emery wheel, lower emery wheel, oilstone piece, oilstone dish, repaiies the seat, repaiies the axle, repaiies band pulley, response piece, proximity switch, wedge, switch support and constitutes its characterized in that: the upper grinding wheel and the lower grinding wheel are horizontally arranged, the vertically arranged trimming seat is arranged on the right side of the upper grinding wheel and the right side of the lower grinding wheel, the trimming shaft is arranged in the middle of the trimming seat, the sensing block and the trimming belt wheel are arranged on the upper portion of the trimming shaft, the oilstone disc is arranged on the lower portion of the trimming shaft, the oilstone disc can rotate 360 degrees around the trimming shaft between the upper grinding wheel and the lower grinding wheel, the oilstone block is fixed on the outer circle of the oilstone disc through the wedge block, the switch support is arranged on the outer side of the sensing block, and the proximity switch is arranged on the switch support.
The utility model discloses owing to take above-mentioned structure, adopt circulating emery wheel to maintain the structure, make the efficiency of emery wheel maintenance improve greatly, the high-speed maintenance of adaptation that can be better, the machining efficiency who makes the lathe simultaneously obtains fine promotion.
Drawings
FIG. 1 is a front view of the structure of the present invention;
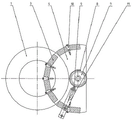
fig. 2 is a top view of the utility model after adjustment;
fig. 3 is a plan view of the utility model before operation.
Labeled in the figure as: 1. the device comprises an upper grinding wheel, a lower grinding wheel, 3. An oilstone block, 4. An oilstone disc, 5. A trimming seat, 6. A trimming shaft, 7. A trimming belt wheel, 8. An induction block, 9. A proximity switch, 10. A wedge block and 11. A switch support.
Detailed Description
The invention will be further described with reference to the accompanying drawings:
as shown in fig. 1, 2 and 3, the utility model relates to a circulating grinding wheel dressing structure of vertical double-ended grinding machine, 1. Go up the emery wheel, 2. Lower emery wheel, 3. Oilstone block, 4. Oilstone disc, 5. Dressing seat, 6. Dressing shaft, 7. Dressing band pulley, 8. Induction block, 9. Proximity switch, 10. Wedge, 11. Switch support component, its characterized in that: go up emery wheel 1 and lower emery wheel 2 be the level and place, install the vertical trimming seat 5 of placing on the right side of last emery wheel 1 and lower emery wheel 2, install trimming shaft 6 in the middle of trimming seat 5, install response piece 8 and trimming belt wheel 7 on the upper portion of trimming shaft 6, install oilstone dish 4 in the lower part of trimming shaft 6, oilstone dish 4 can be around trimming shaft 6 and do 360 rotations between last emery wheel 1 and lower emery wheel 2, oilstone piece 3 fix on the excircle of oilstone dish 4 through wedge 10, install switch support 11 in the outside of response piece 8, install proximity switch 9 on the switch support 11.
The utility model discloses when using, adjust earlier the position of response piece 8 and proximity switch 9, make oilstone dish 4 when reacing the position of figure 2 adjustment back position, breach on the response piece 8 is just to proximity switch 9, proximity switch 9 signal disappears this moment, install oilstone piece 3 on oilstone dish 4, then fix with wedge 10, adjust the clearance between emery wheel 1 and lower emery wheel 2, two upper and lower planes that make oilstone piece 3 just in time can contact the terminal surface of emery wheel 1 and lower emery wheel 2. At this moment, the upper grinding wheel 1 and the lower grinding wheel 2 are started firstly, then the finishing belt wheel 7 is started, the finishing belt wheel 7 drives the finishing shaft 6 to rotate, the finishing shaft 6 drives the oilstone disc 4 and the oilstone block 3 to start rotating, and finishing of the end face of the grinding wheel is completed. When the proximity switch 9 senses the signal loss again along with the rotation of the trimming shaft 7, a complete trimming process is completed. The oilstone disc 4 drives the oilstone block 3 to continuously dress the end faces of the upper grinding wheel 1 and the lower grinding wheel 2 by controlling the rotating speed and the number of rotating turns of the dressing belt wheel 7, so that the end faces of the upper grinding wheel 1 and the lower grinding wheel 2 all reach required precision. When finishing, whetstone dish 4 and whetstone 3 rotate to figure 2 adjustment back position again, proximity switch 9 signal disappears again, finishing band pulley 7 stops rotating, namely finishes the whole finishing course.
The utility model discloses owing to take above-mentioned structure, after introducing the repairment of double-ended grinding machine with the circulating emery wheel of vertical double-ended grinding machine structure of repairing, promoted the dressing efficiency of emery wheel, guaranteed the repairment effect of emery wheel simultaneously, make the processing availability factor of lathe promote greatly.
Claims (1)
1. The utility model provides a circulating emery wheel of vertical double-ended grinding machine repaiies structure, by last emery wheel, lower emery wheel, oilstone piece, oilstone dish, repaiies the seat, repaiies the axle, repaiies band pulley, response piece, proximity switch, wedge, switch support and constitutes its characterized in that: the upper grinding wheel and the lower grinding wheel are horizontally arranged, the vertically arranged trimming seat is arranged on the right side of the upper grinding wheel and the right side of the lower grinding wheel, the trimming shaft is arranged in the middle of the trimming seat, the sensing block and the trimming belt wheel are arranged on the upper portion of the trimming shaft, the oilstone disc is arranged on the lower portion of the trimming shaft, the oilstone disc can rotate 360 degrees around the trimming shaft between the upper grinding wheel and the lower grinding wheel, the oilstone block is fixed on the outer circle of the oilstone disc through the wedge block, the switch support is arranged on the outer side of the sensing block, and the proximity switch is arranged on the switch support.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221376353.8U CN217668357U (en) | 2022-06-05 | 2022-06-05 | Circulating grinding wheel dressing structure of vertical double-end-face grinding machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221376353.8U CN217668357U (en) | 2022-06-05 | 2022-06-05 | Circulating grinding wheel dressing structure of vertical double-end-face grinding machine |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN217668357U true CN217668357U (en) | 2022-10-28 |
Family
ID=83705118
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202221376353.8U Active CN217668357U (en) | 2022-06-05 | 2022-06-05 | Circulating grinding wheel dressing structure of vertical double-end-face grinding machine |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN217668357U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115847295A (en) * | 2022-12-16 | 2023-03-28 | 宇环数控机床股份有限公司 | Linear trimming method and structure of double-ended grinding machine |
-
2022
- 2022-06-05 CN CN202221376353.8U patent/CN217668357U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115847295A (en) * | 2022-12-16 | 2023-03-28 | 宇环数控机床股份有限公司 | Linear trimming method and structure of double-ended grinding machine |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201769102U (en) | Rotary disc multi-station automatic polishing machine | |
| CN106737127B (en) | An automatic grinding and polishing machine with irrational speed ratio | |
| CN110695838B (en) | A centerless superfinishing and polishing processing device for precision shaft parts | |
| CN105108593A (en) | Polishing device for automobile wheel hub | |
| CN202607435U (en) | Grinding and edging device for blades of shears | |
| CN214080787U (en) | Precise numerical control grinding machine for machining | |
| CN101259600A (en) | A method for dressing the end face and outer circle of a grinding wheel | |
| CN205021335U (en) | Automobile wheel hub grinding device | |
| CN216883179U (en) | Head walking type follow-up grinding machine suitable for processing inner and outer curves | |
| CN217019669U (en) | Grinding machine capable of synchronously and uniformly performing standard finishing on grinding wheel and guide wheel in high-precision manner | |
| CN210968450U (en) | Circulating online grinding and finishing device for CBN grinding wheel | |
| CN206140218U (en) | High -efficient double -ended grinding machine | |
| CN210255701U (en) | A flipping device for a polishing machine | |
| CN209648323U (en) | A kind of oval outer profile polishing machine of uniaxial grinding | |
| CN207077303U (en) | A kind of automatic saw blade polishing machine | |
| CN205904791U (en) | Unsteady bistrique of outer profile automatic grinding of casting iron pan | |
| CN2054393U (en) | Multi-working position semi-automatic glassing and buffing machine | |
| CN213319420U (en) | Composite grinding device for main shaft of bracket bearing | |
| CN203357218U (en) | Precise numerical-control double-grinding-head gem roll-grinding forming machine | |
| JPS61146471A (en) | Dressing device | |
| CN209811894U (en) | Peripheral grinding machine | |
| CN103042462B (en) | The two bistrique jewel barreling forming machine of a kind of accurate digital control | |
| CN102626901A (en) | Numerical control machining method for ball polishing wheel | |
| CN205290713U (en) | Stone material lines buffing wheel feeler mechanism and profiling mechanism that has this feeler mechanism thereof | |
| CN213411378U (en) | Vertical turntable grinding machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |