CN217512786U - A fully automatic loading and unloading screw thread rolling device with positioning function - Google Patents
A fully automatic loading and unloading screw thread rolling device with positioning function Download PDFInfo
- Publication number
- CN217512786U CN217512786U CN202221200652.6U CN202221200652U CN217512786U CN 217512786 U CN217512786 U CN 217512786U CN 202221200652 U CN202221200652 U CN 202221200652U CN 217512786 U CN217512786 U CN 217512786U
- Authority
- CN
- China
- Prior art keywords
- thread rolling
- cylinder
- positioning
- base
- conveying mechanism
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Specific Conveyance Elements (AREA)
Abstract
本实用新型公开一种具有定位功能的全自动上下料螺杆滚丝装置,包括底座一、底座二、滚丝机组、导料槽、上下料机构、定位机构、收集箱和控制台,所述底座一上安装有收集箱和输送机构支架,所述输送机构支架固定安装在输送机构下方,所述上下料机构包括气缸支撑台一、气缸支撑台二、输送机构、气缸一、气缸二和驱动电机一,所述底座二通过螺栓与定位机构中的定位导轨连接,底座二上方安装有滚丝机组和控制台。本实用新型的有益效果是:整个工作过程无需人工干预,通过上下料机构、定位机构和滚丝机组的联动工作,便可自动对螺杆坯料进行上料、定位、滚丝和下料,能够节约人工,提高螺杆滚丝效率和滚丝精度的同时,提高工作环境的安全性。
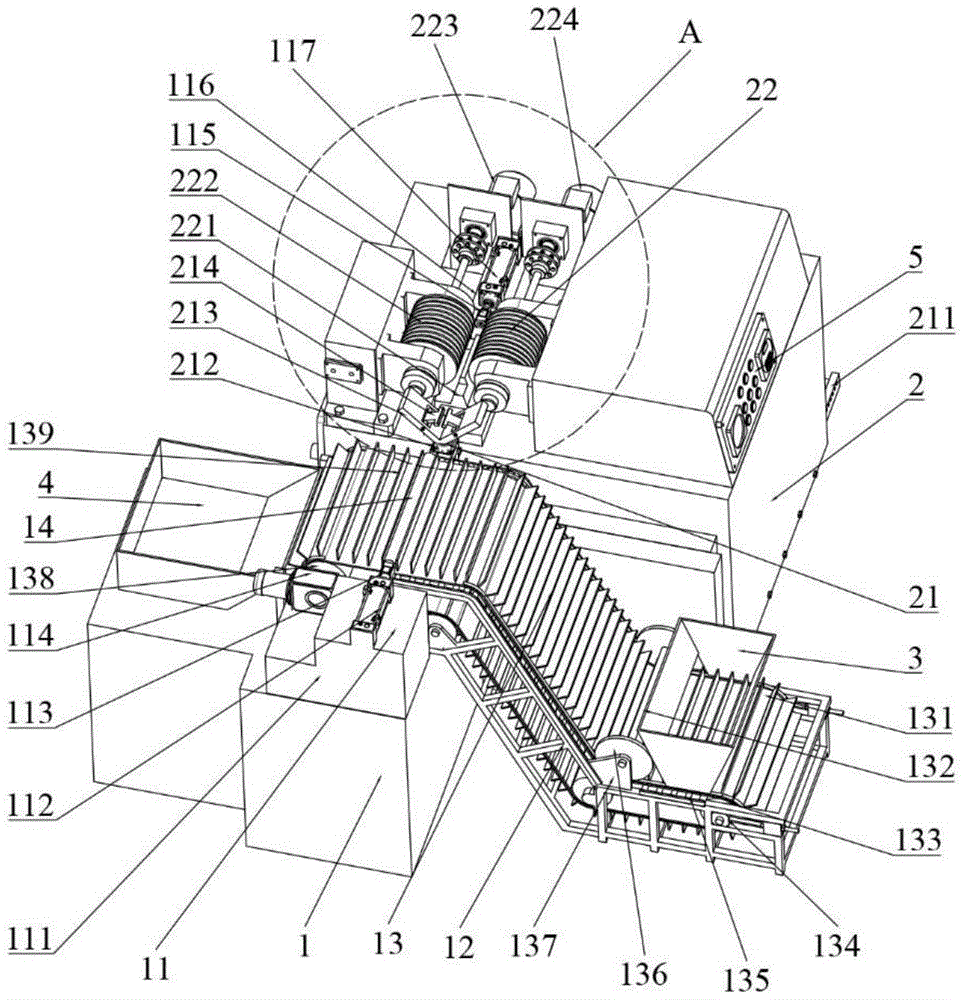
The utility model discloses a fully automatic loading and unloading screw thread rolling device with positioning function, which comprises a base 1, a base 2, a thread rolling unit, a material guide trough, a loading and unloading mechanism, a positioning mechanism, a collection box and a console. A collection box and a conveying mechanism bracket are installed on the first, and the conveying mechanism bracket is fixedly installed under the conveying mechanism. The loading and unloading mechanism includes a cylinder support table 1, a cylinder support table 2, a conveying mechanism, a cylinder 1, a cylinder 2 and a drive motor. First, the second base is connected with the positioning guide rail in the positioning mechanism through bolts, and a thread rolling unit and a console are installed above the second base. The beneficial effects of the utility model are: the whole working process does not need manual intervention, and the screw blank can be automatically loaded, positioned, rolled and unloaded through the linkage work of the loading and unloading mechanism, the positioning mechanism and the thread rolling unit, which can save Manually, while improving the screw thread rolling efficiency and thread rolling accuracy, it also improves the safety of the working environment.
Description
技术领域technical field
本实用新型涉及机械加工技术领域,具体为一种具有定位功能的全自动上下料螺杆滚丝装置。The utility model relates to the technical field of mechanical processing, in particular to a fully automatic loading and unloading screw thread rolling device with a positioning function.
背景技术Background technique
机械加工是指通过一种机械设备对工件的外形尺寸或性能进行改变的过程,在工件的加工过程中,一般采用滚丝机进行螺纹的加工。螺杆是一种外表面有螺旋槽的圆柱。滚丝机是一种多功能冷挤压成形机床,滚丝机能在其滚压力范围内对工件进行螺纹,直纹,斜纹等各种成形滚压,滚丝加工工艺能有效地提高工件表面质量和材料利用率,加工时产生的径向压应力,能显著提高工件的疲劳强度和扭转强度,是一种高效、节能、低耗的理想工艺。Machining refers to the process of changing the dimensions or performance of the workpiece through a mechanical device. In the process of machining the workpiece, a thread rolling machine is generally used for thread processing. A screw is a cylinder with a helical groove on its outer surface. The thread rolling machine is a multi-functional cold extrusion forming machine. The thread rolling machine can perform various forming and rolling operations on the workpiece such as thread, straight grain and twill grain within its rolling force range. The thread rolling process can effectively improve the surface quality of the workpiece. And material utilization rate, radial compressive stress generated during processing, can significantly improve the fatigue strength and torsional strength of the workpiece, is an ideal process with high efficiency, energy saving and low consumption.
现有的滚丝机通常是通过人工将螺杆放进滚丝机中手持螺杆进行定位和滚丝,滚丝完成之后还需要人工将螺杆从滚丝机上取下,导致工人工作强度较大,整个过程十分繁琐,耗费人工,生产效率低,由于工人在上料、定位和下料时都需要反复将手靠近滚丝轮,在工人长时间工作后,不仅无法保证滚丝精度,而且整个操作过程容易出现安全事故。为了解决此类问题,提出一种具有定位功能的全自动上下料螺杆滚丝装置。The existing thread rolling machine usually manually puts the screw into the thread rolling machine to hold the screw for positioning and thread rolling. After the thread rolling is completed, the screw needs to be manually removed from the thread rolling machine, resulting in a high workload of the workers. The process is very cumbersome, labor-intensive, and low in production efficiency. Because workers need to repeatedly bring their hands close to the thread rolling wheel when loading, positioning and unloading, after workers work for a long time, not only the accuracy of thread rolling cannot be guaranteed, but also the entire operation process. Security incidents are prone to occur. In order to solve such problems, a fully automatic loading and unloading screw thread rolling device with positioning function is proposed.
实用新型内容Utility model content
针对现有技术的不足,提供了一种具有定位功能的全自动上下料螺杆滚丝装置,整个工作过程无需人工干预,只需将需要滚丝的若干个螺杆坯料放入导料槽,便可通过上下料机构、定位机构和滚丝机组的联动工作,自动对螺杆坯料进行上料、定位、滚丝和下料,能够节约人工,提高螺杆滚丝工作效率和滚丝精度的同时,提高工作环境的安全性。Aiming at the shortcomings of the prior art, a fully automatic loading and unloading screw thread rolling device with positioning function is provided. The whole working process does not require manual intervention. It only needs to put several screw blanks that need to be rolled into the guide groove, and then Through the linkage work of the loading and unloading mechanism, the positioning mechanism and the thread rolling unit, the screw blank is automatically loaded, positioned, rolled and unloaded, which can save labor, improve the working efficiency and accuracy of screw thread rolling, and improve the work efficiency. safety of the environment.
为实现上述目的,本实用新型提供如下技术方案:一种具有定位功能的全自动上下料螺杆滚丝装置,包括底座一、底座二、滚丝机组、导料槽、上下料机构、定位机构、收集箱和控制台,所述底座一上安装有收集箱、输送机构支架,所述输送机构支架固定安装在输送机构下方,所述上下料机构包括气缸支撑台一、气缸支撑台二、输送机构、气缸一、气缸二和驱动电机一,所述底座二通过螺栓与定位机构中的定位导轨连接,底座二上方安装有滚丝机组和控制台。In order to achieve the above purpose, the utility model provides the following technical solutions: a fully automatic loading and unloading screw thread rolling device with positioning function, comprising a
优选的,所述上下料机构包括气缸支撑台一、气缸支撑台二、输送机构、气缸一、气缸二和驱动电机一,所述气缸支撑台一固定安装在底座一上方,其顶部安装有气缸一,侧方安装有驱动电机一,驱动电机一的输出端连接轴承固定安装在输送机构支架顶部的一端,气缸二安装在气缸支撑台二的上方,气缸支撑台二安装在底座二的上方。Preferably, the loading and unloading mechanism includes a cylinder support table 1, a cylinder support table 2, a conveying mechanism, a
优选的,所述定位机构包括V型定位块、夹持块、气缸三和定位导轨,所述V型定位块固定安装在气缸三的伸缩端上,所述气缸三安装在定位导轨上,所述定位导轨通过螺栓连接螺栓孔固定安装在底座一的侧壁。Preferably, the positioning mechanism includes a V-shaped positioning block, a clamping block, a third cylinder and a positioning guide rail, the V-shaped positioning block is fixedly installed on the telescopic end of the third cylinder, and the third cylinder is installed on the positioning guide rail, so The positioning guide rail is fixedly installed on the side wall of the
优选的,所述滚丝机组包括一组滚丝轮、滚压支撑台、驱动电机二和驱动电机三,所述驱动电机二和驱动电机三的输出轴安装有大皮带轮,所述大皮带轮通过皮带和小皮带轮连接,所述小皮带轮通过联轴器和轴承与滚丝轮输入轴相连。Preferably, the thread rolling unit includes a set of thread rolling wheels, a rolling support table, a second drive motor and a third drive motor, and the output shafts of the second drive motor and the third drive motor are equipped with large pulleys, and the large pulleys pass through the The belt is connected with the small pulley, and the small pulley is connected with the input shaft of the thread rolling wheel through the coupling and the bearing.
优选的,所述输送机构包括与驱动电机一连接的传动滚筒、改向滚筒、Z型输送带、两组改向压轮、两组改向压轮轴和两组螺旋拉紧装置,所述传动滚筒和改向滚筒安装在输送机构支架上,分别与Z型输送带的顶部和底部相连接,所述改向压轮通过压轮架与Z型输送带连接,两组改向压轮上均安装有改向压轮轴。Preferably, the conveying mechanism includes a transmission roller, a reversing roller, a Z-shaped conveyor belt, two groups of reversing pinch rollers, two groups of reversing pinch roller shafts and two groups of screw tensioning devices connected to the driving motor. The roller and the reversing roller are installed on the conveying mechanism bracket and are respectively connected with the top and bottom of the Z-shaped conveyor belt. A reversing pinch roller shaft is installed.
优选的,所述气缸一和气缸二的伸缩端分别安装有电磁铁一和电磁铁二。Preferably, an
优选的,所述V型定位块定位端面为倾斜面,所述定位块端面设置有夹持块,夹持块通过小滚筒与V型定位块连接。Preferably, the positioning end surface of the V-shaped positioning block is an inclined surface, the end surface of the positioning block is provided with a clamping block, and the clamping block is connected to the V-shaped positioning block through a small roller.
优选的,所述Z型输送带上安装有横隔板和导料槽,通过支撑托辊、传动滚筒、改向滚筒和螺旋拉紧装置与输送机构支架连接,Z型输送带顶部设有螺杆坯料本体。Preferably, the Z-shaped conveyor belt is installed with a transverse partition and a material guide groove, and is connected to the conveyor mechanism bracket through a supporting roller, a transmission roller, a reversing roller and a screw tensioning device, and the top of the Z-shaped conveyor belt is provided with a screw Blank body.
优选的,所述横隔板的高度和横隔板两两之间的距离略大于螺杆坯料的直径。Preferably, the height of the diaphragms and the distance between the diaphragms are slightly larger than the diameter of the screw blanks.
本实用新型的有益效果是:整个工作过程无需人工干预,只需将需要滚丝的若干个螺杆坯料放入导料槽,便可通过上下料机构、定位机构和滚丝机组的联动工作,自动对螺杆坯料进行上料、定位、滚丝和下料,能够节约人工,提高螺杆滚丝工作效率的同时,提高工人工作环境的安全性。The beneficial effects of the utility model are: the whole working process does not need manual intervention, and only needs to put several screw blanks that need to be rolled into the material guide trough, and the loading and unloading mechanism, the positioning mechanism and the thread rolling unit can be linked to work automatically. Loading, positioning, thread rolling and unloading of screw blanks can save labor, improve the work efficiency of screw thread rolling, and improve the safety of workers' working environment.
附图说明Description of drawings
图1,整体结构示意图;Figure 1 is a schematic diagram of the overall structure;
图2,A处放大示意图;Fig. 2, the enlarged schematic diagram at A;
图3,定位机构连接示意图;Figure 3 is a schematic diagram of the connection of the positioning mechanism;
图4,V型定位块定位示意图;Figure 4, a schematic diagram of the positioning of the V-shaped positioning block;
图5,滚丝阶段示意图。Figure 5. Schematic diagram of the thread rolling stage.
图中:1、底座一;11、上下料机构111、气缸支撑台一;112、气缸一;113、电磁铁一;114、驱动电机一;115、电磁铁二;116、气缸支撑台二;117、气缸二;12、输送机构支架;13、输送机构;131、Z型输送带;132、改向压轮轴;133、改向滚筒;134、螺旋拉紧装置;135、支撑托辊;136、改向压轮;137、压轮架;138、传动滚筒;139、横隔板;14、螺杆坯料;2、底座二;21、定位机构;211、定位导轨;212、气缸三;213、V型定位块;214、夹持块;215、螺栓;216、螺栓孔;217、小滚筒;22、滚丝机组;221、滚压支撑台;222、滚丝轮;223、驱动电机二;224、驱动电机三;225、小皮带轮;226、皮带;227、大皮带轮;3、导料槽;4、收集箱;5、控制台。In the figure: 1.
具体实施方式:Detailed ways:
下面将结合本实用新型实施例中的附图,对本实用新型实施例中的技术方案进行清楚、完整地描述,显然,所描述的实施例仅仅是本实用新型一部分实施例,而不是全部的实施例。The technical solutions in the embodiments of the present utility model will be clearly and completely described below with reference to the accompanying drawings in the embodiments of the present utility model. Obviously, the described embodiments are only a part of the embodiments of the present utility model, rather than all the implementations. example.
请参阅图1-2,一种具有定位功能的全自动上下料螺杆滚丝装置,包括底座一1、底座二2、滚丝机组22、导料槽3、上下料机构11、定位机构21、收集箱4、控制台5,所述底座一1上安装有收集箱4、输送机构支架12,所述输送机构支架12固定安装在输送机构13下方,所述上下料机构11包括气缸支撑台一111、气缸支撑台二116、输送机构13、气缸一112、气缸二117和驱动电机一114,所述气缸支撑台一111固定安装在底座一1上方,其顶部安装有气缸一112,侧方安装有驱动电机一114,驱动电机一114的输出端连接轴承并固定安装在输送机构支架12顶部的一端,气缸二117安装在气缸支撑台二116的上方,气缸支撑台二116安装在底座二2的上方,所述气缸一112和气缸二117的伸缩端分别安装有电磁铁一113和电磁铁二115,所述底座二2通过螺栓215与定位机构21中的定位导轨211连接,底座二2上方安装有滚丝机组22和控制台5。Please refer to Figure 1-2, a fully automatic loading and unloading screw thread rolling device with positioning function, including
请参阅图3-5,定位机构21包括V型定位块213、气缸三212和定位导轨211,其中V型定位块213固定安装在气缸三212的伸缩端上,V型定位块213的倾斜面上安装有夹持块214,夹持块214通过小滚筒217安装在V型定位块213的倾斜面上,夹持块214侧边有倒圆角,方便螺杆坯料14挤入夹持块214和V型定位块213的倾斜面之间进行定位,螺杆坯料14未滚丝的一端在滚丝过程中处于V型定位块213的倾斜面和夹持块214之间,通过气缸三212伸长或者收缩,使螺杆坯料14中轴线与滚丝轮222滚轴的中轴线位于同一水平面,保证滚丝加工得到的螺纹精确度,同时提高V型定位块213提高对工件的夹持定位效果,防止在滚丝过程中螺杆坯料14产生晃动而从滚丝轮222之间挤出。定位导轨211与底座一1的侧壁通过螺栓215和螺栓孔216固定连接,底座二2通过螺栓215安装在定位导轨211上,对于不同长度的螺杆坯料14可通过移动底座二2调整定位导轨211和底座二2上的不同位置上的螺栓孔216并对螺栓孔216进行对齐,再通过螺栓215连接定位导轨211和底座二2,可以在一定范围内调节V型定位块213与滚丝轮222之间的水平距离,以便对不同长度螺杆坯料14进行上料和定位。3-5, the
请参阅图1,输送机构13中安装在Z型输送带131上的横隔板139的高度和相邻横隔板139两两之间的距离略大于螺杆坯料14的直径,可保证到达Z型输送带131顶部的横隔板139之间的螺杆坯料14只有一个,从而使需要滚丝的若干个螺杆坯料14排齐并储存在输送带131上,有利于后续精准上料。Referring to FIG. 1, the height of the
本实用新型的工作原理为:The working principle of the utility model is:
请参阅图1-2,在本实施方案中,该设备的用电设备由控制台5进行控制。使用时,将需要加工的若干个螺杆坯料14放置于Z型输送带131底部的导料槽3中,操控控制台5启动驱动电机一114,在Z型输送带131开始传动后,螺杆坯料14开始从Z型输送带131底部向Z型输送带131顶部输送,在螺杆坯料14经过Z型输送带131斜坡阶段时,在横隔板139和重力的影响下,相邻的两块横隔板139之间多余的螺杆坯料14将滚落至Z型输送带131底部,在此作用下,到达Z型输送带131顶部的相邻的两块横隔板139之间只存在一个螺杆坯料14,当螺杆坯料14移动到滚丝机组22待加工位置的时候,驱动电机一114暂停转动,Z型输送带131停止输送,控制台5控制气缸支撑台一111上方的电磁铁一113通电和气缸一112伸缩端伸长,气缸一112带动电磁铁一113推动螺杆坯料14向V型定位块213移动。Please refer to FIGS. 1-2 , in this embodiment, the electrical equipment of the device is controlled by the
请参阅图1、图2、图4和图5,当螺杆坯料14接触并开始穿过V型定位块213时,控制台5控制气缸三212伸长或者收缩,使得通过V型定位块213的螺杆坯料14中轴线将与滚丝轮222滚轴的中轴线处于同一水平面。此时气缸一112继续伸长,同时气缸二117伸缩端伸长和电磁铁二115通电,直到电磁铁二115接触并吸住螺杆坯料14,此时气缸一112停止伸长并保持不动,电磁铁一113断电,气缸二117伸缩端收缩直到将螺杆坯料14加工部分拖至滚丝轮222之间的滚压支撑台221上完成上料和定位。此时螺杆坯料14加工端位于滚丝轮222之间,另一端位于V型定位块213和夹持块214之间进行定位,驱动电机二223和驱动电机三224启动,滚丝轮222转动开始进行滚丝,滚丝完成之后,驱动电机二223和驱动电机三224停止转动,控制台5控制电磁铁二115通电和气缸二117伸缩端伸长,直到电磁铁二115吸住螺杆坯料14并推动螺杆坯料14穿过V型定位块213直到螺杆坯料14接触电磁铁一113,当螺杆坯料14接触电磁铁一113后,气缸二117停止伸长并保持不动,电磁铁二115断电,同时电磁铁一113通电,气缸一112伸缩端收缩,拖动螺杆坯料14回到滚丝前在Z型输送带131顶部的位置,此时驱动电机一114再次通电转动,Z型输送带131继续输送滚丝完成的螺杆,同时输送下一个相邻横隔板139之间的未滚丝的螺杆坯料14移动到滚丝机组22待加工位置,并重复上述过程。当完成滚丝的螺杆到达Z型输送带131顶部尽头后,将顺着收集箱4的斜边滚落至安装在底座一1上方的收集箱4中,完成对螺杆的下料。1 , 2 , 4 and 5 , when the screw blank 14 contacts and starts to pass through the V-shaped
以上所述,仅是本实用新型的较佳实施例,任何熟悉本领域的技术人员均可能利用上述阐述的技术方案对本实用新型加以修改或将其修改为等同的技术方案。因此,依据本实用新型的技术方案所进行的任何简单修改或等同置换,尽属于本实用新型要求保护的范围。The above are only preferred embodiments of the present invention, and any person skilled in the art may modify the present invention by using the technical solutions described above or modify them into equivalent technical solutions. Therefore, any simple modification or equivalent replacement performed according to the technical solution of the present invention falls within the protection scope of the present invention.
尽管本文较多地使用了1、底座一;11、上下料机构111、气缸支撑台一;112、气缸一;113、电磁铁一;114、驱动电机一;115、电磁铁二;116、气缸支撑台二;117、气缸二;12、输送机构支架;13、输送机构;131、Z型输送带;132、改向压轮轴;133、改向滚筒;134、螺旋拉紧装置;135、支撑托辊;136、改向压轮;137、压轮架;138、传动滚筒;139、横隔板;14、螺杆坯料;2、底座二;21、定位机构;211、定位导轨;212、气缸三;213、V型定位块;214、夹持块;215、螺栓;216、螺栓孔;217、小滚筒;22、滚丝机组;221、滚压支撑台;222、滚丝轮;223、驱动电机二;224、驱动电机三;225、小皮带轮;226、皮带;227、大皮带轮;3、导料槽;4、收集箱;5、控制台等术语,但并不排除使用其它术语的可能性。使用这些术语仅仅是为了更方便地描述和解释本实用新型的本质;把它们解释成任何一种附加的限制都是与本实用新型精神相违背的。Although this article mostly uses 1,
在本实用新型描述中,如有术语“一”、“二”仅用于描述目的,而不能理解为指示或暗示相对重要性或隐含指明技术特征的数量。“若干个”的含义是两个或两个以上,除非另有明确具体的限定。In the description of the present invention, the terms "one" and "two" are only used for the purpose of description, and should not be understood as indicating or implying relative importance or indicating the number of technical features. "Several" means two or more, unless expressly and specifically limited otherwise.
Claims (9)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221200652.6U CN217512786U (en) | 2022-05-18 | 2022-05-18 | A fully automatic loading and unloading screw thread rolling device with positioning function |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202221200652.6U CN217512786U (en) | 2022-05-18 | 2022-05-18 | A fully automatic loading and unloading screw thread rolling device with positioning function |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN217512786U true CN217512786U (en) | 2022-09-30 |
Family
ID=83389571
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202221200652.6U Expired - Fee Related CN217512786U (en) | 2022-05-18 | 2022-05-18 | A fully automatic loading and unloading screw thread rolling device with positioning function |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN217512786U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114951519A (en) * | 2022-05-18 | 2022-08-30 | 湘潭大学 | Full-automatic feeding and discharging screw rod thread rolling device with positioning function |
-
2022
- 2022-05-18 CN CN202221200652.6U patent/CN217512786U/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114951519A (en) * | 2022-05-18 | 2022-08-30 | 湘潭大学 | Full-automatic feeding and discharging screw rod thread rolling device with positioning function |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN211540158U (en) | Full-automatic rotor bearing press-fitting machine | |
| CN108655751A (en) | Intelligent single steel bar sawing mantle fiber polishing production line | |
| CN206435927U (en) | Fully automatic feeding roll squeezer | |
| CN207390425U (en) | An automatic rolling machine for assembly line | |
| CN114951519A (en) | Full-automatic feeding and discharging screw rod thread rolling device with positioning function | |
| CN217006676U (en) | Online hydraulic detection system for PVC water supply pipe | |
| CN114473235A (en) | Precise thin-walled tube laser cutting system capable of automatically feeding and discharging | |
| CN220906257U (en) | A logistics conveying device for automated production line | |
| CN110743949A (en) | A kind of steel pipe online grooving equipment | |
| CN218856599U (en) | A feeding device for a metal processing grinding and polishing machine | |
| CN206763420U (en) | A glass detection robot unloading table | |
| CN212557917U (en) | Steel pipe surface treatment tank | |
| CN210099719U (en) | An automatic unloading and recycling device for oil pump workpiece carrier plate | |
| CN210702192U (en) | A discharge device for a CNC bending machine | |
| CN112091236A (en) | a peeling machine | |
| CN220200581U (en) | Pipe feeding machine | |
| CN107138797A (en) | A kind of numerical control saw | |
| CN220825129U (en) | Finished product acceptance machine | |
| CN222203923U (en) | NG product unloading station | |
| CN222373832U (en) | Tear dish hoisting device open and tear dish machine open | |
| CN211662174U (en) | High-efficient guillootine in abrasive band | |
| CN112059044A (en) | Auxiliary feeding and discharging device of numerical control synchronous bending machine | |
| CN220461986U (en) | Auxiliary feeding device for veneer reeling machine | |
| CN110919311A (en) | Efficient chain assembly production line | |
| CN222664711U (en) | Textile equipment capable of automatically feeding |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20220930 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |