CN217071578U - Milling and fixing tool for inner shape characteristics of thin-wall cylinder part - Google Patents
Milling and fixing tool for inner shape characteristics of thin-wall cylinder part Download PDFInfo
- Publication number
- CN217071578U CN217071578U CN202220697228.0U CN202220697228U CN217071578U CN 217071578 U CN217071578 U CN 217071578U CN 202220697228 U CN202220697228 U CN 202220697228U CN 217071578 U CN217071578 U CN 217071578U
- Authority
- CN
- China
- Prior art keywords
- thin
- block
- positioning
- wall
- wall cylinder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003801 milling Methods 0.000 title claims abstract description 18
- 230000007246 mechanism Effects 0.000 claims abstract description 25
- 238000003825 pressing Methods 0.000 claims description 40
- 238000003754 machining Methods 0.000 abstract description 5
- 230000009286 beneficial effect Effects 0.000 abstract description 2
- 238000007906 compression Methods 0.000 description 6
- 230000006835 compression Effects 0.000 description 5
- 235000017166 Bambusa arundinacea Nutrition 0.000 description 2
- 235000017491 Bambusa tulda Nutrition 0.000 description 2
- 241001330002 Bambuseae Species 0.000 description 2
- 235000015334 Phyllostachys viridis Nutrition 0.000 description 2
- 239000011425 bamboo Substances 0.000 description 2
- 230000008859 change Effects 0.000 description 2
- 230000009471 action Effects 0.000 description 1
- 230000003139 buffering effect Effects 0.000 description 1
- 239000002173 cutting fluid Substances 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
Images


Landscapes
- Jigs For Machine Tools (AREA)
Abstract
The utility model provides a fixed frock of shape characteristic milling process in thin wall barrel spare, including the base, be equipped with the stand on the base, the base is equipped with positioning mechanism with the junction of stand, and the stand upper end is equipped with detachable and ring clamp, and positioning mechanism presss from both sides tight thin wall barrel spare with the ring clamp cooperation, and the stand inboard is equipped with the side pressure mechanism. The utility model discloses the beneficial effect who produces is: the fixing tool is matched with the annular pressure plate through the positioning mechanism to position and axially clamp the thin-wall cylinder, so that the axial deformation of the thin-wall cylinder is prevented; the pressure measuring mechanism is used for providing support for the side wall of the thin-wall cylinder piece, so that the deformation of the thin-wall cylinder piece in the circumferential direction is prevented; and fixed frock accessible locating piece and guide block carry out the quick location of thin wall barrel spare, and the location alignment time is short, improves machining efficiency.
Description
Technical Field
The utility model relates to a thin wall section of thick bamboo clamping frock technical field especially indicates a fixed frock of shape characteristic milling process in thin wall section of thick bamboo.
Background
In the traditional machining method, the internal shape characteristic of a large-sized thin-wall cylinder is difficult to machine, and parts are easily clamped and deformed due to improper clamping, the size of a machining position is out of tolerance, and the parts are scrapped in severe cases. Therefore, a special tool is needed when a large-size thin-wall cylinder is processed to assist in clamping of the parts, and the tool has the characteristics of convenience in clamping and alignment.
SUMMERY OF THE UTILITY MODEL
The utility model provides a fixed frock of shape characteristic milling process in thin wall barrel spare has solved among the prior art problem that thin wall barrel spare warp easily in the interior shape course of working.
The technical scheme of the utility model is realized like this:
the milling and fixing tool for the inner shape characteristics of the thin-wall barrel part comprises a base, wherein a stand column is arranged on the base, a positioning mechanism is arranged at the joint of the base and the stand column, a detachable annular pressing plate is arranged at the upper end of the stand column, the positioning mechanism and the annular pressing plate are matched to clamp the thin-wall barrel part tightly, and a side pressing mechanism is arranged on the inner side of the stand column. The positioning mechanism and the annular pressing plate are matched to position and axially clamp the thin-wall barrel part, and the side pressing mechanism supports the side wall of the thin-wall barrel part, so that the side wall of the thin-wall barrel part is prevented from being stressed and deformed during inner shape processing, and the processing stability of the thin-wall barrel part is ensured.
The quantity of stand is at least two, and the stand is the annular array and arranges. The stand provides the support for annular pressure plate, guarantees that annular pressure plate is fixed stable to guarantee the lateral wall atress of thin wall barrel spare even.
The positioning mechanism comprises a positioning block and a guide block, the guide block is fixedly arranged on the base, and the positioning block is connected with the guide block in a sliding mode. The positioning block slides on the guide block, so that the relative position of the positioning block and the thin-wall barrel part is changed, and the positioning of the positioning block on the thin-wall barrel part is realized.
The positioning block is of an L-shaped structure, the upright post is provided with a positioning bolt, the vertical part of the positioning block is matched with the positioning bolt, and the horizontal part of the positioning block is connected with the guide block. The positioning bolt rotates to push the positioning block to slide on the guide block, and the vertical part and the horizontal part of the positioning block are matched to position the thin-wall barrel part.
The bottom of the transverse part of the positioning block is provided with an inclined sliding groove, the top of the guide block is provided with an inclined convex block, and the inclined sliding groove is in sliding fit with the inclined convex block. When the positioning block slides on the guide block, the height of the transverse part of the positioning block is changed, and when the vertical part and the transverse part of the positioning block are simultaneously contacted with the thin-wall barrel part, the positioning of the thin-wall barrel part is completed.
The side pressing mechanism comprises a pressing bolt and a pressing block, the pressing bolt is in threaded connection with the stand column, and the pressing bolt penetrates through the stand column and is movably connected with the pressing block. The compression bolts rotate to change the relative positions of the compression blocks, and then the compression blocks clamp the side wall of the thin-wall barrel part.
The pressing block comprises an upper pressing block and a lower pressing block, and elastic pads are arranged on pressing surfaces of the upper pressing block and the lower pressing block. The combined action of the upper pressing block and the lower pressing block ensures that the side wall of the thin-wall cylinder part is stressed uniformly, and meanwhile, the elastic pad provides buffering and protects the outer wall of the thin-wall cylinder part.
The bottom of base is equipped with at least one chip groove. And during the machining of the inner shape, the cutting fluid and the cut chips are discharged through the chip discharge grooves, so that the fixed tool is convenient to clean.
The annular pressing plate is connected with the upright post through a screw. And the annular pressing plate is fixed on the stand column by screwing the screw, and the annular pressing plate axially compresses the thin-wall barrel part.
The utility model discloses the beneficial effect who produces is: the fixing tool is matched with the annular pressure plate through the positioning mechanism to position and axially clamp the thin-wall cylinder, so that the axial deformation of the thin-wall cylinder is prevented; the pressure measuring mechanism is used for providing support for the side wall of the thin-wall cylinder piece, so that the deformation of the thin-wall cylinder piece in the circumferential direction is prevented; and fixed frock accessible locating piece and guide block carry out the quick location of thin wall barrel spare, and the location alignment time is short, improves machining efficiency.
Drawings
In order to more clearly illustrate the embodiments of the present invention or the technical solutions in the prior art, the drawings used in the description of the embodiments or the prior art will be briefly described below, it is obvious that the drawings in the following description are only some embodiments of the present invention, and for those skilled in the art, other drawings can be obtained according to these drawings without creative efforts.
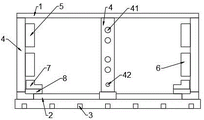
FIG. 1 is a schematic structural view of a thin-wall cylinder internal shape feature milling and fixing tool.
Fig. 2 is a top view of the fixture.
Fig. 3 is a schematic view of the positioning block and the guide block.
In the figure: 1-annular pressing plate, 2-base, 3-chip groove, 4-upright post, 41-compression bolt, 42-positioning bolt, 5-upper compression block, 6-lower compression block, 7-positioning block, 71-inclined chute, 8-guide block and 81-inclined lug.
Detailed Description
The technical solutions in the embodiments of the present invention will be described clearly and completely with reference to the accompanying drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only some embodiments of the present invention, not all embodiments. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without any creative effort belong to the protection scope of the present invention.
Embodiment 1, as shown in fig. 1 and 2, a milling and fixing tool for internal shape characteristics of a thin-wall cylinder comprises a base 2, wherein the base 2 is provided with at least two upright columns 4, the number of the upright columns 4 is 8, the upright columns 4 are arranged in an annular array, and the upright columns 4 are uniformly arranged; a positioning mechanism is arranged at the joint of the base 2 and the upright post 4, and is used for aligning and positioning the thin-wall cylinder piece, so that the mounting position of the thin-wall cylinder piece is accurate; the upper end of the upright post 4 is provided with a detachable annular pressure plate 1, the positioning and clamping mechanism is matched with the annular pressure plate 1 to clamp the thin-wall barrel part, and after the positioning mechanism is aligned, the annular pressure plate 1 clamps the thin-wall barrel part to prevent the axial deformation of the thin-wall barrel part; the inner side of the upright post 4 is provided with a side pressing mechanism which supports the side wall of the thin-wall cylinder and prevents the thin-wall cylinder from deforming in the circumferential direction during processing.
Further, positioning mechanism includes locating piece 7 and guide block 8, and guide block 8 is fixed to be set up on base 2, and locating piece 7 and guide block 8 sliding connection. The positioning blocks 7 slide along the radial direction of the thin-wall cylinder part, and the plurality of positioning blocks 7 slide to position the side wall of the thin-wall cylinder part. The positioning block 7 is of an L-shaped structure, the upright post 4 is provided with a positioning bolt 42, the vertical part of the positioning block 7 is matched with the positioning bolt 42, and the horizontal part of the positioning block 7 is connected with the guide block 8. The side wall of the thin-wall cylinder part is contacted with the vertical part of the positioning block 7, and the end surface of the thin-wall cylinder part is contacted with the horizontal part of the positioning block 7. The positioning bolt 42 is rotated to push the positioning block 7 to slide, the relative position of the positioning block 7 and the guide block 8 is changed, and the clamping and positioning of the thin-wall barrel part are realized.
Further, as shown in fig. 3, an inclined sliding groove 71 is formed at the bottom of the transverse portion of the positioning block 7, an inclined protrusion 81 is formed at the top of the guide block 8, and the inclined sliding groove 71 is in sliding fit with the inclined protrusion 81; specifically, the inclined projection 81 is inclined obliquely upward along the radial direction of the thin-walled cylinder, so that the positioning block 7 gradually rises when sliding toward the center of the thin-walled cylinder. When the positioning blocks 7 slide, the height of the transverse part of each positioning block 7 can be changed, and when the transverse part and the vertical part of each positioning block 7 are simultaneously contacted with the thin-wall barrel, the alignment and the positioning of the thin-wall barrel are completed.
Further, the bottom of the base 2 is provided with at least one chip groove 3. In this embodiment, the number of chip grooves 3 is 16, and chip grooves 3 are evenly arranged along the circumferential direction, and chip grooves 3 conveniently carry out the clearance of fixed frock.
Further, the annular pressure plate 1 is connected with the upright post 4 by screws. After the thin-wall cylinder is positioned, the annular pressing plate 1 is placed at the upper end of the thin-wall cylinder, and the screw is screwed down to fix the annular pressing plate 1, so that the thin-wall cylinder is axially fixed.
The other structure is the same as that of embodiment 1.
The use of fixed frock: placing the thin-wall cylinder to be processed between the upright columns 4, rotating the positioning bolts 42 to enable the positioning blocks 7 to slide, and completing positioning of the thin-wall cylinder when the transverse part and the vertical part of each positioning block 7 are in contact with the thin-wall cylinder; placing the annular pressure plate 1 at the upper end of the upright post 4, and screwing down the screw to ensure that the annular pressure plate 1 is matched with the positioning block 7 to axially clamp the thin-wall barrel part; and rotating the hold-down bolt 41 to enable the upper hold-down block 5 and the lower hold-down block 6 to be respectively contacted with the side wall of the thin-wall cylinder part, so that the thin-wall cylinder part is clamped in the circumferential direction.
The above description is only for the preferred embodiment of the present invention, and should not be taken as limiting the invention, and any modifications, equivalent replacements, improvements, etc. made within the spirit and principle of the present invention should be included in the protection scope of the present invention.
Claims (9)
1. The utility model provides a fixed frock of shape characteristic milling process in thin wall barrel spare, includes base (2), its characterized in that is equipped with stand (4) on base (2), and the junction of base (2) and stand (4) is equipped with positioning mechanism, can dismantle on stand (4) and be equipped with annular clamp plate (1), and positioning and clamping mechanism presss from both sides tight thin wall barrel spare with annular clamp plate (1) cooperation, and stand (4) inboard is equipped with the side pressure mechanism.
2. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 1, wherein the number of the columns (4) is at least two, and the columns (4) are arranged in an annular array.
3. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 1 or 2, wherein the positioning mechanism comprises a positioning block (7) and a guide block (8), the guide block (8) is fixedly arranged on the base (2), and the positioning block (7) is in sliding connection with the guide block (8).
4. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 3, wherein the positioning block (7) is of an L-shaped structure, the upright post (4) is provided with a positioning bolt (42), the vertical part of the positioning block (7) is matched with the positioning bolt (42), and the horizontal part of the positioning block (7) is connected with the guide block (8).
5. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 4, wherein the bottom of the transverse part of the positioning block (7) is provided with an inclined sliding groove (71), the top of the guide block (8) is provided with an inclined lug (81), and the inclined sliding groove (71) is in sliding fit with the inclined lug (81).
6. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to any one of claims 1, 2, 4 and 5, wherein the side pressing mechanism comprises a pressing bolt (41) and a pressing block, the pressing bolt (41) is in threaded connection with the upright column (4), and the pressing bolt (41) penetrates through the upright column (4) and is movably connected with the pressing block.
7. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 6, wherein the pressing block comprises an upper pressing block (5) and a lower pressing block (6), and elastic pads are arranged on the pressing surfaces of the upper pressing block (5) and the lower pressing block (6).
8. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 1 or 7, wherein the bottom of the base (2) is provided with at least one chip groove (3).
9. The milling and fixing tool for the internal shape characteristics of the thin-wall cylinder part according to claim 8, wherein the annular pressure plate (1) is connected with the upright column (4) through a screw.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202220697228.0U CN217071578U (en) | 2022-03-29 | 2022-03-29 | Milling and fixing tool for inner shape characteristics of thin-wall cylinder part |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202220697228.0U CN217071578U (en) | 2022-03-29 | 2022-03-29 | Milling and fixing tool for inner shape characteristics of thin-wall cylinder part |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN217071578U true CN217071578U (en) | 2022-07-29 |
Family
ID=82553159
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202220697228.0U Active CN217071578U (en) | 2022-03-29 | 2022-03-29 | Milling and fixing tool for inner shape characteristics of thin-wall cylinder part |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN217071578U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116460620A (en) * | 2023-04-20 | 2023-07-21 | 中国工程物理研究院激光聚变研究中心 | Clamping device and clamping method for inner surface processing of high-steep thin-walled components |
-
2022
- 2022-03-29 CN CN202220697228.0U patent/CN217071578U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116460620A (en) * | 2023-04-20 | 2023-07-21 | 中国工程物理研究院激光聚变研究中心 | Clamping device and clamping method for inner surface processing of high-steep thin-walled components |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN114055211A (en) | Clamp and method for turning thin-wall disc-shaped part on lathe | |
| CN105345552A (en) | Milling jig for machining four peripheral faces of lathe tool apron rack | |
| CN218746397U (en) | Multi-workpiece milling tool clamp | |
| CN114346618B (en) | Processing method of triangular section sealing ring | |
| CN212191275U (en) | A car anchor clamps for processing water pump box | |
| CN205915057U (en) | Vertical machining center anchor clamps that processing engine cylinder used | |
| CN204868248U (en) | Reverse gear and shift cantilever at anchor clamps of machine with central end face milling | |
| CN219275177U (en) | Clamping tool for tilting pad bearing pad of turbine unit | |
| CN217667990U (en) | Clamping device for machine tool | |
| CN214816630U (en) | CNC is multi-angle curved surface processing tool for lathe | |
| CN214444676U (en) | Integral type frock clamp | |
| CN211136919U (en) | Multilayer apron processing frock | |
| CN201552455U (en) | Fixture for processing outer surface of multi-insert rotary combined workpiece | |
| CN208713461U (en) | A kind of frock clamp of motor turning part | |
| CN212599047U (en) | Special tooling for oil pipe joint drilling | |
| CN112025370A (en) | Clamp for four-axis machining center of chain wheel seat | |
| CN223313802U (en) | Six-station automatic clamp for U-shaped shell parts | |
| CN218341166U (en) | Universal clamp for machining spindle gear shaping | |
| CN222903303U (en) | A fixture for rough turning the inner hole of a thin-walled motor inner housing | |
| CN204868249U (en) | Cantilever anchor clamps combination of shifting of reversing gear | |
| CN204818856U (en) | A anchor clamps that is used for machining center to mill cantilever terminal surface of shifting gears that reverses gear | |
| CN219444340U (en) | Pneumatic turntable clamp for support | |
| CN220196997U (en) | Workpiece positioning fixture for numerical control plane drilling machine | |
| CN105081778A (en) | Efficient and reliable locating clamp for gear reversing and shifting cantilever | |
| CN219189455U (en) | Drilling and milling clamp for thin-wall flat workpiece |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| EE01 | Entry into force of recordation of patent licensing contract |
Assignee: HENAN AEROSPACE PRECISION MACHINING Co.,Ltd. Assignor: HENAN AEROSPACE HYDRAULIC AND PNEUMATIC TECHNOLOGY Co.,Ltd. Contract record no.: X2023980052075 Denomination of utility model: A fixed fixture for milling the internal shape characteristics of thin-walled cylindrical parts Granted publication date: 20220729 License type: Common License Record date: 20231215 |
|
| EE01 | Entry into force of recordation of patent licensing contract |