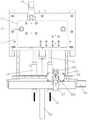
Disclosure of Invention
The utility model aims at providing a porous pipe fitting processing equipment, its porous processing that can realize the pipe fitting has the characteristics of processing fast, efficient, still has the characteristics that automated control system is high, the controllability is strong and processing good quality is stable.
The utility model discloses a following technical scheme of purpose accessible realizes:
a porous pipe fitting processing device comprises a rack, wherein the rack comprises a rack plate, vertical guide pillars and a lower pressing plate, 2 vertical guide pillars are symmetrically arranged on the rack plate of the rack, the lower pressing plate is positioned above the rack plate, two ends of the lower pressing plate are respectively movably sleeved on the 2 vertical guide pillars, and the lower pressing plate can move up and down along the vertical guide pillars above the rack plate; the method is characterized in that: the device also comprises a front hole machining mechanism and a rear hole machining mechanism arranged near one side of the front hole machining mechanism.
The front hole machining mechanism comprises a front hole cutter and a front hole positioning head, the front hole cutter and the front hole positioning head are arranged in a vertically corresponding mode, the front hole cutter is of a vertically-arranged cylindrical structure and is arranged in the front portion of the lower pressing plate, the front hole positioning head is of a longitudinally-arranged cylindrical structure and is arranged in the front portion of the upper portion of the frame plate, a front hole is formed in the front hole positioning head and is right aligned to the front hole cutter, and the lower pressing plate is stressed to move downwards to enable the front hole cutter to be inserted into the front hole of the front hole positioning head in the machining process.
The back hole processing mechanism comprises a back hole positioning upper block, a back hole positioning lower block, a movable cutter assembly and a cutter resetting mechanism. The rear hole positioning upper block is arranged at the front part below the lower pressure plate, and the bottom of the rear hole positioning upper block is provided with an arc-shaped positioning upper groove which is longitudinally arranged. The top that the rack plate was located to piece under the back hole location is anterior, its top has the arc location lower groove of vertical setting, and the arc location upper groove corresponds the setting from top to bottom with the arc location lower groove, and the arc location has the processing back hole of vertical setting in the groove down.
The movable cutter component comprises a cutter mounting block, a cylindrical mounting head and a rear hole cutter, the cutter mounting block is vertically movably arranged at the rear part of the lower block positioned in the rear hole above the frame plate, the bottom of the cutter mounting block movably penetrates through the frame plate, the cylindrical mounting head is longitudinally arranged at the front part of the cutter mounting block, and the rear hole cutter is a vertically arranged cylindrical structure which is arranged on the cylindrical mounting head and is just opposite to a processed rear hole of the lower block positioned in the rear hole.
The cutter resetting mechanism comprises a resetting fixed plate, a resetting movable plate and a resetting spring, the resetting fixed plate is fixedly arranged below the frame plate, the resetting movable plate is movably arranged between the frame plate and the resetting fixed plate and is positioned below the bottom of the cutter mounting block of the movable cutter assembly, and the resetting spring is arranged between the resetting fixed plate and the resetting movable plate.
The cutter mounting block of the movable cutter component is stressed to move downwards, the reset movable plate can be pushed to move downwards to enable a reset spring of the cutter reset mechanism to compress and store force, and meanwhile, a rear hole cutter moves downwards to be inserted into a rear processing hole of the rear hole positioning lower block; when the reset spring is extended and reset, the reset movable plate can be pushed to move upwards to enable the cutter mounting block and the rear hole cutter to move upwards to reset.
According to the optimized scheme, the utility model also comprises a front end processing mechanism arranged near the other side of the front hole processing mechanism, the front end processing mechanism comprises a vertical pressing plate, a front end movable block, a front end cutter, a front end positioning head and a reset cylinder, the vertical pressing plate is of a vertically arranged plate-shaped structure and is arranged at the rear part below the lower pressing plate, and the rear end of the lower part of the vertical pressing plate is gradually narrowed towards the front end of the lower part so that the lower part of the vertical pressing plate has an oblique pressing surface; the front end movable block is longitudinally and movably arranged above the frame plate, the rear end of the front end movable block is provided with an oblique guide surface matched with an oblique pressing surface of the vertical pressing plate, the front end cutter is of a plate-shaped structure obliquely arranged on the bottom of the front end movable block, and the cutter edge end of the front end cutter is positioned at the front part above the frame plate; the front end positioning head is a longitudinally arranged cylindrical structure and is arranged below the front end cutter at the front part above the frame plate; the reset cylinder is arranged near the rear end of the front end movable block on the frame plate, and the output shaft of the reset cylinder is over against the front end movable block.
The lower pressing plate is stressed to move downwards, so that the oblique pressing surface of the vertical pressing plate pushes the oblique guide surface of the front end movable block, and the front end movable block drives the front end cutter to move backwards; when the output shaft of the reset cylinder extends out, the front end movable block can be pushed to move forwards until the front end cutter resets.
Further, the front end processing agency is still including the movable block cap with the front end movable block shroud, and the both sides of front end movable block have 2 plugs that the symmetry set up, and the plug that corresponds the front end movable block on the movable block cap has rectangular shape slot, and the plug of front end movable block can follow the rectangular shape slot removal of movable block cap.
According to the optimized scheme, the lower front part of the upper frame plate of the middle frame is provided with 2 symmetrically arranged longitudinal supporting rods, and the longitudinal supporting rods are provided with a station moving mechanism and a pipe fitting clamping mechanism; the station moving mechanism comprises a moving bottom plate, a transverse guide rod, a transverse screw rod, a transverse moving block, a transverse moving driving motor and a longitudinal moving driving cylinder.
The transverse screw and the transverse guide rod are sequentially arranged on the moving base plate in a front-back close manner, one end of the transverse moving block is in threaded connection with the transverse screw, the other end of the transverse moving block is movably arranged on the transverse guide rod, and an output shaft of the transverse moving drive motor is coaxially connected with the transverse screw and can drive the transverse screw to rotate so as to enable the transverse moving block to move along the transverse guide rod; the movable bottom plate is movably arranged on the 2 longitudinal supporting rods.
The longitudinal movement driving cylinder is arranged below the moving bottom plate and fixedly connected with the moving bottom plate, the tail end of an output shaft of the longitudinal movement driving cylinder is fixedly connected to the position close to a frame plate of the rack, and the longitudinal movement driving cylinder can drive the moving bottom plate to move along the longitudinal supporting rod to enable the transverse guide rod, the transverse screw rod, the transverse moving block and the transverse movement driving motor to synchronously move along the longitudinal supporting rod.
The pipe fitting clamping mechanism comprises a clamping head and a clamping head cylinder, the clamping head is composed of 2 clamping plates movably hinged in the middle, the clamping head cylinder is arranged in front of the clamping head, an output shaft of the clamping head cylinder is opposite to the clamping head, and when the output shaft of the clamping head cylinder extends out, the rear ends of the 2 clamping plates can be close to each other; the pipe fitting clamping mechanism can be driven by the longitudinal movement driving cylinder to move longitudinally along the longitudinal supporting rod and can also be driven by the transverse movement driving motor to move transversely along the transverse guide rod.
Furthermore, the longitudinal support rod is connected with a frame plate of the frame through a longitudinal guide rod, the longitudinal guide rod is fixedly connected with the frame plate, the front end of the longitudinal guide rod is in threaded connection with a longitudinal screw rod, one end of the longitudinal support rod is connected to the longitudinal guide rod, the other end of the longitudinal support rod is in threaded connection with the longitudinal screw rod, the longitudinal support rod can move back and forth along the longitudinal guide rod by rotating the longitudinal screw rod, and then the distance between the pipe fitting clamping mechanism and the frame plate of the frame is adjusted.
According to the technical scheme, the utility model discloses near middle-frame plate is kept away from one side of back spot facing work mechanism and is equipped with feed mechanism, feed mechanism including anterior feeding guide arm, rear portion feeding guide arm and feeding slide, the symmetry sets up around anterior feeding guide arm and the rear portion feeding guide arm and forms the feeding guide frame.
The tail end of the front feeding guide rod is positioned in the upper front of the frame plate and close to the station moving mechanism, the tail end of the front feeding guide rod is positioned in the feeding guide frame and is movably provided with a longitudinal telescopic rod, and the outer wall of the longitudinal telescopic rod is provided with a pipe fitting positioning groove.
The tail end of the rear feeding guide rod is close to the frame plate, the tail end of the rear feeding guide rod is positioned in the feeding guide frame, and the feeding valve plate is movably hinged, and the top of the feeding valve plate can be driven by a valve plate cylinder to open or block the tail end of the feeding guide frame.
The feeding sliding plate is transversely movably arranged, the top of the feeding sliding plate is provided with a longitudinal clamping groove, one end of the feeding sliding plate is arranged below the tail end of the feeding guide frame, the other end of the feeding sliding plate is arranged on the frame plate, and the feeding sliding plate can be pushed by a sliding plate air cylinder to transversely move between the feeding guide frame and the frame plate.
The utility model has the following outstanding substantive characteristics and obvious progress:
1. the utility model discloses a preceding spot facing work mechanism and back spot facing work mechanism have realized the porous processing of pipe fitting, further set up vertical floating groove through front end processing agency on the trompil of pipe fitting, play the effect that prevents the bolt and skid when the pipe fitting finished product carries out bolted connection. The utility model further enables the pipe clamping mechanism to clamp the pipe to continuously move to a plurality of processing stations through the cooperation of the station moving mechanism and the pipe clamping mechanism, thereby realizing the automatic control in the multi-hole processing process of the pipe; and further realize the continuous, automatic and positioning feeding of the pipe fittings through the feeding mechanism.
2. The utility model discloses an automatic control is high, need not manual operation again after the pipe fitting gets into feed mechanism, can realize the removal that corresponds the part through regulating and controlling each cylinder to and can realize the rotation that corresponds the part through regulating and controlling each motor, and then reach regulation and control purposes such as displacement, have the characteristics of processing fast, efficient, still have automatic control system height, the controllability is strong and the characteristics of processing good quality stability.
Detailed Description
The present invention will be further explained with reference to the accompanying drawings.
Examples
Referring to fig. 1 to 9, a multi-hole pipe processing apparatus includes a frame 1, a feeding mechanism, a station moving mechanism, a pipe clamping mechanism, a front end processing mechanism, a front hole processing mechanism, and a rear hole processing mechanism.
The frame 1 comprises a frame plate 11, vertical guide pillars 12 and a lower press plate 13, wherein the frame plate 11 of the frame 1 is symmetrically provided with 2 vertical guide pillars 12, the lower press plate 13 is positioned above the frame plate 11, two ends of the lower press plate are respectively movably sleeved on the 2 vertical guide pillars 12, and the lower press plate 13 can move up and down above the frame plate 11 along the vertical guide pillars 12.
As shown in fig. 6 and 7, the front end processing mechanism includes a vertical pressing plate 7, a front end movable block 71, a front end cutter 72, a front end positioning head 73 and a reset cylinder 74, the vertical pressing plate 7 is a vertically arranged plate-shaped structure and is arranged at the lower rear part of the lower pressing plate 13, and the lower rear end of the vertical pressing plate 7 gradually narrows towards the lower front end, so that the lower part of the vertical pressing plate 7 has an inclined pressing surface 70; the front end movable block 71 is longitudinally movably arranged above the frame plate 11, the rear end of the front end movable block is provided with an oblique guide surface 710 matched with the oblique pressing surface 70 of the vertical pressing plate 7, the front end cutter 72 is of a plate-shaped structure obliquely arranged on the bottom of the front end movable block 71, and the knife edge end of the front end cutter is positioned at the front part above the frame plate 11; the front end positioning head 73 is a longitudinally arranged cylindrical structure and is arranged below the front end cutter 72 at the front part above the frame plate 11; the reset cylinder 74 is arranged near the rear end of the front end movable block 71 on the frame plate 11, and the output shaft of the reset cylinder is arranged opposite to the front end movable block 71;
the downward movement of the lower pressing plate 13 under stress can make the oblique pressing surface 70 of the vertical pressing plate 7 push the oblique guide surface 710 of the front end movable block 71, so that the front end movable block 71 drives the front end cutter 72 to move backwards; when the output shaft of the reset cylinder 74 extends, the front end movable block 71 can be pushed to move forwards until the front end cutter 72 is reset.
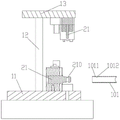
Referring to fig. 8, the front hole machining mechanism includes a front hole cutter 2, a front hole positioning head 21, and a movable block cover 75. The front hole cutter 2 and the front hole positioning head 21 are correspondingly arranged up and down, the front hole cutter 2 is a vertically arranged cylindrical structure and is arranged in the front portion of the lower pressing plate 13, the front hole positioning head 21 is a longitudinally arranged cylindrical structure and is arranged in the front portion of the upper portion of the frame plate 11, a front processing hole 211 which is right opposite to the front hole cutter 2 is arranged on the front hole positioning head 21, and the lower pressing plate 13 can move downwards under the stress to enable the front hole cutter 2 to be inserted into the front processing hole 211 of the front hole positioning head 21.
The movable block cover 75 covers the front movable block 71, 2 plugs 711 symmetrically arranged on two sides of the front movable block 71 are arranged on two sides of the movable block cover 75, the plug 711 corresponding to the front movable block 71 on the movable block cover 75 is provided with a long strip-shaped slot 751, and the plug 711 of the front movable block 71 can move along the long strip-shaped slot 751 of the movable block cover 75.
As shown in fig. 9, the rear hole machining mechanism includes a rear hole positioning upper block 3, a rear hole positioning lower block 4, a movable cutter assembly, and a cutter returning mechanism. The rear hole positioning upper block 3 is arranged at the lower front part of the lower pressure plate 13, and the bottom of the rear hole positioning upper block is provided with an arc-shaped positioning upper groove 31 which is arranged longitudinally.
The arc location lower groove 41 that the top that the frame plate 11 was located to piece 4 was anterior, its top in the back hole location has vertical setting has, and the arc location upper groove 31 corresponds the setting from top to bottom with the arc location lower groove 41, has the processing back hole 42 of vertical setting in the arc location lower groove 41.
The movable cutter component comprises a cutter mounting block 51, a cylindrical mounting head 52 and a rear hole cutter 5, the cutter mounting block 51 is vertically and movably arranged at the rear part of the rear hole positioning lower block 4 above the frame plate 11, the bottom of the cutter mounting block movably penetrates through the frame plate 11, the cylindrical mounting head 52 is longitudinally arranged at the front part of the cutter mounting block 51, and the rear hole cutter 5 is a vertically arranged cylindrical structure which is arranged on the cylindrical mounting head 52 and is opposite to a processed rear hole 42 of the rear hole positioning lower block 4.
The cutter reset mechanism comprises a reset fixed plate 6, a reset movable plate 61 and a reset spring 62, wherein the reset fixed plate 6 is fixedly arranged below the frame plate 11, the reset movable plate 61 is movably arranged between the frame plate 11 and the reset fixed plate 6 and is positioned below the bottom of the cutter mounting block 51 of the movable cutter assembly, and the reset spring 62 is arranged between the reset fixed plate 6 and the reset movable plate 61.
The tool mounting block 51 of the movable tool assembly is forced to move downwards, the reset movable plate 61 can be pushed to move downwards to enable the reset spring 62 of the tool reset mechanism to compress and store force, and meanwhile, the rear hole tool 5 moves downwards and is inserted into the rear processing hole 42 of the rear hole positioning lower block 4; the reset spring 62 is extended to reset and can push the reset movable plate 61 to move upwards so that the cutter mounting block 51 and the rear hole cutter 5 move upwards to reset.
2 longitudinal supporting rods 14 which are symmetrically arranged are arranged at the lower front part of an upper frame plate 11 of the frame 1, and the station moving mechanism and the pipe fitting clamping mechanism are arranged on the longitudinal supporting rods 14.
As shown in fig. 5, the station moving mechanism includes a moving bottom plate 8, a transverse guide rod 81, a transverse screw 82, a transverse moving block 83, a transverse moving drive motor 84, and a longitudinal moving drive cylinder 85.
The transverse screw 82 and the transverse guide rod 81 are sequentially arranged on the moving bottom plate 8 in a front-back approaching manner, one end of the transverse moving block 83 is in threaded connection with the transverse screw 82, the other end of the transverse moving block is movably arranged on the transverse guide rod 81, and an output shaft of the transverse moving drive motor 84 is coaxially connected with the transverse screw 82 and can drive the transverse screw 82 to rotate so as to enable the transverse moving block 83 to move along the transverse guide rod 81; the movable bottom plate 8 is movably arranged on 2 longitudinal struts 14.
The longitudinal movement driving cylinder 85 is arranged below the moving bottom plate 8 and fixedly connected with the moving bottom plate 8, the tail end of an output shaft of the longitudinal movement driving cylinder 85 is fixedly connected to the position close to the frame plate 11 of the machine frame 1, and the longitudinal movement driving cylinder 85 can drive the moving bottom plate 8 to move along the longitudinal support rod 14, so that the transverse guide rod 81, the transverse screw 82, the transverse moving block 83 and the transverse movement driving motor 84 synchronously move along the longitudinal support rod 14.
The pipe fitting clamping mechanism comprises a clamping head 86 and a clamping head cylinder 87, wherein the clamping head 86 is composed of 2 clamping plates 861 movably hinged to the middle part, the clamping head cylinder 87 is arranged in front of the clamping head 86, the output shaft of the clamping head cylinder 87 faces the clamping head 86, and when the output shaft of the clamping head cylinder 87 extends out, the rear ends of the 2 clamping plates 861 can be close to each other; the tube gripping mechanism can be driven by a longitudinal movement driving cylinder 85 to move longitudinally along the longitudinal support rod 14 and can also be driven by a transverse movement driving motor 84 to move transversely along the transverse guide rod 81.
The longitudinal support rod 14 is connected with a frame plate 11 of the frame 1 through a longitudinal guide rod 15, the longitudinal guide rod 15 is fixedly connected with the frame plate 11, the front end of the longitudinal guide rod 15 is in threaded connection with a longitudinal screw rod 16, one end of the longitudinal support rod 14 is connected to the longitudinal guide rod 15, the other end of the longitudinal support rod 14 is in threaded connection with the longitudinal screw rod 16, the longitudinal support rod 14 can move back and forth along the longitudinal guide rod 15 by rotating the longitudinal screw rod 16, and therefore the distance between the pipe fitting clamping mechanism and the frame plate 11 of the frame 1 is adjusted.
As shown in fig. 1 and 2, the front end processing mechanism, the front hole processing mechanism, and the rear hole processing mechanism are sequentially provided at intervals. A feeding mechanism is arranged on one side, close to the front end machining mechanism, of the frame plate 11 on the machine frame 1, the feeding mechanism comprises a front feeding guide rod 91, a rear feeding guide rod 92 and a feeding sliding plate 9, and the front feeding guide rod 91 and the rear feeding guide rod 92 are symmetrically arranged front and back to form a feeding guide frame.
The tail end of the front feeding guide rod 91 is positioned at the upper front part of the frame plate 11 and close to the station moving mechanism, the tail end of the front feeding guide rod is movably provided with a longitudinal telescopic rod 911 in the feeding guide frame, and the outer wall of the longitudinal telescopic rod 911 is provided with a pipe fitting positioning groove 912 as shown in fig. 3.
The rear feeding guide rod 92 has its end near the frame plate 11 and its end in the feeding guide frame movably hinged with a feeding valve plate 921, the top of the feeding valve plate 921 can be driven by a valve plate cylinder 922 to open or close the end of the feeding guide frame, as shown in fig. 4. The feeding sliding plate 9 is transversely movably arranged, the top of the feeding sliding plate is provided with a longitudinal clamping groove 90, one end of the feeding sliding plate 9 is arranged below the tail end of the feeding guide frame, the other end of the feeding sliding plate 9 is arranged on the frame plate 11, and the feeding sliding plate 9 can be pushed by a sliding plate cylinder 901 to transversely move between the feeding guide frame and the frame plate 11.
The utility model discloses a theory of operation does:
the pipe fitting 101 enters from the feeding guide frame of the feeding mechanism, the feeding valve plate 921 can prevent the pipe fitting 101 from suspending at the tail end of the feeding guide frame, the longitudinal telescopic rod 911 is inserted into the tail end of the pipe fitting 101, and the position of the pipe fitting 101 is adjusted by matching the groove position preset on the pipe wall of the tail end of the pipe fitting 101 with the pipe fitting positioning groove 912, so that the pipe fitting 101 can enter the subsequent procedures at the same position. Then, the feed valve plate 921 is opened to drop the pipe 101 into the longitudinal slot 90 of the feed slide 9, and the slide cylinder 901 pushes the feed slide 9 to feed the pipe 101 to the vicinity of the front end processing mechanism
Subsequently, the station moving mechanism drives the pipe clamping mechanism to move longitudinally through the longitudinal movement driving cylinder 85 and drives the pipe clamping mechanism to move transversely through the transverse movement driving motor 84, so that the pipe clamping mechanism moves to the 4 stations right in front of the feeding sliding plate 9, the front end processing mechanism, the front hole processing mechanism and the rear hole processing mechanism in sequence.
First, at the station of the feeding slide plate 9, the longitudinal movement driving cylinder 85 moves backward before the pipe clamping mechanism, the opened collet 86 clamps the pipe 101 at the station of the feeding slide plate 9, then the collet cylinder 87 always abuts against the collet 86 to clamp the pipe 101, and then the longitudinal movement driving cylinder 85 drives the pipe clamping mechanism to move forward to clamp the pipe 101 on the feeding slide plate 9.
Then, the traverse driving motor 84 drives the pipe clamping mechanism to move transversely to the station of the front end processing mechanism, the longitudinal movement drives the cylinder 85 to move backwards, the end of the pipe 101 is sleeved on the front end positioning head 73 of the front end processing mechanism, the lower press plate 13 is driven by an external pressure device such as a punch press, an oil press and the like to press downwards, the oblique press surface 70 of the vertical press plate 7 pushes the oblique guide surface 710 of the front end movable block 71, the front end movable block 71 drives the front end cutter 72 to move backwards, and a longitudinal floating groove 1011 is processed on the end of the pipe 101. Then, the lower press plate 13 is forced to move upwards, and the longitudinal movement driving cylinder 85 drives the pipe clamping mechanism to move forwards, so that the pipe 101 is retreated from the front end positioning head 73, as shown in fig. 6 and 7.
Then, the traverse driving motor 84 drives the pipe clamping mechanism to move transversely to the front hole machining mechanism station, the longitudinal driving cylinder 85 drives the front pipe clamping mechanism to move backwards, the end portion of the pipe 101 is sleeved on the front hole positioning head 21 of the front hole machining mechanism, the lower pressing plate 13 is pressed downwards under the stress, the front hole cutter 2 is pressed into the pipe 101 to be inserted into a machining front hole 211 on the front hole positioning head 21, and a front hole 1012 is machined in a longitudinal floating groove 1011 on the end portion of the pipe 101. Then, the lower press plate 13 is forced to move upwards, and the longitudinal movement driving cylinder 85 drives the pipe clamping mechanism to move forwards, so that the pipe 101 is pulled upwards by the front hole positioning head 21, as shown in fig. 8.
Finally, the traverse driving motor 84 drives the pipe clamping mechanism to move transversely to the rear hole machining mechanism station, the longitudinal movement drives the cylinder 85 to move backwards and drive the front pipe clamping mechanism to sleeve the end of the pipe 101 on the cylindrical mounting head 52 of the rear hole machining mechanism, the lower pressing plate 13 is pressed to the cutter mounting block 51 under the force of the lower pressing plate, and then the rear hole cutter 5 moves downwards and presses the end of the pipe 101 until the rear hole cutter 5 penetrates out of the end of the pipe 101, and then the rear hole cutter is inserted into the rear machining hole 42 of the rear hole positioning lower block 4, and a rear hole 1013 is machined below the front hole 1012 on the end of the pipe 101. Thereafter, the lower platen 13 is forced to move upward, and the vertical movement driving cylinder 85 drives the tube holding mechanism to move forward, so that the tube 101 is withdrawn from the column-shaped mounting head 52, as shown in fig. 9. The output shaft of the collet cylinder 87 of the tube gripping mechanism moves away from the collet 86 causing the collet 86 to release the tube 101 and finish the process.