CN216611660U - Automatic drilling and riveting assembly tool for aircraft panel - Google Patents
Automatic drilling and riveting assembly tool for aircraft panel Download PDFInfo
- Publication number
- CN216611660U CN216611660U CN202123387439.9U CN202123387439U CN216611660U CN 216611660 U CN216611660 U CN 216611660U CN 202123387439 U CN202123387439 U CN 202123387439U CN 216611660 U CN216611660 U CN 216611660U
- Authority
- CN
- China
- Prior art keywords
- automatic drilling
- riveting
- support frame
- main framework
- assembly
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Landscapes
- Drilling And Boring (AREA)
Abstract
The utility model discloses an automatic drilling and riveting assembly tool for an aircraft panel, which solves the problems of low assembly efficiency and large machining error of the conventional automatic drilling and riveting assembly tool. The technical scheme adopted by the utility model is as follows: the automatic drilling and riveting assembly tool for the aircraft panel comprises a tool main framework and an automatic drilling and riveting support frame, wherein the tool main framework is of a frame structure, a frame positioner, a stringer positioner and a skin inner clamping plate are fixedly arranged on the tool main framework, two slide rails are arranged on one side of the tool main framework, which is used for being matched with the automatic drilling and riveting support frame, and a slide rail assembly is arranged on each slide rail; the automatic drilling and riveting support frame is of a frame structure, two sides of the automatic drilling and riveting support frame are respectively provided with a sliding rail joint and are arranged in a sliding rail assembly, the sliding rail joints are matched with the sliding rail assembly, the automatic drilling and riveting support frame is provided with a drilling and riveting machine joint and a skin inner clamping plate, and the skin inner clamping plate is provided with a stringer locator and a skin lug locator. The automatic drilling and riveting machine is used for automatic drilling and riveting of the aircraft panel, and can reduce the times and the period of clamping the aircraft panel.
Description
Technical Field
The utility model relates to the technical field of aircraft manufacturing, in particular to an assembly tool for automatic drilling and riveting of an aircraft panel.
Background
Under the continuously developed form of aerospace industry, the automatic drilling and riveting technology is widely applied, and the automatic drilling and riveting rate in the assembly of airplane structures is gradually improved. There are two requirements before the automatic drilling and riveting of aircraft wallboard products: firstly, pre-assembly is carried out on an assembly type frame; secondly, secondary positioning is carried out on the automatic drilling and riveting support frame after pre-assembly.
The automatic drilling and riveting assembly tool comprises an automatic drilling and riveting support frame and an assembly fixture. At present, an automatic drilling and riveting support frame and an assembly fixture are independently designed and manufactured, and a connecting interface is not arranged between the automatic drilling and riveting support frame and the assembly fixture. Before the automatic drilling and riveting of the aircraft panel, the aircraft panel needs to be pre-assembled on an assembly type frame, then the pre-assembled aircraft panel is transported to an automatic drilling and riveting support frame of an automatic drilling and riveting machine to be secondarily positioned, and finally automatic drilling and riveting work is carried out. The whole process needs to utilize the automatic drilling and riveting support frame to reposition the aircraft wallboard, and the aircraft wallboard needs secondary dismouting, and this not only leads to the automatic drilling and riveting machining error of aircraft wallboard, has still reduced assembly efficiency, has increased production cycle.
SUMMERY OF THE UTILITY MODEL
The utility model provides an automatic drilling and riveting assembly tool for an aircraft panel, and solves the problems of low assembly efficiency and large machining error of the conventional automatic drilling and riveting assembly tool.
The technical scheme adopted by the utility model is as follows: the automatic drilling and riveting assembly tool for the aircraft panel comprises a tool main framework and an automatic drilling and riveting support frame, wherein the tool main framework is of a frame structure, support legs are arranged at the bottom of the tool main framework, a frame positioner, a stringer positioner and a skin inner clamping plate are fixedly arranged on the tool main framework, two slide rails are arranged on one side of the tool main framework, which is matched with the automatic drilling and riveting support frame, the two slide rails are equal in installation height, are parallel to each other and are horizontally arranged, and each slide rail is provided with a slide rail assembly; the automatic drilling and riveting support frame is of a frame structure, two sides of the automatic drilling and riveting support frame are respectively provided with a sliding rail joint and are arranged in a sliding rail assembly, the sliding rail joints are matched with the sliding rail assembly, the automatic drilling and riveting support frame is provided with a drilling and riveting machine joint and a skin inner clamping plate, and the skin inner clamping plate is provided with a stringer locator and a skin lug locator.
Further, the method comprises the following steps: the tool main framework is used for arranging at least two guide pins on one side matched with the automatic drilling and riveting support frame, the axial direction of each guide pin is parallel to the sliding direction of the corresponding sliding rail, and the automatic drilling and riveting support frame is used for arranging pin holes matched with the guide pins on one side matched with the tool main framework.
Specifically, the method comprises the following steps: the upper part and the lower part of the tool main framework are respectively provided with a guide pin.
Further, the method comprises the following steps: the frock main frame sets up three vertical supports of left, well, right side, and the upper and lower parts of three vertical supports of group are respectively through two sets of crossbeam welded connection, and the clamp plate subassembly is all connected to the crossbeam of upper and lower part, and frame locator and stringer locator are all installed between the clamp plate subassembly of upper and lower part.
Further, the method comprises the following steps: the automatic drilling and riveting support frame is of an aluminum alloy welding frame structure.
The utility model has the beneficial effects that: the utility model realizes the integration of the main framework of the tool and the automatic drilling and riveting frame, can be well combined with the automatic drilling and riveting machine, avoids the secondary positioning of the aircraft panel on the automatic drilling and riveting frame, reduces the times and the period of the clamping of the aircraft panel and improves the assembly efficiency. And a guide pin and a pin hole are arranged between the tool main framework and the automatic drilling and riveting support frame, so that the automatic drilling and riveting support frame is convenient to position on the tool main framework.
Drawings
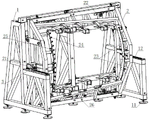
Fig. 1 is a schematic structural diagram of the automatic drilling and riveting assembly tool for the aircraft panel.
Fig. 2 is an enlarged view of a portion of the slide rail assembly of fig. 1.
Fig. 3 is a schematic structural view of the slide rail assembly of fig. 2.
Fig. 4 is a schematic structural diagram of the main skeleton of the tool in fig. 1.
Fig. 5 is a schematic structural view of the automatic drill-rivet support frame in fig. 1.
Fig. 6 is a partially enlarged view of fig. 5.
Reference numerals: the tool comprises a tool main framework 1, support legs 11, a slide rail 12, a guide pin 13, an automatic drilling and riveting support frame 2, a slide rail joint 21, a drilling and riveting machine joint 22, a skin inner clamping plate 23, a stringer positioner 24, a skin lug positioner 25, a pin hole 26 and a slide rail assembly 3.
Detailed Description
The utility model will be further explained with reference to the drawings.
As shown in fig. 1-6, the automatic drilling and riveting assembly tool for the aircraft panel comprises a tool main framework 1 and an automatic drilling and riveting support frame 2. The main framework 1 of the tool is of a frame structure and preferably consists of metal sections, and the metal sections are welded or connected through bolts. The tool main framework 1 comprises at least two groups of vertical supports, supporting legs 11 are arranged at the bottoms of the vertical supports, and the vertical supports are connected through a cross beam. For example, referring to fig. 1 and 4, the tool main frame 1 is provided with three groups of vertical supports, namely a left vertical support, a middle vertical support and a right vertical support, the bottoms of the vertical supports are respectively provided with support legs 11, the upper part and the lower part of the three groups of vertical supports are respectively connected through two groups of cross beams in a welding manner, so that the three groups of vertical supports are connected through four cross beams, and a stable integral structure is formed. The main framework 1 of the tooling is fixedly provided with a frame positioner, a stringer positioner and a skin inner-type clamping plate, which are not shown in fig. 1 and 4. For example, the upper and lower beams each connect the card assemblies, and the frame locators and stringer locators are each mounted between the upper and lower card assemblies.
The tool main framework 1 is used for arranging two slide rails 12 on one side matched with the automatic drilling and riveting support frame 2, the installation heights of the two slide rails 12 are equal, parallel to each other and horizontally arranged, and each slide rail 12 is provided with one slide rail assembly 3. The two slide rails 12 are preferably disposed on two sides of the tool main frame 1, for example, on the left and right vertical supports, respectively. The slide rail assembly 3 is conventional and can run linearly along the slide rail 12, such as a hiwin linear slide rail.
The automatic drilling and riveting support frame 2 is of a frame structure and preferably consists of metal profiles, and the metal profiles are welded or connected through bolts. For example, the automatic drill-rivet support frame 2 is an aluminum alloy welding frame structure. Referring to fig. 1 and 5, the two sides of the automatic drilling and riveting support frame 2 are respectively provided with a sliding rail joint 21, and the sliding rail joints 21 are adapted to the sliding rail assemblies 3 and are used for being arranged in the sliding rail assemblies 3, so that the automatic drilling and riveting support frame 2 can linearly slide along the two sliding rails 12. The automatic drilling and riveting support frame 2 is provided with a drilling and riveting machine connector 22 and a skin inner type clamping plate 23, the drilling and riveting machine connector 22 is used for connecting the automatic drilling and riveting machine, for example, the automatic drilling and riveting support frame 2 is provided with four drilling and riveting machine connectors 22 which are respectively used for connecting with a cylinder clamp holder of the automatic drilling and riveting machine; the skin in-lay strap 23 is provided with stringer locators 24 and skin tab locators 25, see fig. 1, 5 and 6.
In order to facilitate the positioning of the automatic drilling and riveting support frame 2 on the tool main framework 1, one side of the tool main framework 1, which is used for being matched with the automatic drilling and riveting support frame 2, is provided with at least two guide pins 13, and the axial directions of the guide pins 13 are parallel to the sliding direction of the sliding rail 12. Meanwhile, one side of the automatic drilling and riveting support frame 2, which is used for being matched with the tool main framework 1, is provided with a pin hole 26 matched with the guide pin 13. For example, the upper and lower portions of the tool main frame 1 are respectively provided with one guide pin 13, and the corresponding positions of the automatic drill-rivet support frame 2 are respectively provided with one pin hole 26. The slide rail joint 21 of the automatic drilling and riveting support frame 2 is arranged on the slide rail component 3 on the slide rail 12 of the tool main framework 1, and the guide pin 13 is positioned in the pin hole 26.
After the airplane wallboard is positioned, sealed and pre-connected, the airplane wallboard and the automatic drilling and riveting frame 2 are separated from the sliding rail assembly 3 together, so that the automatic drilling and riveting frame 2 is quickly separated from the main framework 1 of the tool, and then the airplane wallboard and the automatic drilling and riveting frame 2 are transported to an automatic drilling and riveting station together for automatic drilling and riveting, so that the times and the period of airplane wallboard clamping are reduced.
Claims (5)
1. Automatic drilling and riveting assembly fixture for aircraft panels comprises a fixture main framework (1) and an automatic drilling and riveting support frame (2), wherein the fixture main framework (1) is of a frame structure, the bottom of the fixture main framework (1) is a support leg (11), the fixture main framework (1) is fixedly provided with a frame positioner, a stringer positioner and a skin inner clamping plate, and the automatic drilling and riveting assembly fixture is characterized in that: one side, used for being matched with the automatic drilling and riveting support frame (2), of the tool main framework (1) is provided with two sliding rails (12), the two sliding rails (12) are equal in installation height, parallel to each other and horizontally arranged, and each sliding rail (12) is provided with a sliding rail assembly (3); the automatic drilling and riveting support frame (2) is of a frame type structure, two sides of the automatic drilling and riveting support frame (2) are respectively provided with a sliding rail joint (21) and are arranged in a sliding rail assembly (3), the sliding rail joint (21) is matched with the sliding rail assembly (3), the automatic drilling and riveting support frame (2) is provided with a drilling and riveting machine joint (22) and a skin inner type clamping plate (23), and the skin inner type clamping plate (23) is provided with a long purlin positioner (24) and a skin lug positioner (25).
2. The automatic drilling and riveting assembly tool for the aircraft panel according to claim 1, characterized in that: the tool main framework (1) is used for arranging at least two guide pins (13) on one side matched with the automatic drilling and riveting support frame (2), the axial direction of each guide pin (13) is parallel to the sliding direction of the sliding rail (12), and the automatic drilling and riveting support frame (2) is used for arranging pin holes (26) matched with the guide pins (13) on one side matched with the tool main framework (1).
3. The automatic drilling and riveting assembly tool for the aircraft panel according to claim 2, characterized in that: the upper part and the lower part of the tool main framework (1) are respectively provided with a guide pin (13).
4. An automatic drilling and riveting assembly tool for an aircraft panel according to claim 1, 2 or 3, wherein: the fixture main framework (1) is provided with a left group of vertical supports, a middle group of vertical supports and a right group of vertical supports, the upper parts and the lower parts of the three groups of vertical supports are respectively connected through two groups of cross beams in a welding manner, the cross beams at the upper part and the lower part are all connected with the clamping plate assemblies, and the frame positioner and the stringer positioner are all installed between the clamping plate assemblies at the upper part and the lower part.
5. An automatic drilling and riveting assembly tool for an aircraft panel according to claim 1, 2 or 3, wherein: the automatic drilling and riveting support frame (2) is of an aluminum alloy welding frame structure.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202123387439.9U CN216611660U (en) | 2021-12-30 | 2021-12-30 | Automatic drilling and riveting assembly tool for aircraft panel |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202123387439.9U CN216611660U (en) | 2021-12-30 | 2021-12-30 | Automatic drilling and riveting assembly tool for aircraft panel |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN216611660U true CN216611660U (en) | 2022-05-27 |
Family
ID=81685311
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202123387439.9U Active CN216611660U (en) | 2021-12-30 | 2021-12-30 | Automatic drilling and riveting assembly tool for aircraft panel |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN216611660U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115946865A (en) * | 2023-02-28 | 2023-04-11 | 中航成飞民用飞机有限责任公司 | Assembly tool for righting integration of lower assembly of large airplane and construction method thereof |
| CN117697432A (en) * | 2023-11-29 | 2024-03-15 | 江西洪都航空工业集团有限责任公司 | Flexible platform for automatic drilling and riveting of robot |
| CN119590635A (en) * | 2024-11-22 | 2025-03-11 | 中航成飞民用飞机有限责任公司 | Assembly method of semi-enclosed bulkhead panel for aircraft nose |
| CN119871044A (en) * | 2025-03-25 | 2025-04-25 | 杭州艾美依航空制造装备有限公司 | Flexible positioning tool for wall plate for drilling and riveting |
-
2021
- 2021-12-30 CN CN202123387439.9U patent/CN216611660U/en active Active
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN115946865A (en) * | 2023-02-28 | 2023-04-11 | 中航成飞民用飞机有限责任公司 | Assembly tool for righting integration of lower assembly of large airplane and construction method thereof |
| CN115946865B (en) * | 2023-02-28 | 2023-05-12 | 中航成飞民用飞机有限责任公司 | Assembly fixture for righting integration of lower assembly of large aircraft and construction method of assembly fixture |
| CN117697432A (en) * | 2023-11-29 | 2024-03-15 | 江西洪都航空工业集团有限责任公司 | Flexible platform for automatic drilling and riveting of robot |
| CN119590635A (en) * | 2024-11-22 | 2025-03-11 | 中航成飞民用飞机有限责任公司 | Assembly method of semi-enclosed bulkhead panel for aircraft nose |
| CN119871044A (en) * | 2025-03-25 | 2025-04-25 | 杭州艾美依航空制造装备有限公司 | Flexible positioning tool for wall plate for drilling and riveting |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN111940977B (en) | Bogie frame manipulator welding fixture positioned by utilizing air spring guide post holes | |
| CN113579672A (en) | Movable clamping plate-based flexible wall plate pre-assembly tool and assembly method | |
| CN112497107B (en) | Pre-assembly method suitable for drilling and riveting of extra-large-diameter carrier rocket cabin section | |
| CN113305460A (en) | Automatic welding device and process method suitable for finned radiator oil collecting pipe | |
| CN102328231A (en) | Flexible clamp for numerical-control processing and application thereof | |
| CN212169493U (en) | Ultra-light aircraft fuselage steel pipe skeleton welding frock | |
| CN114523240A (en) | Rail vehicle side wall assembly welding frock | |
| CN111822976B (en) | Improved expansion press-fitting system and method thereof | |
| CN203726029U (en) | Cardboard type rapidly combined welding tool | |
| CN218657521U (en) | Tool for welding and positioning mounting seat of steering mechanism of agricultural robot | |
| CN216938246U (en) | Automatic drilling and riveting type tool for single wall board of airplane | |
| CN215316718U (en) | Rapid die changing universal tool for large part assembly welding clamp of railway passenger car | |
| CN206795202U (en) | A kind of rack top underframe crimp connection fixture | |
| CN214978789U (en) | Multi-vehicle type rolling window frame assembly welding jig | |
| CN213560769U (en) | Assembly welding fixing tool with multipoint accurate positioning function | |
| CN215154610U (en) | Rivet connection structure of composite board framework and framework with same | |
| CN213730146U (en) | Group welding tool for cross beam assembly in a skeleton car | |
| CN219465294U (en) | Helicopter fuselage truss welding fixture | |
| CN211761027U (en) | Water tank front beam installation auxiliary fixtures | |
| CN109318005B (en) | Luggage traction axle arm machine tool machining tool | |
| CN221389470U (en) | Modularized aluminum alloy framework assembly welding device | |
| CN222405601U (en) | A tool suitable for positioning parts | |
| CN223353337U (en) | A diversified construction hoist cage main channel steel machining tool | |
| CN205290239U (en) | Electric automobile girder welding jig | |
| CN218745781U (en) | Tool for welding and positioning mounting seat of walking mechanism of agricultural robot |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |