CN216544477U - Downward-pressing injection type mold - Google Patents
Downward-pressing injection type mold Download PDFInfo
- Publication number
- CN216544477U CN216544477U CN202123376536.8U CN202123376536U CN216544477U CN 216544477 U CN216544477 U CN 216544477U CN 202123376536 U CN202123376536 U CN 202123376536U CN 216544477 U CN216544477 U CN 216544477U
- Authority
- CN
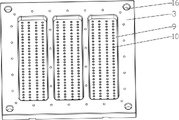
- China
- Prior art keywords
- template
- cavity
- injection
- group
- positioning
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000002347 injection Methods 0.000 title claims abstract description 59
- 239000007924 injection Substances 0.000 title claims abstract description 59
- 238000003825 pressing Methods 0.000 title description 2
- 238000001746 injection moulding Methods 0.000 claims abstract description 29
- 208000032544 Cicatrix Diseases 0.000 abstract description 2
- 231100000241 scar Toxicity 0.000 abstract description 2
- 230000037387 scars Effects 0.000 abstract description 2
- 238000009966 trimming Methods 0.000 abstract description 2
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 description 5
- 239000007788 liquid Substances 0.000 description 5
- 239000000741 silica gel Substances 0.000 description 5
- 229910002027 silica gel Inorganic materials 0.000 description 5
- 239000002994 raw material Substances 0.000 description 4
- 238000001816 cooling Methods 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 239000004033 plastic Substances 0.000 description 2
- 238000007789 sealing Methods 0.000 description 2
- 238000005520 cutting process Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000001125 extrusion Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
- 239000002699 waste material Substances 0.000 description 1
Images



Landscapes
- Moulds For Moulding Plastics Or The Like (AREA)
Abstract
The utility model discloses a lower-pressure injection type mold. The technical scheme adopted comprises the following steps: the injection molding machine comprises an upper template, an intermediate template, a lower template and an injection molding template which are sequentially arranged, wherein the upper end surface of the upper template is provided with a group of upper cavity convex cores which are arranged at intervals, the end surface of the intermediate template is provided with a group of intermediate grooves which are arranged at intervals, the lower end surface of the lower template is provided with a group of lower cavity convex cores which are arranged at intervals, the upper cavity convex cores are arranged in the intermediate grooves, gaps between the lower cavity convex cores form cavities of products, the bottom of the lower template is provided with injection molding cavities, the injection molding cavities are communicated with the cavities through injection molding holes, and the injection molding template upper end surface is provided with injection convex cores which are extruded in the injection molding cavities. The advantages are as follows: trimming is not needed, and only technological scars with unevenness of about 0.1mm are left at the bottom of the product.
Description
Technical Field
The utility model relates to an injection molding die.
Background
The traditional mold for injection molding of rubber or silica gel products (such as sealing rings, sheaths and the like) generally comprises an upper template, a lower template and a cavity module arranged between the upper template and the lower template, wherein the cavity module comprises a cavity male mold and a cavity female mold. After the die is closed, a gap between the cavity male die and the cavity female die forms a cavity of the product, then liquid plastic or rubber is injected into the cavity, and after cooling, the injection molding product is obtained. The traditional injection molding raw materials are all opened an upper template and put into pressure injection, and the defects existing in the mode are as follows: the injection molding product is connected with waste edges, further cutting is needed, the production efficiency is low, the raw materials are wasted, and the technical edges are arranged on the surface of the product, so that the sealing performance and the attractiveness are affected.
SUMMERY OF THE UTILITY MODEL
The utility model aims to provide a lower-pressure injection type mold.
In order to solve the above problems, the technical scheme adopted by the utility model comprises: the injection molding machine comprises an upper template, an intermediate template, a lower template and an injection molding template which are sequentially arranged, wherein the upper end surface of the upper template is provided with a group of upper cavity convex cores which are arranged at intervals, the end surface of the intermediate template is provided with a group of intermediate grooves which are arranged at intervals, the lower end surface of the lower template is provided with a group of lower cavity convex cores which are arranged at intervals, the upper cavity convex cores are arranged in the intermediate grooves, gaps between the lower cavity convex cores form cavities of products, the bottom of the lower template is provided with injection molding cavities, the injection molding cavities are communicated with the cavities through injection molding holes, and the injection molding template upper end surface is provided with injection convex cores which are extruded in the injection molding cavities.
The lower pressure injection type mould is characterized in that: and first prying die openings are formed in two ends of the pressure injection template, second prying die openings are formed in two ends of the lower template, and third prying die openings are formed in two ends of the upper template.
The lower pressure injection type mould is characterized in that: four corners of the pressure injection template are provided with first positioning columns, and the lower template is provided with first positioning holes matched with the first positioning columns in a positioning mode.
The lower pressure injection type mould is characterized in that: the edge of the upper end of the middle template is provided with a group of positioning grooves, and the upper template is provided with a group of positioning convex blocks matched with the positioning grooves in a positioning mode.
The lower pressure injection type mould is characterized in that: the upper end of the lower template is provided with a group of second positioning columns, and the middle template is provided with a group of second positioning holes matched with the second positioning columns in a positioning mode.
The lower pressure injection type mould is characterized in that: and the lower template is provided with injection holes corresponding to the side of each lower cavity convex core.
The lower pressure injection type mould is characterized in that: and a group of mutually communicated flow channels are arranged on the surface of the pressure injection convex core.
The lower pressure injection type mould is characterized in that: and the left side and the right side of the lower template corresponding to the convex core of each lower cavity are respectively provided with a pressure injection hole.
The down-pressure injection type die has the following advantages: liquid plastic is injected into a cavity of a product at the bottom of the lower template, and due to the fact that the top of the injection hole is only provided with a pinhole (about 0.1 mm), after the product is demoulded, trimming is not needed, and the product is only provided with process scars with unevenness of about 0.1mm at the bottom, so that production efficiency is improved, raw materials are saved, and the surface of the product is more smooth.
The utility model is further described below with reference to the accompanying drawings.
Drawings
FIG. 1 is an exploded view of a lower injection mold of the present invention;
FIG. 2 is a cross-sectional view of the lower injection mold of the present invention;
FIG. 3 is a schematic structural view of the upper die plate of the present invention;
FIG. 4 is a schematic structural view of an intermediate template according to the present invention;
FIG. 5 is a schematic structural view of the lower template of the present invention showing the top structure;
FIG. 6 is a schematic structural view of the lower template of the present invention showing the bottom structure;
fig. 7 is a schematic structural view of the injection molding plate of the present invention.
Detailed Description
Referring to fig. 1 to 7, the lower injection mold of the present invention comprises: the die comprises an upper die plate 1, a middle die plate 2, a lower die plate 3 and an injection die plate 4 which are arranged in sequence. The upper end face of the upper template 1 is provided with a group of upper cavity convex cores 5 which are arranged at intervals, the end face of the middle template 2 is provided with a group of hollow middle grooves 6 which are arranged at intervals, and the lower end face of the lower template 3 is provided with a group of lower cavity convex cores 7 which are arranged at intervals. And the convex core 7 of the cavity of the lower template 3 extends out of the hollow part of the middle groove 6 of the middle template 2. After the die is closed, a die cavity 8 of a product is formed by gaps among the upper die cavity convex core 5, the middle type groove 6 and the lower die cavity convex core 7. The bottom of the lower template 3 is provided with an injection cavity 9, the injection cavity 9 is communicated with the cavity 8 through a group of injection holes 10, and the upper end surface of the injection template 4 is provided with an injection convex core 11 extruded in the injection cavity 9. The injection hole 10 is small at the top and big at the bottom and takes the shape of a syringe. The injection cavities 9 are ideally 3 and arranged side by side, and the injection convex cores 11 are also 3 corresponding to the injection cavities. During injection molding, the silica gel raw material is placed into the pressure injection concave cavity 9, the melted liquid silica gel is pressure injected into the cavity 8 of the product through the extrusion of the pressure injection convex core 11 of the pressure injection template 4, and the injection molded product is obtained after cooling.
Preferably, the two ends of the pressure injection template 4 are provided with first prying die orifices 12, the two ends of the lower template 3 are provided with second prying die orifices 13, and the two ends of the upper template 1 are provided with third prying die orifices 14. Through setting up sled die orifice, make things convenient for the operator to realize the drawing of patterns with the template separation.
Preferably, four corners of the injection molding plate 4 are provided with first positioning posts 15, and the lower mold plate 3 is provided with first positioning holes 16 matched with the first positioning posts 15 in a positioning manner. The edge of the upper end of the middle template 2 is provided with a group of positioning grooves 17, and the upper template 1 is provided with a group of positioning lugs 18 which are matched with the positioning grooves 17 in a positioning way. A group of second positioning columns 19 is arranged at the upper end of the lower template 3, and a group of second positioning holes 20 matched with the second positioning columns 19 in a positioning mode are arranged on the middle template 2. Through the structure, the upper template 1, the middle template 2, the lower template 3 and the injection template 4 are accurately positioned, so that the precision of a product is ensured.
Preferably, the lower template 3 is provided with injection holes 10 corresponding to each lower cavity convex core 7. And finally, injection molding holes 10 are formed in the lower template 3 corresponding to the left side and the right side of each lower cavity convex core 7. Liquid silica gel can be more uniformly injected into the cavity 8 of the product, so that the surface of the product is more smooth.
Preferably, the surface of the injection molding convex core 11 is provided with a group of mutually communicated flow channels 21, and liquid silica gel can flow mutually on the surface of the injection molding convex core 11 through the flow channels 21, so that the injection molding is more uniform.
Although the present invention has been described with reference to the above embodiments, it will be understood by those skilled in the art that various changes in form and details may be made therein without departing from the spirit and scope of the utility model.
Claims (8)
1. A down-pressure injection mold, comprising: an upper template (1), a middle template (2), a lower template (3) and an injection template (4) which are arranged in sequence, the upper end surface of the upper template (1) is provided with a group of upper cavity convex cores (5) which are arranged at intervals, a group of hollow middle grooves (6) which are arranged at intervals are arranged on the end surface of the middle template (2), a group of lower cavity convex cores (7) which are arranged at intervals are arranged on the lower end surface of the lower template (3), the gaps among the upper cavity convex core (5), the middle groove (6) and the lower cavity convex core (7) form a cavity (8) of the product, the bottom of the lower template (3) is provided with an injection cavity (9), the injection cavity (9) is communicated with the cavity (8) through an injection hole (10), and the upper end surface of the injection molding template (4) is provided with an injection molding convex core (11) extruded in the injection molding concave cavity (9).
2. The lower-pressure injection mold of claim 1, wherein: and first prying die openings (12) are formed in two ends of the pressure injection template (4), second prying die openings (13) are formed in two ends of the lower template (3), and third prying die openings (14) are formed in two ends of the upper template (1).
3. The lower-pressure injection mold of claim 1, wherein: four corners of the pressure injection template (4) are provided with first positioning columns (15), and the lower template (3) is provided with first positioning holes (16) matched with the first positioning columns (15) in a positioning manner.
4. The lower-pressure injection mold of claim 1, wherein: the middle die plate is characterized in that a group of positioning grooves (17) are formed in the edge of the upper end of the middle die plate (2), and a group of positioning convex blocks (18) matched with the positioning grooves (17) in a positioning mode are arranged on the upper die plate (1).
5. The lower-pressure injection mold of claim 1, wherein: the upper end of the lower template (3) is provided with a group of second positioning columns (19), and the middle template (2) is provided with a group of second positioning holes (20) which are matched with the second positioning columns (19) in a positioning mode.
6. The lower-pressure injection mold of claim 1, wherein: and an injection hole (10) is formed beside each lower die cavity convex core (7) of the lower template (3).
7. The lower-pressure injection mold of claim 1, wherein: and a group of mutually communicated flow channels (21) are arranged on the surface of the injection convex core (11).
8. The lower-pressure injection mold of claim 6, wherein: and pressure injection holes (10) are formed in the left side and the right side of the lower template (3) corresponding to each lower cavity convex core (7).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202123376536.8U CN216544477U (en) | 2021-12-30 | 2021-12-30 | Downward-pressing injection type mold |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202123376536.8U CN216544477U (en) | 2021-12-30 | 2021-12-30 | Downward-pressing injection type mold |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN216544477U true CN216544477U (en) | 2022-05-17 |
Family
ID=81558979
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202123376536.8U Active CN216544477U (en) | 2021-12-30 | 2021-12-30 | Downward-pressing injection type mold |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN216544477U (en) |
-
2021
- 2021-12-30 CN CN202123376536.8U patent/CN216544477U/en active Active
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN112060508B (en) | A multi-color car light injection mold with rotary demoulding | |
| CN221271882U (en) | Anti-deformation plastic product injection molding die | |
| CN221067087U (en) | Precise injection mold for aluminum | |
| CN216635205U (en) | Waterproof ring mould | |
| CN212446122U (en) | Injection mold | |
| CN216609863U (en) | Mould with vertical structure | |
| CN214111329U (en) | Synchronous forming die for plastic bottom cover and reflecting cover | |
| CN219055182U (en) | High-efficiency multi-point injection molding mold | |
| CN211993980U (en) | Multicolor silica gel forming die | |
| CN211891759U (en) | Injection molding device of silica gel sealing member | |
| CN212171180U (en) | Injection mold who possesses exhaust overflow structure | |
| CN218462788U (en) | A dual-channel injection mold for notebook keys | |
| CN210940151U (en) | Small-hole self-detaching mold for rubber part forming | |
| CN223314397U (en) | An injection type runnerless molding mold | |
| CN221271889U (en) | Efficient ribbon forming die | |
| CN210011265U (en) | Plastic panel injection mold for water purifier | |
| CN223199439U (en) | Plastic daily necessities overmolding mold | |
| CN222521919U (en) | Garbage can mold with balanced hot runner system | |
| CN222079950U (en) | A hexagonal hole battery shell injection mold | |
| CN112476991A (en) | Demoulding device without external power for injection mould | |
| CN221089824U (en) | High-efficiency single-cavity and multi-cavity detachable injection mold | |
| CN220841264U (en) | Runner system of injection mould | |
| CN223630874U (en) | A pen insert injection mold | |
| CN217395609U (en) | Injection mold for small products | |
| CN214353841U (en) | Reusable injection mold for medical instrument production |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |