CN216262999U - Multi-station progressive die for rotating shaft bracket - Google Patents
Multi-station progressive die for rotating shaft bracket Download PDFInfo
- Publication number
- CN216262999U CN216262999U CN202122623445.3U CN202122623445U CN216262999U CN 216262999 U CN216262999 U CN 216262999U CN 202122623445 U CN202122623445 U CN 202122623445U CN 216262999 U CN216262999 U CN 216262999U
- Authority
- CN
- China
- Prior art keywords
- template
- station
- core
- punch
- embedded
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 230000000750 progressive effect Effects 0.000 title claims abstract description 15
- 238000005452 bending Methods 0.000 claims abstract description 42
- 238000004080 punching Methods 0.000 claims description 6
- 238000000034 method Methods 0.000 description 7
- 238000010276 construction Methods 0.000 description 5
- 230000007423 decrease Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
Images





Landscapes
- Manufacture Of Motors, Generators (AREA)
- Iron Core Of Rotating Electric Machines (AREA)
Abstract
The utility model discloses a rotating shaft support multi-station progressive die with higher stamping precision. The technical scheme adopted by the device comprises an upper template, a lower template, and a first bending station, a second bending station and a third bending station which are sequentially arranged in the upper template and the lower template; the first bending station comprises two opposite first upper cores embedded on the upper template and two opposite first lower cores embedded on the lower template, a 90-degree punch is arranged on the inner side of the lower end of each first upper core, and a 90-degree groove matched with the 90-degree punch is arranged on the inner side of the upper end of each first lower core. The third bending station comprises two third upper cores which are embedded on the upper template and two third lower cores which are embedded on the lower template, a square punch is arranged at the lower end of each third upper core, and a square groove matched with the square punch is formed in the inner side of the upper end of each third lower core.
Description
Technical Field
The utility model relates to a multi-station progressive die.
Background
The pivot support has the support arm that the bottom plate and bottom plate both ends formed through 3 continuous 90 degrees bends, and it has the screw hole to stretch in the bottom plate bottom, is equipped with the shaft hole on the support arm, is connected with the pivot through the shaft hole. The rotating shaft support can be widely applied to equipment such as a circuit breaker. The punching press of 90 degrees departments of bending of traditional counter shaft support, generally for direct one-step stamping forming, stamping forming's precision is lower, destroys the metallographic structure of section bar easily simultaneously, leads to the intensity decline of counter shaft support, is not conform to and uses on the equipment of present high accuracy.
SUMMERY OF THE UTILITY MODEL
The utility model aims to provide a rotating shaft support multi-station progressive die with higher stamping precision.
In order to solve the problems, the technical scheme adopted by the utility model comprises an upper template, a lower template, and a first bending station, a second bending station and a third bending station which are sequentially arranged in the upper template and the lower template;
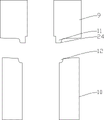
the first bending station comprises two opposite first upper cores embedded on the upper template and two opposite first lower cores embedded on the lower template, a 90-degree punch is arranged on the inner side of the lower end of each first upper core, and a 90-degree groove matched with the 90-degree punch is arranged on the inner side of the upper end of each first lower core;
the second bending station comprises a second upper core embedded in the upper template and two second lower cores embedded in the lower template oppositely, a 45-degree punch is arranged at the lower end of the second upper core, and a 45-degree groove matched with the 45-degree punch is formed in the inner side of the upper end of the second lower core;
the third bending station comprises two third upper cores which are embedded on the upper template and two third lower cores which are embedded on the lower template, a square punch is arranged at the lower end of each third upper core, and a square groove matched with the square punch is formed in the inner side of the upper end of each third lower core.
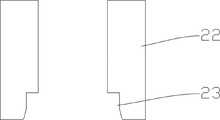
The multi-station progressive die for the rotating shaft support is characterized in that: the correcting device further comprises a correcting station arranged behind the third bending station, the correcting station comprises two correcting cores embedded on the upper template, and 90-degree correcting grooves matched with the supporting arms of the rotating shaft support are formed in the inner sides of the correcting cores.
The multi-station progressive die for the rotating shaft support is characterized in that: and an arc-shaped chamfer is arranged at the included angle of the 90-degree punch.
The multi-station progressive die for the rotating shaft support is characterized in that: and a yielding groove is formed in the third upper core corresponding to the upper end of the square punch.
The multi-station progressive die for the rotating shaft bracket has the advantages that: the rotary shaft support is subjected to punch forming through the combination of the three bending working procedures and the correction working procedure, the punching precision is higher, and the metallographic structure of the section bar is basically not damaged.
The present invention will be described in further detail with reference to the accompanying drawings and specific embodiments.
Drawings
FIG. 1 is a schematic view of the construction of a spindle bracket according to the present invention;
FIG. 2 is a side view of the spindle bracket of the present invention;
FIG. 3 is a schematic structural view of a multi-station progressive die of a spindle bracket according to the present invention;
FIG. 4 is a cross-sectional view taken along line A-A of FIG. 3, showing a schematic view of a first bending station;
FIG. 5 is a cross-sectional view taken along line B-B of FIG. 3, showing a schematic view of a second bending station;
FIG. 6 is a cross-sectional view taken along line C-C of FIG. 3, showing a schematic view of a third bending station;
FIG. 7 is a cross-sectional view taken along line D-D of FIG. 3, showing a schematic view of a rework station;
FIG. 8 is a schematic view showing the construction of a first upper core and a first lower core according to the present invention;
FIG. 9 is a schematic view showing the construction of a second upper core and a second lower core according to the present invention;
FIG. 10 is a schematic view showing the construction of a third upper core and a third lower core according to the present invention;
FIG. 11 is a schematic view of the present invention illustrating the construction of a correction core;
fig. 12 is a schematic structural diagram of the tape of the present invention.
Detailed Description
As shown in fig. 1 to 11, the multi-station progressive die for a spindle bracket of the present invention is used for stamping a spindle bracket 1, wherein the stamped spindle bracket 1 has a bottom plate 2 and a support arm 3 formed by 3 times of continuous 90-degree bending at two ends of the bottom plate 2. The multi-station progressive die for stamping the rotating shaft bracket 1 comprises: the bending device comprises an upper template 4, a lower template 5, and a first bending station 6, a second bending station 7 and a third bending station 8 which are sequentially arranged in the upper template 4 and the lower template 5. The upper template 4 and the lower template 5 are both provided with backing plates for embedding cores. The first bending station 6 comprises two opposite first upper cores 9 embedded in the upper template 4 and two opposite first lower cores 10 embedded in the lower template 5. The inner side of the lower end of the first upper core 9 is provided with a 90-degree punch 11, and the inner side of the upper end of the first lower core 10 is provided with a 90-degree groove 12 matched with the 90-degree punch 11. The thickness of the first upper core 9 and the first lower core 10 is adapted to the width of the punched part of the punched rotating shaft bracket 1 (same as or slightly larger than the width of the punched part). The bending of the upper end of the support arm 3 is first stamped by this process.
The second bending station 7 comprises a second upper core 13 embedded in the upper template 4 and two second lower cores 14 embedded in the lower template 5 oppositely, a 45-degree punch 15 is arranged at the lower end of the second upper core 13, and a 45-degree groove 16 matched with the 45-degree punch 15 is formed in the inner side of the upper end of the second lower core 14. The thicknesses of the second upper core 13 and the second lower core 14 are adapted to the width of the punched part of the punched rotating shaft bracket 1 (the same as or slightly larger than the width of the punched part). The lower end of the support arm 3 is firstly punched into a 45-degree bend through the process.
The third bending station 8 comprises two third opposite upper cores 17 embedded in the upper template 4 and two third opposite lower cores 18 embedded in the lower template 5. The lower end of the third upper core 17 is provided with a square punch 19, and the inner side of the upper end of the third lower core 18 is provided with a square groove 20 matched with the square punch 19. The thickness of the third upper core 17 and the third lower core 18 is adapted to the width of the punched part of the punched rotating shaft bracket 1 (the same as or slightly larger than the width of the punched part). The lower end of the support arm 3 is continuously punched to be bent by 90 degrees through the process.
During actual stamping, the upper template 4 and the lower template 5 are provided with processes of punching and the like corresponding to the front of the first bending station 6, the material belt is stamped to be as shown in fig. 12, and then the material belt sequentially enters the first bending station 6, the second bending station 7 and the third bending station 8 to be stamped step by step.
Preferably, the bending machine further comprises a correction station 21 arranged behind the third bending station 8, the correction station 21 comprises two correction cores 22 embedded in the upper template 4, and the inner side of each correction core 22 is provided with a 90-degree correction slot 23 corresponding to the support arm 3 of the rotating shaft support 1. The upper end of the support arm 3 is punched through this process to ensure the height uniformity of the support arm 3.
Preferably, an arc-shaped chamfer 24 is arranged at an included angle of the 90-degree punch 11 to prevent the bending scratch of the rotating shaft bracket 1 caused by an over-sharp corner of the punch.
Preferably, the third upper core 17 is provided with a yielding groove 25 corresponding to the upper end of the square punch 19, and the bent part of the rotating shaft bracket 1 has enough deformation space through the yielding groove 25, so as to ensure that the bent part is bent by 90 degrees.
The above description is only for the purpose of illustrating the preferred embodiments of the present invention and is not to be construed as limiting the utility model, and any modifications, equivalents and improvements made within the spirit and principle of the present invention are included in the scope of the present invention.
Claims (4)
1. The utility model provides a pivot support multistation upgrades mould for punching press pivot support (1), punching press pivot support (1) have bottom plate (2) and support arm (3) that form are bent through 3 times continuous 90 degrees in bottom plate (2) both ends, its characterized in that is used for the punching press the multistation of pivot support (1) upgrades the mould and includes: the bending device comprises an upper template (4), a lower template (5), and a first bending station (6), a second bending station (7) and a third bending station (8) which are sequentially arranged in the upper template (4) and the lower template (5);
the first bending station (6) comprises two opposite first upper cores (9) embedded on the upper template (4) and two opposite first lower cores (10) embedded on the lower template (5), a 90-degree punch (11) is arranged on the inner side of the lower end of each first upper core (9), and a 90-degree groove (12) matched with the 90-degree punch (11) is arranged on the inner side of the upper end of each first lower core (10);
the second bending station (7) comprises a second upper core (13) embedded in the upper template (4) and two opposite second lower cores (14) embedded in the lower template (5), a 45-degree punch (15) is arranged at the lower end of the second upper core (13), and a 45-degree groove (16) matched with the 45-degree punch (15) is formed in the inner side of the upper end of the second lower core (14);
the third bending station (8) comprises two third upper cores (17) which are embedded in the upper template (4) in a relative mode and two third lower cores (18) which are embedded in the lower template (5) in a relative mode, a square punch (19) is arranged at the lower end of each third upper core (17), and a square groove (20) matched with the square punch (19) is formed in the inner side of the upper end of each third lower core (18).
2. The multi-station progressive die for the spindle bracket according to claim 1, wherein: the bending machine is characterized by further comprising a correction station (21) arranged behind the third bending station (8), wherein the correction station (21) comprises two correction cores (22) embedded on the upper template (4), and 90-degree correction grooves (23) matched with the supporting arms (3) of the rotating shaft support (1) are formed in the inner sides of the correction cores (22).
3. The multi-station progressive die for the spindle bracket according to claim 1, wherein: and an arc-shaped chamfer (24) is arranged at the included angle of the 90-degree punch (11).
4. The multi-station progressive die for the spindle bracket according to claim 1, wherein: and the third upper core (17) is provided with a yielding groove (25) corresponding to the upper end of the square punch (19).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122623445.3U CN216262999U (en) | 2021-10-29 | 2021-10-29 | Multi-station progressive die for rotating shaft bracket |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122623445.3U CN216262999U (en) | 2021-10-29 | 2021-10-29 | Multi-station progressive die for rotating shaft bracket |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN216262999U true CN216262999U (en) | 2022-04-12 |
Family
ID=81003389
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202122623445.3U Active CN216262999U (en) | 2021-10-29 | 2021-10-29 | Multi-station progressive die for rotating shaft bracket |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN216262999U (en) |
-
2021
- 2021-10-29 CN CN202122623445.3U patent/CN216262999U/en active Active
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105618575A (en) | Automobile fender stretching die | |
| CN207823710U (en) | A continuous stamping die for a connector shell | |
| CN220760765U (en) | Stamping part die for integrated automobile | |
| CN216297726U (en) | Stamping device for processing environment-friendly composite board of automobile | |
| CN210435097U (en) | High-efficient bending machine convenient to operation | |
| CN210565718U (en) | Punch forming connecting piece capable of realizing double-shaft connection | |
| CN211247929U (en) | Stamping mechanism for automatic stamping production line | |
| CN209393820U (en) | Blade automatic moulding blanking system | |
| CN210023494U (en) | Novel car seat support turn-ups mould | |
| CN209977081U (en) | Punch forming support capable of fixing rotating shaft | |
| CN221133649U (en) | Rotatable stamping bending die structure | |
| CN223300701U (en) | Bending device for sheet metal part machining | |
| CN207026365U (en) | A kind of bar bending forming frock | |
| CN220679072U (en) | A mould structure for 5G equipment processing | |
| CN217831542U (en) | Aluminum profile cold bending device | |
| CN220697896U (en) | Prevent inserting and hinder mould structure of bending | |
| CN215143925U (en) | Double-station stamping die of seat wire harness mounting bracket | |
| CN211938532U (en) | Channel beam elbow forming mechanism | |
| CN215314908U (en) | Steel bar traceless bending die | |
| CN217044232U (en) | Cold and hot punching die | |
| CN2865922Y (en) | Stamping continuous die auto-feeder | |
| CN213856441U (en) | Small plate bending machine | |
| CN217617245U (en) | Narrow U type mould of bending | |
| CN220127275U (en) | Rotatory mould of bending of refrigerator outward appearance spare | |
| CN216990018U (en) | Positioning device for steel pipe punching |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |