CN216205187U - Distributed high-efficiency energy-saving environment-friendly industrial kiln - Google Patents
Distributed high-efficiency energy-saving environment-friendly industrial kiln Download PDFInfo
- Publication number
- CN216205187U CN216205187U CN202122187666.0U CN202122187666U CN216205187U CN 216205187 U CN216205187 U CN 216205187U CN 202122187666 U CN202122187666 U CN 202122187666U CN 216205187 U CN216205187 U CN 216205187U
- Authority
- CN
- China
- Prior art keywords
- kiln
- preheating
- bin
- hot air
- cooling
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images





Landscapes
- Furnace Details (AREA)
- Tunnel Furnaces (AREA)
Abstract
本申请提供了一种分布式高效节能环保工业窑炉,包括以下部件:若干独立单体设置的预热仓,包括预热仓体和可活动开闭的预热仓门;若干独立单体设置并与预热仓间隔分布的烧成窑,包括窑体、可活动开闭窑体顶部的窑盖和智能电火焰加热设备;若干独立单体设置并与预热仓和烧成窑间隔分布的冷却仓,包括冷却仓体和可活动开闭冷却仓体顶部的冷却仓盖;吊装设备设于装载区、预热仓、烧成窑和冷却仓以及卸载区的上方,可移动并用于将放置有陶瓷制品的吊出或装入;智能通风系统分别连通烧成窑、预热仓以及冷却仓。控制系统与上述部件分别连接以实现智能控制。本申请提供的分布式高效节能环保工业窑炉具有安全节能环保的优点。

The application provides a distributed high-efficiency, energy-saving and environmentally friendly industrial kiln, which includes the following components: a preheating chamber set up by several independent monomers, including a preheating chamber body and a preheating chamber door that can be opened and closed movably; a number of independent monomer settings are provided Firing kilns that are spaced apart from the preheating chamber, including the kiln body, a kiln cover that can be movably opened and closed at the top of the kiln body, and intelligent electric flame heating equipment; The cooling silo, including the cooling silo body and the cooling silo cover at the top of the cooling silo body that can be opened and closed; the hoisting equipment is arranged above the loading area, the preheating silo, the firing kiln, the cooling silo and the unloading area, which can be moved and used to place the There are hoisting or loading of ceramic products; the intelligent ventilation system is respectively connected to the firing kiln, preheating bin and cooling bin. The control system is respectively connected with the above components to realize intelligent control. The distributed industrial kiln with high efficiency, energy saving and environmental protection provided by the present application has the advantages of safety, energy saving and environmental protection.
Description
技术领域technical field
本申请属于工业窑炉技术领域,更具体地说,是涉及一种分布式高效节能环保工业窑炉。The present application belongs to the technical field of industrial kilns, and more specifically, relates to a distributed industrial kiln with high efficiency, energy saving and environmental protection.
背景技术Background technique
在陶瓷工业中,目前常见的工业窑炉主要分为隧道窑炉和辊道窑炉两种。装载有待烧制的陶瓷制品的窑车在这两种工业窑炉中,都会依次经过装载区、预热仓、烧成区、冷却区、卸载区,然后再次回到装载区,如此循环往复以完成整个烧制过程。这两种工业窑炉的主要区别在于辊道窑炉的窑车是依靠辊的转动而实现向前运动,隧道窑炉的窑车则是自身带有车轮并依靠拖拉向前运动。然而,在窑车向前运动的过程中,无论是隧道窑炉还是辊道窑炉都有可能会发生窑车倒塌事故,特别是多层窑更容易发生此类事故,而任意一个区的任意一台窑车发生事故,都会导致整条生产线的停产。一但停产,由于在清理故障前需要对整个隧道进行缓慢降温,在清理故障后也需要对整个隧道进行缓慢升温,故整个清理和重启生产线的过程将会耗费巨大的时间、人力、物力以及财力。因此,如何避免因发生窑车倒塌事故而导致整条生产线停产是所有陶瓷生产企业都必须面对的难题。In the ceramic industry, the common industrial kilns are mainly divided into two types: tunnel kilns and roller kilns. In these two industrial kilns, the kiln car loaded with the ceramic products to be fired will pass through the loading area, the preheating bin, the firing area, the cooling area, the unloading area, and then return to the loading area again, and so on. Complete the entire firing process. The main difference between the two industrial kilns is that the kiln car of the roller kiln relies on the rotation of the rollers to achieve forward movement, while the kiln car of the tunnel kiln has its own wheels and moves forward by dragging. However, during the forward movement of the kiln car, whether it is a tunnel kiln or a roller kiln, a kiln car collapse accident may occur, especially multi-layer kilns are more prone to such accidents. An accident of a kiln car will lead to the shutdown of the entire production line. Once production is stopped, the entire tunnel needs to be slowly cooled before the fault is cleared, and the entire tunnel needs to be slowly heated up after the fault is cleared. Therefore, the entire process of cleaning and restarting the production line will consume huge time, manpower, material and financial resources. . Therefore, how to avoid the shutdown of the entire production line due to the collapse of the kiln car is a difficult problem that all ceramic manufacturers must face.
此外,目前常见的工业窑炉还存在投资大、碳排放大、用地规模大,但产能相对较小的行业现实。具体来说,首先,新建一条普通的陶瓷生产线,仅设备、厂房至少就需要投入5000万以上,投资规模较大但产能较小;其次,新建一条普通的陶瓷生产线大约需要50亩用地,如此大规模的用地,在土地越来越昂贵的情况下是难以为继的;再次,工业窑炉在烧制陶瓷制品时通常使用燃气,例如但不限于天然气、煤制燃气、重油燃气等,此加热方式不但要消耗大量的燃气资源,还会产生大量的二氧化碳排放,特别是在如今碳中和的环保要求下,普通的陶瓷生产线将会被严格的限制生产,而且排放不合格的老旧生产线也会被逐步关停。In addition, the current common industrial kilns still have the reality of large investment, large carbon emissions, large land use, but relatively small production capacity. Specifically, first of all, to build an ordinary ceramic production line, at least 50 million yuan needs to be invested in equipment and workshops. The investment scale is large but the production capacity is small; secondly, a new ordinary ceramic production line needs about 50 acres of land, so large Large-scale land use is unsustainable when land is becoming more and more expensive; again, industrial kilns usually use gas when firing ceramic products, such as but not limited to natural gas, coal gas, heavy oil gas, etc. This method not only consumes a large amount of gas resources, but also produces a large amount of carbon dioxide emissions. Especially under the current environmental protection requirements of carbon neutrality, ordinary ceramic production lines will be strictly limited in production, and the old production lines with unqualified emissions will also be produced. will be gradually shut down.
因此,如何设计出环保节能、占地面积小、产出高且安全性好的工业窑炉就成了陶瓷工业领域中亟需解决的问题。Therefore, how to design an industrial kiln that is environmentally friendly and energy-saving, occupies a small area, has high output and has good safety has become an urgent problem to be solved in the field of ceramic industry.
实用新型内容Utility model content
本申请实施例的目的在于提供一种分布式高效节能环保工业窑炉,以解决现有技术中存在的工业窑炉安全性较差且低效不环保的技术问题。The purpose of the embodiments of the present application is to provide a distributed industrial kiln with high efficiency, energy saving and environmental protection, so as to solve the technical problems in the prior art that the industrial kiln has poor safety, low efficiency and environmental protection.
为实现上述目的,本申请采用的技术方案是:提供一种分布式高效节能环保工业窑炉,用于陶瓷制品的烧制,该分布式高效节能环保工业窑炉包括:In order to achieve the above-mentioned purpose, the technical scheme adopted in the present application is to provide a distributed high-efficiency, energy-saving and environment-friendly industrial kiln for firing ceramic products, and the distributed, high-efficiency, energy-saving and environment-friendly industrial kiln includes:
若干预热仓,每一预热仓均呈独立的单体设置,预热仓包括预热仓体以及设于预热仓体的仓口的预热仓门,预热仓门可活动开合以打开或关闭预热仓体;There are several preheating chambers, each of which is set up as an independent unit. The preheating chamber includes a preheating chamber body and a preheating chamber door located at the opening of the preheating chamber body. The preheating chamber door can be movably opened and closed. to open or close the preheating chamber;
若干烧成窑,每一烧成窑均呈独立的单体设置,并与预热仓间隔分布;烧成窑包括窑体、盖合窑体顶端并可活动开合的窑盖、以及设置在窑体的侧壁上的智能电火焰加热设备;There are several firing kilns, each of which is set up as an independent unit and is spaced apart from the preheating bin; Intelligent electric flame heating equipment on the side wall of the kiln body;
若干冷却仓,每一冷却仓均呈独立的单体设置,并与预热仓以及烧成窑间隔分布;冷却仓包括冷却仓体以及设于冷却仓体的仓口的冷却仓盖,冷却仓盖可活动开合以打开或关闭冷却仓体;There are several cooling bins, each of which is set up as an independent unit and is spaced apart from the preheating bin and the firing kiln; the cooling bin includes a cooling bin body and a cooling bin cover located at the bin mouth of the cooling bin body. The cover can be movably opened and closed to open or close the cooling compartment;
吊装设备,设于预热仓、烧成窑以及冷却仓的上方,吊装设备可移动并用于将放置有陶瓷制品的装载板分别从预热仓、烧成窑以及冷却仓中吊出或装入;The hoisting equipment is installed above the preheating silo, firing kiln and cooling silo. The hoisting equipment is movable and used to lift or load the loading plate with ceramic products from the preheating silo, firing kiln and cooling silo, respectively. ;
智能通风系统,智能通风系统分别连通烧成窑、预热仓以及冷却仓;以及,Intelligent ventilation system, the intelligent ventilation system connects the firing kiln, the preheating chamber and the cooling chamber respectively; and,
控制系统,控制系统分别与预热仓、烧成窑、冷却仓、吊装设备以及智能通风系统连接。The control system is connected with the preheating bin, the firing kiln, the cooling bin, the hoisting equipment and the intelligent ventilation system respectively.
可选地,预热仓和/或烧成窑和/或冷却仓设置于地面以下。Optionally, the preheating chamber and/or the firing kiln and/or the cooling chamber are arranged below ground level.
可选地,预热仓体具有预热隧道,预热隧道具有隧道进口和隧道出口,隧道进口和隧道出口处均设有预热仓门,隧道出口邻近烧成窑设置,冷却仓邻近烧成窑设置。Optionally, the preheating bin body has a preheating tunnel, the preheating tunnel has a tunnel inlet and a tunnel outlet, both the tunnel inlet and the tunnel outlet are provided with a preheating bin door, the tunnel outlet is arranged adjacent to the firing kiln, and the cooling bin is adjacent to the firing kiln. Kiln settings.
可选地,预热仓体呈U型,预热仓体内部形成有U型的预热隧道;Optionally, the preheating bin body is U-shaped, and a U-shaped preheating tunnel is formed inside the preheating bin body;
预热仓还包括回型轨道,回型轨道包括第一轨道段和第二轨道段,第一轨道段呈U型并内置在预热隧道内,第二轨道段位于预热仓体外部,第一轨道段呈沿轨道方向自隧道进口向隧道出口逐渐向下倾斜设置。The preheating bin also includes a return track, the return track includes a first track segment and a second track segment, the first track segment is U-shaped and is built in the preheating tunnel, the second track segment is located outside the preheating bin body, and the first track segment is located outside the preheating bin body. A track section is gradually inclined downward along the track direction from the tunnel entrance to the tunnel exit.
可选地,预热仓体的底部、预热仓体的的侧壁以及预热仓盖均由保温材料制成;Optionally, the bottom of the preheating bin body, the side wall of the preheating bin body and the preheating bin cover are all made of thermal insulation materials;
预热仓体包括两相对间隔平行的平行段和连接两平行段的弧形段,烧成窑和冷却仓位于两平行段之间的区域。The preheating silo body includes two parallel sections that are parallel to each other and an arc section connecting the two parallel sections, and the firing kiln and the cooling bin are located in the area between the two parallel sections.
可选地,预热仓还包括防倾倒窑车;防倾倒窑车包括车板、车轮以及挂钩;Optionally, the preheating bin further includes an anti-dumping kiln car; the anti-dumping kiln car includes a car board, wheels and hooks;
回型轨道包括两间隔平行的车轨,车板具有两相对的并超越车轨外侧面的车板边缘;车轮安装在车板底面并可在车轨上滑动,多个挂钩分设于两车板边缘,且挂钩具有朝向车轨外侧面的弯钩部。The return track includes two spaced and parallel rails, the car board has two opposite edges of the car board and surpasses the outer side of the car track; the wheels are installed on the bottom surface of the car board and can slide on the car rails, and a plurality of hooks are arranged on the two car boards. edge, and the hook has a hook portion facing the outer side of the rail.
可选地,工业窑炉还包括装载区和卸载区,装载区和卸载区均相对于预热仓、烧成窑以及冷却仓独立设置;Optionally, the industrial kiln further includes a loading area and an unloading area, and the loading area and the unloading area are independently set relative to the preheating bin, the firing kiln and the cooling bin;
装载区邻近隧道进口设置,卸载区邻近隧道出口设置。The loading area is set adjacent to the tunnel entrance, and the unloading area is set adjacent to the tunnel exit.
可选地,工业窑炉还包括智能机械臂,且智能机械臂邻近预热仓和装载区设置。Optionally, the industrial kiln further includes an intelligent robotic arm, and the intelligent robotic arm is disposed adjacent to the preheating bin and the loading area.
可选地,窑体的底部、窑体的侧壁以及窑盖均由耐火材料制成,窑体的底部、窑体的侧壁以及窑盖围合形成加热腔,陶瓷制品放置在装载板上并内置于加热腔中;Optionally, the bottom of the kiln body, the side wall of the kiln body and the kiln cover are all made of refractory materials, the bottom of the kiln body, the side wall of the kiln body and the kiln cover are enclosed to form a heating cavity, and the ceramic products are placed on the loading plate. And built into the heating chamber;
智能电火焰加热设备包括多组电火焰枪,每组电火焰枪的一端均与窑体的侧壁连接,电火焰枪的另一端伸入加热腔中。The intelligent electric flame heating equipment includes multiple groups of electric flame guns, one end of each group of electric flame guns is connected to the side wall of the kiln body, and the other end of the electric flame guns extends into the heating cavity.
可选地,智能电火焰加热设备还包括安装在窑体的侧壁上的移动装置,电火焰枪的一端通过移动装置安装在窑体的侧壁上;Optionally, the intelligent electric flame heating device further comprises a moving device installed on the side wall of the kiln body, and one end of the electric flame gun is installed on the side wall of the kiln body through the moving device;
移动装置包括第一驱动机构和滑动件,窑体的侧壁上设有滑动安装孔,滑动件安装在滑动安装孔处并与窑体的侧壁滑动连接,且滑动件在滑动过程中始终盖合滑动安装孔;The moving device includes a first drive mechanism and a sliding piece, the side wall of the kiln body is provided with a sliding installation hole, the sliding piece is installed at the sliding installation hole and is slidably connected with the side wall of the kiln body, and the sliding piece is always covered during the sliding process. Close the sliding mounting hole;
电火焰枪的一端与滑动件连接;第一驱动机构设于窑体的外侧,并用于驱动滑动件以带动电火焰枪移动以及驱动电火焰枪旋转。One end of the electric flame gun is connected with the sliding piece; the first driving mechanism is arranged on the outer side of the kiln body and is used for driving the sliding piece to drive the electric flame gun to move and drive the electric flame gun to rotate.
可选地,电火焰枪呈丰字型或F型设置,包括主杆和多个支杆;主杆与滑动件连接,支杆自主杆上沿主杆的横截面径向延伸形成,且多个支杆沿主杆的轴向间隔排布;支杆远离主杆的自由端处开设有喷火口。Optionally, the electric flame gun is arranged in a F-shaped or F-shaped configuration, including a main rod and a plurality of supporting rods; the main rod is connected with the sliding piece, and the supporting rod is formed by extending radially from the main rod along the cross-section of the main rod, and there are many rods. The supporting rods are arranged at intervals along the axial direction of the main rod; the free end of the supporting rods away from the main rod is provided with a flame outlet.
可选地,窑盖包括位于里层的耐火层以层叠在耐火层外侧的金属板;Optionally, the kiln cover includes a refractory layer on the inner layer to laminate a metal plate outside the refractory layer;
烧成窑还包括第二驱动机构以及锁合装置;第二驱动机构安装在窑体的外表面,并与金属板连接,用于驱动窑盖打开或闭合;锁合装置设于金属板上,用于锁合或解锁窑盖。The firing kiln also includes a second driving mechanism and a locking device; the second driving mechanism is installed on the outer surface of the kiln body and connected with the metal plate to drive the kiln cover to open or close; the locking device is arranged on the metal plate, For locking or unlocking the kiln cover.
可选地,智能通风系统包括风道组、多组风机、多个通风连通装置以及多个测温计;预热仓的进风口和出风口、烧成窑的进风口和出风口、冷却仓的进风口和出风口处均设有一通风连通装置;Optionally, the intelligent ventilation system includes an air duct group, multiple groups of fans, multiple ventilation communication devices, and multiple thermometers; the air inlet and outlet of the preheating chamber, the air inlet and outlet of the firing kiln, and the cooling chamber. There is a ventilation communication device at both the air inlet and the air outlet;
风道组包括若干低温冷风通道、若干低温热风通道、若干中温热风通道以及若干高温热风通道;高温热风通道和中温热风通道中均设置有测温计;高温热风通道、中温热风通道、低温热风通道以及低温冷风通道中均设有一风机;The air duct group includes several low-temperature cold air passages, several low-temperature hot air passages, several medium-temperature hot air passages, and several high-temperature hot air passages; thermometers are set in both the high-temperature hot air passages and the medium-temperature hot air passages; the high-temperature hot air passages, the medium-temperature hot air passages A fan is arranged in the air passage, the low temperature hot air passage and the low temperature cold air passage;
烧成窑的进风口通过一通风连通装置分别与一中温热风通道和一高温热风通道连通;烧成窑的出风口通过一通风连通装置与一高温热风通道连通;The air inlet of the firing kiln is communicated with a medium temperature hot air channel and a high temperature hot air channel respectively through a ventilation communication device; the air outlet of the firing kiln is communicated with a high temperature hot air channel through a ventilation communication device;
预热仓的进风口通过一通风连通装置和高温热风通道与烧成窑的出风口连通,预热仓的出风口通过中温热风通道与烧成窑的进风口连通;The air inlet of the preheating bin is communicated with the air outlet of the firing kiln through a ventilation communication device and a high-temperature hot air passage, and the air outlet of the preheating bin is communicated with the air inlet of the firing kiln through a medium-temperature hot air passage;
冷却仓的进风口通过一通风连通装置分别和一个中温热风通道、一个低温热风通道以及一个低温冷风通道连通;冷却仓的出风口通过一通风连通装置分别和一个高温热风通道、一个中温热风通道以及一个低温热风通道连通,其中,均与冷却仓的出风口连通的高温热风通道和中温热风通道连通。The air inlet of the cooling bin is respectively connected with a medium temperature hot air channel, a low temperature hot air channel and a low temperature cold air channel through a ventilation communication device; The hot air channel is communicated with a low temperature hot air channel, wherein the high temperature hot air channel and the medium temperature hot air channel which are both communicated with the air outlet of the cooling bin are communicated.
可选地,工业窑炉还包括风干塔,风干塔的进风口通过一中温热风通道与预热仓的出风口连通;风干塔的出风口通过一低温热风通道与冷却仓的进风口连通。Optionally, the industrial kiln also includes an air-drying tower, and the air inlet of the air-drying tower is communicated with the air outlet of the preheating bin through a medium-temperature hot air passage; the air outlet of the air-drying tower is communicated with the air inlet of the cooling bin through a low-temperature hot air passage. .
可选地,冷却仓体的底部、冷却仓体的的侧壁以及冷却仓盖均由保温材料制成;冷却仓体的底部、冷却仓体的的侧壁以及冷却仓盖围合形成冷却腔。Optionally, the bottom of the cooling bin body, the side wall of the cooling bin body and the cooling bin cover are all made of thermal insulation materials; the bottom of the cooling bin body, the side wall of the cooling bin body and the cooling bin cover are enclosed to form a cooling cavity. .
可选地,装载板的底部设有第一定位部,窑体的底部以及冷却仓体的底部均设有与第一定位部适配定位连接的第二定位部;Optionally, the bottom of the loading plate is provided with a first positioning portion, and both the bottom of the kiln body and the bottom of the cooling bin body are provided with a second positioning portion that is adapted and connected to the first positioning portion;
装载板的上表面还设有第三定位部,多个装载板可叠加设置。The upper surface of the loading plate is further provided with a third positioning portion, and a plurality of loading plates can be superimposed and arranged.
可选地,工业窑炉还包括保温吊装箱,保温吊装箱由保温材料制成,保温吊装箱与装载板连接,并罩盖住放置在装载板上的陶瓷制品。Optionally, the industrial kiln further includes a thermal insulation hoisting box, the thermal insulation hoisting box is made of thermal insulation material, the thermal insulation hoisting box is connected to the loading plate, and covers the ceramic products placed on the loading plate.
本申请提供的分布式高效节能环保工业窑炉的有益效果在于:相较于目前常见的工业窑炉,本分布式高效节能环保工业窑炉具有以下优点:The beneficial effects of the distributed high-efficiency, energy-saving and environment-friendly industrial kiln provided by the present application are: compared with the current common industrial kilns, the distributed high-efficiency, energy-saving and environment-friendly industrial kiln has the following advantages:
第一、由于预热仓、烧成窑以及冷却仓是完全独立的单体设置并间隔式分布,这些单独的生产设备可以并行运行且互不干扰,故生产人员就可以根据产能的需求,任意的扩大或停产某仓而不影响整体生产线的正常生产,例如当预热仓、烧成窑以及冷却仓中的某一项生产设备是产能瓶颈时,就可以独立增加该项生产设备的数量,如此就可以显著提高产能,甚至实现最大限度的释放产能;当然,在某一生产设备发生故障时,也可以直接停用,并直接使用另一个同类的生产设备而不影响,这样就能彻底避免因窑车倒塌事故而导致整条生产线停产的情况发生,极大地提高整条生产线的生产安全性。同时,使用本申请的技术方案,在最低产能和最大产能之间,可实现弹性产能生产。First, since the preheating bin, firing kiln and cooling bin are completely independent units and are distributed at intervals, these separate production equipment can run in parallel without interfering with each other. The expansion or shutdown of a certain warehouse will not affect the normal production of the overall production line. For example, when a certain production equipment in the preheating warehouse, firing kiln and cooling warehouse is the capacity bottleneck, the number of this production equipment can be increased independently. In this way, the production capacity can be significantly increased, and even the maximum release capacity can be achieved; of course, when a certain production equipment fails, it can also be directly stopped, and another similar production equipment can be directly used without affecting it, which can be completely avoided. The entire production line was stopped due to the collapse of the kiln car, which greatly improved the production safety of the entire production line. At the same time, using the technical solution of the present application, between the minimum production capacity and the maximum production capacity, flexible production capacity can be achieved.
第二、在烧成窑中,烧制陶瓷制品用的是设置在烧成窑内侧壁上的智能电火焰加热设备,该智能电火焰加热设备喷射的是电火焰,而电火焰加热使用的是电能,例如但不限于光伏电、风电、水电、核电、生物质电等再生能源,从而达到生产时零碳排放的目的,具有积极的环保意义。Second, in the firing kiln, the intelligent electric flame heating equipment installed on the inner side wall of the firing kiln is used for firing ceramic products. The intelligent electric flame heating equipment sprays an electric flame, and the electric flame heating uses Electric energy, such as but not limited to photovoltaic power, wind power, hydropower, nuclear power, biomass power and other renewable energy sources, so as to achieve the goal of zero carbon emission during production, which has positive environmental protection significance.
第三、在使用智能电火焰加热设备时,烧成窑的窑盖是闭合的,即智能电火焰加热设备在加热时是在密闭的窑体中,从而可大大减少热能流失;当然,预热仓也可通过预热仓盖密闭,冷却仓也可通过冷却仓盖密闭,这同样有利于减少能量流失;此外,由于智能通风系统分别连通烧成窑、预热仓以及冷却仓,故烧成窑在冷却过程中的热能也能通过智能通风系统而再次被利用于预热仓的预热和风干塔的风干等。换言之,烧成窑、预热仓以及冷却仓可开合密闭设置以及智能通风系统的连通作用,可使得本分布式高效节能环保工业窑炉非常节能。Third, when using the intelligent electric flame heating equipment, the kiln cover of the firing kiln is closed, that is, the intelligent electric flame heating equipment is in a closed kiln body during heating, which can greatly reduce the loss of heat energy; of course, preheating The silo can also be sealed through the preheating silo cover, and the cooling silo can also be sealed through the cooling silo cover, which is also beneficial to reduce energy loss; The thermal energy of the kiln during the cooling process can also be reused for the preheating of the preheating chamber and the drying of the drying tower through the intelligent ventilation system. In other words, the opening and closing of the firing kiln, the preheating bin and the cooling bin and the connection of the intelligent ventilation system can make the distributed high-efficiency, energy-saving and environment-friendly industrial kiln very energy-saving.
附图说明Description of drawings
为了更清楚地说明本申请实施例中的技术方案,下面将对实施例或现有技术描述中所需要使用的附图作简单地介绍,显而易见地,下面描述中的附图仅仅是本申请的一些实施例,对于本领域普通技术人员来讲,在不付出创造性劳动性的前提下,还可以根据这些附图获得其他的附图。In order to illustrate the technical solutions in the embodiments of the present application more clearly, the following briefly introduces the accompanying drawings that need to be used in the description of the embodiments or the prior art. Obviously, the drawings in the following description are only for the present application. In some embodiments, for those of ordinary skill in the art, other drawings can also be obtained according to these drawings without any creative effort.
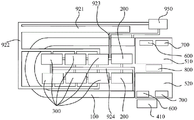
图1为本申请实施例提供的分布式高效节能环保工业窑炉的平面分布图;Fig. 1 is the plane distribution diagram of the distributed high-efficiency, energy-saving and environment-friendly industrial kiln provided by the embodiment of the present application;
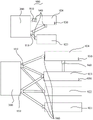
图2为本申请实施例提供的分布式高效节能环保工业窑炉的智能通风系统分布示意图;2 is a schematic diagram of the distribution of an intelligent ventilation system of a distributed, high-efficiency, energy-saving, and environment-friendly industrial kiln provided by an embodiment of the present application;
图3为本申请实施例提供的智能电火焰加热设备的结构示意图;3 is a schematic structural diagram of an intelligent electric flame heating device provided by an embodiment of the application;
图4为本申请实施例提供的智能电火焰加热设备另一角度的结构示意图;4 is a schematic structural diagram of another angle of the intelligent electric flame heating device provided by the embodiment of the application;
图5为本申请实施例提供的智能通风系统的连接示意图;5 is a schematic diagram of the connection of the intelligent ventilation system provided by the embodiment of the present application;
图6为本申请实施例提供的预热仓的平面分布图;FIG. 6 is a plane distribution diagram of a preheating bin provided by an embodiment of the present application;
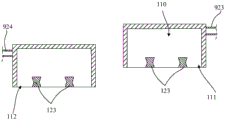
图7为本申请实施例提供的预热仓的回型轨道的截面示意图;7 is a schematic cross-sectional view of a return track of a preheating bin provided by an embodiment of the present application;
图8为本申请实施例提供的装载板的部分结构示意图;8 is a schematic diagram of a partial structure of a loading plate provided by an embodiment of the present application;
图9为本申请实施例提供的防倾倒窑车的结构示意图。FIG. 9 is a schematic structural diagram of an anti-dumping kiln car according to an embodiment of the present application.
具体实施方式Detailed ways
为了使本申请的目的、技术方案及优点更加清楚明白,以下结合附图及实施例,对本申请进行进一步详细说明。应当理解,此处所描述的具体实施例仅用以解释本发明,并不用于限定本申请。In order to make the purpose, technical solutions and advantages of the present application more clearly understood, the present application will be described in further detail below with reference to the accompanying drawings and embodiments. It should be understood that the specific embodiments described herein are only used to explain the present invention, but not to limit the present application.
需说明的是,当部件被称为“固定于”或“设置于”另一个部件,它可以直接在另一个部件上或者间接在该另一个部件上。当一个部件被称为是“连接于”另一个部件,它可以是直接或者间接连接至该另一个部件上。术语“上”、“下”、“左”、“右”等指示的方位或位置关系为基于附图所示的方位或位置关系,仅是为了便于描述,而不是指示或暗示所指的装置或元件必须具有特定的方位、以特定的方位构造和操作,因此不能理解为对本申请的限制,对于本领域的普通技术人员而言,可以根据具体情况理解上述术语的具体含义。术语“第一”、“第二”仅用于便于描述目的,而不能理解为指示或暗示相对重要性或者隐含指明技术特征的数量。“多个”的含义是两个或两个以上,除非另有明确具体的限定。It should be noted that when a component is referred to as being "fixed to" or "disposed on" another component, it can be directly on the other component or indirectly on the other component. When an element is referred to as being "connected to" another element, it can be directly or indirectly connected to the other element. The orientation or positional relationship indicated by the terms "upper", "lower", "left", "right", etc. is based on the orientation or positional relationship shown in the drawings, and is only for the convenience of description, rather than indicating or implying the referred device Or the elements must have a specific orientation, be constructed and operated in a specific orientation, so it cannot be construed as a limitation to the present application, and those of ordinary skill in the art can understand the specific meanings of the above terms according to specific situations. The terms "first" and "second" are only used for the purpose of description, and should not be understood as indicating or implying relative importance or implying indicating the number of technical features. "Plurality" means two or more, unless expressly specifically limited otherwise.
为了说明本申请所提供的技术方案,以下结合具体附图及实施例进行详细说明。In order to illustrate the technical solutions provided in the present application, the following detailed description is given in conjunction with the specific drawings and embodiments.
本申请实施例提供一种分布式高效节能环保工业窑炉。The embodiments of the present application provide a distributed industrial kiln with high efficiency, energy saving and environmental protection.
请参阅图1和图2,在一实施例中,该分布式高效节能环保工业窑炉包括若干预热仓100、若干烧成窑200、若干冷却仓300、吊装设备(未图示)、智能通风系统900以及控制系统(未图示)。其中,每一预热仓100均呈完全独立的单体设置,预热仓100具体包括预热仓体(未图示)以及设于预热仓体的仓口的预热仓门(未图示),预热仓门可活动开合以打开或关闭预热仓体。每一烧成窑200也均呈完全独立的单体设置,并与预热仓100间隔分布;烧成窑200具体包括窑体(未图示)、窑盖(未图示)以及智能电火焰加热设备210,窑盖设于窑体顶端,并可活动开合以打开或关闭窑体,智能电火焰加热设备210设置在窑体的侧壁上,用于喷射电火焰以实现对放置在窑体中的陶瓷制品的烧制。每一冷却仓300也均呈完全独立的单体设置,并与烧成窑200和预热仓100间隔分布;冷却仓300具体包括冷却仓体(未图示)以及设于冷却仓体的仓口的冷却仓盖,冷却仓盖可活动开合以打开或关闭冷却仓体。吊装设备设于预热仓100、烧成窑200以及冷却仓300的上方,例如但不限于设于厂房的横梁上,吊装设备可移动并用于将放置有陶瓷制品的装载板700分别从预热仓100、烧成窑200以及冷却仓300中吊出或装入。智能通风系统900分别连通烧成窑200、预热仓100以及冷却仓300;控制系统分别与预热仓100、烧成窑200、冷却仓300、吊装设备以及智能通风系统900电连接,以实现对上述各个部件的智能化控制。Please refer to FIG. 1 and FIG. 2. In one embodiment, the distributed high-efficiency, energy-saving and environment-friendly industrial kiln includes several preheating
在此,控制系统可以看成是一套自动化生产管理的调度系统,可用于各生产设备的状态采集、生产设备的生产调度指令的发布和接收、生产设备当前生产工序的时间管理、生产设备当前工序的指令执行步骤管理、以及各生产设备之间的指令执行步骤之间的协调,进而可实现按不同条件,例如按照最大产能、最大节能或最低产能等条件,进行生产指令执行步骤的规划以及最佳生产指令执行步骤的优化。具体地,控制系统包含设有主机的智能控制室410以及各个信息采集和传输部件,进而形成预热仓故障管理分系统、烧成窑自动化管理分系统、冷却仓自动化管理分系统、智能通风管理分系统、吊装自动化协调管理分系统等,其中,烧成窑自动化管理分系统中包括对智能电火焰的加热管理功能。当然,本工业窑炉还包括装载区510和卸载区520,相应地,控制系统也包括装载区的自动化装载管理分系统以及卸载区自动化卸载管理分系统等。如此,通过控制系统的智能化调度,就能极大地提高本分布式高效节能环保工业窑炉的生产效率,进而实现扩大产出,降低陶瓷制品的成本。Here, the control system can be regarded as a set of scheduling system for automatic production management, which can be used for the status collection of each production equipment, the issuance and reception of production scheduling instructions of production equipment, the time management of the current production process of production equipment, the current status of production equipment The management of the order execution steps of the process and the coordination between the order execution steps among the various production equipment can realize the planning of the production order execution steps according to different conditions, such as maximum production capacity, maximum energy saving or minimum production capacity, etc. Optimization of optimal production order execution steps. Specifically, the control system includes an
基于此结构设计,在本申请中,相较于目前常见的工业窑炉,本分布式高效节能环保工业窑炉具有以下优点:Based on this structural design, in this application, compared with the current common industrial kilns, this distributed industrial kiln with high efficiency, energy saving and environmental protection has the following advantages:
第一、由于预热仓100、烧成窑200以及冷却仓300是完全独立的单体设置并间隔式分布,这些单独的生产设备可以并行运行且互不干扰,故生产人员就可以根据产能的需求,任意的扩大或停产某仓而不影响整体生产线的正常生产,例如当预热仓100、烧成窑200以及冷却仓300中的某一项生产设备是产能瓶颈时,就可以独立增加该项生产设备的数量,如此就可以显著提高产能,甚至实现最大限度的释放产能;当然,在某一生产设备发生故障时,也可以直接停用,并直接使用另一个同类的生产设备而不影响,这样就能彻底避免因窑车倒塌事故而导致整条生产线停产的情况发生,极大地提高整条生产线的生产安全性。同时,使用本申请的技术方案,在最低产能和最大产能之间,可实现弹性产能生产。First, since the
第二、在烧成窑200中,烧制陶瓷制品用的是设置在烧成窑200内侧壁上的智能电火焰加热设备210,该智能电火焰加热设备210喷射的是电火焰,而电火焰加热使用的是电能,例如但不限于光伏电、风电、水电、核电、生物质电等再生能源,从而达到生产时零碳排放的目的,具有积极的环保意义。Second, in the
第三、在使用智能电火焰加热设备210时,烧成窑200的窑盖是闭合的,即智能电火焰加热设备210在加热时是在密闭的窑体中,从而可大大减少热能流失;当然,预热仓100也可通过预热仓盖密闭,冷却仓300也可通过冷却仓盖密闭,这同样有利于减少能量流失;此外,由于智能通风系统900分别连通烧成窑200、预热仓100以及冷却仓300,故烧成窑200在冷却过程中的热能也能通过智能通风系统900而再次被利用于预热仓100的预热和风干塔950的风干等。换言之,烧成窑200、预热仓100以及冷却仓300可开合密闭设置以及智能通风系统900的连通作用,可使得本分布式高效节能环保工业窑炉非常节能。Third, when the intelligent electric flame heating device 210 is used, the kiln cover of the
在此需说明的是,本分布式高效节能环保工业窑炉主要用于陶瓷制品的烧制,特别适用于发泡陶瓷的制造。在现今提倡绿色节能建筑、安全环保施工的前提下,发泡陶瓷作为一种新型无机建筑材料,具有轻质、不燃、保温、隔热、防水防潮等优点,能更好的符合逐渐提高的房地产建筑材料的保温隔热性能要求,因而越来越受到人们的重视。通常,由发泡陶瓷制成的隔墙板应是厚度较厚但强度高且轻质的大板,例如,参照一般建筑物的墙体标准,隔墙板的厚度范围一般是10至15cm,应用在北方地区的隔墙板的厚度应大于20cm,其抗压强度要达到6兆帕以上。由于这些较高的性能标准,故若采用目前常见的普通工业窑炉烧制发泡陶瓷,将会导致烧成时间长、耗能高、碳排放高、产能低等问题,进而导致发泡陶瓷成本很高、市场价格更高,不利于该环保产品的市场拓展。具体地,在发泡陶瓷的综合成本中,约1/3为能源成本,约1/3为设备折旧和土地使用等成本。而在本申请中,本分布式高效节能环保工业窑炉在同等甚至更少投资、更少用地的情况下,产能至少可以提升3倍或以上,还具有显著的节能效果。因此,使用本分布式高效节能环保工业窑炉制成的发泡陶瓷能够将成本降低到400元/立方左右,进而具备更多的价格优势,而发泡陶瓷产品一旦同时具有价格和性能优势,则会极大的有利于该性能优异的绿色环保产品的市场开发。It should be noted here that the distributed industrial kiln with high efficiency, energy saving and environmental protection is mainly used for the firing of ceramic products, and is especially suitable for the manufacture of foamed ceramics. Under the premise of advocating green energy-saving buildings, safe and environmentally friendly construction, as a new type of inorganic building material, foamed ceramics have the advantages of light weight, non-combustibility, heat preservation, heat insulation, waterproof and moisture-proof, etc., and can better meet the gradually increasing real estate Therefore, people pay more and more attention to the thermal insulation performance requirements of building materials. Usually, the partition board made of foamed ceramics should be a large board with a thick thickness but high strength and light weight. For example, referring to the wall standard of a general building, the thickness of the partition board is generally 10 to 15cm. The thickness of the partition board used in the northern region should be greater than 20cm, and its compressive strength should reach more than 6 MPa. Due to these high performance standards, if the common industrial kilns are used to fire foamed ceramics, it will lead to problems such as long firing time, high energy consumption, high carbon emissions, and low production capacity, which will lead to foamed ceramics. The cost is high and the market price is higher, which is not conducive to the market expansion of this environmentally friendly product. Specifically, in the comprehensive cost of foamed ceramics, about 1/3 is the energy cost, and about 1/3 is the cost of equipment depreciation and land use. In the present application, the distributed high-efficiency, energy-saving and environmentally friendly industrial kiln can increase the production capacity by at least 3 times or more with the same or even less investment and less land, and also has a significant energy-saving effect. Therefore, the use of this distributed high-efficiency, energy-saving and environmentally friendly industrial kiln for foamed ceramics can reduce the cost to about 400 yuan/cubic, and thus have more price advantages. Once foamed ceramic products have both price and performance advantages, It will be greatly beneficial to the market development of the green product with excellent performance.
下面以具体数据来说明本分布式高效节能环保工业窑炉相较于目前常见的工业窑炉的各项优势。其中,表2为目前常见的隧道窑炉、辊道窑炉以及本申请的分布式高效节能环保工业窑炉的发泡陶瓷烧成时间对比表。表1为三层隧道窑炉、辊道窑炉、本申请的分布式高效节能环保工业窑炉在投资、用地、用气、用电以及产能方面的综合成本对比表。由表1和表2可知,在同等甚至更少投资、更少用地、更环保、更节能的情况下,本分布式高效节能环保工业窑炉产能至少可以提升3倍或以上,而成本却相对较低。The advantages of the distributed high-efficiency, energy-saving and environment-friendly industrial kiln compared with the currently common industrial kilns are described below with specific data. Wherein, Table 2 is a comparison table of the firing time of foamed ceramics of the currently common tunnel kilns, roller kilns, and the distributed high-efficiency, energy-saving, and environment-friendly industrial kilns of the present application. Table 1 is a comprehensive cost comparison table of the three-layer tunnel kiln, the roller kiln, and the distributed high-efficiency, energy-saving and environmental protection industrial kiln of the present application in terms of investment, land use, gas consumption, electricity consumption and production capacity. From Table 1 and Table 2, it can be seen that under the same or even less investment, less land, more environmental protection and more energy saving, the production capacity of this distributed high-efficiency, energy-saving and environmentally friendly industrial kiln can be increased by at least 3 times or more, while the cost is relatively low. lower.
在此需说明是,在表2中,发泡陶瓷烧成时间是指待烧制品进隧道/窑到烧制成品出隧道/窑的时间差,该时间包含了预热时间、烧成时间、冷却时间;由于隧道窑炉、辊道窑炉的预热区、烧成区、冷却区是一体式线性串联的,故烧成时间是取这三个时间中最大的时间值;在本分布式高效节能环保工业窑炉中,由于预热仓100、烧成窑200、冷却仓300是分别独立的,且并行运行,互不干扰,故可以实现用空间换时间,达到节省大量的时间的目的。在表1中,发泡陶瓷的综合成本是按以下条件下计算的:燃气价格2.8元/立方米;平均电价1.1元/度(用电波峰、波谷加权平均值);按照国家标准的设备折旧率进行设备折旧分摊至成本。It should be noted here that in Table 2, the firing time of foamed ceramics refers to the time difference between the product to be fired entering the tunnel/kiln and the fired product exiting the tunnel/kiln, which includes preheating time, firing time, cooling time time; since the preheating zone, firing zone and cooling zone of the tunnel kiln and roller kiln are integrated and linearly connected in series, the firing time is the maximum time value among these three times; in this distributed and efficient In the energy saving and environmental protection industrial kiln, since the
表1Table 1

表2Table 2

在此需特别说明的是,为节省生产用地,避免宝贵的土地资源浪费,预热仓100和/或烧成窑200和/或冷却仓300设于地面以下。例如,烧成窑200、冷却仓300、预热仓100等都可以建在地下,甚至可以叠成建设,即烧成窑200、冷却仓300可以建在预热仓100之上。其中,烧成窑200优选建在地面以下,当然,烧成窑200也可以建在地面以上,其规格大小可以按实际需求制定;冷却仓300优选建在地面以下,当然,冷却仓300也可以建在地面以上,其规格大小可以按实际需求制定;预热仓100优选建在地面以下,此时,预热仓100地面以上空间全部可以按实际需求使用,包括建成陶瓷制品的加工区等,当然,预热仓100也可以建在地面以上,其规格大小可以按实际需求制定。It should be noted here that, in order to save production land and avoid waste of valuable land resources, the preheating
请参阅图1、图2以及图6和图7,在本实施例中,预热仓体具有预热隧道110,预热隧道110具有隧道进口111和隧道出口112,隧道进口111和隧道出口112处均设有预热仓门(未图示),隧道出口112邻近烧成窑200设置,冷却仓300邻近烧成窑200设置。在此,预热仓100还包括防倾倒窑车600,预热仓门可以自动开合以方便防倾倒窑车600进出,且在防倾倒窑车600进入预热隧道110后,预热仓门关闭,以尽可能避免热量流失。而隧道出口112邻近烧成窑200设置,具体可优选将烧成窑200建于隧道出口112附近的地下,如此可方便预热后的陶瓷制品更快捷地被吊装设备装载入烧成窑200中,同理,冷却仓300邻近烧成窑200设置也方便烧制好的陶瓷制品更快捷地从烧成窑200中转入冷却仓300中进行下一步的冷却。Please refer to FIG. 1 , FIG. 2 , and FIGS. 6 and 7 , in this embodiment, the preheating bin body has a preheating
具体在本实施例中,预热仓体呈U型,预热仓体内部形成有U型的预热隧道110;预热仓100还包括回型轨道120,回型轨道120包括第一轨道段121和第二轨道段122,第一轨道段121呈U型并内置在预热隧道110内,第二轨道段122位于预热仓体外部,第一轨道段121呈沿轨道方向自隧道进口111向隧道出口112逐渐向下倾斜设置。具体地,第一轨道段121的倾斜坡度在千分之一到千分之十之间,这样,防倾倒窑车600就可以在重力作用下,从隧道入口自行滑行至隧道出口112,而在防倾倒窑车600滑行过程中,装载在防倾倒窑车600上的陶瓷制品就能完成预热。Specifically in this embodiment, the preheating bin body is U-shaped, and a
请参阅图1和图2,在本实施例中,预热仓体的底部、预热仓体的侧壁以及预热仓盖均由保温材料制成;具体地,预热仓100的底部设有保温砖、预热仓体的侧壁则为保温墙。U型的预热仓体包括两相对间隔平行的平行段和连接两平行段的弧形段,烧成窑200和冷却仓300位于两平行段之间的区域,如此,就可以在尽可能减少土地占用的情况下,延长预热隧道110的长度,确保陶瓷制品可以得到充分预热,而且也方便了后续工序的操作。Please refer to FIG. 1 and FIG. 2 , in this embodiment, the bottom of the preheating bin body, the side wall of the preheating bin body and the preheating bin cover are all made of thermal insulation materials; The side walls with thermal insulation bricks and preheating silo body are thermal insulation walls. The U-shaped preheating bin body includes two parallel sections that are spaced apart and parallel to each other and an arc section connecting the two parallel sections. The firing
请参阅图7至图9,在本实施例中,防倾倒窑车600包括车板610、车轮620以及挂钩630;回型轨道120包括两间隔平行的车轨123,车板610具有两相对的并超越车轨123外侧面的车板610边缘;车轮620安装在车板610底面并可在车轨123上滑动,多个挂钩630分设于两车板610边缘,且挂钩630具有朝向车轨123外侧面的弯钩部。当然,在防倾倒窑车600上还设有故障报警装置。可以理解,防倾倒窑车600的车板610用于放置装载板700,装载板700上装载有陶瓷制品;当防倾倒窑车600在轨道上滑行时,L型的挂钩630自动放下,挂钩630与车轨123之间留有合适的允许防倾倒窑车600抬高的间隙;当有异物使得防倾倒窑车600单侧抬高时,该抬高侧的挂钩630也随之抬高,当防倾倒窑车600的抬高高度超过挂钩630与车轨123之间的间隙时,挂钩630将紧紧卡在车轨123上,达到防止防倾倒窑车600单侧车体过度抬高而导致侧翻的情况发生,同时,挂钩630与车轨123卡紧时也会触发故障报警装置,使得生产人员能够尽快获知故障状况。Referring to FIGS. 7 to 9 , in this embodiment, the
进一步地,在本实施例中,工业窑炉还包括智能机械臂800,且智能机械臂800邻近预热仓100和装载区510设置。具体如图1所示,机械臂优选位于装载区510和卸载区520之间,以便于更加方便陶瓷制品的装载和卸载。Further, in this embodiment, the industrial kiln further includes an intelligent
请参阅图1和图2,在本实施例中,装载区510和卸载区520均相对于预热仓100、烧成窑200以及冷却仓300独立设置;装载区510邻近隧道进口111设置,卸载区520邻近隧道出口112设置。具体来说,装载区510和卸载区520均通过轨道与回型轨道120的第二轨道段122连接,防倾倒窑车600可从隧道出口112自动滑行到卸载区520,然后,智能机械臂800取下装载有陶瓷制品的装载板700,然后将防倾倒窑车600推送至装载区510以供下次使用。在此,卸载区520与装载区510之间有轨道连接,但由于装载区510高于卸载区520,故该轨道有较大的坡度,需要外力推送防倾倒窑车600到装载区510。然后,在装载区510,通过智能机械臂800将待烧制的陶瓷制品放在装载板700上,并通过智能机械臂800将装载板700放置在防倾倒窑车600上并限位固定,然后,防倾倒窑车600、装载板700及待烧的陶瓷制品会经过U型的预热隧道110进行预热,最后到达隧道出口112。1 and FIG. 2, in this embodiment, the
请参阅图4和图3,在本实施例中,窑体的底部、窑体的侧壁以及窑盖均由耐火材料制成,窑体的底部、窑体的侧壁以及窑盖围合形成加热腔(未图示),陶瓷制品放置在装载板700上并内置于加热腔中。具体地,窑体的底部设有耐火砖,窑体的侧壁形成耐火墙,在窑盖关闭后,加热腔就是一个密闭空间。Please refer to FIG. 4 and FIG. 3 , in this embodiment, the bottom of the kiln body, the side walls of the kiln body and the kiln cover are all made of refractory materials, and the bottom of the kiln body, the side walls of the kiln body and the kiln cover are enclosed to form A heating chamber (not shown) in which the ceramic product is placed on the
在此,智能电火焰加热设备210包括多组电火焰枪211,每组电火焰枪211的一端均与窑体的侧壁连接,电火焰枪211的另一端伸入加热腔中。具体在本实施例中,如图3所示,电火焰枪211呈丰字型或F型设置,包括主杆211a和多个支杆211b;主杆211a与滑动件212a连接,支杆211b自主杆211a上沿主杆211a的横截面径向延伸形成,且多个支杆211b沿主杆211a的轴向间隔排布;支杆211b远离主杆211a的自由端处开设有喷火口211c,在烧制时,这些喷火口211c可以喷出20-30cm长的火焰。可以理解,本申请中使用电火焰加热的方式具有以下优点:其一、电火焰使用的是电能而非燃气能源,故可以实现零碳排放,十分环保。其二、由于在烧制时烧成窑200是封闭的,故在烧制过程中基本无热量流失,从而可以实现更快的升温,减少烧成时间,具体每窑的平均烧成时间至少可以减少2小时以上;而无热量流失也意味这能够节省更多的能量,至少可节省3倍以上的能量。其三、由于电火焰是高温等离子体,故可以直接接触陶瓷制品而不会导致污染,具有加热更快且陶瓷制品受热更均匀的优点;其四、在密闭的窑体中,可以根据烧制的陶瓷制品的实际需求,通过控制系统对智能电火焰加热设备210的智能控制,而实现精确的升温控制,进而确保陶瓷制品的烧成质量,有利于提高产品的良品率;当然,在烧制完成后,通过智能通风系统900,也能实现精确的降温控制,以防止出现不受控的剧烈降温而导致产品质量出现问题。Here, the intelligent electric flame heating device 210 includes multiple groups of
请参阅图4和图3,在本实施例中,智能电火焰加热设备210还包括安装在窑体的侧壁上的移动装置(未标示),电火焰枪211的一端通过移动装置安装在窑体的侧壁上;移动装置包括第一驱动机构216和滑动件212a,窑体的侧壁上设有滑动安装孔,滑动件212a安装在滑动安装孔处并与窑体的侧壁滑动连接,且滑动件212a在滑动过程中始终盖合滑动安装孔;电火焰枪211的一端与滑动件212a连接;第一驱动机构216设于窑体的外侧,并用于驱动滑动件212a以带动电火焰枪211移动以及驱动电火焰枪211旋转。这样,通过控制系统就可智能控制第一驱动机构216带动滑动件212a运动,进而实现电火焰枪211的前后、水平移动以及180°旋转,达到使得烧制的陶瓷制品受热更均匀以确保烧制质量的目的。此外,智能电火焰加热设备210还包括多组特斯拉线圈215、低压接口213、高压接口214以及工业测温计930等,其中,特斯拉线圈215、低压接口213、高压接口214均设置在窑体外部,低压接口213用于接入工业用电,然后低压接口213通过线路连接到特斯拉线圈215,再经过特斯拉线圈215升高到特定电压,并通过线路连接到高压接口214,同时,电火焰枪211通过导线与高压接口214连接,这样,在通电后,电火焰枪211的喷火口211c处就能产生电火焰来加热陶瓷制品。具体地,在窑盖关闭预备加热前,控制系统可控制第一驱动机构216实现将电火焰枪211移动到装载板700之间,同时控制丰字型的电火焰枪211旋转,以使其喷火口211c与待烧制的陶瓷制品成5°至10°的夹角;在烧制过程中,受控的滑动件212a可带动电火焰枪211同时前后、水平左右移动,当电火焰移动到陶瓷制品的边缘时,可将电火焰枪211旋转170°左右,再往回前后、水平方向左右移动,从而可使电火焰可以均匀加热陶瓷制品,同时,根据工业测温计930传回的温度变化,还可以控制丰字型电火焰枪211开启的喷火口211c的数量,以便实现对烧成窑200内的升温曲线的精确控制;在烧制完成后,窑盖打开时或预备打开时,第一驱动机构216可驱动滑动件212a以带动电火焰枪211通过前后、水平移动以及旋转180°而移回窑体的侧壁即耐火墙内。Please refer to FIG. 4 and FIG. 3 , in this embodiment, the intelligent electric flame heating device 210 further includes a moving device (not marked) installed on the side wall of the kiln body, and one end of the
进一步地,在本实施例中,窑盖包括位于里层的耐火层以层叠在耐火层外侧的金属板;烧成窑200还包括第二驱动机构(未图示)以及锁合装置(未图示);第二驱动机构安装在窑体的外表面,并与金属板连接,用于驱动窑盖打开或闭合;锁合装置设于金属板上,用于锁合或解锁窑盖。具体地,窑盖的耐火层主要由耐火砖组成,金属板优选为钢板,耐火砖与钢板通过粘合剂粘接,第二驱动机构可以但不限于为带有驱动轮的一体化驱动电机,导轨固定在烧成窑200的外侧墙面上;当控制系统发送窑盖开启指令至烧成窑200自动化管理分系统后,该管理分系统就会控制锁合装置自动解锁,然后,第二驱动机构通电,驱动电机驱动一体化的驱动轮在导轨上移动,以打开窑盖;当控制系统发送窑盖关闭指令后,其关闭过程与打开过程相反,且在窑盖关闭后,锁合装置会自动加锁,以防止在烧制过程中,窑盖突然打开而导致烧制失败甚至发生安全事故。然本设计不限于此,于其他实施例中,还可以通过其他结构设计的第二驱动机构等实现窑盖的打开与关闭。Further, in this embodiment, the kiln cover includes a refractory layer on the inner layer and a metal plate stacked on the outside of the refractory layer; the firing
此外,在本实施例中,冷却仓体的底部、冷却仓体的的侧壁以及冷却仓盖均由保温材料制成;冷却仓体的底部、冷却仓体的的侧壁以及冷却仓盖围合形成冷却腔。具体地,在冷却仓体的底部设有保温砖,冷却仓体的侧壁形成保温墙,冷却腔与智能通风系统900连通,以确保烧制完成后的陶瓷制品在被吊装设备放入冷却腔后能得到充分冷却。In addition, in this embodiment, the bottom of the cooling chamber body, the side wall of the cooling chamber body and the cooling chamber cover are all made of thermal insulation materials; the bottom of the cooling chamber body, the side wall of the cooling chamber body and the cooling chamber cover surround combined to form a cooling chamber. Specifically, the bottom of the cooling bin body is provided with thermal insulation bricks, the side walls of the cooling bin body form thermal insulation walls, and the cooling cavity is communicated with the
请参阅图8和图9,在本实施例中,装载板700的底部设有第一定位部710,窑体的底部以及冷却仓体的底部均设有与第一定位部710适配定位连接的第二定位部;此外,在装载板700的上表面还设有第三定位部720,多个装载板700可叠加设置,在防倾倒窑车600的车板610上也同样可设置第二定位部。具体地,装载板700为矩形板,当然也可以是其他根据实际需求设置的形状,第一定位部710可以但不限于是实心的定位杆,第二定位部为与定位杆适配的空心的定位孔,且为提高定位连接效果,在装载板700的四个转角处均设有一个定位杆,第三定位部720也可以为与定位杆适配的空心的定位孔。在使用时,首先将待烧制的陶瓷制品放置到装载板700上,然后,装载板700被吊装到防倾倒窑车600上时,就可以通过定位杆插入对应的定位孔中而实现装载板700的定位放置,如此,就能防止装载板700在防倾倒窑车600上发生前后左右移动。同理,当装载板700放置在烧成窑200和冷却仓300中时,也可以通过定位杆和设于烧成窑200和冷却仓300底部的定位孔的适配连接而达到防止装载板700移动的目的。Please refer to FIG. 8 and FIG. 9 , in this embodiment, the bottom of the
在此还需说明的是,在本实施例中,工业窑炉还包括保温吊装箱(未图示),保温吊装箱由保温材料制成,保温吊装箱与装载板700连接,并罩盖住放置在装载板700上的陶瓷制品,在此,保温吊装箱主要对吊装过程中的陶瓷制品的保温作用,防止陶瓷制品在吊装过程中发生较大的温度改变。具体地,保温吊装箱呈向下敞口设置,包括顶板和围住四周的四个侧板,其主要框架优选用钢材制成,顶板和侧板优选由保温材料制成;顶板的顶面上设有多个吊装勾、侧板的底部边缘则设有多组无线控制的自动锁合设备等。在吊装之前,控制系统会发送无线信号以无线控制自动锁合设备解锁;然后,等装载板700上的陶瓷制品放好后,就可移动吊装设备将保温吊装箱吊起,并罩住装载板700和陶瓷制品,此时,控制系统会无线控制自动锁合设备加锁,使得侧板底部与装载板700稳固连接,以确保在保温吊装箱吊起时装载板700不会脱落;当完成吊装,装载板700和陶瓷制品放置好后,控制系统会再次无线控制自动锁合设备解锁,以使保温吊装箱与装载板700脱离,最后,再使用吊装设备将保温吊装箱吊离。It should also be noted here that, in this embodiment, the industrial kiln further includes a thermal insulation hoisting box (not shown), the thermal insulation hoisting box is made of thermal insulation material, and the thermal insulation hoisting box is connected to the
请参阅图1、图2以及图5,在本实施例中,智能通风系统900包括风道组、多组风机940、多个通风连通装置910以及多个测温计930。预热仓100的进风口和出风口、烧成窑200的进风口和出风口、冷却仓300的进风口和出风口处均设有一通风连通装置910。风道组包括若干低温冷风通道921、若干低温热风通道922、若干中温热风通道923以及若干个高温热风通道924;高温热风通道924和中温热风通道923中均设置有测温计930,以实时测量通道中的温度,且这些温度测试值会上传至控制系统;高温热风通道924、中温热风通道923、低温热风通道922以及低温冷风通道921中均设有一风机940。在此,高温热风通道924中的高温热风温度在800℃以上,中温热风通道923中的中温热风温度在200℃至500℃之间;低温热风通道922中的低温热风温度在30℃至60℃之间;低温冷风通道921中的低温冷风温度在-40℃至10℃之间。Referring to FIG. 1 , FIG. 2 and FIG. 5 , in this embodiment, the
具体地,烧成窑200的进风口通过一通风连通装置910分别与一中温热风通道923和一高温热风通道924连通;烧成窑200的出风口通过一通风连通装置910与一高温热风通道924连通;预热仓100的进风口通过一通风连通装置910和一个高温热风通道924与烧成窑200的出风口连通,以使烧成窑200在冷却过程中的热风能够进入预热仓100中,实现热量再次利用,降低整体能耗;预热仓100的出风口通过一中温热风通道923与烧成窑200的进风口连通;冷却仓300的进风口通过一通风连通装置910分别和一个中温热风通道923、一个低温热风通道922以及一个低温冷风通道921连通;冷却仓300的出风口通过一通风连通装置910分别和一个高温热风通道924、一个中温热风通道923以及一个低温热风通道922连通,其中,均与冷却仓300的出风口连通的高温热风通道924和中温热风通道923也通过一管道连通。Specifically, the air inlet of the firing
进一步地,在本实施例中,工业窑炉还包括风干塔950,风干塔950也是完全独立的单体设置,风干塔950的进风口通过一中温热风通道923与预热仓100的出风口连通,以使预热仓100中的中温热风能够进入风干塔950中,以提高风干塔950的风干效率;风干塔950的出风口通过一低温热风通道922与冷却仓300的进风口连通,这是低温热风的一个供应渠道。此外,低温冷风通道921的一端与外界环境连通,另一端则与高温热风通道924连通,这样,外界的冷风就能和高温热风混合而形成中温热风。当然,在冷却仓300中,通过冷却仓300的进风口进入的中温热风和后来通过冷却仓300的进风口进入的低温冷风混合后即形成低温热风,该低温热风可通过冷却仓300的出风口进入对应的低温热风通道922中,以实现循环利用。Further, in this embodiment, the industrial kiln also includes an air-drying
下面详细说明本分布式高效节能环保工业窑炉的运行过程,特别是智能通风系统900的智能调度过程。The operation process of the distributed industrial kiln with high efficiency, energy saving and environmental protection, especially the intelligent scheduling process of the
首先,在装载区510,生产人员使用智能机械臂800将待烧制的陶瓷制品放在装载板700上,装载板700再通过智能机械臂800放置在防倾倒窑车600上并定位固定。First, in the
然后,装载有待烧制陶瓷制品的防倾倒窑车600进入U型的预热仓100中进行预热,预热好后到达预热仓100的隧道出口112;生产人员通过智能机械臂800将装载板700和防倾倒窑车600分离,防倾倒窑车600返回装载区510以待下次使用;在此,多块装载板700可通过智能机械臂800定位堆叠为多层,陶瓷制品即位于两相邻的装载板700之间的空间中。Then, the
然后,控制系统控制烧成窑200的窑盖打开,烧成窑200的进风口和出风口关闭;吊装设备将放置有陶瓷制品的装载板700吊入窑体的加热腔中,且最下层的装载板与窑体底部定位固定;关闭窑盖,控制系统控制智能电火焰加热设备210通电,多组电火焰枪211产生电火焰,以实现对陶瓷制品的加热;烧制完成后停电,此时,通风连通装置910受控将其中的高温风口打开,并通过对应的风机940将加热腔内的热风从烧成窑200的出风口抽送到高温热风通道924中,同时,中温风口也打开,并通过对应的风机940将中温热风从窑体的进风口处送入加热腔内以实现降温;在此,为确保烧制质量,加热腔内的温度不应当急速降低,而应当通过中温热风的输送不断缓慢降温,而且通过控制中温热风的送风量和高温热风的抽出量,以此实现对烧成窑200降温曲线的精确控制,中温热风通道923中的中温热风可来源于预热仓100以及风干塔950等处;当烧成窑200内的温度达到预设温度时,关闭中温风口,但热风还是不断抽送到高温热风通道924中,此时,可开启窑盖,实现双出风口排热风,吊装设备将保温吊装箱放入窑体内与装载板700连接,然后再将保温吊装箱和装载板700等吊出烧成窑200并放入冷却仓300中。Then, the control system controls the kiln cover of the firing
然后,当装载板700和需要冷却的陶瓷制品在冷却仓300中放置好后,通风连通装置910受控将其中的高温风口打开,并将冷却仓300中的热风通过冷却仓300的出风口抽入高温热风通道924中,同时,通风连通装置910受控将中温风口打开,将中温热风通过冷却仓300的进风口送入冷却仓300内,用于冷却仓300的第一阶段降温,在该降温阶段,通过控制中温热风的送风量和热风的抽出量,以此来实现对冷却仓300降温曲线的精确控制;在冷却仓300的温度达到预设温度时,冷却仓300内应是中温热风,此时关闭高温风口,并将冷却仓300内的中温热风通过冷却仓300的出风口抽送到中温热风通道923,同时,通风连通装置910的低温风口打开,低温热风通过通过冷却仓300的进风口从低温热风通道922中进入冷却仓300内,以实现进一步降温,如此,在此第二阶段降温后,冷却仓300内的温度会接近常温。当然,若需要进一步降温或在第二降温阶段快速降温,可将通风连通装置910的低温风口打开,然后将低温冷风通道921中的低温冷风通过冷却仓300的进风口输送进冷却仓300内。Then, after the
然后,打开冷却仓300的仓门,使用吊装设备将放置有陶瓷制品的装载板700吊出放置在卸载区520内,智能机械臂800将烧制好的陶瓷制品从装载板700上取下以便进行后续的加工处理,而空余的装载板700则留待下次使用。Then, the door of the
以上所述仅为本申请的较佳实施例而已,并不用以限制本申请,凡在本申请的精神和原则之内所作的任何修改、等同替换和改进等,均应包含在本申请的保护范围之内。The above descriptions are only preferred embodiments of the present application, and are not intended to limit the present application. Any modifications, equivalent replacements and improvements made within the spirit and principles of the present application shall be included in the protection of the present application. within the range.
Claims (17)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122187666.0U CN216205187U (en) | 2021-09-09 | 2021-09-09 | Distributed high-efficiency energy-saving environment-friendly industrial kiln |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122187666.0U CN216205187U (en) | 2021-09-09 | 2021-09-09 | Distributed high-efficiency energy-saving environment-friendly industrial kiln |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN216205187U true CN216205187U (en) | 2022-04-05 |
Family
ID=80919208
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202122187666.0U Expired - Fee Related CN216205187U (en) | 2021-09-09 | 2021-09-09 | Distributed high-efficiency energy-saving environment-friendly industrial kiln |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN216205187U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113803991A (en) * | 2021-09-09 | 2021-12-17 | 付朝品 | Distributed high-efficiency energy-saving environment-friendly industrial kiln |
-
2021
- 2021-09-09 CN CN202122187666.0U patent/CN216205187U/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113803991A (en) * | 2021-09-09 | 2021-12-17 | 付朝品 | Distributed high-efficiency energy-saving environment-friendly industrial kiln |
| CN113803991B (en) * | 2021-09-09 | 2025-01-21 | 付朝品 | Distributed high-efficiency energy-saving and environmentally friendly industrial kilns |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN104070598B (en) | The curing kilns of a kind of air energy | |
| WO2023035191A1 (en) | Distributed high-efficiency energy-saving environment-friendly industrial kiln | |
| CN107084608A (en) | A kind of sand mold, which is used, passes through type micro-wave drying system | |
| CN113803991B (en) | Distributed high-efficiency energy-saving and environmentally friendly industrial kilns | |
| CN102925635B (en) | Rail locomotive bolster lateral frame continuous pushing-disc type heat treatment production line | |
| CN201555443U (en) | Externally-heated electric heating rotary kiln | |
| CN203396236U (en) | Large size alumina ceramic substrate sintering kiln | |
| CN213873772U (en) | Green rattan brick firing equipment | |
| CN102062529A (en) | Mesh tape-free silicon cell slice sintering furnace | |
| CN108164259B (en) | Material de-gluing sintering production line | |
| CN101984508B (en) | Led aging method | |
| CN101786074B (en) | Surface coating drying technology and special device for wind power tower | |
| CN205051223U (en) | Integration photovoltaic box -type substation | |
| CN203602670U (en) | Air circulation gas furnace | |
| CN207563215U (en) | A kind of drying equipment of casting mold, sand core surface coating | |
| CN2867242Y (en) | Full-automatic curing furnace for crystal silicon solar cell package | |
| CN207358108U (en) | The drying equipment of medium-and-large-sized casting mold, sand core surface coating | |
| CN217788512U (en) | Negative pressure formation equipment | |
| CN202049226U (en) | Constant high-temperature aging house for battery cores | |
| CN201527177U (en) | Photovoltaic industry electrical furnace with thermal energy recycling device | |
| CN211367422U (en) | Photovoltaic glass anti-reflection strengthening continuous production device | |
| CN108588382A (en) | A kind of mixed type brass tube annealing furnace | |
| CN209853653U (en) | An automatic loading device for prefabricated insulation boards | |
| CN110981210B (en) | A continuous production device and method for anti-reflection strengthening of photovoltaic glass | |
| CN210943576U (en) | Graphite boat conveyer |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| TR01 | Transfer of patent right | ||
| TR01 | Transfer of patent right |
Effective date of registration: 20230829 Address after: 518000 Room 601, Nanguang Jiejia building, Shennan Middle Road, Futian District, Shenzhen, Guangdong Province Patentee after: Shenzhen Si Chao science and Technology Co.,Ltd. Address before: 518000 601 Nanguang Jiejia building, 3037 Shennan Middle Road, Futian District, Shenzhen City, Guangdong Province Patentee before: Fu Chaopin |
|
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20220405 |