CN215614619U - Servo quick material collecting device of lower mould punching sheet - Google Patents
Servo quick material collecting device of lower mould punching sheet Download PDFInfo
- Publication number
- CN215614619U CN215614619U CN202121966761.4U CN202121966761U CN215614619U CN 215614619 U CN215614619 U CN 215614619U CN 202121966761 U CN202121966761 U CN 202121966761U CN 215614619 U CN215614619 U CN 215614619U
- Authority
- CN
- China
- Prior art keywords
- section bar
- receiving
- conveying belt
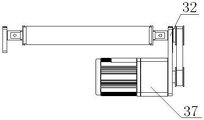
- speed reducer
- material receiving
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images





Landscapes
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
- Press Drives And Press Lines (AREA)
Abstract
The utility model discloses a servo rapid material receiving device for lower die punching sheets, which comprises a profile rack, wherein the profile rack is fixedly connected with a workbench, a conveying mechanism is arranged in the middle of the profile rack, and a motion material receiving mechanism is arranged on the profile rack; the material receiving mechanism comprises a receiving mechanism mounting seat, the bottom of the receiving mechanism mounting seat is connected with a sliding block matched with the linear rail, and a receiving mechanism is arranged on the receiving mechanism mounting seat; the electromagnetic chuck has the advantages of novel structure and convenience in use, the bottom surface of the electromagnetic chuck can be flush with the bottom surface of the feeding manipulator, the longitudinal space required by feeding and receiving is reduced, the receiving mechanism is high in speed during working, the gap of relative movement between the manipulator and a punch can be effectively utilized to complete the work, and the production efficiency is improved.
Description
Technical Field
The utility model relates to the technical field of quick material receiving devices, in particular to a servo quick material receiving device for lower die punching sheets.
Background
The permanent magnet motor mainly comprises a rotor, a stator and other parts, wherein the rotor and the stator are generally formed by stacking permanent magnet stamped sheets, the permanent magnet stamped sheets generally have a plurality of magnetic steel grooves, the distance between the magnetic steel grooves and the periphery of the stamped sheets is small, and in order to ensure the quality of the stamped sheets, part of manufacturers choose to leave the stamped sheets on a lower die; when the stamped sheet is arranged on the lower die, the common lower feeding and upper receiving integrated manipulator cannot realize the receiving function; the functional mechanical arm of the lower feeding and receiving manipulator has large thickness, needs a large longitudinal space, is slow in working speed, has small slide block stroke of a punch press, cannot realize quick receiving, and therefore needs to provide a servo quick receiving device.
Disclosure of Invention
The utility model aims to solve the technical problems and provides a servo rapid material receiving device for lower die punching sheets.
In order to achieve the technical purpose and achieve the technical requirements, the utility model adopts the technical scheme that: the utility model provides a servo quick material collecting device of lower mould punching, includes the section bar frame, its characterized in that: the section bar frame is fixedly connected with the workbench, a conveying mechanism is arranged in the middle of the section bar frame, and a moving material receiving mechanism is arranged on the section bar frame; the section bar frame comprises a rear supporting section bar, a main assembly section bar is connected onto the rear supporting section bar through a fixing seat, a linear track is arranged on the top surface of the main assembly section bar, front supports are arranged on two sides of the front end of the main assembly section bar, the front supports are connected with a workbench, an open slot is formed in the front end of the main assembly section bar, and a front limiting plate is arranged on the front end surface of the main assembly section bar;
the conveying mechanism comprises conveying belt driving roller mounting seats, the two conveying belt driving roller mounting seats are symmetrically arranged on two sides of the middle of the main assembly section bar, two ends of a conveying belt driving roller respectively penetrate through the main assembly section bar to be connected with the conveying belt driving roller mounting seats, two ends of a conveying belt driven roller are respectively arranged in open slots, conveying belts are arranged on the conveying belt driving roller and the conveying belt driven roller, a transmission sleeve is arranged at the joint of the conveying belt driven roller and the conveying belt, and bearings are arranged inside two ends of the transmission sleeve; a conveyor belt speed reducer base and a conveyor belt speed reducer connected with the conveyor belt speed reducer base are arranged on the main mounting section on one side of the conveyor belt driving roller mounting base, a conveyor belt servo motor is connected onto the conveyor belt speed reducer, and one end of the conveyor belt driving roller is connected with the conveyor belt speed reducer through a conveyor belt synchronous transmission mechanism;
the motion material receiving mechanism comprises a material receiving mechanism mounting seat, the bottom of the material receiving mechanism mounting seat is connected with a sliding block matched with the linear track, and a material receiving mechanism is arranged on the material receiving mechanism mounting seat; the material receiving servo motor is connected with the material receiving servo motor, a material receiving synchronous transmission mechanism is connected to an output shaft of the material receiving speed reducer, and the material receiving synchronous transmission mechanism is connected with the material receiving mechanism mounting seat through a power transmission seat; the receiving agencies mount pad side still is provided with the tablet, be provided with spacing proximity switch on the tablet homonymy main sectional material.
Preferably: the receiving agencies includes two receipts material arms, receive the material arm front end and be connected with a plurality of electromagnet through the locating pin, electromagnet sets up in pairs, the hole that the locating pin is connected with the receipts material arm sets up to waist shape hole, two receipts material arm symmetries set up on the receiving agencies mount pad.
Preferably: the limiting proximity switch comprises a front limiting proximity switch and a rear limiting proximity switch, and the limiting proximity switch and the material receiving synchronous transmission mechanism are arranged oppositely.
Preferably: the two ends of the conveying belt driven roller are provided with threaded holes, and the front limiting plate, the conveying belt driven roller and the bolt form a conveying belt tensioning mechanism.
Preferably: the conveyer belt speed reducer base and the material receiving driven synchronous wheel base are respectively connected with a slide block nut on the main assembly section through connecting pieces.
Compared with the traditional structure, the utility model has the beneficial effects that:
1. the electromagnetic chuck has the advantages of novel structure and convenience in use, the bottom surface of the electromagnetic chuck can be flush with the bottom surface of the feeding manipulator, the longitudinal space required by feeding and receiving is reduced, the receiving mechanism is high in speed during working, the gap of relative movement between the manipulator and a punch can be effectively utilized to complete the work, and the production efficiency is improved.
2. The equal accessible slider nut of receipts material driven synchronizing wheel seat, conveyer belt speed reducer seat is along main mounting section bar notch direction regulating distance for the tensioning hold-in range has strengthened the suitability of hold-in range, has prolonged the life cycle of hold-in range, and it is convenient to adjust.
3. The head of the driven roller of the conveying belt is provided with a threaded hole, and can be matched with a front limiting plate of a main assembly profile to tension the conveying belt, so that the slipping phenomenon of the conveying belt in the transmission process is reduced.
4. Receive the material arm front end installation electromagnet, the electromagnet position is adjustable to the punching sheet of coping different types has increased the flexibility of device.
5. The sensing plate is installed at one side edge of the receiving mechanism mounting seat, the front limit proximity switch and the rear limit proximity switch are installed on the corresponding side of the main sectional material, the front limit proximity switch and the rear limit proximity switch are used for providing front and rear end position signals required by the movement receiving mechanism, and the working stability and reliability of the movement receiving mechanism are improved.
Drawings
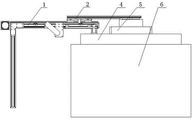
FIG. 1 is a front view of the present invention;
FIG. 2 is a top view of the present invention;
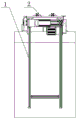
FIG. 3 is a left side view of the present invention;
FIG. 4 is a front view of the profile holder of the present invention;
FIG. 5 is a top view of FIG. 4;
FIG. 6 is a right side view of FIG. 4;
FIG. 7 is a front view of the movement collection mechanism of the present invention;
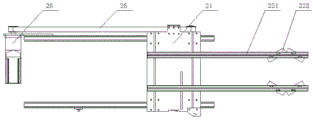
FIG. 8 is a top view of FIG. 7;
FIG. 9 is a rear view of FIG. 7;
FIG. 10 is a left side view of FIG. 7;
FIG. 11 is a front view of the delivery mechanism of the present invention;
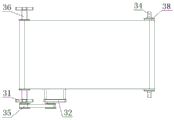
FIG. 12 is a top view of FIG. 11;
FIG. 13 is a left side view of FIG. 11;
in the figure: 1. the automatic material collecting and conveying device comprises a section bar frame, 11 parts of rear supporting section bars, 12 parts of fixing seats, 13 parts of linear rails, 14 parts of main mounting section bars, 141 parts of open grooves, 16 parts of front limiting plates, 17 parts of front supporting seats, 2 parts of moving material collecting mechanisms, 21 parts of material collecting mechanism mounting seats, 22 parts of material collecting mechanisms, 221 parts of material collecting arms, 222 parts of electromagnetic chucks, 23 parts of sliders, 24 parts of limiting proximity switches, 241 parts of front limiting proximity switches, 242 parts of rear limiting proximity switches, 25 parts of material collecting synchronous transmission mechanisms, 26 parts of material collecting speed reducers, 27 parts of material collecting speed reducer mounting seats, 28 parts of material collecting driven synchronous wheel seats, 29 parts of power transmission seats, 210 parts of induction plates, 3 parts of conveying mechanisms, 31 parts of conveying belt driving roller mounting seats, 32 parts of conveying belt speed reducing machine seats, 33 parts of conveying belts, 34 parts of conveying belts, 35 parts of conveying belt synchronous transmission mechanisms, 36 parts of conveying belt driving rollers, 37 parts of conveying belt speed reducers, 38 parts of transmission sleeves, 4. the working table, 5, the die and 6, the punch press.
Detailed Description
The present invention is further described below.
Referring to the attached drawings, the servo quick material receiving device for the lower die punching sheet comprises a section bar frame 1 and is characterized in that: the section bar frame 1 is fixedly connected with a workbench 4, a conveying mechanism 3 is arranged in the middle of the section bar frame 1, and a moving material receiving mechanism 2 is arranged on the section bar frame 1; the section bar frame 1 comprises a rear supporting section bar 11, the rear supporting section bar 11 is connected with a main mounting section bar 14 through a fixing seat 12, the top surface of the main mounting section bar 14 is provided with a linear rail 13, two sides of the front end of the main mounting section bar 14 are provided with front support seats 17, the front support seats 17 are connected with a workbench 4, the front end of the main mounting section bar 14 is provided with an open slot 141, and the front end surface of the main mounting section bar 14 is provided with a front limiting plate 16;
the conveying mechanism 3 comprises conveying belt driving roller mounting seats 31, the two conveying belt driving roller mounting seats 31 are symmetrically arranged on two sides of the middle of the main assembly section bar 14, two ends of a conveying belt driving roller 36 penetrate through the main assembly section bar 14 respectively to be connected with the conveying belt driving roller mounting seats 31, two ends of a conveying belt driven roller 34 are arranged in the open grooves 141 respectively, conveying belts 33 are arranged on the conveying belt driving roller 36 and the conveying belt driven roller 34, a transmission sleeve 38 is arranged at the joint of the conveying belt driven roller 34 and the conveying belt 33, and bearings are arranged inside two ends of the transmission sleeve 38; a conveyor belt speed reducer base 32 and a conveyor belt speed reducer 37 connected with the conveyor belt speed reducer base 32 are arranged on the main mounting section 14 on one side of the conveyor belt driving roller mounting base 31, a conveyor belt servo motor is connected to the conveyor belt speed reducer 37, and one end of the conveyor belt driving roller 36 is connected with the conveyor belt speed reducer 37 through a conveyor belt synchronous transmission mechanism 35;
the movement material receiving mechanism 2 comprises a material receiving mechanism mounting seat 21, the bottom of the material receiving mechanism mounting seat 21 is connected with a sliding block 23 matched with the linear track 13, and a material receiving mechanism 22 is arranged on the material receiving mechanism mounting seat 21; the receiving device is characterized in that a receiving driven synchronous wheel seat 28 is arranged at the front end of the outer side of the main mounting section bar 14, a receiving speed reducer mounting seat 27 and a receiving speed reducer 26 connected with the receiving speed reducer mounting seat 27 are arranged at the rear end of the outer side of the main mounting section bar, the receiving speed reducer 26 is connected with a receiving servo motor, a receiving synchronous transmission mechanism 25 is connected to the output shaft of the receiving speed reducer 26, and the receiving synchronous transmission mechanism 25 is connected with a receiving mechanism mounting seat 21 through a power transmission seat 29; the side of the receiving mechanism mounting seat 21 is also provided with an induction plate 210, and the induction plate 210 is provided with a limit proximity switch 24 on the main mounting section bar 14 on the same side.
In this preferred embodiment, the material receiving mechanism 22 includes two material receiving arms 221, the front end of the material receiving arm 221 is connected with a plurality of electromagnetic chucks 222 through positioning pins, the electromagnetic chucks 222 are arranged in pairs, holes formed by the positioning pins and the material receiving arms 221 are arranged in a waist-shaped hole, and the two material receiving arms 221 are symmetrically arranged on the material receiving mechanism mounting base 21.
In the preferred embodiment, the limit proximity switch 24 includes a front limit proximity switch 241 and a rear limit proximity switch 242, and the limit proximity switch 24 is disposed opposite to the material receiving synchronous transmission mechanism 25.
In the preferred embodiment, threaded holes are formed in two ends of the conveying belt driven roller 34, and the front limiting plate 16, the conveying belt driven roller 34 and the bolts form a conveying belt 33 tensioning mechanism.
In the preferred embodiment, the belt speed reducer seat 32 and the material receiving driven synchronous wheel seat 28 are respectively connected with the slide block nut on the main mounting section bar 14 through connecting pieces.
In specific implementation, the automatic feeding device is matched with a punch 6 and a feeding manipulator for use, after the automatic feeding device is started, the default position movement material receiving mechanism 2 is positioned at the rear limit close switch 242, and the conveying mechanism 3 always keeps running at a constant speed; when the feeding manipulator carries out primary feeding and punching of the punch is finished, a sliding block of the punch moves upwards, the receiving servo motor drives the receiving speed reducer 26 to work after receiving a signal of the punch 6, so that the receiving synchronous transmission mechanism 25 is driven to operate, the receiving synchronous transmission mechanism 25 drives the power transmission seat 29 and the receiving mechanism mounting seat 21 on the power transmission seat to move forwards and quickly enter the upper part of the die 5, and when the sensing plate 210 on the receiving mechanism mounting seat 21 reaches the front limit proximity switch 241, the electromagnetic chuck 222 works, absorbs punching sheets of a lower die of the die 5 and then quickly exits from the die 5; when the induction plate 210 on the receiving mechanism mounting seat 21 returns to the rear limit proximity switch 242, the electromagnetic chuck 222 stops working, and the punched piece falls onto the conveying belt 33, moves backwards along with the conveying belt 33, finally breaks away from the conveying belt 33, and enters a receiving box; repeating the above steps to form a complete material sending and receiving program.
The above-mentioned embodiments of the present invention are only examples for clearly illustrating the present invention, but not intended to limit the scope of the present invention, and all equivalent technical solutions also belong to the scope of the present invention, and the scope of the present invention should be defined by the claims.
Claims (5)
1. The utility model provides a servo quick material collecting device of lower mould punching, includes section bar frame (1), its characterized in that: the section bar frame (1) is fixedly connected with the workbench (4), a conveying mechanism (3) is arranged in the middle of the section bar frame (1), and a moving material receiving mechanism (2) is arranged on the section bar frame (1); the section bar frame (1) comprises a rear supporting section bar (11), the rear supporting section bar (11) is connected with a main assembly section bar (14) through a fixing seat (12), a linear rail (13) is arranged on the top surface of the main assembly section bar (14), front supports (17) are arranged on two sides of the front end of the main assembly section bar (14), the front supports (17) are connected with a workbench (4), an open slot (141) is arranged at the front end of the main assembly section bar (14), and a front limiting plate (16) is arranged on the front end surface of the main assembly section bar (14);
the conveying mechanism (3) comprises conveying belt driving roller mounting seats (31), the two conveying belt driving roller mounting seats (31) are symmetrically arranged on two sides of the middle of a main assembly section bar (14), two ends of a conveying belt driving roller (36) penetrate through the main assembly section bar (14) respectively to be connected with the conveying belt driving roller mounting seats (31), two ends of a conveying belt driven roller (34) are arranged in open grooves (141) respectively, conveying belts (33) are arranged on the conveying belt driving roller (36) and the conveying belt driven roller (34), a transmission sleeve (38) is arranged at the joint of the conveying belt driven roller (34) and the conveying belt (33), and bearings are arranged inside two ends of the transmission sleeve (38); a conveyor belt speed reducer base (32) and a conveyor belt speed reducer (37) connected with the conveyor belt speed reducer base (32) are arranged on the main installation section (14) on one side of the conveyor belt driving roller mounting base (31), a conveyor belt servo motor is connected onto the conveyor belt speed reducer (37), and one end of a conveyor belt driving roller (36) is connected with the conveyor belt speed reducer (37) through a conveyor belt synchronous transmission mechanism (35);
the moving material receiving mechanism (2) comprises a material receiving mechanism mounting seat (21), the bottom of the material receiving mechanism mounting seat (21) is connected with a sliding block (23) matched with the linear track (13), and a material receiving mechanism (22) is arranged on the material receiving mechanism mounting seat (21); the receiving device is characterized in that a receiving driven synchronous wheel seat (28) is arranged at the front end of the outer side of the main mounting section bar (14), a receiving speed reducer mounting seat (27) and a receiving speed reducer (26) connected with the receiving speed reducer mounting seat (27) are arranged at the rear end of the outer side of the main mounting section bar, the receiving speed reducer (26) is connected with a receiving servo motor, a receiving synchronous transmission mechanism (25) is connected to the output shaft of the receiving speed reducer (26), and the receiving synchronous transmission mechanism (25) is connected with a receiving mechanism mounting seat (21) through a power transmission seat (29); the receiving agencies mount pad (21) side still is provided with tablet (210), be provided with spacing proximity switch (24) on tablet (210) homonymy owner dress section bar (14).
2. The servo rapid material receiving device for the lower die punching sheet as claimed in claim 1, which is characterized in that: receiving agencies (22) include two receipts material arms (221), it is connected with a plurality of electromagnetic chuck (222) through the locating pin to receive material arm (221) front end, electromagnetic chuck (222) set up in pairs, the hole that locating pin and receipts material arm (221) are connected sets up to waist shape hole, two receive material arm (221) symmetries and set up on receiving agencies mount pad (21).
3. The servo rapid material receiving device for the lower die punching sheet as claimed in claim 1, which is characterized in that: the limiting proximity switch (24) comprises a front limiting proximity switch (241) and a rear limiting proximity switch (242), and the limiting proximity switch (24) and the material receiving synchronous transmission mechanism (25) are arranged oppositely.
4. The servo rapid material receiving device for the lower die punching sheet as claimed in claim 1, which is characterized in that: threaded holes are formed in two ends of the conveying belt driven roller (34), and the front limiting plate (16), the conveying belt driven roller (34) and the bolts form a conveying belt (33) tensioning mechanism.
5. The servo rapid material receiving device for the lower die punching sheet as claimed in claim 1, which is characterized in that: the conveyer belt speed reducer base (32) and the material receiving driven synchronous wheel base (28) are respectively connected with a slide block nut on the main mounting section bar (14) through connecting pieces.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202121966761.4U CN215614619U (en) | 2021-08-20 | 2021-08-20 | Servo quick material collecting device of lower mould punching sheet |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202121966761.4U CN215614619U (en) | 2021-08-20 | 2021-08-20 | Servo quick material collecting device of lower mould punching sheet |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN215614619U true CN215614619U (en) | 2022-01-25 |
Family
ID=79900060
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202121966761.4U Active CN215614619U (en) | 2021-08-20 | 2021-08-20 | Servo quick material collecting device of lower mould punching sheet |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN215614619U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102022116488A1 (en) | 2022-07-01 | 2024-01-04 | Hsf Automation Gmbh | Gripping device for a punching system, dividing head, punching system and method for adapting a gripping device and a dividing head |
-
2021
- 2021-08-20 CN CN202121966761.4U patent/CN215614619U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| DE102022116488A1 (en) | 2022-07-01 | 2024-01-04 | Hsf Automation Gmbh | Gripping device for a punching system, dividing head, punching system and method for adapting a gripping device and a dividing head |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201036799Y (en) | Automatic transferring mechanical arm | |
| CN219966187U (en) | Stamping head convenient replacement structure of stamping die | |
| CN110883881B (en) | Furniture board groover | |
| CN113084533A (en) | Double-root synchronous corner penetrating stacking machine | |
| CN114570797B (en) | A CNC forming device for the labyrinth groove of the end of the refrigerator shell | |
| CN120243764A (en) | A stamping equipment for automobile parts production | |
| CN109676050A (en) | A kind of punching machine automatic charging device | |
| CN219378755U (en) | Elastic suspension type punching feeding device and movable feeding equipment | |
| CN218891151U (en) | Sheet inner cavity side wall spin riveting mechanism | |
| CN215902519U (en) | Novel feeding mechanism of character bending machine | |
| CN218555272U (en) | Multi-station high-precision ultra-thin special material in-mold riveting cold stamping die | |
| CN219632420U (en) | Punching machine with garbage collection function | |
| CN111872253B (en) | Feeding mechanism for mechanical stamping capable of feeding and positioning rapidly | |
| CN210586761U (en) | Conveying structure pushed by cylinder of numerical control lathe for fixing die | |
| CN220837535U (en) | High-speed progressive stamping device for iron core production | |
| CN219688364U (en) | Interval feeding mechanism for metal processing | |
| CN221342460U (en) | Track structure for conveying circuit board | |
| CN207839836U (en) | A kind of continuous punching die device with rotation function | |
| CN217315348U (en) | Positioning and adjusting device for machining hardware stamping parts | |
| CN223836447U (en) | A double-plate feeding mechanism | |
| CN219561137U (en) | Automatic riveter | |
| CN218556394U (en) | Feeding fixing mechanism for sheet metal part machining | |
| CN222587927U (en) | A punching machine feeding tool | |
| CN221136171U (en) | Shearing mechanism is used in production of plastics meal pad | |
| CN223616998U (en) | Conveying equipment for automobile body-in-white welding production line |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |