CN215431833U - An automatic cutting and blanking device for pipe materials - Google Patents
An automatic cutting and blanking device for pipe materials Download PDFInfo
- Publication number
- CN215431833U CN215431833U CN202122060326.1U CN202122060326U CN215431833U CN 215431833 U CN215431833 U CN 215431833U CN 202122060326 U CN202122060326 U CN 202122060326U CN 215431833 U CN215431833 U CN 215431833U
- Authority
- CN
- China
- Prior art keywords
- feeding
- cutting
- cylinder
- supporting
- automatic
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images



Landscapes
- Sawing (AREA)
Abstract
The utility model discloses an automatic cutting and blanking device for pipe fitting materials, which comprises a rack and a PLC (programmable logic controller) installed on the rack; the automatic cutting device is characterized by further comprising an automatic cutting mechanism for automatically cutting the pipe fittings on the mounting rack, a supporting and feeding mechanism for supporting and feeding the pipe fittings and an automatic blanking mechanism for blanking the cut pipe fittings. The utility model realizes automatic feeding, clamping, cutting and discharging through the arrangement and the matched use of the PLC controller, the automatic cutting mechanism, the supporting feeding mechanism and the automatic discharging mechanism, has high automation degree, low labor intensity, low labor demand and high efficiency, simultaneously improves the accuracy of the cutting position of the pipe fitting, and improves the quality of the cut product; through the arrangement of the supporting and feeding mechanism, the pipe fitting is supported and simultaneously clamped and fed, automatic feeding is carried out on the pipe fitting through the feeding mechanism, and manual feeding is not needed.
Description
Technical Field
The utility model relates to automatic cutting of pipe fitting materials, in particular to an automatic cutting and blanking device for pipe fitting materials.
Background
At present, a positioning tool is arranged in most of factories when cutting pipes, the positioning tool is matched with an electric saw for use, the cutting distance is limited and positioned by the positioning tool, then the electric saw is used for cutting the pipes by an operator, although the adopted positioning tool does not need to measure the size during each cutting by the arrangement of the positioning tool, the mode is still relatively troublesome during operation, manual feeding, clamping, cutting and blanking are needed, and for some pipes needing to be cut at two ends, the pipe needs to be turned around for cutting after the cutting at one end is finished, even a tool is possibly designed for positioning the cutting at the other end, the efficiency is lower, the labor intensity of the operator is high, the labor demand is high, the automation degree is low, and the requirement of large-batch workpieces cannot be met; an automatic cutting and blanking device for pipe fitting materials is provided.
SUMMERY OF THE UTILITY MODEL
The utility model aims to solve the problems and provides an automatic cutting and blanking device for pipe fitting materials.
In order to achieve the aim, the utility model provides an automatic cutting and blanking device for pipe fitting materials, which comprises a rack and a PLC (programmable logic controller) installed on the rack, wherein the PLC is used for controlling the automatic cutting and blanking device to cut and discharge the pipe fitting materials; the automatic cutting device is characterized by further comprising an automatic cutting mechanism for automatically cutting the pipe fittings on the mounting rack, a supporting and feeding mechanism for supporting and feeding the pipe fittings and an automatic blanking mechanism for blanking the cut pipe fittings.
Further preferably, the supporting and feeding mechanism comprises a supporting mechanism and a feeding mechanism; the supporting mechanism comprises a supporting frame, a pushing cylinder arranged on the supporting frame, a pushing block arranged on the supporting frame in a sliding manner, a positioning block arranged on the supporting frame and corresponding to the pushing block, a jacking cylinder arranged on one side of the supporting frame and a jacking block arranged on the jacking cylinder; and the rack is also provided with a supporting mechanism.
Further preferably, a guide wheel bracket is further installed on the other side of the support frame, and a guide wheel is installed on the guide wheel bracket.
Preferably, the feeding mechanism is installed on the frame and the supporting mechanism, the feeding mechanism comprises a guide rod installed on the supporting frame and the frame, a feeding cylinder installed on the supporting frame, a feeding seat installed on the guide rod in a sliding manner and connected with the cylinder, a feeding rod installed on the feeding seat, and a clamping cylinder installed on the feeding rod, and the clamping cylinder is further provided with a clamping jaw.
Further preferably, the automatic cutting mechanism comprises a sliding rod mounted on the frame, a servo motor mounted on the frame, a screw rod movably mounted on the frame and in transmission connection with the servo motor, a nut seat movably mounted on the screw rod, a moving seat slidably mounted on the sliding rod and fixedly connected with the nut seat, a cutting motor mounted on the moving seat, a protective shell mounted on the moving seat, and a cutting blade arranged on the moving seat and in transmission connection with the cutting motor through a belt.
Further preferably, the protective shell is further provided with a material channel, the protective shell is further provided with an empty groove corresponding to the material channel in position, the protective shell is further provided with a material pressing cylinder, the material pressing cylinder is provided with a pressing block, and the pressing block is located in the empty groove and corresponds to the material channel in position.
Further preferably, the material channel, the protective shell and the pressing block are all provided with cutting grooves corresponding in position.
Preferably, the automatic blanking mechanism comprises a blanking cylinder arranged on the rack, a rotating rod movably arranged on the rack, a supporting rod arranged on the rotating rod, a clamping cylinder arranged on the supporting rod and a clamping jaw arranged on the clamping cylinder; the unloading cylinder movable mounting has the connecting rod, the connecting rod other end and rotary rod fixed connection.
According to the automatic pipe fitting cutting machine, the PLC, the automatic cutting mechanism, the supporting feeding mechanism and the automatic blanking mechanism are arranged and used in a matched mode, automatic feeding, clamping, cutting and blanking are achieved, the automation degree is high, the labor intensity is low, the labor demand is low, the efficiency is high, meanwhile, the accuracy of the pipe fitting cutting position is improved, and the quality of a cut product is improved;
the supporting and feeding mechanism is arranged, so that the pipe fitting is supported, clamped and fed, and the pipe fitting is automatically fed by the feeding mechanism without manual feeding;
through the setting of automatic unloading mechanism, the pipe fitting after will cutting carries out automatic unloading and stacks it with the waste material subregion, need not follow-up staff and picks, saves the process, reduces intensity of labour.
Drawings
FIG. 1 is a schematic structural view of the present invention;
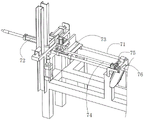
FIG. 2 is a schematic view of a part of the supporting and feeding mechanism of the present invention;
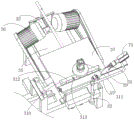
FIG. 3 is a schematic view of a partial structure of an automatic cutting mechanism and an automatic blanking mechanism in the present invention;
FIG. 4 is a schematic structural view of an automatic blanking mechanism in the utility model;
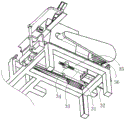
FIG. 5 is a schematic view of another perspective of the automatic cutting mechanism of the present invention;
FIG. 6 is a partial schematic view of the automatic cutting mechanism of the present invention;
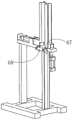
fig. 7 is a schematic structural view of the support mechanism of the present invention.
Illustration of the drawings: 1. a frame; 2. a PLC controller; 3. an automatic cutting mechanism; 31. a slide bar; 32. a servo motor; 33. a screw rod; 34. a nut seat; 35. a movable seat; 36. cutting the motor; 37. a protective shell; 38. cutting the slices; 39. a material channel; 310. an empty groove; 311. a material pressing cylinder; 312. briquetting; 313. cutting the groove; 4. supporting the feeding mechanism; 5. an automatic blanking mechanism; 51. a blanking cylinder; 52. rotating the rod; 53. a strut; 54. a material clamping cylinder; 55. a connecting rod; 6. a support mechanism; 61. a support frame; 62. tightly pushing the air cylinder; 63. a pushing block; 64. positioning blocks; 65. jacking a cylinder; 66. jacking blocks; 67. a guide wheel bracket; 68. a guide wheel; 7. a feeding mechanism; 71. a guide bar; 72. a feeding cylinder; 73. a feeding seat; 74. a feed bar; 75. a clamping cylinder; 76. a clamping jaw.
Detailed Description
The automatic cutting and blanking device for pipe materials according to the present invention will be further described with reference to the accompanying drawings.
Referring to fig. 1, the automatic cutting and blanking device for pipe materials of the present embodiment includes a frame 1 and a PLC controller 2 installed on the frame 1; the automatic cutting device is characterized by also comprising an automatic cutting mechanism 3 for automatically cutting the pipe fittings, a supporting and feeding mechanism 4 for supporting and feeding the pipe fittings and an automatic blanking mechanism 5 for blanking the cut pipe fittings, which are arranged on the mounting rack 1; the PLC controller 2, the automatic cutting mechanism 3, the supporting feeding mechanism 4 and the automatic blanking mechanism 5 are arranged and used in a matched mode, so that automatic feeding, clamping, cutting and blanking are achieved, the automation degree is high, the labor intensity is low, the labor demand is low, and the efficiency is high; the supporting and feeding mechanism 4 is arranged, so that the pipe fitting is supported, clamped and fed, and the pipe fitting is automatically fed through the feeding mechanism 7 without manual feeding; through the setting of automatic unloading mechanism 5, the pipe fitting after will cutting carries out automatic unloading and stacks it with the waste material subregion, need not follow-up staff and picks, saves the process, reduces intensity of labour.
Further, referring to fig. 1-2, the supporting and feeding mechanism 4 comprises a supporting mechanism 6 and a feeding mechanism 7; the supporting mechanism 6 comprises a supporting frame 61, a pushing cylinder 62 arranged on the supporting frame 61, a pushing block 63 slidably arranged on the supporting frame 61, a positioning block 64 arranged on the supporting frame 61 and corresponding to the pushing block 63, a jacking cylinder 65 arranged on one side of the supporting frame 61 and a jacking block 66 arranged on the jacking cylinder 65; the frame 1 is also provided with a supporting mechanism 6; the pushing block 63 is pushed to move by the arrangement of the pushing cylinder 62, so that the distance between the pushing block 63 and the positioning block 64 is changed, and the pipe fitting is suitable for pipe fittings of different sizes and models; through the setting of jacking cylinder 65, drive jacking piece 66 upward movement for the jacking pipe fitting is placed the height of adjusting on support frame 61 to the pipe fitting.
Further, referring to fig. 7, a guide wheel bracket 67 is further installed on the other side of the support frame 61, a guide wheel 68 is installed on the guide wheel bracket 67, and a certain assistance effect is exerted on the movement of the pipe fitting through the arrangement of the guide wheel 68, so that the friction force during the movement is reduced.
Further, referring to fig. 2, the feeding mechanism 7 is mounted on the frame 1 and the supporting mechanism 6, the feeding mechanism 7 includes a guide rod 71 mounted on the supporting frame 61 and the frame 1, a feeding cylinder 72 mounted on the supporting frame 61, a feeding base 73 slidably mounted on the guide rod 71 and connected to the feeding cylinder 72, a feeding rod 74 mounted on the feeding base 73, and a clamping cylinder 75 mounted on the feeding rod 74, and a clamping jaw 76 is further mounted on the clamping cylinder 75; the guide rod 71 is arranged to guide and support the feeding seat 73; the feeding cylinder 72 drives the feeding seat 73 to move, the feeding seat 73 drives the feeding rod 74 and the clamping cylinder 75 to move, and the clamping cylinder 75 clamps the pipe fitting through the clamping jaw 76, so that the pipe fitting is driven to carry out automatic feeding.
Further, referring to fig. 3 and 5-6, the automatic cutting mechanism 3 includes a sliding rod 31 mounted on the frame 1, a servo motor 32 mounted on the frame 1, a lead screw 33 movably mounted on the frame 1 and in transmission connection with the servo motor 32, a nut seat 34 movably mounted on the lead screw 33, a moving seat 35 slidably mounted on the sliding rod 31 and fixedly connected with the nut seat 34, a cutting motor 36 mounted on the moving seat 35, a protective shell 37 mounted on the moving seat 35, and a cutting blade 38 disposed on the moving seat 35 and in transmission connection with the cutting motor 36 through a belt; the servo motor 32 drives the screw rod 33 to rotate, the screw rod 33 drives the moving seat 35 to move through matching with the nut seat 34, so that the cutting motor 36 and the cutting blade 38 are driven to move, the cutting blade 38 is enabled to frequently cut the pipe fitting, and automatic cutting is achieved.
Further, as shown in fig. 3-4, a material channel 39 is further installed on the protective shell 37, an empty slot 310 corresponding to the material channel 39 is further provided on the protective shell 37, a material pressing cylinder 311 is further installed on the protective shell 37, a pressing block 312 is installed on the material pressing cylinder 311, and the pressing block 312 is located in the empty slot 310 and corresponds to the material channel 39; through the arrangement of the empty groove 310, the position of the pressing block 312 is limited and the pressing block is guided; the pressing cylinder 311 drives the pressing block 312 to move up and down, so that the pipe fitting is pressed tightly, and the phenomenon that the size and the shape of a cut product are unqualified due to the fact that the cutting position is changed due to displacement or jumping of the pipe fitting during cutting is avoided; by the arrangement of the protective shell 37, the safety during cutting is increased.
Further, referring to fig. 3, the material channel 39, the protective shell 37 and the pressing block 312 are provided with cutting grooves 313 corresponding to each other in position; by the arrangement of the cutting groove 313, the material channel 39, the protective shell 37 and the pressing block 312 are prevented from interfering with the cutting sheet 38.
Further, referring to fig. 3-4, the automatic blanking mechanism 5 includes a blanking cylinder 51 mounted on the frame 1, a rotating rod 52 movably mounted on the frame 1, a supporting rod 53 mounted on the rotating rod 52, a clamping cylinder 54 mounted on the supporting rod 53, and a clamping jaw 76 disposed on the clamping cylinder 54; the blanking cylinder 51 is movably provided with a connecting rod 55, and the other end of the connecting rod 55 is fixedly connected with the rotating rod 52; the clamping jaw 76 is driven by the clamping cylinder to clamp the cut pipe fitting, then the blanking cylinder 51 pushes the connecting rod 55, the connecting rod 55 drives the rotating rod 52 to rotate, so that the clamping cylinder 54 and the pipe fitting are driven to rotate, the pipe fitting is moved to the pipe fitting stacking position, and the cut waste material is ejected out of the material channel 39 along with the feeding of the subsequent pipe fitting and falls into a waste material area, so that the subsequent staff is not required to pick the waste material, the working procedure is saved, and the labor intensity is reduced.
The working process of the utility model is as follows: referring to fig. 1-7, firstly, a worker drives a pushing block 63 to move through a pushing cylinder 62, drives a jacking block 66 to ascend through a jacking cylinder 65, so as to adjust the position of the pushing block 63 according to the size of a pipe, adjusts the position of the jacking block 66 according to the height requirement, places the raw material of the pipe on a support frame 61, controls a material clamping cylinder 54 on the support frame 61 to start through a PLC (programmable logic controller) 2, drives a clamping jaw 76 to clamp the pipe, then starts a feeding cylinder 72, drives a feeding seat 73 to move forward through the feeding cylinder 72, so as to drive the pipe to move forward, enables one end of the pipe to move to a material channel 39, and releases the feeding cylinder 72 to reset after the clamping jaw 76 moves forward to a set position; then the PLC 2 controls the pressing cylinder 311 to start, the pressing cylinder 311 drives the pressing block 312 to move downwards to press the pipe, then the cutting motor 36 is started to drive the cutting blade 38 to rotate, meanwhile, the servo motor 32 is started, the servo motor 32 drives the screw rod 33 to rotate, the screw rod 33 drives the moving seat 35 to move through the cooperation with the nut seat 34, the moving seat 35 drives the cutting motor 36 and the cutting blade 38 to move forwards until the cutting blade 38 cuts off the pipe and then resets, then the feeding cylinder 72 is started again to drive the pipe to be conveyed forwards, at the moment, one end of the pipe pushes out the pipe finished product which is just cut along the material channel 39, then the clamping cylinder 75 on the automatic blanking mechanism 5 is started to control the clamping jaw 76 to clamp the pipe finished product, then the blanking cylinder 51 is started, the blanking cylinder 51 pushes the connecting rod 55 forwards to drive the connecting rod 55 and the rotating rod 52 to rotate, the rotating rod 52 drives the material clamping cylinder 54 and the finished pipe fittings to rotate, and the clamping jaws 76 are loosened after the finished pipe fittings are transferred to a finished product stacking area and then reset, so that the finished pipe fittings are stacked together.
The scope of protection of the utility model is not limited to the above embodiments and variations thereof. The present invention is not limited to the above embodiments, but may be modified in various ways.
Claims (8)
1. An automatic cutting and blanking device for pipe fitting materials comprises a rack (1) and a PLC (programmable logic controller) controller (2) arranged on the rack (1); the automatic cutting device is characterized by further comprising an automatic cutting mechanism (3) for automatically cutting the pipe fittings on the mounting rack (1), a supporting and feeding mechanism (4) for supporting and feeding the pipe fittings and an automatic blanking mechanism (5) for blanking the cut pipe fittings.
2. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 1, wherein: the supporting and feeding mechanism (4) comprises a supporting mechanism (6) and a feeding mechanism (7); the supporting mechanism (6) comprises a supporting frame (61), a pushing cylinder (62) arranged on the supporting frame (61), a pushing block (63) slidably arranged on the supporting frame (61), a positioning block (64) arranged on the supporting frame (61) and corresponding to the pushing block (63), a jacking cylinder (65) arranged on one side of the supporting frame (61) and a jacking block (66) arranged on the jacking cylinder (65); and a support mechanism (6) is also arranged on the frame (1).
3. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 2, wherein: a guide wheel support (67) is further mounted on the other side of the support frame (61), and a guide wheel (68) is mounted on the guide wheel support (67).
4. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 2, wherein: the feeding mechanism (7) is installed on the rack (1) and the supporting mechanism (6), the feeding mechanism (7) comprises a guide rod (71) installed on the supporting frame (61) and the rack (1), a feeding cylinder (72) installed on the supporting frame (61), a feeding seat (73) installed on the guide rod (71) in a sliding mode and connected with the feeding cylinder (72), a feeding rod (74) installed on the feeding seat (73) and a clamping cylinder (75) installed on the feeding rod (74), and a clamping jaw (76) is further installed on the clamping cylinder (75).
5. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 1, wherein: the automatic cutting mechanism (3) comprises a sliding rod (31) installed on the rack (1), a servo motor (32) installed on the rack (1), a screw rod (33) movably installed on the rack (1) and in transmission connection with the servo motor (32), a nut seat (34) movably installed on the screw rod (33), a moving seat (35) slidably installed on the sliding rod (31) and in fixed connection with the nut seat (34), a cutting motor (36) installed on the moving seat (35), a protective shell (37) installed on the moving seat (35) and a cutting blade (38) arranged on the moving seat (35) and connected with the cutting motor (36) through belt transmission.
6. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 5, wherein: still install material way (39) on protective housing (37), still be equipped with on protective housing (37) and say empty groove (310) that (39) position corresponds with the material, still install on protective housing (37) and press material cylinder (311), press and install briquetting (312) on material cylinder (311), briquetting (312) are in empty groove (310) and are corresponding with material way (39) position.
7. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 6, wherein: the material channel (39), the protective shell (37) and the pressing block (312) are provided with cutting grooves (313) corresponding in position.
8. The automatic cutting and blanking device for pipe fitting materials as claimed in claim 1, wherein: the automatic blanking mechanism (5) comprises a blanking cylinder (51) arranged on the rack (1), a rotating rod (52) movably arranged on the rack (1), a support rod (53) arranged on the rotating rod (52), a clamping cylinder (54) arranged on the support rod (53) and a clamping jaw (76) arranged on the clamping cylinder (54); the blanking air cylinder (51) is movably provided with a connecting rod (55), and the other end of the connecting rod (55) is fixedly connected with the rotating rod (52).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122060326.1U CN215431833U (en) | 2021-08-30 | 2021-08-30 | An automatic cutting and blanking device for pipe materials |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202122060326.1U CN215431833U (en) | 2021-08-30 | 2021-08-30 | An automatic cutting and blanking device for pipe materials |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN215431833U true CN215431833U (en) | 2022-01-07 |
Family
ID=79697275
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202122060326.1U Expired - Fee Related CN215431833U (en) | 2021-08-30 | 2021-08-30 | An automatic cutting and blanking device for pipe materials |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN215431833U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117260853A (en) * | 2023-09-08 | 2023-12-22 | 东莞市银科智芯科技有限公司 | An automatic cutting production line for oil cup tubes |
-
2021
- 2021-08-30 CN CN202122060326.1U patent/CN215431833U/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN117260853A (en) * | 2023-09-08 | 2023-12-22 | 东莞市银科智芯科技有限公司 | An automatic cutting production line for oil cup tubes |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN112387848B (en) | Rapid bar cutting machine and cutting method thereof | |
| CN101428426A (en) | Automatic shearing method for pouring head | |
| CN110112871B (en) | Automatic production line of motor stator | |
| CN107009219B (en) | Lens processing device | |
| CN116460318A (en) | Numerical control lathe for machining thin-wall workpiece and method thereof | |
| CN115570365B (en) | Automated production equipment for telescopic rod and control method thereof | |
| CN111515414A (en) | Machine vision auxiliary unmanned numerical control turning machine tool | |
| CN111266492A (en) | Automatic wire feeding system for thermocouple compensation wire | |
| CN109850622B (en) | Intelligent logistics cutting production line | |
| CN118699474B (en) | Rod-shaped hydraulic cylinder processing and cutting mechanism | |
| CN220880735U (en) | Stainless steel pipe cutting device | |
| CN114798896A (en) | Multifunctional profile pipe fitting punching equipment and punching and cutting method | |
| CN201455534U (en) | Full-automatic screw welding machine | |
| CN220073982U (en) | Automatic rod piece machining equipment | |
| CN209465535U (en) | A kind of new automatic hole punched device | |
| CN218837968U (en) | Slicer for meat product processing | |
| CN211866468U (en) | Automatic wire feeding system for thermocouple compensation wire | |
| CN215657582U (en) | Wire cutting machine | |
| CN210755447U (en) | Copper bar cutting device | |
| CN105149401A (en) | Fully-automatic key blank punch press | |
| CN210451188U (en) | Automatic sawing and conveying integrated equipment for continuous casting copper bars | |
| CN206263333U (en) | Automatic cutting machine | |
| CN107214779B (en) | A centre gripping transport mechanism for chopping block processing | |
| CN220196464U (en) | Adjustable positioning device for plate cutting equipment | |
| CN218224914U (en) | Heat pipe end cutting device that contracts |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20220107 |