Disclosure of Invention
In view of the above technical problem, the utility model aims at providing a compatible punctuation and storage mode car seat delivery platform, this delivery platform can realize multiple product collineation, satisfies the punctuation delivery demand of customer simultaneously.
In order to achieve the above purpose, the utility model adopts the following technical scheme:
a vehicle seat delivery platform compatible with punctualization and storage modes comprises a first speed chain packing and conveying mechanism, a second speed chain packing and conveying line, a third speed chain packing and conveying line, a first speed chain transition conveying line, a second speed chain transition conveying line, a jacking and transferring mechanism, a conveying mechanism, a first lifting mechanism, a second lifting mechanism, a third lifting mechanism, a steel platform and a main controller;
the first speed chain packing and conveying mechanism is in butt joint with seat outlets of a front-row seat production line and a mixed line production line; the second double-speed chain packing conveying line is in butt joint with a seat outlet of a rear-row seat production line with slow production rhythm; the third speed chain packing conveying line is arranged close to the first speed chain transition conveying line;
the speed-multiplying chain packing and conveying mechanism comprises N speed-multiplying chain conveying lines, the N speed-multiplying chain conveying lines are distributed in a snake shape, jacking and transferring mechanisms are arranged at the head ends and the tail ends of two adjacent speed-multiplying chain conveying lines, a transmission mechanism is arranged between the head ends and the tail ends of the two speed-multiplying chain conveying lines which are relatively far away from each other, the jacking and transferring mechanisms are used for jacking trays on the speed-multiplying chain conveying lines and transferring the trays in a direction perpendicular to the speed-multiplying chain conveying lines, and the two adjacent speed-multiplying chain conveying lines are butted through the jacking and transferring mechanisms and the transmission mechanism; the tail end of the last speed-multiplying chain conveying line is also provided with a jacking and transferring mechanism, the jacking and transferring mechanism is butted with one end of a conveying mechanism outside the speed-multiplying chain conveying line after jacking, the other end of the conveying mechanism is arranged close to a ladder entrance of a first lifting mechanism, the bottom of the first lifting mechanism is provided with the conveying mechanism, the first lifting mechanism and the ladder entrance are opposite to a ladder exit, and the ladder exit is arranged close to a seat delivery warehouse;
a steel platform is arranged above the speed-multiplying chain conveying mechanism, the steel platform and the speed-multiplying chain conveying mechanism form a two-layer structure, a second speed-multiplying chain packing conveying line and a first speed-multiplying chain transition conveying line are respectively arranged on two sides of the speed-multiplying chain conveying mechanism, a second lifting mechanism is arranged between the second speed-multiplying chain packing conveying line and the steel platform, a jacking and transferring mechanism is arranged at a position, opposite to the second lifting mechanism, of the second speed-multiplying chain packing conveying line, a transmission mechanism is arranged at the bottom of the second lifting mechanism, when the second lifting mechanism is not lifted, the transmission mechanism at the bottom is in butt joint with the jacking mechanism lifted on the second speed-multiplying chain packing conveying line, and the transmission mechanism at the bottom is in butt joint with the steel platform after the second lifting mechanism is lifted;
a transmission mechanism is arranged at the butt joint position of the steel platform and the second lifting mechanism, the transmission mechanism close to the second lifting mechanism is vertically butted with the first speed-multiplying chain warehousing conveying line, a jacking and transferring mechanism is arranged at the position of the first speed-multiplying chain warehousing conveying line opposite to the transmission mechanism, and the tail end of the first speed-multiplying chain warehousing conveying line is butted with the rotary speed-multiplying chain transition line; the rotating speed-multiplying chain transition line can rotate by 90 degrees, the rotating speed-multiplying chain transition line is butted with a second speed-multiplying chain warehousing conveying line after rotating by 90 degrees, the second speed-multiplying chain warehousing conveying line is perpendicular to the first speed-multiplying chain warehousing conveying line, and a tray on the first speed-multiplying chain warehousing conveying line can enter the second speed-multiplying chain warehousing conveying line after passing through the rotating speed-multiplying chain transition line;
the steel platform is also provided with a second speed doubling chain ex-warehouse conveying line parallel to the second speed doubling chain in-warehouse conveying line, a plurality of seat storage libraries are arranged between the second speed doubling chain in-warehouse conveying line and the second speed doubling chain out-warehouse conveying line at intervals, and the in-warehouse end and the out-warehouse end of each seat storage library are provided with scanners for scanning trays entering the seat storage libraries or trays exiting the seat storage libraries and sending scanning results to the main controller; the bottoms of the plurality of seat storage libraries are provided with transmission mechanisms; jacking and transferring mechanisms are arranged on the second speed-doubling chain warehousing conveying line and the second speed-doubling chain ex-warehousing conveying line and are opposite to the seat storage warehouse;
the end part of the second speed doubling chain ex-warehouse conveying line is vertically butted with the first speed doubling chain ex-warehouse conveying line, one end of the first speed doubling chain ex-warehouse conveying line, which is butted with the second speed doubling chain ex-warehouse conveying line, is provided with a jacking rotating mechanism, and the jacking rotating mechanism is used for checking and rotating the placing direction of the trays on the first speed doubling chain ex-warehouse conveying line so as to enable the directions of the ex-warehouse trays to be consistent; the other end of the first speed-multiplying chain ex-warehouse conveying line is vertically butted with the transmission mechanism, and a jacking and transferring mechanism is arranged at the position, opposite to the transmission mechanism, of the first speed-multiplying chain ex-warehouse conveying line; the other end of the transmission mechanism close to the first speed-multiplying chain delivery conveying line is butted with the transmission mechanism at the bottom of the lifted third lifting mechanism, the transmission mechanism at the bottom is butted with a second speed-multiplying chain transition conveying line when the third lifting mechanism is not lifted, the tail end of the second speed-multiplying chain transition conveying line is vertically butted with the first speed-multiplying chain transition conveying line, a jacking and transferring mechanism is arranged at the position where the head end of the first speed-multiplying chain transition conveying line is butted with the second speed-multiplying chain transition conveying line, the tail end of the first speed-multiplying chain transition conveying line is vertically butted with the end part of one of the speed-multiplying chain conveying lines, and a scanner is arranged at the end part of the speed-multiplying chain conveying line butted with the first speed-multiplying chain transition conveying line;
the third speed chain packing conveying line and the first speed chain transition conveying line are arranged in parallel, the position where the third speed chain packing conveying line and the first speed chain transition conveying line are in butt joint is provided with a jacking transfer mechanism, and trays on the third speed chain packing conveying line are transmitted to the first speed chain transition conveying line through the jacking transfer mechanism.
As the utility model discloses preferred, speed chain transfer chain, second speed chain packing transfer chain are bilayer structure, including last speed chain, lower speed chain, last speed chain is used for the delivery, lower speed chain is used for the transport of empty tray; a fourth lifting mechanism is arranged on the outer side of the first speed-multiplying chain transition conveying line, a first empty tray speed-multiplying chain empty return line is arranged between the fourth lifting mechanism and a lower speed-multiplying chain of the speed-multiplying chain conveying line opposite to the fourth lifting mechanism, one end of the first empty tray speed-multiplying chain empty return line is in butt joint with a transmission mechanism at the bottom of the fourth lifting mechanism when the first empty tray speed-multiplying chain empty return line is not lifted, the other end of the first empty tray speed-multiplying chain empty return line is in butt joint with the end part of the speed-multiplying chain conveying line, and empty trays on the first empty tray speed-multiplying chain empty return line are conveyed to the upper layer through the fourth lifting mechanism; an empty tray speed-multiplying chain diversion line, a second empty tray speed-multiplying chain empty return line and a third empty tray speed-multiplying chain empty return line are further arranged between the speed-multiplying chain conveying line and the second speed-multiplying chain packing conveying line, the empty tray speed-multiplying chain diversion line is arranged close to the stacker crane, a scanner is arranged at the end of the empty tray speed-multiplying chain diversion line, two jacking and transferring mechanisms are arranged on the empty tray speed-multiplying chain diversion line at intervals, one jacking and transferring mechanism is in butt joint with a lower speed-multiplying chain of the speed-multiplying chain conveying line opposite to the first empty tray speed-multiplying chain empty return line, and the other jacking and transferring mechanism is in butt joint with a lower speed-multiplying chain of the other speed-multiplying chain conveying line; the second empty tray speed-multiplying chain empty return line is vertically butted with an empty tray speed-multiplying chain shunt line, the third empty tray speed-multiplying chain empty return line and the second empty tray speed-multiplying chain empty return line are arranged in parallel, the position where the second empty tray speed-multiplying chain empty return line is butted with the third empty tray speed-multiplying chain empty return line is provided with a jacking and transferring mechanism, the other end of the third empty tray speed-multiplying chain empty return line is butted with a lower speed-multiplying chain of the second speed-multiplying chain packing conveying line, the position where the third empty tray speed-multiplying chain empty return line is butted with the second speed-multiplying chain packing conveying line is provided with a jacking and transferring mechanism, the position where the second speed-multiplying chain packing conveying line is butted with the third empty tray speed-multiplying chain empty return line is provided with a jacking and transferring mechanism, the tail end of the lower speed-multiplying chain of the second speed-multiplying chain packing conveying line is provided with a jacking and transferring mechanism, and transferring mechanism is butted with the bottom of a fifth lifting and transferring mechanism outside the lower speed-multiplying chain of the second speed-multiplying chain packing conveying line, and conveying the empty tray on the lower speed-multiplying chain of the second speed-multiplying chain packing conveying line to the upper layer through a fifth lifting mechanism.
As the utility model discloses a preferred, one side of fourth elevating system still sets up monitor, alarm, the monitor is used for detecting whether empty tray that lets in the fourth elevating system has accumulatively, if empty tray piles up the influence operation, then sends inductive signal for main control unit, and main control unit starts the alarm and reports to the police, and personnel manually discharge empty tray.
As the utility model discloses a preferred, seat delivery storehouse is bilayer structure to the one end that second elevating system kept away from the shipment mouth as the parting line is stock unit, and the one end that is close to the shipment mouth is delivery unit, and four independent conveying mechanism are installed respectively to upper and lower two-layer stock unit and delivery unit, and inside the seat that carries from second elevating system entered into stock unit under conveying mechanism's effect, and the rethread conveying mechanism carries the seat to delivery unit after upper and lower two-layer stock unit all filled the seat, accomplishes the loading through the shipment mouth at last.
As the utility model discloses a preferred, rotatory doubly fast chain transition line includes rotary mechanism and installs the doubly fast chain line body on rotary mechanism, rotary mechanism is used for the rotation of the doubly fast chain line body of drive.
As the optimization of the utility model, the jacking and transferring mechanism comprises a fixed plate, a supporting plate, a long side plate, a short side plate, a cylinder, a motor, a driving shaft, a long driven shaft, a short driven shaft and a driving wheel; the device comprises a fixed plate, a supporting plate, a main controller and a speed-multiplying chain conveying line body, wherein the fixed plate is arranged on the speed-multiplying chain conveying line body, two symmetrically arranged air cylinders are arranged between the fixed plate and the supporting plate, bases of the air cylinders are fixed to the bottom of the supporting plate, telescopic rods of the air cylinders face the fixed plate, and the main controller controls the air cylinders to act, so that the supporting plate is jacked up; the long side plates are arranged at two short sides of the supporting plate, the long side plates and the supporting plate form a frame type structure, a driving shaft and a long driven shaft are arranged between the two long side plates, two short side plates are arranged on the supporting plate and on the inner sides of the two long side plates, and a short driven shaft is arranged between the long side plates and the short side plates; a driving chain wheel is arranged on the driving shaft and is connected with an output shaft of a motor arranged at the bottom of the supporting plate through a chain; all be provided with the sprocket on both ends of driving shaft, short driven shaft and the long driven shaft, through chain drive between two adjacent sprockets, still install the drive wheel on the both ends of driving shaft and long driven shaft, the short driven shaft, main control unit control motor rotates, and the motor drives the driving shaft and rotates, and the driving shaft drives short driven shaft, long driven shaft and rotates, and the drive wheel on driving shaft, long driven shaft, the short driven shaft rotates, realizes the removal to the tray on the jacking transfer mechanism.
As the optimization of the utility model, the jacking rotating mechanism comprises a bottom plate, a motor fixing plate, a motor top plate, a cylinder, a motor and a photoelectric switch; the motor fixing plate comprises a base plate, a motor fixing plate, a telescopic rod, a guide post and a motor fixing plate, wherein two cylinders are installed on the base plate, the telescopic rod of each cylinder penetrates through the base plate and is arranged between the base plate and the motor fixing plate, four guide sleeves are installed on the base plate and on the outer sides of the two cylinders, the guide posts are installed in the guide sleeves, and the top ends of the guide posts are inserted into installation seats at the bottom of the motor fixing plate and are fixedly connected with the motor fixing plate through bolts; a floating fixing seat is installed at a position, opposite to the telescopic rod of the air cylinder, of the motor fixing plate, a floating connecting block is installed at the end part of the telescopic rod of the air cylinder, and the floating connecting block is installed in the floating fixing seat; motor avoiding units are processed on the bottom plate and the motor fixing plate, the motor is arranged on the motor avoiding units, the motor is installed on the motor fixing plate through a motor connecting piece, and a motor gear is installed on an output shaft of the motor; the motor top plate is arranged on the motor fixing plate, the motor top plate can rotate relative to the motor fixing plate, a driven gear is arranged at the bottom of the motor top plate, the driven gear is meshed with the motor gear, the motor top plate is driven to rotate through a motor, a fixing pin is machined at a position above the motor top plate, which is opposite to a third empty tray double-speed chain empty return line and a through hole of a tray on a first double-speed chain ex-warehouse conveying line, and the end part of the fixing pin is of a conical structure; a buffer fixed block or a hydraulic buffer is also arranged between the motor top plate and the motor fixed plate; the photoelectric switch is arranged on the third empty tray speed-multiplying chain empty return line and the first speed-multiplying chain delivery line and used for detecting the directions of the trays delivered from the third empty tray speed-multiplying chain empty return line and the first speed-multiplying chain delivery line and sending detection information to the main controller, and the main controller controls the motor to rotate forwards or reversely according to the detection information of the photoelectric switch.
As the utility model discloses a preferred, first elevating system, second elevating system, third elevating system, fourth elevating system, fifth elevating system are the same structure, include: the device comprises a frame, a transmission system, a lifting platform, a transmission mechanism, a sensor and a protective cushion block; the two sides of the frame, which are in butt joint with the speed-doubling chain conveying line, are of an open structure, one side of the frame is an elevator entrance, the side opposite to the elevator entrance is an elevator exit, the frame is provided with a sensor, the sensor is used for detecting the position information of the lifting platform and sending a detection signal to the main controller, guide rails are machined on the two opposite side walls of the frame, and four protective cushion blocks are arranged at the bottom of the frame at intervals; the transmission system is arranged at the top end of the frame, the lifting platform is driven to lift through the transmission system, the lifting platform is arranged above the protective cushion block and is in transmission with the transmission system through a chain or a belt, guide wheels are arranged on two sides of the lifting platform through connecting pieces and are arranged in the guide rails and roll up and down along the guide rails, a transmission mechanism is arranged on the lifting platform and is in butt joint with a double-speed chain transmission line, the transmission mechanism comprises two brackets and a motor which are symmetrically arranged, the brackets are fixed on the lifting platform, a plurality of driven shafts and a driving shaft are arranged between the two brackets, the driving shaft and the motor on the lifting platform are in transmission through the chain or the belt, chain wheels are arranged at the end parts of the driving shaft and the driven shaft, the two adjacent chain wheels are in transmission through the chain, and rolling wheels are also arranged at the two ends of the driving shaft and the driven shaft, the main controller controls the motor to rotate, the motor drives the driving shaft to rotate, and the driving shaft drives the driven shaft to rotate, so that the rolling wheels are driven to rotate.
The utility model has the advantages and beneficial effect:
(1) the utility model provides a many products collineation problem can be solved to the delivery platform, and this platform is applicable to 5 kinds of products, and the mixed line is shipped, and its installation is compact, and occupation space is little, and the steel platform on two layers can enough realize seat storage function moreover, can't satisfy the technological problem of punctuality delivery when the setting of two layers of platforms can also solve current many products collineation simultaneously.
(2) The utility model provides a delivery platform can realize that empty tray returns delivery end from the irregular back automatic classification of returning of host computer factory, can realize the automatic rotation of distinguishing to the tray that needs distinguish the direction moreover, guarantees that the empty tray direction that returns is unanimous, the follow-up delivery of being convenient for.
Detailed Description
The technical solutions in the embodiments of the present application will be clearly and completely described below with reference to the drawings in the embodiments of the present application, and it is obvious that the described embodiments are only a part of the embodiments of the present application, and not all of the embodiments. All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present application.
In the description of the present application, it is to be noted that the terms "inside", "below", and the like refer to orientations or positional relationships based on orientations or positional relationships shown in the drawings or orientations or positional relationships that are conventionally arranged when products of the application are used, and are used only for convenience in describing the application and simplifying the description, but do not indicate or imply that the devices or elements referred to must have a specific orientation, be constructed in a specific orientation, and be operated, and thus, should not be construed as limiting the application. Furthermore, the terms "first," "second," and the like are used merely to distinguish one description from another, and are not to be construed as indicating or implying relative importance.
In the description of the present application, it is also to be noted that, unless otherwise explicitly specified or limited, the terms "disposed" and "connected" are to be interpreted broadly, e.g., as being either fixedly connected, detachably connected, or integrally connected; they may be mechanically coupled, directly coupled, indirectly coupled through intervening media, or may be interconnected between two elements. The specific meaning of the above terms in the present application can be understood in a specific case by those of ordinary skill in the art.
Example 1
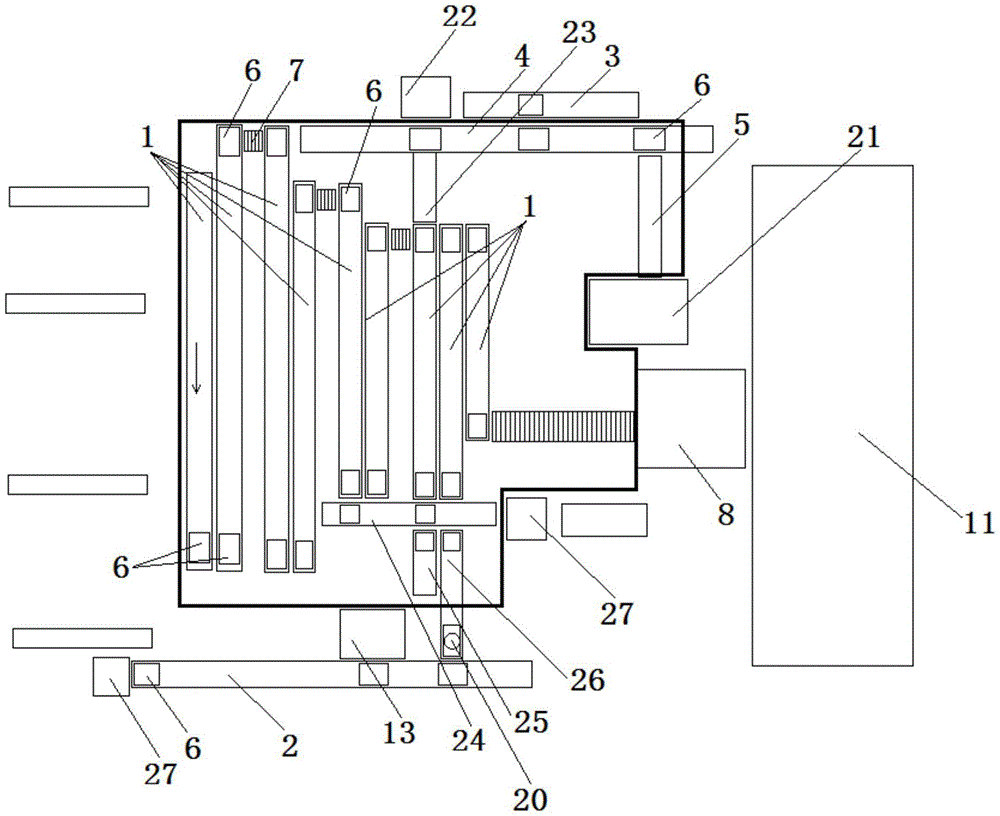
Referring to fig. 1 to 4, the utility model provides a compatible punctuality and storage mode car seat delivery platform, including first doubly fast chain packing conveyor, second doubly fast chain packing transfer chain 2, third doubly fast chain packing transfer chain 3, first doubly fast chain transition transfer chain 4, second doubly fast chain transition transfer chain 5, jacking transfer mechanism 6, transmission mechanism 7, first elevating system 8, second elevating system 9, third elevating system 10, steel platform 12, main control unit;
the first speed chain packing and conveying mechanism is in butt joint with seat outlets of a front-row seat production line and a mixed line production line; the second double-speed chain packing and conveying line 2 is in butt joint with a seat outlet of a rear-row seat production line with slow production rhythm; the third speed chain packing conveying line 3 is arranged close to the first speed chain transition conveying line 4;
the speed-multiplying chain packing and conveying mechanism comprises N speed-multiplying chain conveying lines 1, the N speed-multiplying chain conveying lines are distributed in a snake shape, jacking and transferring mechanisms 6 are arranged at the head ends and the tail ends of two adjacent speed-multiplying chain conveying lines 1, a conveying mechanism 7 is arranged between the head ends and the tail ends of the two speed-multiplying chain conveying lines 1 which are relatively far away from each other, the jacking and transferring mechanisms 6 are used for jacking pallets on the speed-multiplying chain conveying lines and transferring the pallets in the direction perpendicular to the speed-multiplying chain conveying lines, and the two adjacent speed-multiplying chain conveying lines 1 are butted through the jacking and transferring mechanisms 6 and the conveying mechanism 7; the tail end of the last speed-multiplying chain conveying line 1 is also provided with a jacking and transferring mechanism 6, the jacking and transferring mechanism is butted with one end of a conveying mechanism 7 outside the speed-multiplying chain conveying line after being jacked up, the other end of the conveying mechanism 7 is arranged close to a ladder entrance door opening of a first lifting mechanism 8, the bottom of the first lifting mechanism 8 is provided with the conveying mechanism, the first lifting mechanism and the ladder entrance door opening are opposite to a ladder exit door opening, and the ladder exit door opening is arranged close to a seat delivery warehouse 11;
a steel platform 12 is arranged above the speed-multiplying chain conveying mechanism, the steel platform and the speed-multiplying chain conveying mechanism form a two-layer structure, a second speed-multiplying chain packing conveying line 2 and a first speed-multiplying chain transition conveying line 4 are respectively arranged on the upper side and the lower side of the speed-multiplying chain conveying mechanism, a second lifting mechanism 13 is arranged between the second speed-multiplying chain packing conveying line 2 and the steel platform 12, a jacking transfer mechanism 6 is arranged at a position, opposite to the second lifting mechanism 13, of the second speed-multiplying chain packing conveying line 2, a transmission mechanism is arranged at the bottom of the second lifting mechanism, when the second lifting mechanism is not lifted, the transmission mechanism at the bottom is in butt joint with the jacking transfer mechanism lifted on the second speed-multiplying chain packing conveying line, and after the second lifting mechanism 13 is lifted, the transmission mechanism at the bottom is in butt joint with the steel platform;
a transmission mechanism 7 is arranged at the butt joint position of the steel platform 12 and the second lifting mechanism, the transmission mechanism close to the second lifting mechanism is vertically butt-jointed with a first speed-multiplying chain warehousing conveying line 14, a jacking transfer mechanism 6 is arranged at the position of the first speed-multiplying chain warehousing conveying line 14 opposite to the transmission mechanism 7, and the tail end of the first speed-multiplying chain warehousing conveying line is butt-jointed with a rotary speed-multiplying chain transition line 15; the rotating speed-multiplying chain transition line 15 can rotate by 90 degrees, the rotating speed-multiplying chain transition line 15 rotates by 90 degrees and then is in butt joint with a second speed-multiplying chain warehousing conveying line 16, the second speed-multiplying chain warehousing conveying line 16 is perpendicular to the first speed-multiplying chain warehousing conveying line 14, and a tray on the first speed-multiplying chain warehousing conveying line 14 can enter the second speed-multiplying chain warehousing conveying line 16 after passing through the rotating speed-multiplying chain transition line 15;
a second speed doubling chain ex-warehouse conveying line 17 parallel to the second speed doubling chain in-warehouse conveying line 16 is further arranged on the steel platform, a plurality of seat storage libraries 18 are arranged between the second speed doubling chain in-warehouse conveying line 16 and the second speed doubling chain out-warehouse conveying line 17 at intervals, and scanners are arranged at the in-warehouse end and the out-warehouse end of each seat storage library and used for scanning trays entering the seat storage libraries 18 or trays going out of the seat storage libraries and sending scanning results to the main controller; the bottoms of the plurality of seat storage libraries are provided with transmission mechanisms; a jacking and transferring mechanism 6 is arranged on the second speed doubling chain warehousing conveying line 16 and the second speed doubling chain ex-warehousing conveying line 17 at the position opposite to the seat storage warehouse, so that the tray can enter the seat storage warehouse 18 after the jacking and transferring mechanism on the second speed doubling chain warehousing conveying line is jacked up, and the tray can be ex-warehouse after the jacking and transferring mechanism on the second speed doubling chain ex-warehousing conveying line is jacked up;
the end part of the second speed doubling chain ex-warehouse conveying line 17 is vertically butted with the first speed doubling chain ex-warehouse conveying line 19, a jacking rotating mechanism 20 is arranged at one end, butted with the second speed doubling chain ex-warehouse conveying line, of the first speed doubling chain ex-warehouse conveying line, and the jacking rotating mechanism 20 is used for checking and rotating the placing direction of the trays on the first speed doubling chain ex-warehouse conveying line 19 so as to enable the direction of the ex-warehouse trays to be consistent; the other end of the first speed doubling chain ex-warehouse conveying line 19 is vertically butted with the transmission mechanism 7, and a jacking and transferring mechanism 6 is arranged at the position, opposite to the transmission mechanism, of the first speed doubling chain ex-warehouse conveying line; the other end of the transmission mechanism close to the first speed-multiplying chain delivery conveying line is butted with the transmission mechanism at the bottom of the lifted third lifting mechanism 21, the transmission mechanism at the bottom is butted with a second speed-multiplying chain transition conveying line 5 when the third lifting mechanism is not lifted, the tail end of the second speed-multiplying chain transition conveying line 5 is vertically butted with a first speed-multiplying chain transition conveying line 4, a jacking and transferring mechanism 6 is arranged at the position where the head end of the first speed-multiplying chain transition conveying line 4 is butted with the second speed-multiplying chain transition conveying line, the tail end of the first speed-multiplying chain transition conveying line 4 is vertically butted with the end part of one of the speed-multiplying chain conveying lines 1, and a scanner is arranged at the end part of the speed-multiplying chain conveying line 1 butted with the first speed-multiplying chain transition conveying line 4;
third doubly fast chain packing transfer chain 3 and 4 parallel arrangement of first doubly fast chain transition transfer chain, the position of third doubly fast chain packing transfer chain 3 and the butt joint of first doubly fast chain transition transfer chain all is provided with jacking transfer mechanism 6, transmits the tray on the third doubly fast chain packing transfer chain to first doubly fast chain transition transfer chain on through jacking transfer mechanism.
Further, the speed doubling chain conveying line and the second speed doubling chain packing conveying line are both of a double-layer structure and comprise an upper speed doubling chain a and a lower speed doubling chain b, the upper speed doubling chain is used for delivering goods, and the lower speed doubling chain is used for conveying empty trays; a fourth lifting mechanism 22 is arranged on the outer side of the first speed-multiplying chain transition conveying line 4, a first empty tray speed-multiplying chain empty return line 23 is arranged between the fourth lifting mechanism and a lower speed-multiplying chain b of the speed-multiplying chain conveying line opposite to the fourth lifting mechanism, one end of the first empty tray speed-multiplying chain empty return line 23 is in butt joint with a transmission mechanism at the bottom of the fourth lifting mechanism 22 when the empty tray speed-multiplying chain empty return line is not lifted, the other end of the first empty tray speed-multiplying chain empty return line 23 is in butt joint with the end part of the speed-multiplying chain conveying line 1, and empty trays on the first empty tray speed-multiplying chain empty return line are conveyed to the upper layer through the fourth lifting mechanism; an empty tray speed-multiplying chain diversion line 24, a second empty tray speed-multiplying chain empty return line 25 and a third empty tray speed-multiplying chain empty return line 26 are further arranged between the speed-multiplying chain conveying line 1 and the second speed-multiplying chain packing conveying line 2, the empty tray speed-multiplying chain diversion line 24 is arranged close to the stacker crane 27, a scanner is arranged at the end of the empty tray speed-multiplying chain diversion line 26, two jacking transfer mechanisms 6 are arranged on the empty tray speed-multiplying chain diversion line 26 at intervals, one of the jacking transfer mechanisms is in butt joint with a lower speed-multiplying chain of the speed-multiplying chain conveying line 1 opposite to the first empty tray speed-multiplying chain empty return line 23, and the other jacking transfer mechanism is in butt joint with a lower speed-multiplying chain of the other speed-multiplying chain conveying line 1; the empty return line 25 of the speed-multiplying chain of the second empty tray is vertically butted with the speed-multiplying chain diversion line 24 of the empty tray, the empty return line 26 of the speed-multiplying chain of the third empty tray is arranged in parallel with the empty return line 25 of the speed-multiplying chain of the second empty tray, the empty return line of the speed-multiplying chain of the second empty tray is butted with the empty return line of the speed-multiplying chain of the third empty tray, the other end of the empty return line 26 of the speed-multiplying chain of the third empty tray is butted with the lower speed-multiplying chain of the second speed-multiplying chain packing conveying line 2, the jacking rotating mechanism 20 is arranged at the position where the empty return line 26 of the speed-multiplying chain of the third empty tray is butted with the second speed-multiplying chain packing conveying line, the jacking transferring mechanism 6 is arranged at the position where the empty return line 2 of the speed-multiplying chain of the third empty tray is butted with the lower speed-multiplying chain 26 of the third empty tray, the jacking transferring mechanism 6 is arranged at the tail end of the lower speed-multiplying chain of the jacking rotating chain of the second speed-multiplying chain packing conveying line, and transferring mechanism is vertically butted with the bottom of the fifth lifting mechanism 27 at the outer side of the lower speed-multiplying chain of the second speed-multiplying chain transferring mechanism and the second speed multiplying chain of the second speed multiplying chain The conveying mechanisms are in butt joint, and empty trays on the lower speed doubling chain of the second speed doubling chain packing conveying line are conveyed to the upper layer through a fifth lifting mechanism 27.
One side of fourth elevating system still sets up monitor, alarm, the monitor is used for detecting whether empty tray that lets in the fourth elevating system piles up, if empty tray piles up the influence operation, then sends inductive signal for main control unit, and main control unit starts the alarm and reports to the police, and personnel manually discharge empty tray.
The seat delivery storehouse is bilayer structure to the one end that the export was kept away from as the partition line to second elevating system is the stock unit, and the one end that is close to the export is the delivery unit, and four independent conveying mechanism are installed respectively to upper and lower two-layer stock unit and delivery unit, and inside the seat that carries from second elevating system entered into the stock unit under conveying mechanism's effect, and the rethread conveying mechanism carries the seat to the delivery unit after the seat was all filled to upper and lower two-layer stock unit, and the loading is accomplished through the export at last.
With continued reference to fig. 4, the rotating speed-multiplying chain transition line 15 includes a rotating mechanism 151 and a speed-multiplying chain body 152 mounted on the rotating mechanism, and the rotating mechanism is configured to drive the speed-multiplying chain body to rotate;
referring to fig. 5 to 7, the jacking-moving mechanism 6 includes: a fixed plate 610, a supporting plate 69, a long side plate 68, a short side plate 64, a cylinder 63, a motor 61, a driving shaft 66, a long driven shaft 67, a short driven shaft 65 and a driving wheel 611; the fixed plate 610 is mounted on the double-speed chain conveyor line body, two symmetrically arranged air cylinders 63 are mounted between the fixed plate 610 and the supporting plate 69, bases of the air cylinders 63 are fixed to the bottom of the supporting plate 69, telescopic rods of the air cylinders 63 face the fixed plate, and the air cylinders are controlled by the main controller to act, so that the supporting plate is jacked; the long side plates 68 are mounted on two short sides of the supporting plate 69, the long side plates 68 and the supporting plate 69 form a frame type structure, a driving shaft 66 and a long driven shaft 67 are mounted between the two long side plates 68, two short side plates 64 are arranged on the supporting plate 69 and on the inner sides of the two long side plates 68, and a short driven shaft 65 is mounted between the long side plates 68 and the short side plates 64; a driving chain wheel 612 is installed on the driving shaft 66, and the driving chain wheel 612 is connected with an output shaft of the motor 61 installed at the bottom of the supporting plate through a chain; all be provided with sprocket 613 on the both ends of driving shaft, short driven shaft and the long driven shaft, through chain drive between two adjacent sprockets, still install drive wheel 611 on the both ends of driving shaft and long driven shaft, the short driven shaft, main control unit control motor rotates, and the motor drives the driving shaft and rotates, and the driving shaft drives short driven shaft, long driven shaft and rotates, and the drive wheel on driving shaft, long driven shaft, the short driven shaft rotates, realizes the removal to the tray on the jacking transfer mechanism. Guide sleeve mounting holes are processed on the supporting plate, guide sleeves are mounted on the guide sleeve mounting holes, guide posts 62 are arranged on the fixing plate and on two sides of each air cylinder, and the guide posts are mounted in the guide sleeves.
Referring to fig. 8 to 11, the lifting and rotating mechanism 20 includes a bottom plate 201, a motor fixing plate 202, a motor top plate 203, an air cylinder 204, a motor 205, and a photoelectric switch 206; the motor fixing plate comprises a base plate 201, a motor fixing plate 202, a guide post 208 and a guide post 204, wherein two air cylinders 204 are installed on the base plate 201, telescopic rods of the air cylinders 204 penetrate through the base plate 201 and are arranged between the base plate 201 and the motor fixing plate 202, four guide sleeves 207 are installed on the base plate 201 and on the outer sides of the two air cylinders, the guide sleeves are internally provided with the guide post 208, and the top end of the guide post 208 is inserted into an installation seat 2021 at the bottom of the motor fixing plate 202 and is fixedly connected with the motor fixing plate 202 through bolts; a floating fixing seat 209 is installed at a position where the motor fixing plate 202 is opposite to an expansion link of the air cylinder, a floating connecting block 2010 is installed at the end part of the expansion link of the air cylinder, and the floating connecting block 2010 is installed in the floating fixing seat 209; a motor avoiding unit 2011 is processed on the bottom plate and the motor fixing plate, the motor is arranged on the motor avoiding unit 11, the motor is arranged on the motor fixing plate 202 through a motor connecting piece 2014, and a motor gear 2051 is arranged on an output shaft of the motor; the motor top plate 203 is arranged on the motor fixing plate 202, the motor top plate 203 can rotate relative to the motor fixing plate 202, a driven gear is arranged at the bottom of the motor top plate 203, the driven gear is meshed with the motor gear, the motor top plate 203 is driven to rotate through a motor 205, a fixing pin 2012 is processed at a position above the motor top plate 203, which is opposite to a through hole of a tray on a third empty tray double-speed chain empty return line and a first double-speed chain ex-warehouse conveying line, the end part of the fixing pin is of a conical structure, and a buffering fixing block and/or a hydraulic buffer 2013 are arranged between the motor top plate and the motor fixing plate; the photoelectric switch 206 is installed on the third empty tray speed-multiplying chain empty return line and the first speed-multiplying chain delivery line, and is used for detecting the position of a tray conveyed from the third empty tray speed-multiplying chain empty return line and the first speed-multiplying chain delivery line (an iron column is arranged on one side of the tray, and the photoelectric switch judges the position of the tray by sensing whether the iron column is detected or not) and sending detection information to the main controller.
Referring to fig. 12 and 13, the first lifting mechanism, the second lifting mechanism, the third lifting mechanism, the fourth lifting mechanism, and the fifth lifting mechanism are all the same structure, and the first lifting mechanism 8 includes: the device comprises a frame 81, a transmission system 82, a lifting platform 83, a transmission mechanism, a sensor 85 and a protective cushion block 810; the two sides of the frame 1, which are in butt joint with the double-speed chain conveying line, are of an open structure, one side of the frame is an entrance door, the side opposite to the entrance door is an exit door, the frame is provided with a sensor 85, the sensor 85 is used for detecting the position information of the lifting platform and sending a detection signal to the main controller, two opposite side walls of the frame 81 are provided with guide rails 86, and four protective cushion blocks 810 are arranged at intervals at the bottom of the frame; the transmission system 82 is installed at the top end of the frame 81, the lifting platform 83 is driven to lift through the transmission system 82, the lifting platform 83 is arranged above the protective cushion block 810, the lifting platform is connected with the transmission system 82 through a chain or a belt, guide wheels 87 are installed on two sides of the lifting platform 83 through connecting pieces 813, the guide wheels 87 are arranged in the guide rails 86 and roll up and down along the guide rails, a transmission mechanism is installed on the lifting platform 83 and is in butt joint with a double-speed chain conveying line, the transmission mechanism comprises two brackets 88 and a motor 84 which are symmetrically arranged, the brackets 88 are fixed on the lifting platform 83, a plurality of driven shafts and a driving shaft 89 are installed between the two brackets 83, the driving shaft 89 and the motor 84 on the lifting platform 83 are in transmission through a chain or a belt, and chain wheels 814 are installed at the end parts of the driving shaft and the driven shafts, the two adjacent chain wheels are driven by chains, rolling wheels 811 are further mounted at two ends of the driving shaft and the driven shaft, the main controller controls the motor to rotate, the motor drives the driving shaft to rotate, and the driving shaft drives the driven shaft to rotate, so that the rolling wheels are driven to rotate.
Further, a straight ladder 811 is arranged outside the frame, and a guard rail 812 is arranged around the top end of the frame.
Example 2
A use method of a car seat delivery platform compatible with a punctuality and storage mode specifically comprises the following steps:
step S1, a production line of rear-row seats with slow production rhythm produces a batch of seats in advance, and when the produced seats are conveyed to a seat outlet, the seats are placed on a tray of the second-speed chain packing conveying line 2 by an intelligent robot;
step S2, when the tray on the second speed doubling chain packing conveying line 2 reaches the position corresponding to the second lifting mechanism 13, the main controller controls the jacking and transferring mechanism to jack up, and the tray is conveyed into the second lifting mechanism 8 under the action of the jacking and transferring mechanism 6 and the bottom conveying mechanism of the second lifting mechanism 8;
step S3, the main controller controls the second lifting mechanism 8 to lift, trays in the second lifting mechanism are conveyed to the first speed-multiplying chain warehousing conveying line 14 through the conveying mechanism 7 on the steel platform, the first speed-multiplying chain warehousing conveying line 14 is in butt joint with the rotating speed-multiplying chain transition line 15, the trays enter the rotating speed-multiplying chain transition line 15 along the first speed-multiplying chain warehousing conveying line 14, then the main controller controls the rotating speed-multiplying chain transition line 15 to rotate, the rotating speed-multiplying chain transition line 15 is in butt joint with the second speed-multiplying chain warehousing conveying line 16, and the trays enter the second speed-multiplying chain warehousing conveying line 16 along the rotating speed-multiplying chain transition line;
step S4, the main controller controls the storage position of the tray by controlling the lifting of the lifting and transferring mechanism 6 on the second double-speed chain warehousing conveyor line 16, the two-dimensional code information on the seat is scanned by the scanner installed at the front end of the seat storage 18 before the tray is stored in the seat storage 18, and then the two-dimensional code information is associated with the two-dimensional code information of the tray and stored in the main controller; all the stored seats are used as standby, and when the delivery requirements cannot be met, the seats can be delivered from the seat storage library so as to meet the delivery punctuality;
step S5, when the main controller receives a delivery task, the seat production line starts to work, when seats produced by the front seat production line and the mixed line production line are conveyed to a seat outlet, the intelligent robot puts the seats on a tray of the first speed chain packing and conveying mechanism, then scans two-dimensional code information on the seats, associates the two-dimensional code information with the two-dimensional code information of the placed tray, and stores the two-dimensional code information in the main controller; the production line of the back row seat with slow production rhythm continues to produce and put in storage according to the steps of S1-S4 for standby;
step S6, the trays bearing the seats are sequentially conveyed according to the route of the first speed-multiplying chain packing and conveying mechanism, and when the position reaches the junction of the first speed-multiplying chain transition conveying line 4 and the speed-multiplying chain conveying line 1, the main controller selects and controls the trays on the third speed-multiplying chain packing and conveying line 3 to pass in advance or the trays sent from the seat storage 18 to pass in advance according to the delivery sequence given by the tasks;
step S7, when a tray passes through the junction, the scanner mounted at the junction reads the two-dimensional code information passing through the tray and then sends the two-dimensional code information to the main controller, the main controller checks the acquired information with the shipping sequence set in the main controller, and when the information is consistent, the sequentially conveyed trays are continuously conveyed according to the route of the first double-speed chain packing and conveying mechanism and finally conveyed into the seat shipping warehouse 11; when the main controller detects that the order of the conveyed trays is different from the delivery order set in the system, controlling the speed-doubling chain conveying line at the junction to reversely rotate and discharging the trays;
step S8, when the seat delivery warehouse 11 is full of seats, driving a conveying mechanism inside the seat delivery warehouse to complete delivery;
step S9, when the delivered empty trays return, all the trays are placed on a stacker crane, the stacker crane places the empty trays on the empty tray speed-multiplying chain diversion line 26, a scanner at the end of the empty tray speed-multiplying chain diversion line 26 scans the empty trays and sends scanning information to a main controller, and the main controller judges an empty tray return line according to the scanning information;
step S10, if the empty pallet needs to return to the delivery end of the second speed-doubling chain packing and conveying line 2, the main controller controls the jacking and transferring mechanisms 6 on the second speed-doubling chain empty return line 25 and the third speed-doubling chain empty return line 26 to lift, at this time, the pallet on the empty pallet speed-doubling chain diversion line 26 enters the third speed-doubling chain empty return line 26, when the position of the jacking rotary mechanism 20 of the third empty pallet double-speed chain empty return line is reached, the main controller controls the jacking rotary mechanism 20 to lift, meanwhile, the positive and negative rotation conditions of the jacking and rotating mechanism are judged according to the detection information of the photoelectric switch in the jacking and rotating mechanism 20, the checking of the placing direction of the empty trays is realized, the empty trays after the angle adjustment are finally conveyed to a fifth lifting mechanism through a lower speed multiplying chain of the second speed multiplying chain packing conveyor line 2, conveying empty trays on the lower speed doubling chain of the second speed doubling chain packing conveying line to an upper layer through a fifth lifting mechanism 27;
step S11, if the empty pallet needs to return to the delivery end of the third speed-multiplying chain packing conveying line 3, the main controller controls the empty return line 23 of the first empty pallet speed-multiplying chain and the lower speed-multiplying chain action of the speed-multiplying chain conveying line opposite to the fourth lifting mechanism, at the moment, the pallet on the empty pallet speed-multiplying chain shunting line 26 sequentially enters the speed-multiplying chain conveying line and the empty return line 23 of the first empty pallet speed-multiplying chain, and finally enters the fourth lifting mechanism, and the empty pallet is conveyed to the upper layer through the fourth lifting mechanism;
and step S12, if the empty tray needs to return to the delivery end of the first speed-multiplying chain packing and conveying mechanism, the main controller controls the lower speed-multiplying chain of the corresponding speed-multiplying chain conveying line in the first speed-multiplying chain packing and conveying mechanism to operate.