CN214721829U - A kind of screw support production process assembly spot welding device - Google Patents

A kind of screw support production process assembly spot welding device Download PDF

Info

Publication number
CN214721829U
CN214721829U CN202120436787.1U CN202120436787U CN214721829U CN 214721829 U CN214721829 U CN 214721829U CN 202120436787 U CN202120436787 U CN 202120436787U CN 214721829 U CN214721829 U CN 214721829U
Authority
CN
China
Prior art keywords
rectangular
spot welding
welding device
support
production process
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Expired - Fee Related
Application number
CN202120436787.1U
Other languages
Chinese (zh)
Inventor
刘环康
刘晓璐
刘晓伟
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
Handan Sande Fastener Manufacturing Co ltd
Original Assignee
Handan Yongnian Dacheng Standard Parts Manufacturing Co ltd
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by Handan Yongnian Dacheng Standard Parts Manufacturing Co ltd filed Critical Handan Yongnian Dacheng Standard Parts Manufacturing Co ltd
Priority to CN202120436787.1U priority Critical patent/CN214721829U/en
Application granted granted Critical
Publication of CN214721829U publication Critical patent/CN214721829U/en
Expired - Fee Related legal-status Critical Current
Anticipated expiration legal-status Critical

Links

Images

Landscapes

  • Butt Welding And Welding Of Specific Article (AREA)

Abstract

本实用新型公开了一种螺杆支撑生产过程组装点焊装置,包括矩形支架,矩形支架设有两个且互相平行,所述矩形支架上端设有拨动固定机构,所述矩形支架一侧设有对接固定机构。本实用新型的有益效果是,通过拨动固定机构的作用可以避免人工反复的搬动管件,降低工作强度;通过对接固定机构的作用可以提高管件与底座之间的固定精度,提高点焊效率。

Figure 202120436787

The utility model discloses a spot welding device for screw-supported production process assembly, comprising a rectangular bracket, two rectangular brackets are arranged in parallel with each other, an upper end of the rectangular bracket is provided with a toggle fixing mechanism, and one side of the rectangular bracket is provided with Docking fixing mechanism. The beneficial effect of the utility model is that the manual repeated movement of the pipe fittings can be avoided by the action of the toggle fixing mechanism, and the working strength is reduced; the fixing accuracy between the pipe fittings and the base can be improved by the action of the docking fixing mechanism, and the spot welding efficiency can be improved.

Figure 202120436787

Description

Screw rod supports production process equipment spot welding device
Technical Field
The utility model relates to a screw rod supports production technical field, and more specifically says, relates to a screw rod supports production process equipment spot welding device.
Background
The screw support is a support tool used in civil engineering construction, and the screw support mainly fixes a building template on a roof, so that a roof beam can be poured conveniently; the screw support needs to weld the base and the pipe fitting during production, corresponding workpieces need to be assembled together for spot welding before welding, and then full welding is carried out; the traditional operation mode is that workpieces are moved manually for welding, a round pipe needs to be moved frequently, and the labor force is large; after the pipe rigidity, need hold on one hand and weld on one hand and hold the base, carry out spot welding again, manually operation's precision is relatively poor, and efficiency is lower.
SUMMERY OF THE UTILITY MODEL
To above defect, the utility model provides a screw rod supports production process equipment spot welding device solves above-mentioned problem.
In order to achieve the above purpose, the utility model adopts the following technical scheme:
a screw rod supports production process equipment spot welding device, including the rectangular support, the rectangular support has two and parallel to each other, there are striking fixing mechanisms on the said rectangular support, there are butt joint fixing mechanisms on one side of the said rectangular support;
the stirring fixing mechanism comprises a first bearing at the center of the lower end of the rectangular support, a rotating shaft is arranged on the inner ring of the first bearing, stirring pieces are arranged at two ends of the rotating shaft, a trapezoidal opening is formed in one side of each stirring piece, a first belt pulley is arranged at one end of the rotating shaft, a first stepping motor is arranged at one end of the rectangular support, a second belt pulley is arranged at the rotating end of the first stepping motor, and a conveying belt is arranged between the second belt pulley and the first belt pulley; the side surface of the rectangular support is provided with a fixing plate, the upper surface of the fixing plate is provided with a supporting plate, the upper end of the supporting plate is provided with two transmission gears, the two transmission gears are hinged with the supporting plate, the upper end of each transmission gear is provided with a clamping block, the upper surface of the fixing plate is provided with a second stepping motor, and the rotating end of the second stepping motor is provided with a driving wheel meshed with the transmission gears;
the butt joint fixing mechanism comprises a v-21274arranged on one side of the rectangular support, a v-21274arranged on the upper end of the v-shaped frame, a first hydraulic cylinder is arranged at one end of the v-shaped frame, a second hydraulic cylinder is arranged at the other end of the v-shaped frame, an electromagnet is arranged at the telescopic end of the first hydraulic cylinder, a conical hopper and a v-21274are arranged at the lower end of the v-shaped frame, and a third hydraulic cylinder is arranged at the lower end of the third hydraulic cylinder and a v-21274arranged at the telescopic end of the third hydraulic cylinder.
Furthermore, a rectangular plate is arranged in the containing box.
Furthermore, a hydraulic cylinder IV is installed at one end of the rectangular support.
Furthermore, a circular pipe workpiece is installed at the upper end of the rectangular support.
The utility model has the advantages that: the pipe fitting can be prevented from being repeatedly moved manually by stirring the fixing mechanism, so that the working strength is reduced; the fixing precision between the pipe fitting and the base can be improved through the action of the butt joint fixing mechanism, and the spot welding efficiency is improved.
Drawings
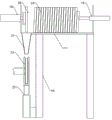
Fig. 1 is a schematic structural diagram of an assembled spot welding device in a screw support production process according to the present invention;
FIG. 2 is a schematic side view of the toggle fixing mechanism;
FIG. 3 is a partial schematic view of the docking fixture;
FIG. 4 is a side schematic view of the docking fixture;
in the figure, 1, a rectangular bracket; 2. a first bearing; 3. a rotating shaft; 4. a toggle sheet; 5. a trapezoidal opening; 6. a first belt pulley; 7. a first stepping motor; 8. a second belt pulley; 9. a conveyor belt; 10. a fixing plate; 11. a support plate; 12. a transmission gear; 13. a clamping block; 14. a second stepping motor; 15. a driving wheel; 16. contraband form rack; 17. a containing box; 18. a first hydraulic cylinder; 19. a second hydraulic cylinder; 20. an electromagnet; 21. a conical hopper; 22. a hydraulic cylinder III; 23. \ 21274and a frame; 24. a rectangular plate; 25. a fourth hydraulic cylinder; 26. a round tube workpiece.
Detailed Description
The utility model is described in detail with reference to the accompanying drawings, as shown in fig. 1-4, a screw rod supporting production process assembly spot welding device comprises a rectangular bracket 1, two rectangular brackets 1 are arranged and parallel to each other, a toggle fixing mechanism is arranged at the upper end of the rectangular bracket 1, and a butt fixing mechanism is arranged at one side of the rectangular bracket 1;
the toggle fixing mechanism comprises a first bearing 2 at the center of the lower end of the rectangular support 1, a rotating shaft 3 is arranged on the inner ring of the first bearing 2, toggle pieces 4 are arranged at two ends of the rotating shaft 3, a trapezoidal notch 5 is formed in one side of each toggle piece 4, a first belt pulley 6 is arranged at one end of the rotating shaft 3, a first stepping motor 7 is arranged at one end of the rectangular support 1, a second belt pulley 8 is arranged at the rotating end of the first stepping motor 7, and a conveying belt 9 is arranged between the second belt pulley 8 and the first belt pulley 6; the side surface of the rectangular support 1 is provided with a fixing plate 10, the upper surface of the fixing plate 10 is provided with a supporting plate 11, the upper end of the supporting plate 11 is provided with two transmission gears 12, the two transmission gears 12 are hinged with the supporting plate 11, the upper end of the transmission gear 12 is provided with a clamping block 13, the upper surface of the fixing plate 10 is provided with a second stepping motor 14, and the rotating end of the second stepping motor 14 is provided with a driving wheel 15 which is meshed with the transmission gear 12;
the butt joint fixing mechanism comprises a v-21274arranged on one side of the rectangular support 1, a containing box 17 is arranged at the upper ends of the v-shaped frames 16 and Contraband, a hydraulic cylinder I18 is arranged at one end of the containing box 17, a hydraulic cylinder II 19 is arranged at the other end of the containing box 17, an electromagnet 20 is arranged at the telescopic end of the hydraulic cylinder I18, a conical hopper 21 is arranged at the lower end of the containing box 17, a hydraulic cylinder III 22 is arranged at the lower end of the Contraband-shaped frame 16, and a v-21274and a v-shaped frame 23 are arranged at the telescopic end of the hydraulic cylinder III 22.
A rectangular plate 24 is provided in the housing box 17.
And a hydraulic cylinder IV 25 is arranged at one end of the rectangular bracket 1.
The upper end of the rectangular bracket 1 is provided with a round pipe workpiece 26.
In the embodiment, the electric equipment of the equipment is controlled by an external controller, a batch of circular pipe workpieces 26 are placed on the upper surface of the rectangular bracket 1 during spot welding, the rectangular plate 24 is manually placed in the containing box 17 and arranged, meanwhile, the hydraulic cylinder I18 and the hydraulic cylinder II 19 are in an extending state, the hydraulic cylinder II 19 and the hydraulic cylinder I18 clamp the arranged rectangular plate 24, so that the rectangular plate 24 is in a stable state, and the rectangular plate 24 is in an inclined state and is abutted against one end of the hydraulic cylinder II 19;
by utilizing the oblique cutting effect of the upper surface of the rectangular support 1, the circular tube workpiece 26 can have a rolling trend, the circular tube workpiece 26 close to one side of the poking piece 4 is in a static rotary table, when spot welding is needed, the controller controls the first stepping motor 7 to rotate, the first stepping motor 7 rotates to drive the second belt pulley 8 to rotate, the second belt pulley 8 rotates to drive the first belt pulley 6 to rotate through the conveying belt 9, the first belt pulley 6 drives the rotating shaft 3 to rotate, the two ends of the rotating shaft 3 drive the poking piece 4 to rotate for 360 degrees, the trapezoidal notch 5 rotates along with the poking piece 4, when the trapezoidal notch 5 rotates to the position of the circular tube workpiece 26, the circular tube workpiece 26 can automatically roll into the trapezoidal notch 5, then the poking piece 4 rotates for 45 degrees, the opening of the trapezoidal notch 5 faces upwards, and the circular tube workpiece 26 is at the welding position, as shown in fig. 2;
the controller controls the electromagnet 20 to be electrified, the electromagnet 20 adsorbs the rectangular plate 24, then the first hydraulic cylinder 18 contracts to drive the rectangular plate 24 to move right above the conical hopper 21, then the electromagnet 20 is powered off to release the rectangular plate 24, the rectangular plate 24 falls, the rectangular plate 24 can accurately fall into the v-21274under the action of the conical hopper 21, then the third hydraulic cylinder 22 extends, the third hydraulic cylinder 22 extends to drive the rectangular plate 24 to rise for a certain distance, then the fourth hydraulic cylinder 25 extends to enable one end of the circular pipe workpiece 26 to be abutted against the rectangular plate 24, and at the moment, spot welding is conducted.
Above-mentioned technical scheme has only embodied the utility model discloses technical scheme's preferred technical scheme, some changes that this technical field's technical personnel probably made to some parts wherein have all embodied the utility model discloses a principle belongs to within the protection scope of the utility model.

Claims (4)

1. The assembling spot welding device in the screw support production process comprises two rectangular supports (1), wherein the two rectangular supports (1) are parallel to each other, and the assembling spot welding device is characterized in that a poking and fixing mechanism is arranged at the upper end of each rectangular support (1), and a butt joint fixing mechanism is arranged on one side of each rectangular support (1);
the stirring fixing mechanism comprises a first bearing (2) arranged at the center of the lower end of a rectangular support (1), a rotating shaft (3) is arranged on the inner ring of the first bearing (2), stirring sheets (4) are arranged at two ends of the rotating shaft (3), a trapezoidal opening (5) is formed in one side of each stirring sheet (4), a first belt pulley (6) is arranged at one end of the rotating shaft (3), a first stepping motor (7) is arranged at one end of the rectangular support (1), a second belt pulley (8) is arranged at the rotating end of the first stepping motor (7), and a conveying belt (9) is arranged between the second belt pulley (8) and the first belt pulley (6); a fixing plate (10) is mounted on the side surface of the rectangular support (1), a supporting plate (11) is mounted on the upper surface of the fixing plate (10), two transmission gears (12) are mounted at the upper end of the supporting plate (11), the transmission gears (12) are hinged to the supporting plate (11), a clamping block (13) is mounted at the upper end of each transmission gear (12), a second stepping motor (14) is mounted on the upper surface of the fixing plate (10), and a driving wheel (15) meshed with the transmission gears (12) is mounted at the rotating end of the second stepping motor (14);
butt joint fixed establishment includes Contraband shape frame (16) of rectangle support (1) one side, Contraband shape frame (16) upper end is installed and is held box (17), hold box (17) one end and install pneumatic cylinder (18), hold box (17) the other end and install pneumatic cylinder two (19), electro-magnet (20) are installed to pneumatic cylinder one (18) flexible end, hold box (17) lower extreme and install toper fill (21), pneumatic cylinder three (22) are installed to Contraband shape frame (16) lower extreme, hydraulic cylinder three (22) flexible end is installed \\ 21274; "shape frame (23).
2. Screw-supported production process assembly spot welding device according to claim 1, characterized in that a rectangular plate (24) is provided in the holding box (17).
3. Screw support manufacturing process assembly spot welding device according to claim 1, characterized in that the rectangular bracket (1) is fitted with a hydraulic cylinder four (25) at one end.
4. Screw-supported production process assembly spot welding device according to claim 1, characterized in that a round pipe workpiece (26) is mounted on the upper end of the rectangular support (1).
CN202120436787.1U 2021-03-01 2021-03-01 A kind of screw support production process assembly spot welding device Expired - Fee Related CN214721829U (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN202120436787.1U CN214721829U (en) 2021-03-01 2021-03-01 A kind of screw support production process assembly spot welding device

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN202120436787.1U CN214721829U (en) 2021-03-01 2021-03-01 A kind of screw support production process assembly spot welding device

Publications (1)

Publication Number Publication Date
CN214721829U true CN214721829U (en) 2021-11-16

Family

ID=78590613

Family Applications (1)

Application Number Title Priority Date Filing Date
CN202120436787.1U Expired - Fee Related CN214721829U (en) 2021-03-01 2021-03-01 A kind of screw support production process assembly spot welding device

Country Status (1)

Country Link
CN (1) CN214721829U (en)

Cited By (1)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN117718652A (en) * 2024-02-18 2024-03-19 江苏新迅达不锈钢制品有限公司 Stainless steel screw welding device

Cited By (2)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN117718652A (en) * 2024-02-18 2024-03-19 江苏新迅达不锈钢制品有限公司 Stainless steel screw welding device
CN117718652B (en) * 2024-02-18 2024-05-24 江苏新迅达不锈钢制品有限公司 Stainless steel screw welding device

Similar Documents

Publication Publication Date Title
CN115401353A (en) Full-automatic steel pipe welding device and welding method thereof
WO2019136789A1 (en) Gantry type pipe and plat plate cutting machine
WO2021036351A1 (en) Rotary automatic welding robot and welding method thereof
CN107097033A (en) A kind of 90 ° of elbow internal wall built-up welding displacement devices
CN120715381B (en) Steel pipe cutting machine with anti-splashing scrap iron adhesion pipe orifice and cutting process
CN111015382B (en) Negative chamfering grinding machine tool
CN105127607A (en) Straight slit mechanical welding machine
CN215787726U (en) Chuck type steel pipe flange welding equipment
CN210360029U (en) Pipe Flange Welding Robot System
CN210125780U (en) An industrial automatic cutting machine
CN210024051U (en) Automatic pipeline cutting machine
CN120362873A (en) Welding platform for shifting iron tower welding piece
CN220073682U (en) An automatic welding device for automobile parts
CN112720246A (en) Grinding equipment for machining based on pneumatic control
CN211219350U (en) Turnover type operation table top for laser welding
CN202162526U (en) Wing plate and web plate centering and clamping device of H-shaped steel assembling machine
CN216912739U (en) Automobile coaxial air conditioner pipe welding fixture
CN205032864U (en) Transversal joint mechanically welded machine
CN205414826U (en) U formula gripper jaw is from feeling relieved slewer
CN219274795U (en) Double-sided synchronous seamless laser welding machine
CN208450949U (en) An intercooler welding tool
CN116586855A (en) Bearing structure of a welding robot
CN211052946U (en) Circular cutting device
CN215280566U (en) Automatic welding machine suitable for valve body
CN115837532A (en) Metal collapsible tube automatic weld is rotatory frock

Legal Events

Date Code Title Description
GR01 Patent grant
GR01 Patent grant
TR01 Transfer of patent right

Effective date of registration: 20231016

Address after: 057150 West of Xiduanzhuang Village, Linmingguan Town, Yongnian District, Handan City, Hebei Province

Patentee after: Handan Sande Fastener Manufacturing Co.,Ltd.

Address before: 057150 yongnianzhuang Industrial Zone, Handan City, Hebei Province

Patentee before: Handan Yongnian Dacheng standard parts manufacturing Co.,Ltd.

CU01 Correction of utility model

Correction item: Patentee|Address

Correct: Handan Yongnian Dacheng standard parts manufacturing Co.,Ltd.|057150 yongnianzhuang Industrial Zone, Handan City, Hebei Province

False: Handan Sande Fastener Manufacturing Co.,Ltd.|057150 West of Xiduanzhuang Village, Linmingguan Town, Yongnian District, Handan City, Hebei Province

Number: 44-01

Volume: 39

TR01 Transfer of patent right

Effective date of registration: 20231103

Address after: 057150 West of Xiduanzhuang Village, Linmingguan Town, Yongnian District, Handan City, Hebei Province

Patentee after: Handan Sande Fastener Manufacturing Co.,Ltd.

Address before: 057150 yongnianzhuang Industrial Zone, Handan City, Hebei Province

Patentee before: Handan Yongnian Dacheng standard parts manufacturing Co.,Ltd.

CF01 Termination of patent right due to non-payment of annual fee

Granted publication date: 20211116