SUMMERY OF THE UTILITY MODEL
An object of the utility model is to provide a car seat power angle modulation ware external tooth fine blanking die to solve the problem that proposes in the above-mentioned background art.
In order to achieve the above object, the utility model provides a following technical scheme: fine blanking die for outer teeth of electric angle adjuster of automobile seat comprises a base and a connecting seat, wherein two fixed blocks and two fixed blocks are symmetrically welded on the upper surface of the base, a third plate body is slidably connected to the inner side wall of the fixed blocks, a hydraulic cylinder is installed on the inner side wall of the base, a piston rod of the hydraulic cylinder is welded on the bottom of the third plate body, a first shell is welded on the top of the third plate body, a first rod body is connected to the upper surface of the first shell in a threaded manner, a first stamping plate is slidably connected to the outer side wall of the first rod body, a second rod body is connected to the upper surface of the first shell in an equidistant and threaded manner, a second shell is welded on the lower surface of the connecting seat, a third cylinder is installed on the inner side wall of the second shell, a first plate body is welded on the lower surface of the second shell, a second cylinder is installed on the inner side wall of the second shell, and a piston rod of the third cylinder is all penetrated through the inner side wall of the first plate body and is welded on the upper surface of the second shell The mould, first cylinder is installed to the inside wall of going up the mould.
As further preferable in the present technical solution: the outer side wall of the second rod body is connected with the inner side wall of the first die plate in a sliding mode, three second through holes are formed in the upper surface of the first die plate, the first through holes are formed in the upper surface of the first die plate, the inner side wall of the first die plate is connected with first stamping blocks in a sliding mode, and the inner side wall of the first die plate is connected with second stamping blocks in a sliding mode.
As further preferable in the present technical solution: the outer side wall of the first rod body is connected with a second die plate in a sliding mode, the outer side wall of the second rod body is connected with the inner side wall of the second die plate in a sliding mode, a die groove is formed in the inner side wall of the second die plate, and a third through hole is formed in the inner side wall of the second die plate.
As further preferable in the present technical solution: the outer side wall of the first rod body is connected with a third die plate in a sliding mode, the outer side wall of the second rod body is connected with the inner side wall of the third die plate in a sliding mode, a fourth through hole is formed in the inner side wall of the third die plate, and a fifth through hole is formed in the inner side wall of the third die plate.
As further preferable in the present technical solution: a fourth cylinder is installed on the inner side wall of the upper die, and a second plate body is welded to a piston rod of the fourth cylinder.
As further preferable in the present technical solution: the welding of the inside wall of second casing has the third body of rod, the lateral wall of the third body of rod with go up the inside wall sliding connection of mould.
Compared with the prior art, the beneficial effects of the utility model are that: the utility model discloses a set up first die plate, first die plate and first die plate, and correspond the position of the first body of rod of position adjustment and the second body of rod of through-hole on the different die plates, place the die plate after on first casing, make this device carry out the punching press to panel according to the shape of first punching press piece and second punching press piece, it is not convenient for change the die to have solved under the prerequisite of guaranteeing the essence towards, the part size of production is comparatively fixed, it is single, be unsuitable for the problem of diversified automobile parts production, thereby the efficiency that makes production improves.
Detailed Description
The technical solutions in the embodiments of the present invention will be described clearly and completely with reference to the accompanying drawings in the embodiments of the present invention, and it is obvious that the described embodiments are only some embodiments of the present invention, not all embodiments. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
Example one
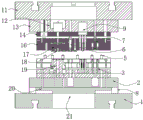
Referring to fig. 1-2, the present invention provides a technical solution: the external tooth fine blanking die for the electric angle adjuster of the automobile seat comprises a base 1 and a connecting seat 11, a hydraulic cylinder 21 is installed on the inner side wall of the base 1, two fixing blocks 8 are symmetrically welded on the upper surface of the base 1, the inner side walls of the two fixing blocks 8 are slidably connected with a third plate body 20, the hydraulic cylinder 21 is installed on the inner side wall of the base 1, a piston rod of the hydraulic cylinder 21 is welded at the bottom of the third plate body 20, a first shell 2 is welded on the top of the third plate body 20, a first rod body 3 is in threaded connection with the upper surface of the first shell 2, a first blanking plate 19 is in sliding connection with the outer side wall of the first rod body 3, a second rod body 5 is in uniform threaded connection with the upper surface of the first shell 2 at equal intervals, a second shell 13 is welded on the lower surface of the connecting seat 11, a third cylinder 12 is installed on the inner side wall of, piston rods of the second cylinder 9 and the third cylinder 12 penetrate through the inner side wall of the first plate 14 and are welded with an upper die 16, and the first cylinder 7 is mounted on the inner side wall of the upper die 16.
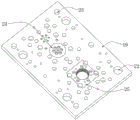
In this embodiment, specifically: the outer side wall of the first rod body 3 is connected with a first die plate 19 in a sliding mode, the outer side wall of the second rod body 5 is connected with the inner side wall of the first die plate 19 in a sliding mode, three second through holes 23 are formed in the upper surface of the first die plate 19, a first through hole 22 is formed in the upper surface of the first die plate 19, the inner side wall of the first die plate 19 is connected with a first stamping block 24 in a sliding mode, and the inner side wall of the first die plate 19 is connected with a second stamping block 25 in a sliding mode; after the first die plate 19 is placed on the first housing 2 by adjusting the positions of the first rod 3 and the second rod 5 corresponding to the positions of the first through hole 22 and the second through hole 23, the present apparatus punches the plate material according to the shapes of the first punch block 24 and the second punch block 25.
In this embodiment, specifically: a fourth cylinder 17 is mounted on the inner side wall of the upper die 16, and a piston rod of the fourth cylinder 17 is welded with a second plate 18; the piston rod of the fourth cylinder 17 pushes the second plate 18, and the second plate 18 presses the first die plate 19 and the plate downwards.
In this embodiment, specifically: a third rod body 6 is welded on the inner side wall of the second shell 13, and the outer side wall of the third rod body 6 is connected with the inner side wall of the upper die 16 in a sliding manner; the third rod 6 acts as a centering element for the first plate 14 and the upper die 16, so that the upper die 16 slides in the direction of the third rod 6.
Example two
Referring to fig. 1-3, the present invention provides a technical solution: the external tooth fine blanking die for the electric angle adjuster of the automobile seat comprises a base 1 and a connecting seat 11, a hydraulic cylinder 21 is installed on the inner side wall of the base 1, two fixing blocks 8 are symmetrically welded on the upper surface of the base 1, the inner side walls of the two fixing blocks 8 are slidably connected with a third plate body 20, the hydraulic cylinder 21 is installed on the inner side wall of the base 1, a piston rod of the hydraulic cylinder 21 is welded at the bottom of the third plate body 20, a first shell 2 is welded on the top of the third plate body 20, a first rod body 3 is in threaded connection with the upper surface of the first shell 2, a first blanking plate 19 is in sliding connection with the outer side wall of the first rod body 3, a second rod body 5 is in uniform threaded connection with the upper surface of the first shell 2 at equal intervals, a second shell 13 is welded on the lower surface of the connecting seat 11, a third cylinder 12 is installed on the inner side wall of the second shell 13, a first plate body 14 is welded on the lower surface of the second shell 13, a second cylinder 9 is installed on the inner side wall of the second shell 13, piston rods of the second cylinder 9 and the third cylinder 12 penetrate through the inner side wall of the first plate 14 and are welded with an upper die 16, and the first cylinder 7 is mounted on the inner side wall of the upper die 16.
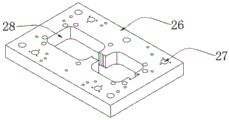
In this embodiment, specifically: the outer side wall of the first rod body 3 is connected with a second die plate 26 in a sliding mode, the outer side wall of the second rod body 5 is connected with the inner side wall of the second die plate 26 in a sliding mode, a die groove 28 is formed in the inner side wall of the second die plate 26, and a third through hole 27 is formed in the inner side wall of the second die plate 26; after the second die plate 26 is placed on the first housing 2 by adjusting the position of the second rod 5 corresponding to the position of the third through hole 27, the present apparatus presses the plate material according to the shape of the die cavity 28.
In this embodiment, specifically: a fourth cylinder 17 is mounted on the inner side wall of the upper die 16, and a piston rod of the fourth cylinder 17 is welded with a second plate 18; the piston rod of the fourth cylinder 17 pushes the second plate 18, and the second plate 18 presses the first die plate 19 and the plate downwards.
In this embodiment, specifically: a third rod body 6 is welded on the inner side wall of the second shell 13, and the outer side wall of the third rod body 6 is connected with the inner side wall of the upper die 16 in a sliding manner; the third rod 6 acts as a centering element for the first plate 14 and the upper die 16, so that the upper die 16 slides in the direction of the third rod 6.
EXAMPLE III
Referring to fig. 1-4, the present invention provides a technical solution: the external tooth fine blanking die for the electric angle adjuster of the automobile seat comprises a base 1 and a connecting seat 11, a hydraulic cylinder 21 is installed on the inner side wall of the base 1, two fixing blocks 8 are symmetrically welded on the upper surface of the base 1, the inner side walls of the two fixing blocks 8 are slidably connected with a third plate body 20, the hydraulic cylinder 21 is installed on the inner side wall of the base 1, a piston rod of the hydraulic cylinder 21 is welded at the bottom of the third plate body 20, a first shell 2 is welded on the top of the third plate body 20, a first rod body 3 is in threaded connection with the upper surface of the first shell 2, a first blanking plate 19 is in sliding connection with the outer side wall of the first rod body 3, a second rod body 5 is in uniform threaded connection with the upper surface of the first shell 2 at equal intervals, a second shell 13 is welded on the lower surface of the connecting seat 11, a third cylinder 12 is installed on the inner side wall of the second shell 13, a first plate body 14 is welded on the lower surface of the second shell 13, a second cylinder 9 is installed on the inner side wall of the second shell 13, piston rods of the second cylinder 9 and the third cylinder 12 penetrate through the inner side wall of the first plate 14 and are welded with an upper die 16, and the first cylinder 7 is mounted on the inner side wall of the upper die 16.
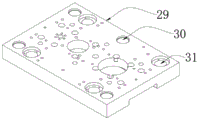
In this embodiment, specifically: the outer side wall of the first rod body 3 is connected with a third die plate 29 in a sliding mode, the outer side wall of the second rod body 5 is connected with the inner side wall of the third die plate 29 in a sliding mode, a fourth through hole 30 is formed in the inner side wall of the third die plate 29, and a fifth through hole 31 is formed in the inner side wall of the third die plate 29; after the third die plate 29 is placed on the first housing 2 by adjusting the positions of the first rod 3 and the second rod 5 corresponding to the positions of the fourth through hole 30 and the fifth through hole 31, the present apparatus punches a plate material according to the shape of the third die plate 29.
In this embodiment, specifically: a fourth cylinder 17 is mounted on the inner side wall of the upper die 16, and a piston rod of the fourth cylinder 17 is welded with a second plate 18; the piston rod of the fourth cylinder 17 pushes the second plate 18, and the second plate 18 presses the first die plate 19 and the plate downwards.
In this embodiment, specifically: a third rod body 6 is welded on the inner side wall of the second shell 13, and the outer side wall of the third rod body 6 is connected with the inner side wall of the upper die 16 in a sliding manner; the third rod 6 acts as a centering element for the first plate 14 and the upper die 16, so that the upper die 16 slides in the direction of the third rod 6.
When the device is used, the first cylinder 7, the second cylinder 9, the third cylinder 12 and the fourth cylinder 17 are connected to an external compressed air source and used for controlling the opening and closing of the first cylinder 7, the second cylinder 9, the third cylinder 12 and the fourth cylinder 17 and providing compressed air as a power source, the hydraulic cylinder 21 is connected to an external switch, the hydraulic cylinder 21 is started to raise the position of the third plate body 20, then the second cylinder 9 and the third cylinder 12 are started to push the upper die 16 downwards, the upper die 16 is covered on a plate, the positions of the first rod body 3 and the second rod body 5 are adjusted by the positions corresponding to the first through hole 22 and the second through hole 23, the first die plate 19 is placed on the first shell 2, the device is enabled to punch the plate according to the shapes of the first punch block 24 and the second punch block 25, and the position of the second rod body 5 can be adjusted by the position corresponding to the third through hole 27, after the second die plate 26 is placed on the first shell 2, the device can stamp a plate according to the shape of the die cavity 28, the positions of the first rod body 3 and the second rod body 5 can be adjusted by the positions corresponding to the fourth through hole 30 and the fifth through hole 31, after the third die plate 29 is placed on the first shell 2, the device can stamp a plate according to the shape of the third die plate 29, the piston rod of the fourth cylinder 17 pushes the second plate body 18, the second plate body 18 stamps the first die plate 19 and the plate downwards, the third rod body 6 has a function of centering the first plate body 14 and the upper die 16, and the upper die 16 slides along the direction of the third rod body 6.
Although embodiments of the present invention have been shown and described, it will be appreciated by those skilled in the art that changes, modifications, substitutions and alterations can be made in these embodiments without departing from the principles and spirit of the invention, the scope of which is defined in the appended claims and their equivalents.