CN213256985U - Mould for hub casting - Google Patents
Mould for hub casting Download PDFInfo
- Publication number
- CN213256985U CN213256985U CN202021312309.1U CN202021312309U CN213256985U CN 213256985 U CN213256985 U CN 213256985U CN 202021312309 U CN202021312309 U CN 202021312309U CN 213256985 U CN213256985 U CN 213256985U
- Authority
- CN
- China
- Prior art keywords
- mould
- hole
- connecting rod
- bottom plate
- spreader cone
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000005266 casting Methods 0.000 title claims abstract description 13
- 238000001816 cooling Methods 0.000 claims description 8
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 4
- 230000001174 ascending effect Effects 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 230000007246 mechanism Effects 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
Images



Landscapes
- Molds, Cores, And Manufacturing Methods Thereof (AREA)
Abstract
The utility model discloses a wheel hub casts mould for casting of technical field, including last mould, side forms and the lower mould that is used for constituting the die cavity, the top parallel of going up the mould is equipped with bottom plate and last fly leaf, the middle part of going up the mould is equipped with through-hole and reposition of redundant personnel awl, form the air guide clearance between reposition of redundant personnel awl and the through-hole, be equipped with the second ejector pin between reposition of redundant personnel awl and the bottom plate, go up and be equipped with first connecting rod between fly leaf and the last mould, the middle part of first connecting rod sets up in the guiding hole on the bottom plate. The utility model discloses middle part at last mould is equipped with through-hole and spreader cone, and forms between spreader cone and the through-hole and be used for intracavity air escape's exhaust clearance, and through second ejector pin fixed connection again between spreader cone and the bottom plate simultaneously, the spreader cone can provide decurrent effort to the product middle part when the drawing of patterns for the product atress is even, and the drawing of patterns operation of not only being convenient for has also guaranteed higher product quality.
Description
Technical Field
The utility model relates to a wheel hub casts technical field, concretely relates to mould for wheel hub casting.
Background
The hub mold is a special mold with a fixed structure, and comprises an upper mold, a bottom mold and a side mold which are used for forming a hub cavity. As shown in fig. 4, when the existing hub casting mold is demolded, the edge position of the product is supported by the first ejector rod connected with the upper mold in a sliding manner, and then the upper mold is driven to ascend through the first connecting rod to complete the demolding operation, because the stress position of the product is at the edge position and the edge position of the product is thinner, the edge of the product is deformed during demolding, so that the quality of the product is reduced; meanwhile, when the mold is formed, the middle part of the cavity is higher than the edge position, so that the problem that air in the middle part of the cavity is not easy to exhaust is easily caused, and an exhaust hole is required to be arranged on the upper mold independently.
SUMMERY OF THE UTILITY MODEL
In view of the above, the present invention is directed to a mold for casting a hub.
The utility model discloses the technical scheme who adopts does:
the utility model provides a mould is used in wheel hub casting, is including last mould, side forms and the lower mould that is used for constituting the die cavity the top parallel of going up the mould is equipped with bottom plate and last fly leaf, the middle part of going up the mould is equipped with the through-hole, be equipped with the reposition of redundant personnel awl in the through-hole, just form the air guide clearance between reposition of redundant personnel awl and the through-hole, be equipped with the second ejector pin between reposition of redundant personnel awl and the bottom plate, go up and be equipped with first connecting rod between fly leaf and the last mould, the middle part of first connecting rod sets up in the.
Preferably, the upper die is provided with an air guide hole communicated with the top of the cavity, the lower fixing plate is connected with the top end of the first ejector rod, and the bottom end of the first ejector rod extends downwards into the air guide hole.
Preferably, an annular cooling channel is arranged in the upper die, a second connecting rod is arranged between the upper die and the upper movable plate, the second connecting rod is hollow, the bottom end of the second connecting rod is communicated with the cooling channel, and the top end of the second connecting rod penetrates through the lower fixing plate upwards and then is fixedly connected with the upper movable plate.
Preferably, the through hole is in a circular truncated cone shape.
Preferably, the bottom end of the first connecting rod is rotatably connected with the spreader cone through a bearing.
Compared with the prior art, the utility model has the advantages that:
the utility model discloses be equipped with the through-hole and the spreader cone of round platform form at the middle part of last mould, and form the exhaust clearance between spreader cone and the through-hole, the exhaust clearance is used for the discharge of intracavity air of type, and simultaneously between spreader cone and the bottom plate again through second ejector pin fixed connection, during the drawing of patterns, the spreader cone can provide a decurrent effort to the product middle part for the product atress is even, and the drawing of patterns operation of not only being convenient for has also guaranteed higher product quality.
Drawings
Fig. 1 is a schematic structural view of the present invention;
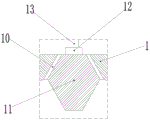
FIG. 2 is a partial enlarged view B of FIG. 1;
FIG. 3 is a partial enlarged view A of FIG. 1;
FIG. 4 is a schematic diagram of a prior art configuration;
the device comprises an upper die 1, a side die 2, a lower die 3, a cavity 4, a lower fixing plate 5, an upper movable plate 6, a first connecting rod 7, an air guide hole 8, a first ejector rod 9, a through hole 10, a spreader 11, a bearing 12, a second ejector rod 13, a cooling channel 14, a second connecting rod 15, a water inlet pipe 16, a water outlet pipe 17 and a lifting hydraulic cylinder 18.
Detailed Description
The following embodiments are only intended to illustrate the present invention in detail, and do not limit the scope of the present invention in any way. The unit module components, structures, mechanisms, sensors and other devices referred to in the following examples are all conventional and commercially available products unless otherwise specified.
Example (b): as shown in fig. 1-4, a mold for casting a wheel hub comprises an upper mold 1, a side mold 2 and a lower mold 3 for forming a cavity 4, a lower fixed plate 5 and an upper movable plate 6 are arranged above the upper mold 1 in parallel, the upper movable plate 6 is arranged above the lower fixed plate 5, a lifting hydraulic cylinder 18 for driving the upper movable plate 6 to move up and down in a reciprocating manner is arranged between the upper movable plate 6 and the lower fixed plate 5, a first connecting rod 7 is arranged between the upper movable plate 6 and the upper mold 1, the middle part of the first connecting rod 7 is arranged in a guide hole (not shown) on the lower fixed plate 5, an air guide hole 8 communicated with the top of the cavity 4 is arranged on the upper mold 1, the lower fixed plate 5 is connected with the top end of a first ejector rod 9, and the bottom end of the first ejector rod 9 extends; the middle of the upper die 1 is provided with a circular truncated cone-shaped through hole 10, a shunt cone 11 is arranged in the through hole 10, an annular air guide gap is formed between the shunt cone 11 and the through hole 10, the thickness of the air guide gap is 0.1-0.15 mm, the top end of the shunt cone 11 is rotatably connected with the bottom end of a second ejector rod 13 through a bearing 12, and the top end of the second ejector rod 13 is fixedly connected with the lower fixing plate 5.
In this embodiment, in order to facilitate the ascending and cooling of the upper mold 1, an annular cooling channel 14 is disposed in the upper mold 1, a second connecting rod 15 is disposed between the upper mold 1 and the upper movable plate 6, the second connecting rod 15 is hollow, a bottom end of the second connecting rod 15 is communicated with the cooling channel 14, a top end of the second connecting rod 15 penetrates the lower fixed plate 5 upwards and then is fixedly connected with the upper movable plate 6, and the two second connecting rods 15 are respectively connected with a water inlet pipe 16 and a water outlet pipe 17.
During molding, air in the middle of the cavity 4 is discharged from an air guide gap between the shunting cone 11 and the through hole 10, and air outside the cavity 4 is discharged from a gap between the air guide hole 8 and the first ejector rod 9; during demoulding, the first ejector rod 9 provides downward action for the edge position of a product, and the shunt cone 11 provides downward action force for the middle part of the product under the action of the second ejector rod 15, so that the product is uniformly stressed and separated from the upper die 1, and the product quality is effectively guaranteed.
Finally, the above embodiments are only used for illustrating the technical solutions of the present invention and not for limiting, and other modifications or equivalent replacements made by the technical solutions of the present invention by those of ordinary skill in the art should be covered within the scope of the claims of the present invention as long as they do not depart from the spirit and scope of the technical solutions of the present invention.
Claims (5)
1. The utility model provides a mould is used in wheel hub casting, is including last mould, side forms and the lower mould that is used for constituting the die cavity the top parallel of going up the mould is equipped with bottom plate and last fly leaf, its characterized in that: the middle part of going up the mould is equipped with the through-hole, be equipped with the spreader cone in the through-hole, just form the air guide clearance between spreader cone and the through-hole, be equipped with the second ejector pin between spreader cone and the bottom plate, it is equipped with first connecting rod to go up between fly leaf and the mould, the middle part of first connecting rod sets up in the guiding hole on the bottom plate.
2. The mold for hub casting according to claim 1, wherein: the upper die is provided with an air guide hole communicated with the top of the cavity, the lower fixing plate is connected with the top end of the first ejector rod, and the bottom end of the first ejector rod extends downwards into the air guide hole.
3. The mold for hub casting according to claim 1, wherein: the upper die is internally provided with an annular cooling channel, a second connecting rod is arranged between the upper die and the upper movable plate, the second connecting rod is hollow, the bottom end of the second connecting rod is communicated with the cooling channel, and the top end of the second connecting rod upwards penetrates through the lower fixing plate and then is fixedly connected with the upper movable plate.
4. The mold for hub casting according to claim 1, wherein: the through hole is in a round table shape.
5. The mold for hub casting according to claim 1, wherein: the bottom end of the first connecting rod is rotatably connected with the spreader cone through a bearing.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202021312309.1U CN213256985U (en) | 2020-07-07 | 2020-07-07 | Mould for hub casting |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202021312309.1U CN213256985U (en) | 2020-07-07 | 2020-07-07 | Mould for hub casting |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN213256985U true CN213256985U (en) | 2021-05-25 |
Family
ID=75958392
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202021312309.1U Expired - Fee Related CN213256985U (en) | 2020-07-07 | 2020-07-07 | Mould for hub casting |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN213256985U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113477911A (en) * | 2021-06-29 | 2021-10-08 | 江苏苏美达铝业有限公司 | High-efficient automatic gravity casting wheel hub apparatus for producing |
-
2020
- 2020-07-07 CN CN202021312309.1U patent/CN213256985U/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113477911A (en) * | 2021-06-29 | 2021-10-08 | 江苏苏美达铝业有限公司 | High-efficient automatic gravity casting wheel hub apparatus for producing |
| CN113477911B (en) * | 2021-06-29 | 2023-02-21 | 江苏苏美达铝业有限公司 | High-efficient automatic gravity casting wheel hub apparatus for producing |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN208682035U (en) | A kind of Double-ejection injection mold | |
| CN109530616A (en) | A kind of internal core-pulling mechanism and cold box die | |
| CN109435180A (en) | A kind of hollow grid product one-pass molding automatic stripping die | |
| CN219378946U (en) | Mold ejection structure for preventing mold from being blocked | |
| CN202752549U (en) | Cooler core box core shooting machine | |
| CN215360092U (en) | Automatic ejection of compact's mechanical die | |
| CN109746340A (en) | A kind of 3 balanced type stamping die liftout attachments | |
| CN210651545U (en) | Plastic cover plate forming equipment for center console | |
| CN209320211U (en) | A kind of hollow grid product one-pass molding automatic stripping die | |
| CN218891119U (en) | Stamping die with bearing structure | |
| CN205289715U (en) | Wheel hub dead -weight loading casts mould | |
| CN207825386U (en) | A kind of mould structure with ejecting mechanism | |
| CN220127385U (en) | Production mould of impeller front disc | |
| CN211683309U (en) | Jacking type die | |
| CN208410714U (en) | A mold release structure for a thermoforming mold | |
| CN211566351U (en) | Demoulding assembly line of brick machine | |
| CN2882846Y (en) | Mould changing gear of combined mould | |
| CN208357778U (en) | A kind of three template die secondary ejection devices | |
| CN221584205U (en) | Composite material plate forming die structure | |
| CN208322039U (en) | Structure of cast die | |
| CN215434855U (en) | Portable ejector pin mechanism that resets | |
| CN216828510U (en) | Pneumatic demoulding structure of turbine precision casting mould | |
| CN224044357U (en) | Precise electronic processing die convenient for demolding | |
| CN220534697U (en) | Guide sleeve blank making die ejection device | |
| CN222473108U (en) | Integrated frame forming die with ejection mechanism |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20210525 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |