Automatic rubber coating device of transformer
Technical Field
The utility model relates to a machine-building field, specific automatic rubber coating device of transformer that says so.
Background
For the operation, the operation mode of enterprises at present mainly adopts two modes of manual rubber coating and mechanical rubber coating, wherein the manual rubber coating is to wind a rubber belt manually, so that a large amount of manpower resources are wasted and the production efficiency is low; the mechanical rubber coating is carried out on a rubber coating platform, the main structure of the mechanical rubber coating is a turntable controlled to rotate by a motor, two magnetic core frames are mounted on the turntable and controlled to rotate by an independent motor, in addition, a cutter and a rubber tape roll for cutting off the rubber tape are arranged on the rubber coating platform, the action process of the mechanical rubber coating is that firstly, a magnetic core is placed on one magnetic core frame, the rubber tape is adhered to the magnetic core, then the motor controls the magnetic core frame to rotate, the rubber coating of the magnetic core is started, after the rubber coating is finished, a new magnetic core is manually placed on the other magnetic core frame, at the moment, the turntable rotates for a half circle, after the rubber tape is adhered to the new magnetic core, the cutter cuts off the rubber tape, then, the magnetic core which is subjected to rubber. At present, the magnetic core still needs to be manually replaced by mechanical rubber coating, and because the action processes of a motor for controlling the rotation of the magnetic core frame and a motor for controlling the rotation of the turntable are preset, a worker needs to follow the motor and the motor for operation, so that the fatigue of the operator is easily caused, safety accidents are generated, and the improvement is needed.
Disclosure of Invention
The utility model aims at the above-mentioned problem provide an automatic rubber coating, alleviate artifical burden, the automatic rubber coating device of transformer of using manpower sparingly.
In order to achieve the above object, the utility model relates to an automatic rubber coating device of transformer, its structural feature is: the automatic lifting device comprises a workbench, the rotary table is installed in the rotary table in a rotating mode, two magnetic core frames used for placing magnetic cores are fixedly installed on the upper side of the rotary table, the two magnetic core frames are spaced from each other on the left and right sides, a stepping motor used for driving the rotary table to rotate is installed on the rotary table, a first conveying belt is further installed on the rotary table, the first conveying belt is located on the right side of the rotary table, a lifting frame capable of ascending and descending is arranged above the rotary table, a lifting cylinder used for driving the lifting frame to ascend and descend is installed on the rotary table, a sliding rail extending from left to right is fixedly installed on the lifting frame, a first sliding block is installed on the sliding rail in a sliding mode, a sliding table is installed on the first sliding block, a first clamp and a second clamp which are used for clamping the magnetic cores are fixedly installed on the lower side of the sliding.
After adopting above-mentioned structure, the installation conveyer belt passes through conveyer belt conveying magnetic core on the workstation, the working process utilizes anchor clamps two to place the magnetic core on the conveyer belt and carries out the rubber coating area on the magnetic core frame, the rubber coating is accomplished the back, take off the magnetic core on the magnetic core frame through anchor clamps one, and place next station, this device mechanical action is accurate, can be accurate place the rubber coating station with the magnetic core on, accomplish the rubber coating operation back when the magnetic core, again can be accurate take off the magnetic core and place follow-up station, need not artifical the participation in carrying out transformer rubber coating process, alleviate manual operation burden.
Regarding the concrete structure of anchor clamps one and anchor clamps two, the slide of extending around having seted up on the slip table, anchor clamps one includes slider two of slidable mounting in the slide, slider two is equipped with two and interval around both, slider two stretches out from the slip table downside, the downside of slider two has set firmly splint, the screw hole that runs through around all seting up on two sliders, two screw holes revolve to opposite, install the anchor clamps motor on the slip table, the lead screw is installed to the output shaft of anchor clamps motor, be equipped with two sets of screw threads that revolve to opposite on the lead screw, two sets of screw threads extend to both sides from lead screw central authorities, the lead screw spiral shell dress is in two screwed holes, anchor clamps two are the same with anchor clamps. After adopting above-mentioned structure, when anchor clamps one centre gripping magnetic core, drive the lead screw by the motor earlier and rotate, two splint draw close to the centre, carry out the centre gripping to the magnetic core, after the magnetic core removed predetermined station, the motor drove lead screw antiport, and two splint remove to the direction of bearing back, and the magnetic core breaks away from the centre gripping of anchor clamps one this moment.
In order to guarantee that the second clamp can accurately clamp the magnetic core, the front side and the rear side of the first conveyor belt are respectively provided with a material blocking block, the material blocking blocks extend along the length direction of the first conveyor belt, the upper edges of the material blocking blocks are higher than the height of the first conveyor belt, the front-rear intervals of the two material blocking blocks correspond to the width of the magnetic core, a limiting frame is installed at the left end of the first conveyor belt, and the height of the limiting frame is not higher than the height of the magnetic core. The relative position of magnetic core on conveyer belt one is guaranteed to the material blocking piece, is intercepted by spacing behind the magnetic core is conveyed the conveyer belt left end, makes the magnetic core get into the centre gripping station, waits for by two centre grippings of anchor clamps.
In order to further realize the automation of the device, a second conveying belt is further installed on the workbench and is positioned on the left side of the turntable, and the distance between the second conveying belt and the magnetic core frame is not larger than the distance between the first clamp and the second clamp. After the magnetic core finishes the rubber coating work, the second clamp clamps the magnetic core, and the magnetic core is taken down from the magnetic core frame and placed on the second conveyor belt.
In order to ensure the stability of the lifting frame in up-down lifting, a plurality of vertical rods extending up and down are installed on the workbench, a sliding sleeve corresponding to the vertical rods is fixedly installed on the lifting frame, a top spring is sleeved on each vertical rod, the lower end of each top spring abuts against the upper side of the workbench, and the upper end of each top spring abuts against the lower side of the sliding sleeve.
Regarding the mounting structure of the adhesive tape roll, a reel is vertically mounted on the workbench, and the adhesive tape roll is rotatably mounted on the reel. And a cutter cylinder is fixedly arranged on the workbench, the cutter cylinder is positioned on the front side of the turntable, a cutter is fixedly arranged at the top end of the cutter cylinder, and the top end of the cutter faces between the two magnetic core frames. After the magnetic core is encapsulated, the cutter cylinder pushes the cutter to cut off the adhesive tape.
Because above-mentioned technical scheme's application is following right the utility model discloses an advantage effect carries out concrete analysis.
To sum up the utility model discloses the installation conveyer belt passes through conveyer belt conveying magnetic core on the workstation, and the work process utilizes two magnetic cores of anchor clamps to place the magnetic core on the conveyer belt and carries out the rubber coating area on the magnetic core frame, and the rubber coating is accomplished the back, takes off the magnetic core on the magnetic core frame through anchor clamps one to place next station, this device mechanical action is accurate, can be accurate place the rubber coating station with the magnetic core on, accomplish the rubber coating operation back when the magnetic core, again can be accurate take off the magnetic core and place follow-up station, need not artifical the participation in carrying out transformer rubber coating process, alleviate manual operation burden.
Drawings
The following detailed description of the embodiments of the present invention is provided with reference to the accompanying drawings:
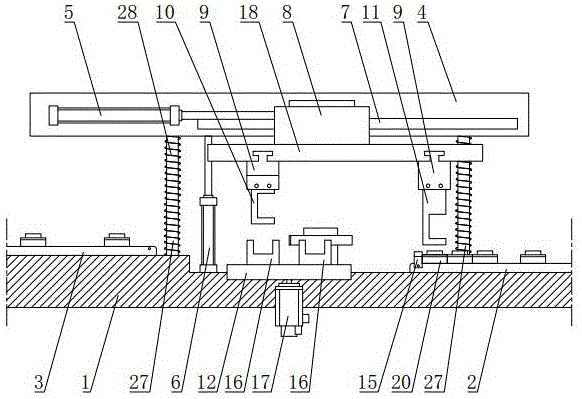
fig. 1 is a schematic structural view of the present invention;
FIG. 2 is a schematic top view of the worktable;
fig. 3 is a schematic structural diagram of the first clamp.
In the figure: the device comprises a workbench 1, a first conveyor belt 2, a second conveyor belt 3, a lifting frame 4, a sliding cylinder 5, a lifting cylinder 6, a sliding rail 7, a first slider 8, a second slider 9, a first clamp 10, a second clamp 11, a rotary table 12, a cutter cylinder 13, a cutter 14, a limiting frame 15, a magnetic core frame 16, a stepping motor 17, a sliding table 18, an adhesive tape roll 19, a magnetic core 20, a clamping plate 21, a clamp motor 22, a screw rod 23, a slide rail 24, a threaded hole 25, a material blocking block 26, an upright rod 27, a top spring 28 and a reel 29.
Detailed Description
The technical solutions of the present invention will be described clearly and completely with reference to the accompanying drawings, and it should be understood that the described embodiments are some, but not all embodiments of the present invention.
The components of embodiments of the present invention generally described and illustrated in the figures herein may be arranged and designed in a wide variety of different configurations. Thus, the following detailed description of the embodiments of the present invention, presented in the figures, is not intended to limit the scope of the invention, as claimed, but is merely representative of selected embodiments of the invention.
All other embodiments, which can be derived by a person skilled in the art from the embodiments given herein without making any creative effort, shall fall within the protection scope of the present invention.
In the description of the present invention, it should be noted that the terms "center", "upper", "lower", "left", "right", "vertical", "horizontal", "inner", "outer", etc., indicate orientations or positional relationships based on the orientations or positional relationships shown in the drawings, and are only for convenience of description and simplicity of description, but do not indicate or imply that the device or element being referred to must have a particular orientation, be constructed and operated in a particular orientation, and thus, should not be construed as limiting the present invention. Furthermore, the terms "first," "second," and "third" are used for descriptive purposes only and are not to be construed as indicating or implying relative importance.
In the description of the present invention, it should be noted that, unless otherwise explicitly specified or limited, the terms "mounted," "connected," and "connected" are to be construed broadly, e.g., as meaning either a fixed connection, a removable connection, or an integral connection; can be mechanically or electrically connected; they may be connected directly or indirectly through intervening media, or they may be interconnected between two elements. The specific meanings of the above terms in the present invention can be understood in specific cases to those skilled in the art.
Referring to the drawings, the utility model discloses an automatic rubber coating device of transformer: the magnetic core lifting device comprises a workbench 1, a turntable 12 is rotatably mounted on the workbench 1, two magnetic core frames 16 for placing a magnetic core 20 are fixedly mounted on the upper side of the turntable 12, the two magnetic core frames 16 are mutually spaced from left to right, a stepping motor 17 for driving the turntable 12 to rotate is mounted on the workbench 1, a first conveyor belt 2 is further mounted on the workbench 1, the first conveyor belt 2 is positioned on the right side of the turntable 12, a lifting frame 4 capable of lifting up and down is arranged above the workbench 1, a lifting cylinder 6 for driving the lifting frame 4 to lift up and down is mounted on the workbench 1, a slide rail 7 extending left and right is fixedly mounted on the lifting frame 4, a first slide block 8 is slidably mounted on the slide rail 7, a sliding cylinder 5 capable of driving the first slide block 8 to slide left and right is mounted on the lifting frame 4, a sliding table 18 is fixedly mounted on the first slide block 8, and a first clamp 10 and a second clamp 11, the first clamp 10 and the second clamp 11 correspond to the magnetic core frame 16 and the first conveyor belt 2 respectively. After adopting above-mentioned structure, refer to figure 1, installation conveyer belt passes through conveyer belt conveying magnetic core 20 on workstation 1, the working process utilizes anchor clamps two 11 to place magnetic core 20 on the conveyer belt and carry out the rubber coating area on magnetic core frame 16, after the rubber coating is accomplished, take off magnetic core 20 on magnetic core frame 16 through anchor clamps one 10, and place next station, this device mechanical action is accurate, can be accurate place magnetic core 20 on the rubber coating station, after magnetic core 20 accomplished the rubber coating operation, again can be accurate take off magnetic core 20 and place follow-up station, need not artifical the participation in carrying out transformer rubber coating process, alleviate manual operation burden.
Regarding the specific structure of the first clamp 10 and the second clamp 11, referring to fig. 3, a slide 24 extending forward and backward is formed on the sliding table 18, the first clamp 10 includes a second slider 9 slidably mounted in the slide 24, the second slider 9 is provided with two and spaced forward and backward, the second slider 9 extends out from the lower side of the sliding table 18, a clamping plate 21 is fixedly arranged on the lower side of the second slider 9, two threaded holes 25 penetrating forward and backward are formed in the second slider 9, the two threaded holes 25 are opposite in rotation direction, the clamp motor 22 is mounted on the sliding table 18, the screw 23 is mounted on an output shaft of the clamp motor 22, two sets of threads opposite in rotation direction are arranged on the screw 23, the two sets of threads extend from the center of the screw 23 to two sides, the screw 23 is screwed in the two threaded holes 25, and. After the structure is adopted, when the first fixture 10 clamps the magnetic core 20, the motor drives the lead screw 23 to rotate, the two clamping plates 21 are closed towards the middle to clamp the magnetic core 20, after the magnetic core 20 moves to a preset station, the motor drives the lead screw 23 to rotate in the reverse direction, the two clamping plates 21 move towards the back, and the magnetic core 20 is separated from the first fixture 10.
In order to guarantee that the second clamp 11 can accurately clamp the magnetic core 20, referring to fig. 1 and fig. 2, the front side and the rear side of the first conveyor belt 2 are respectively provided with a material blocking block 26, the material blocking block 26 extends along the length direction of the first conveyor belt 2, the upper edge of the material blocking block 26 is higher than the height of the first conveyor belt 2, the front-rear distance of the two material blocking blocks 26 corresponds to the width of the magnetic core 20, the left end of the first conveyor belt 2 is provided with a limiting frame 15, and the height of the limiting frame 15 is not higher than the height of the. The material blocking block 26 ensures the relative position of the magnetic core 20 on the first conveyor belt 2, and after the magnetic core 20 is conveyed to the left end of the first conveyor belt, the magnetic core 20 is intercepted by the limiting frame 15, so that the magnetic core 20 enters a clamping station to wait for being clamped by the second clamp 11. In order to further realize the automation of the device, a second conveyor belt 3 is further installed on the workbench 1, the second conveyor belt 3 is located on the left side of the rotary table 12, and the distance between the second conveyor belt 3 and the magnetic core frame 16 is not larger than the distance between the first clamp 10 and the second clamp 11. After the magnetic core 20 is subjected to the encapsulation work, the second clamp 11 clamps the magnetic core 20, and the magnetic core 20 is taken down from the magnetic core frame 16 and placed on the second conveyor belt 3.
In order to ensure the stability of the lifting frame 4 in up-down lifting, referring to fig. 1, a plurality of vertical rods 27 extending up and down are installed on the working platform 1, a sliding sleeve corresponding to the vertical rods 27 is fixedly installed on the lifting frame 4, a top spring 28 is sleeved on the vertical rod 27, the lower end of the top spring 28 abuts against the upper side of the working platform 1, and the upper end abuts against the lower side of the sliding sleeve. With regard to the mounting structure of the tape roll 19, a reel 29 is vertically mounted on the table 1, and the tape roll 19 is rotatably mounted on the reel 29. A cutter cylinder 13 is fixedly arranged on the workbench 1, the cutter cylinder 13 is positioned on the front side of the rotary table 12, a cutter 14 is fixedly arranged at the top end of the cutter cylinder 13, and the top end of the cutter 14 faces to the position between the two magnetic core frames 16. After the magnetic core 20 is encapsulated, the cutter cylinder 13 advances the cutter 14 to cut off the adhesive tape.
The rubber coating device executes a working cycle, the first conveyor belt 2 transmits the magnetic core to the left end of the first conveyor belt 2, when the magnetic core is intercepted by the limiting frame 15, the magnetic core enters a waiting station, at the moment, the sliding cylinder 5 extends to push the first slider 8 to slide rightwards, the second clamp 11 moves to the position above the magnetic core, the lifting cylinder 6 contracts to drive the lifting frame 4 to fall, at the moment, the clamp motor 22 acts, the second clamp 11 clamps the magnetic core which is not rubber coated on the first conveyor belt 2, the first clamp 10 clamps the magnetic core which is rubber coated on the magnetic core frame 16, then the lifting cylinder 6 contracts to drive the lifting frame 4 to rise, the sliding cylinder 5 contracts to drive the first slider 8 to slide leftwards, after the second clamp 11 moves to the position above the magnetic core frame 16, the lifting cylinder 6 contracts to drive the lifting frame 4 to fall, at the moment, the clamp motor 22 acts, the second clamp 11 places the magnetic core on the, the cores on the core frame 16 enter the encapsulation station to begin encapsulation.
Finally, it should be noted that: the above embodiments are only used to illustrate the technical solution of the present invention, and not to limit the same; while the invention has been described in detail and with reference to the foregoing embodiments, it will be understood by those skilled in the art that: the technical solutions described in the foregoing embodiments may still be modified, or some or all of the technical features may be equivalently replaced; and the modifications or the substitutions do not make the essence of the corresponding technical solutions depart from the scope of the technical solutions of the embodiments of the present invention.
To sum up, the present invention is not limited to the above-mentioned specific embodiments. Those skilled in the art can make various changes and modifications without departing from the spirit and scope of the present invention, and all such changes and modifications are intended to be within the scope of the present invention.