CN212191431U - Double-sided milling cutter - Google Patents
Double-sided milling cutter Download PDFInfo
- Publication number
- CN212191431U CN212191431U CN202020594545.0U CN202020594545U CN212191431U CN 212191431 U CN212191431 U CN 212191431U CN 202020594545 U CN202020594545 U CN 202020594545U CN 212191431 U CN212191431 U CN 212191431U
- Authority
- CN
- China
- Prior art keywords
- milling cutter
- double
- installation department
- terminal surface
- sided
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003801 milling Methods 0.000 title claims abstract description 85
- 238000009434 installation Methods 0.000 claims abstract description 35
- 238000002347 injection Methods 0.000 claims abstract description 19
- 239000007924 injection Substances 0.000 claims abstract description 19
- 238000001816 cooling Methods 0.000 claims abstract description 18
- 230000002093 peripheral effect Effects 0.000 claims abstract description 12
- 239000002826 coolant Substances 0.000 claims description 22
- 239000007788 liquid Substances 0.000 claims description 21
- 239000000110 cooling liquid Substances 0.000 abstract description 7
- 238000012986 modification Methods 0.000 description 3
- 230000004048 modification Effects 0.000 description 3
- ZZUFCTLCJUWOSV-UHFFFAOYSA-N furosemide Chemical compound C1=C(Cl)C(S(=O)(=O)N)=CC(C(O)=O)=C1NCC1=CC=CO1 ZZUFCTLCJUWOSV-UHFFFAOYSA-N 0.000 description 2
- 238000003754 machining Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 239000000243 solution Substances 0.000 description 2
- 229910000851 Alloy steel Inorganic materials 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 239000007921 spray Substances 0.000 description 1
Images


Landscapes
- Milling Processes (AREA)
Abstract
The utility model provides a double-sided milling cutter, which solves the technical problems that the temperature of the milling cutter rises faster during milling and the service life is obviously reduced in the prior art; the milling cutter comprises a milling cutter body and a plurality of installation parts, wherein the milling cutter body is annular, the number of the installation parts is even, the installation parts are uniformly distributed on the peripheral surface of the milling cutter body, each installation part is provided with a first end surface, a top surface and a second end surface which are sequentially connected, the first end surface and the second end surface are both connected with the peripheral surface of the milling cutter body, a cutter head clamping groove is formed in the second end surface of each installation part, and the cutter head clamping grooves of every two adjacent installation parts are arranged on two sides of the corresponding second end surface in a; a cooling liquid injection port is formed in the first end face of each installation portion, a cooling flow channel is formed in the milling cutter body corresponding to each installation portion, one end of each cooling flow channel extends to the cooling liquid injection port communicated with the corresponding installation portion, and the other end of each cooling flow channel extends to the inner peripheral face of the milling cutter body to form a cooling liquid inflow port.
Description
Technical Field
The utility model relates to a machine tool machining cutter technical field, concretely relates to two-sided milling cutter.
Background
The milling cutter is usually used for milling a workpiece needing to be machined, the milling amount is large when a large workpiece is machined, the milling cutter continuously works and rubs the workpiece greatly, the temperature of the milling cutter rises quickly in the milling process, the service life of the milling cutter is obviously shortened, materials to be machined are easy to carbonize, and the milling efficiency and quality are seriously reduced.
SUMMERY OF THE UTILITY MODEL
The utility model provides a two-sided milling cutter to solve among the prior art milling cutter temperature rise when milling very fast, the technical problem that the life-span obviously reduced.
In order to solve the technical problem, the utility model discloses a technical scheme be:
the utility model provides a two-sided milling cutter, includes milling cutter main part and a plurality of installation department, the milling cutter main part is the ring form, the figure of installation department is the even number, and a plurality of installation department evenly distributed in on the outer peripheral face of milling cutter main part, each the installation department has first terminal surface, top surface and the second terminal surface that connects gradually, first terminal surface with the second terminal surface all with the outer peripheral face of milling cutter main part is connected, is formed with a tool bit draw-in groove that is used for installing the tool bit on the second terminal surface of each installation department, every two adjacent tool bit draw-in grooves of installation department crisscross set up in the both sides of corresponding the second; each be formed with a coolant liquid injection mouth on the first terminal surface of installation department, coolant liquid injection mouth orientation with correspond the adjacent second terminal surface setting of first terminal surface, the inside each that corresponds of milling cutter main part the installation department is formed with a cooling channel, cooling channel's one end extends to the intercommunication and corresponds the coolant liquid injection mouth of installation department, the other end extends to the inner peripheral surface of milling cutter main part forms the coolant liquid inflow mouth.
The utility model discloses the two-sided milling cutter who adopts, a plurality of coolant liquid injection ports and cooling runner through setting up, make milling cutter at the during operation, each mounting groove corresponds coolant liquid injection port and cooling runner, circle is connected with the lathe pivot in the discoid milling cutter main part, connect through the lathe pivot and pour into the coolant liquid into, make the coolant liquid pour into mouthful by the coolant liquid and pour into, spout to the tool bit position from the coolant liquid injection port behind the cooling runner, make the tool bit in milling can cool off, the cooling runner passes from milling cutter main part is inside simultaneously, ensure that milling cutter main part's temperature maintains the lower temperature, extension milling cutter life.
The above description is only an overview of the technical solution of the present invention, and in order to make the technical means of the present invention clearer and can be implemented according to the content of the description, the following detailed description is made with reference to the preferred embodiments of the present invention and accompanying drawings. The detailed description of the present invention is given by the following examples and the accompanying drawings.
Drawings
The accompanying drawings, which are included to provide a further understanding of the invention and are incorporated in and constitute a part of this application, illustrate embodiment(s) of the invention and together with the description serve to explain the invention without undue limitation to the invention. In the drawings:
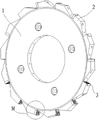
fig. 1 is a schematic perspective view of a double-sided milling cutter according to an embodiment of the present invention;
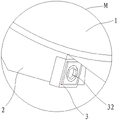
FIG. 2 is a schematic enlarged view of a portion of the area M in FIG. 1;
fig. 3 is a schematic cross-sectional view of a double-sided milling cutter according to an embodiment of the present invention;
fig. 4 is a schematic perspective view of a double-sided milling cutter according to an embodiment of the present invention after a cutter head is hidden;
FIG. 5 is an enlarged partial view of the area X in FIG. 4;
fig. 6 is a schematic structural diagram of a cutter head in an embodiment of the present invention.
Detailed Description
The principles and features of the present invention are described below in conjunction with the following drawings, the examples given are only intended to illustrate the present invention and are not intended to limit the scope of the present invention. The invention is described in more detail in the following paragraphs by way of example with reference to the accompanying drawings. The advantages and features of the present invention will become more fully apparent from the following description and appended claims. It should be noted that the drawings are in simplified form and are not to precise scale, and are provided for convenience and clarity in order to facilitate the description of the embodiments of the present invention.
As shown in fig. 1 to 6, the present embodiment discloses a double-sided milling cutter, which includes a milling cutter body 1, a plurality of mounting portions 2, and a plurality of tool bits 3.
Wherein, the milling cutter body 1 is annular; the number of the mounting portions 2 is even, in this embodiment, the number of the mounting portions is 14, the 14 mounting portions are uniformly distributed on the outer peripheral surface of the milling cutter body 1, and preferably, the mounting portions 2 and the milling cutter body 1 are of an integrally formed structure.
Each mounting part 2 is provided with a first end face 21, a top face 22 and a second end face 23 which are sequentially connected, wherein the first end face 21 and the second end face 23 are both connected with the peripheral surface of the milling cutter body 1, a cutter head clamping groove 2a for mounting a cutter head 3 is formed on the second end face 23 of each mounting part 2, and the cutter head clamping grooves 2a of every two adjacent mounting parts 2 are arranged on two sides of the corresponding second end face 23 in a staggered manner; therefore, the number of the insert pocket 2a is also 14, 7 of them are located on the left side of the second end surface 23, and 7 are located on the right side of the second end surface 23, and can be used for machining the inner wall surface and the outer wall surface of the workpiece, respectively.
A cooling liquid injection port 21a is formed in a first end face 21 of each mounting portion 2, the cooling liquid injection port 21a is arranged towards a second end face 23 adjacent to the corresponding first end face 21, a cooling flow channel 11 is formed in the milling cutter body 1 corresponding to each mounting portion 2, one end of each cooling flow channel 11 extends to the corresponding cooling liquid injection port 21a of the mounting portion 2 in a communicating manner, and the other end of each cooling flow channel extends to the inner peripheral face of the milling cutter body 1 to form a cooling liquid inflow port 1 a.
In this embodiment, the tool bit 3 is a prism, the material is hard alloy steel, the tool bit slot 2a is a quadrangle, one set of opposite edges of the tool bit 3 is a cutting edge 31, the size of the bottom angle of the tool bit slot 2a is consistent with the size of the vertex angle of the edge where the cutting edge 31 is located, and the bottom angle of the tool bit slot 2a is consistent with the vertex angle of the edge where the cutting edge 31 is located, and the tool bit slot 2a and the vertex angle of the edge where the cutting edge 31 is located are exactly;
preferably, the size of the vertex angle of the edge on which the cutting edge 31 is positioned is 82 degrees to 85 degrees, and more preferably, the size of the vertex angle of the edge on which the cutting edge 31 is positioned is 82.88 degrees.
The bottom corner of the tool bit clamping groove 2a is concave to form a fan-shaped avoiding groove a1 with the depth of 0.6-0.8 mm.
In order to facilitate the installation of the cutting head 3, a mounting hole 3a is formed in the middle of the cutting head 3, a threaded hole 2b is formed in the bottom of the cutting head clamping groove 2a, and the cutting head 3 is fixedly connected to the cutting head clamping groove 2a through a screw 32.
Preferably, the screw 32 is a socket head cap screw with a left-handed fine thread to ensure the stability of fastening and prevent the loosening of the tool bit during use.
In actual use, after the cutting head 3 is mounted, in order to prevent the cutting head 3 from being broken in order to facilitate cutting work, the distance between one side of the cutting edge 31 for cutting and the mounting part 2 is preferably controlled to be 0.8-1.2 mm.
The tool bit 3 adopts the rhombus form, only need during milling one side cutting edge 31 can, when a cutting edge 31 work leads to milling efficiency and quality to descend for a long time, rotatable tool bit 3 is cut edge, adopts another and the cutting edge 31 of milling cutter to carry out milling process, 3 life of great promotion tool bit.
In order to ensure the structural stability of the installation part, the widths of the two sides of the installation part 2 are gradually increased along the direction away from the milling cutter body 1, and the included angle range between the plane where the side wall (the left side in the figure) on one side of the installation part 2 and the plane where the side wall of the milling cutter body is located is 15-17 degrees.
The number of installation department is 14, each the first terminal surface 21 of installation department 2 links to each other with adjacent the second terminal surface 22 of installation department, and every two adjacent installation departments 2 link together like this, guarantee milling cutter holistic structural integrity and stability, the jet direction of coolant liquid jet orifice 21a and the corresponding contained angle alpha of first terminal surface 21 is 118 ~ 120.
Use the example of figure 1 direction processing pump head body, milling cutter is at the during operation, and milling cutter anticlockwise high-speed rotation mills the outer wall of pump head body, adopts 7 dorsad milling cutter to mill, when needs mill the inner wall of pump head body face, adopts tool bit 3 towards this moment to mill, so, the utility model discloses alright with milling workpiece outer wall and work piece inner wall.
The utility model discloses the two-sided milling cutter that adopts, a plurality of coolant liquid injection ports 21a and cooling runner 11 through setting up, make milling cutter at the during operation, each mounting groove 2a corresponds a coolant liquid injection port 21a and cooling runner 11, circle is connected with the lathe pivot in the discoid milling cutter main part 1, connect through the lathe pivot and pour into the coolant liquid, make the coolant liquid pour into the mouth by the coolant liquid, spray 3 positions to tool bit from coolant liquid injection port 2a behind cooling runner 11, make the tool bit 3 in milling can cool off, the cooling runner passes from milling cutter main part is inside simultaneously, ensure that the temperature of milling cutter main part maintains the lower temperature, extension milling cutter life.
The above description is only a preferred embodiment of the present invention, and is not intended to limit the present invention in any way; the present invention can be smoothly implemented by those skilled in the art according to the drawings and the above description; however, those skilled in the art should understand that changes, modifications and variations made by the above-described technology can be made without departing from the scope of the present invention, and all such changes, modifications and variations are equivalent embodiments of the present invention; meanwhile, any changes, modifications, evolutions, etc. of the above embodiments, which are equivalent to the actual techniques of the present invention, still belong to the protection scope of the technical solution of the present invention.
Claims (10)
1. The utility model provides a two-sided milling cutter, its characterized in that, includes milling cutter main part and a plurality of installation department, the milling cutter main part is the ring form, the figure of installation department is the even number, and a plurality of the installation department evenly distributed in on the outer peripheral face of milling cutter main part, each the installation department has first terminal surface, top surface and the second terminal surface that connects gradually, first terminal surface with the second terminal surface all with the outer peripheral face of milling cutter main part is connected, is formed with a tool bit draw-in groove that is used for installing the tool bit on the second terminal surface of each installation department, every two adjacent tool bit draw-in grooves of installation department set up in the both sides corresponding the second terminal; each be formed with a coolant liquid injection mouth on the first terminal surface of installation department, coolant liquid injection mouth orientation with correspond the adjacent second terminal surface setting of first terminal surface, the inside each that corresponds of milling cutter main part the installation department is formed with a cooling channel, cooling channel's one end extends to the intercommunication and corresponds the coolant liquid injection mouth of installation department, the other end extends to the inner peripheral surface of milling cutter main part forms the coolant liquid inflow mouth.
2. The double-sided milling cutter according to claim 1, further comprising a plurality of cutting inserts, wherein the cutting inserts are prism-shaped, the cutting insert pockets are quadrilateral, a set of opposing edges of the cutting inserts are cutting edges, and the bottom corners of the cutting insert pockets are sized to coincide with the top corners of the edges on which the cutting edges are located.
3. The double-sided milling cutter according to claim 2, wherein the apex angle of the edge on which the cutting edge is located is 82 ° to 85 °.
4. The double-sided milling cutter according to claim 3, wherein the apex angle of the edge on which the cutting edge is located is 82.88 °.
5. The double-sided milling cutter according to claim 2, wherein the bottom corner of the insert pocket is recessed to form a fan-shaped escape groove having a depth of 0.6-0.8 mm.
6. The double-sided milling cutter according to claim 2, wherein a mounting hole is formed at a middle portion of the insert, a threaded hole is formed at a bottom of the insert pocket, and the insert is fixedly coupled to the insert pocket by a screw.
7. The double-sided milling cutter according to claim 6, wherein the screw is a socket head cap screw having a left-handed fine thread.
8. The double-sided milling cutter according to claim 1, wherein widths of both sides of the mounting portion are gradually increased in a direction away from the milling cutter body, and an included angle between a plane of a side wall of the mounting portion and a plane of a side wall of the milling cutter body ranges from 15 ° to 17 °.
9. The double-sided milling cutter according to claim 1, wherein the number of the mounting portions is 14, and the first end surface of each of the mounting portions is connected to the second end surface of an adjacent one of the mounting portions.
10. The double-sided milling cutter according to claim 9, wherein the injection direction of the coolant injection port is at an angle of 118 ° to 120 ° with respect to the corresponding first end surface.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202020594545.0U CN212191431U (en) | 2020-04-20 | 2020-04-20 | Double-sided milling cutter |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202020594545.0U CN212191431U (en) | 2020-04-20 | 2020-04-20 | Double-sided milling cutter |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN212191431U true CN212191431U (en) | 2020-12-22 |
Family
ID=73832358
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202020594545.0U Expired - Fee Related CN212191431U (en) | 2020-04-20 | 2020-04-20 | Double-sided milling cutter |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN212191431U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113510299A (en) * | 2021-03-10 | 2021-10-19 | 东方电气集团东方汽轮机有限公司 | A single section and complete set of internal cooling carbide blade broach |
-
2020
- 2020-04-20 CN CN202020594545.0U patent/CN212191431U/en not_active Expired - Fee Related
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113510299A (en) * | 2021-03-10 | 2021-10-19 | 东方电气集团东方汽轮机有限公司 | A single section and complete set of internal cooling carbide blade broach |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109365846B (en) | Indexable turning blade | |
| KR20050084127A (en) | Tangential cutting insert and milling cutter | |
| CN110695386B (en) | Indexable turning tool | |
| CN103769663B (en) | Wide face and side cutter is cut in blisk special change of slotting | |
| CN113695653B (en) | Ball end milling cutter | |
| CN211727541U (en) | Indexable turning insert | |
| CN212217194U (en) | Insert for a hole machining tool | |
| CN117644221B (en) | Cutting insert and cutting tool with stable cutting | |
| CN207710013U (en) | A kind of PCD reamers | |
| CN218425840U (en) | Square shoulder milling cutter blade and cutter | |
| CN212191435U (en) | End-mounted milling cutter blade | |
| CN212469902U (en) | Indexable drilling blade | |
| CN211966065U (en) | Finish machining face milling cutter | |
| CN115740576A (en) | Drill bit blade with stepped cutting edge | |
| CN207668535U (en) | A kind of anticaustic turning tool rod of lathe | |
| CN206869197U (en) | A kind of cutting edge cutter blade of double-sided indexable four | |
| CN210648700U (en) | Profiling blade and cutter with same | |
| CN107414155A (en) | The cutting edge cutter blade of double-sided indexable four | |
| CN223056737U (en) | A multifunctional tool with turning, boring and drilling functions | |
| CN207086997U (en) | One kind is used for the flat cutter of blind hole | |
| CN113996873A (en) | A double-sided multi-edge thread insert and cutting tool | |
| CN210587327U (en) | Replaceable drilling blade | |
| CN211218847U (en) | Hard alloy drilling and chamfering combined tool | |
| CN214290886U (en) | Boring cutter | |
| CN218745092U (en) | Single-sided milling insert and milling tool therefor |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20201222 |