CN211638413U - Auxiliary tool for drilling and riveting of chassis boundary beam and casting - Google Patents
Auxiliary tool for drilling and riveting of chassis boundary beam and casting Download PDFInfo
- Publication number
- CN211638413U CN211638413U CN202020006276.1U CN202020006276U CN211638413U CN 211638413 U CN211638413 U CN 211638413U CN 202020006276 U CN202020006276 U CN 202020006276U CN 211638413 U CN211638413 U CN 211638413U
- Authority
- CN
- China
- Prior art keywords
- riveting
- drilling
- casting
- side beam
- positioning
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000005266 casting Methods 0.000 title claims abstract description 57
- 238000005553 drilling Methods 0.000 title claims abstract description 49
- 238000000034 method Methods 0.000 abstract description 24
- 230000008569 process Effects 0.000 abstract description 16
- 229910000838 Al alloy Inorganic materials 0.000 abstract description 12
- 238000012545 processing Methods 0.000 abstract description 9
- 238000005096 rolling process Methods 0.000 description 21
- 238000012360 testing method Methods 0.000 description 10
- 238000013461 design Methods 0.000 description 9
- 238000010586 diagram Methods 0.000 description 8
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 7
- 229910052782 aluminium Inorganic materials 0.000 description 7
- 238000004519 manufacturing process Methods 0.000 description 4
- 230000009471 action Effects 0.000 description 3
- 230000006872 improvement Effects 0.000 description 2
- 238000009434 installation Methods 0.000 description 2
- 238000003754 machining Methods 0.000 description 2
- 239000003973 paint Substances 0.000 description 2
- 230000008439 repair process Effects 0.000 description 2
- 241000271559 Dromaiidae Species 0.000 description 1
- 230000008859 change Effects 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 238000009826 distribution Methods 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000007689 inspection Methods 0.000 description 1
- 230000001788 irregular Effects 0.000 description 1
- 239000000463 material Substances 0.000 description 1
- 238000005457 optimization Methods 0.000 description 1
- 238000011112 process operation Methods 0.000 description 1
- 238000012795 verification Methods 0.000 description 1
- 238000003466 welding Methods 0.000 description 1
Images


Landscapes
- Connection Of Plates (AREA)
Abstract
本实用新型所述用于底架边梁与铸件钻孔铆接的辅助工装,提出新型的钻孔铆接辅助工装,以针对性地解决铝合金底架边梁与铸件的铆接加工问题,以期实现一种实用性强、钻孔精准度高、加工效率高的钻孔铆接工艺,有效地解决现有底架边梁难于精准钻孔和拉铆后产品质量不稳定的问题,降低现场加工工作强度和提高生产效率。辅助工装包括有托板,F型卡栏,支撑框架,定位支撑块和磁力钻。所述的托板具有平板状结构,支撑框架的截面形状为L型,定位支撑块具有至少两个连接为一体的连续的T型结构。所述的支撑框架在其两个直角折边之间设置一截面为矩形的通槽,边梁的外缘抵入通槽中。
The utility model provides an auxiliary tool for drilling and riveting between the edge beam of the chassis frame and the casting, and proposes a new auxiliary tool for drilling and riveting, so as to solve the problem of riveting processing of the edge beam and the casting of the aluminum alloy chassis in a targeted manner, so as to realize a It is a drilling riveting process with strong practicability, high drilling accuracy and high processing efficiency, which effectively solves the problem that the existing underframe side beams are difficult to drill accurately and the product quality is unstable after riveting, and reduces the intensity of on-site processing work and Increase productivity. Auxiliary tooling includes pallets, F-type clip bars, support frames, positioning support blocks and magnetic drills. The support plate has a flat plate-like structure, the cross-sectional shape of the support frame is L-shape, and the positioning support block has at least two continuous T-shape structures that are connected as a whole. The support frame is provided with a through groove with a rectangular cross-section between the two right-angle folded edges, and the outer edge of the side beam abuts into the through groove.
Description
技术领域technical field
本实用新型涉及一种适用于铝合金动车组的底架边梁与铸件实施钻孔铆接加工的辅助工装,属于轨道车辆设计领域。The utility model relates to an auxiliary tool which is suitable for drilling and riveting processing of an underframe side beam and a casting of an aluminum alloy EMU, and belongs to the field of rail vehicle design.
背景技术Background technique
随着动车组技术的快速发展与列车运行速度的提高,车体结构设计与组装加工工艺不断地得以优化与提升,车体结构设计日趋成熟。With the rapid development of EMU technology and the improvement of train running speed, the structure design and assembly process of the car body have been continuously optimized and improved, and the structure design of the car body has become more and more mature.
底架作为铝合金车体的重要部件之一,直接与转向架相连接且起到举足轻重的连接与承载分配的基础作用。而边梁上的重要附件—抗侧滚安装座的精准定位尺寸会直接影响到车体的质量及安全,因此,对于此类抗侧滚安装座的加工位置与尺寸、产品质量等性能均提出了较高的要求。As one of the important parts of the aluminum alloy car body, the underframe is directly connected to the bogie and plays a pivotal role in connection and load distribution. The important accessory on the side beam, the precise positioning size of the anti-rolling mount, will directly affect the quality and safety of the car body. higher requirements.
现有铝合金车体的底架边梁附件—抗侧滚安装座,是直接焊接在边梁上的铝合金结构,受焊接变形因素的影响,难于调修,且很难保证尺寸公差要求。较为新型改进设计,是将抗侧滚安装座由铝合金结构改为铸件结构,采用现场手动配钻的方式通过铆钉将铸件固定在边梁上,因此边梁的设计结构、抗侧滚安装座的安装空间位置和手动钻孔等人为不确定因素等,直接决定了现场配钻孔的难易及所钻孔的精准度。The side beam attachment of the existing aluminum alloy car body, the anti-rolling mount, is an aluminum alloy structure directly welded on the side beam. It is difficult to adjust and repair due to the influence of welding deformation factors, and it is difficult to ensure the dimensional tolerance requirements. The relatively new and improved design is to change the anti-rolling mounting seat from an aluminum alloy structure to a casting structure, and use on-site manual drilling to fix the casting on the side beam by rivets. Therefore, the design structure of the side beam, the anti-rolling mounting seat The installation space location and manual drilling and other human uncertain factors directly determine the difficulty and accuracy of drilling on-site drilling.
例如申请人现有设计与使用的某型铝合金城轨列车,抗侧滚安装座为铸件结构,边梁结构及抗侧滚安装座的空间位置使得现场难于将抗侧滚安装座进行夹持固定;同时受抗侧滚安装座的空间安装位置和手动操作等人为不确定因素的影响,一方面铝合金边梁型材配钻孔的尺寸难以满足铆接所需的公差尺寸要求,即无法保证钻孔精准度;另一方面手动现场配钻工作强度大,生产效率低;此外,铆接工艺步骤不合理,会增加铆接难度,易造成铆钉松动或铸件与边梁接触面出现间隙,无法保证产品质量。For example, in a certain type of aluminum alloy urban rail train currently designed and used by the applicant, the anti-rolling mounting seat is a casting structure, and the side beam structure and the spatial position of the anti-rolling mounting seat make it difficult to clamp the anti-rolling mounting seat on site. Fixed; at the same time, affected by human uncertain factors such as the space installation position of the anti-rolling mounting seat and manual operation, on the one hand, the size of the aluminum alloy side beam profile with the drill hole is difficult to meet the tolerance size requirements required for riveting, that is, the drill hole cannot be guaranteed. Hole accuracy; on the other hand, manual on-site drilling has high work intensity and low production efficiency; in addition, the unreasonable riveting process steps will increase the difficulty of riveting, which is easy to cause loosening of rivets or gaps in the contact surface between castings and edge beams, which cannot guarantee product quality. .
有鉴于此,特提出本申请。In view of this, this application is hereby made.
实用新型内容Utility model content
本实用新型所述的用于底架边梁与铸件钻孔铆接的辅助工装,其设计目的在于解决上述现有技术存在的问题而提出新型的钻孔铆接辅助工装,以针对性地解决铝合金底架边梁与铸件的铆接加工问题,以期实现一种实用性强、钻孔精准度高、加工效率高的钻孔铆接工艺,有效地解决现有底架边梁难于精准钻孔和拉铆后产品质量不稳定的问题,降低现场加工工作强度和提高生产效率。The auxiliary tooling for drilling and riveting between the edge beam of the underframe and the casting of the utility model is designed to solve the problems existing in the prior art and propose a new auxiliary tooling for drilling and riveting, so as to solve the problem of aluminum alloys in a targeted manner. The problem of riveting processing between the edge beam of the chassis and the casting is expected to realize a drilling and riveting process with strong practicability, high drilling accuracy and high processing efficiency, and effectively solve the difficulty of accurate drilling and riveting of the existing edge beam of the chassis. After the problem of unstable product quality, reduce the intensity of on-site processing work and improve production efficiency.
为实现上述设计目的,本申请提出一种新的用于底架边梁与铸件钻孔铆接的辅助工装,主要包括有托板,F型卡栏,支撑框架,定位支撑块和磁力钻。In order to achieve the above design purpose, the present application proposes a new auxiliary tool for drilling and riveting the side beam of the underframe and the casting, which mainly includes a pallet, an F-type clip, a support frame, a positioning support block and a magnetic drill.
其中,所述的托板具有平板状结构,支撑框架的截面形状为L型,定位支撑块具有至少两个连接为一体的连续的T型结构。Wherein, the support plate has a plate-like structure, the cross-sectional shape of the support frame is L-shaped, and the positioning support block has at least two continuous T-shaped structures connected as one.
进一步地,可采取的优化与改进方案是,所述的支撑框架在其两个直角折边之间设置一截面为矩形的通槽,边梁的外缘抵入通槽中。Further, an optimization and improvement solution that can be adopted is that a through groove with a rectangular cross-section is arranged between the two right-angle folded edges of the support frame, and the outer edge of the side beam abuts into the through groove.
具体的钻孔与铆接定位结构是,在边梁下表面处,所述的托板、铸件各自位于边梁下表面上,磁力钻位于托板上;至少一个F型卡栏夹持固定于托板上表面与边梁下表面的垂向两端,至少一个F型卡栏夹持于铸件与边梁下表面的垂向两端;The specific drilling and riveting positioning structure is as follows: at the lower surface of the side beam, the supporting plate and the casting are respectively located on the lower surface of the side beam, and the magnetic drill is located on the supporting plate; at least one F-shaped clip is clamped and fixed on the supporting plate. At the vertical ends of the upper surface of the board and the lower surface of the side beam, at least one F-type clip is clamped at the vertical ends of the casting and the lower surface of the side beam;
在边梁内斜面处,所述的定位支撑块、铸件各自位于边梁内斜面上,磁力钻位于定位支撑块上,支撑框架位于边梁的下表面外缘;至少一个F型卡栏夹持固定于定位支撑块的上表面与支撑框架底面的垂向之间,至少一个F型卡栏夹持于铸件与支撑框架底面的垂向两端。At the inner slope of the side beam, the positioning support block and the casting are respectively located on the inner slope of the side beam, the magnetic drill is located on the positioning support block, and the support frame is located on the outer edge of the lower surface of the side beam; at least one F-type clip clamps It is fixed between the upper surface of the positioning support block and the vertical direction of the bottom surface of the supporting frame, and at least one F-shaped clip is clamped between the vertical ends of the casting and the bottom surface of the supporting frame.
如上述辅助工装的结构设计与定位连接方式,是依据边梁和铸件的结构特点设计的,能够通过灵活地转换磁力钻定位基准参考面,以边梁内斜面和边梁下表面作为定位基准面,平行于边梁内斜面设计定位支撑块,平行于边梁下表面设计托板,对铸件分别进行侧向和竖直方向夹紧定位,为机械钻孔的精准性提供了必要的前提条件。For example, the structural design and positioning connection method of the above-mentioned auxiliary tooling are designed according to the structural characteristics of the side beams and castings. It can flexibly convert the magnetic drill to locate the datum reference plane, and use the inner slope of the side beam and the lower surface of the side beam as the positioning datum plane. , the positioning support block is designed parallel to the inner slope of the side beam, the pallet is designed parallel to the lower surface of the side beam, and the castings are clamped and positioned in the lateral and vertical directions respectively, which provides the necessary prerequisites for the accuracy of mechanical drilling.
所述定位支撑块的结构设计,是根据边梁的结构及铸件的形状尺寸特点,避免与铸件发生干涉,满足在边梁内斜面处的磁力钻机械钻孔对行程的需求。能够从整体上保证平面度、垂直度等位置尺寸公差的要求,保证所钻的孔的精准度。The structural design of the positioning support block is based on the structure of the side beam and the shape and size characteristics of the casting to avoid interference with the casting, and to meet the travel requirements of the magnetic drill mechanical drilling at the inner slope of the side beam. It can guarantee the requirements of positional dimensional tolerances such as flatness and verticality as a whole, and ensure the accuracy of the drilled holes.
应用上述用于底架边梁与铸件钻孔铆接的辅助工装的基础上,本申请同时提出一种改进型铆接工艺方法。包括有以下实施步骤:Based on the application of the above-mentioned auxiliary tool for drilling and riveting the edge beam of the chassis and the casting, the present application simultaneously proposes an improved riveting process method. The following implementation steps are included:
(1)铆钉拉铆工艺试验;(1) Rivet pull riveting process test;
(2)边梁划线对铸件进行尺寸定位;(2) Scribing the edge beam to locate the size of the casting;
(3)匹配铸件铆钉孔对边梁下表面铝型材钻定位孔及拉铆定位;(3) Drilling positioning holes and pulling riveting positioning of the aluminum profile on the lower surface of the side beam to match the rivet hole of the casting;
(4)匹配铸件铆钉孔对边梁内斜面铝型材钻定位孔及拉铆定位;(4) Drilling positioning holes and pulling riveting positioning for matching casting rivet holes to the inner sloped aluminum profile of the side beam;
(5)匹配铸件铆钉孔对边梁铝型材其余位置钻孔及拉铆。(5) Match the rivet hole of the casting to drill and rivet the rest of the aluminum profile of the side beam.
进一步地,在对实物产品拉铆前,对铆钉进行拉铆工艺试验以对铆钉枪设备能力及铆钉质量进行工艺验证。Further, before the riveting of the physical product, the riveting process test is performed on the rivet to verify the process verification of the equipment capability of the rivet gun and the quality of the rivet.
进一步地,采用磁力钻匹配铸件铆钉孔对边梁型材进行机械式钻孔。Further, a magnetic drill is used to match the rivet holes of the casting to mechanically drill the side beam profiles.
应用辅助工装分别进行如下钻孔与铆接定位,在边梁下表面处,所述的托板、铸件各自位于边梁下表面上,磁力钻位于托板上;至少一个F型卡栏夹持固定于托板上表面与边梁下表面的垂向两端,至少一个F型卡栏夹持于铸件与边梁下表面的垂向两端;Use auxiliary tooling to carry out the following drilling and riveting positioning respectively. At the lower surface of the side beam, the supporting plate and casting are respectively located on the lower surface of the side beam, and the magnetic drill is located on the supporting plate; at least one F-type clip is clamped and fixed. On the vertical ends of the upper surface of the pallet and the lower surface of the side beam, at least one F-shaped clip is clamped at the vertical ends of the casting and the lower surface of the side beam;
在边梁内斜面处,所述的定位支撑块、铸件各自位于边梁内斜面上,磁力钻位于定位支撑块上,支撑框架位于边梁的下表面外缘;至少一个F型卡栏夹持固定于定位支撑块的上表面与支撑框架底面的垂向之间,至少一个F型卡栏夹持于铸件与支撑框架底面的垂向两端。At the inner slope of the side beam, the positioning support block and the casting are respectively located on the inner slope of the side beam, the magnetic drill is located on the positioning support block, and the support frame is located on the outer edge of the lower surface of the side beam; at least one F-type clip clamps It is fixed between the upper surface of the positioning support block and the vertical direction of the bottom surface of the supporting frame, and at least one F-shaped clip is clamped between the vertical ends of the casting and the bottom surface of the supporting frame.
综上内容,本申请用于底架边梁与铸件钻孔铆接的辅助工装具有的优点是:To sum up, the advantages of the auxiliary tooling used for drilling and riveting the edge beam of the underframe and the casting of the present application are:
1、针对现有铝合金动车组的边梁与铸件的结构特点,通过提出的钻孔铆接辅助工装能够灵活地转换磁力钻定位基准参考面,分别以边梁内斜面与下表面作为定位基准面,为机械钻孔的精准性提供了必要的前提条件,辅助工装实用性强、操作灵活。1. According to the structural characteristics of the side beams and castings of the existing aluminum alloy EMUs, the proposed drilling and riveting auxiliary tool can flexibly convert the magnetic drill positioning datum reference plane, and use the inner slope and lower surface of the side beam as the positioning datum plane respectively. , which provides the necessary prerequisites for the accuracy of mechanical drilling, and the auxiliary tooling is practical and flexible.
2、采用磁力钻匹配铸件铆钉孔对边梁型材进行机械式钻孔,相比以往的手动钻孔,避免了外界不确定干扰因素的影响,保证了钻孔的精准性,降低了工作强度,显著的提高了生产效率,保证了产品质量。2. The magnetic drill is used to match the rivet holes of the castings to mechanically drill the side beam profiles. Compared with the previous manual drilling, it avoids the influence of external uncertain interference factors, ensures the accuracy of drilling, and reduces the work intensity. Significantly improve production efficiency and ensure product quality.
3、改进后的边梁与铸件钻孔及铆接工艺流程,对钻孔和拉铆操作步骤进行明确,极大的保证了产品质量,避免实物产品拉铆后的返修。3. The improved drilling and riveting process of the edge beam and castings clearly defines the operation steps of drilling and riveting, which greatly ensures the quality of the product and avoids the rework after the riveting of the physical product.
附图说明Description of drawings
图1是底架边梁与铸件组装加工的位置和结构示意图;Fig. 1 is the position and structure schematic diagram of underframe side beam and casting assembly processing;
图2是边梁与铸件进行钻孔及铆接的工艺流程图;Fig. 2 is the process flow diagram of drilling and riveting the side beam and the casting;
图3是铆钉工艺试验的示意图;Fig. 3 is the schematic diagram of rivet process test;
图4是底架边梁下表面与铸件钻孔铆接的示意图;Fig. 4 is the schematic diagram of the bottom surface of underframe side beam and casting drilling riveting;
图5是图4的A-A向剖面示意图;Fig. 5 is the A-A sectional schematic diagram of Fig. 4;
图6是底架边梁内斜面与铸件钻孔铆接的示意图;Figure 6 is a schematic diagram of the riveting of the inner inclined surface of the side beam of the underframe and the drilling hole of the casting;
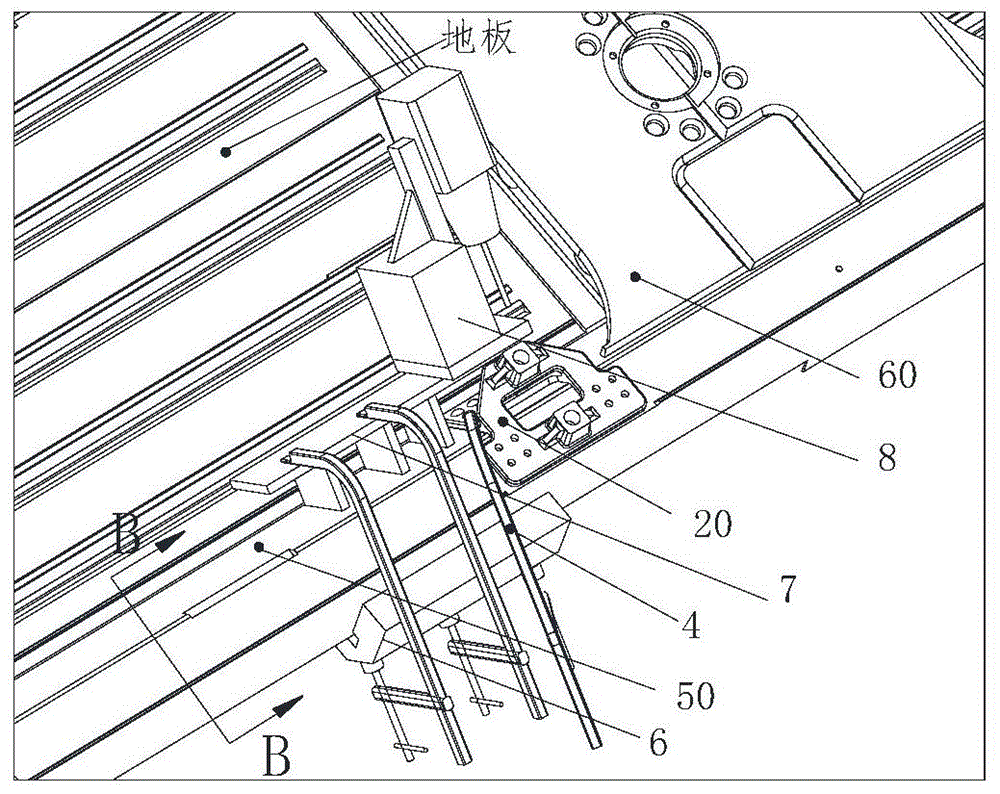
图7是图6的B-B向剖面示意图;Fig. 7 is the B-B sectional schematic diagram of Fig. 6;
图8是支撑框架和定位支撑块的结构对比示意图;Fig. 8 is the structural comparison schematic diagram of the support frame and the positioning support block;
具体实施方式Detailed ways
下面结合附图对本实用新型作进一步详细描述。The present utility model will be described in further detail below in conjunction with the accompanying drawings.
实施例1,以城际轨道车辆的铝合金底架边梁与抗侧滚安装座铸件进行钻孔铆接加工为例。Example 1, taking as an example the drilling and riveting processing of the aluminum alloy underframe side beam and the anti-rolling mounting seat casting of the intercity rail vehicle.
如图1所示,在底架(图中显示有构成底架的枕梁60、以及安装于底架的地板70)单侧边梁10的靠近端部处,抗侧滚安装座20通过铆钉30分别安装固定于边梁下表面40、边梁内斜面50。As shown in FIG. 1 , at the near end of the
边梁10的结构为近圆柱形、不规则形状,抗侧滚安装座20采用整体机加工方式以保证铸件上的机加工铆钉孔、铸件平面度、角度等位置尺寸与公差的标准要求。The structure of the
位于边梁下表面40上的铆钉孔数量为8个,位于边梁内斜面50上的铆钉孔数量为6个。The number of rivet holes located on the
为实现上述底架边梁与抗侧滚安装座钻孔铆接的加工精度要求,本申请所述的辅助工装主要包括有托板3,F型卡栏4,支撑框架6,定位支撑块7和磁力钻8。In order to realize the machining accuracy requirements of the above-mentioned underframe side beams and the anti-rolling mounting seat drilling and riveting, the auxiliary tooling described in this application mainly includes a
其中,所述的托板3具有平板状结构;Wherein, the
如图8所示,所述支撑框架6的截面形状为L型,在其两个直角折边之间设置一截面为4mm2矩形的通槽61,将支撑框架6衬垫于边梁10的外侧时,边梁10的外缘抵入通槽61中;As shown in FIG. 8 , the cross-sectional shape of the
所述的定位支撑块7,优选具有至少两个连接为一体的连续的T型结构。The
如图4和图5所示,在边梁下表面40处,应用上述辅助工装,所述的托板3、抗侧滚安装座20各自位于边梁下表面40上,磁力钻8位于托板3上;两个F型卡栏4夹持固定于托板3上表面与边梁下表面40的垂向两端,另外两个F型卡栏4夹持于抗侧滚安装座20与边梁下表面40的垂向两端。As shown in FIG. 4 and FIG. 5 , at the
如图6和图7所示,在边梁内斜面50处,应用上述辅助工装,所述的定位支撑块7、抗侧滚安装座20各自位于边梁内斜面50上,磁力钻8位于定位支撑块7上,支撑框架6位于边梁10的下表面外缘;两个F型卡栏4夹持固定于定位支撑块7的上表面与支撑框架6底面的垂向之间,另外一个F型卡栏4夹持于抗侧滚安装座20与支撑框架6底面的垂向两端。As shown in FIG. 6 and FIG. 7 , at the
如图2所示,应用于铝合金底架边梁10与抗侧滚安装座20的铸件铆接工艺方法,包括有以下实施步骤:As shown in FIG. 2 , the casting riveting process method applied to the
将边梁铆接区域进行清洁及涂漆,待油漆干燥后继续后工序作业;Clean and paint the riveted area of the side beam, and continue the post-process operation after the paint is dry;
进行铆钉工艺试验,如图3所示,为验证铆钉枪80设备能力及铆钉30质量,需模拟实物产品进行拉铆试验,如用试板1模拟边梁型材材质和壁厚,试板2模拟铸件材质和壁厚,且按试板1和试板2需按拉铆所需尺寸预机加出铆钉孔,将两块试板贴紧固定后用铆钉枪进行拉铆;拉铆试验结束后,在试板上标识车号、时间、操作者等信息,便于产品质量追溯,铆钉外观和尺寸检验合格后再进行正式产品件拉铆作业;Carry out the rivet process test, as shown in Figure 3, in order to verify the equipment capability of the
在边梁10上,对抗侧滚安装座20按图纸尺寸进行定位尺寸划线,同时根据底架宽度尺寸对抗侧滚安装座铸件通过垫片调整间距尺寸;On the
匹配铸件铆钉孔对边梁下表面40铝型材钻定位孔,如图5所示,将抗侧滚安装座20按定位尺寸放置在边梁下表面40上,用2个F卡栏4将其在竖直方向进行夹紧固定;将机加工后的托板3放置于靠近铸件的边梁下表面40上,用2个F卡栏4将其在垂直方向进行夹紧固定;将磁力钻8放置托板3上,通电后在电磁力的作用下,磁力钻8吸附于托板3的表面,完成图1所示的边梁下表面40区域的2个铆钉钻孔;然后,在F卡栏4夹紧状态下进行边梁下表面40定位孔的拉铆操作,定位拉铆结束后,拆卸夹持在边梁下表面40的全部F卡栏4;Match the rivet holes of the casting to drill positioning holes for the aluminum profiles on the
匹配铸件铆钉孔对边梁内斜面50铝型材钻定位孔,如图7所示,先在定位支撑块7和F卡栏4的作用下,将贴附在边梁内斜面50的抗侧滚安装座20进行夹紧固定,以避免磁力钻8钻孔过程与抗侧滚安装座20发生共振而颤抖,影响钻孔精准度;然后将支撑框架6放置于边梁内斜面50上,用2个F卡栏4将定位支撑块7和支撑框架6进行夹紧固定,将磁力钻8放置支撑框架6上,通电后在电磁力的作用下,磁力钻8吸附于支撑框架6的表面,如图1所示的边梁内斜面50区域的2个铆钉钻孔;最后,在F卡栏4夹紧状态下进行边梁内斜面50定位孔的拉铆操作;Drill positioning holes for the rivet holes on the
继续匹配铸件铆钉孔对边梁内斜面50铝型材其它区域的钻孔,数量为4个;完成边梁内斜面50其余孔的拉铆操作后,拆卸相关的辅助工装;Continue to match the casting rivet holes to the other areas of the 50 aluminum profile on the inner slope of the side beam, and the number is 4; after completing the riveting operation of the remaining holes on the
继续匹配铸件铆钉孔对边梁下表面40铝型材其它区域的钻孔,数量为6个;完成边梁下表面40其余孔的拉铆操作后,拆卸相关的辅助工装;Continue to match the casting rivet holes to the other areas of the 40 aluminum profile on the lower surface of the side beam, the number is 6; after completing the riveting operation of the remaining holes on the
对铆接后铆钉进行尺寸和松动检验,合格后流转至下道工序。After riveting, the rivets are inspected for size and looseness, and the qualified ones are transferred to the next process.
如上所述,本申请所述用于底架边梁与铸件钻孔铆接的辅助工装,提出了一种实用性强、精准度高、效率高的辅助工装结构设计与连接方式,依据边梁和铸件的结构特点进行设计。所实现的铆接工艺方法,通过灵活地转换磁力钻8定位基准参考面,以边梁内斜面50和边梁下表面40分别作为定位基准面,为机械钻孔的精准性提供了必要的前提条件;采用磁力钻8匹配铸件铆钉孔对边梁10型材机械钻孔,相比以往的手动钻孔,避免了外界不确定干扰因素的影响,保证了钻孔的精准性,降低了工作强度,显著的提高了生产效率。所提出的边梁10与铸件钻孔及铆接的工艺流程,对钻孔和拉铆操作步骤进行明确,极大地保证了产品质量,避免实物产品拉铆后的返修;As mentioned above, the auxiliary tooling used for drilling and riveting the side beam of the underframe and the casting described in this application proposes a structural design and connection method of the auxiliary tooling with strong practicability, high precision and high efficiency. The structural characteristics of the casting are designed. The realized riveting process method, by flexibly converting the magnetic drill 8 to locate the datum reference plane, uses the inner sloped
综合地,辅助工装实用性强、操作灵活,极大的保证了对钻孔的精度和位置尺寸要求;同时,本申请对其他相似部件的钻孔和铆接提供了一定的经验借鉴。In general, the auxiliary tooling has strong practicability and flexible operation, which greatly ensures the accuracy and position and size requirements of drilling; at the same time, the present application provides certain experience and reference for drilling and riveting of other similar components.
如上所述,结合附图和描述给出的方案内容,但凡是未脱离本申请的结构方案,均仍属于本申请方案的保护范围。As mentioned above, the content of the solutions given in conjunction with the drawings and descriptions, provided that they do not depart from the structural solutions of the present application, still belong to the protection scope of the solutions of the present application.
Claims (3)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202020006276.1U CN211638413U (en) | 2020-01-02 | 2020-01-02 | Auxiliary tool for drilling and riveting of chassis boundary beam and casting |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN202020006276.1U CN211638413U (en) | 2020-01-02 | 2020-01-02 | Auxiliary tool for drilling and riveting of chassis boundary beam and casting |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211638413U true CN211638413U (en) | 2020-10-09 |
Family
ID=72703169
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN202020006276.1U Active CN211638413U (en) | 2020-01-02 | 2020-01-02 | Auxiliary tool for drilling and riveting of chassis boundary beam and casting |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211638413U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111085707A (en) * | 2020-01-02 | 2020-05-01 | 青岛四方庞巴迪铁路运输设备有限公司 | Auxiliary tooling and method for drilling and riveting of underframe side beams and castings |
| CN116689822A (en) * | 2023-07-20 | 2023-09-05 | 中车青岛四方机车车辆股份有限公司 | Drilling auxiliary device and method for rail transit vehicle |
-
2020
- 2020-01-02 CN CN202020006276.1U patent/CN211638413U/en active Active
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN111085707A (en) * | 2020-01-02 | 2020-05-01 | 青岛四方庞巴迪铁路运输设备有限公司 | Auxiliary tooling and method for drilling and riveting of underframe side beams and castings |
| CN111085707B (en) * | 2020-01-02 | 2025-02-21 | 青岛四方阿尔斯通铁路运输设备有限公司 | Auxiliary tooling and method for drilling and riveting chassis side beams and castings |
| CN116689822A (en) * | 2023-07-20 | 2023-09-05 | 中车青岛四方机车车辆股份有限公司 | Drilling auxiliary device and method for rail transit vehicle |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN107856688B (en) | Delay the lightweight Subway Body of structure with novel pillow pulling | |
| CN111085707B (en) | Auxiliary tooling and method for drilling and riveting chassis side beams and castings | |
| CN201500869U (en) | Welding and Clamping Equipment for Longitudinal Beam of Locomotive Underframe | |
| CN101774100A (en) | Adjustable position welding device of space truss structure | |
| CN110405399A (en) | A general welding tool for the roof frame of a passenger car | |
| CN106799554B (en) | A special welding fixture system for gas spring type full load frame assembly | |
| CN112355539A (en) | Assembling tool and assembling and welding system for bogie frame | |
| CN105562993B (en) | A kind of coach compartment door skeleton weld jig | |
| CN210615590U (en) | New forms of energy car battery box bottom plate stir welding anchor clamps | |
| CN202033015U (en) | Flexible support for three-coordinate measuring of body in white | |
| CN206445414U (en) | A kind of metal plate weld jig | |
| WO2025246103A1 (en) | Apparatus and method for producing high-speed maglev train body | |
| CN206231401U (en) | A kind of chassis of rail vehicle equipment suspension arrangement and chassis apparatus mounting structure | |
| CN210703298U (en) | General frock of passenger train top cap skeleton welding | |
| CN111702481A (en) | Traction beam assembly device and assembly method | |
| CN202317535U (en) | Electric locomotive roof assembly welding fixture | |
| CN116586876B (en) | A steel structure three-dimensional benchmark working platform | |
| CN212240826U (en) | Motor car switching mechanism equipment frock | |
| CN207464571U (en) | Side wall automatic welding tooling | |
| CN107030369A (en) | A kind of large-sized aluminium alloy flat board agitating friction welding clamp | |
| CN216178007U (en) | Universal type B-type urban railway vehicle bogie frame welding auxiliary tool | |
| CN214444202U (en) | Integrated modular welding tool for rail car power system mounting seat | |
| CN214868329U (en) | A welding tool for motor suspension mounting plate | |
| CN212722083U (en) | Load test tool for car lifting jack | |
| CN110732851B (en) | Manufacturing method of body structure of sleeper beam-free metro vehicle |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address |
Address after: No.86, Jinhong East Road, Chengyang District, Qingdao City, Shandong Province Patentee after: Qingdao Sifang Alstom railway transportation equipment Co.,Ltd. Address before: No.86, Jinhong East Road, Chengyang District, Qingdao City, Shandong Province 266111 Patentee before: BOMBARDIER SIFANG (QINGDAO) TRANSPORTATION Ltd. |
|
| CP03 | Change of name, title or address |