CN211520861U - A transfer device for the corner of an assembly line and an assembly line for circulating transfer of a material tray - Google Patents
A transfer device for the corner of an assembly line and an assembly line for circulating transfer of a material tray Download PDFInfo
- Publication number
- CN211520861U CN211520861U CN201922095569.1U CN201922095569U CN211520861U CN 211520861 U CN211520861 U CN 211520861U CN 201922095569 U CN201922095569 U CN 201922095569U CN 211520861 U CN211520861 U CN 211520861U
- Authority
- CN
- China
- Prior art keywords
- conveying
- assembly
- assembly line
- channel
- tray
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Automatic Assembly (AREA)
Abstract
本实用新型提供了一种流水线转角的转运装置和一种料盘循环转运的流水线,涉及物料转运技术领域。其中,这种流水线转角的转运装置包含:机架;输送机构,其包括配置于机架且连接于第一流水线的第一输送组件,第一输送组件用以沿着第一流水线的方向输送料盘,第一输送组件设置有上下贯穿第一输送组件的至少两个缺口;换向机构,其包括设置于第一输送组件下方且能够同时自至少两个缺口伸出的第二输送组件,第二输送组件能够连接于第二流水线且沿着第二流水线的方向输送料盘。这种料盘循环转运的流水线,至少包含用以输送料盘的第一输送装置和第二输送装置,以及连接于所述第一输送装置和所述第二输送装置且用以转运料盘的转运装置。
The utility model provides a transfer device for the corner of an assembly line and an assembly line for circulating transfer of a material tray, which relates to the technical field of material transfer. Wherein, the transfer device for the corner of the assembly line includes: a rack; a conveying mechanism, which includes a first conveying assembly disposed on the rack and connected to the first assembly line, and the first conveying assembly is used for conveying materials along the direction of the first assembly line The tray, the first conveying assembly is provided with at least two notches that penetrate the first conveying assembly up and down; the reversing mechanism includes a second conveying assembly disposed below the first conveying assembly and capable of extending from the at least two notches at the same time, the first conveying assembly The two conveying assemblies can be connected to the second assembly line and convey the trays along the direction of the second assembly line. This kind of pipeline for cyclic transfer of material trays at least includes a first conveying device and a second conveying device for conveying the material trays, and a conveyor connected to the first conveying device and the second conveying device and used for transferring the material trays transfer device.
Description
技术领域technical field
本实用新型涉及物料转运领域,具体而言,涉及一种流水线转角的转运装置和一种料盘循环转运的流水线。The utility model relates to the field of material transfer, in particular to a transfer device for the corner of an assembly line and an assembly line for circulating transfer of material trays.
背景技术Background technique
目前车间内部的物料转运均是通过人工摆放、拖运,不仅成本高昂而且效率低下。自动化的物料转运流水线,物料通常是放置在料盘上面通过流水线运输,但是流水线没办法直角转弯,导致流水线往往需要很大的圆弧才能实现料盘的转弯,对空间造成了极大的浪费,且流水线往往是单向流转的,料盘仍然需要人工从流水线的尾部拿到头部,造成了生产线的效率低下。有鉴于此,发明人在研究了现有的技术后特提出本申请。At present, the material transfer in the workshop is manually placed and hauled, which is not only expensive but also inefficient. In the automatic material transfer line, the material is usually placed on the tray and transported through the assembly line, but the assembly line cannot turn at right angles, so the assembly line often needs a large arc to realize the turning of the tray, which causes a great waste of space. In addition, the assembly line is often unidirectional, and the material tray still needs to be manually taken from the tail of the assembly line to the head, resulting in low efficiency of the production line. In view of this, the inventor hereby proposes the present application after studying the prior art.
实用新型内容Utility model content
本实用新型提供了一种流水线转角的转运装置和一种料盘循环转运的流水线,旨在改善流水线的料盘不能直角换向的问题。The utility model provides a transfer device for the rotation angle of an assembly line and an assembly line for circulating transfer of material trays, aiming at improving the problem that the material trays of the assembly line cannot be reversed at right angles.
为解决上述技术问题,本实用新型提供了一种流水线转角的转运装置,其用以连接相交的第一流水线和第二流水线并输送来自第一流水线和第二流水线上的料盘,该转运装置包含:In order to solve the above-mentioned technical problems, the utility model provides a transfer device for the corner of an assembly line, which is used to connect the intersecting first assembly line and the second assembly line and transport the material tray from the first assembly line and the second assembly line. Include:
机架;frame;
输送机构,其包括配置于所述机架且连接于所述第一流水线的第一输送组件,所述第一输送组件用以沿着所述第一流水线的方向输送料盘,所述第一输送组件设置有上下贯穿所述第一输送组件的至少两个缺口;a conveying mechanism, which includes a first conveying component disposed on the frame and connected to the first assembly line, the first conveying assembly is used for conveying the trays along the direction of the first assembly line, the first conveying component The conveying assembly is provided with at least two notches penetrating the first conveying assembly up and down;
换向机构,其包括设置于所述第一输送组件下方且能够同时自至少两个所述缺口伸出的第二输送组件,所述第二输送组件能够连接于所述第二流水线且沿着所述第二流水线的方向输送料盘;A reversing mechanism, which includes a second conveying assembly disposed below the first conveying assembly and capable of protruding from at least two of the notches at the same time, the second conveying assembly being capable of being connected to the second assembly line and extending along the the direction conveying tray of the second assembly line;
料盘能够被所述第一流水线输送到所述第一输送组件上方,所述第二输送组件能够自所述缺口伸出以支撑料盘并连接于所述第二流水线,以将料盘输送给所述第二流水线;所述第二输送组件能够自所述缺口伸出以连接于所述第二流水线,料盘能够被所述第二流水线输送到所述第二输送组件上方,所述第二输送组件能够自所述缺口缩回,以使料盘支撑于所述第一输送组件上方,所述第一输送组件能够将料盘输送至所述第一流水线。The tray can be conveyed by the first assembly line above the first conveying assembly, and the second conveying assembly can protrude from the gap to support the tray and be connected to the second assembly line to convey the tray to the second assembly line; the second conveying assembly can be protruded from the gap to be connected to the second assembly line, the material tray can be conveyed by the second assembly line above the second conveying assembly, the The second conveying assembly is retractable from the indentation to support the tray above the first conveying assembly capable of conveying the tray to the first assembly line.
作为进一步优化,所述第一输送组件包括平行配置于所述机架的多根支撑辊,所述输送机构还包括用以驱动多根所述支撑辊同向转动的第一驱动组件,所述缺口为相邻两根支撑辊之间的空隙。As a further optimization, the first conveying assembly includes a plurality of supporting rollers arranged in parallel with the frame, and the conveying mechanism further includes a first driving assembly for driving the plurality of supporting rollers to rotate in the same direction. The gap is the gap between two adjacent support rollers.
作为进一步优化,所述换向机构还包括用以驱动所述第二输送组件上下活动的第二驱动组件,所述第二驱动组件包括配置于所述机架的第二安装座,所述第二输送组件包括可活动的配置于所述第二安装座的第一安装座。As a further optimization, the reversing mechanism further includes a second drive assembly for driving the second conveying assembly to move up and down, the second drive assembly includes a second mounting seat disposed on the frame, the first The second conveying assembly includes a first mounting seat movably disposed on the second mounting seat.
作为进一步优化,所述第二安装座呈板状,且设置有向上延伸的至少两个支撑部;所述第二输送组件还包括分别配置于所述支撑部的至少两个支撑件,以及用以驱动所述支撑件在所述支撑部滑动的第一驱动件。As a further optimization, the second mounting seat is in the shape of a plate, and is provided with at least two supporting parts extending upward; the second conveying assembly further includes at least two supporting parts respectively disposed on the supporting parts, and a A first driving member for driving the supporting member to slide on the supporting portion.
作为进一步优化,所述第二驱动组件还包括配置于所述第二安装座且顶接于所述第一安装座的凸轮,以及用以驱动所述凸轮旋转以带动所述第一安装座上下活动的第二驱动件。As a further optimization, the second driving assembly further includes a cam disposed on the second mounting seat and abutting against the first mounting seat, and used to drive the cam to rotate to drive the first mounting seat up and down Active second drive.
本申请另提供一种料盘循环转运的流水线,用以输送能够放置产品的料盘,该流水线至少包含用以输送料盘的第一输送装置和第二输送装置,以及连接于所述第一输送装置和所述第二输送装置且用以转运料盘的转运装置;所述转运装置为上述任一实施例所述的转运装置。The present application further provides an assembly line for cyclic transfer of trays for conveying trays capable of placing products. The assembly line at least includes a first conveying device and a second conveying device for conveying trays, and a first conveying device connected to the first conveying device. The conveying device and the second conveying device are used for conveying the pallet; the conveying device is the conveying device described in any one of the above embodiments.
作为进一步优化,所述第一输送装置,设置有用以输送料盘的第一输送通道和第二输送通道;As a further optimization, the first conveying device is provided with a first conveying channel and a second conveying channel for conveying the tray;
该流水线还包含连接装置,所述连接装置包括可切换的连接于所述第一输送通道和所述第二输送通道的第三输送组件,以及用以驱动所述第三输送组件移动的第三驱动组件;所述第三输送组件能够驱动料盘移动;The assembly line also includes a connecting device, the connecting device includes a third conveying assembly switchably connected to the first conveying channel and the second conveying channel, and a third conveying assembly for driving the movement of the third conveying assembly. a driving component; the third conveying component can drive the material tray to move;
所述第三驱动组件能够驱动所述第三输送组件移动,以切换连接于所述第一输送通道和所述第二输送通道,所述第二输送通道能够输送料盘至所述第三输送组件;所述第三输送组件能够驱动料盘至所述第一输送通道。The third driving assembly can drive the third conveying assembly to move, so as to switch and connect to the first conveying channel and the second conveying channel, and the second conveying channel can convey the tray to the third conveying assembly; the third conveying assembly can drive the tray to the first conveying channel.
作为进一步优化,所述第二输送装置,设置有用以输送料盘的第三输送通道和第四输送通道;As a further optimization, the second conveying device is provided with a third conveying channel and a fourth conveying channel for conveying the tray;
所述第一输送通道和所述第二输送通道上下设置,所述第三输送通道和所述第四输送通道上下设置,且所述第一输送通道和所述第二输送通道所在的平面垂直于所述第三输送通道和所述第四输送通道所在的平面;The first conveying passage and the second conveying passage are arranged up and down, the third conveying passage and the fourth conveying passage are arranged up and down, and the planes where the first conveying passage and the second conveying passage are located are vertical in the plane where the third conveying channel and the fourth conveying channel are located;
该流水线还包含升降装置,所述转运装置配置于所述升降装置;The assembly line also includes a lifting device, and the transfer device is configured on the lifting device;
所述升降装置能够驱动所述转运装置上下移动,以使所述转运装置连接于所述第一输送通道、所述第二输送通道、所述第三输送通道,以及所述第四输送通道中的任一个。The lifting device can drive the transfer device to move up and down, so that the transfer device is connected to the first conveying passage, the second conveying passage, the third conveying passage, and the fourth conveying passage. any of the .
作为另一种优化,所述第二输送装置,设置有用以输送料盘的第三输送通道和第四输送通道;该流水线包含一对所述转运装置,一对转运装置分别连接于所述第一输送通道和所述第三输送通道,以及所述第四输送通道和所述第二输送通道。As another optimization, the second conveying device is provided with a third conveying channel and a fourth conveying channel for conveying the material tray; the assembly line includes a pair of the conveying devices, and a pair of conveying devices are respectively connected to the first conveying device. A delivery channel and the third delivery channel, and the fourth delivery channel and the second delivery channel.
作为进一步优化,所述流水线还包含码垛装置,其用以将生产装置生产的产品摆放于料盘;所述码垛装置为3轴机械手。As a further optimization, the assembly line also includes a palletizing device, which is used to place the products produced by the production device on the tray; the palletizing device is a 3-axis manipulator.
通过采用上述技术方案,本实用新型可以取得以下技术效果:该转运装置能够实现料盘在第一流水线和第二流水线之间的切换输送,并且在不执行换向操作时,能够保证第一流水线的输送。具体地,第一流水线与第二流水线相交,第一输送组件连接于第一流水线并沿着第一流水线的方向输送料盘。第二输送组件自第一输送组件的缺口向上伸出后连接于第二流水线,并用以将第一流水线上的料盘输送至第二流水线,或者将第二流水线上的料盘输送到第一流水线。第二输送组件位于第一输送组件的下面时,第一输送组件的输送平面与第一流水线的输送平面平齐,能够保证第一流水线上的料盘不断的沿着第一流水线的方向输送,当有来自第二流水线的料盘要转移到第一流水线时,或者有来自第一流水线的料盘要转移到第二流水线时,第二输送组件向上移动,以自第一输送组件的缺口伸出,并支撑在料盘上,完成料盘在两条流水线上的切换动作。具有很好的实际意义。By adopting the above technical solution, the present invention can achieve the following technical effects: the transfer device can realize the switching and conveying of the material tray between the first assembly line and the second assembly line, and when the reversing operation is not performed, the first assembly line can be guaranteed delivery. Specifically, the first assembly line intersects with the second assembly line, and the first conveying assembly is connected to the first assembly line and conveys the trays along the direction of the first assembly line. The second conveying assembly protrudes upward from the notch of the first conveying assembly and is connected to the second assembly line, and is used for conveying the trays on the first assembly line to the second assembly line, or conveying the trays on the second assembly line to the first assembly line assembly line. When the second conveying assembly is located below the first conveying assembly, the conveying plane of the first conveying assembly is flush with the conveying plane of the first assembly line, which can ensure that the trays on the first assembly line are continuously conveyed along the direction of the first assembly line. When there are trays from the second assembly line to be transferred to the first assembly line, or when there are trays from the first assembly line to be transferred to the second assembly line, the second conveying assembly moves upward to extend from the notch of the first conveying assembly out, and supported on the tray to complete the switching action of the tray on the two assembly lines. has good practical significance.
本实用新型的转运装置,不仅能够实现在第一流水线和第二流水线之间的切换输送,并且在不执行换向操作时,能够保证第一流水线的持续输送,以保证装置的工作效率,具有很好的实际意义。The transfer device of the utility model can not only realize the switching and conveying between the first assembly line and the second assembly line, but also ensure the continuous conveying of the first assembly line when the reversing operation is not performed, so as to ensure the working efficiency of the device, and has the advantages of Good practical sense.
另外,本案还提供了一种流水线,具体地,在流水线的转角处和/或输送通道的相交处设置有上述的转运装置,使得流水线在转角处和/或输送通道的相交处的结构变得更为简单,且体积大大减小了,具有很好的实际意义。In addition, this case also provides an assembly line, specifically, the above-mentioned transfer device is provided at the corner of the assembly line and/or the intersection of the conveying channel, so that the structure of the assembly line at the corner and/or the intersection of the conveying channel becomes It is simpler, and the volume is greatly reduced, which has good practical significance.
附图说明Description of drawings
为了更清楚地说明本实用新型实施方式的技术方案,下面将对实施方式中所需要使用的附图作简单地介绍,应当理解,以下附图仅示出了本实用新型的某些实施例,因此不应被看作是对范围的限定,对于本领域普通技术人员来讲,在不付出创造性劳动的前提下,还可以根据这些附图获得其他相关的附图。In order to illustrate the technical solutions of the embodiments of the present invention more clearly, the accompanying drawings required in the embodiments will be briefly introduced below. It should be understood that the following drawings only show some embodiments of the present invention. Therefore, it should not be regarded as a limitation of the scope. For those of ordinary skill in the art, other related drawings can also be obtained from these drawings without any creative effort.
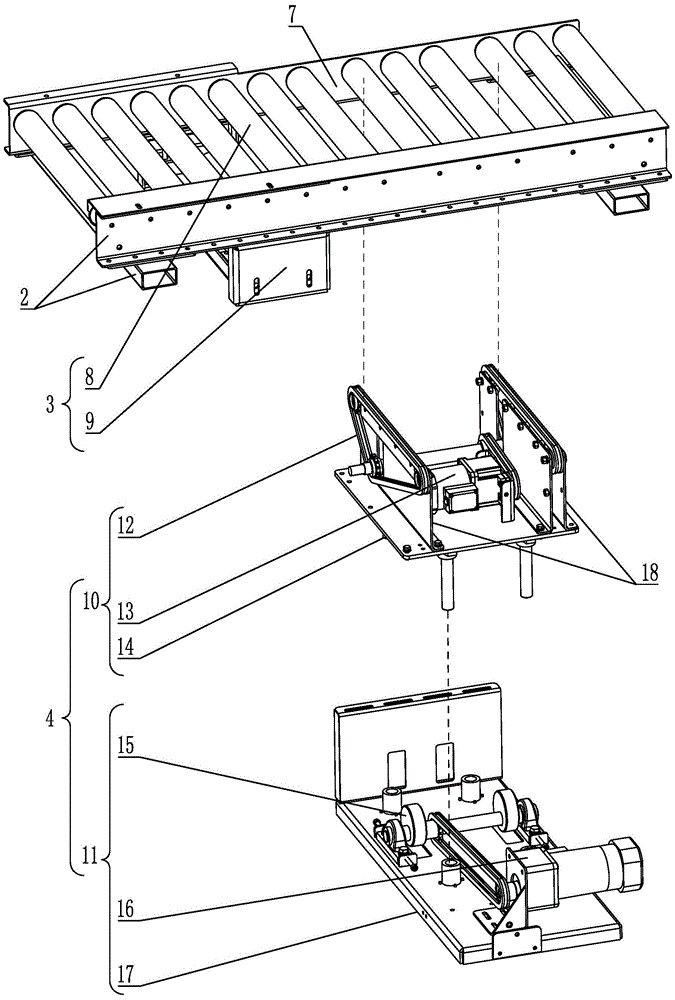
图1是本实用新型第一实施例,转运装置的轴测图;Fig. 1 is the first embodiment of the present utility model, the axonometric view of the transfer device;
图2是本实用新型第一实施例,转运装置的第一爆炸图;Fig. 2 is the first embodiment of the present utility model, the first exploded view of the transfer device;
图3是本实用新型第一实施例,转运装置的第二爆炸图;Fig. 3 is the first embodiment of the present utility model, the second exploded view of the transfer device;
图4是本实用新型第二实施例,流水线的轴测图;Fig. 4 is a second embodiment of the present utility model, an axonometric view of an assembly line;
图5是本实用新型第二实施例,流水线的爆炸图;Figure 5 is the second embodiment of the present utility model, an exploded view of the assembly line;
图6是本实用新型第二实施例,连接装置和第一输送装置的轴测图;Fig. 6 is the axonometric view of the second embodiment of the present invention, the connecting device and the first conveying device;
图7是本实用新型第二实施例,连接装置的爆炸图;Figure 7 is the second embodiment of the present utility model, an exploded view of the connecting device;
图8是本实用新型第二实施例,连接装置和第一输送装置的爆炸图;Figure 8 is the second embodiment of the present utility model, an exploded view of the connecting device and the first conveying device;
图9是本实用新型第二实施例,流水线的爆炸图(为了便于显示隐去了第二输送装置后面的装置);Figure 9 is the second embodiment of the present utility model, an exploded view of the assembly line (the device behind the second conveying device is hidden for ease of display);
图中标记:1-转运装置;2-机架;3-输送机构;4-换向机构;5-第一流水线;6-第二流水线;7-缺口;8-第一输送组件;9-第一驱动组件;10- 第二输送组件;11-第二驱动组件;12-支撑件;13-第一驱动件;14-第一安装座;15-凸轮;16-第二驱动件;17-第二安装座;18-支撑部;19-升降装置;20-码垛装置;21-第一输送装置;22-料盘;23-连接装置;24-第二输送装置;25-第一输送通道;26-第二输送通道;27-第三输送组件;28- 第三驱动组件;29-第三输送通道;30-第四输送通道;31-夹紧件;32-伸缩件。Markings in the figure: 1-transfer device; 2-frame; 3-conveying mechanism; 4-reversing mechanism; 5-first assembly line; 6-second assembly line; 7-notch; 8-first conveying assembly; 9- 10-second conveying assembly; 11-second driving assembly; 12-supporting member; 13-first driving member; 14-first mounting seat; 15-cam; 16-second driving member;17 -Second mounting seat; 18-Support; 19-Lifting device; 20-Palletizing device; 21-First conveying device; 22-Pallet; 23-Connecting device; conveying channel; 26-second conveying channel; 27-third conveying component; 28-third driving component; 29-third conveying channel; 30-fourth conveying channel; 31-clamping piece; 32- telescopic piece.
具体实施方式Detailed ways
为使本实用新型实施方式的目的、技术方案和优点更加清楚,下面将结合本实用新型实施方式中的附图,对本实用新型实施方式中的技术方案进行清楚、完整地描述,显然,所描述的实施方式是本实用新型一部分实施方式,而不是全部的实施方式。基于本实用新型中的实施方式,本领域普通技术人员在没有作出创造性劳动前提下所获得的所有其他实施方式,都属于本实用新型保护的范围。因此,以下对在附图中提供的本实用新型的实施方式的详细描述并非旨在限制要求保护的本实用新型的范围,而是仅仅表示本实用新型的选定实施方式。基于本实用新型中的实施方式,本领域普通技术人员在没有作出创造性劳动前提下所获得的所有其他实施方式,都属于本实用新型保护的范围。In order to make the purposes, technical solutions and advantages of the embodiments of the present invention more clear, the technical solutions in the embodiments of the present invention will be clearly and completely described below with reference to the accompanying drawings in the embodiments of the present invention. Obviously, the described The embodiments of the present invention are a part of the embodiments of the present invention, but not all of the embodiments. Based on the embodiments of the present invention, all other embodiments obtained by those of ordinary skill in the art without creative work fall within the protection scope of the present invention. Accordingly, the following detailed description of the embodiments of the invention provided in the accompanying drawings is not intended to limit the scope of the invention as claimed, but is merely representative of selected embodiments of the invention. Based on the embodiments of the present invention, all other embodiments obtained by those of ordinary skill in the art without creative work fall within the protection scope of the present invention.
在本实用新型的描述中,需要理解的是,术语“中心”、“纵向”、“横向”、“长度”、“宽度”、“厚度”、“上”、“下”、“前”、“后”、“左”、“右”、“竖直”、“水平”、“顶”、“底”、“内”、“外”、“顺时针”、“逆时针”等指示的方位或位置关系为基于附图所示的方位或位置关系,仅是为了便于描述本实用新型和简化描述,而不是指示或暗示所指的设备或元件必须具有特定的方位、以特定的方位构造和操作,因此不能理解为对本实用新型的限制。In the description of the present invention, it should be understood that the terms "center", "longitudinal", "lateral", "length", "width", "thickness", "upper", "lower", "front", "Back", "Left", "Right", "Vertical", "Horizontal", "Top", "Bottom", "Inner", "Outer", "Clockwise", "Counterclockwise" etc. Or the positional relationship is based on the orientation or positional relationship shown in the accompanying drawings, which is only for the convenience of describing the present invention and simplifying the description, rather than indicating or implying that the referred device or element must have a specific orientation, be constructed in a specific orientation and operation, so it cannot be construed as a limitation to the present invention.
此外,术语“第一”、“第二”仅用于描述目的,而不能理解为指示或暗示相对重要性或者隐含指明所指示的技术特征的数量。由此,限定有“第一”、“第二”的特征可以明示或者隐含地包括一个或者更多个该特征。在本实用新型的描述中,“多个”的含义是两个或两个以上,除非另有明确具体的限定。In addition, the terms "first" and "second" are only used for descriptive purposes, and should not be construed as indicating or implying relative importance or implying the number of indicated technical features. Thus, a feature defined as "first" or "second" may expressly or implicitly include one or more of that feature. In the description of the present invention, "plurality" means two or more, unless otherwise expressly and specifically defined.
在本实用新型中,除非另有明确的规定和限定,术语“安装”、“相连”、“连接”、“固定”等术语应做广义理解,例如,可以是固定连接,也可以是可拆卸连接,或成一体;可以是机械连接,也可以是电连接;可以是直接相连,也可以通过中间媒介间接相连,可以是两个元件内部的连通或两个元件的相互作用关系。对于本领域的普通技术人员而言,可以根据具体情况理解上述术语在本实用新型中的具体含义。In the present utility model, unless otherwise expressly specified and limited, the terms "installation", "connection", "connection", "fixed" and other terms should be understood in a broad sense, for example, it may be a fixed connection or a detachable connection Connection, or integration; it can be a mechanical connection or an electrical connection; it can be a direct connection or an indirect connection through an intermediate medium, and it can be the internal communication between the two elements or the interaction relationship between the two elements. For those of ordinary skill in the art, the specific meanings of the above terms in the present invention can be understood according to specific situations.
在本实用新型中,除非另有明确的规定和限定,第一特征在第二特征之“上”或之“下”可以包括第一和第二特征直接接触,也可以包括第一和第二特征不是直接接触而是通过它们之间的另外的特征接触。而且,第一特征在第二特征“之上”、“上方”和“上面”包括第一特征在第二特征正上方和斜上方,或仅仅表示第一特征水平高度高于第二特征。第一特征在第二特征“之下”、“下方”和“下面”包括第一特征在第二特征正下方和斜下方,或仅仅表示第一特征水平高度小于第二特征。In the present invention, unless otherwise expressly specified and limited, a first feature "on" or "under" a second feature may include the first and second features in direct contact, or may include the first and second features The features are not in direct contact but through additional features between them. Also, the first feature being "above", "over" and "above" the second feature includes the first feature being directly above and obliquely above the second feature, or simply means that the first feature is level higher than the second feature. The first feature is "below", "below" and "below" the second feature includes the first feature being directly below and diagonally below the second feature, or simply means that the first feature has a lower level than the second feature.
下面结合附图与具体实施方式对本实用新型作进一步详细描述:Below in conjunction with the accompanying drawings and specific embodiments, the present utility model is described in further detail:
本申请提供一种流水线转角的转运装置The application provides a transfer device for the corner of an assembly line
由图1至图3所示,在本实施例中,一种流水线转角的转运装置,其用以连接相交的第一流水线5和第二流水线6并输送来自第一流水线5和第二流水线6上的料盘22,该转运装置1包含:As shown in FIG. 1 to FIG. 3 , in this embodiment, a transfer device for a corner of an assembly line is used to connect the intersecting
机架2;
输送机构3,其包括配置于机架2且连接于第一流水线5的第一输送组件8,第一输送组件8用以沿着第一流水线5的方向输送料盘22,第一输送组件8设置有上下贯穿第一输送组件8的至少两个缺口7;The conveying
换向机构4,其包括设置于第一输送组件8下方且能够同时自至少两个缺口7伸出的第二输送组件10,第二输送组件10能够连接于第二流水线6 且沿着第二流水线6的方向输送料盘22;The reversing
料盘22能够被第一流水线5输送到第一输送组件8上方,第二输送组件10能够自缺口7伸出以支撑料盘22并连接于第二流水线6,以将料盘 22输送给第二流水线6;第二输送组件10能够自缺口7伸出以连接于第二流水线6,料盘22能够被第二流水线6输送到第二输送组件10上方,第二输送组件10能够自缺口7缩回,以使料盘22支撑于第一输送组件8上方,第一输送组件8能够将料盘22输送至第一流水线5。具体地,第一流水线 5与第二流水线6相交,第一输送组件8连接于第一流水线5并沿着第一流水线5的方向输送料盘22。第二输送组件10自第一输送组件8的缺口7向上伸出后连接于第二流水线6,并用以将第一流水线5上的料盘22输送至第二流水线6,或者将第二流水线6上的料盘22输送到第一流水线5。第二输送组件10位于第一输送组件8的下面时,第一输送组件8的输送平面与第一流水线5的输送平面平齐,能够保证第一流水线5上的料盘22不断的沿着第一流水线5的方向输送,当有来自第二流水线6的料盘22要转移到第一流水线5时,或者有来自第一流水线5的料盘22要转移到第二流水线6时,第二输送组件10向上移动,以自第一输送组件8的缺口7伸出,并支撑在料盘22上,完成料盘22在两条流水线上的切换动作。该转运装置1,不仅能够实现在第一流水线5和第二流水线6之间的切换输送,并且在不执行换向操作时,能够保证第一流水线5的持续输送,以保证装置的工作效率,具有很好的实际意义。The
由图1至图3所示,在本实施例中,第一输送组件8包括平行配置于机架2的多根支撑辊,输送机构3还包括用以驱动多根支撑辊同向转动的第一驱动组件9,缺口7为相邻两根支撑辊之间的空隙。具体地,第一输送组件8包括平行配置于机架2的多根支撑辊,其中某两根相邻的支撑辊之间的间距较大,并形成平行于支撑辊且上下贯穿第一输送组件8的条状的缺口7。第一流水线5和第二流水线6呈“十”、“T”、“L”形的任一种连接方式,且第一流水线5也为多根平行的支撑棒,该支撑棒与支撑辊平行且相邻的设置在一起,以使第一流水线5连接于第一输送组件8。第二驱动组件11能够沿着缺口7的方向,即沿着支撑辊的轴向输送料盘22。在另一实施例中,第一流水线5和第二流水线6相交的夹角呈锐角或者钝角。第一支撑组件平行设置的多根支撑辊之间的长度不一致,沿着第一流水线5 的输送方向支撑辊的长度依次变短,以形成相对于支撑辊的轴线倾斜的上下贯穿第一输送组件8的条状的开口,该条状开口沿着第二流水线6的方向伸展。第二驱动组件11能够沿着缺口7的方向即第二流水线6的输送方向输送料盘22。相邻的两根支撑辊之间通过齿轮、链条传动在一起,第一驱动组件9为电机,并传动连接于支撑辊,以驱动支撑辊转动。As shown in FIG. 1 to FIG. 3, in this embodiment, the first conveying assembly 8 includes a plurality of support rollers arranged in parallel with the
由图1至图3所示,在本实施例中,换向机构4还包括用以驱动第二输送组件10上下活动的第二驱动组件11,第二驱动组件11包括配置于机架2的第二安装座17,第二输送组件10包括可活动的配置于第二安装座 17的第一安装座14。具体地,第二输送组件10需要同时从至少两个缺口7 伸出才能平稳的支撑住料盘22,因此第二输送组件10设置有可活动的第一安装座14,保证配置于第一安装座14的所有零部件同步运动,并保证同时伸出至少两个缺口7并平稳的支撑料盘22,具有很好的实际意义。As shown in FIGS. 1 to 3 , in this embodiment, the reversing
由图1至图3所示,在本实施例中,第二安装座17呈板状,且设置有向上延伸的至少两个支撑部18;第二输送组件10还包括分别配置于支撑部18的至少两个支撑件12,以及用以驱动支撑件12在支撑部18滑动的第一驱动件13。具体地,该支撑件12为皮带,支撑部18为配置在第二安装座 17的底板且向上延伸的筋板,该筋板上配置有两个可转动的旋转件,支撑件12配置于旋转件上且能够沿着支撑件12的轴线运动。在本实施例中该皮带为齿轮皮带,该旋转件为齿轮,在另一实施例中该支撑件12为普通皮带,该旋转件为皮带轮。第一驱动件13为电机,传动连接于支撑件12,用以带动支撑件12运动。As shown in FIG. 1 to FIG. 3 , in this embodiment, the second mounting
由图1至图3所示,在本实施例中,第二驱动组件11还包括配置于第二安装座17且顶接于第一安装座14的凸轮15,以及用以驱动凸轮15旋转以带动第一安装座14上下活动的第二驱动件16。具体地,第一安装座14 通过导套、导杆,可上下活动的配置在第二安装座17上,第二安装座17 上设置有顶接在第一安装座14下方的凸轮15,且设置有驱动凸轮15转动的第二驱动件16,该第二驱动件16为电机,并且通过减速器、齿轮、链条等常用传动连接手段传动连接于凸轮15,能够很好的保证凸轮15的主动,以保证第二输送组件10上下移动得到很好的驱动。As shown in FIGS. 1 to 3 , in this embodiment, the second driving assembly 11 further includes a
本申请另提供一种料盘循环转运的流水线:The present application further provides an assembly line for cyclic transfer of trays:
由图4、图5所示,在本实施例中,一种料盘循环转运的流水线,用以输送能够放置产品的料盘22,该流水线至少包含用以输送料盘22的第一输送装置21和第二输送装置24,以及连接于第一输送装置21和第二输送装置24且用以转运料盘22的转运装置1;转运装置1为上述任一实施例所述的转运装置1。具体地,第一输送装置21与第二输送装置24相交。并且在相交处设置有上述任一段所述的转运装置1。该转运装置1不仅能够使第一输送装置21和第二输送装置24上的料盘22在两个输送装置之间进行移动,还能够使料盘22持续的在第一输送装置21和第二输送装置24上持续的输送。在流水线的转角处和/或输送通道的相交处设置有上述任一段所述的转运装置1,使得流水线在转角处和/或输送通道的相交处的结构变得更为简单,且体积大大减小了,具有很好的实际意义。As shown in FIG. 4 and FIG. 5 , in this embodiment, an assembly line for cyclic transfer of trays is used to transport
由图6、图8、图9所示,在本实施例中,第一输送装置21,设置有用以输送料盘22的第一输送通道25和第二输送通道26;As shown in FIG. 6 , FIG. 8 and FIG. 9 , in this embodiment, the first conveying
该流水线还包含连接装置23,连接装置23包括可切换的连接于第一输送通道25和第二输送通道26的第三输送组件27,以及用以驱动第三输送组件27移动的第三驱动组件28;第三输送组件27能够驱动料盘22移动;The assembly line also includes a connecting
第三驱动组件28能够驱动第三输送组件27移动,以切换连接于第一输送通道25和第二输送通道26,第二输送通道26能够输送料盘22至第三输送组件27;第三输送组件27能够驱动料盘22至第一输送通道25。具体地,第一输送通道25与第二输送通道26的输送方向相反,以保证料盘22 通过连接装置23能够在第一输送装置21上持续不断来回输送,使设备不需要人工便能持续不断的运行,具有很好的实际意义。第一输送通道25和第二输送通道26平行设置,第三输送组件27只需平移即可切换的连接于第二输送通道26和第三输送通道29。第三驱动组件28包括架子,配置于第三输送组件27和架子的导向件,以及用以驱动第三输送组件27移动的伸缩件32,该导向件为导杆、导套,该伸缩件32为气缸或油缸。The
由图9所示,在本实施例中,第二输送装置24,设置有用以输送料盘 22的第三输送通道29和第四输送通道30;As shown in FIG. 9 , in this embodiment, the second conveying
第一输送通道25和第二输送通道26上下设置,第三输送通道29和第四输送通道30上下设置,且第一输送通道25和第二输送通道26所在的平面垂直于第三输送通道29和第四输送通道30所在的平面;The first conveying passage 25 and the second conveying passage 26 are arranged up and down, the third conveying passage 29 and the fourth conveying passage 30 are arranged up and down, and the plane where the first conveying passage 25 and the second conveying passage 26 are located is perpendicular to the third conveying passage 29 and the plane where the fourth conveying channel 30 is located;
该流水线还包含升降装置19,转运装置1配置于升降装置19;The assembly line also includes a
升降装置19能够驱动转运装置1上下移动,以使转运装置1连接于第一输送通道25、第二输送通道26、第三输送通道29,以及第四输送通道 30中的任一个。具体地,由于现场需要,第一输送装置21和第二输送装置 24之间可能存在这高度差以及转角,因此在第一输送装置21和第二输送装置24相交的地方设置有上述任一段所述的转运装置1,并且设置有用以支撑该转运装置1的升降装置19,以使该转运装置1能够切换连接于第一输送通道25、第二输送通道26、第三输送通道29,以及第四输送通道30中的任一个,即大大节约了流水线转角处的体积,还能够保证料盘22在第一输送装置21和第二输送装置24之间流转,且不需要人工,具有很好的实际意义。在另一实施例中第一输送装置21和第二输送装置24没有高度差,第二输送装置24,设置有用以输送料盘22的第三输送通道29和第四输送通道30,第一输送通道25与第三输送通道29在同一水平面,第二输送通道26与第四输送通道30在同一水平面,第一输送通道25与第三输送通道29通过一个转运装置1连接,第二输送通道26与第四输送通道30 通过另一个转运装置1连接。The lifting
由图5所示,在本实施例中,第二输送装置24后面还连接有第三输送装置,第三输送装置设置有上下两层输送通道,且第三输送装置与第二输送装置24之间没有高度差,第三输送通道29通过一个转运装置1连接于第三输送装置的上层输送通道,第四输送通道30通过另一个转运装置1连接于第三输送装置的下层输送通道。As shown in FIG. 5 , in this embodiment, a third conveying device is also connected behind the second conveying
由图8、图9所示,在本实施例中,该流水线还包含码垛装置20,其用以将生产装置生产的产品摆放于料盘22;码垛装置20为3轴机械手。具体地,第三输送组件27将来自第二输送通道26的料盘22转移到第一输送通道25,码垛机构将生产装置生产出来的产品规则的摆放在该料盘22上,并由第一输送通道25通过转运装置1输送给第三输送通道29,最终输送到加工装置,并将产品从料盘22上取下,并将料盘22输送到第四输送通道 30,通过转运装置1输送回第二输送通道26,料盘22完成一个循环后继续下一个循环。As shown in FIG. 8 and FIG. 9 , in this embodiment, the assembly line further includes a
由图7所示,在本实施例中,连接装置23还包括可活动的配置于第三输送组件27的一对夹紧件31,以及用以驱动一对夹紧件31同时向第三输送组件27中间移动的伸缩件32,料盘22自第二输送通道26输送到第三输送组件27上后,伸缩件32驱动夹紧件31推动料盘22,以使料盘22移动到第三输送组件27的中心位置,完成料盘22的定位。As shown in FIG. 7 , in this embodiment, the connecting
以上所述仅为本实用新型的优选实施方式而已,并不用于限制本实用新型,对于本领域的技术人员来说,本实用新型可以有各种更改和变化。凡在本实用新型的精神和原则之内,所作的任何修改、等同替换、改进等,均应包含在本实用新型的保护范围之内。The above descriptions are only preferred embodiments of the present invention, and are not intended to limit the present invention. For those skilled in the art, the present invention may have various modifications and changes. Any modification, equivalent replacement, improvement, etc. made within the spirit and principle of the present invention shall be included in the protection scope of the present invention.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922095569.1U CN211520861U (en) | 2019-11-28 | 2019-11-28 | A transfer device for the corner of an assembly line and an assembly line for circulating transfer of a material tray |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922095569.1U CN211520861U (en) | 2019-11-28 | 2019-11-28 | A transfer device for the corner of an assembly line and an assembly line for circulating transfer of a material tray |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211520861U true CN211520861U (en) | 2020-09-18 |
Family
ID=72444166
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201922095569.1U Expired - Fee Related CN211520861U (en) | 2019-11-28 | 2019-11-28 | A transfer device for the corner of an assembly line and an assembly line for circulating transfer of a material tray |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211520861U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112896914A (en) * | 2021-01-06 | 2021-06-04 | 山东九龙新材料有限公司 | Transfer chain is used in anhydrous stemming refractory material production for blast furnace |
| CN114751120A (en) * | 2021-12-03 | 2022-07-15 | 上海同健远大环保机械工程有限公司 | Device and method for improving work efficiency of empty and solid barrel replacement of garbage barrel transfer trolley |
| CN118220796A (en) * | 2023-11-02 | 2024-06-21 | 湖南智能运护科技有限公司 | Conveying device and conveying system |
| CN119218696A (en) * | 2024-11-28 | 2024-12-31 | 大连美德乐工业自动化股份有限公司 | A reversing conveying device for transmission line |
-
2019
- 2019-11-28 CN CN201922095569.1U patent/CN211520861U/en not_active Expired - Fee Related
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112896914A (en) * | 2021-01-06 | 2021-06-04 | 山东九龙新材料有限公司 | Transfer chain is used in anhydrous stemming refractory material production for blast furnace |
| CN114751120A (en) * | 2021-12-03 | 2022-07-15 | 上海同健远大环保机械工程有限公司 | Device and method for improving work efficiency of empty and solid barrel replacement of garbage barrel transfer trolley |
| CN118220796A (en) * | 2023-11-02 | 2024-06-21 | 湖南智能运护科技有限公司 | Conveying device and conveying system |
| CN118220796B (en) * | 2023-11-02 | 2026-07-03 | 湖南智能运护科技有限公司 | Conveying device and conveying system |
| CN119218696A (en) * | 2024-11-28 | 2024-12-31 | 大连美德乐工业自动化股份有限公司 | A reversing conveying device for transmission line |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| US10384887B2 (en) | Transfer device with two tensioning wheels | |
| CN110562764B (en) | Stacking devices, loaders and loading systems | |
| CN210972598U (en) | Low temperature is transported bucket and is docked module | |
| US9233441B2 (en) | Machining system | |
| CN209442095U (en) | Belt conveyor and sorting equipment | |
| CN110371609A (en) | The double-deck vertical conveyor, the double-deck sorting system and its method for sorting | |
| US8550231B2 (en) | Conveying device | |
| WO2022237051A1 (en) | Intelligent consignment machine suitable for large components and consignment method therefor | |
| CN110733872A (en) | plate steering conveying system with aligning mechanism | |
| CN210029129U (en) | Alternate transfer mechanism and alternate conveying system | |
| CN108213953A (en) | It draws case assembling equipment and draws case Automatic Assembly Line | |
| CN109867107B (en) | Conveying device | |
| CN211282786U (en) | Carrier circulating conveying device | |
| CN210943617U (en) | Steering conveying device | |
| JP6765705B2 (en) | Transfer device and transfer device | |
| KR101079229B1 (en) | Transfer direction convertible conveyor and conveyor system using the same | |
| CN218318795U (en) | Material handling mechanism and feeding device | |
| CN216763374U (en) | Double-cargo-space rotary conveyor | |
| CN116654586A (en) | Logistics conveying line capable of overturning | |
| KR20200004064A (en) | Conveyor with directional structure | |
| KR100836195B1 (en) | Goods transfer device | |
| CN211394297U (en) | bottle delivery mechanism | |
| CN209442146U (en) | Transmitting device, transmission line and sorting device | |
| CN216234340U (en) | Inclined hole processing fixing device | |
| CN220033310U (en) | Double-clamp material conveying device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20200918 |