CN211086851U - Automatic alignment crimping lighting device for liquid crystal screen - Google Patents
Automatic alignment crimping lighting device for liquid crystal screen Download PDFInfo
- Publication number
- CN211086851U CN211086851U CN201922410598.2U CN201922410598U CN211086851U CN 211086851 U CN211086851 U CN 211086851U CN 201922410598 U CN201922410598 U CN 201922410598U CN 211086851 U CN211086851 U CN 211086851U
- Authority
- CN
- China
- Prior art keywords
- assembly
- liquid crystal
- alignment
- crystal screen
- crimping
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images





Landscapes
- Devices For Indicating Variable Information By Combining Individual Elements (AREA)
- Liquid Crystal (AREA)
Abstract
本实用新型公开了一种液晶屏幕自动对位压接点灯装置,属于液晶屏幕检测技术领域。该液晶屏幕自动对位压接点灯装置,用于对液晶屏幕点灯测试,包括治具调节机构、压接机构和产品对位机构,其中,治具调节机构用于支撑液晶屏幕,且治具调节机构能根据液晶屏幕的大小进行调节;压接机构用于对液晶屏幕压接并点灯,且压接机构的位置能调节以适用于不同的液晶屏幕;产品对位机构用于将液晶屏幕定位于压接机构上。本实用新型的液晶屏幕自动对位压接点灯装置,通过治具调节机构、产品对位机构及压接机构进行尺寸调整,实现了对多种不同尺寸液晶屏幕的兼容,并实现了自动对位压接点灯,进而降低了生产成本,提高了生产效率。
The utility model discloses a liquid crystal screen automatic alignment crimping lighting device, which belongs to the technical field of liquid crystal screen detection. The liquid crystal screen automatic alignment crimp lighting device is used for the lighting test of the liquid crystal screen, and includes a fixture adjustment mechanism, a crimp mechanism and a product alignment mechanism, wherein the fixture adjustment mechanism is used to support the liquid crystal screen, and the fixture adjusts The mechanism can be adjusted according to the size of the LCD screen; the crimping mechanism is used to crimp and light the LCD screen, and the position of the crimping mechanism can be adjusted to suit different LCD screens; the product alignment mechanism is used to position the LCD screen on the on the crimping mechanism. The liquid crystal screen automatic alignment and crimping lighting device of the utility model can adjust the size through the jig adjusting mechanism, the product alignment mechanism and the crimping mechanism, so as to realize the compatibility of various liquid crystal screens of different sizes, and realize the automatic alignment. Crimp lighting, thereby reducing production costs and improving production efficiency.
Description
技术领域technical field
本实用新型涉及液晶屏幕检测技术领域,尤其涉及一种液晶屏幕自动对位压接点灯装置。The utility model relates to the technical field of liquid crystal screen detection, in particular to a liquid crystal screen automatic alignment crimping lighting device.
背景技术Background technique
随着液晶显示行业的快速发展,工厂对产品的良率要求也是越来越高。现有技术中常见的液晶屏幕压接方式有伸缩气缸压接和人工压接;对于人工压接,首先将待检测的液晶屏幕搬运到治具压接的工位,然后操作工人将翻盖压接头进行压合,手动压接治具耗时耗力,难以满足大批量生产需求,而且人工压接效果的一致性差,合格率低;对于伸缩气缸压接,检测系统的每个工位上有多个待检测的液晶屏幕,利用伸缩气缸的运动控制治具的压接,工作方式受限于设备的空间尺寸;液晶屏幕尺寸的规格变化,自动压接设备结构冗杂,人力以及设备成本日益上升。With the rapid development of the liquid crystal display industry, factories have higher and higher requirements for product yield. Common liquid crystal screen crimping methods in the prior art include telescopic cylinder crimping and manual crimping; for manual crimping, the liquid crystal screen to be tested is first transported to the crimping station of the jig, and then the operator presses the flip cover to the joint. For crimping, the manual crimping fixture is time-consuming and labor-intensive, and it is difficult to meet the needs of mass production, and the consistency of the manual crimping effect is poor, and the pass rate is low; For a liquid crystal screen to be tested, the motion control jig of the telescopic cylinder is used for crimping, and the working method is limited by the space size of the equipment; the size of the liquid crystal screen changes, the structure of the automatic crimping equipment is complicated, and the cost of manpower and equipment is increasing.
实用新型内容Utility model content
本实用新型的目的在于提供一种液晶屏幕自动对位压接点灯装置,实现对多种不同尺寸液晶屏幕的兼容,并实现自动对位压接点灯,降低生产成本,提高生产效率。The purpose of the utility model is to provide an automatic alignment and crimp lighting device for liquid crystal screens, which realizes compatibility with a variety of liquid crystal screens of different sizes, and realizes automatic alignment and crimping lighting, thereby reducing production costs and improving production efficiency.
为达此目的,本实用新型采用以下技术方案:For this purpose, the utility model adopts the following technical solutions:
一种液晶屏幕自动对位压接点灯装置,用于对液晶屏幕点灯测试,包括:A liquid crystal screen automatic alignment crimp lighting device, used for lighting test of the liquid crystal screen, including:
治具调节机构,用于支撑液晶屏幕,且治具调节机构能根据液晶屏幕的大小进行调节;The fixture adjustment mechanism is used to support the LCD screen, and the fixture adjustment mechanism can be adjusted according to the size of the LCD screen;
压接机构,用于对液晶屏幕压接并点灯,且压接机构的位置能调节以适用于不同的液晶屏幕;The crimping mechanism is used for crimping and lighting the liquid crystal screen, and the position of the crimping mechanism can be adjusted to be suitable for different liquid crystal screens;
产品对位机构,用于将液晶屏幕定位于压接机构上。The product alignment mechanism is used to position the LCD screen on the crimping mechanism.
可选地,治具调节机构包括移动治具组件、第一驱动组件和固定治具组件,第一驱动组件带动移动治具组件运动以使移动治具组件与固定治具组件的间距适合于液晶屏幕的尺寸。Optionally, the jig adjustment mechanism includes a movable jig assembly, a first drive assembly and a fixed jig assembly, and the first drive assembly drives the movable jig assembly to move so that the distance between the movable jig assembly and the fixed jig assembly is suitable for the liquid crystal. screen size.
可选地,第一驱动组件包括第一驱动件和第一传动件,移动治具组件包括透明治具,透明治具用于支撑液晶屏幕,第一传动件与透明治具连接,第一驱动组件驱动第一传动件并带动透明治具靠近或远离固定治具组件运动。Optionally, the first driving component includes a first driving component and a first transmission component, the moving fixture component includes a transparent fixture, the transparent fixture is used to support the liquid crystal screen, the first transmission component is connected with the transparent fixture, and the first driving component The assembly drives the first transmission member and drives the transparent jig to move closer to or away from the fixed jig assembly.
可选地,产品对位机构包括固定端第一对位组件、活动端第一对位组件和第二驱动组件,固定端第一对位组件与活动端第一对位组件相对设置,第二驱动组件带动活动端第一对位组件运动以使活动端第一对位组件靠近或远离固定端第一对位组件。Optionally, the product alignment mechanism includes a first alignment assembly at the fixed end, a first alignment assembly at the movable end, and a second driving assembly, the first alignment assembly at the fixed end and the first alignment assembly at the movable end are arranged opposite to each other, and the second The driving component drives the first aligning component of the movable end to move, so that the first aligning component of the movable end is close to or away from the first aligning component of the fixed end.
可选地,产品对位机构包括第一定位组件,压接机构包括与第一定位组件相对设置的第二定位组件,第一定位组件和第二定位组件用于对液晶屏幕定位。Optionally, the product alignment mechanism includes a first positioning assembly, the crimping mechanism includes a second positioning assembly disposed opposite to the first positioning assembly, and the first positioning assembly and the second positioning assembly are used for positioning the liquid crystal screen.
可选地,第一定位组件包括定位板和用于驱动定位板运动的第三对位件,定位板在靠近液晶屏幕的一侧连接有多个第一滚轮,第一滚轮用于对液晶屏幕定位。Optionally, the first positioning assembly includes a positioning plate and a third positioning member for driving the positioning plate to move. The positioning plate is connected with a plurality of first rollers on the side close to the liquid crystal screen, and the first rollers are used for positioning the liquid crystal screen. position.
可选地,定位板上设置有长条孔,定位板通过长条孔安装在第三对位件上。Optionally, the positioning plate is provided with elongated holes, and the positioning plate is mounted on the third alignment member through the elongated holes.
可选地,压接机构包括用于夹紧液晶屏幕的探针压紧组件和产品压紧组件,探针压紧组件上设置有用于与液晶屏幕连接的探针。Optionally, the crimping mechanism includes a probe pressing component for clamping the liquid crystal screen and a product pressing component, and the probe pressing component is provided with a probe for connecting with the liquid crystal screen.
可选地,压接机构还包括压接调节组件,压接调节组件用于驱动探针压紧组件和产品压紧组件运动,使探针与液晶屏幕的连接处相对应。Optionally, the crimping mechanism further includes a crimping adjustment component, and the crimping adjustment component is used to drive the probe pressing component and the product pressing component to move, so that the connection between the probe and the liquid crystal screen corresponds.
可选地,压接调节组件包括第三驱动件和第三传动件,第三传动件与探针压紧组件和产品压紧组件连接,第三驱动件驱动第三传动件并带动探针压紧组件和产品压紧组件运动。Optionally, the crimping adjustment assembly includes a third driving member and a third transmission member, the third transmission member is connected with the probe pressing assembly and the product pressing assembly, and the third driving member drives the third transmission member and drives the probe to press. movement of the compression assembly and the product compression assembly.
本实用新型的有益效果:The beneficial effects of the present utility model:
本实用新型提供的液晶屏幕自动对位压接点灯装置,液晶屏幕放置在治具调节机构上,产品对位机构用于对液晶屏幕对位,之后压接机构对液晶屏幕压接点灯;通过治具调节机构、产品对位机构及压接机构进行尺寸调整,实现了对多种不同尺寸液晶屏幕的兼容,并实现了自动对位压接点灯,进而降低了生产成本,提高了生产效率。The utility model provides an automatic alignment and crimping lighting device for a liquid crystal screen. The liquid crystal screen is placed on the jig adjusting mechanism, and the product alignment mechanism is used to align the liquid crystal screen, and then the crimping mechanism crimps and lights the liquid crystal screen; The adjustment mechanism, the product alignment mechanism and the crimping mechanism are used to adjust the size, which realizes the compatibility of various LCD screens of different sizes, and realizes the automatic alignment and crimping lighting, thereby reducing the production cost and improving the production efficiency.
附图说明Description of drawings
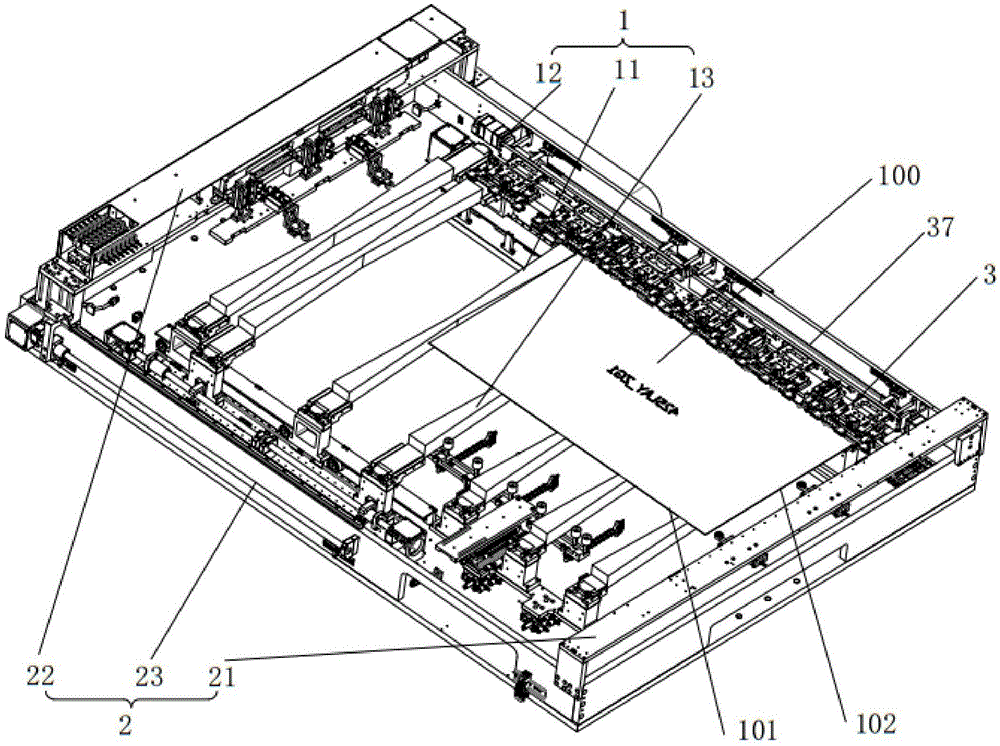
图1是本实用新型的具体实施方式提供的液晶屏幕自动对位压接点灯装置的结构示意图;1 is a schematic structural diagram of a liquid crystal screen automatic alignment crimp lighting device provided by a specific embodiment of the present invention;
图2是本实用新型的具体实施方式提供的治具调节机构结构示意图;2 is a schematic structural diagram of a fixture adjustment mechanism provided by a specific embodiment of the present invention;
图3是本实用新型的具体实施方式提供的固定治具组件结构示意图;3 is a schematic structural diagram of a fixture assembly provided by a specific embodiment of the present invention;
图4是本实用新型的具体实施方式提供的移动治具组件结构示意图;4 is a schematic structural diagram of a mobile jig assembly provided by a specific embodiment of the present invention;
图5是本实用新型的具体实施方式提供的第一驱动组件结构示意图;5 is a schematic structural diagram of a first drive assembly provided by a specific embodiment of the present invention;
图6是本实用新型的具体实施方式提供的活动端第一对位组件结构示意图;FIG. 6 is a schematic structural diagram of the first alignment component of the movable end provided by the specific embodiment of the present invention;
图7是本实用新型的具体实施方式提供的第二驱动组件结构示意图;7 is a schematic structural diagram of a second drive assembly provided by a specific embodiment of the present invention;
图8是本实用新型的具体实施方式提供的固定端第一对位组件结构示意图;FIG. 8 is a schematic structural diagram of the first alignment component of the fixed end provided by the specific embodiment of the present invention;
图9是本实用新型的具体实施方式提供的第二定位组件结构示意图;9 is a schematic structural diagram of a second positioning assembly provided by a specific embodiment of the present invention;
图10是本实用新型的具体实施方式提供的压接机构结构示意图;10 is a schematic structural diagram of a crimping mechanism provided by a specific embodiment of the present invention;
图11是图10的A处局部放大图;Fig. 11 is a partial enlarged view at A of Fig. 10;
图12是本实用新型的具体实施方式提供的压接调节组件结构示意图。12 is a schematic structural diagram of a crimping adjustment assembly provided by a specific embodiment of the present invention.
图中:In the picture:
100-液晶屏幕;101-第一侧边;102-第二侧边;100-LCD screen; 101-first side; 102-second side;
1-治具调节机构;2-产品对位机构;3-压接机构;1- Fixture adjustment mechanism; 2- Product alignment mechanism; 3- Crimping mechanism;
11-移动治具组件;12-第一驱动组件;13-固定治具组件;11-movable fixture assembly; 12-first drive assembly; 13-fixed fixture assembly;
111-透明治具;112-主动端;113-从动端;1131-辅助滑轮;121-第一驱动件;122-第一传动件;111-transparent fixture; 112-active end; 113-driven end; 1131-auxiliary pulley; 121-first driving part; 122-first transmission part;
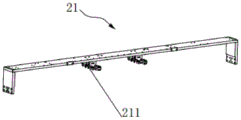
21-固定端第一对位组件;22-活动端第一对位组件;23-第二驱动组件;24-第一定位组件;21 - the first alignment component at the fixed end; 22 - the first alignment component at the movable end; 23 - the second driving component; 24 - the first positioning component;
211-第一对位件;211 - the first alignment piece;
221-第二对位件;222-微调机构;223-移动连接件;221-second alignment piece; 222-fine adjustment mechanism; 223-movement connection piece;
231-第二驱动件;232-第二传动件;233-移动安装架;231 - the second driving part; 232 - the second transmission part; 233 - the moving mounting frame;
241-第三对位件;242-定位板;243-第一滚轮;2421-长条孔;241-third alignment piece; 242-positioning plate; 243-first roller; 2421-long hole;
31-压接驱动件;32-缓冲器;33-产品压紧组件;34-探针压紧组件;35-弹簧件;36-第二定位组件;37-压接调节组件;31-crimping driver; 32-buffer; 33-product pressing component; 34-probe pressing component; 35-spring component; 36-second positioning component; 37-crimping adjustment component;
341-探针;361-推力气缸;362-第二滚轮;371-第三驱动件;372-导向件;373-第三传动件。341-probe; 361-thrust cylinder; 362-second roller; 371-third drive part; 372-guide part; 373-third transmission part.
具体实施方式Detailed ways
为使本实用新型解决的技术问题、采用的技术方案和达到的技术效果更加清楚,下面将结合附图对本实用新型实施例的技术方案做进一步的详细描述,显然,所描述的实施例仅仅是本实用新型一部分实施例,而不是全部的实施例。基于本实用新型中的实施例,本领域技术人员在没有做出创造性劳动前提下所获得的所有其他实施例,都属于本实用新型保护的范围。In order to make the technical problems solved by the present invention, the technical solutions adopted and the technical effects achieved more clearly, the technical solutions of the embodiments of the present invention will be described in further detail below in conjunction with the accompanying drawings. Obviously, the described embodiments are only Some embodiments of the present invention, but not all embodiments. Based on the embodiments of the present invention, all other embodiments obtained by those skilled in the art without creative work fall within the protection scope of the present invention.
在本实用新型的描述中,除非另有明确的规定和限定,术语“相连”、“连接”、“固定”应做广义理解,例如,可以是固定连接,也可以是可拆卸连接,或成一体;可以是机械连接,也可以是电连接;可以是直接相连,也可以通过中间媒介间接相连,可以是两个元件内部的连通或两个元件的相互作用关系。对于本领域的普通技术人员而言,可以具体情况理解上述术语在本实用新型中的具体含义。In the description of the present invention, unless otherwise expressly specified and limited, the terms "connected", "connected" and "fixed" should be understood in a broad sense, for example, it may be a fixed connection, a detachable connection, or a fixed connection. It can be a mechanical connection or an electrical connection; it can be a direct connection or an indirect connection through an intermediate medium, and it can be an internal connection between two elements or an interaction relationship between the two elements. For those of ordinary skill in the art, the specific meanings of the above terms in the present invention can be understood in specific situations.
在本实用新型中,除非另有明确的规定和限定,第一特征在第二特征之“上”或之“下”可以包括第一和第二特征直接接触,也可以包括第一和第二特征不是直接接触而是通过它们之间的另外的特征接触。而且,第一特征在第二特征“之上”、“上方”和“上面”包括第一特征在第二特征正上方和斜上方,或仅仅表示第一特征水平高度高于第二特征。第一特征在第二特征“之下”、“下方”和“下面”包括第一特征在第二特征正下方和斜下方,或仅仅表示第一特征水平高度小于第二特征。In the present invention, unless otherwise expressly specified and limited, a first feature "on" or "under" a second feature may include the first and second features in direct contact, or may include the first and second features The features are not in direct contact but through additional features between them. Also, the first feature being "above", "over" and "above" the second feature includes the first feature being directly above and obliquely above the second feature, or simply means that the first feature is level higher than the second feature. The first feature is "below", "below" and "below" the second feature includes the first feature being directly below and diagonally below the second feature, or simply means that the first feature has a lower level than the second feature.
一种液晶屏幕自动对位压接点灯装置,用于对液晶屏幕100点灯测试,包括治具调节机构1、压接机构3和产品对位机构2。如图1所示,治具调节机构1用于支撑液晶屏幕100,且治具调节机构1能根据液晶屏幕100的大小进行调节;压接机构3用于对液晶屏幕100压接并点灯,且压接机构3的位置能调节以适用于不同的液晶屏幕100;产品对位机构2用于将液晶屏幕100定位于压接机构3上。液晶屏幕100放置在治具调节机构1上,产品对位机构2用于对液晶屏幕100对位,之后压接机构3对液晶屏幕100压接点灯;通过治具调节机构1、产品对位机构2及压接机构3进行尺寸调整,实现了对多种不同尺寸液晶屏幕100的兼容,并实现了自动对位压接点灯,进而降低了生产成本,提高了生产效率。A liquid crystal screen automatic alignment crimping lighting device is used for lighting test of the
可选地,治具调节机构1包括移动治具组件11、第一驱动组件12和固定治具组件13,第一驱动组件12带动移动治具组件11运动以使移动治具组件11与固定治具组件13的间距适合于液晶屏幕100的尺寸。如图2所示,固定治具组件13固定在液晶屏幕100自动对位压接点灯装置的架体的一端,移动治具组件11设置在固定治具组件13的一侧,根据液晶屏幕100的尺寸大小决定第一驱动组件12驱动移动治具组件11移动的距离,使液晶屏幕100的两端分别放置在固定治具组件13和移动治具组件11上。Optionally, the jig adjusting mechanism 1 includes a moving
可选地,为了使液晶屏幕100得到稳定支撑,继续参照图2,移动治具组件11包括多个透明治具111,以增加对液晶屏幕100的支撑;如图3所示,固定治具组件13上设置有多个透明治具111,以增加固定治具组件13的宽度。可选地,透明治具111的材质为有机玻璃,具有较高的机械性能和介电性能,绝缘性良好,能使液晶屏幕100得到稳定的支撑,且能避免检测过程中产生电性干扰。Optionally, in order to stably support the
可选地,如图4和图5所示,第一驱动组件12包括第一驱动件121和第一传动件122,第一传动件122与透明治具111连接,第一驱动组件12驱动第一传动件122并带动透明治具111靠近或远离固定治具组件13运动。具体地,第一驱动件121为电机,第一传动件122为滚珠丝杠螺母副,电机驱动丝杠转动,丝杠螺母与透明治具111连接,电机旋转运动时带动透明治具111沿丝杠移动。进一步具体地,为保证透明治具111在移动过程中保持平稳,避免透明治具111两端运动不同步而出现偏移,透明治具111在与第一驱动组件12相对的一端设置有滑动导轨机构;可选地,透明治具111的两端分别为主动端112和从动端113,主动端112通过丝杠螺母与丝杠连接,从动端113通过滑块在导轨上移动;可选地,在从动端113上还安装有辅助滑轮1131,辅助滑轮1131在导轨上滑动,减小透明治具111在导轨上的摩擦阻力,同时增加从动端113与导轨的接触面积,使运动平稳。Optionally, as shown in FIG. 4 and FIG. 5 , the
进一步可选地,设置两组分别在移动治具组件11两侧的第一驱动组件12,以增强多个透明治具111的运动平稳性,使多个透明治具111能有序地对液晶屏幕100起到支撑作用。Further optionally, two sets of
可选地,如图6-8所示,产品对位机构2包括固定端第一对位组件21、活动端第一对位组件22和第二驱动组件23,固定端第一对位组件21与活动端第一对位组件22相对设置,第二驱动组件23带动活动端第一对位组件22运动以使活动端第一对位组件22靠近或远离固定端第一对位组件21,以保证对不同尺寸液晶屏幕100的定位。可选地,液晶屏幕100包括两组对应设置的第一侧边101和第二侧边102,本实施例中,固定端第一对位组件21与活动端第一对位组件22用于对两个第二侧边102定位。Optionally, as shown in FIGS. 6-8 , the
可选地,第二驱动组件23包括第二驱动件231和第二传动件232,活动端第一对位组件22和第二传动件232连接;继续参照图6-8,本实施例中,第二驱动件231为电机,第二传动件232为丝杠螺母副,丝杠螺母上安装有移动安装架233,活动端第一对位组件22包括设置在两端的移动连接件223,移动连接件223安装在移动安装架233上,电机旋转从而带动活动端第一对位组件22在丝杠上移动,并调节活动端第一对位组件22与固定端第一对位组件21的间距;可选地,活动端第一对位组件22与第二驱动组件23相对的一侧设置有导轨滑块副,活动端第一对位组件22一端的移动连接件223连接在滑块上,使活动端第一对位组件22沿导轨滑块副移动,保证运行平稳不偏移。Optionally, the
具体地,固定端第一对位组件21还包括第一对位件211,活动端第一对位组件22包括第二对位件221,当活动端第一对位组件22移动到位时,第一对位件211和第二对位件221用于对液晶屏幕100进行夹紧定位。可选地,第一对位件211和第二对位件221均包括气缸和设置在气缸上的滚轮,气缸驱动滚轮对液晶屏幕100进行夹紧定位;由于聚醚醚酮具有自润滑、易加工和高机械强度等优异性能,为避免碰伤与刮伤液晶屏幕100,滚轮可选用聚醚醚酮材质。Specifically, the
可选地,活动端第一对位组件22包括安装板,第二对位件221安装在安装板上,安装板安装在微调机构222上,根据不同液晶屏幕100的尺寸大小,使用微调机构222对安装板进行调节,使第二对位件221能对准液晶屏幕100,避免定位过程中出现偏移;可选地,安装板和微调机构222之间还安装有驱动气缸,驱动气缸能带动安装板和第二对位件221上下移动,避免在活动端第一对位组件22在第二驱动组件23驱动移动过程中对其下方的零部件产生干涉。Optionally, the
可选地,如图9所示,产品对位机构2还包括第一定位组件24,压接机构3包括与第一定位组件24相对设置的第二定位组件36,第一定位组件24和第二定位组件36用于对液晶屏幕100定位。本实施例中,第一定位组件24和第二定位组件36用于对第一侧边101进行定位。避免液晶屏幕100在沿第二侧边102的方向产生偏移。Optionally, as shown in FIG. 9 , the
继续参照图9,本实施例中,第一定位组件24包括定位板242和用于驱动定位板242运动的第三对位件241,定位板242在靠近液晶屏幕100的一侧连接有多个第一滚轮243,第一滚轮243用于对液晶屏幕100定位,多个第一滚轮243能增大与液晶屏幕100的接触面积,使定位平稳不偏移;可选地,第三对位件241包括滑台气缸;可选地,定位板242上设置有长条孔2421,定位板242通过长条孔2421安装在第三对位件241上,通过调节长条孔2421的位置以适用不同尺寸的液晶屏幕100。进一步可选地,滚轮可选用聚醚醚酮材质。Continuing to refer to FIG. 9 , in this embodiment, the
如图10和图11所示,可选地,压接机构3包括用于夹紧液晶屏幕100的探针压紧组件34和产品压紧组件33,探针压紧组件34上设置有用于与液晶屏幕100连接的探针341,探针341与液晶屏幕100连接实现压接点灯;可选地,压接机构3还包括压接驱动件31、缓冲器32和弹簧件35,压接驱动件31的活动端与探针压紧组件34连接;缓冲器32的固定端连接在探针压紧组件34上,缓冲器32的活动端连接在产品压紧组件33上;弹簧件35的两端安装在产品压紧组件33和探针压紧组件34上;当压接驱动件31带动探针压紧组件34往上移动接触液晶屏幕100时,缓冲件在反作用力下带动产品压紧组件33往下压紧液晶屏幕100,使液晶屏幕100与探针341充分接触;压接完成后,压接驱动件31往下移动远离液晶屏幕100,弹簧件35能驱动产品压紧机构往上抬起;可选地,产品压紧组件33包括与液晶屏幕100接触的压紧块,压紧块采用铁氟龙材质,可以很好防止损伤产品。As shown in FIGS. 10 and 11 , optionally, the crimping mechanism 3 includes a probe pressing assembly 34 for clamping the liquid crystal screen 100 and a product pressing assembly 33 , and the probe pressing assembly 34 is provided with a The probe 341 connected to the liquid crystal screen 100, the probe 341 is connected to the liquid crystal screen 100 to realize crimping lighting; optionally, the crimping mechanism 3 further includes a crimping driver 31, a buffer 32 and a spring member 35, and the crimping driver The movable end of 31 is connected to the probe pressing assembly 34; the fixed end of the buffer 32 is connected to the probe pressing assembly 34, and the movable end of the buffer 32 is connected to the product pressing assembly 33; both ends of the spring member 35 Installed on the product pressing component 33 and the probe pressing component 34; when the crimping driver 31 drives the probe pressing component 34 to move up and contact the liquid crystal screen 100, the buffer member drives the product pressing component 33 under the reaction force Press down the liquid crystal screen 100 to make the liquid crystal screen 100 fully contact with the probes 341; after the crimping is completed, the crimping driving member 31 moves down and away from the liquid crystal screen 100, and the spring member 35 can drive the product pressing mechanism to lift up ; Optionally, the product pressing component 33 includes a pressing block in contact with the liquid crystal screen 100, and the pressing block is made of Teflon material, which can well prevent damage to the product.
由于不同批次的液晶屏幕100的工艺边宽度可能会有所变化,为了使探针341与液晶屏幕100定位准确,需要根据不同的工艺边进行调整,以保证对位准确,使液晶屏幕100与探针341接触良好。本实施例中,根据第一侧边101的工艺边宽度不同,第二定位组件36包括推力气缸361和连接在推力气缸361上的第二滚轮362,推力气缸361推动第二滚轮362对液晶屏幕100的位置进行调整,以保证液晶屏幕100与探针341接触良好。可选地,根据第二侧边102的工艺边宽度不同,压接机构3还包括压接调节组件37,压接调节组件37用于驱动探针压紧组件34和产品压紧组件33运动,使探针341与液晶屏幕100的连接处相对应,避免出现对应偏差而产生测试误差。Since the process edge widths of different batches of
如图12所示,可选地,压接调节组件37包括第三驱动件371和第三传动件373,第三传动件373与探针压紧组件34和产品压紧组件33连接,第三驱动件371驱动第三传动件373并带动探针压紧组件34和产品压紧组件33运动。可选地,第三驱动件371为电机,第三传动件373为丝杠螺母副,电机驱动丝杠螺母副带动探针压紧组件34和产品压紧组件33运动;可选地,压接调节组件37还包括导向件372,导向件372可以为导轨机构,通过滑块连接于丝杠螺母上,以保证探针压紧组件34和产品压紧组件33运行平稳不偏移。As shown in FIG. 12 , optionally, the crimping
进一步可选地,液晶屏幕100自动对位压接点灯装置的工艺步骤,包括:Further optionally, the process steps of automatically aligning the
S1:治具调节机构1调节位置以用于放置不同尺寸的液晶屏幕100;S1: The jig adjusting mechanism 1 adjusts the position for placing
S2:放置液晶屏幕100;S2: place the
S3:第二驱动组件23驱动活动端第一对位组件22调节位置,以适应液晶屏幕100的尺寸;S3: the
S4:根据液晶屏幕100的第一侧边101工艺边的宽度,第二定位组件36的推力气缸361驱动第二滚轮362进行微调;S4: according to the width of the process edge of the
S5:调节第二对位件221的位置与第一对位件211配合对液晶屏幕100的第二侧边102夹紧定位;第一定位组件24的第三对位件241驱动定位板242,使第一滚轮243和第二定位组件36配合对液晶屏幕100的两个第一侧边101夹紧定位;S5: Adjust the position of the
S6:根据液晶屏幕100的第二侧边102工艺边的宽度,压接调节组件37对探针压紧组件34和产品压紧组件33的位置进行微调,调节至适用于液晶屏幕100的位置,使探针341能连接在液晶屏幕100上;S6: According to the width of the process edge of the
S7:压接驱动件31驱动,并和缓冲器32一起带动产品压紧组件33和探针341压紧组件34压紧液晶屏幕100,使探针341与液晶屏幕100充分接触;S7: The crimping
S8:测试完成后,压接驱动件31复位,与弹簧件35一起松开液晶屏幕100;S8: After the test is completed, the crimping driving
S9:取走液晶屏幕100。S9: The
进行一下屏幕测试,依次循环S1-S9。Perform a screen test and cycle through S1-S9 in turn.
显然,本实用新型的上述实施例仅仅是为了清楚说明本实用新型所作的举例,而并非是对本实用新型的实施方式的限定。对于所属领域的普通技术人员来说,在上述说明的基础上还可以做出其它不同形式的变化或变动。这里无需也无法对所有的实施方式予以穷举。凡在本实用新型的精神和原则之内所作的任何修改、等同替换和改进等,均应包含在本实用新型权利要求的保护范围之内。Obviously, the above-mentioned embodiments of the present invention are only examples for clearly illustrating the present invention, rather than limiting the implementation of the present invention. For those of ordinary skill in the art, changes or modifications in other different forms can also be made on the basis of the above description. There is no need and cannot be exhaustive of all implementations here. Any modifications, equivalent replacements and improvements made within the spirit and principles of the present utility model shall be included within the protection scope of the claims of the present utility model.
Claims (10)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922410598.2U CN211086851U (en) | 2019-12-28 | 2019-12-28 | Automatic alignment crimping lighting device for liquid crystal screen |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922410598.2U CN211086851U (en) | 2019-12-28 | 2019-12-28 | Automatic alignment crimping lighting device for liquid crystal screen |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN211086851U true CN211086851U (en) | 2020-07-24 |
Family
ID=71626278
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201922410598.2U Active CN211086851U (en) | 2019-12-28 | 2019-12-28 | Automatic alignment crimping lighting device for liquid crystal screen |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN211086851U (en) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112271529A (en) * | 2020-10-29 | 2021-01-26 | 苏州广林达电子科技有限公司 | A double-sided crimping device for a display screen |
| CN112284694A (en) * | 2020-11-19 | 2021-01-29 | 苏州科韵激光科技有限公司 | Crimping device and display panel testing equipment |
| CN113281927A (en) * | 2021-06-15 | 2021-08-20 | 上海金东唐科技有限公司 | Lighting jig discharging mechanism and lighting jig |
| CN114094402A (en) * | 2022-01-22 | 2022-02-25 | 深圳市伟盛丰科技有限公司 | Notebook computer maintenance display screen tool of lighting a lamp |
| CN114895487A (en) * | 2022-05-30 | 2022-08-12 | 厦门特仪科技有限公司 | Lighting test system |
| CN115857204A (en) * | 2022-12-19 | 2023-03-28 | 惠州帆声智创科技有限公司 | Universal fixture for LCD automatic lighting |
-
2019
- 2019-12-28 CN CN201922410598.2U patent/CN211086851U/en active Active
Cited By (8)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112271529A (en) * | 2020-10-29 | 2021-01-26 | 苏州广林达电子科技有限公司 | A double-sided crimping device for a display screen |
| CN112271529B (en) * | 2020-10-29 | 2025-11-04 | 苏州广林达电子科技有限公司 | A double-sided crimping device for display screens |
| CN112284694A (en) * | 2020-11-19 | 2021-01-29 | 苏州科韵激光科技有限公司 | Crimping device and display panel testing equipment |
| CN113281927A (en) * | 2021-06-15 | 2021-08-20 | 上海金东唐科技有限公司 | Lighting jig discharging mechanism and lighting jig |
| CN114094402A (en) * | 2022-01-22 | 2022-02-25 | 深圳市伟盛丰科技有限公司 | Notebook computer maintenance display screen tool of lighting a lamp |
| CN114895487A (en) * | 2022-05-30 | 2022-08-12 | 厦门特仪科技有限公司 | Lighting test system |
| CN114895487B (en) * | 2022-05-30 | 2023-08-25 | 厦门特仪科技有限公司 | Lighting test system |
| CN115857204A (en) * | 2022-12-19 | 2023-03-28 | 惠州帆声智创科技有限公司 | Universal fixture for LCD automatic lighting |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN109061915B (en) | Automatic crimping mechanism of general LCD module lamp | |
| CN112875290A (en) | Automatic loading and unloading device for products and automatic test equipment | |
| CN110879490B (en) | Detection device and production line | |
| CN113560882B (en) | Automatic assembly mechanism and assembly method for engine accessories for aerospace | |
| CN110480196A (en) | Fixture jacking and positioning mechanism, welding pressing assembly and welding device | |
| CN118527821B (en) | Laser welding equipment and method for hot formed plate | |
| CN111595780A (en) | Lighting system of screen | |
| CN121061533A (en) | Processing device for cold plate combination | |
| CN118363196B (en) | Liquid crystal display paster equipment | |
| CN216302643U (en) | ADS screen pastes screen equipment | |
| CN116038271B (en) | Automatic assembly equipment | |
| CN107037620A (en) | Locating tool and alignment method | |
| CN219465016U (en) | A clamping mechanism, positioning transmission device and processing equipment | |
| CN217747884U (en) | Beat mucilage binding and put with visual detection function | |
| CN212496250U (en) | Barrel assembly device | |
| CN117549072B (en) | Automatic assembly device and automatic assembly system for miniature gears | |
| CN223598046U (en) | Automatic displacement angle device of PCB | |
| CN221406229U (en) | Backlight automatic lighting device | |
| CN116100276B (en) | A two-way regularizing mechanism and camera assembly equipment | |
| CN114629983A (en) | Automatic mobile phone test equipment | |
| CN222431022U (en) | Timber positioner is used in cupboard production | |
| CN222746402U (en) | Press fit jig | |
| CN223465835U (en) | Be applicable to high-accuracy positioner of camera lens automatic installation plane XYR | |
| CN218447851U (en) | Wafer carrying device | |
| CN219919621U (en) | Automatic assembling clamp for LCD |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |