CN210908804U - Automatic assembly device for head shell and rotor of angle grinder - Google Patents
Automatic assembly device for head shell and rotor of angle grinder Download PDFInfo
- Publication number
- CN210908804U CN210908804U CN201921600352.5U CN201921600352U CN210908804U CN 210908804 U CN210908804 U CN 210908804U CN 201921600352 U CN201921600352 U CN 201921600352U CN 210908804 U CN210908804 U CN 210908804U
- Authority
- CN
- China
- Prior art keywords
- feeding
- bearing
- platform
- nut
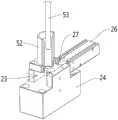
- cylinder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 230000005540 biological transmission Effects 0.000 claims abstract description 5
- 239000000463 material Substances 0.000 claims description 17
- 230000007246 mechanism Effects 0.000 claims description 12
- 230000008878 coupling Effects 0.000 claims description 3
- 238000010168 coupling process Methods 0.000 claims description 3
- 238000005859 coupling reaction Methods 0.000 claims description 3
- 239000004744 fabric Substances 0.000 claims description 3
- 238000009434 installation Methods 0.000 abstract description 6
- 238000005498 polishing Methods 0.000 abstract description 6
- 238000010586 diagram Methods 0.000 description 6
- 238000010276 construction Methods 0.000 description 2
- 230000007547 defect Effects 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 229910052751 metal Inorganic materials 0.000 description 2
- 239000002184 metal Substances 0.000 description 2
- 238000003466 welding Methods 0.000 description 2
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 description 1
- 229910000831 Steel Inorganic materials 0.000 description 1
- 229910052782 aluminium Inorganic materials 0.000 description 1
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 description 1
- 239000011324 bead Substances 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000004140 cleaning Methods 0.000 description 1
- 238000004891 communication Methods 0.000 description 1
- 229910052802 copper Inorganic materials 0.000 description 1
- 239000010949 copper Substances 0.000 description 1
- 238000002474 experimental method Methods 0.000 description 1
- 238000003780 insertion Methods 0.000 description 1
- 230000037431 insertion Effects 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 230000008569 process Effects 0.000 description 1
- 239000010959 steel Substances 0.000 description 1
- 238000005491 wire drawing Methods 0.000 description 1
Images




Landscapes
- Constituent Portions Of Griding Lathes, Driving, Sensing And Control (AREA)
Abstract
The utility model discloses an automatic assembly device for a head shell and a rotor of an angular polishing machine, which comprises a platform plate, wherein the platform plate is rotationally connected with a chuck, the chuck is provided with a hollow shaft, a first belt pulley is arranged on the hollow shaft, a first motor is arranged on the platform plate, a second belt pulley is arranged on the first motor, and a transmission belt is arranged between the second belt pulley and the first belt pulley; the top of chuck is equipped with assembly platform, and the last head shell anchor clamps that have of assembly platform is equipped with rotary clamping cylinder on the assembly platform, and sliding connection has on the assembly platform to get a platform, gets to be equipped with on the platform and gets a cylinder one and get a cylinder two, gets to be equipped with flexible push rod one on the cylinder one, is equipped with the nut on the flexible push rod one and presss from both sides and get the arm, gets to be equipped with flexible push rod two on the cylinder two, is equipped with the umbrella tooth on the flexible push rod two and presss from both sides. The device realizes automatic assembly, and the installation effectiveness is high, and the operation is swift, and overall function is perfect, and the practicality is strong.
Description
Technical Field
The utility model relates to a mechanical automation technical field, more specifically say, it relates to an angle grinder is with first shell and rotor automatic assembly device.
Background
An angle grinder is an electric tool used for grinding weld beads, removing welding defects, cleaning welding roots and the like. The angle grinder has the advantages of high rotating speed, high defect removing speed, attractive and clean grinding weld joint and the like. The diameter of the angle grinder is divided into various specifications of 100mm, 125mm, 150mm, 180mm, 250mm and the like according to the diameter of a used grinding sheet.
The polishing machine is a manual electric tool for polishing metal surfaces. The polishing machine is specially used for carrying out effect treatment on the surfaces and pipes of metal products such as steel, aluminum, copper and the like, dozens of original factory accessories meet different requirements, snow patterns, wire drawing patterns, wavy patterns, matte surfaces, mirror surfaces and the like with different precisions can be easily manufactured, deep scratches and slight scratches can be quickly repaired, and the polishing machine can be quickly polished and polished.
In the existing process of assembling the angle grinder, manual or semi-automatic operation is mostly adopted, the assembly efficiency is low, and the assembly error rate is high; and as the labor cost is increased year by year, the manual or semi-automatic assembly cost is high, and the product pricing is higher, so that the market competition is not facilitated. As shown in fig. 17 and 18, the head housing part 100 and the rotor part 200 of the conventional angle grinder are provided, an upper shaft end 201 of the rotor part 200 needs to extend into the head housing part 100, and then is sleeved with bevel gears, and then is screwed with nuts, while a lower shaft end 202 of the rotor part 200 needs to be sleeved with bearings, which are mostly manually assembled, and thus, the installation is tedious and time-consuming, and the overall effect is not good. Therefore, the utility model provides a head shell and rotor automatic assembly device for angle grinder.
SUMMERY OF THE UTILITY MODEL
An object of the utility model is to overcome not enough among the above-mentioned prior art, provide an angle is head shell and rotor automatic assembly device for grinding machine.
In order to solve the technical problem, the purpose of the utility model is to realize like this: the utility model relates to an automatic assembly device of a head shell and a rotor for an angular grinding machine, which comprises a platform plate, wherein a chuck is rotatably connected on the platform plate, the chuck is provided with a hollow shaft extending out of the lower end surface of the platform plate, the hollow shaft rotates along with the chuck, a first belt pulley is sleeved on the hollow shaft, a first motor is also arranged on the platform plate, a second belt pulley is arranged at the output end of the first motor, and a transmission belt is arranged between the second belt pulley and the first belt pulley; an assembly platform which can move up and down is arranged above the chuck, a head shell clamp is arranged on the assembly platform, a rotor stretching hole is arranged on the head shell clamp, a rotary clamping cylinder is arranged on the assembly platform, a rotary clamping arm is arranged on the rotary clamping cylinder, a pickup platform is connected on the assembly platform in a sliding manner, a pickup cylinder I and a pickup cylinder II are arranged on the pickup platform, a telescopic push rod I is arranged on the pickup cylinder I, a nut clamping arm which is connected on the pickup platform in a sliding manner is arranged on the telescopic push rod I, a telescopic push rod II is arranged on the pickup cylinder II, a bevel gear clamping arm which is connected on the pickup platform in a sliding manner is arranged on the telescopic push rod II, the bevel gear clamping arm and the nut clamping arm are arranged in parallel, a nut feeding seat is arranged at the front end of the nut clamping arm, a nut feeding groove is arranged on the nut feeding seat, and a feeding cylinder I is arranged, the feeding cylinder I is provided with a telescopic push rod III which extends into the nut feeding groove and faces the nut clamping arm, the front end of the bevel gear clamping arm is provided with a bevel gear feeding seat, the bevel gear feeding seat is provided with a bevel gear feeding groove, the bevel gear feeding seat is provided with a feeding cylinder II, and the feeding cylinder II is provided with a telescopic push rod IV which extends into the bevel gear feeding groove and faces the bevel gear clamping arm; the end part of the nut clamping arm is embedded with a first magnet, and the end part of the bevel gear clamping arm is embedded with a second magnet.
The utility model discloses further set up to: the bearing feeding mechanism comprises a bearing feeding seat, a linear bearing feeding groove is formed in the bearing feeding seat, a jacking hole located right below the hollow shaft is formed in the bearing feeding groove, a push plate for pushing the bearing to the position above the jacking hole is connected in the bearing feeding groove in a sliding mode, and the bearing feeding mechanism further comprises a feeding cylinder fifth for controlling the push plate to slide in the bearing feeding groove; the bearing jacking mechanism is arranged below the jacking hole and comprises a jacking frame arranged on the platform plate, a first push rod cylinder is arranged on the jacking frame, and a fifth telescopic push rod which stretches into the jacking hole and pushes the bearing from the bearing feeding groove to the hollow shaft is arranged on the first push rod cylinder.
The utility model discloses further set up to: still include the automatic feed frame, the automatic feed frame is including establishing on bearing feed seat and inside bearing feed sleeve that piles up there is the bearing, and bearing feed sleeve is located the top in bearing feed groove just makes the bearing of below fall into the bearing feed groove, bearing feed sleeve interpolation has the bearing locating lever rather than the coaxial line setting.
The utility model discloses further set up to: the nut feeding device is used for feeding the nut feeding groove.
The utility model discloses further set up to: nut feedway includes the material seat, has seted up the feed bin on the material seat, is equipped with in the feed bin to rotate to be connected charging tray on the material seat, the charging tray is located the side of feed bin, be equipped with a plurality of guide pieces around charging tray rotation axis annular array distribution on the charging tray, the outer wall cloth of charging tray has the teeth of a cogwheel, be equipped with motor two on the material seat, the output of motor two is equipped with and meshes driven gear with the teeth of a cogwheel, still includes that one end stretches into the charging tray, the other end stretches into the material way in nut feed groove.
The utility model discloses further set up to: the umbrella tooth feeding device is used for feeding the umbrella tooth feeding groove.
The utility model discloses further set up to: bevel feed device is including establishing on bevel feed seat and inside bevel feed sleeve that piles up the bevel, bevel feed sleeve is located the top of bevel feed groove just makes the below bevel fall into the bevel feed groove, bevel feed sleeve interpolation has the bevel locating lever rather than the coaxial line setting.
The utility model discloses further set up to: be equipped with stand one on the landing plate, be equipped with slide rail one on the stand, sliding connection has to establish on slide rail one slider one on the assembly platform, still be equipped with motor three on the landing plate, the output hookup of motor three has the lead screw, and the cooperation has screw-nut on the lead screw, and the last rigid coupling that is equipped with of screw-nut is in slider two on the assembly platform, still be equipped with on the landing plate and supply two sliding connection of slider to have slide rail two.
The utility model discloses further set up to: the bottom of the piece taking platform is connected with a third sliding rail arranged on the assembling platform in a sliding mode, a second push rod cylinder is arranged on the assembling platform, and the second push rod cylinder is provided with a sixth telescopic push rod for controlling the piece taking platform to slide on the assembling platform.
The utility model discloses further set up to: the end part of the nut clamping arm is provided with a nut matching groove, and the first magnet is embedded in the nut matching groove; the end part of the bevel gear clamping arm is provided with a bevel gear matching groove, and the second magnet is embedded in the bevel gear matching groove.
To sum up, the utility model discloses following beneficial effect has: the utility model relates to an angle is first shell and rotor automatic assembly device for grinder accomplishes the bearing of rotor part bottom through automatic equipment to and the bevel gear on rotor part top, and be connected it with first shell part, realize automatic assembly, improve assembly efficiency, the error rate is low, and the installation is swift, and overall function is perfect, and the practicality is strong.
Drawings
Fig. 1 is a schematic view of the overall structure of the present invention;
FIG. 2 is a schematic view of a part of the structure of the present invention;
FIG. 3 is a schematic view of the structure of FIG. 2 from another perspective;
fig. 4 is a partial structural schematic diagram of the present invention;
fig. 5 is a schematic structural diagram of the bearing feeding mechanism according to the present invention;
fig. 6 is a schematic structural view of the bearing feeding seat of the present invention;
fig. 7 is a schematic structural view of the present invention for embodying a push plate and a feeding cylinder;
fig. 8 is a schematic structural diagram of the first push rod cylinder according to the present invention;
fig. 9 is a schematic structural diagram of the assembly platform according to the present invention;
fig. 10 is a schematic structural diagram of the present invention for showing a pickup platform;
fig. 11 is a schematic structural diagram of the assembly platform and the pickup platform according to the present invention;
fig. 12 is a schematic structural view of the bevel gear feeding device of the present invention;
fig. 13 is a schematic structural view for embodying the nut gripper arm of the present invention;
fig. 14 is a schematic structural view of the bevel gear gripping arm according to the present invention;
fig. 15 is a schematic structural view of the nut feeder according to the present invention;
FIG. 16 is a schematic view of the structure of FIG. 15 from another perspective;
figure 17 is a schematic of the construction of the head housing component and rotor component of the prior art angle grinder;
figure 18 is a schematic view of the construction of the head housing components on a prior art angle grinder.
Detailed Description
In order to make the technical solutions of the present invention better understood by those skilled in the art, the following description of the preferred embodiments of the present invention is provided in conjunction with the specific examples, but it should be understood that these descriptions are only for the purpose of further illustrating the features and advantages of the present invention, and are not intended to limit the patent requirements of the present invention. Based on the embodiments in the present invention, all other embodiments obtained by a person skilled in the art without creative work belong to the protection scope of the present invention.
The invention will be further described with reference to the accompanying drawings and preferred embodiments.
Referring to fig. 1 to 18, the automatic assembly device for the head shell and the rotor of the angular polishing machine according to the embodiment includes a platform plate 1, a chuck 2 is rotatably connected to the platform plate 1, the chuck 2 has a hollow shaft 3 extending out of the lower end surface of the platform plate 1, the hollow shaft 3 rotates with the chuck 2, a first belt pulley 4 is sleeved on the hollow shaft 3, a first motor 5 is further arranged on the platform plate 1, a second belt pulley 6 is arranged at the output end of the first motor 5, and a transmission belt 7 is arranged between the second belt pulley 6 and the first belt pulley 4; an assembly platform 8 which moves up and down is arranged above the chuck 2, a head shell clamp 9 is arranged on the assembly platform 8, a rotor extending hole 10 is arranged on the head shell clamp 9, a rotary clamping cylinder 11 is arranged on the assembly platform 8, a rotary clamping arm 12 is arranged on the rotary clamping cylinder 11, a pickup platform 13 is connected on the assembly platform 8 in a sliding manner, a pickup cylinder 14 and a pickup cylinder 15 are arranged on the pickup platform 13, a telescopic push rod 16 is arranged on the pickup cylinder 14, a nut clamping arm 17 which is connected on the pickup platform 13 in a sliding manner is arranged on the telescopic push rod 16, a telescopic push rod 18 is arranged on the pickup cylinder 15, a bevel gear clamping arm 19 which is connected on the pickup platform 13 in a sliding manner is arranged on the telescopic push rod 18, the bevel gear clamping arm 19 is arranged in parallel to the nut clamping arm 17, and a nut feeding seat 20 is arranged at the front end of the nut clamping arm 17, a nut feeding groove 21 is formed in the nut feeding seat 20, a feeding cylinder I22 is arranged on the nut feeding seat 20, the feeding cylinder I22 is provided with a third telescopic push rod 23 which extends into the nut feeding groove 21 and faces the nut clamping arm 17, the front end of the bevel gear clamping arm 19 is provided with a bevel gear feeding seat 24, a bevel gear feeding groove 25 is formed in the bevel gear feeding seat 24, a second feeding cylinder 26 is arranged on the bevel gear feeding seat 24, and the second feeding cylinder 26 is provided with a fourth telescopic push rod 27 which extends into the bevel gear feeding groove 25 and faces the bevel gear clamping arm 19; a first magnet 28 is embedded in the end of the nut gripper arm 17, and a second magnet 29 is embedded in the end of the bevel gear gripper arm 19.
Further, the bearing feeding mechanism 30 is arranged on the platform plate 1, the bearing feeding mechanism 30 comprises a bearing feeding seat 31, a linear bearing feeding groove 32 is formed in the bearing feeding seat 31, a jacking hole 33 located right below the hollow shaft 3 is formed in the bearing feeding groove 32, a push plate 34 for pushing a bearing to the position above the jacking hole 33 is connected in the bearing feeding groove 32 in a sliding mode, and the bearing feeding mechanism further comprises a feeding cylinder five 35 for controlling the push plate 34 to slide in the bearing feeding groove 32; the bearing jacking mechanism 36 is arranged below the jacking hole 33, the bearing jacking mechanism 36 comprises a jacking frame 37 arranged on the platform plate 1, a first push rod cylinder 38 is arranged on the jacking frame 37, and the first push rod cylinder 38 is provided with a fifth telescopic push rod 39 which extends into the jacking hole 33 and pushes the bearing from the bearing feeding groove 32 to the hollow shaft 3.
Further, still include automatic feed frame 40, automatic feed frame 40 is including establishing on bearing feed seat 31 and inside bearing feed sleeve 41 that piles up the bearing, and bearing feed sleeve 41 is located bearing feed groove 32's top just makes the bearing of the below fall into bearing feed groove 32, bearing feed sleeve 41 interpolation has rather than the bearing locating lever 42 of coaxial line setting.
Further, a nut feeding device 43 for feeding the nut feeding groove 32 is further included.
Further, nut feedway 43 includes material seat 44, has seted up feed bin 45 on the material seat 44, is equipped with in the feed bin 45 to rotate to be connected charging tray 46 on the material seat 44, and charging tray 46 is located the side of feed bin 45, be equipped with a plurality of guide pieces 47 that distribute around charging tray 46 rotation axis annular array on the charging tray 46, the outer wall cloth of charging tray 46 has the teeth of a cogwheel 48, be equipped with two 49 motors on the material seat 44, the output of two 49 motors is equipped with and engages driven gear 50 with the teeth of a cogwheel 48, still includes that one end stretches into charging tray 46, the other end stretches into the material way 51 of nut feed tank 21. The nuts put into the bin 45 are centrifugally thrown by the charging tray 46 by the rotation of the second motor 49, and part of the nuts fall on the material channel 51 and are pushed into the nut feeding groove 21 one by one.
Further, the umbrella tooth feeding device is also provided for feeding the umbrella tooth feeding groove 25.
Further, the bevel feeding device comprises a bevel feeding sleeve 52 which is arranged on the bevel feeding seat 24 and is internally stacked with bevel, the bevel feeding sleeve 52 is positioned above the bevel feeding groove 25 and enables the lowest bevel to fall into the bevel feeding groove 25, and a bevel positioning rod 53 which is coaxial with the bevel feeding sleeve 52 is inserted in the bevel feeding sleeve 52.
Further, be equipped with stand 54 on the landing slab 1, be equipped with slide rail 55 on stand 54, sliding connection has to establish on slide rail 55 slider 56 on the assembly platform 8, still be equipped with three 57 of motors on the landing slab 1, the output of three 57 of motors is connected with lead screw 58, and the cooperation has screw-nut 59 on the lead screw 58, is equipped with the rigid coupling on the screw-nut 59 two 60 of sliders on the assembly platform 8, still be equipped with on the landing slab 1 and supply two 60 sliding connection of slider to have two 61 of slide rails.
Furthermore, the bottom of the pickup platform 13 is slidably connected with a third slide rail 62 arranged on the assembly platform 8, the assembly platform 8 is provided with a second push rod cylinder 64, and the second push rod cylinder 64 is provided with a sixth telescopic push rod 65 for controlling the pickup platform 13 to slide on the assembly platform 8.
Further, a nut fitting groove 66 is formed in the end portion of the nut clamping arm 17, and the first magnet 28 is embedded in the nut fitting groove 66; the end part of the bevel gear clamping arm 19 is provided with a bevel gear matching groove 67, and the second magnet 29 is embedded in the bevel gear matching groove 67.
In this embodiment, the rotor portion 200 of the angle grinder is taken out and clamped on the chuck 2, the upper shaft end 201 of the rotor portion 200 passes through the rotor insertion hole 10, extends out of the taking platform 13, and after clamping, the head housing portion 100 is mounted on the head housing clamp 9, and the rotary clamping cylinder 11 is operated to rotate and tighten the rotary clamping arm 12 to press the head housing portion 100, so as to complete clamping of the head housing portion 100, wherein the upper shaft end 201 also extends into the head housing portion 100. At the moment, a bearing is to be installed on the part of the lower shaft end 202, the bearing is sleeved on the positioning rod 42 in advance, the upper end of the positioning rod 42 is fixed with the platform plate 1, part of the bearing is located in the bearing feeding sleeve 41, and the lowest bearing is attached to the bearing feeding groove 32, at the moment, when the bearing needs to be sleeved on the lower shaft end 202, the feeding cylinder five 35 operates, the carrying push plate 34 slides in the bearing feeding groove 32, the lowest bearing is pushed to be above the jacking hole 33 and is arranged coaxially with the jacking hole 33, the push rod cylinder one 38 is operated, the telescopic push rod five 39 is lifted upwards, penetrates through the jacking hole 33 and continues to be lifted until the end part of the telescopic push rod carries the bearing to be lifted together and extends into the shaft hole of the hollow shaft 3, and finally the bearing is jacked to be sleeved on the position of the lower shaft end 202 of the rotor part 200;
then adding a proper amount of nuts in the bin 45 of the nut feeding device 43, sleeving a proper amount of bevel gears on the bevel gear positioning rod 53, discontinuously pushing the nuts from the material channel 51 into the nut feeding groove 21, dropping the bevel gears into the bevel gear feeding groove 25 one by one, sliding the telescopic push rod six 65 carrying platform 13 on the assembly platform 8 in a reciprocating manner by operating the push rod cylinder two 64, when the nut clamping arm 17 and the nut feeding groove 21 are in the same straight line, operating the first taking cylinder 14, contracting the telescopic push rod one 16, extending the nut clamping arm 17 into the nut feeding groove 21, adsorbing the nuts in the nut feeding groove 21 by the magnet one 28, extending the telescopic push rod one 16, withdrawing the nut clamping arm 17 from the nut feeding groove 21, adsorbing the nuts on the magnet one 28, moving the nut clamping arm 17 together, moving the carrying platform 13 to the bevel gear feeding groove 25, when the nut clamping arm 17 faces the head shell part 100, at this time, when the bevel gear clamping arm 19 and the bevel gear feeding groove 25 are on the same straight line, the part taking cylinder two 15 operates to contract the telescopic push rod two 18, the bevel gear clamping arm 19 is carried to extend into the bevel gear feeding groove 25, the bevel gears in the bevel gear feeding groove 25 are adsorbed by the magnet two 29, the telescopic push rod two 18 is extended, the bevel gear clamping arm 19 is carried to be drawn out from the bevel gear feeding groove 25, the bevel gears are adsorbed on the magnet two 29 and move along with the bevel gear clamping arm 19, the bevel gears are firstly placed into the head shell part 100 by the bevel gear clamping arm 19 and are sleeved on the upper shaft end 201, and then the nut is connected with the upper shaft end 201 through the nut feeding groove 21 in a threaded manner, wherein, the mounting platform 8 can be lifted and lowered adaptively so that two accessories can be mounted and placed into the head shell part 100, the bevel gears only need to be sleeved on the upper shaft end 201, and when the nut is located at the upper shaft end 201, the motor one 5 operates, the second belt pulley 6 is driven to rotate by the transmission belt 7, and the first belt pulley 4 drives the hollow shaft 3 and the upper chuck 2 to rotate, so that the rotor part 200 rotates, the upper shaft end 201 is screwed with the nut, and the installation of the bevel gear and the nut is completed. The reciprocating nut clamping arm 17 and the bevel gear clamping arm 19 can realize that one end is installed, and the other end is responsible for taking a piece (taking the bevel gear when the nut is installed; taking the nut when the bevel gear is installed), so that the time is saved, and the installation efficiency is higher.
The utility model relates to an angle is first shell and rotor automatic assembly device for grinder accomplishes the bearing of rotor part bottom through automatic equipment to and the bevel gear on rotor part top, and be connected it with first shell part, realize automatic assembly, improve assembly efficiency, the error rate is low, and the installation is swift, and overall function is perfect, and the practicality is strong.
Unless otherwise specified, in the present invention, if the terms "length", "width", "upper", "lower", "front", "rear", "left", "right", "vertical", "horizontal", "top", "bottom", "inner", "outer", "clockwise", "counterclockwise", "axial", "radial", "circumferential" and the like indicate an orientation or positional relationship based on the orientation or positional relationship shown in the drawings, it is only for convenience of describing the present invention and simplifying the description, rather than to indicate or imply that the device or element so referred to must have a particular orientation, be constructed and operated in a particular orientation, therefore, the terms describing orientation or positional relationship in the present invention are used for illustrative purposes only, and should not be construed as limiting the present patent, specific meanings of the above terms can be understood by those of ordinary skill in the art in light of the specific circumstances in conjunction with the accompanying drawings.
Unless expressly stated or limited otherwise, the terms "disposed," "connected," and "connected" are used broadly and encompass both fixed and removable connections, or integral connections; the connection may be direct or indirect via an intermediate medium, and may be a communication between the two elements. The specific meaning of the above terms in the present invention can be understood in specific cases to those skilled in the art.
The foregoing has described in detail preferred embodiments of the present invention. It should be understood that numerous modifications and variations can be devised by those skilled in the art in light of the present teachings without departing from the inventive concepts. Therefore, the technical solutions that can be obtained by a person skilled in the art through logic analysis, reasoning or limited experiments based on the prior art according to the concepts of the present invention should be within the scope of protection defined by the claims.
Claims (10)
1. First shell and rotor automatic assembly device for angle grinder, including the landing slab, the last rotation of landing slab is connected with chuck, its characterized in that: the chuck is provided with a hollow shaft extending out of the lower end face of the platform plate, the hollow shaft rotates along with the chuck, a first belt pulley is sleeved on the hollow shaft, a first motor is further arranged on the platform plate, a second belt pulley is arranged at the output end of the first motor, and a transmission belt is arranged between the second belt pulley and the first belt pulley; an assembly platform which can move up and down is arranged above the chuck, a head shell clamp is arranged on the assembly platform, a rotor stretching hole is arranged on the head shell clamp, a rotary clamping cylinder is arranged on the assembly platform, a rotary clamping arm is arranged on the rotary clamping cylinder, a pickup platform is connected on the assembly platform in a sliding manner, a pickup cylinder I and a pickup cylinder II are arranged on the pickup platform, a telescopic push rod I is arranged on the pickup cylinder I, a nut clamping arm which is connected on the pickup platform in a sliding manner is arranged on the telescopic push rod I, a telescopic push rod II is arranged on the pickup cylinder II, a bevel gear clamping arm which is connected on the pickup platform in a sliding manner is arranged on the telescopic push rod II, the bevel gear clamping arm and the nut clamping arm are arranged in parallel, a nut feeding seat is arranged at the front end of the nut clamping arm, a nut feeding groove is arranged on the nut feeding seat, and a feeding cylinder I is arranged, the feeding cylinder I is provided with a telescopic push rod III which extends into the nut feeding groove and faces the nut clamping arm, the front end of the bevel gear clamping arm is provided with a bevel gear feeding seat, the bevel gear feeding seat is provided with a bevel gear feeding groove, the bevel gear feeding seat is provided with a feeding cylinder II, and the feeding cylinder II is provided with a telescopic push rod IV which extends into the bevel gear feeding groove and faces the bevel gear clamping arm; the end part of the nut clamping arm is embedded with a first magnet, and the end part of the bevel gear clamping arm is embedded with a second magnet.
2. The automatic assembling device for the head housing and the rotor of the angle grinder as claimed in claim 1, wherein: the bearing feeding mechanism comprises a bearing feeding seat, a linear bearing feeding groove is formed in the bearing feeding seat, a jacking hole located right below the hollow shaft is formed in the bearing feeding groove, a push plate for pushing the bearing to the position above the jacking hole is connected in the bearing feeding groove in a sliding mode, and the bearing feeding mechanism further comprises a feeding cylinder fifth for controlling the push plate to slide in the bearing feeding groove; the bearing jacking mechanism is arranged below the jacking hole and comprises a jacking frame arranged on the platform plate, a first push rod cylinder is arranged on the jacking frame, and a fifth telescopic push rod which stretches into the jacking hole and pushes the bearing from the bearing feeding groove to the hollow shaft is arranged on the first push rod cylinder.
3. The automatic assembling device for the head housing and the rotor for the angle grinder of claim 2, wherein: still include the automatic feed frame, the automatic feed frame is including establishing on bearing feed seat and inside bearing feed sleeve that piles up there is the bearing, and bearing feed sleeve is located the top in bearing feed groove just makes the bearing of below fall into the bearing feed groove, bearing feed sleeve interpolation has the bearing locating lever rather than the coaxial line setting.
4. The automatic assembling device for the head housing and the rotor for the angle grinder as claimed in any one of claims 1 to 3, wherein: the nut feeding device is used for feeding the nut feeding groove.
5. The automatic assembling device for the head housing and the rotor for the angle grinder of claim 4, wherein: nut feedway includes the material seat, has seted up the feed bin on the material seat, is equipped with in the feed bin to rotate to be connected charging tray on the material seat, the charging tray is located the side of feed bin, be equipped with a plurality of guide pieces around charging tray rotation axis annular array distribution on the charging tray, the outer wall cloth of charging tray has the teeth of a cogwheel, be equipped with motor two on the material seat, the output of motor two is equipped with and meshes driven gear with the teeth of a cogwheel, still includes that one end stretches into the charging tray, the other end stretches into the material way in nut feed groove.
6. The automatic assembling device for the head housing and the rotor for the angle grinder as claimed in any one of claims 1 to 3, wherein: the umbrella tooth feeding device is used for feeding the umbrella tooth feeding groove.
7. The automatic assembling device for the head housing and the rotor for the angle grinder of claim 6, wherein: bevel feed device is including establishing on bevel feed seat and inside bevel feed sleeve that piles up the bevel, bevel feed sleeve is located the top of bevel feed groove just makes the below bevel fall into the bevel feed groove, bevel feed sleeve interpolation has the bevel locating lever rather than the coaxial line setting.
8. The automatic assembling device for the head housing and the rotor of the angle grinder as claimed in claim 1, wherein: be equipped with stand one on the landing plate, be equipped with slide rail one on the stand, sliding connection has to establish on slide rail one slider one on the assembly platform, still be equipped with motor three on the landing plate, the output hookup of motor three has the lead screw, and the cooperation has screw-nut on the lead screw, and the last rigid coupling that is equipped with of screw-nut is in slider two on the assembly platform, still be equipped with on the landing plate and supply two sliding connection of slider to have slide rail two.
9. The automatic assembling device for the head housing and the rotor of the angle grinder as claimed in claim 1, wherein: the bottom of the piece taking platform is connected with a third sliding rail arranged on the assembling platform in a sliding mode, a second push rod cylinder is arranged on the assembling platform, and the second push rod cylinder is provided with a sixth telescopic push rod for controlling the piece taking platform to slide on the assembling platform.
10. The automatic assembling device for the head housing and the rotor of the angle grinder as claimed in claim 1, wherein: the end part of the nut clamping arm is provided with a nut matching groove, and the first magnet is embedded in the nut matching groove; the end part of the bevel gear clamping arm is provided with a bevel gear matching groove, and the second magnet is embedded in the bevel gear matching groove.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921600352.5U CN210908804U (en) | 2019-09-25 | 2019-09-25 | Automatic assembly device for head shell and rotor of angle grinder |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921600352.5U CN210908804U (en) | 2019-09-25 | 2019-09-25 | Automatic assembly device for head shell and rotor of angle grinder |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210908804U true CN210908804U (en) | 2020-07-03 |
Family
ID=71349805
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921600352.5U Expired - Fee Related CN210908804U (en) | 2019-09-25 | 2019-09-25 | Automatic assembly device for head shell and rotor of angle grinder |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210908804U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113601148A (en) * | 2021-08-27 | 2021-11-05 | 浙江丰硕智能科技有限公司 | Automatic assembly equipment and assembly method for angle grinder rotor gear box |
| CN116871860A (en) * | 2023-07-11 | 2023-10-13 | 武义智能制造产业技术研究院 | A head shell and rotor assembly system |
-
2019
- 2019-09-25 CN CN201921600352.5U patent/CN210908804U/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN113601148A (en) * | 2021-08-27 | 2021-11-05 | 浙江丰硕智能科技有限公司 | Automatic assembly equipment and assembly method for angle grinder rotor gear box |
| CN116871860A (en) * | 2023-07-11 | 2023-10-13 | 武义智能制造产业技术研究院 | A head shell and rotor assembly system |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110842788B (en) | Sand blasting equipment for sand blasting and rust removing of pipeline surface | |
| CN117532263B (en) | All-round adjustable automatic welding device for water conservancy and hydropower pipelines and how to use it | |
| CN114290171A (en) | Chemical storage tank welding forming welding beading processing machinery of polishing | |
| CN217166728U (en) | Automatic special plane of new forms of energy pipe fitting | |
| CN220407751U (en) | Adjustable ship pipeline welding fixture | |
| CN113352040A (en) | Be applied to automatic welded anchor clamps of column foot | |
| CN119609261B (en) | A high-precision AI intelligent positioning tapping machine | |
| CN113601148B (en) | Angle grinding rotor gearbox automatic assembly equipment and assembly method | |
| CN221494497U (en) | Gear grinding device for helical gear machining | |
| CN211249109U (en) | A flush end machine for pipe bending | |
| CN220240425U (en) | Assembly line type iron net welding device | |
| CN220217840U (en) | Scratch repairing and polishing equipment for motorcycle lenses | |
| CN115673989B (en) | Corrosion-resistant polishing automation device for stainless steel pipe | |
| CN115446218B (en) | Automatic positioning tube shrinking device | |
| CN215999221U (en) | Manipulator conveying device of automatic welding machine | |
| CN210909461U (en) | Rotary mounting seat for assembling parts of angle grinder | |
| CN216066732U (en) | Precision machine part burring device | |
| CN223492897U (en) | An automatic rust removal device for pipes | |
| CN116460611B (en) | A machining fixture for a CNC machining center | |
| CN220740574U (en) | Polishing equipment for iron accessory production | |
| CN116276455B (en) | Welding spot cleaning device for laser welding | |
| CN112192342A (en) | Heating pipeline interface grinding device | |
| CN216066248U (en) | Automatic feeding device of automatic assembly equipment for angle grinder rotor gear box | |
| CN113878630A (en) | Efficient cutting device is used in production of PE feed pipe | |
| CN213998554U (en) | General formula car water pump processing frock |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20200703 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |