CN210907657U - A punching machine with automatic continuous punching function - Google Patents
A punching machine with automatic continuous punching function Download PDFInfo
- Publication number
- CN210907657U CN210907657U CN201922039688.5U CN201922039688U CN210907657U CN 210907657 U CN210907657 U CN 210907657U CN 201922039688 U CN201922039688 U CN 201922039688U CN 210907657 U CN210907657 U CN 210907657U
- Authority
- CN
- China
- Prior art keywords
- plate
- punching
- length direction
- groove
- sliding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000004080 punching Methods 0.000 title claims abstract description 43
- 230000008878 coupling Effects 0.000 claims 5
- 238000010168 coupling process Methods 0.000 claims 5
- 238000005859 coupling reaction Methods 0.000 claims 5
- 230000000694 effects Effects 0.000 abstract description 4
- 238000010586 diagram Methods 0.000 description 5
- 238000000034 method Methods 0.000 description 5
- 229910000831 Steel Inorganic materials 0.000 description 4
- 239000010959 steel Substances 0.000 description 4
- 239000000758 substrate Substances 0.000 description 3
- 230000009286 beneficial effect Effects 0.000 description 2
- 230000005540 biological transmission Effects 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 238000006073 displacement reaction Methods 0.000 description 1
- 238000012423 maintenance Methods 0.000 description 1
- 238000000465 moulding Methods 0.000 description 1
- 239000002994 raw material Substances 0.000 description 1
- 238000000926 separation method Methods 0.000 description 1
Images


Landscapes
- Perforating, Stamping-Out Or Severing By Means Other Than Cutting (AREA)
Abstract
本实用新型公开了一种带有自动连续冲孔功能的冲压机,属于冲压机冲孔的技术领域,其技术方案包括竖直设置的机架,所述机架上端竖直固接有冲头,机架上端还设置有能够驱动冲头向下滑移的驱动机构,所述机架对应冲头的下方固接有水平设置的工作台,所述机架对应工作台的下方沿其长度方向固接有一齿条,所述工作台上侧沿其长度方向滑移连接有一承接板,所述承接板转动连接有啮合于齿条的缺齿轮,所述缺齿轮转轴一端固接有驱动缺齿轮转动的伺服电机,所述承接板上设置有夹持板材的夹持组件。本实用新型实现了通过自动对板材进行连续定距冲孔进而降低工人劳动强度的效果。
The utility model discloses a punching machine with automatic continuous punching function, which belongs to the technical field of punching punching machines. , the upper end of the frame is also provided with a driving mechanism capable of driving the punch to slide downward, a horizontally arranged workbench is fixedly connected to the bottom of the frame corresponding to the punch, and the bottom of the frame corresponding to the workbench is along its length direction A rack is fixedly connected, the upper side of the worktable is slidingly connected with a bearing plate along its length direction, the bearing plate is rotatably connected with a missing gear engaged with the rack, and one end of the missing gear shaft is fixed with a driving missing gear A rotating servo motor, the holding plate is provided with a clamping component for clamping the plate. The utility model realizes the effect of reducing the labor intensity of workers by automatically punching the plate at a constant distance.
Description
技术领域technical field
本实用新型涉及冲压机冲孔的技术领域,尤其是涉及一种带有自动连续冲孔功能的冲压机。The utility model relates to the technical field of punching by punching machines, in particular to a punching machine with automatic continuous punching function.
背景技术Background technique
冲压机是通过电动机驱动飞轮,并通过离合器,传动齿轮带动曲柄连杆机构使滑块上下运动,带动拉伸模具对钢板成型。其工作原理一般是通过模具在冲压动力的作用下带动上模与下模的开合而将其之间的原材料进行裁切、冲孔、拉伸等定形,形成冲压件。The punching machine drives the flywheel through the motor, and drives the crank connecting rod mechanism through the clutch and transmission gear to move the slider up and down, and drives the drawing die to form the steel plate. The working principle is generally that the mold drives the upper mold and the lower mold to open and close under the action of the stamping power, and the raw materials between them are cut, punched, stretched, etc. to form a stamping part.
现有可参考专利申请号为CN201821399370.7的中国实用新型专利,公开了一种板材冲压机,涉及板材加工技术领域,包括工作台,所述工作台包括下基板和上基板,所述下基板和上基板之间固定连接支撑杆,所述上基板下方固定连接液压杆,所述下基板上方固定连接下模座和下模,上述实用新型结构简单,操作便捷,通过设置凹模与凸模的配合运动,实现产品的成型,通过设置凸轮驱动结构与顶杆,可以实现产品与凸模的分离,便于工人取件,提高了工作效率,维护方便。The existing Chinese utility model patent with patent application number CN201821399370.7 is disclosed, which discloses a plate punching machine, which relates to the technical field of plate processing, and includes a workbench, the workbench includes a lower substrate and an upper substrate, and the lower substrate The support rod is fixedly connected with the upper base plate, the hydraulic rod is fixedly connected below the upper base plate, and the lower die base and the lower die are fixedly connected above the lower base plate. The above-mentioned utility model has a simple structure and convenient operation. The cooperating movement of the machine can realize the molding of the product. By setting the cam drive structure and the ejector rod, the separation of the product and the punch can be realized, which is convenient for workers to take the parts, improves the work efficiency and facilitates maintenance.
但是上述现有技术方案存在以下缺陷:当对板材进行冲孔时,均需要工人先推动工件至冲压位置,然后随着凹模与凸模配合运动从而对工件进行冲孔,但是当需要定距连续多次冲孔时,则需要工人多次推动工件移动,从而增加工人的劳动强度。However, the above-mentioned prior art solutions have the following defects: when punching the plate, workers are required to push the workpiece to the punching position first, and then the workpiece is punched with the cooperating movement of the concave die and the punch, but when a fixed distance is required When punching holes for many times in a row, the worker needs to push the workpiece to move many times, thereby increasing the labor intensity of the worker.
实用新型内容Utility model content
本实用新型的目的是提供一种带有自动连续冲孔功能的冲压机,达到能够自动对板材进行连续定距冲孔进而降低工人劳动强度的有益效果。The purpose of the utility model is to provide a punching machine with the function of automatic continuous punching, which achieves the beneficial effect of automatically punching the plate at a constant distance and thereby reducing the labor intensity of workers.
本实用新型的上述发明目的是通过以下技术方案得以实现的:The above-mentioned purpose of the present invention is achieved through the following technical solutions:
一种带有自动连续冲孔功能的冲压机,包括竖直设置的机架,所述机架上端滑移有竖直设置的冲头,机架上端还设置有能够驱动冲头向下滑移的驱动组件,所述机架对应冲头的下方固接有水平设置的工作台,所述机架对应工作台的下方沿其长度方向固接有一齿条,所述工作台上侧沿其长度方向滑移连接有一承接板,所述承接板转动连接有啮合于齿条的缺齿轮,所述缺齿轮转轴一端固接有驱动缺齿轮转动的伺服电机,所述承接板上设置有夹持板材的夹持组件。A punching machine with automatic continuous punching function includes a vertically arranged frame, the upper end of the frame is slid with a vertically arranged punch, and the upper end of the frame is also provided with a punch capable of driving the punch to slide down The drive assembly, a horizontally arranged workbench is fixed below the frame corresponding to the punch, a rack is fixed along the length direction below the frame corresponding to the workbench, and the upper side of the workbench is along its length. There is a bearing plate connected to the direction sliding, the bearing plate is rotatably connected with a missing gear meshed with the rack, one end of the missing gear shaft is fixed with a servo motor that drives the missing gear to rotate, and the bearing plate is provided with a clamping plate clamping components.
通过采用上述技术方案,先将板材放置到承接板上,通过夹持组件将板材进行夹持,然后开启伺服电机,伺服电机驱动缺齿轮转动,当缺齿轮轮齿转动到与齿条啮合的状态时,从而能够带动承接板沿工作台长度方向在工作台上滑移,带动板材向前移动,当缺齿轮轮齿转动到不与齿条啮合的状态时,承接板停止滑移,此时冲头向下运动,从而对钢板进行冲孔,随着缺齿轮轮齿继续转动至与齿条啮合的状态时,承接板继续在工作台上滑移,从而带动板材继续向前移动,进而冲头能够对板材进行下一次冲孔,通过缺齿轮在齿条上的移动从而达到对板材连续冲孔的效果。By adopting the above technical solution, the plate is first placed on the receiving plate, the plate is clamped by the clamping component, and then the servo motor is turned on, and the servo motor drives the missing gear to rotate. When the missing gear teeth rotate to the state of meshing with the rack At this time, the receiving plate can be driven to slide on the table along the length direction of the table, and the plate can be driven to move forward. The head moves downward to punch the steel plate. As the missing gear teeth continue to rotate to the state of meshing with the rack, the receiving plate continues to slide on the worktable, thereby driving the plate to continue to move forward, and then the punch The plate can be punched for the next time, and the effect of continuous punching of the plate can be achieved by the movement of the missing gear on the rack.
本实用新型进一步设置为:所述工作台两侧沿其长度方向均开设有一纵切面呈T型的滑槽,所述承接板两侧对应于滑槽的位置均固接有一能够滑移连接于滑槽内的滑条。The utility model is further configured as follows: both sides of the working table are provided with a T-shaped chute along its length direction, and both sides of the receiving plate are fixedly connected to the positions corresponding to the chute, which can be slidably connected to the Slider inside the chute.
通过采用上述技术方案,滑条与滑槽相适配能够防止承接板在滑移过程中发生位置的偏移。By adopting the above technical solution, the matching of the sliding bar and the sliding groove can prevent the positional deviation of the receiving plate during the sliding process.
本实用新型进一步设置为:所述夹持组件包括设置于承接板两端的限位板,所述承接板内部转动连接有一对丝螺杆,所述对丝螺杆轴线方向平行于承接板长度方向,两所述限位板下端分别螺纹连接于对丝螺杆两端的相反的螺纹段,所述对丝螺杆一端还固接有一驱动对丝螺杆转动的驱动机构。The utility model is further configured as follows: the clamping assembly includes limit plates arranged at both ends of the receiving plate, a pair of wire screws are rotatably connected inside the receiving plate, the axis direction of the pair of wire screws is parallel to the length direction of the receiving plate, and the two The lower ends of the limiting plates are respectively threadedly connected to opposite thread segments at both ends of the paired wire screw, and one end of the paired wire screw is also fixedly connected with a driving mechanism for driving the paired wire screw to rotate.
通过采用上述技术方案,驱动机构能够驱动对丝螺杆沿其轴线方向转动,从而能够带动两限位板趋向靠近的方向移动,进而能够实现调节两限位板之间的间距,进而能够使两限位板之间能够夹持不同长度的板材。By adopting the above technical solution, the driving mechanism can drive the thread-aligning screw to rotate along its axis direction, so as to drive the two limit plates to move in the direction of approaching, thereby realizing the adjustment of the distance between the two limit plates, thereby enabling the two limit plates to move toward each other. Plates of different lengths can be clamped between the plates.
本实用新型进一步设置为:所述驱动机构包括固接于对丝螺杆一端的蜗轮,所述承接板一端固接有能够啮合于蜗轮的蜗杆。The utility model is further configured as follows: the driving mechanism comprises a worm wheel fixed to one end of the thread-aligning screw rod, and one end of the receiving plate is fixed to a worm that can be engaged with the worm wheel.
通过采用上述技术方案,转动蜗杆能够驱动蜗轮转动从而能够带动蜗轮转动,从而能够带动对丝螺杆转动,且蜗轮与蜗杆配合具有自锁性。By adopting the above technical solution, the rotating worm can drive the worm wheel to rotate, thereby driving the worm wheel to rotate, thereby driving the thread-pairing screw to rotate, and the cooperation between the worm wheel and the worm has self-locking properties.
本实用新型进一步设置为:两所述限位板相互靠近的一侧分别开设有一夹持槽,两所述夹持槽内均竖直滑移连接有一水平设置的压板,两所述限位板上侧分别螺纹连接有一竖直设置的顶紧螺栓,两所述顶紧螺栓的下端分别能够延伸至各对应夹持槽内且转动连接于各压板的上侧。The utility model is further configured as follows: a clamping groove is respectively provided on the side of the two limiting plates that are close to each other, and a horizontally arranged pressure plate is vertically slidingly connected in the two clamping grooves, and the two limiting plates The upper sides are respectively connected with a vertically arranged jacking bolt, and the lower ends of the two jacking bolts can respectively extend into the corresponding clamping grooves and are rotatably connected to the upper sides of the pressing plates.
通过采用上述技术方案,当限位板将板材两端夹持住后,向下转动两顶紧螺栓,使两压板下侧均能够紧密抵接于板材的两端的上侧,从而能够通过调节两顶紧螺栓来适用于压紧不同厚度的板材。By adopting the above technical solution, after the limiting plate clamps the two ends of the plate, the two tightening bolts are turned downward, so that the lower sides of the two pressure plates can be in close contact with the upper sides of the two ends of the plate. The top bolt is suitable for pressing plates of different thicknesses.
本实用新型进一步设置为:两所述夹持槽相互靠近的一侧沿垂直于限位板长度方向均开设有一纵切面呈T型的的滑移槽,两所述压板两端分别固接有一能够滑移连接于各对应滑移槽内的滑移条。The utility model is further arranged as follows: one side of the two clamping grooves that are close to each other is provided with a sliding groove with a T-shaped longitudinal section along the length direction perpendicular to the length of the limiting plate, and two ends of the two pressing plates are respectively fixed with a sliding groove. The sliding bars in the corresponding sliding grooves can be slidably connected.
通过采用上述技术方案,滑移条与滑移槽配合能够防止压板在通槽内滑移过程中发生位置的偏移。By adopting the above technical solution, the cooperation between the sliding bar and the sliding groove can prevent the positional deviation of the pressing plate during the sliding process in the through groove.
本实用新型进一步设置为:所述承接板上侧对应冲头的下方竖直开设有一沿承接板长度方向设置的竖槽,所述竖槽内竖直滑移连接有一沿竖槽长度方向设置的缓冲板,所述缓冲板与所述竖槽之间竖直设置有多个常态下能够推动缓冲板上侧与承接板上侧平齐的缓冲弹簧。The utility model is further configured as follows: a vertical groove arranged along the length direction of the receiving plate is vertically opened below the corresponding punch on the upper side of the receiving plate, and a vertical sliding connection in the vertical groove is arranged along the length direction of the vertical groove. A buffer plate, a plurality of buffer springs that can push the upper side of the buffer plate to be flush with the upper side of the receiving plate under normal conditions are vertically arranged between the buffer plate and the vertical slot.
通过采用上述技术方案,当冲头向下运动对板材进行冲孔时,缓冲板因受到冲头瞬间的冲击力从而沿竖槽内向下滑移,此时缓冲弹簧被压缩,从而对冲头瞬间的冲击力进行缓冲,当冲孔完成后,随着缓冲弹簧恢复为常态的过程中,能够推动缓冲板向上运动从而能够使缓冲板上侧与承接板上侧平齐。By adopting the above technical solution, when the punch moves downward to punch the plate, the buffer plate slides down along the vertical groove due to the instantaneous impact force of the punch, and the buffer spring is compressed at this time, so that the impact of the punch is instantaneous. After the punching is completed, as the buffer spring returns to the normal state, it can push the buffer plate to move upward so that the upper side of the buffer plate can be flush with the upper side of the receiving plate.
综上所述,本实用新型的有益技术效果为:To sum up, the beneficial technical effects of the present utility model are:
1.通过采用上述技术方案,先将板材放置到承接板上,通夹持组件将板材进行夹持,然后开启伺服电机,伺服电机驱动缺齿轮转动,当缺齿轮轮齿转动到与齿条啮合的状态时,从而能够带动承接板沿工作台长度方向在工作台上滑移,带动板材向前移动,当缺齿轮轮齿转动到不与齿条啮合的状态时,承接板停止滑移,此时驱动机构驱动冲头下降,从而对钢板进行冲孔,随着缺齿轮轮齿继续转动至与齿条啮合的状态时,承接板继续在工作台上滑移,从而带动板材继续向前移动,进而冲头能够对板材进行下一次冲孔,通过缺齿轮在齿条上的移动从而达到对板材连续冲孔的效果;1. By adopting the above technical solutions, first place the plate on the receiving plate, clamp the plate through the clamping component, then turn on the servo motor, the servo motor drives the missing gear to rotate, and when the missing gear teeth rotate to mesh with the rack In this state, the receiving plate can be driven to slide on the table along the length direction of the table, and the plate can be driven to move forward. When the driving mechanism drives the punch down, the steel plate is punched. As the missing gear teeth continue to rotate to the state of meshing with the rack, the receiving plate continues to slide on the worktable, thereby driving the plate to continue to move forward. Then the punch can punch the plate next time, and the effect of continuous punching of the plate can be achieved by the movement of the missing gear on the rack;
2.通过设置有夹持组件,驱动机构能够驱动对丝螺杆沿其轴线方向转动,从而能够带动两限位板趋向靠近离的方向移动,进而能够实现调节两限位板之间的间距,进而能够使两限位板之间能够夹持不同宽度的板材;2. By being provided with a clamping assembly, the driving mechanism can drive the aligning screw to rotate along its axis direction, so as to drive the two limit plates to move in the direction of approaching and away from each other, so as to realize the adjustment of the distance between the two limit plates, and then It can clamp plates of different widths between the two limit plates;
3.通过设置有压板,当两限位板将板材夹持住后,向下转动两顶紧螺栓,使压板下侧能够紧密抵接于板材的上侧,从而能够通过调节顶紧螺栓来适用于压紧不同厚度的板材。3. By setting the pressure plate, after the two limit plates clamp the plate, turn the two top bolts downward, so that the lower side of the pressure plate can be closely contacted with the upper side of the plate, so that it can be applied by adjusting the top bolts. For pressing plates of different thicknesses.
附图说明Description of drawings
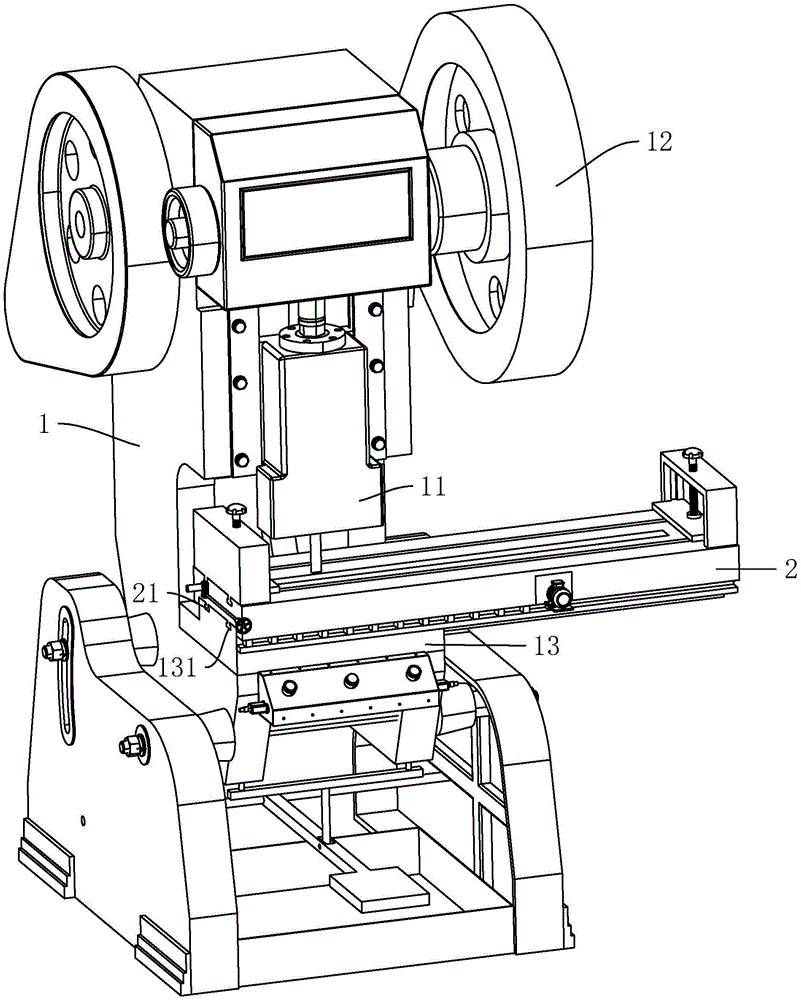
图1是本实施例的整体结构的示意图;Fig. 1 is the schematic diagram of the overall structure of this embodiment;
图2是本实施例中缺齿轮结构的示意图;Fig. 2 is the schematic diagram of missing gear structure in the present embodiment;
图3是本实施例中限位板结构的示意图;3 is a schematic diagram of the structure of the limiting plate in this embodiment;
图4是图3中A部的局部放大示意图;Fig. 4 is the partial enlarged schematic diagram of A part in Fig. 3;
图5是本实施例中缓冲板结构的示意图。FIG. 5 is a schematic diagram of the structure of the buffer plate in this embodiment.
图中,1、机架;11、冲头;12、驱动组件;13、工作台;131、滑槽;132、齿条;2、承接板;21、滑条;22、缺齿轮;23、伺服电机;24、容纳槽;25、竖槽;26、缓冲板;27、缓冲弹簧;3、对丝螺杆;31、蜗轮;32、蜗杆;33、手轮;4、限位板;41、夹持槽;411、滑移槽;42、压板;421、滑移条;5、顶紧螺栓。In the figure, 1, frame; 11, punch; 12, drive assembly; 13, worktable; 131, chute; 132, rack; 2, receiving plate; 21, slider; 22, missing gear; 23, Servo motor; 24, accommodating slot; 25, vertical slot; 26, buffer plate; 27, buffer spring; 3, threaded screw; 31, worm gear; 32, worm; 33, hand wheel; 4, limit plate; 41, Clamping groove; 411, sliding groove; 42, pressing plate; 421, sliding bar; 5, top tightening bolt.
具体实施方式Detailed ways
以下结合附图对本实用新型作进一步详细说明。The present utility model will be described in further detail below in conjunction with the accompanying drawings.
参照图1,一种带有自动连续冲孔功能的冲压机,包括竖直设置的机架1,机架1的上端滑移有竖直设置的冲头11,机架1上端还设置有能够驱动冲头11向下滑移的驱动组件12(此处为现有技术不再赘述),机架1对应冲头11的下方固接有水平设置的工作台13,工作台13上侧沿其长度方向滑移连接有一承接板2,工作台13两侧沿其长度方向均开设有一纵切面呈T型的滑槽131,承接板2两侧对应于滑槽131的位置均固接有一能够滑移连接于滑槽131内的滑条21,滑条21与滑槽131配合从而能够防止承接板2在滑移过程中发生位置的偏移。1, a punching machine with automatic continuous punching function includes a vertically arranged frame 1, the upper end of the frame 1 slides with a vertically arranged
参照图2,工作台13一侧对应承接板2的下方沿其长度方向固接有一齿条132,承接板2下侧对应齿条132的位置转动连接一有啮合于齿条132的缺齿轮,承接板2一侧对应缺齿轮22的位置还固接有一能够驱动缺齿轮22转动的伺服电机23,伺服电机23的输出轴与缺齿轮22的转轴固接。工作时,先开启伺服电机23,伺服电机23能够驱动缺齿轮22转动,当缺齿轮22轮齿转动到与齿条132啮合的状态时,从而能够带动承接板2沿工作台13长度方向在工作台13上滑移,带动板材向前移动,当缺齿轮22轮齿转动到不与齿条132啮合的状态时,承接板2停止滑移,同时冲头11向下运动,从而对钢板进行冲孔一次,随着缺齿轮22轮齿继续转动至与齿条132啮合的状态时,承接板2继续在工作台13上滑移,从而带动板材继续向前移动,直至缺齿轮22轮齿转动到不与齿条132啮合的状态时,承接板2停止滑移,同时冲头11向下运动从而能够对板材进行下一次冲孔。Referring to FIG. 2 , a
参照图3和图4,夹持组件包括滑移连接于承接板2两端的限位板4,两限位板4的长度方向均垂直于承接板2的长度方向设置,承接板2上表面两侧沿其长度均竖直开设有一纵切面呈T型的容纳槽24,一侧容纳槽24内转动连接有一对丝螺杆3,对丝螺杆3轴线方向平行于容纳槽24长度方向,两限位板4下端均螺纹连接于对丝螺杆3两端的相反的螺纹段,两限位板4能够随对丝螺杆3的转动而趋向相互靠近的方向滑移,对丝螺杆3一端还固接有一驱动对丝螺杆3转动的驱动机构。驱动机构包括固接于对丝螺杆3一端的蜗轮31,蜗轮31与对丝螺杆3同轴线设置,承接板2对应蜗轮31的位置还固接有一能够啮合于蜗轮31的蜗杆32,蜗杆32的转轴一端固接有同轴线设置的手轮33。两限位板4相互靠近的一侧分别开设有一夹持槽41,两夹持槽41呈框型结构且开口相对设置,两夹持槽41下侧均延伸出限位板4的下侧,各夹持槽41内均竖直滑移连接有一水平设置的压板42,两夹持槽41相互靠近的一侧沿垂直于限位板4长度方向均开设有一纵切面呈T型的滑移槽411,压板42两端水平固接有一能够分别滑移连接于滑移槽411内的滑移条421,滑移槽411与滑移条421配合从而能够防止压板42在夹持槽41内滑移过程中发生位置的偏移。两限位板4的上侧分别螺纹连接有一竖直设置的顶紧螺栓5,两顶紧螺栓5的下端分别能够延伸至各对应夹持槽41内且转动连接于压板42上侧。先将板材放置于承接板2上侧的两限位板4之间,然后转动手轮33能够带动蜗杆32转动,从而能够驱动蜗轮31转动,从而能够带动对丝螺杆3转动,从而能够带动两限位板4趋向相互靠近的方向移动,直至两限位板4的两夹持槽41相互靠近的一侧分别紧密抵接于板材的两端,通过调节两限位板4之间的间距,进而能够使两限位板4之间能够夹持不同宽度的板材,之后向下转动两顶紧螺栓5,使两压板42下侧均能够紧密抵接于板材的两端的上侧,从而能够通过调节两顶紧螺栓5来适用于压紧不同厚度的板材。3 and 4, the clamping assembly includes limit plates 4 slidably connected to both ends of the receiving
参照图5,承接板2上侧对应冲头11的下方竖直开设有一竖槽25,竖槽25的长度方向与承接板2的长度方向相同,竖槽25内均竖直滑移连接有一缓冲板26,缓冲板26的长度方向与竖槽25的长度方向相同,竖槽25与缓冲板26之间竖直设置有多个常态下能够推动缓冲板26上侧与承接板2上侧平齐的缓冲弹簧27,各缓冲弹簧27的一端均固接于承接板2的下侧且其另一端均固接于竖槽25的底侧。当冲头11向下运动对板材进行冲孔时,缓冲板26因受到冲头11瞬间的冲击力从而沿竖槽25内向下滑移,此时缓冲弹簧27被压缩,从而对冲头11瞬间的冲击力进行缓冲,当冲孔完成后,随着缓冲弹簧27恢复为常态的过程中,能够推动缓冲板26向上运动从而能够使缓冲板26上侧与承接板2上侧平齐。Referring to FIG. 5 , a
本实施例的实施原理为:先将板材放置于承接板2上侧的两限位板4之间,先将板材放置于承接板2上侧的两限位板4之间,然后转动手轮33能够带动蜗杆32转动,从而能够驱动蜗轮31转动,从而能够带动对丝螺杆3转动,从而能够带动两限位板4趋向相互靠近的方向移动,直至两限位板4的两夹持槽41相互靠近的一侧分别紧密抵接于板材的两端,从而完成板材的夹持,之后向下转动两顶紧螺栓5,使两压板42下侧均能够紧密抵接于板材的两端的上侧,从而完成板材的压紧;将板材固定在承接板2上后,然后开启伺服电机23,伺服电机23能够驱动缺齿轮22转动,当缺齿轮22轮齿转动到与齿条132啮合的状态时,从而能够带动承接板2沿工作台13长度方向在工作台13上滑移,带动板材向前移动,直至缺齿轮22轮齿转动到不与齿条132啮合的状态时,承接板2停止滑移,同时冲头11向下运动进行冲孔一次,缓冲板26因受到冲头11瞬间的冲击力从而沿竖槽25向下滑移,此时缓冲弹簧27被压缩,从而对冲头11瞬间的冲击力进行缓冲,当冲孔完成后,随着缓冲弹簧27恢复为常态的过程中,能够推动缓冲板26向上运动从而能够使缓冲板26上侧与承接板2上侧平齐;随着缺齿轮22轮齿继续转动至与齿条132啮合的状态时,承接板2继续在工作台13上滑移,从而带动板材继续向前移动,直至缺齿轮22轮齿转动到不与齿条132啮合的状态时,承接板2停止滑移,同时冲头11向下运动从而能够对板材进行下一次冲孔,进而实现自动对板材进行连续定距冲孔。The implementation principle of this embodiment is as follows: first place the plate between the two limit plates 4 on the upper side of the receiving
本具体实施方式的实施例均为本实用新型的较佳实施例,并非依此限制本实用新型的保护范围,故:凡依本实用新型的结构、形状、原理所做的等效变化,均应涵盖于本实用新型的保护范围之内。The examples of this specific embodiment are all preferred embodiments of the present invention, and are not intended to limit the protection scope of the present invention. Therefore: all equivalent changes made according to the structure, shape and principle of the present invention are not It should be covered within the protection scope of the present invention.
Claims (7)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922039688.5U CN210907657U (en) | 2019-11-22 | 2019-11-22 | A punching machine with automatic continuous punching function |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201922039688.5U CN210907657U (en) | 2019-11-22 | 2019-11-22 | A punching machine with automatic continuous punching function |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210907657U true CN210907657U (en) | 2020-07-03 |
Family
ID=71359249
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201922039688.5U Expired - Fee Related CN210907657U (en) | 2019-11-22 | 2019-11-22 | A punching machine with automatic continuous punching function |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210907657U (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112338045A (en) * | 2020-10-15 | 2021-02-09 | 奚尹莉 | Punching machine tool with adjustable pitch |
| CN112453252A (en) * | 2020-10-29 | 2021-03-09 | 张�杰 | Iron ladle stamping equipment |
| CN113414287A (en) * | 2021-07-14 | 2021-09-21 | 刘秀莲 | Steel strip and manufacturing process thereof |
| CN114289607A (en) * | 2022-03-09 | 2022-04-08 | 河南英邦冷弯科技有限公司 | Online continuous punching device in cold roll forming |
| CN117816834A (en) * | 2024-03-05 | 2024-04-05 | 成都德安金属制品有限公司 | A punching device for annular workpiece |
-
2019
- 2019-11-22 CN CN201922039688.5U patent/CN210907657U/en not_active Expired - Fee Related
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112338045A (en) * | 2020-10-15 | 2021-02-09 | 奚尹莉 | Punching machine tool with adjustable pitch |
| CN112453252A (en) * | 2020-10-29 | 2021-03-09 | 张�杰 | Iron ladle stamping equipment |
| CN113414287A (en) * | 2021-07-14 | 2021-09-21 | 刘秀莲 | Steel strip and manufacturing process thereof |
| CN114289607A (en) * | 2022-03-09 | 2022-04-08 | 河南英邦冷弯科技有限公司 | Online continuous punching device in cold roll forming |
| CN114289607B (en) * | 2022-03-09 | 2022-05-27 | 河南英邦冷弯科技有限公司 | Online continuous punching device in cold roll forming |
| CN117816834A (en) * | 2024-03-05 | 2024-04-05 | 成都德安金属制品有限公司 | A punching device for annular workpiece |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN112845894B (en) | Method capable of quickly fixing stamping die | |
| CN218697192U (en) | Sheet metal part flanging and polishing device | |
| CN107282777B (en) | A kind of die adjustment mechanism | |
| CN115889569A (en) | Aluminum template stamping equipment | |
| CN220880259U (en) | Board clamping structure for numerical control punch | |
| CN209407186U (en) | A traction device for an open fixed table press | |
| CN211915100U (en) | A new type of channel steel press brake | |
| CN220049535U (en) | Hardware bending device | |
| CN220445802U (en) | Adjustable positioning device for production and processing of mechanical parts | |
| CN217474611U (en) | Portable multifunctional adjustable die | |
| CN217667352U (en) | Cabinet panel beating welding set | |
| CN218983385U (en) | A sealing plate cutting machine | |
| CN206492805U (en) | Sheet material bar folder | |
| CN116900159A (en) | Hardware mold with automatic feeding function | |
| CN219724288U (en) | Inclined plane punching die for automobile part | |
| CN219985896U (en) | Punch press with direction correcting structure | |
| CN217913138U (en) | Numerical control cutting positioning mechanism | |
| CN220560359U (en) | Sheet metal part autorotation riveting device | |
| CN222711318U (en) | A new type of welding tool | |
| CN217019408U (en) | Multi-functional frock of ready-package | |
| CN219236271U (en) | Adjustable die machining clamp | |
| CN219746539U (en) | An electro-galvanized steel plate cutting machine | |
| CN115846487B (en) | Lateral stamping device for automobile parts and application method thereof | |
| CN221715425U (en) | Chair production punch press with pay-off positioning mechanism | |
| CN221064123U (en) | A stamping die for front and rear panels of refrigerator with discharge function |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20200703 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |