CN210708135U - Vertical film glove bagging machine - Google Patents
Vertical film glove bagging machine Download PDFInfo
- Publication number
- CN210708135U CN210708135U CN201921451712.XU CN201921451712U CN210708135U CN 210708135 U CN210708135 U CN 210708135U CN 201921451712 U CN201921451712 U CN 201921451712U CN 210708135 U CN210708135 U CN 210708135U
- Authority
- CN
- China
- Prior art keywords
- film
- bag
- roller
- pair
- vertical
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000007789 sealing Methods 0.000 claims abstract description 30
- 239000002699 waste material Substances 0.000 claims abstract description 29
- 239000000463 material Substances 0.000 claims abstract description 9
- 239000010408 film Substances 0.000 claims description 165
- 238000003825 pressing Methods 0.000 claims description 14
- 239000010409 thin film Substances 0.000 claims description 11
- 238000010438 heat treatment Methods 0.000 claims description 10
- 230000003014 reinforcing effect Effects 0.000 claims description 9
- 230000000149 penetrating effect Effects 0.000 claims description 5
- 230000000712 assembly Effects 0.000 claims description 4
- 238000000429 assembly Methods 0.000 claims description 4
- 229920001971 elastomer Polymers 0.000 claims description 4
- 229920001342 Bakelite® Polymers 0.000 claims description 3
- 239000004637 bakelite Substances 0.000 claims description 3
- 238000005520 cutting process Methods 0.000 claims description 3
- 238000009413 insulation Methods 0.000 claims description 2
- 239000012528 membrane Substances 0.000 description 26
- 238000000034 method Methods 0.000 description 6
- 230000006835 compression Effects 0.000 description 3
- 238000007906 compression Methods 0.000 description 3
- 229920001296 polysiloxane Polymers 0.000 description 3
- VYPSYNLAJGMNEJ-UHFFFAOYSA-N Silicium dioxide Chemical compound O=[Si]=O VYPSYNLAJGMNEJ-UHFFFAOYSA-N 0.000 description 2
- 231100000252 nontoxic Toxicity 0.000 description 2
- 230000003000 nontoxic effect Effects 0.000 description 2
- 230000009965 odorless effect Effects 0.000 description 2
- 229920006280 packaging film Polymers 0.000 description 2
- 239000012785 packaging film Substances 0.000 description 2
- 238000004806 packaging method and process Methods 0.000 description 2
- 239000000741 silica gel Substances 0.000 description 2
- 229910002027 silica gel Inorganic materials 0.000 description 2
- 230000001360 synchronised effect Effects 0.000 description 2
- 239000004698 Polyethylene Substances 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000015572 biosynthetic process Effects 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000012858 packaging process Methods 0.000 description 1
- 238000012856 packing Methods 0.000 description 1
- -1 polyethylene Polymers 0.000 description 1
- 229920000573 polyethylene Polymers 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 125000006850 spacer group Chemical group 0.000 description 1
Images




Landscapes
- Containers And Plastic Fillers For Packaging (AREA)
Abstract
The utility model relates to a vertical film glove bagging machine, which comprises a frame, a glove waste tearing mechanism, a film feeding mechanism, a bag forming mechanism and a vertical bag feeding mechanism, wherein the glove waste tearing mechanism, the film feeding mechanism, the bag forming mechanism and the vertical bag feeding mechanism are arranged on the frame; the film feeding mechanism is used for guiding the film to the bag forming mechanism from two film rolls positioned at two ends of the rack; the bag forming mechanism is located in the middle of the rack and used for forming two films from the two film rolls into a bag with an upper opening and sealing the bag, the vertical bag feeding mechanism comprises a bag feeding groove, a material clamping assembly and a bag feeding assembly, the bag feeding groove extends into the space between the two films of the bag to be formed, the material clamping assembly is used for transferring the film gloves to the upper portion of the bag feeding groove from the glove waste tearing mechanism, and the bag feeding assembly is installed right above the bag feeding groove and used for feeding the film gloves into the bag.
Description
Technical Field
The utility model relates to a equipment for packing field specifically relates to a vertical film gloves sack filling machine.
Background
The disposable film gloves are made of nontoxic and odorless polyethylene materials, and are nontoxic, harmless, odorless, firm and durable. Most of the existing film gloves are packaged by manual operation, which causes great labor intensity, easy fatigue and lower efficiency. Chinese patent application CN206664999U discloses an automatic glove bagging machine, which is operated to remove glove waste, transport the glove to the bottom, and lay a layer of packaging film, and then finish the glove packaging by a heat sealing device, and has the following disadvantages of 1) low automation degree, and 2) waste of a large amount of packaging film.
Disclosure of Invention
The utility model aims at providing a vertical film gloves sack filling machine to solve above-mentioned technical problem. Therefore, the utility model discloses a specific technical scheme as follows:
a vertical type film glove bagging machine comprises a rack, and a glove waste tearing mechanism, a film feeding mechanism, a bag forming mechanism and a vertical bag feeding mechanism which are arranged on the rack, wherein the glove waste tearing mechanism is arranged at the feeding end of the rack and is used for removing waste of a whole stack of semi-finished film gloves to obtain film gloves to be packaged, and the semi-finished film gloves comprise film gloves which are connected together in a virtual mode and waste materials which wrap the film gloves; the film feeding mechanism is used for guiding the film to the bag forming mechanism from two film rolls positioned at two ends of the rack; the bag forming mechanism is positioned in the middle of the rack and used for forming two films from the two film rolls into a bag with an upper opening, sealing the upper opening of the bag with the thin film gloves and cutting off the bag with the thin film gloves, the vertical bag feeding mechanism comprises a bag feeding groove, a material clamping component and a bag feeding component, the bag feeding groove extends into the space between the two films of the bag to be formed, the material clamping component is used for transferring the thin film gloves from the glove waste tearing mechanism to the upper portion of the bag feeding groove, and the bag feeding component is positioned right above the bag feeding groove and used for feeding the thin film gloves into the bag.
Further, vertical film gloves sack filling machine still includes easy tear mouth forming mechanism, easy tear mouth forming mechanism arranges on the horizontal segment of film feeding mechanism for form the semicircular easy tear mouth on one of them membrane.
Further, easily tear a mouthful formation mechanism and include mount pad, bottom plate, cutter mount pad, semi-circular cutter, pillar, cylinder mount pad and cylinder, bottom plate fixed mounting be in on the mount pad and with the mount pad forms a clearance that supplies the membrane to pass through, the bottom plate is equipped with the semi-circular cutter passageway that runs through from top to bottom, semi-circular cutter fixed mounting is in the cutter mount pad and aims at semi-circular cutter passageway, the cylinder mount pad passes through the pillar is installed on the bottom plate, the cylinder fixed mounting be in on the cylinder mount pad and its piston rod pass cylinder mount pad fixed connection in the cutter mount pad.
Furthermore, a rubber block is embedded on the upper surface of the cutter mounting seat and is positioned right below the semicircular cutter channel.
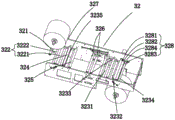
Further, send membrane mechanism including drawing membrane subassembly and symmetrical arrangement and be in draw two on membrane subassembly both sides and walk the membrane subassembly, it includes deflector roll one, conveying roller pair, swing tensioning roller mechanism, deflector roll two, deflector roll three and deflector roll four to walk the membrane subassembly, the conveying roller is to being rotatory by motor drive, swing tensioning roller mechanism is located conveying roller pair, deflector roll two and deflector roll three below, go into the sack and insert between two deflector rolls of walking the membrane subassembly, draw the membrane subassembly to include the membrane wheel pair of drawing, draw the membrane wheel pair down and drive the membrane drive mechanism that draws that the membrane wheel pair rotates is drawn to the membrane wheel pair and draw the membrane wheel pair down, bag forming mechanism is located draw the membrane wheel pair with draw between the membrane wheel pair down, the membrane is rolled up from the membrane and is expanded to pass through in proper order deflector roll one conveying roller pair the tensioning roller one of swing tensioning roller mechanism guide roll two, the tensioning roller two of tensioning roller of swing tensioning roller mechanism are drawn the membrane driving mechanism, The guide roller III, the guide roller IV, the film upwards-drawing wheel pair and the film downwards-drawing wheel pair.
Further, swing tensioning roller mechanism includes tensioning roller one, tensioning roller two, two tensioning curb plates, a tensioning pivot and a reinforcing plate, the tensioning pivot tensioning roller two and two the rectangle structure is assembled into to the tensioning curb plate, install in the frame at the both ends of tensioning pivot for this rectangle structure can wind the swing of tensioning pivot, reinforcing plate and tensioning roller one be on a parallel with tensioning roller two is installed in this rectangle structure, the reinforcing plate is located tensioning roller one with between the tensioning roller two.
The film walking assembly further comprises a clutch shaft, a clutch swing arm, a spring pressing block and a spring, wherein the clutch shaft is parallelly installed below the conveying roller pair, the lower end of the clutch swing arm is rotatably installed on the rack, a driven roller of the conveying roller pair is installed at the upper end of the clutch swing arm, the spring pressing block is installed on the rack, one end of the spring is abutted to the spring pressing block, the other end of the spring is abutted to the side face of the upper end of the clutch swing arm, and a groove matched with a notch of the clutch shaft is formed in one side, away from the spring, of the clutch swing arm.
Further, the film drawing driving mechanism comprises a motor, a main gear, an upper driven gear pair, a lower driven gear pair, an upper belt pulley, a lower belt pulley and a synchronous belt, wherein the main gear is installed on an output shaft of the motor, the upper driven gear pair and the lower driven gear pair are respectively and fixedly installed on rotating shafts of the upper film drawing wheel pair and the lower film drawing wheel pair, the main gear is meshed with one of the upper driven gear pair, the upper belt pulley is fixedly connected with the other one of the upper driven gear pair, the lower belt pulley is fixedly connected with one of the lower driven gear pair, and the synchronous belt is wound on the upper belt pulley and the lower belt pulley.
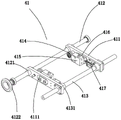
Further, sack forming mechanism indulges two and seals subassembly and a violently seal the subassembly about including, indulge and seal the subassembly and be located draw membrane wheel pair and draw down between the membrane wheel pair, violently seal the subassembly and be located draw down membrane wheel pair below, indulge and seal the subassembly and include mounting panel, gyro wheel, heating member, slider and cylinder, be equipped with an opening on the mounting panel, the cylinder with the gyro wheel is installed respectively on the mounting panel of open-ended both sides, the heating member passes through the thermal-insulated fixed mounting of bakelite circle and is in on the slider, the telescopic link fixed connection of cylinder the slider is in order to drive the heating member moves towards or keeps away from the gyro wheel.
Further, the longitudinal sealing assembly further comprises a width adjusting screw rod and a guide rod, the width adjusting screw rod is arranged at one end of the two mounting plates in a penetrating mode through an adjusting nut, and the guide rod is arranged at the other end of the two mounting plates in a penetrating mode through a linear bearing.
The utility model adopts the above technical scheme, the beneficial effect who has is: the utility model discloses compact structure, sack are sealed by two membrane edgewise and are formed, can not waste the membrane, and whole packaging process all goes on automatically, and production efficiency is big, has saved the labour greatly.
Drawings
To further illustrate the embodiments, the present invention provides the accompanying drawings. The accompanying drawings, which are incorporated in and constitute a part of this disclosure, illustrate embodiments of the invention and, together with the description, serve to explain the principles of the embodiments. With these references, one of ordinary skill in the art will appreciate other possible embodiments and advantages of the present invention. Elements in the figures are not drawn to scale and like reference numerals are generally used to indicate like elements.
Fig. 1 is a perspective view of the vertical film glove bagging machine of the present invention with one side panel removed to show the internal mechanism;
FIG. 2 is a perspective view of the glove waste removal mechanism of the vertical film glove bagging machine shown in FIG. 1;
FIG. 3 is a perspective view of a film feeding assembly of the film feeding mechanism of the vertical film glove bagging machine shown in FIG. 1;
FIG. 4 is a perspective view of a film drawing assembly of the film feeding mechanism of the vertical film glove bagging machine shown in FIG. 1;
fig. 5 is a perspective view of a longitudinal sealing assembly of the bag forming mechanism of the vertical film glove bag loader shown in fig. 1;
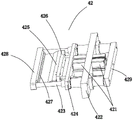
fig. 6 is a perspective view of the cross seal assembly of the bag forming mechanism of the vertical film glove bag loader shown in fig. 1;
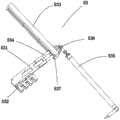
FIG. 7 is a perspective view of a gripper assembly of the vertical bag feeding mechanism of the vertical film glove bag filling machine of FIG. 1;
fig. 8 is a perspective view of a bag inlet assembly of the vertical bag inlet mechanism of the vertical film glove bag loader shown in fig. 1;
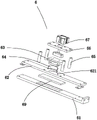
fig. 9 is an exploded perspective view of the easy-tear opening forming mechanism of the vertical film glove bag loader shown in fig. 1.
Detailed Description
The present invention will now be further described with reference to the accompanying drawings and detailed description.
As shown in fig. 1, the vertical film glove bagging machine comprises a frame 1, a glove waste tearing mechanism 2, a film feeding mechanism 3, a bag forming mechanism 4, a vertical bag feeding mechanism 5 and a control system, wherein the glove waste tearing mechanism 2, the film feeding mechanism 3, the bag forming mechanism 4 and the vertical bag feeding mechanism 5 are installed on the frame. The control system is used for controlling each mechanism to automatically operate so as to realize the automatic packaging of the thin film gloves. The control system may be a PLC-based automated control system, and the specific configuration thereof may be selected and set by those skilled in the art as required, and will not be described herein.
As shown in fig. 1 and 2, a glove waste tearing mechanism 2 is arranged at the feed end of the frame 1 for removing waste of a stack of semi-finished film gloves to obtain film gloves to be packaged, wherein the semi-finished film gloves comprise film gloves which are virtually joined together and waste which surrounds the film gloves. Specifically, the glove waste tearing mechanism 2 includes a receiver plate 21, a waste chute 22, a waste clamping assembly 23, a glove pressing assembly 24, a guide bar 25, and a tearing cylinder 26. The receiving plate 21 is used for receiving semi-finished film gloves. A scrap chute 22 is located below the jaws 231 of the scrap clamping assembly 23 for receiving scrap material. The scrap clamping assembly 23 includes left and right jaws 231 and left and right jaw cylinders 232, the jaw cylinders 232 driving the jaws 232 to clamp and unclamp. Glove compression assembly 24 may include a base plate 241, a compression block 242, a support plate 243, a cylinder mounting plate 244, and a compression cylinder 245. Protrusions are provided on the opposing surfaces of the base plate 241 and the press piece 242 to grip the glove. The pressing cylinder 245 drives the pressing block 242 to ascend or descend so as to loosen or press the gloves. The base plate 241 is slidably mounted on the guide bar 25 and fixedly connected to the piston rod of the tear cylinder 26. The glove waste process is that firstly the clamping jaw air cylinder 232 drives the clamping jaw 232 to clamp the waste part of the semi-finished film glove from two sides, meanwhile the pressing air cylinder 245 drives the pressing block 242 to press down to press the head part of the glove part of the semi-finished film glove, and then the tearing air cylinder 26 drives the base plate 241 to move away from the clamping jaw 232 to separate the waste from the glove.
As shown in fig. 1, 3 and 4, the film feeding mechanism 3 serves to guide the film from two film rolls 7 located at both ends of the frame 1 to the bag forming mechanism 4. Specifically, the film feeding mechanism 3 comprises a film drawing assembly 31 and two film moving assemblies 32 symmetrically arranged at two sides of the film drawing assembly 31. The film moving assembly 32 comprises a first guide roller 321, a conveying roller pair 322, a swinging tensioning roller mechanism, a second guide roller 324, a third guide roller 325 and a fourth guide roller 326. The conveying roller pair 322 is composed of a driving roller 3221 and a driven roller 3222, wherein one end of the driving roller 3221 is fixedly connected to an output shaft of the motor 327. The film passes between the driving roller 3221 and the driven roller 3222 and is nipped by the driving roller 3221 and the driven roller 3222, and is unwound from the film roll 7 by rotation of the motor 327. The swing tensioning roller mechanism is located below the conveying roller pair 322, the guide roller pair 324 and the guide roller pair 325, wherein the swing tensioning roller mechanism comprises a first tensioning roller 3231, a second tensioning roller 3232, two tensioning side plates 3233, a tensioning rotating shaft 3234 and a reinforcing plate 3235, and the tensioning rotating shaft 3234, the tensioning roller pair 3232 and the two tensioning side plates 3233 are assembled into a rectangular structure. Both ends of the tension rotating shaft 3234 are rotatably mounted on the frame 1 so that the rectangular structure can swing around the tension rotating shaft 3234. A reinforcing plate 3235 and a tension roller one 3231 are mounted in the rectangular structure parallel to the tension roller two 3232, the reinforcing plate 3235 being located between the tension roller one 3231 and said tension roller two 3232.
In addition, the film moving assembly 32 further comprises a clutch structure consisting of a clutch shaft 3281, a clutch swing arm 3282, a spring pressing block 3283 and a spring 3284. The clutch shaft 3281 is installed in parallel below the conveying roller pair 322, and an operation handle is fixed to one end thereof. The lower end of a clutch swing arm 3282 is rotatably installed on the machine frame 1, a driven roller 3222 of the conveying roller pair 322 is installed at the upper end of the clutch swing arm 3282, a spring pressing block 3283 is fixedly installed on the machine frame 1, one end of the spring 3284 is abutted against the side face of the spring pressing block, the other end of the spring 3284 is abutted against the side face of the upper end of the clutch swing arm 3282, and a groove matched with a notch of a clutch shaft 3281 is formed in the other side face, far away from the spring 3284. By operating the handle to rotate the clutch shaft 3281, the driven roller 3222 can be moved toward or away from the driving roller 3221, thereby clamping or releasing the film.
The film drawing assembly 31 comprises an upper film drawing wheel pair 311, a lower film drawing wheel pair 312 and a film drawing driving mechanism 313 for driving the upper film drawing wheel pair 311 and the lower film drawing wheel pair 312 to rotate. The bag forming mechanism 4 is located between a pair of draw-up film wheels 311 and a pair of draw-down film wheels 312. The film pulling-up wheel pair 311 is similar to the film pulling-down wheel pair 312 in structure, and includes a pair of rotating shafts and a pair of wheels fixed on the rotating shafts, the film passes through between the pair of wheels and is clamped with the pair of wheels, the rotating direction of the pair of wheels is opposite, and the film pulling is realized by the rotation of the pair of wheels.
The film-drawing driving mechanism 313 includes a motor 3131, a main gear 3132, an upper driven gear pair 3133, a lower driven gear pair 3134, an upper belt pulley 3135, a lower belt pulley 3136, and a timing belt 3137. A main gear 3132 is mounted on an output shaft of the motor 3131, an upper driven gear 3133 and a lower driven gear 3134 are fixedly mounted on rotating shafts of the upper and lower film pulling wheel pairs 311 and 312, respectively, the main gear 3132 is engaged with one of the upper driven gear 3133, an upper driven pulley 3135 is fixedly connected with the other of the upper driven gear 3133, the lower driven gear 3136 is fixedly connected with one of the lower driven gear 3134 (specifically, a lower driven gear on the same side as the upper driven gear connected with the upper driven gear 3135), and a timing belt 3137 is wound around the upper and lower driven gears 3135. The motor 3131 rotates, the main gear 3132 drives the upper driven gear pair 3133 to rotate relatively, so that the wheels of the upper membrane-drawing wheel pair 311 rotate relatively, and the upper belt pulley 3135, the lower belt pulley 3136 and the timing belt 3137 drive the lower driven gear pair 3134 to rotate relatively, so that the wheels of the lower membrane-drawing wheel pair 312 rotate relatively, and membrane drawing is achieved.
Preferably, the film drawing assembly 31 may further include an upper clutch structure and a lower clutch structure for moving the wheels of the upper film drawing wheel pair 311 and the lower film drawing wheel pair 312 toward or away from each other. An operating handle is fixedly arranged on a clutch shaft of the upper clutch structure and the lower clutch structure, and the wheels of the upper film-drawing wheel pair 111 and the wheels of the lower film-drawing wheel pair 112 can be clutched by rotating the operating handle.
Now, the working process of the film feeding mechanism 3 will be briefly described, 1, the preparation stage: the film is unwound from a film roll and sequentially passes through a guide roller I321, a conveying roller pair 322, a tension roller I3231 of a swinging tension roller mechanism 323, a guide roller II 324, a tension roller II 3232 of the swinging tension roller mechanism, a guide roller III 325, a guide roller IV 326, an upward film drawing wheel pair 311 and a downward film drawing wheel pair 312; 2. and (3) film feeding process: the motor 327 rotates to drive the film to be unwound from the film roll 7, the swinging tension roller mechanism 323 swings downwards to a preset position, the motor 327 stops, then the film pulling driving mechanism 313 drives the film pulling-up wheel pair 311 and the film pulling-down wheel pair 312 to rotate, the film is pulled to advance, in the film advancing process, after the swinging tension roller mechanism 323 is pulled back to the initial position, the motor of the film pulling driving mechanism 313 stops rotating, namely the film is conveyed in place, and the film conveying process is circularly carried out until the film is used up.
As shown in fig. 1, 5 and 6, a bag forming mechanism 4 is located in the middle of the frame for forming two films from two film rolls 7 into a bag having an upper opening and closing the upper opening of the bag with film gloves and cutting the bag. Specifically, the bag forming mechanism 4 includes two longitudinal sealing assemblies 41 and a transverse sealing assembly 42. Wherein, the longitudinal sealing component 41 is arranged between an upper film drawing wheel pair and a lower film drawing wheel pair of the film feeding mechanism 3, and the transverse sealing component 42 is arranged below the lower film drawing wheel pair. The longitudinal sealing assembly 41 may include a mounting plate 411, a width adjustment screw 412, a guide 413, a roller 414, a heating body 415, a slider 416, and a cylinder 417. The width adjusting screw 412 is arranged on one end of the mounting plates 411 of the left and right longitudinal sealing components through adjusting nuts 4121, and the guide rod 413 is arranged on the other end of the mounting plates 411 of the left and right longitudinal sealing components through a linear bearing 4131. One end of the width adjustment screw 412 is mounted with a hand wheel 4122, and by operating the hand wheel 4122, the distance between the two mounting plates 411 can be adjusted to fit a film of a corresponding width. An opening 4111 is formed in the mounting plate 411, the air cylinder 417 and the roller 414 are respectively mounted on the mounting plates on two sides of the opening 4111, the heating body 415 is fixedly mounted on the sliding block 416 through a bakelite ring in a heat insulation manner, and an expansion rod of the air cylinder 417 is fixedly connected with the sliding block 416 to drive the heating body 415 to move towards or away from the roller 414. The roller 414 is aligned with the wheels of the pair of upper film pulling wheels 311 and the pair of lower film pulling wheels 312. During operation, the left and right sides of the two films are clamped between the heating body 415 and the roller 414, and the films are longitudinally sealed in the advancing process under the action of the upward film pulling wheel pair 311 and the downward film pulling wheel pair 312.
It should be understood that the mounting plate 411 may be stationary with the width of the package constant, i.e., without the width adjustment mechanism of the width adjustment screw 412, the adjustment nut 4121, the hand wheel 4122, the guide rod 413, and the linear bearing 4131.
The transverse sealing assembly 42 comprises a double cylinder 421, a transverse sealing cylinder mounting plate 422, a guide rod 423, a cylinder push block 424, a transverse sealing cutter 425, a transverse sealing cutter mounting plate 426, a silicone strip 427, a silicone strip mounting plate 428 and a connecting plate 429. The transverse sealing cylinder mounting plate 422 is fixedly mounted on the frame 1, the double cylinders 421 are fixedly mounted on the opposite surface of the transverse sealing cylinder mounting plate 422, the guide rods 423 are movably arranged on the transverse sealing cylinder mounting plate 422 and the cylinder push block 424 in a penetrating manner, one end of each guide rod is fixedly connected to the connecting plate 429, the other end of each guide rod is fixedly connected to the silica gel strip mounting plate 428, the piston rod of one of the double cylinders 421 is fixedly connected to the connecting plate 429, the other piston rod of the one of the double cylinders 421 is fixedly connected to the cylinder push block 424, the transverse sealing cutter mounting plate 426 is fixedly mounted on the cylinder push block 424, the transverse sealing cutter 425 is fixedly mounted on the side, facing the silica gel strip 427. The double cylinder 421 pushes the cross sealing cutter 425 to move toward the silicone strip 427 to seal the upper opening of one bag and the lower opening of the next bag and separate the two bags.
As shown in fig. 1, 3, 7 and 8, the vertical bag feeding mechanism 5 includes a discharge platform 51, a bag feeding chute 52, a material clamping assembly 53 and a bag feeding assembly 54. The discharging platform 51 is positioned above the four guide rollers 326 of the film feeding mechanism 3 and is used for placing gloves to be bagged. The discharge platform 51 has an opening in the middle thereof, and the bag inlet 52 is fixedly installed in the opening and extends downward to be inserted between two films of the bag to be formed from between the two guide rollers 326. That is, the lower end of the pocket 52 is substantially aligned with the longitudinal seal assembly 41. It should be understood that the emptying platform 51 may also be formed integrally with the bag feeding groove 52. The clamping assembly 53 comprises a clamping jaw mounting plate 531, a clamping jaw 532, a guide base 533, a guide rod 534 and a clamping jaw moving cylinder 535, wherein the clamping jaw 532 is fixedly mounted on the clamping jaw mounting plate 531 and used for clamping the thin film gloves. The jaws 532 are formed by upper and lower jaws hinged together. The jaw mounting plate 531 is fixed to one end of the guide bar 534, and the other end of the guide bar 534 is fixed to the connection plate 536. The guide rod 534 is provided with a bearing 537, the bearing 537 is slidably mounted in the guide groove of the guide holder 533, and the piston rod of the jaw moving cylinder 535 is drivingly connected to the connecting plate 536. The gripper cylinder 535 drives the gripper fingers 532 back and forth to transfer from the glove waste removal mechanism to the drop platform 51. The bag feeding assembly 54 comprises a guide groove 541, an inserting plate 542 and a driving cylinder 543, wherein the guide groove 541 is installed right above the bag feeding groove 52, the inserting plate 542 is slidably installed in the guide groove 541, and the upper end of the inserting plate is fixedly connected with a piston rod of the driving cylinder 543. The air cylinder 543 is driven to act to drive the inserting plate 542 to move downwards, and the gloves on the emptying platform 51 are inserted into the bag slots 52, so that the film gloves are put into the bags.
As shown in fig. 1 and 9, the vertical film glove bagging machine further comprises an easy-tear opening forming mechanism 6, wherein the easy-tear opening forming mechanism 6 is arranged on the horizontal section of the film feeding mechanism and is used for forming a semicircular easy-tear opening on one film. Specifically, the easy-tear-opening forming mechanism 6 includes a mounting seat 61, a bottom plate 62, a cutter mounting seat 63, a semicircular cutter 64, a pillar 65, a cylinder mounting seat 66, and a cylinder 67. The base plate 62 is fixedly mounted on the mounting base 61 and forms a gap for the film to pass through with the mounting base 61 through the spacer 68. The bottom plate 62 is provided with a semicircular cutter passage 621 penetrating up and down. The semicircular cutter 64 is fixedly mounted to the cutter mount 63 and aligned with the semicircular cutter channel 621. The semicircular cutter 64 has a toothed edge to form a virtual line. The cylinder mount 66 is mounted on the base plate 62 by a post, and the cylinder 67 is fixedly mounted on the cylinder mount 66 and its piston rod is fixedly connected to the tool mount 63 through the cylinder mount 66. A rubber block 69 is embedded on the upper surface of the mounting seat 61, and the rubber block 69 is located right below the semicircular cutter channel 621. The cylinder 67 drives the semicircular cutter 64 to move downwards, and a semicircular easy-tearing opening is formed in the film.
Returning to fig. 1, the vertical film glove bagging machine may further include a conveyor belt 8, the conveyor belt 8 being horizontally disposed with one end below the cross seal assembly 42 and the other end at the end of the frame (opposite the infeed end). The conveyor belt 8 is used for conveying the packaged gloves in bags.
While the invention has been particularly shown and described with reference to a preferred embodiment, it will be understood by those skilled in the art that various changes in form and detail may be made therein without departing from the spirit and scope of the invention as defined by the appended claims.
Claims (10)
1. A vertical type film glove bagging machine is characterized by comprising a rack, and a glove waste tearing mechanism, a film feeding mechanism, a bag forming mechanism and a vertical bag feeding mechanism which are arranged on the rack, wherein the glove waste tearing mechanism is arranged at the feeding end of the rack and is used for removing waste of a whole stack of semi-finished film gloves to obtain film gloves to be packaged, and the semi-finished film gloves comprise film gloves which are connected together in a virtual mode and waste materials which wrap the film gloves; the film feeding mechanism is used for guiding the film to the bag forming mechanism from two film rolls positioned at two ends of the rack; the bag forming mechanism is positioned in the middle of the rack and used for forming two films from the two film rolls into a bag with an upper opening, sealing the upper opening of the bag with the thin film gloves and cutting off the bag with the thin film gloves, the vertical bag feeding mechanism comprises a bag feeding groove, a material clamping component and a bag feeding component, the bag feeding groove extends into the space between the two films of the bag to be formed, the material clamping component is used for transferring the thin film gloves from the glove waste tearing mechanism to the upper portion of the bag feeding groove, and the bag feeding component is positioned right above the bag feeding groove and used for feeding the thin film gloves into the bag.
2. The vertical film glove bagging machine according to claim 1, further comprising an easy-tear port forming mechanism disposed on a horizontal section of the film feeding mechanism for forming a semicircular easy-tear port on one of the films.
3. The vertical film glove bagging machine according to claim 2, wherein the easy-tear port forming mechanism comprises a mounting seat, a bottom plate, a cutter mounting seat, a semicircular cutter, a pillar, a cylinder mounting seat and a cylinder, the bottom plate is fixedly mounted on the mounting seat and forms a gap for the film to pass through with the mounting seat, the bottom plate is provided with a semicircular cutter channel penetrating up and down, the semicircular cutter is fixedly mounted on the cutter mounting seat and aligned with the semicircular cutter channel, the cylinder mounting seat is mounted on the bottom plate through the pillar, and the cylinder is fixedly mounted on the cylinder mounting seat and a piston rod of the cylinder passes through the cylinder mounting seat and is fixedly connected to the cutter mounting seat.
4. The vertical film glove bagging machine of claim 3, wherein a rubber block is embedded on the upper surface of the mounting base and is positioned directly below the semicircular knife channel.
5. The vertical type thin film glove bagging machine according to claim 1, wherein the film feeding mechanism comprises a film pulling assembly and two film moving assemblies symmetrically arranged at two sides of the film pulling assembly, each film moving assembly comprises a first guide roller, a first conveying roller pair, a swinging tensioning roller mechanism, a second guide roller, a third guide roller and a fourth guide roller, the conveying roller pairs are driven by a motor to rotate, the swinging tensioning roller mechanism is positioned below the first conveying roller pair, the second guide roller pair and the third guide roller, the bag feeding groove is inserted between the fourth guide rollers of the two film moving assemblies, the film pulling assembly comprises an upper film pulling wheel pair, a lower film pulling wheel pair and a film pulling driving mechanism for driving the upper film pulling wheel pair and the lower film pulling wheel pair to rotate, and the film is unfolded from a film roll and sequentially passes through the first guide roller pair, the first conveying roller pair, the first tensioning roller of the swinging tensioning roller mechanism, the second guide roller, the second tensioning roller of the swinging tensioning roller mechanism, The guide roller III, the guide roller IV, the film upwards-drawing wheel pair and the film downwards-drawing wheel pair.
6. The vertical film glove bagging machine according to claim 5, wherein the swinging tension roller mechanism comprises a first tension roller, a second tension roller, two tension side plates, a tension rotating shaft and a reinforcing plate, the tension rotating shaft, the second tension roller and the two tension side plates are assembled into a rectangular structure, two ends of the tension rotating shaft are installed on the machine frame, so that the rectangular structure can swing around the tension rotating shaft, the reinforcing plate and the first tension roller are installed in the rectangular structure in parallel with the second tension roller, and the reinforcing plate is located between the first tension roller and the second tension roller.
7. The vertical film glove bagging machine according to claim 5, wherein the film moving assembly further comprises a clutch shaft, a clutch swing arm, a spring pressing block and a spring, the clutch shaft is installed below the conveying roller pair in parallel, the lower end of the clutch swing arm is rotatably installed on the machine frame, a driven roller of the conveying roller pair is installed at the upper end of the clutch swing arm, the spring pressing block is installed on the machine frame, one end of the spring abuts against the spring pressing block, the other end of the spring abuts against the side face of the upper end of the clutch swing arm, and a groove matched with a notch of the clutch shaft is formed in one side, away from the spring, of the clutch swing arm.
8. The vertical film glove bagging machine according to claim 5, wherein the film drawing driving mechanism comprises a motor, a main gear, an upper driven gear pair, a lower driven gear pair, an upper belt pulley, a lower belt pulley, and a timing belt, wherein the main gear is mounted on an output shaft of the motor, the upper driven gear pair and the lower driven gear pair are respectively fixedly mounted on rotating shafts of the upper film drawing wheel pair and the lower film drawing wheel pair, the main gear is engaged with one of the upper driven gear pair, the upper belt pulley is fixedly connected with the other of the upper driven gear pair, the lower belt pulley is fixedly connected with one of the lower driven gear pair, and the timing belt is looped around the upper belt pulley and the lower belt pulley.
9. The vertical film glove bagging machine according to claim 5, wherein the bag forming mechanism comprises a left longitudinal sealing assembly and a right longitudinal sealing assembly and a transverse sealing assembly, the longitudinal sealing assembly is located between the upper film drawing wheel pair and the lower film drawing wheel pair, the transverse sealing assembly is located below the lower film drawing wheel pair, the longitudinal sealing assembly comprises a mounting plate, a roller, a heating body, a sliding block and an air cylinder, an opening is formed in the mounting plate, the air cylinder and the roller are respectively mounted on the mounting plate on two sides of the opening, the heating body is fixedly mounted on the sliding block in a heat insulation mode through a bakelite ring, and a telescopic rod of the air cylinder is fixedly connected with the sliding block to drive the heating body to move towards or away from the roller.
10. The vertical film glove bagging machine according to claim 9, wherein the vertical sealing assembly further comprises a width adjusting screw inserted through one end of the two mounting plates by an adjusting nut, and a guide rod inserted through the other end of the two mounting plates by a linear bearing.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921451712.XU CN210708135U (en) | 2019-09-03 | 2019-09-03 | Vertical film glove bagging machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921451712.XU CN210708135U (en) | 2019-09-03 | 2019-09-03 | Vertical film glove bagging machine |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210708135U true CN210708135U (en) | 2020-06-09 |
Family
ID=70956888
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921451712.XU Active CN210708135U (en) | 2019-09-03 | 2019-09-03 | Vertical film glove bagging machine |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210708135U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112571694A (en) * | 2020-11-24 | 2021-03-30 | 江西美宝利实业有限公司 | Automatic glove remainder removing device |
| CN112758373A (en) * | 2020-12-26 | 2021-05-07 | 浙江神英科技股份有限公司 | Automatic filling system for bagged shampoo |
-
2019
- 2019-09-03 CN CN201921451712.XU patent/CN210708135U/en active Active
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN112571694A (en) * | 2020-11-24 | 2021-03-30 | 江西美宝利实业有限公司 | Automatic glove remainder removing device |
| CN112758373A (en) * | 2020-12-26 | 2021-05-07 | 浙江神英科技股份有限公司 | Automatic filling system for bagged shampoo |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN108639422A (en) | A kind of whistle lollipop packing machine | |
| CN115258299A (en) | Automatic film sleeving machine | |
| US20030159401A1 (en) | Continuous motion sealing apparatus for packaging machine | |
| CN112249388B (en) | A device for automatic carton packaging | |
| CN119190549A (en) | A multi-row charter aircraft | |
| CN109466815B (en) | File bag packagine machine | |
| CN110877783A (en) | Automatic sealing and bundling packaging device | |
| CN207956223U (en) | A kind of packaging facilities of foam films self-adhesion bag automatic bag-opening and envelope | |
| CN211443626U (en) | Automatic sealing and bundling packaging device | |
| CN212023147U (en) | Automatic change tubular product packagine machine | |
| CN116588428A (en) | Fertilizer bagging mechanism | |
| CN117002792A (en) | A kind of segmented meat packaging equipment | |
| CN208544463U (en) | A kind of whistle lollipop packing machine | |
| CA1078726A (en) | Horizontal packaging apparatus | |
| CN110182411B (en) | Blood bag packaging machine and working method thereof | |
| CN210823020U (en) | Horizontal film glove bagging machine | |
| CN211196791U (en) | Full-automatic prefabricated bag packagine machine | |
| CN221969909U (en) | Automatic bag making device on batching mechanism | |
| CN220721565U (en) | PE (polyethylene) barrel bag packaging machine | |
| CN210116667U (en) | High-speed bottom sealing type plastic packaging machine | |
| CN221138851U (en) | Automatic straight tube bag sleeving and packaging machine | |
| CN220743553U (en) | Rice bag sealing device | |
| CN117755596A (en) | sanitary napkin production system | |
| CN109156270A (en) | Automatic bagging tying is taped all-in-one machine | |
| CN214527109U (en) | Film feeding and bag making device of stretching film sleeving machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |