CN210649300U - Welding tool and automatic assembly welding device - Google Patents
Welding tool and automatic assembly welding device Download PDFInfo
- Publication number
- CN210649300U CN210649300U CN201921316016.8U CN201921316016U CN210649300U CN 210649300 U CN210649300 U CN 210649300U CN 201921316016 U CN201921316016 U CN 201921316016U CN 210649300 U CN210649300 U CN 210649300U
- Authority
- CN
- China
- Prior art keywords
- tensioning
- welding
- movable
- ring
- movable wedge
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003466 welding Methods 0.000 title claims abstract description 99
- 210000004907 gland Anatomy 0.000 claims abstract description 31
- 230000009471 action Effects 0.000 claims abstract description 9
- 230000000694 effects Effects 0.000 claims description 55
- 238000001125 extrusion Methods 0.000 claims description 12
- 238000003825 pressing Methods 0.000 claims description 6
- 230000008093 supporting effect Effects 0.000 claims description 5
- 235000017166 Bambusa arundinacea Nutrition 0.000 abstract description 10
- 235000017491 Bambusa tulda Nutrition 0.000 abstract description 10
- 241001330002 Bambuseae Species 0.000 abstract description 10
- 235000015334 Phyllostachys viridis Nutrition 0.000 abstract description 10
- 239000011425 bamboo Substances 0.000 abstract description 10
- 238000012423 maintenance Methods 0.000 abstract 1
- 238000000034 method Methods 0.000 description 13
- 230000008569 process Effects 0.000 description 8
- 230000006872 improvement Effects 0.000 description 7
- 230000008859 change Effects 0.000 description 2
- 238000010276 construction Methods 0.000 description 2
- 238000013461 design Methods 0.000 description 2
- 238000010586 diagram Methods 0.000 description 2
- 238000004519 manufacturing process Methods 0.000 description 2
- 230000007246 mechanism Effects 0.000 description 2
- 230000001737 promoting effect Effects 0.000 description 2
- 238000013519 translation Methods 0.000 description 2
- 230000015572 biosynthetic process Effects 0.000 description 1
- 230000006835 compression Effects 0.000 description 1
- 238000007906 compression Methods 0.000 description 1
- 238000005034 decoration Methods 0.000 description 1
- 238000001514 detection method Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 239000013013 elastic material Substances 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 230000002035 prolonged effect Effects 0.000 description 1
- 239000000126 substance Substances 0.000 description 1
Images

Landscapes
- Butt Welding And Welding Of Specific Article (AREA)
Abstract
The utility model discloses a welding frock, the on-line screen storage device comprises a base, be equipped with vertical tensioning section of thick bamboo on the base and treat that the welding object covers in proper order and establish on tensioning section of thick bamboo in order to be used for making two, the last cover is equipped with the gland down to the cover on the tensioning section of thick bamboo, first tensioning ring, guide ring and second tensioning ring, it is equipped with a plurality of first movable voussoirs to enclose on the first tensioning ring, it is equipped with a plurality of second movable voussoirs to enclose on the second tensioning ring, the gland extrudees down under the exogenic action during operation, so that be used for making a plurality of first movable voussoirs and second movable voussoirs all simultaneously outwards roll-off and tightly two inner walls of treating the welding object in order to carry out the tensioning spacing. The utility model also discloses an automatic assembly welding device. The utility model has the advantages of simple and compact structure, easy processing preparation and maintenance, can improve the assembly welding centering precision, reduce manual work and emphasize, improve work efficiency.
Description
Technical Field
The utility model mainly relates to the automatic weld equipment field, concretely relates to welding frock and an automatic assembly welding device.
Background
In the prior art, flange joints are simple welded connections that have found numerous applications in the automotive, mechanical manufacturing, marine and chemical industries. With the rapid development of scientific technology and industrial economy in the recent years, the demand for welding structural members of flange joints is increasing. Before welding, the two parts of the flange and the barrel are assembled and aligned, and then welding (also called butt welding or assembly welding) is carried out. Because the part is applied to the structure of the pressure vessel, the quality requirement is high, and welding seams all need one hundred percent of nondestructive detection and need to be completed by experienced technicians. The following technical problems exist at present:
firstly, spot welding is leaned on artifical spot welding group to right between flange and the barrel, and the workman can lead to spot welding group to the inefficiency because of the problem of experience and proficiency, is unfavorable for automatic high-efficient operation.
Secondly, when the work piece is heavier, can increase workman's intensity of labour to the barrel topples over when preventing to weld, has certain operation risk.
Thirdly, due to the low efficiency of manual assembly to welding, if the assembly workers are increased, the labor cost is increased.
Fourthly, the phenomenon that the alignment error of the flange and the cylinder body is large often appears in the welding assembly operation of the prior art, and the welding quality and the welding strength are seriously influenced.
In the prior art, the thickness of the flange and the thickness of the cylinder body are consistent, but the outer wall surfaces of the flange and the cylinder body are required to be aligned and consistent for welding, so that centering is more difficult to operate, operation errors are larger, and welding quality and strength are seriously influenced.
SUMMERY OF THE UTILITY MODEL
The utility model solves the technical problem that: aiming at the problems in the prior art, the welding tool has a simple and compact structure, is easy to machine, manufacture and maintain, can improve the assembly welding centering precision, reduce the manual work emphasis and improve the working efficiency, and the automatic assembly welding device based on the welding tool is also provided.
In order to solve the technical problem, the utility model discloses a following technical scheme:
the utility model provides a welding frock, includes the base, be equipped with vertical tensioning section of thick bamboo on the base and treat that the welding object covers in proper order and establish on a tensioning section of thick bamboo in order to be used for making two, last from last to overlapping of tensioning section of thick bamboo down is equipped with gland, first tensioning ring, guide ring and second tensioning ring, it is equipped with a plurality of first activity voussoirs to enclose on the first tensioning ring, it is equipped with a plurality of second activity voussoirs to enclose on the second tensioning ring, the lower part of gland is equipped with the round and is used for the first direction hypotenuse with first activity voussoir sliding fit, be equipped with one on the guide ring and circle down the hypotenuse of leading, in order to be used for respectively with first activity voussoir and second activity voussoir sliding fit, be equipped with the convex second direction hypotenuse of round on the base in order to be used for with second activity voussoir sliding fit, during the operation the gland extrudees down under the exogenic action so that a plurality of first activity voussoirs and second activity The inner walls of the two objects to be welded are tensioned for limiting.
As a further improvement of the present invention, a first guiding and limiting groove is formed on one side of the first movable wedge block close to the first tensioning ring, and the first tensioning ring is clamped in the first guiding and limiting groove to support the first movable wedge block and guide and limit the sliding stroke of the first movable wedge block; the second movable wedge block is close to one side of the second tensioning ring, and a second guide limiting groove is formed in the side, close to the second tensioning ring, of the second movable wedge block, and the second tensioning ring is clamped in the second guide limiting groove and used for supporting the second movable wedge block and guiding and limiting the sliding stroke of the second movable wedge block.
As the utility model discloses a further improvement still includes two elastic rings, two on the lateral surface of a plurality of first activity voussoirs and second activity voussoirs was located respectively to the elastic ring, two during the welding the elastic ring all is by the extrusion stretch in order to make a plurality of first activity voussoirs and second activity voussoirs reset simultaneously through elastic restoring force after the operation finishes.
As the utility model discloses a further improvement, it is a plurality of the fixed slot has all been seted up in the outside of first activity voussoir and second activity voussoir, so that two the elasticity circle card respectively goes into the fixed slot by spacingly.
As a further improvement, two the elastic ring all protrudes from a plurality of first movable wedge blocks and second movable wedge blocks, so that the two elastic rings are respectively pressed on two inner walls of objects to be welded during welding operation.
As a further improvement of the utility model, a tensioning section of thick bamboo cavity is in order to be used for holding extrusion drive arrangement, the top surface of gland is equipped with the mounting hole, is used for and extrudees drive arrangement's drive end fixed connection in order to go up and down to extrude the operation.
As a further improvement of the utility model, the elastic ring is a spring ring.
The utility model discloses still relate to an automatic assembly welding device, which comprises a frame, install as above arbitrary one on the frame welding frock.
As a further improvement, install vertical cylinder assembly in the frame, cylinder assembly's drive end stretches into in the tensioning section of thick bamboo and be connected, carry out the extrusion operation in order to be used for driving the gland to go up and down with the gland.
Compared with the prior art, the utility model has the advantages of:
firstly, the utility model discloses a welding frock, through set up on a tensioning section of thick bamboo mutually support, the gland of mutual support, first tensioning ring, guide ring and second tensioning ring, first activity voussoir, parts such as second activity voussoir, can cooperate with outside actuating mechanism, and then treat two and treat that the welding object forms fine tensioning spacing effect, it is right to be convenient for two treat between welding object (flange and barrel) spot welding, the group is to the process and need not artificial intervention, the work efficiency that the spot welding is right has been improved greatly, intensity of labour and cost of labor have been reduced, the automatic high-efficient operation of very being convenient for.
Secondly the utility model discloses a welding frock, setting through above special construction, make a plurality of first activity voussoirs, the translation rate of second activity voussoir, the removal process is all even, at this removal extrusion in-process, a plurality of first activity voussoirs, second activity voussoir can be with two of originally not centering treat that the welding object realizes progressively promoting and finally pushing away the position of centering with both, also be a plurality of first activity voussoirs, second activity voussoir has the function of accurate regulation, this accurate requirement when not only having reduced artifical when placing originally, workman's intensity of labour has been reduced, and can not take place to empty when two treat that the welding object removes, the operation risk has been reduced.
Thirdly, the utility model discloses a welding frock, a plurality of first movable voussoirs, second movable voussoirs can be simultaneously from inside to two treat that the welding object carries out the tensioning spacing, and this kind of special structure setting makes two treat that welding object (flange and barrel) centering is accurate with removing spacing mode, has improved the right accurate nature of spot welding greatly, has improved final welding quality and intensity greatly.
Fourth is the utility model discloses a welding frock, because first activity voussoir, second activity voussoir all is movable mounting on respective first tensioning ring and second tensioning ring, and be through first activity voussoir, the second activity voussoir realizes the tight spacing in top, make can be to the flange or the barrel of different thickness, change the first activity voussoir and the second activity voussoir of different thickness in a flexible way, and then realize even flange and barrel both own thickness unanimity, but also can make outer wall between them align unanimous splendid technological effect, welding quality and intensity have been improved greatly.
Fifthly the utility model discloses a welding frock, tension ring can form splendid supporting effect to the activity voussoir firstly for the activity voussoir can not drop at removal and extruded in-process, has guaranteed follow-up spacing realization. Secondly, the tensioning ring can also guide and limit the sliding stroke of the movable wedge blocks, so that the plurality of movable wedge blocks can keep the same direction and the same stroke when sliding, and further the same jacking effect can be realized.
Sixthly, the first movable wedges and the second movable wedges can automatically and simultaneously reset under the action of the elastic restoring force of the two elastic rings, so that the two objects to be welded can be quickly prevented from being limited, the later-stage carrying operation can be conveniently and quickly carried out, and the welding tool cannot be damaged during carrying; and secondly, the automatic resetting is realized, so that the subsequent batch of objects to be welded can be placed quickly, the whole process does not need manual intervention, the working efficiency is greatly improved, and the working intensity is reduced.
Seventhly, the utility model discloses a fixed slot has all been seted up in the outside of welding frock, a plurality of first activity voussoirs and second activity voussoir, and this makes two elastic ring spacing and can not drop, has improved the stability of frock. Two elastic rings all bulge in a plurality of first movable voussoirs and the setting of second movable voussoir, this has reduced a plurality of first movable voussoirs, second movable voussoirs and two and has treated the hard contact and the friction of welding object internal face, can not treat to two and treat that welding object internal face causes the damage, extension equipment life, two elastic rings also can realize coordinating certain position fine setting when removing the centering.
Eighthly, the utility model discloses an automatic assembly welding device through the installation as above welding frock for this automatic assembly welding device can greatly reduced workman's intensity of labour, reduces the operation risk, and can improve spot welding group right precision greatly, improve ultimate welding quality and intensity greatly.
Drawings
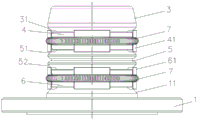
Fig. 1 is a schematic view of the front view structure of the welding tool of the present invention.
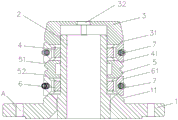
Fig. 2 is a schematic view of the cross-sectional structure of fig. 1.
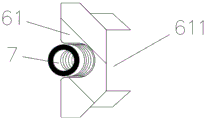
Fig. 3 is a schematic cross-sectional structural diagram of the first movable wedge according to the present invention.
Fig. 4 is a schematic diagram of the cross-sectional structure of the second movable wedge according to the present invention.
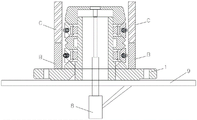
FIG. 5 is a schematic view of the structural principle of the automatic assembly welding device of the present invention
Illustration of the drawings:
1. a base; 11. a second hypotenuse; 2. a tensioning cylinder; 3. a gland; 31. a first hypotenuse; 32. mounting holes; 4. a first tensioning ring; 41. a first movable wedge; 411. a first guide limit groove; 5. a guide ring; 51. an upper beveled guide edge; 52. a lower guiding bevel edge; 6. a second tension ring; 61. a second movable wedge; 611. a second guide limit groove; 7. an elastic ring; 8. a cylinder assembly; 9. and a frame.
Detailed Description
The present invention will be described in further detail with reference to the following embodiments and drawings.
As shown in fig. 1, fig. 2, fig. 3, fig. 4, and fig. 5, the utility model provides a welding tool, including base 1, base 1 is last to be equipped with a plurality of fixed hole portions (as shown in fig. 2 a) and is used for fixing base 1 on operation frame or operation station. The base 1 is provided with a vertical tensioning cylinder 2 for covering two objects to be welded on the tensioning cylinder 2 in sequence (the two objects to be welded are shown as B and C in fig. 5, B is a flange, C is a cylinder, and BC is welded together for operation purpose). The tensioning cylinder 2 is sleeved with a gland 3, a first tensioning ring 4, a guide ring 5 and a second tensioning ring 6 from top to bottom. A plurality of first movable wedges 41 are arranged on the first tensioning ring 4 in a surrounding manner, namely, the plurality of first movable wedges 41 are movably arranged on the first tensioning ring 4; a plurality of second movable wedges 61 are arranged on the second tensioning ring 6 in a surrounding manner, namely, the plurality of second movable wedges 61 are movably arranged on the second tensioning ring 6;
the lower part of the gland 3 is provided with a circle of first oblique guiding edges 31 which are used for being in sliding fit with the first movable wedge blocks 41, the guide ring 5 is provided with a circle of upper oblique guiding edges 51 and a circle of lower oblique guiding edges 52 which are used for being in sliding fit with the first movable wedge blocks 41 and the second movable wedge blocks 61 respectively, the base 1 is provided with a circle of convex second oblique guiding edges 11 which are used for being in sliding fit with the second movable wedge blocks 61, and the wedge blocks are provided with an upper oblique surface and a lower oblique surface, so that the arrangement can be clearly known that the first oblique guiding edges 31 are in sliding fit with the upper oblique surfaces of the first movable wedge blocks 41, and the upper oblique guiding edges 51 are in sliding fit with the lower oblique surfaces of; the lower oblique guide edge 52 is in sliding fit with the upper oblique surface of the second movable wedge 61, and the second oblique guide edge 11 is in sliding fit with the lower oblique surface of the second movable wedge 61.
During operation, the gland 3 is pressed downwards under the action of external force so as to enable the first movable wedges 41 and the second movable wedges 61 to simultaneously slide outwards under the pressing and guiding actions and respectively push against the inner walls of the two objects to be welded for tensioning and limiting. Regarding the external force, a vertical cylinder assembly 8 may be disposed below the gland 3 for driving the gland 3 to ascend and descend for performing the extrusion operation, or a vertical cylinder assembly may be disposed above the gland 3 for driving the gland 3 to ascend and descend for performing the extrusion operation (because the cylinder C is hollow), which will not be described in detail herein. The specific implementation principle is as follows:
during operation, two objects to be welded are sequentially covered on the tensioning cylinder 2, and at the moment, the inner wall surfaces of the two objects to be welded are not in contact with the first movable wedge 41 and the second movable wedge 61. Then the gland 3 extrudes downwards under the action of external force, at this time, the gland 3 tends to extrude the first movable wedge block 41 downwards, the first movable wedge block 41 extrudes on the guide ring 5 below, the guide ring 5 extrudes the second movable wedge block 61 below downwards, and the lower inclined surface of the second movable wedge block 61 extrudes on the second guide inclined edge 11 protruding on the base 1 and is limited and can not move downwards. In the above sequential pressing process, due to the continuous downward movement of the gland 3, and due to the slidable fitting arrangement of the first movable wedge 41 and the second movable wedge 61, the first movable wedge 41 and the second movable wedge 61 tend to slide outward (i.e. be extruded outward), and finally, the plurality of first movable wedges 41 simultaneously contact and abut against the inner wall of the object to be welded C, the plurality of second movable wedges 61 simultaneously contact and abut against the inner wall of the object to be welded B, and the two objects to be welded are tensioned and limited, and then the welding operation is performed. Through the special scientific design, the method has the following technical advantages:
firstly, the utility model discloses a welding frock, through set up on a tensioning section of thick bamboo 2 and mutually support, gland 3 of mutual support, first tensioning ring 4, guide ring 5 and second tensioning ring 6, first activity voussoir 41, parts such as second activity voussoir 61, can cooperate with outside actuating mechanism, and then treat two welding object formation fine tensioning spacing effect, it is right to be convenient for two treat between welding object (flange and barrel) spot welding, group need not artificial intervention to the process, the right work efficiency of spot welding has been improved greatly, labor intensity and cost of labor have been reduced, the automatic high-efficient operation of ten minutes of being convenient for.
Secondly the utility model discloses a welding frock, setting through above special construction, make a plurality of first movable voussoir 41, the translation rate of second movable voussoir 61, the removal process is even, in this removal extrusion process, a plurality of first movable voussoir 41, second movable voussoir 61 can treat two of originally centering and treat that the welding object realizes progressively promoting and finally pushing away both to the position of centering, also be a plurality of first movable voussoir 41, second movable voussoir 61 has the function of accurate regulation, this accurate requirement when not only having reduced artifical original placing, the intensity of labour of the workman is reduced, and two can not take place to empty when treating the welding object removal, the operation risk is reduced.
Thirdly, the utility model discloses a welding frock, a plurality of first movable voussoirs 41, second movable voussoir 61 can be simultaneously from inside to two treat that the welding object carries out the tensioning spacing, and this kind of special structure setting makes two treat that the welding object (flange and barrel) centering is accurate with the spacing mode of removal, has improved the right accurate nature of spot welding greatly, has improved final welding quality and intensity greatly.
Fourth, the utility model discloses a welding frock, because first activity voussoir 41, second activity voussoir 61 all is movable mounting on respective first tension ring 4 and second tension ring 6, and through first activity voussoir 41, second activity voussoir 61 realizes the tight spacing in top, make can be to the flange or the barrel of different thickness, change the first activity voussoir 41 and the second activity voussoir 61 of different thickness in a flexible way, and then realize even flange and barrel both thickness itself unanimous, but also can make the outer wall between them align unanimous splendid technological effect, welding quality and intensity have been improved greatly.
Further, in a preferred embodiment, a first guiding and limiting groove 411 is formed on one side of the first movable wedge 41 close to the first tensioning ring 4, and the first tensioning ring 4 is clamped in the first guiding and limiting groove 411 to support the first movable wedge 41 and guide and limit the sliding stroke of the first movable wedge 41; a second guiding limiting groove 611 is formed in one side, close to the second tensioning ring 6, of the second movable wedge 61, and the second tensioning ring 6 is clamped in the second guiding limiting groove 611 to support the second movable wedge 61 and guide and limit the sliding stroke of the second movable wedge 61. Through the special scientific design, the method has the following technical advantages:
firstly, make the tensioning ring can form splendid supporting effect to the activity voussoir for the activity voussoir can not drop at removal and extruded in-process, has guaranteed follow-up spacing realization. Secondly, the tensioning ring can also guide and limit the sliding stroke of the movable wedge blocks, so that the plurality of movable wedge blocks can keep the same direction and the same stroke when sliding, and further the same jacking effect can be realized. It is assumed that if the moving directions and the moving strokes of the first movable wedge 41 and the second movable wedge 61 are inconsistent, the contact surfaces and the tightening force of the two objects to be welded are inconsistent, and the final assembly and centering effect is not good.
Further, in the preferred embodiment, two elastic rings 7 are further included, and the two elastic rings 7 are respectively hooped on the outer side surfaces of the plurality of first movable wedges 41 and the plurality of second movable wedges 61, that is, one elastic ring 7 is hooped on the plurality of first movable wedges 41, and the other elastic ring 7 is hooped on the outer side surface of the plurality of second movable wedges 61. Both the elastic rings 7 are compressed and stretched for simultaneously restoring the plurality of first movable wedges 41 and the second movable wedge 61 by elastic restoring force after the work is finished. Once the gland 3 is not pressed downwards any more, the first movable wedge blocks 41 and the second movable wedge blocks 61 can be automatically reset simultaneously under the action of the elastic restoring force of the two elastic rings 7, so that firstly, two objects to be welded can be quickly prevented from being limited, the later-stage carrying operation can be conveniently and quickly carried out, and the carrying tool cannot be damaged; and secondly, the automatic resetting is realized, so that the subsequent batch of objects to be welded can be placed quickly, the whole process does not need manual intervention, the working efficiency is greatly improved, and the working intensity is reduced.
Further, in the preferred embodiment, the outer sides of the first movable wedge 41 and the second movable wedge 61 are respectively provided with a fixing groove for the two elastic rings 7 to be respectively clamped into the fixing grooves for being limited. This makes two elastic ring 7 spacing and can not drop, has improved the stability of frock.
Further, in the preferred embodiment, two elastic rings 7 are protruded from the plurality of first movable wedges 41 and the plurality of second movable wedges 61, so that the two elastic rings 7 are respectively pressed on the inner walls of two objects to be welded during the welding operation. The first one is that hard contact and friction of the first movable wedge blocks 41, the second movable wedge blocks 61 and the inner wall surfaces of the two objects to be welded are reduced, the inner wall surfaces of the two objects to be welded cannot be damaged, the service life of equipment is prolonged, and the two elastic rings 7 can be matched with a certain position for fine adjustment when moving and centering.
Further, in the preferred embodiment, the tension cylinder 2 is hollow for accommodating the extrusion driving device, and the top surface of the gland 3 is provided with a mounting hole 32 for fixedly connecting with the driving end of the extrusion driving device for lifting and pressing operation. This facilitates the mounting and placement of the compression drive.
Further, in the preferred embodiment, the elastic ring 7 is a spring ring. Of course, in other embodiments, the elastic ring 7 may be made of other elastic materials, such as an elastic ribbon ring, and the like, which shall fall within the protection scope of the present invention.
As shown in fig. 5, the utility model also provides an automatic assembly welding device, including frame 9, the welding frock as above arbitrary is installed on frame 9. Through installing this welding frock for this automatic assembly welding device can greatly reduced workman's intensity of labour, reduces the operation risk, and can improve spot welding group to right accurate nature greatly, improve ultimate welding quality and intensity greatly.
Further, in the preferred embodiment, a vertical cylinder assembly 8 is installed on the frame 9, and a driving end of the cylinder assembly 8 extends into the tensioning cylinder 2 and is connected with the gland 3 so as to drive the gland 3 to lift and lower for extrusion operation.
Above only the utility model discloses an it is preferred embodiment, the utility model discloses a scope of protection not only limits in above-mentioned embodiment, and the all belongs to the utility model discloses a technical scheme under the thinking all belongs to the utility model discloses a scope of protection. It should be noted that, for those skilled in the art, a plurality of modifications and decorations without departing from the principle of the present invention should be considered as the protection scope of the present invention.
Claims (9)
1. The welding tool is characterized by comprising a base (1), wherein the base (1) is provided with a vertical tensioning cylinder (2) for enabling two objects to be welded to be sequentially covered on the tensioning cylinder (2), the tensioning cylinder (2) is sleeved with a gland (3), a first tensioning ring (4), a guide ring (5) and a second tensioning ring (6) from top to bottom, the first tensioning ring (4) is provided with a plurality of first movable wedge blocks (41), the second tensioning ring (6) is provided with a plurality of second movable wedge blocks (61), the lower part of the gland (3) is provided with a first guide inclined edge (31) in a circle for sliding fit with the first movable wedge blocks (41), the guide ring (5) is provided with an upper guide inclined edge (51) in a circle and a lower guide inclined edge (52) in a circle for sliding fit with the first movable wedge blocks (41) and the second movable wedge blocks (61) respectively, be equipped with convex second guided bevel (11) of round on base (1) in order to be used for with second activity voussoir (61) sliding fit, during the operation gland (3) extrude down under the exogenic action, so that a plurality of first activity voussoir (41) and second activity voussoir (61) all outwards roll-off simultaneously and tightly push up the inner wall of two waiting to weld the thing respectively with the tensioning spacing under extrusion and guiding action.
2. The welding tool according to claim 1, wherein a first guide limiting groove (411) is formed in one side, close to the first tensioning ring (4), of the first movable wedge (41), and the first tensioning ring (4) is clamped in the first guide limiting groove (411) and used for supporting the first movable wedge (41) and guiding and limiting the sliding stroke of the first movable wedge (41); second direction spacing groove (611) have been seted up to one side that second activity voussoir (61) are close to second tensioning ring (6), second tensioning ring (6) card is located in second direction spacing groove (611), in order to be used for supporting second activity voussoir (61) and to the slip stroke of second activity voussoir (61) lead spacing.
3. The welding tooling of claim 1, further comprising two elastic rings (7), wherein the two elastic rings (7) are respectively hooped on the outer side surfaces of the first movable wedges (41) and the second movable wedges (61), and the two elastic rings (7) are extruded and stretched during welding so as to enable the first movable wedges (41) and the second movable wedges (61) to be reset simultaneously through elastic restoring force after operation is finished.
4. The welding tooling as claimed in claim 3, wherein a plurality of fixing grooves are formed in the outer sides of the first movable wedge (41) and the second movable wedge (61) for enabling the two elastic rings (7) to be respectively clamped into the fixing grooves to be limited.
5. The welding tooling of claim 3, wherein the two elastic rings (7) are arranged to protrude from the plurality of first movable wedges (41) and the plurality of second movable wedges (61) so that the two elastic rings (7) are respectively pressed against the inner walls of the two objects to be welded during welding operation.
6. The welding tool according to claim 1, characterized in that the tensioning cylinder (2) is hollow for accommodating a pressing driving device, and the top surface of the gland (3) is provided with a mounting hole (32) for fixedly connecting with a driving end of the pressing driving device for lifting and pressing operation.
7. The welding tool according to claim 3, characterized in that the elastic ring (7) is a spring ring.
8. An automatic assembly welding device, characterized by comprising a frame (9), wherein the welding tool according to any one of claims 1 to 7 is mounted on the frame (9).
9. The automatic assembly welding device according to claim 8, characterized in that a vertical cylinder assembly (8) is mounted on the frame (9), and a driving end of the cylinder assembly (8) extends into the tensioning cylinder (2) and is connected with the gland (3) so as to drive the gland (3) to lift for extrusion operation.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921316016.8U CN210649300U (en) | 2019-08-14 | 2019-08-14 | Welding tool and automatic assembly welding device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921316016.8U CN210649300U (en) | 2019-08-14 | 2019-08-14 | Welding tool and automatic assembly welding device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210649300U true CN210649300U (en) | 2020-06-02 |
Family
ID=70840935
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921316016.8U Active CN210649300U (en) | 2019-08-14 | 2019-08-14 | Welding tool and automatic assembly welding device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210649300U (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110421311A (en) * | 2019-08-14 | 2019-11-08 | 长沙华恒机器人系统有限公司 | A kind of welding tooling, automatic assembly welding device |
| CN115111836A (en) * | 2022-08-12 | 2022-09-27 | 北京中科富海低温科技有限公司 | Cold box convenient to transportation |
| CN115303640A (en) * | 2022-08-12 | 2022-11-08 | 北京中科富海低温科技有限公司 | Limiting device |
-
2019
- 2019-08-14 CN CN201921316016.8U patent/CN210649300U/en active Active
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110421311A (en) * | 2019-08-14 | 2019-11-08 | 长沙华恒机器人系统有限公司 | A kind of welding tooling, automatic assembly welding device |
| CN115111836A (en) * | 2022-08-12 | 2022-09-27 | 北京中科富海低温科技有限公司 | Cold box convenient to transportation |
| CN115303640A (en) * | 2022-08-12 | 2022-11-08 | 北京中科富海低温科技有限公司 | Limiting device |
| CN115111836B (en) * | 2022-08-12 | 2023-09-08 | 北京中科富海低温科技有限公司 | A cold box for easy transportation |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110802390A (en) | Be used for two-way O type sealing washer suit equipment of tubulose work piece | |
| CN216097346U (en) | Harmless pressure equipment device of sealing washer | |
| CN107639409A (en) | A kind of assembly method of device for assembling sealing ring and sealing ring | |
| CN220144772U (en) | Compact metal 3D printer | |
| CN210998485U (en) | Rubber ring sleeving machine for producing automobile valve sleeves | |
| CN206595348U (en) | Battery core edge sealing and lug leveling fixture | |
| CN109048345A (en) | Multistation rivet hole perforating press | |
| CN108747307B (en) | Semi-automatic assembly device and assembly method for piston body sealing ring of hydraulic cylinder | |
| CN215146363U (en) | Cylinder container assembly welding fixture tool | |
| CN116638295B (en) | Automatic lasso workstation | |
| CN108526371A (en) | A kind of hydraulic forging press centering clamping device and its application method | |
| CN209867174U (en) | An automatic loading and unloading pipe expanding machine | |
| CN110625568A (en) | Rubber ring sleeving machine for producing automobile valve sleeves | |
| CN207480010U (en) | A kind of device for assembling sealing ring | |
| CN118559631A (en) | Machining clamp based on aluminum profile extrusion die manufacturing and clamping method thereof | |
| CN206595349U (en) | Battery core edge sealing and lug apparatus for leveling | |
| CN210412352U (en) | Automatic pier nose equipment of high pressure fuel pipe | |
| CN208960716U (en) | A kind of can die with edge-folded | |
| CN111468915B (en) | Piston down-pressing type piston ring assembly fixture | |
| CN211490352U (en) | Bearing bush frock of impressing | |
| CN212154484U (en) | Aluminum alloy window removes wheel structure | |
| CN210679777U (en) | Riveting device | |
| KR102169380B1 (en) | Apparatus and method for bending car interior parts | |
| CN120920924A (en) | High-energy laser beam-based plate cutting machine for machining and manufacturing mechanical equipment | |
| CN223801339U (en) | Cylinder shrink plastic mechanism |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |