Plastic film calendering device for manufacturing decorative plate
Technical Field
The utility model belongs to decorative board processing equipment field, in particular to plastic film calendering device of manufacturing decorative board.
Background
The rolling process is a process of forming a thin product with certain thickness and width by extruding and extending materials through the gaps of one or more pairs of rollers rotating oppositely. At present, products such as decorative films, decorative plates and the like on the market need to use a calendering process.
In the production process of the decorative plate, the surface of the plate can be coated with a plastic film, and then the plastic film is rolled by a heated roller, because the roller is engraved with grains, the film on the surface of the decorative plate can generate corresponding patterns after hot extrusion.
The existing calendering device has some defects, for example, "a calender for producing environment-friendly plastics" described in chinese patent document CN 207889006U, has the following technical problems:
1. before the calender performs calendering treatment, a film to be calendered is conveyed to the calender by a conveying device, dust or other impurities easily fall into the film, and when the heated roller performs extrusion forming on the film, the dust or the impurities are easily pressed on the film together, so that the grains of a decorative film or a decorative plate can be damaged, and the appearance defect of a product is caused;
2. the film after calendering does not cool off in time, makes the film just leave behind the calender and belongs to the softened state like this, and the line receives external disturbance very easily and produces deformation, and natural cooling is adopted to traditional cooling method, and its cooling effect is slow.
SUMMERY OF THE UTILITY MODEL
In view of the technical problem that the background art exists, the utility model provides a make plastic film calendering device of decorative board can remove dust to the tectorial membrane panel before rolling and handle, can cool down the decorative pattern on the tectorial membrane panel after rolling simultaneously and handle.
In order to solve the technical problem, the utility model discloses following technical scheme has been taken and has been realized:
a plastic film calendering device for manufacturing a decorative plate comprises a transmission roller and a calendering roller, wherein the transmission roller is used for transmitting a film-coated plate to be calendered, the calendering roller is heated by a heating device and then used for extruding the film-coated surface of the plate, the transmission roller is arranged on a first platform, a second platform is arranged on the first platform, the calendering roller is arranged on the second platform, a purging device is arranged at the front end of the calendering roller, and the purging device is arranged on the second platform; the blowing device comprises a hollow cylinder, the hollow cylinder is communicated with an air source through an air pipe, and an air nozzle is arranged on the hollow cylinder and used for blowing the film-coated plate in front of the calendering roller.
In the preferred scheme, the hollow cylinder is fixed on a second platform through a bearing seat, the second platform is provided with a reserved opening of the purging device, and the hollow cylinder is positioned above the reserved opening of the purging device; the air nozzles on the hollow cylinder are multiple, the multiple air nozzles are annularly arranged on the cylinder wall of the hollow cylinder around the central axis of the hollow cylinder, a brush is arranged between every two adjacent air nozzles, and the brush is arranged on the cylinder wall of the hollow cylinder; the hollow cylinder is driven to rotate by the first driving device, the center of the bottom surface of the hollow cylinder is provided with an air source inlet hole, and the air source inlet hole is connected with an air pipe through a bearing.
In the preferred scheme, the air nozzle include flat casing, flat casing and the axis parallel arrangement of hollow section of thick bamboo, be equipped with the sharp air cock of a plurality of in the flat casing, sharp air cock and hollow section of thick bamboo inner space intercommunication, sharp air cock is linear arrangement in flat casing.
In a preferable scheme, the first driving device comprises a first motor, the first motor is installed on the second platform, and the front shaft end of the first motor is coaxially connected with the hollow cylinder.
In a preferred scheme, a cooling device is arranged on the second platform and is positioned at the rear end of the calendering roller; the cooling device comprises an air injection cover, the air injection cover is communicated with the air pipe, and the air injection cover is downwards used for aligning the arrangement of the film-coated plate after the rolling is finished.
In the preferred scheme, an air injection cover reserved port is formed in the second platform, and the air injection cover penetrates through the air injection cover reserved port.
In the preferred scheme, the air injection cover is in a square horn shape, and a plurality of air outlet holes are formed in the bottom surface of the air injection cover.
In a preferable scheme, the number of the transmission rollers is multiple, one of the transmission rollers is in transmission with the second driving device through a belt, and two adjacent transmission rollers are in transmission through the belt; the calendering roller is driven by a third driving device through a belt.
In a preferred scheme, the second driving device comprises a second motor, the second motor is arranged on a bottom plate, and the bottom plate is arranged below the first platform; the third driving device comprises a third motor, and the third motor is installed on the second platform.
In a preferred scheme, the air pipe is fixed on the second platform through a bracket.
This patent can reach following beneficial effect:
1. the blowing device is arranged at the front end of the calendering roller, and before the laminated plate to be calendered enters the calendering device, dust removal treatment is carried out through an air nozzle of the blowing device, so that dust or other falling sundries on the laminated plate can be blown away, the calendering quality is improved, and the decorative plate is ensured to be formed without flaws in decorative patterns;
2. the blowing device is simultaneously provided with the air nozzle and the brush, when the hollow cylinder rotates, the brush can sweep dust on the upper surface of the coated plate, and the air outlet direction of the air nozzle also has a forward sweeping process, so the blowing effect can be better by the design;
3. the air nozzle includes flat casing, flat casing and the axis parallel arrangement of hollow section of thick bamboo, can make the air nozzle sweep the width like this and can cover the tectorial membrane panel that needs the calendering, is equipped with the sharp air cock of a plurality of in the flat casing, and the sharp air cock can increase the air current velocity of flow.
4. The second platform is provided with a cooling device, and the cooling device can cool the rolled coated sheet material to achieve the purpose of quickly cooling; the cooling device adopts air cooling, and the air source of the cooling device is the same as that of the blowing device, so that the arrangement of pipelines can be reduced;
5. the air injection cover adopts a bell mouth design, and mainly increases the area of an air port, so that the coverage area of the cooling device is increased.
Drawings
The invention will be further explained with reference to the following figures and examples:
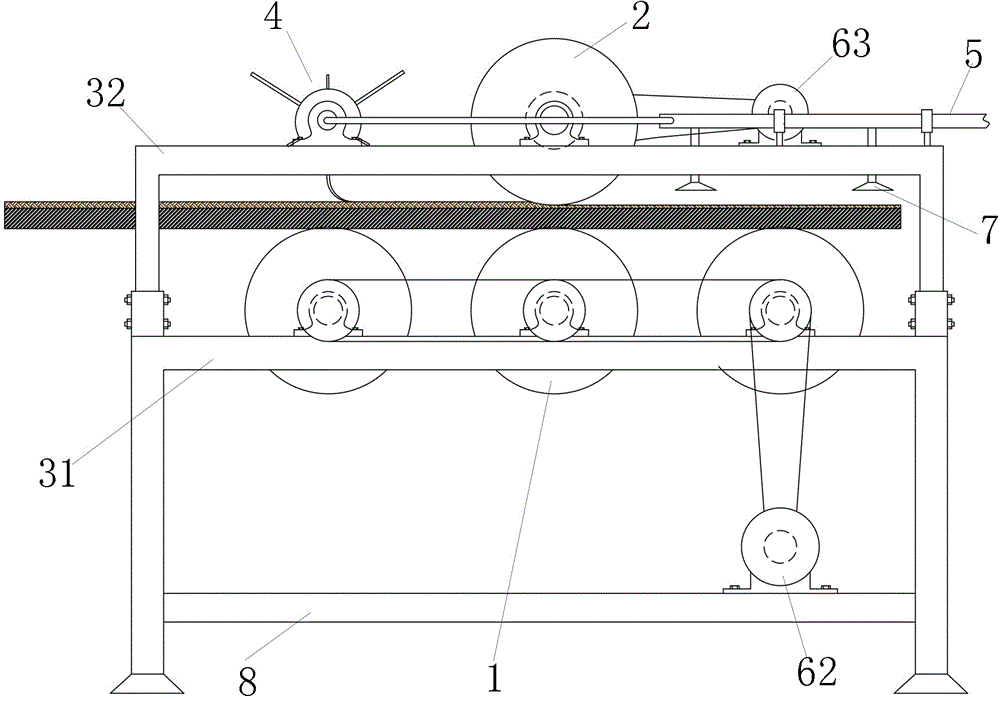
fig. 1 is a side view of the present invention;
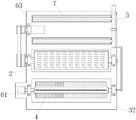
fig. 2 is a top view of a second platform of the present invention;
fig. 3 is a top view of the first platform of the present invention;
FIG. 4 is a structural diagram of the purging device of the present invention;
FIG. 5 is a partial enlarged view of the air nozzle of the purging device of the present invention;
fig. 6 is a structure view of the cooling device of the present invention.
In the figure: the device comprises a transmission roller 1, a calendering roller 2, a first platform 31, a second platform 32, a purging device 4, a hollow cylinder 401, an air nozzle 402, a brush 403, an air inlet hole 404, a supporting cylinder 405, an air pipe 5, a first driving device 61, a second driving device 62, a third driving device 63, a cooling device 7, an air spraying cover 701, an air outlet hole 702 and a bottom plate 8.
Detailed Description
A preferred scheme is as shown in fig. 1 and fig. 4, a plastic film rolling device for manufacturing decorative plates comprises a transmission roller 1 and a rolling roller 2, wherein the transmission roller 1 is used for transmitting a film-coated plate to be rolled, and the rolling roller 2 is used for extruding the film-coated surface of the plate after being heated by a heating device; the heating mode of the calendering roller 2 can adopt circulating oil heating or electric heating, the technical proposal recommends adopting electric heating, and the electric heating mode is disclosed in 'an environment-friendly calender for plastic production' recorded in Chinese patent document CN 207889006U;
the transmission rotating roller 1 is arranged on a first platform 31, a second platform 32 is arranged on the first platform 31, the calendering rotating roller 2 is arranged on the second platform 32, the blowing device 4 is arranged at the front end of the calendering rotating roller 2, and the blowing device 4 is arranged on the second platform 32; the blowing device 4 comprises a hollow cylinder 401, the hollow cylinder 401 is communicated with an air source through an air pipe 5, an air nozzle 402 is arranged on the hollow cylinder 401, and the air nozzle 402 is used for blowing the coated sheet in front of the calendering roller 2;
the first platform 31 and the second platform 32 are supported by legs, four corners of the upper surface of the first platform 31 are provided with fixing sleeves, the fixing sleeves are used for fixing the legs of the second platform 32, and the fixing mode adopts bolt fixing;
the air source can be taken from instrument wind, and if the factory has no instrument wind, the air source is replaced by a blower;
the front end of the calendering roller 2 proposed in the technical scheme refers to: facing the direction of the coated plate needing to be rolled; conversely, the rear end of the calendering roller 2 refers to: towards the laminated plate subjected to the rolling treatment.
As shown in fig. 2 and 4, a hollow cylinder 401 is fixed on the second platform 32 through a bearing seat, the second platform 32 is provided with a purging device reserved opening, and the hollow cylinder 401 is located above the purging device reserved opening; a plurality of air nozzles 402 are arranged on the hollow cylinder 401, the plurality of air nozzles 402 are annularly arranged on the cylinder wall of the hollow cylinder 401 around the central axis of the hollow cylinder 401, a brush 403 is arranged between every two adjacent air nozzles 402, and the brush 403 is arranged on the cylinder wall of the hollow cylinder 401; the hollow cylinder 401 is driven to rotate by the first driving device 61, an air source inlet hole 404 is formed in the center of the bottom surface of the hollow cylinder 401, and the air source inlet hole 404 is connected with the air pipe 5 through a bearing;
supporting cylinders 405 are arranged at the centers of the bottom surfaces of two ends of the hollow cylinder 401, the air source inlet hole 404 is formed in one of the supporting cylinders 405, a bearing is arranged at the air source inlet hole 404, and the center of the bearing is provided with the air pipe 5 in a penetrating manner, so that the air pipe 5 cannot be influenced to enter air when the hollow cylinder 401 rotates; both support cylinders 405 are fixed on the bearing block by bearings;
the brush 403 can be a pig brush which is relatively soft and is not easy to scratch the film-coated plate, the brush 403 is of a flat and long structure, the brush 403 is provided with a plastic handle, and the plastic handle can be fixed on the hollow cylinder 401 by bolts and can also be adhered to the hollow cylinder 401;
the length of the brush 403 is greater than the minimum distance between the wall of the hollow cylinder 401 and the film-coated plate, and preferably, the length of the brush 403 is 1.2 times of the minimum distance between the wall of the hollow cylinder 401 and the film-coated plate, so that when the hollow cylinder 401 rotates, the brush 403 can clean dust or other falling impurities on the film-coated plate.
As shown in fig. 4 and 5, the air nozzle 402 preferably includes a flat housing, the flat housing is disposed parallel to the central axis of the hollow cylinder 401, a plurality of pointed air nozzles are disposed in the flat housing, the pointed air nozzles are communicated with the inner space of the hollow cylinder 401, and the pointed air nozzles are linearly arranged in the flat housing;
the sharp air tap can increase the speed of air current, can increase the intensity that gas swept, and the sharp air tap is linear arrangement in flat casing, can guarantee that the area that sweeps covers the width of tectorial membrane panel.
Preferably, as shown in fig. 2, the first driving device 61 comprises a first motor, which is mounted on the second platform 32, and the front shaft end of the first motor is coaxially connected with the hollow cylinder 401.
As shown in fig. 1, 2 and 6, the cooling device 7 is arranged on the second platform 32, and the cooling device 7 is positioned at the rear end of the calendering roller 2; the cooling device 7 comprises an air injection cover 701, the air injection cover 701 is communicated with the air pipe 5, and the air injection cover 701 faces downwards and is used for aligning the rolled film-coated plate.
In a preferred embodiment, as shown in fig. 1 and 2, an air cap reservation port is opened on the second platform 32, and the air cap 701 is disposed through the air cap reservation port.
As shown in fig. 1, 2 and 6, the gas injection cover 701 is square and horn-shaped, and a plurality of gas outlet holes 702 are arranged on the bottom surface of the gas injection cover 701; the number of the gas injection hoods 701 is at least two.
As shown in fig. 1 and fig. 3, the number of the transmission rollers 1 is multiple, and the number of the transmission rollers is preferably 3 in the present technical solution, one transmission roller 1 of the multiple transmission rollers 1 is in belt transmission with the second driving device 62, and two adjacent transmission rollers 1 are in belt transmission; the calender rolls 2 are driven by a third driving device 63 through a belt.
Preferably, as shown in fig. 1, the second driving device 62 includes a second motor, the second motor is mounted on the bottom plate 8, and the bottom plate 8 is mounted below the first platform 31; the third driving device 63 includes a third motor, and the third motor is installed on the second platform 32;
a transmission rotating roller reserved opening is formed in the first platform 31, a calendering rotating roller reserved opening is formed in the second platform 32, two ends of the calendering rotating roller 2 and two ends of the transmission rotating roller 1 are fixed on bearing seats through bearings, transmission wheels are arranged on the calendering rotating roller 2 and the transmission rotating roller 1, the transmission rotating roller 1 and the calendering rotating roller 2 rotate relatively, the rotating speed is slow, and if the efficiency of the purging device 4 is to be guaranteed, the rotating speed of the hollow cylinder 401 needs to be fast; the hollow cylinder 401 rotates in the opposite direction to the calendering rolls 2;
the first motor can be a 220v single-phase asynchronous motor, and the power is selected from 0.75Kw-1.5 Kw; the second motor and the third motor are speed reducing motors, the type of the speed reducing motors can adopt Taizhong R series helical gear speed reducers, and the rotating speed ratio can be determined according to the process requirements.
In a preferred embodiment, shown in fig. 1, the air tube 5 is fixed to the second platform 32 by a bracket.
The working principle of the whole device is described as follows in conjunction with fig. 1:
the coated sheet material to be rolled enters from the left side of the device, and the following points are pointed out: when the device is used, the front and the rear of the device are provided with the transmission machines which are not shown in the attached drawing 1;
the hollow cylinder 401 of the purging device 4 is driven by the first driving device 61 to rotate, the rotating direction is clockwise rotation, the air nozzle 402 uses air flow to purge dust or other falling impurities on the coated sheet material, and the brush 403 is used for further cleaning the dust or other falling impurities on the coated sheet material; the double purging and cleaning functions are realized;
the transmission roller 1 and the calendering roller 2 rotate relatively, the linear speed is equal, when seen from figure 1, the transmission roller 1 rotates clockwise, the calendering roller 2 rotates anticlockwise, and the film-coated plate is subjected to heating extrusion molding treatment through the calendering roller 2; the grain on the calendering roller 2 can be imprinted on the film coating surface of the plate;
after the coated plate is subjected to calendering treatment, corresponding patterns are formed, the patterns have certain temperature, the cooling device 7 is used for cooling the coated surface of the plate in a gas cooling mode, and if the gas flow of the gas pipe 5 is too large, a valve can be arranged at the gas inlet end of the cooling device 7.