CN210336188U - A4 paper double-rotary-cutter paper cutting, ream paper production and box packaging integrated production line - Google Patents
A4 paper double-rotary-cutter paper cutting, ream paper production and box packaging integrated production line Download PDFInfo
- Publication number
- CN210336188U CN210336188U CN201921073823.1U CN201921073823U CN210336188U CN 210336188 U CN210336188 U CN 210336188U CN 201921073823 U CN201921073823 U CN 201921073823U CN 210336188 U CN210336188 U CN 210336188U
- Authority
- CN
- China
- Prior art keywords
- paper
- assembly
- ream
- driving motor
- packaging
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000004806 packaging method and process Methods 0.000 title claims abstract description 123
- 238000005520 cutting process Methods 0.000 title claims abstract description 116
- 238000004519 manufacturing process Methods 0.000 title claims abstract description 47
- 238000012856 packing Methods 0.000 claims abstract description 86
- 230000007246 mechanism Effects 0.000 claims abstract description 81
- 230000005540 biological transmission Effects 0.000 claims description 198
- 239000000463 material Substances 0.000 claims description 87
- 238000003825 pressing Methods 0.000 claims description 68
- 230000001360 synchronised effect Effects 0.000 claims description 52
- 239000003292 glue Substances 0.000 claims description 27
- 238000005507 spraying Methods 0.000 claims description 18
- 238000005452 bending Methods 0.000 claims description 17
- 210000000078 claw Anatomy 0.000 claims description 12
- 238000003756 stirring Methods 0.000 claims description 12
- 210000001503 joint Anatomy 0.000 claims description 11
- 238000007664 blowing Methods 0.000 claims description 10
- 230000003139 buffering effect Effects 0.000 claims description 9
- 238000007789 sealing Methods 0.000 claims description 9
- 230000003068 static effect Effects 0.000 claims description 9
- 238000000034 method Methods 0.000 claims description 7
- 238000007599 discharging Methods 0.000 claims description 6
- 230000005611 electricity Effects 0.000 claims description 6
- 238000009434 installation Methods 0.000 claims description 6
- 230000007306 turnover Effects 0.000 claims description 5
- 230000000903 blocking effect Effects 0.000 claims description 3
- 230000005484 gravity Effects 0.000 claims description 3
- 238000012546 transfer Methods 0.000 claims description 3
- 238000003754 machining Methods 0.000 abstract description 2
- 238000012545 processing Methods 0.000 description 9
- 230000008569 process Effects 0.000 description 4
- 230000009471 action Effects 0.000 description 2
- 238000011161 development Methods 0.000 description 2
- 238000010030 laminating Methods 0.000 description 2
- 238000012986 modification Methods 0.000 description 2
- 230000004048 modification Effects 0.000 description 2
- 230000002093 peripheral effect Effects 0.000 description 2
- 240000007643 Phytolacca americana Species 0.000 description 1
- 235000009074 Phytolacca americana Nutrition 0.000 description 1
- 230000001133 acceleration Effects 0.000 description 1
- 238000004026 adhesive bonding Methods 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 239000011248 coating agent Substances 0.000 description 1
- 238000000576 coating method Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000003993 interaction Effects 0.000 description 1
- 238000002360 preparation method Methods 0.000 description 1
- 230000007723 transport mechanism Effects 0.000 description 1
Images




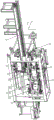



Landscapes
- Packaging Of Special Articles (AREA)
Abstract
The utility model discloses a double-rotary-knife paper cutting, ream production and case packaging integrated production line for A4 paper, which comprises a double-rotary-knife paper cutting mechanism for cutting the roller paper into A4 paper, a ream packaging machine butted with the double-rotary-knife paper cutting mechanism and used for packaging stacked A4 paper into reams, and a case packaging mechanism butted with the ream packaging machine and used for carrying out case packaging on the reams; the double-rotary-knife paper cutting mechanism comprises a paper supply assembly, a traction assembly, a slitting assembly, a transverse cutting assembly, a paper feeding assembly and a paper collecting assembly. The utility model discloses integrated paper cutting, ream packing and case packing are integrative and machining efficiency is high.
Description
Technical Field
The utility model belongs to the technical field of the paper cutting equipment technique and specifically relates to a two gyratory knife cut paper of A4 paper, order paper production and integrative production line of case packing.
Background
The paper cutter is used for cutting paper of required specifications, and the development of the traditional mechanical paper cutter to the microcomputer program control of the present day enables the production preparation time to be shorter, the cutting precision to be higher, the labor intensity to be lower and the operation to be safer, and along with the development of market economy, more and more investors all need the paper cutter which occupies less space, has small investment, fast return and strong operability.
For the processing and production of mass paper, in order to improve the production efficiency, the modern production method adopts a flow production line to operate, and each corresponding department of the flow production line is provided with automatic mechanical equipment, so that the labor intensity of workers is greatly reduced.
Firstly, the existing paper cutting and packaging processing adopts independent paper cutting equipment, ream packaging equipment and case and bag equipment for cutting and packaging, the independent equipment for processing needs to transfer products among the equipment, the processing efficiency is low, and the quality of packaged paper piles is low due to multiple transfer; secondly, the existing production line for processing and producing paper adopts equipment and mechanisms which are arranged in a line, and occupies a large production area; thirdly, an automatic production line integrating paper cutting, ream packaging and box packaging is lacked in the prior art; fourthly, the existing paper cutting equipment still sends the paper roll to the transverse cutter group in a single piece after the paper roll is subjected to slitting, so that the utilization rate of cutting, paper feeding and ream stacking is low, and the production efficiency of the paper cutter is low.
Therefore, the market needs an integrated production line integrating paper cutting, ream packaging and box packaging and having high processing efficiency, namely an A4 paper double-rotary-cutter paper cutting, ream production and box packaging.
SUMMERY OF THE UTILITY MODEL
The utility model provides a technical problem be to the defect of the existence among the above-mentioned prior art, provide an integrative A4 paper pair rotary knife cut paper, the integrative production line of order paper production and case packing of integrative just machining efficiency of integrated paper cutting, order paper packing and case packing.
In order to solve the technical problem, the utility model adopts a technical scheme that the A4 paper double-rotary-knife paper cutting, ream paper production and case packaging integrated production line comprises a double-rotary-knife paper cutting mechanism for cutting the roller paper into A4 paper, a ream packaging machine butted with the double-rotary-knife paper cutting mechanism and used for packaging stacked A4 paper into reams, and a case packaging mechanism butted with the ream packaging machine and used for carrying out case packaging on the ream paper; the paper cutting mechanism with double rotary knives comprises:
the paper feeding assembly comprises a plurality of paper feeding devices which are sequentially arranged along the paper feeding direction, and the plurality of paper feeding devices are matched with the material guide assembly arranged on the bridge frame to stack a plurality of pieces of roll paper and convey the roll paper along the paper feeding direction;
the traction assembly is arranged between the slitting assembly and the transverse cutting assembly and comprises a traction roller and a guide roller which are arranged on the frame through a bearing seat, the traction roller and the guide roller rotate in opposite directions, and the traction roller linearly draws the stacked roll paper conveyed by the paper supply assembly through the slitting assembly and then sends the rolled paper to the transverse cutting assembly;
the slitting assembly is used for longitudinally slitting the stacked roll paper into a plurality of long-strip paper;
the transverse cutting assembly is used for transversely cutting a plurality of long-strip paper into a plurality of bundles of A4 paper;
the paper feeding assembly comprises an upper paper feeding assembly and a lower paper feeding assembly, the upper paper feeding assembly comprises a high-speed upper paper feeding device and an upper paper feeding device, the lower paper feeding assembly comprises a front lower paper feeding device, a rear lower paper feeding device and a high-speed lower paper feeding device arranged between the front lower paper feeding device and the rear lower paper feeding device, the high-speed upper paper feeding device is matched with the front lower paper feeding device and the high-speed lower paper feeding device, the upper paper feeding device is matched with the rear lower paper feeding device, each pile of A4 paper is clamped in a matching mode, the paper feeding speed difference generated by the upper paper feeding assembly and the lower paper feeding assembly is matched, and the pile of A4 paper can be sequentially overlapped onto the front pile of A4 paper and the paper collecting assembly is conveyed;
the paper collecting assembly comprises a paper collecting device capable of vertically lifting, the paper collecting device gradually descends and sequentially receives each pile of A4 paper and transversely conveys the A4 paper to the ream packer after the number of the A4 paper is full of one ream.
As a further elaboration of the above technical solution:
in the technical scheme, the double-rotary-knife paper cutting mechanism further comprises a buffering paper receiving assembly, wherein the buffering paper receiving assembly is used for receiving A4 paper conveyed by the paper feeding assembly in the process that the paper collecting assembly transversely conveys the A4 paper to the ream packaging machine and transferring the received A4 paper to the paper collecting assembly, the buffering paper receiving assembly comprises a driving motor fixedly arranged at the lower part of the frame, the driving motor is connected with a truss arm through a crank matched with a connecting rod, the truss arm can move along a linear guide rail vertically arranged on the frame through transmission of the driving motor, two first linear guide rails longitudinally extending are arranged at two transverse sides of the truss arm, a bracket is arranged on the two first linear guide rails, and the bracket is in transmission connection with the first driving motor fixedly arranged at the bottom end of the truss arm through a synchronous belt transmission pair; the first driving motor drives the bracket to move along the first linear guide rail, the bracket is matched to longitudinally penetrate through a grid plate arranged on the rack, move to the paper collecting assembly and be butted with the paper feeding assembly, and the first driving motor drives the bracket to move along the first linear guide rail to be matched with and bear each pile of A4 paper; the paper receiving device comprises a second driving motor fixedly arranged on a support seat fixedly connected with the rack, the second driving motor is connected with a first truss plate through a first crank matched with a first connecting rod, two longitudinally extending support plates are arranged at the two transverse ends of the first truss plate, the support plates are connected with the rack through lead screws and can slide along the lead screws, a support plate is fixedly arranged on the two support plates, the support plate is connected with a plurality of transversely extending and longitudinally spaced load arms through support columns, a plurality of backing plates are arranged on each load arm at intervals along the transverse direction, the backing plates at the same position of the transverse direction of the load arms are matched to form a tray for supporting A4 paper, and the number of the trays is matched with the number of long-strip paper cut by the cutting assembly; the paper collecting assembly further comprises a paper aligning device, the paper aligning device comprises a truss rod movably connected with the rack through a bearing, a plurality of paper aligning baffles are fixedly arranged on the truss rod, the truss rod is further connected with the rack through an air spring, the truss rod can drive the plurality of paper aligning baffles to turn over and abut against one side surface of A4 paper conveyed to the paper collecting device by the paper feeding assembly in a matching mode, and each pile of A4 paper is arranged in a flush mode; the second driving motor drives the supporting plate and the carrier plate to slide along the screw rod and enables the carrier arm to drive the tray to move vertically, the matched paper receiving device descends gradually and sequentially receives each pile of A4 paper, the matched paper aligning device aligns and aligns each screw A4 paper and the transverse conveyor belt which is embedded between the plurality of carrier arms and fixed relative to the rack transversely conveys each ream of A4 paper, and the paper collecting assembly is enabled to finish transversely conveying the A4 paper to the ream packaging machine.
In the technical scheme, the paper supply assembly is provided with five paper supply devices, and each paper supply device comprises a supporting wall plate, a reciprocating rotary shaft, a force arm with a large end connected with the reciprocating rotary shaft, a push-pull rod movably connected with a small end of the force arm through a shaft pin and a telescopic cylinder in transmission connection with the push-pull rod; the reciprocating rotary shaft and the telescopic cylinder are arranged on the supporting wall plate; the reciprocating rotary shaft comprises a rotary shaft body and a paper roll clamping arm arranged on the rotary shaft body, the rotary shaft body is provided with two linear slide rails, one end of the paper roll clamping arm is connected with the two linear slide rails, the other end of the paper roll clamping arm is connected with a chuck for clamping roll paper, the end, connected with the linear slide rails, of the paper roll clamping arm is also in transmission connection with a first driving cylinder through a locking ring for locking the paper roll clamping arm on the rotary shaft body in a sleeved mode, and the first driving cylinder can drive the paper roll clamping arm to transversely slide along the matched linear slide rails so as to match and adjust the transverse distance between the two chucks which are transversely symmetrically; the guide subassembly includes a plurality of first guide rollers and screw thread conduction roller, all be equipped with at least one on the position of matching each paper supply device on the crane span structure first guide roller and screw thread conduction roller, the cylinder paper of arranging in on the paper supply device twines on the first guide roller and the screw thread conduction roller of matching and along the paper supply direction draft, crane span structure and subassembly butt joint position department of cutting still are equipped with and are used for carrying out range upon range of device with many cylinder paper along the draft of paper supply direction, range upon range of device is passed through including establishing a plurality of paper of leading of crane span structure upper end and vertical interval setting, and each paper leads to lead to the side and just the lower extreme and all be equipped with a conduction roller and receipts material roller respectively, and many cylinder paper along the draft of paper supply direction are twined in proper order and are passed through and are stretched out and accomplish cylinder paper range upon range of after the conduction roller, the paper leads to.
In the technical scheme, the slitting assembly comprises a first slitting knife set and a second slitting knife set arranged at the upper end and/or the lower end of the first slitting knife set; the first slitting knife group comprises a knife shaft, the knife shaft is mounted on the rack through a bearing seat, and a plurality of first slitting knives are separately mounted on the knife shaft through a blocking sleeve; the second slitting knife group comprises a knife holder which extends transversely and is fixedly connected with the rack, a dovetail chute is arranged on the longitudinal side edge of the knife holder, a plurality of mounting blocks matched with the dovetail chute are hung on the knife holder, an air cylinder is fixedly arranged on each mounting block and is in transmission connection with an electric cutter, the electric cutter is matched and right opposite to the first slitting knife in the arrangement position, and the electric cutter can cut a plurality of pieces of laminated roll paper into a plurality of pieces of strip paper by matching with the first slitting knife; the transverse cutting assembly comprises an upper knife roll and a lower knife roll which are transversely arranged and connected with the rack through bearings, one transverse end of the upper knife roll and one transverse end of the lower knife roll are fixedly provided with transmission gears which are meshed with each other, the other transverse end of the upper knife roll and the other transverse end of the lower knife roll are provided with transmission wheels, one of the two transmission wheels is in transmission connection with a guide roll of the traction assembly and a third driving motor through a transmission belt, and the third driving motor drives the upper knife roll and the lower knife roll to reversely rotate through the transmission of the transmission belt and the transmission gears; the cutter mounting grooves are symmetrically arranged in the two axial directions on the side walls of the circular peripheries of the upper cutter roll and the lower cutter roll, a transverse cutter arranged along the radial direction of the upper cutter roll or the lower cutter roll is locked in each cutter mounting groove through a wedge block and a screw, and the transverse cutter is also arranged in a cutter mounting groove matched with the extending edge of the transverse cutter; the third driving motor drives the upper knife roll, the lower knife roll and the transverse cutters arranged on the upper knife roll and the lower knife roll to reversely rotate and be meshed at intervals through the transmission belt and the transmission gear, and a plurality of long-strip papers are transversely cut into a plurality of piles of A4 papers in a matching manner; the high-speed paper feeding device comprises a high-speed paper feeding device, a front-position lower paper feeding device, a high-speed lower paper feeding device and a rear-position lower paper feeding device, wherein the high-speed paper feeding device, the front-position lower paper feeding device and the rear-position lower paper feeding device respectively comprise a paper feeding roller and a tensioning roller which are arranged on a frame through bearings and transversely, the paper feeding roller and the tensioning roller are connected; the high-speed paper feeding device comprises a high-speed upper paper feeding device, a front lower paper feeding device and a high-speed lower paper feeding device, wherein paper feeding rollers of the high-speed upper paper feeding device, the front lower paper feeding device and the high-speed lower paper feeding device are in transmission connection through a first transmission belt, the paper feeding rollers of the front lower paper feeding device are in transmission connection with a third driving motor through a first synchronous transmission wheel, a second transmission belt and a synchronous belt transmission pair, and the diameter sizes of the paper feeding rollers of the high-speed upper paper feeding device and the high-speed lower paper feeding device are the same and are larger;
the paper feeding rollers of the upper paper feeding device and the rear lower paper feeding device are also in transmission connection with a second synchronous transmission wheel arranged at the transverse side end of the frame through a fourth transmission belt, the second synchronous transmission wheel is also in transmission connection with a transmission wheel arranged on the upper knife roller through a third transmission belt, the matching enables the paper feeding rollers of the upper paper feeding device and the rear lower paper feeding device to rotate through the transmission of a third driving motor, and the diameter sizes of the paper feeding rollers of the upper paper feeding device and the rear lower paper feeding device are the same.
In the technical scheme, the ream packaging machine comprises a ream conveying belt, a ream packaging mechanism and a ream packaging mechanism, wherein the ream conveying belt is used for receiving reams from a double-rotary-cutter paper cutting mechanism and conveying the reams to the ream conveying mechanism; the ream conveying mechanism is used for receiving reams from the butt joint position of the ream conveying belt and conveying the reams to the ejection assembly; the packaging paper feeding mechanism is used for cutting the conjoined packaging paper into single packaging paper and/or conveying the single packaging paper to a paper feeding station; the liftout assembly is used for vertically jacking the wrapping paper and the A4 ream of paper to a first packaging station after vertically jacking each A4 ream of paper to the lower end of the wrapping paper positioned on the upper paper station one by one and matching with the transverse packaging assembly to finish transverse edge packaging of the ream of paper; the transverse packaging assembly comprises two paper pushing devices, a side paper clamping device, a paper pressing device and a glue spraying device which are transversely and symmetrically arranged, wherein the glue spraying device is used for spraying glue on one transverse side edge of packaging paper, the paper pressing device is used for pressing and buckling the packaging paper at the top end of an A4 ream, the side paper clamping device is used for clamping and fixing an A4 ream of paper in cooperation with the ejecting assembly, the two paper pushing devices can transversely move oppositely to bend and glue the two transverse side edges of the packaging paper and half-wrap the A4 ream of paper in a matching manner, and the two transverse paper pushing devices are also used for supporting the A4 ream of paper in cooperation with the side paper clamping device to enable the ejecting assembly to retract; the longitudinal angle folding assembly comprises a movable angle folding device and a fixed angle folding device which are transversely and symmetrically arranged, the movable angle folding device can transversely move to fold two vertex angles of one transverse side edge of a piece of packaging paper matched with A4 ream, the fixed edge folding device is matched with the ream material stirring assembly to transversely stir the A4 ream of paper, and the fixed edge folding device is matched to fold two vertex angles of the other transverse side edge of the packaging paper matched with A4 ream of paper; the longitudinal edge sealing assembly comprises two lower side edge folding heads which are longitudinally arranged at intervals, two glue spraying heads which are longitudinally symmetrically arranged and two upper side edge sealing heads which are longitudinally arranged at intervals, wherein the two lower side edge folding heads are used for turning up two lower sides of two longitudinal sides of the packaging paper when the A4 reams of paper are transversely stirred by the ream stirring assembly in a matching way, the two glue spraying heads are used for spraying glue on the two turned lower sides, and the two upper side edge sealing heads are used for turning down two upper sides of two longitudinal sides of the packaging paper and pasting the matched lower sides with the glue when the A4 reams of paper are transversely stirred by the ream stirring assembly to complete ream packaging; a ream kick-out assembly for intermittently kicking the A4 ream in the cross direction and delivering the A4 ream to a ream blanking conveyor.
In the technical scheme, the wrapping paper feeding mechanism is arranged on a traction paper feeding device, a static removing device, a cutting device and a conveying device on the box body along the longitudinal direction; the traction paper supply device comprises a discharging shaft, a drafting shaft, a pressing shaft and a tensioning shaft, wherein the drafting shaft, the pressing shaft and the tensioning shaft are arranged on a box body through bearings; the static electricity removing device comprises an air blowing nozzle fixedly arranged on the box body, and the air blowing nozzle is connected with an ion fan fixedly arranged in the box body through a pipeline and is used for blowing static electricity of the conjoined packing paper pulled by the traction paper supply device; the cutting device comprises an upper cutter holder fixedly arranged on the box body, a driving cylinder in transmission connection with an upper cutting knife is arranged on the upper cutter holder, a lower cutting knife fixedly arranged on the box body through a lower cutter holder is arranged at the matching position of the lower end of the upper cutting knife, and the upper cutting knife and the lower cutting knife are arranged in a staggered mode in the conveying direction; the driving cylinder can drive the upper cutting knife to move towards or away from the lower cutting knife, and the upper cutting knife is matched with the lower cutting knife to cut the conjoined packing paper into single packing paper with matched size; the conveying device comprises two synchronous belt conveying belts which are arranged at intervals along the transverse direction, the two synchronous belt conveying belts are in transmission connection with a fifth driving motor fixedly arranged on the box body through a rotating shaft matched with a first synchronous belt, the fifth driving motor drives the two synchronous belt conveying belts to move and is matched with a material guide plate arranged at the lower end of the fifth driving motor, and the single packing paper is conveyed to a paper feeding station through synchronous transmission; the ream paper conveying mechanism comprises a first conveying belt which is arranged on the cabinet body through a screw rod, the first conveying belt is transversely arranged, and the first conveying belt is in transmission connection with a sixth driving motor fixedly arranged on the cabinet body through a plurality of synchronous belt transmission pairs; the two circulating material guiding devices are symmetrically arranged on two longitudinal sides of the first conveying belt, the two circulating material guiding devices are in synchronous transmission connection through gears matched with a first rotating shaft, the first rotating shaft is in transmission connection with a seventh driving motor fixedly arranged on the cabinet body through a synchronous belt transmission pair, each circulating material guiding device comprises a rotating main shaft, a supporting shaft, a rotating chain wheel and a transmission chain wheel, the rotating main shaft and the supporting shaft are vertically arranged and are connected with the cabinet body through bearing seats, the rotating main shaft is in meshing transmission connection with the first rotating shaft through the gears, the rotating chain wheel and the transmission chain wheel are respectively arranged on the rotating main shaft and the supporting shaft and are in transmission connection through chains, and a plurality of material correcting plates for correcting A4 paper are further arranged on the chains; the sixth driving motor drives the first conveying belt to transversely convey A4 reams of paper, and a seventh driving motor transmission chain of the two-circulation material guide device is matched to drive the material correcting plate to circularly move, so that reams of paper are accurately conveyed to the material ejecting assembly in a matching manner; the ejection assembly comprises a supporting seat fixedly arranged on the cabinet body, an ejection frame is movably arranged on the supporting seat, a first carrier plate is arranged at the upper end of the ejection frame, the bottom end of the ejection frame is in transmission connection with an eighth driving motor fixedly arranged on the cabinet body through a hinged seat, a crank connecting rod and a swing rod, and the eighth driving motor can drive the ejection frame to drive the first carrier plate and A4 reams of paper placed on the first carrier plate to vertically move; an ejector rod is movably arranged on the supporting seat, the upper end of the ejector rod is connected with a supporting block movably embedded on the first support plate, the bottom end of the ejector rod is in transmission connection with a ninth driving motor fixedly arranged on the cabinet body through a first hinge seat, a first crank connecting rod and a first swing rod, the ninth driving motor drives the ejector rod to drive the supporting block to vertically move, and when the first support plate is vertically retracted by matching with a jacking support A4 ream, the two paper pushing devices can support an A4 ream of paper.
In the technical scheme, the two paper pushing devices respectively comprise a linear guide rail which is fixedly arranged on the cabinet body and extends transversely, a push plate is fixedly arranged on the linear guide rail, one end of the push plate is provided with an inclined wedge surface or an arc wedge surface, the other end of the push plate is in transmission connection with a tenth driving motor fixedly arranged on the cabinet body through a second hinge seat, a second crank connecting rod and a second swing rod, the push plate is driven by the tenth driving motor to slide along the linear guide rail, and the push plates of the two paper pushing devices are matched to move oppositely to bend and glue the two transverse side edges of the packaging paper and to cover A4 reams of paper in a half-coating mode; the lateral paper clamping device comprises a fixed clamping plate and a movable clamping plate, wherein the fixed clamping plate is fixedly arranged on the cabinet body, the movable clamping plate can move transversely, the movable clamping plate is connected with a first linear guide rail which is obliquely arranged, the first linear guide rail is arranged on a support which is fixedly connected with the cabinet body, the top end of the support is provided with an eleventh driving motor, the eleventh driving motor is connected with the first linear guide rail through a third oscillating bar, a third crank connecting rod and a third hinge seat and can drive a sliding rail of the first linear guide rail to slide relative to the support, and the movable clamping plate is matched with the fixed clamping plate to move transversely and is matched with the fixed clamping plate to clamp and fix A4 reams of; the paper pressing device comprises a first support fixedly arranged on the cabinet body, a second linear guide rail is vertically arranged on the first support, one end of a sliding rail of the second linear guide rail is connected with the pressing plate, the other end of the sliding rail of the second linear guide rail is in transmission connection with a twelfth driving motor fixedly arranged on the cabinet body through a fourth hinge seat, a fourth crank connecting rod and a fourth swing rod, the twelfth driving motor can drive the sliding rail of the second linear guide rail to drive the pressing plate to extend into a space between the fixed clamping plate and the movable clamping plate, and the transverse packaging assembly is matched with the top end of A4 reams of paper to finish transverse side packaging of A4 reams of paper; the movable angle folding device and the fixed angle folding device both comprise two angle folding blocks fixedly installed through an installation plate, the two angle folding blocks are arranged at intervals in the vertical direction, the installation plate of the movable angle folding device is further arranged on a third linear guide rail extending along the transverse direction, the installation plate is further in transmission connection with a second rotating shaft through a fifth crank connecting rod and a fifth swing rod, and the second rotating shaft is in transmission connection with a thirteenth driving motor fixedly arranged on the cabinet body through a synchronous belt transmission pair; the thirteenth driving motor drives the mounting plate to drive the two matched angle folding blocks to prop against two vertex angles of one transverse side edge of the packaging paper or enable two vertex angles of the other transverse side edge of the packaging paper to prop against two angle folding blocks of the fixed angle folding device when the A4 ream of paper is shifted transversely by the ream shifting assembly, and the angle folding of the longitudinal side edge of the packaging paper is completed in a matched manner; the ream paper material shifting assembly comprises two circulating material shifting devices which are longitudinally and symmetrically arranged, the two circulating material shifting devices are connected through a third rotating shaft, the third rotating shaft is also in transmission connection with a fourteenth driving motor arranged in the cabinet body through two synchronous belt transmission pairs and a fourth rotating shaft, and the fourth rotating shaft is also in transmission connection with a side edge conveying belt of a ream paper blanking conveying belt through a gear and a first transmission shaft; each circulating material shifting device comprises a first rotating chain wheel arranged on the third rotating shaft and a first transmission chain wheel arranged on the cabinet body through a bearing, the first rotating chain wheel and the first transmission chain wheel are in transmission connection through a first chain, and the first chain is further provided with eight shifting claws for shifting A4 reams; the fourteenth driving motor drives the first chain to drive the eight material shifting claws to circularly move, and the A4 reams of paper is shifted in a matched mode to transversely move.
In the technical scheme, the packing mechanism comprises a bag device, a ream feeding assembly arranged at one longitudinal end of the bag device, a discharging mechanism arranged at the other longitudinal end of the bag device and butted with the bag device, a packing box feeding assembly arranged at one transverse side of the bag device and a box cover feeding assembly; the luggage device comprises a frame body, an ejector rod mechanism and a luggage cover packaging mechanism, wherein the frame body is provided with an upper layer feeding frame and a lower layer material receiving frame, the upper layer feeding frame is provided with a feeding hole, the ejector rod mechanism comprises a plurality of ejector rods and a top plate connected with the ejector rods, the top plate is arranged corresponding to the feeding hole, a rear side pressing assembly and a front side baffle are respectively arranged on the lower layer material receiving frame corresponding to two sides of the feeding hole, and the unloading mechanism is provided with two leading-in parts; during packaging, packing box feeding assembly, case lid feeding assembly provide packing box and case lid respectively, on the packing box device will be sent to the ream to ream feeding assembly, ejector pin mechanism first moves ejector pin and roof vertical downstream one section distance, sinks the packing box into the roof after the feed inlet is in order to contact the lapse through the gravity of ream, and ejector pin mechanism drive ejector pin and roof progressively move down, lie in after the packing box fills with the ream of predetermineeing quantity on the lower floor receives the work or material rest, the front and back part of packing box is moved down the in-process and is buckled, thereby back side pressure subassembly, front side baffle and leading-in portion are buckled the week side part of packing box in proper order and are handled the packing of accomplishing the packing box, case lid packagine machine constructs packs the case lid again.
In the technical scheme, the packing box comprises a bearing part, a first bent part connected to the front edge and the rear edge of the bearing part, a second bent part connected to the left edge and the right edge of the bearing part, a third bent part connected to the two side edges of the rear first bent part and a fourth bent part connected to the two side edges of the front first bent part, wherein the rear side pressure component comprises a side pressure cylinder pivoted on the outer side of the frame body and a side pressure block pivoted on the side pressure cylinder, and the side pressure cylinder drives the side pressure block to rotate in a reciprocating manner by 90 degrees along one end of the side pressure block so as to fold and press the third bent part; a pressing assembly is further arranged between the rear side pressing assembly and the front side baffle and comprises a fifteenth driving motor and a pressing block pivoted to the fifteenth driving motor, and the fifteenth driving motor drives the pressing block to rotate back and forth by 90 degrees to press the second bending part at intervals; the place ahead of preceding side shield is located to the guiding-in portion, the top of guiding-in portion is the arcuation setting from bottom to top from the one end that is close to preceding side shield toward the one end of keeping away from preceding side shield, the top of guiding-in portion still is set up to be by the inboard edge outside edge leaned on to the side by being close to the order paper.
In the technical scheme, the box cover packaging mechanism comprises a fixed plate arranged on a frame body, a driving device arranged on the fixed plate, a first mounting plate connected with the driving device, four vertical pressing blocks respectively arranged on four edges of the first mounting plate, a pressing cylinder arranged on the vertical pressing blocks and a horizontal pressing block arranged on the pressing cylinder, wherein the driving device drives the mounting plate to move up and down, and the pressing cylinder pushes the horizontal pressing block to move inwards; the ream feeding assembly comprises a first feeding assembly, a transport frame in butt joint with the first feeding assembly, a first pushing assembly arranged on the transport frame and far away from the butt joint end with the first feeding assembly, and a second pushing assembly which is arranged perpendicular to the first pushing assembly and in butt joint with the luggage device; the first feeding assembly comprises a first belt and a motor for driving the first belt to feed; the conveying frame comprises a conveying rail, a second belt arranged on the conveying rail and a first motor driving the second belt to transmit; the first material pushing assembly comprises a third belt and a second motor for driving the third belt to feed; the second material pushing assembly comprises two first circulating material shifting devices which are transversely and symmetrically arranged, the two first circulating material shifting devices are connected through two fifth rotating shafts, one of the two fifth rotating shafts is further connected with a sixteenth driving motor arranged on the frame body through a synchronous belt transmission pair, each first circulating material shifting device comprises a second transmission chain wheel arranged on the two fifth rotating shafts, the two second transmission chain wheels of each first circulating material shifting device are in transmission connection through a second chain, and a first shifting eight claw used for shifting A4 reams to move is further arranged on each second chain; the sixteenth driving motor drives the second chain to drive the first material shifting eight claws to circularly move, and the A4 reams of paper are shifted in a matched mode to longitudinally move and push the paper to the luggage device; the packing box feeding assembly and the box cover feeding assembly comprise mounting brackets, stop pieces arranged on two sides of the mounting brackets, a third motor, a connecting rod connected with the third motor, two movable rods arranged on the connecting rod, a suction nozzle arranged on the movable rods, a second driving device and conveyor belts arranged on two sides of the mounting brackets, wherein the third motor drives the connecting rod to rotate, so that one end of each movable rod is lifted or lowered, and the second driving device drives the conveyor belts to rotate; the unloading mechanism comprises a plurality of rollers arranged side by side, and the rollers are driven by a third driving device to rotate so as to continuously unload the luggage.
The beneficial effects of the utility model reside in that: firstly, the production line of the utility model integrates paper cutting, paper feeding, ream packaging and box packaging, and the processing from roll paper to A4 paper in box packaging is completed in one time, so that the processing efficiency is high; secondly, the utility model adopts a plurality of pieces of roll paper which are fed once and can be cut and formed into four piles of five pieces of A4 wide paper once after slitting and crosscutting, and the cut paper has no rough selvedge, no sawtooth and high paper size consistency; thirdly, after cutting and forming are completed, the cut and formed paper is directly conveyed to a ream packaging machine through a directly-connected conveying belt for packaging, so that the packaging can be completed in time while the processing efficiency is improved, and the problem of ream scattering in the process of transferring reams is avoided; fourthly, after the ream paper is packed, the ream paper is directly sent to a box packing mechanism for packing the ream paper into a box, so that the ream paper is convenient to store, and the problem of difficult case caused by adopting a secondary box packing mode can be solved; fifthly, the production line of the utility model has smooth actions of cutting paper, packing reams and packing boxes, short time and high working efficiency; sixth, the utility model discloses a production line structural configuration is reasonable, area is little, equipment cost is low.
Drawings
FIG. 1 is an overall assembly view of the production line of the present invention;
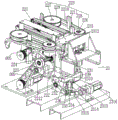
FIG. 2 is a perspective view of the paper cutting mechanism with double rotary knives according to the present invention;
fig. 3 is a perspective view of the paper feeding device of the present invention;
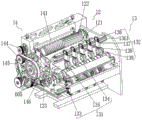
figure 4 is an assembly view of the present invention traction assembly, slitting assembly and cross-cutting assembly;
figure 5 is another assembled view of the present invention traction assembly, slitting assembly and cross-cutting assembly;
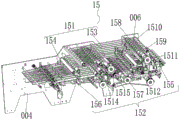
fig. 6 is a schematic structural view of the paper feeding assembly of the present invention;
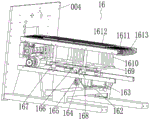
FIG. 7 is a schematic structural view of the delivery assembly of the present invention;
fig. 8 is a schematic structural view of the buffering paper receiving assembly of the present invention;
FIG. 9 is a perspective view of the ream wrap mechanism of the present invention;
FIG. 10 is a schematic structural view of a feeding mechanism for packing paper of the present invention;
FIG. 11 is an assembly view of the ream feed mechanism and ejector assembly of the present invention;
FIG. 12 is an assembly view of the transverse packing assembly, the longitudinal dog-ear assembly, the ream kicker assembly and the longitudinal banding assembly of the present invention;
FIG. 13 is a perspective view of the case and bag mechanism of the present invention;
FIG. 14 is a structural view of the luggage device of the present invention;
FIG. 15 is a view showing the structure of the cover packing mechanism of the present invention;
fig. 16 is a structural view of the feeding assembly of the packing box or the box cover of the present invention.
Detailed Description
The present invention will be described in further detail with reference to the accompanying drawings.
Fig. 1-16 an embodiment of the present invention, referring to fig. 1-16, an integrated production line for cutting paper, ream production and case packaging with a double rotary cutter of a4 paper comprises a double rotary cutter paper cutting mechanism 001 for cutting roll paper into a4 paper, a ream packaging machine 002 butted with the double rotary cutter paper cutting mechanism 001 and used for packaging stacked a4 paper into reams, and a case packaging mechanism 003 butted with the ream packaging machine 002 and used for packaging reams into cases; referring to fig. 1-16, the double rotary knife paper cutting mechanism 001 includes:
a sheet feeding unit 11, including a plurality of sheet feeding devices 111 arranged in sequence along a sheet feeding direction, wherein the plurality of sheet feeding devices 111 are used for conveying a plurality of pieces of rolled sheets in the sheet feeding direction (X direction) in a manner of stacking the plurality of pieces of rolled sheets (stacking means placing the rolled sheets one by one, and the number of the rolled sheets is matched with the number of the sheet feeding devices 111) in cooperation with a sheet guiding unit 17 arranged on the bridge 007;
a drawing assembly 12 arranged between the slitting assembly 13 and the transverse cutting assembly 14 and comprising a drawing roller 122 and a guide roller 123 which are arranged on a frame 004 through a bearing seat 121, wherein the drawing roller 122 and the guide roller 123 rotate reversely, and the drawing roller 122 linearly draws the laminated roll paper conveyed by the paper feeding assembly 11 through the slitting assembly and then conveys the rolled roll paper to the transverse cutting assembly 14;
a slitting component 13 for slitting the laminated roll paper longitudinally into a plurality of long strips, wherein each long strip comprises a plurality of laminated long strips;
the transverse cutting assembly 14 is used for transversely cutting a plurality of long-length paper into a plurality of A4 paper bundles, wherein the plurality of paper bundles means that a bundle of A4 paper can be cut from each long-length paper conveyed by the transverse cutting assembly 14 once, the plurality of long-length paper corresponds to a plurality of bundles of A4 paper, and each bundle of A4 paper comprises a plurality of A4 wide-width paper;
the paper feeding assembly 15 comprises an upper paper feeding assembly 151 and a lower paper feeding assembly 152, the upper paper feeding assembly 151 comprises a high-speed upper paper feeding device 153 and an upper paper feeding device 154, the lower paper feeding assembly 152 comprises a front lower paper feeding device 155, a rear lower paper feeding device 156 and a high-speed lower paper feeding device 157 arranged between the front lower paper feeding device 155 and the rear lower paper feeding device 156, wherein the high-speed upper paper feeding device 153 is matched with the front lower paper feeding device 155 and the high-speed lower paper feeding device 157, the upper paper feeding device 154 is matched with the rear lower paper feeding device 156 to clamp each stack of A4 paper and match with the paper feeding speed difference generated by the upper paper feeding assembly 151 and the lower paper feeding assembly 152, a stack of A4 paper can be sequentially overlapped on the front stack of A4 paper and convey the paper collecting assembly 16, it is required to be noted that the high-speed upper device 153 is matched with the front lower paper feeding device 155 and the high-speed lower paper feeding device 157 and the upper paper feeding device 154 is matched with the rear, the paper is a paper which drives the corresponding transmission belts to rotate respectively, so that A4 paper positioned between the two transmission belts is moved through the contact and matching of the transmission belts, when the rotation speeds of the two transmission belts are consistent, the A4 paper moves forwards along with the two transmission belts, when the speed difference exists between the two transmission belts, the paper clamped between the two transmission belts moves forwards under the acceleration provided by the transmission belt with a fast rotation speed on the basis of following the two transmission belts, in the embodiment, the speed difference exists between the transmission belts of the high-speed upper paper feeding device 153 and the front lower paper feeding device 155, and the speed difference does not exist between the transmission belts of the high-speed upper paper feeding device 153 and the high-speed lower paper feeding device 157, so that the paper moves at a low speed firstly, passes through the transmission section of the high-speed upper paper feeding device 153 matched with the high-speed lower paper feeding device 157, enters the transmission section of the upper paper feeding device 154, the speed is again slowed down so that a stack of a4 sheets is overlapped onto the previous stack of a4 sheets and conveyed forward to the delivery assembly 16;
the paper collecting assembly 16 comprises a paper collecting device 161 capable of vertically lifting, wherein the paper collecting device 161 gradually descends and sequentially receives each pile of A4 paper and transversely conveys the A4 paper to the ream packaging machine 002 after the number of the A4 paper is full of one ream; in this embodiment, the double rotary knife paper cutting mechanism 001 further comprises a buffering paper receiving assembly 18, the buffering paper receiving assembly 18 is used for receiving the a4 paper conveyed by the paper feeding assembly 15 and transferring the received a4 paper to the paper collecting assembly 16 during the paper collecting assembly 16 conveys the a4 paper transversely to the ream packer 002, and the received a4 paper is transferred to the paper collecting assembly 16, namely, the buffering paper receiving assembly 18 returns the paper collecting assembly 16 to the matched paper collecting position.
Referring to fig. 1-2 and fig. 6-8, in this embodiment, the buffering paper receiving assembly 18 includes a driving motor 181 fixed at the lower portion of the rack 004, the driving motor 181 is connected to a truss arm 184 through a crank 182 in cooperation with a connecting rod 183, the truss arm 184 can be driven by the driving motor 181 to move along a linear guide 185 vertically arranged on the rack 004, two first linear guides 186 longitudinally (in the X direction) are arranged on two lateral (in the Y direction) sides of the truss arm 184, a bracket 187 is arranged on the two first linear guides 186, and the bracket 187 is in transmission connection with a first driving motor 188 fixed at the bottom end of the truss arm 184 through a synchronous belt transmission pair 005; the first driving motor 188 drives the bracket 187 to move along the first linear guide 186, so that the bracket 187 longitudinally penetrates through a grid plate 189 arranged on the frame 004 and moves to the paper collecting assembly 16 and is butted with the paper feeding assembly 15, and the first driving motor 188 drives the bracket 187 to move along the first linear guide 186 to match and receive each stack of A4 paper; in this embodiment, the paper receiving device 161 includes a second driving motor 163 fixedly disposed on a support base 162 fixedly connected to a frame 004, the second driving motor 163 is connected to a first truss 166 through a first crank 164 in cooperation with a first connecting rod 165, two longitudinally extending support plates 167 are disposed at two lateral ends of the first truss 166, the support plates 167 are connected to the frame 004 through screws 168 and can slide along the screws 168, a carrier plate 169 is further fixedly disposed on the two support plates 167, the carrier plate 169 is connected 1610 to a plurality of carrier arms 1611 extending in the lateral direction and disposed at longitudinal intervals through support columns, a plurality of base plates 1612 are disposed on each of the carrier arms 1611 at intervals in the lateral direction, the base plates 1613 at the same position in the lateral direction of the carrier arms 1611 are matched to form a tray for carrying a4 paper, and the number of the trays is matched with the number of long-strip papers slit by the slitting assembly 13; the paper collecting assembly 16 further comprises a paper aligning device 1810, the paper aligning device 1810 comprises a truss 1811 movably connected with the rack 004 through a bearing 006, a plurality of paper aligning baffles 1812 are fixedly arranged on the truss 1811, the truss 1811 is further connected with the rack 004 through a gas spring 1813, the truss 1811 can drive the plurality of paper aligning baffles 1812 to overturn to match and abut against one side surface of a4 paper which is sent to the paper collecting device 161 by the paper feeding assembly 15 so as to arrange each bundle of A4 paper; the second driving motor 163 drives the supporting plate 167 and the carrier plate 169 to slide along the screw rod 168, and the carrier arm 1611 drives the tray to move vertically, so that the matching paper receiving device 161 descends gradually and receives each stack of a4 paper in turn, and the matching paper aligning device 1810 aligns each screw a4 paper and horizontally conveys each ream of a4 paper by the horizontal conveying belt 1613 which is embedded between the multiple carrier arms 1611 and fixed relative to the frame 004, so that the paper collecting assembly 16 finishes horizontally conveying the a4 paper to the ream packaging machine 002.
Referring to fig. 1-3, in the present embodiment, the paper feeding assembly 11 is provided with five paper feeding devices 111, each paper feeding device 111 includes a supporting wall plate 112, a reciprocating rotation shaft 113, a force arm 114 with a large end connected to the reciprocating rotation shaft 113, a push-pull rod 115 movably connected to a small end of the force arm 114 via a shaft pin (not numbered in the drawings), and a telescopic cylinder 116 in transmission connection with the push-pull rod 115; wherein, the reciprocating rotary shaft 113 and the telescopic cylinder 116 are installed on the supporting wall plate 112; the reciprocating rotation shaft 113 comprises a rotation shaft body 1131 and a paper roll clamping arm 1132 arranged on the rotation shaft body 1131, the rotation shaft body 1131 is provided with two linear slide rails 117, one end of the paper roll clamping arm 1132 is connected with the two linear slide rails 117, the other end of the paper roll clamping arm 1132 is connected with a clamping head 118 used for clamping roll paper, the end of the paper roll clamping arm 1132 connected with the linear slide rails 117 is also in transmission connection with a first driving cylinder (not shown in the figure) through a locking ring 119 which locks the paper roll clamping arm 1132 on the rotation shaft body 1131 in a sleeving manner, and the first driving cylinder can drive the paper roll clamping arm 1132 to transversely slide along the matched linear slide rails 117 so as to match and adjust the transverse distance between the two clamping heads 118; the material guiding assembly 17 comprises a plurality of first material guiding rollers 171 and a thread transmission roller 172, at least one first material guiding roller 171 and a thread transmission roller 172 are arranged on the bridge 007 at the position matched with each paper feeding device 111, the roll paper placed on the paper feeding device 111 is wound on the matched first material guiding rollers 171 and thread transmission roller 172 and drafted along the paper feeding direction, a laminating device 173 for laminating a plurality of pieces of roll paper drafted along the paper feeding direction is further arranged at the butt joint position of the bridge 007 and the slitting component 13, the stacking device 173 includes a plurality of paper guide passages 174 provided at the upper end of the bridge 007 and longitudinally spaced apart from each other, a guide roller 175 and a receiving roller 176 are provided at the side and right lower end of each paper guide passage 174, and a plurality of rolled papers drafted along the paper feeding direction are sequentially wound around the matched guide roller 175, paper guide passages 174 and receiving rollers 176 and then extend along the stacking paper guide passage 177 to complete the stacking of the rolled papers.
Referring to fig. 1-2 and 3-5, in this embodiment, the slitting assembly 13 includes a first slitting knife set 131 and a second slitting knife set 132 disposed at the upper end and/or the lower end of the first slitting knife set 131, and in practice, the second slitting knife set 132 may be disposed at the upper end or the lower end of the first slitting knife set 131, or the second slitting knife set 132 may be disposed at both the upper end and the lower end according to the requirement; the first slitting knife group 131 comprises a knife shaft 133, the knife shaft 133 is mounted on the frame 004 through a bearing seat 121, and a plurality of first slitting knives 135 are mounted on the knife shaft 133 in a separated manner through a blocking sleeve 134; the second slitting knife group 132 comprises a knife holder 136 which extends transversely and is fixedly connected with the rack 004, a dovetail sliding groove 1361 is formed in the longitudinal side edge of the knife holder 136, a plurality of mounting blocks 137 matched with the dovetail sliding groove 1361 are hung on the knife holder 136, an air cylinder 138 is fixedly arranged on the mounting blocks 137, the air cylinder 138 is in transmission connection with an electric cutter 139, the electric cutter 139 is matched and opposite to the first slitting knife 135 in the arrangement position, and the electric cutter 139 can cut a plurality of pieces of laminated roll paper into a plurality of pieces of long-strip paper by matching with the first slitting knife 135; in this embodiment, the transverse cutting assembly 14 includes an upper knife roller 141 and a lower knife roller 142 which are transversely arranged and connected with the frame 004 through a bearing 006, one transverse end of the upper knife roller 141 and one transverse end of the lower knife roller 142 are fixedly provided with a transmission gear 143 which is engaged with each other, the other transverse end of the upper knife roller 141 and the other transverse end of the lower knife roller 142 are provided with transmission wheels 144, one of the two transmission wheels 144 is in transmission connection with the guide roller 123 of the traction assembly 12 and a third driving motor 146 through a transmission belt 145, and the third driving motor 146 drives the upper knife roller 141 and the lower knife roller 142 to reversely rotate through the transmission of the transmission belt 145 and the transmission gear 143; the circular peripheral side walls of the upper knife roll 141 and the lower knife roll 142 are respectively provided with two axially symmetrical knife installing grooves 1411, a cross knife 148 installed along the radial direction of the upper knife roll 141 or the lower knife roll 142 is locked in each knife installing groove 1411 through a wedge 147 matched with a screw (not shown in the figure), and the cross knife 148 is also arranged as a knife installing groove 1411 matched with the knife edge of the cross knife 148 in a protruding manner; the third driving motor 146 drives the upper knife roll 141, the lower knife roll 142 and the transverse knife 148 arranged on the upper knife roll 141 and the lower knife roll 142 to rotate reversely and engage at intervals through the driving belt 145 and the driving gear 143, so that a plurality of long sheets are transversely cut into a plurality of bundles of A4 sheets.
Referring to fig. 1 and fig. 4-6, in this embodiment, the high-speed paper feeding device 153, the paper feeding device 154, the front paper feeding device 155, the high-speed paper feeding device 157 and the rear paper feeding device 156 each include a paper feeding roller 158 and a tension roller 159 mounted transversely on a frame 004 through a bearing 006, the paper feeding roller 158 and the tension roller 159 are further connected by a transmission belt 1510, and a synchronous transmission wheel 1511 is provided at one transverse end of the paper feeding roller 158; the paper feeding rollers 158 of the high-speed paper feeding device 153, the front lower paper feeding device 155 and the high-speed lower paper feeding device 157 are in transmission connection through a first transmission belt 1512, the paper feeding roller 158 of the front lower paper feeding device 155 is in transmission connection with the third driving motor 146 through a first synchronous transmission wheel 1513, a second transmission belt (not shown in the figures) and a synchronous belt transmission pair 005, and the diameter sizes of the paper feeding rollers 158 of the high-speed paper feeding device 153 and the high-speed lower paper feeding device 157 are the same and larger than that of the paper feeding roller 158 of the front lower paper feeding device 155; the paper feeding rollers 158 of the upper paper feeding device 154 and the rear lower paper feeding device 156 are also in transmission connection with a second synchronous transmission wheel 1515 arranged at the transverse side end of the frame 004 through a fourth transmission belt 1514, the second synchronous transmission wheel 1515 is also in transmission connection with a transmission wheel 144 arranged on the upper knife roller 141 through a third transmission belt (not shown in the figures), matching is realized so that the paper feeding rollers 158 of the upper paper feeding device 154 and the rear lower paper feeding device 156 can be in transmission rotation through a third driving motor 146, and the diameter sizes of the paper feeding rollers 158 of the upper paper feeding device 154 and the rear lower paper feeding device 156 are the same.
Referring to fig. 1, 9-12, in this embodiment, the ream wrap machine 002 includes:
a ream transport belt 21 for receiving reams (a 4 sheets of paper having a matching number) from the double-rotary-blade paper cutting mechanism 001 and transporting the reams to the ream transport mechanism 22;
a ream conveying mechanism 22 for receiving reams from a position abutting the ream conveyor belt 21 and conveying the reams to the ejector assembly 23;
a wrapping paper feeding mechanism 24 for cutting the conjoined wrapping paper into individual wrapping paper and/or conveying the individual wrapping paper to a paper feeding station (not numbered in the figure);
the liftout assembly 23 is used for vertically jacking the wrapping paper and the A4 reams of paper to a first packaging station after vertically jacking each A4 ream (the ream is jacked up one ream) to the lower end of the wrapping paper positioned on the upper paper station, and completing ream transverse edge packaging by matching with the transverse packaging assembly 25;
the transverse packaging assembly 25 comprises two paper pushing devices 251, two side paper clamping devices 252, two paper pressing devices 253 and a glue spraying device 254 which are transversely and symmetrically arranged, wherein the glue spraying device 254 is used for spraying glue on one transverse side edge of the packaging paper, the paper pressing device 253 is used for pressing and buckling the packaging paper at the top end of the A4 ream, the side paper clamping devices 252 are used for clamping and fixing the A4 ream of paper in cooperation with the jacking assembly 23, the two paper pushing devices 251 can transversely move oppositely to bend and glue two transverse side edges of the packaging paper and half wrap the A4 ream of paper, actually, the two transverse paper pushing devices 251 are used for pressing and folding the two side edges which bend 90 degrees at the side edges in the process of vertically jacking the A4 ream and the packaging paper to be parallel to the plane of the top end of the packaging paper and gluing to be a rectangular box-shaped packaging paper, and the two transverse paper pushing devices 251 are also used for supporting the A4 ream in cooperation with the side paper clamping devices 252 to enable the jacking assembly 23; it should be noted that, when actually packaging the ream at the lateral side, the liftout assembly 23 firstly pushes the ream to the paper feeding station and contacts with the wrapping paper, the liftout assembly 23 continues to push up the ream and the wrapping paper to contact with the paper pressing device 253 at low pressure, at this time, the wrapping paper at the lateral sides of the ream is bent by the vertical plate on the rack 004 for 90 degrees, at this time, the liftout assembly 23 continues to push the ream upwards, at the same time, the lateral paper clamping device 252 clamps and fixes the ream and for a short time, and within the short time, the liftout assembly 23 starts to move vertically and move backwards, at this time, the two paper pushing devices 251 rapidly move laterally and extend into the space between the bottom end of the ream and the liftout assembly 23, push the lateral side of the wrapping paper and bend, and at the same time, the lateral paper clamping device 252 cooperates to support and fix the ream, and match to prevent the ream;
the longitudinal angle folding assembly 26 comprises a movable angle folding device 261 and a fixed angle folding device 262 which are transversely and symmetrically arranged, the movable angle folding device 261 can transversely move to fold two vertex angles of one transverse side edge of a packing paper matched with A4 ream, the fixed angle folding device 262 is matched with the ream material shifting assembly 27 to transversely shift A4 ream of paper, and the two vertex angles of the other transverse side edge of the packing paper matched with A4 ream are folded;
a ream kick-out assembly 27 for intermittently kicking a4 reams in the transverse direction and delivering a4 reams to a ream blanking conveyor 29;
longitudinal edge sealing assembly 28 comprises two lower side edge folding heads 281 arranged at a longitudinal interval, two glue spraying heads 282 arranged in a longitudinal symmetrical mode and two upper side edge sealing heads 283 arranged at a longitudinal interval, wherein the two lower side edge folding heads 281 are used for matching with a ream stirring assembly 27 to transversely stir an A4 ream to turn up and turn over two lower sides of two longitudinal sides of packaging paper, the two glue spraying heads 282 are used for spraying glue on the two lower sides of the turn-over, and the two upper side edge sealing heads 283 are used for matching with the ream stirring assembly 27 to transversely stir an A4 ream to turn down and turn over two upper sides of two longitudinal sides of the packaging paper and glue with the matched lower sides to complete ream packaging.
Referring to fig. 9 to 12, in the present embodiment, the wrapping paper feeding mechanism 24 is provided with a drawing paper feeding device 241, a static removing device 242, a cutting device 243 and a conveying device 244 on the box 008 along the longitudinal direction (X direction); the drawing and paper feeding device 241 comprises a discharging shaft 2411, a drawing shaft 2412, a pressing shaft 2413 and a tensioning shaft 2414 which are arranged on the box 008 through a bearing 006, wherein cylindrical conjoined packing paper is placed on the discharging shaft 2411 and is wound on the drawing shaft 2412 and the tensioning shaft 2414, the drawing shaft 2412 is in transmission connection with a fourth driving motor (not shown in the drawing) arranged on the box 008 through a synchronous belt (not numbered in the drawing) or a transmission chain (not numbered in the drawing), in the embodiment, the drawing shafts 2412 are arranged in two numbers, the fourth driving motor can drive the drawing shaft 2412 to rotate and draw the roller packing paper to pass through the cutting device 243 and then send the roller packing paper to the conveying device 244, and the pressing shaft 2413 is arranged at the vertical upper end of the drawing shaft 2412 and can vertically move relative to the drawing shaft 2412 to adjust the vertical distance between the pressing shaft 2412 and match with or loosen the packing paper; the static electricity removing device 242 comprises an air blowing nozzle 2421 fixedly arranged on the box 008, and the air blowing nozzle 2421 is connected with an ion fan 2422 (centrifugal fan) fixedly arranged in the box 008 through a pipeline (not shown in the figure) and is used for blowing the static electricity of the conjoined packing paper drawn by the drawing paper supply device 241; the cutting device 243 comprises an upper cutter holder 2431 fixedly arranged on the box 008, a driving cylinder 2433 in transmission connection with an upper cutting knife 2432 is arranged on the upper cutter holder 2431, a lower cutting knife 2435 fixedly arranged on the box 008 through a lower cutter holder (not shown in the drawing) is arranged at the lower end matching position of the upper cutting knife 2432, and the upper cutting knife 2432 and the lower cutting knife 2435 are arranged in a staggered mode in the conveying direction, so that the packaging paper can be cut through the interaction of the cutter edges of the upper cutting knife 2432 and the lower cutting knife 2435; the driving cylinder 2433 can drive the upper cutting knife 2432 to move towards or away from the lower cutting knife 2435, and the upper cutting knife 2432 is matched with the lower cutting knife 2435 to cut the conjoined packing paper into single packing paper with matched size; the conveying device 244 comprises two synchronous belt conveyor belts 2441 arranged at intervals along the transverse direction, the two synchronous belt conveyor belts 2441 are in transmission connection with a fifth driving motor 2444 fixedly arranged on the box 008 through a rotating shaft 2442 matched with a first synchronous belt 2443, the fifth driving motor 2444 drives the two synchronous belt conveyor belts 2441 to move and is matched with a material guide plate 2445 arranged at the lower end of the fifth synchronous belt conveyor belts, and single packing paper is synchronously driven to be transferred between the two synchronous belt conveyor belts 2441 and the material guide plate 2445 and conveyed to a paper feeding station.
Referring to fig. 9-12, in the present embodiment, the ream feeding mechanism 22 includes a first conveyor belt 221 mounted on the cabinet 008 through a lead screw 168, and the first conveyor belt 221 is installed along the transverse direction, and the first conveyor belt 221 is in transmission connection with a sixth driving motor 222 fixed on the cabinet 008 through a plurality of synchronous belt transmission pairs 005; two circulating material guiding devices 223 are symmetrically arranged on two longitudinal sides of the first conveying belt 221, the two circulating material guiding devices 223 are in synchronous transmission connection through a gear 224 and a first rotating shaft 225, the first rotating shaft 225 is further in transmission connection with a seventh driving motor 2212 fixedly arranged on a cabinet 008 through a synchronous belt transmission pair 005, each circulating material guiding device 223 comprises a rotating main shaft 226, a supporting shaft 227, a rotating chain wheel 228 and a transmission chain wheel 229, the rotating main shaft 226 and the supporting shaft 227 are vertically arranged and are both connected with the cabinet 008 through a bearing seat 121, the rotating main shaft 226 is further in meshing transmission connection with the first rotating shaft 225 through the gear 224, the rotating chain wheel 228 and the transmission chain wheel 229 are respectively arranged on the rotating main shaft 226 and the supporting shaft 227 and are in transmission connection through a chain 2210, and a plurality of material correcting plates 2211 for correcting paper by A4 are further arranged on the chain 2210; the sixth driving motor 222 drives the first conveying belt 221 to transversely convey a4 reams of paper, and the seventh driving motor 2212 of the two-circulation material guiding device 223 drives the material correcting plate 2211 to circularly move by matching with the seventh driving motor 2212, so that the reams of paper are accurately conveyed to the material ejecting assembly 23;
the material ejecting assembly 23 comprises a supporting seat 231 fixedly arranged on the cabinet 008, a material ejecting rack 232 is movably arranged on the supporting seat 231, a first carrier plate 233 is arranged at the upper end of the material ejecting rack 232, the bottom end of the material ejecting rack 232 is in transmission connection with an eighth driving motor 239 fixedly arranged on the cabinet 008 through a hinge seat 234, a crank connecting rod 235 and a swing rod 236, and the eighth driving motor 239 can drive the material ejecting rack 232 to drive the first carrier plate 233 and A4 reams placed on the first carrier plate 233 to vertically move; an ejector rod 2310 is movably arranged on the supporting seat 232, the upper end of the ejector rod 2310 is connected with a supporting block 2312 movably embedded on the first carrier plate 233, the bottom end of the ejector rod 2310 is in transmission connection with a ninth driving motor 2316 fixedly arranged on the cabinet 008 through a first hinge seat 2313, a first crank connecting rod 2314 and a first swing rod 2315, the ninth driving motor 2316 drives the ejector rod 2310 to drive the supporting block 2312 to vertically move, and when the first carrier plate 233 vertically retracts due to the fact that supporting A4 reams are jacked in a matched mode, the two paper pushing devices 251 can support the A4 reams; in this embodiment, each of the two paper pushing devices 251 includes a linear guide 2511 which is fixedly arranged on the cabinet 008 and extends transversely, a push plate 2512 is fixedly arranged on the linear guide 2511, one end of the push plate 2512 is provided with an inclined wedge surface or an arc wedge surface, an air blowing plate is further arranged on the push plate 2512 which is arranged on the arc wedge surface, the side edge of the corresponding side of the wrapping paper is matched with and blown to move transversely, the other end of the push plate 2512 is in transmission connection with a tenth driving motor 2516 which is fixedly arranged on the cabinet 008 through a second hinge seat 2513, a second crank connecting rod 2514 and a second swing rod 2515, the tenth driving motor 2516 drives the push plate 2512 to slide along the linear guide 2511, and the push plates 2512 of the two paper pushing devices 251 are matched to move oppositely to bend and glue the two transverse side edges of the wrapping paper and to half-wrap the a 4; in this embodiment, the paper side-clamping device 252 includes a fixed clamp 2521 fixed on the cabinet 008 and a movable clamp 2522 capable of moving laterally, the movable clamp 2522 is connected to a first linear guide 2523 disposed obliquely, the first linear guide 2523 is disposed on a support 2524 fixedly connected to the cabinet 008, an eleventh driving motor 2525 is disposed at a top end of the support 2524, the eleventh driving motor 2525 is connected to the first linear guide 2523 through a third oscillating bar 2526, a third crank link 2527 and a third hinge 2528 and can drive a sliding rail of the first linear guide 2523 to slide relative to the support 2524, and the movable clamp 2522 is driven to move laterally and cooperate with the fixed clamp 2521 to clamp and fix a4 reams of paper; in this embodiment, the paper pressing device 253 includes a first support 2531 fixed on the cabinet 008, a second linear guide 2532 is vertically installed on the first support 2531, one end of a slide rail of the second linear guide 2532 is connected to the pressing plate 2533, the other end of the slide rail is in transmission connection with a twelfth driving motor 2537 fixed on the cabinet 008 through a fourth hinge seat 2534, a fourth crank link 2535 and a fourth swing rod 2536, the twelfth driving motor 2537 can drive the slide rail of the second linear guide 2532 to drive the pressing plate 2538 to extend into a space between the fixed clamping plate 2521 and the movable clamping plate 2522, and the transverse packing assembly 25 is assisted to complete transverse side packing of a4 reams of paper by matching with the top end of a4 ream of the ream of paper; in this embodiment, each of the movable folding angle device 261 and the fixed folding angle device 262 includes two folding angle blocks 264 fixedly installed through a mounting plate 263, the two folding angle blocks 264 are arranged at intervals in the vertical direction, the mounting plate 263 of the movable folding angle device 261 is further installed on a third linear guide rail 265 extending in the transverse direction, the mounting plate 265 is further in transmission connection with a second rotating shaft 268 through a fifth crank connecting rod 266 and a fifth swing rod 267, and the second rotating shaft 268 is in transmission connection with a thirteenth driving motor 269 fixedly arranged on the cabinet 008 through a synchronous belt transmission pair 005; the thirteenth driving motor 269 drives the mounting plate 265 to drive the two matched corner folding blocks 264 to prop against two top corners of one lateral side of the packaging paper or to prop against two top corners of the other lateral side of the packaging paper by the two corner folding blocks 264 of the fixed corner folding device 262 when the ream shifting assembly 27 shifts a4 ream of paper in the lateral direction, so as to complete the corner folding of the longitudinal side of the packaging paper; the ream material shifting assembly 27 comprises two circulating material shifting devices 271 which are longitudinally and symmetrically arranged, the two circulating material shifting devices 272 are connected through a third rotating shaft 273, the third rotating shaft 273 is in transmission connection with a fourteenth driving motor 275 arranged in the cabinet 008 through two synchronous belt transmission pairs 005 and a fourth rotating shaft 274, and the fourth rotating shaft 274 is in transmission connection with a side edge conveying belt 291 of the ream material blanking conveying belt 29 through a gear 224 and a first transmission shaft 276; each circulating material shifting device 271 comprises a first rotating chain wheel 2711 arranged on the third rotating shaft 273 and a first driving chain wheel 2712 arranged on the cabinet 008 through a bearing 006, the first rotating chain wheel 2711 and the first driving chain wheel 2712 are in transmission connection through a first chain 2713, and the first chain 2713 is further provided with eight shifting claws 2714 for shifting A4 reams to move; the fourteenth driving motor 275 drives the first chain 2713 to drive the eight material poking claws 2714 to circularly move, and pokes A4 to make the paper transversely move in a matching mode.
Referring to fig. 1 and fig. 13-16, in this embodiment, the packing mechanism 003 includes a packing device 31, a ream feeding assembly 32 disposed at one longitudinal end of the packing device 31, a blanking mechanism 33 disposed at the other longitudinal end of the packing device 31 and abutting against the longitudinal end of the packing device, a packing box feeding assembly 34 disposed at one lateral side of the packing device 31, and a box cover feeding assembly 35; wherein,
the luggage device 31 comprises a frame body 009, an ejector rod mechanism 36 and a luggage cover packing mechanism 37, wherein the frame body 009 is provided with an upper layer feeding frame 38 and a lower layer material receiving frame 39, the upper layer feeding frame 38 is provided with a feeding hole (not numbered in the drawing), the ejector rod mechanism 36 comprises a plurality of ejector rods 361 and a top plate 362 connected with the ejector rods 361, the top plate 362 is arranged corresponding to the feeding hole, and the lower layer material receiving frame 39 is respectively provided with a rear side pressure component 310 and a front side baffle 311 at two sides corresponding to the feeding hole; the blanking mechanism 33 is provided with two lead-in parts 334; when the case is packed, the packing case feeding component 34 and the case cover feeding component 35 respectively provide a packing case and a case cover, the ream feeding component 32 feeds reams onto the case device 31, the push rod mechanism 36 drives the push rod 361 and the top plate 362 to vertically move downwards for a certain distance, the packing box is sunk into the feeding hole by the gravity of the paper to contact the top plate 362 which moves downwards, the push rod mechanism 36 drives the push rod 361 and the top plate 362 to move downwards gradually until the packing box is positioned on the lower layer material receiving frame 39 after being filled with the preset number of paper reams, in practice, the push rod 361 is driven by the material pushing motor 363 to carry out jacking action, the front and rear parts of the packing box are bent in the downward moving process, the rear side pressing assembly 310, the front side baffle 311 and the guide-in part sequentially bend the peripheral side part of the packing box to complete the packing of the packing box, and then the box cover packing mechanism 37 packs the box cover; in this embodiment, the packing box includes a carrying portion, a first bending portion connected to the front and rear edges of the carrying portion, a second bending portion connected to the left and right edges of the carrying portion, a third bending portion connected to the two side edges of the rear first bending portion, and a fourth bending portion connected to the two side edges of the front first bending portion, the rear side pressing assembly 310 includes a side pressing cylinder 3101 pivoted outside the frame body 009 and a side pressing block 3102 pivoted on the side pressing cylinder 3101, the side pressing cylinder 3101 drives the side pressing block 3102 to rotate reciprocally 90 ° along one end of the side pressing block 3102 to fold and press the third bending portion; a pressing component 312 is further arranged between the rear side pressing component 310 and the front side baffle 311, the pressing component 312 includes a fifteenth driving motor 3121 and a pressing block 3122 pivoted to the fifteenth driving motor 3121, the fifteenth driving motor 3121 drives the pressing block 3122 to rotate back and forth by 90 degrees, so as to press the second bending portion at intervals; the leading-in part 334 is arranged in front of the front baffle 311, the top of the leading-in part 334 is curved from bottom to top from the end close to the front baffle 311 to the end far away from the front baffle 311, and the top of the leading-in part 334 is also arranged to be inclined upwards from the inner side edge close to the ream to the outer side edge;
in this embodiment, the box cover packing mechanism 37 includes a fixing plate 371 disposed on the frame body 009, a driving device 372 disposed on the fixing plate 371, a first mounting plate 373 connected to the driving device 372, four vertical pressing blocks 374 respectively disposed on four edges of the first mounting plate 373, a pressing cylinder 375 disposed on the vertical pressing blocks 374, and a horizontal pressing block 376 disposed on the pressing cylinder 375, wherein the driving device 372 drives the mounting plate 373 to move up and down, and the pressing cylinder 375 pushes the horizontal pressing block 376 to move inward; in this embodiment, the ream feeding assembly 32 includes a first feeding assembly 321, a transporting rack 322 butted with the first feeding assembly 321, a first pushing assembly 323 arranged on the transporting rack 322 far from the end butted with the first feeding assembly 321, and a second pushing assembly 324 arranged perpendicular to the first pushing assembly 323 and butted with the bag device 31; in this embodiment, the first feeding assembly 321 includes a first belt 3211 and a motor 3212 for driving the first belt to feed 3211; the transportation frame 322 comprises a conveying track 3221, a second belt 3222 arranged on the conveying track 3221, and a first motor 3223 for driving the second belt 3222 to transmit; the first material pushing assembly 323 comprises a third belt 3231 and a second motor 3232 for driving the third belt 3231 to feed; the second pushing assembly 324 comprises two first circulating material shifting devices 3241 which are transversely and symmetrically arranged, the two first circulating material shifting devices 3241 are connected through two fifth rotating shafts 3242, one of the two fifth rotating shafts 3242 is further connected with a sixteenth driving motor 3243 arranged on a frame body 009 through a synchronous belt transmission pair 005, each first circulating material shifting device 3241 comprises a second driving chain wheel 3244 arranged on the two fifth rotating shafts 3242, the two second driving chain wheels 3244 of each first circulating material shifting device 3241 are in transmission connection through a second chain 3245, and the second chain 3245 is further provided with a first shifting eight claw 3246 for shifting A4 to move paper; the sixteenth driving motor 3233 drives the second chain 3245 to drive the first material shifting eight claws 3246 to circularly move, and the A4 is shifted in a matching manner to enable the paper to longitudinally move and push the paper to the luggage device;
the packing box feeding assembly 34 and the box cover feeding assembly 35 both include a mounting bracket 341, a stop member 342, a third motor 343, a connecting rod 344 connected to the third motor 343, two movable rods 345 arranged on the connecting rod 344, suction nozzles 346 arranged on the movable rods 345, a second driving device 347, and conveyor belts 348 arranged on both sides of the mounting bracket 341, wherein the third motor 343 drives the connecting rod 344 to rotate, so that one end of the movable rod 345 is lifted or lowered, and the second driving device 347 drives the conveyor belts 348 to rotate; the blanking mechanism 33 includes a plurality of rollers 331 arranged side by side, and the rollers 331 are in transmission connection with a third driving motor (not shown in the drawings) through a chain transmission pair 333, and are driven by a third driving device to rotate, so that the rollers 331 continuously blank the luggage.
For further explanation of the operation principle of the bag mechanism 003 and the structures of the bag device 31, the unloading mechanism 33, the packing box feeding assembly 34, the box cover feeding assembly 35, the ejector rod mechanism 36 and the box cover packing mechanism 37, reference is made to the fully automatic bag packing machine of the chinese patent (patent No. 201310430464.1, the utility model of which is the creator of the present practice), and detailed description is not given herein.
The above is not intended to limit the technical scope of the present invention, and any modifications, equivalent changes and modifications made to the above embodiments according to the technical spirit of the present invention are all within the scope of the technical solution of the present invention.
Claims (10)
- The production line is characterized by comprising a double-rotary-cutter paper cutting mechanism for cutting roll paper into A4 paper, a ream packaging machine butted with the double-rotary-cutter paper cutting mechanism and used for packaging stacked A4 paper into reams, and a box packaging mechanism butted with the ream packaging machine and used for packaging the reams; the paper cutting mechanism with double rotary knives comprises:the paper feeding assembly comprises a plurality of paper feeding devices which are sequentially arranged along the paper feeding direction, and the plurality of paper feeding devices are matched with the material guide assembly arranged on the bridge frame to stack a plurality of pieces of roll paper and convey the roll paper along the paper feeding direction;the traction assembly is arranged between the slitting assembly and the transverse cutting assembly and comprises a traction roller and a guide roller which are arranged on the frame through a bearing seat, the traction roller and the guide roller rotate in opposite directions, and the traction roller linearly draws the stacked roll paper conveyed by the paper supply assembly through the slitting assembly and then sends the rolled paper to the transverse cutting assembly;the slitting assembly is used for longitudinally slitting the stacked roll paper into a plurality of long-strip paper;the transverse cutting assembly is used for transversely cutting a plurality of long-strip paper into a plurality of bundles of A4 paper;the paper feeding assembly comprises an upper paper feeding assembly and a lower paper feeding assembly, the upper paper feeding assembly comprises a high-speed upper paper feeding device and an upper paper feeding device, the lower paper feeding assembly comprises a front lower paper feeding device, a rear lower paper feeding device and a high-speed lower paper feeding device arranged between the front lower paper feeding device and the rear lower paper feeding device, the high-speed upper paper feeding device is matched with the front lower paper feeding device and the high-speed lower paper feeding device, the upper paper feeding device is matched with the rear lower paper feeding device, each pile of A4 paper is clamped in a matching mode, the paper feeding speed difference generated by the upper paper feeding assembly and the lower paper feeding assembly is matched, and the pile of A4 paper can be sequentially overlapped onto the front pile of A4 paper and the paper collecting assembly is conveyed;the paper collecting assembly comprises a paper collecting device capable of vertically lifting, the paper collecting device gradually descends and sequentially receives each pile of A4 paper and transversely conveys the A4 paper to the ream packer after the number of the A4 paper is full of one ream.
- 2. The A4 paper double-rotary-knife paper-cutting, ream-making, and carton-packing integrated line of claim 1, wherein the double-rotary-knife paper-cutting mechanism further comprises a buffer splicing assembly for receiving A4 paper from the paper-feeding assembly during the lateral transfer of A4 paper from the paper-feeding assembly to the ream-packing machine and for transferring the received A4 paper to the paper-feeding assembly, wherein,the buffering paper receiving assembly comprises a driving motor fixedly arranged at the lower part of the rack, the driving motor is connected with a truss arm through a crank matched with a connecting rod, the truss arm can move along a linear guide rail vertically arranged on the rack through the transmission of the driving motor, two first linear guide rails longitudinally extending are arranged on two transverse sides of the truss arm, a bracket is arranged on the two first linear guide rails, and the bracket is in transmission connection with the first driving motor fixedly arranged at the bottom end of the truss arm through a synchronous belt transmission pair; the first driving motor drives the bracket to move along the first linear guide rail, the bracket is matched to longitudinally penetrate through a grid plate arranged on the rack, move to the paper collecting assembly and be butted with the paper feeding assembly, and the first driving motor drives the bracket to move along the first linear guide rail to be matched with and bear each pile of A4 paper;the paper receiving device comprises a second driving motor fixedly arranged on a support seat fixedly connected with the rack, the second driving motor is connected with a first truss plate through a first crank matched with a first connecting rod, two longitudinally extending support plates are arranged at the two transverse ends of the first truss plate, the support plates are connected with the rack through lead screws and can slide along the lead screws, a support plate is fixedly arranged on the two support plates, the support plate is connected with a plurality of transversely extending and longitudinally spaced load arms through support columns, a plurality of backing plates are arranged on each load arm at intervals along the transverse direction, the backing plates at the same position of the transverse direction of the load arms are matched to form a tray for supporting A4 paper, and the number of the trays is matched with the number of long-strip paper cut by the cutting assembly; the paper collecting assembly further comprises a paper aligning device, the paper aligning device comprises a truss rod movably connected with the rack through a bearing, a plurality of paper aligning baffles are fixedly arranged on the truss rod, the truss rod is further connected with the rack through an air spring, the truss rod can drive the plurality of paper aligning baffles to turn over and abut against one side surface of A4 paper conveyed to the paper collecting device by the paper feeding assembly in a matching mode, and each pile of A4 paper is arranged in a flush mode; the second driving motor drives the supporting plate and the carrier plate to slide along the screw rod and enables the carrier arm to drive the tray to move vertically, the matched paper receiving device descends gradually and sequentially receives each pile of A4 paper, the matched paper aligning device aligns and aligns each screw A4 paper and the transverse conveyor belt which is embedded between the plurality of carrier arms and fixed relative to the rack transversely conveys each ream of A4 paper, and the paper collecting assembly is enabled to finish transversely conveying the A4 paper to the ream packaging machine.
- 3. The A4 paper double-rotary-knife paper cutting, ream production and carton packaging integrated production line as claimed in claim 2,the paper supply assembly is provided with five paper supply devices, and each paper supply device comprises a supporting wall plate, a reciprocating rotary shaft, a force arm with a large end connected with the reciprocating rotary shaft, a push-pull rod movably connected with a small end of the force arm through a shaft pin and a telescopic cylinder in transmission connection with the push-pull rod; the reciprocating rotary shaft and the telescopic cylinder are arranged on the supporting wall plate; the reciprocating rotary shaft comprises a rotary shaft body and a paper roll clamping arm arranged on the rotary shaft body, the rotary shaft body is provided with two linear slide rails, one end of the paper roll clamping arm is connected with the two linear slide rails, the other end of the paper roll clamping arm is connected with a chuck for clamping roll paper, the end, connected with the linear slide rails, of the paper roll clamping arm is also in transmission connection with a first driving cylinder through a locking ring for locking the paper roll clamping arm on the rotary shaft body in a sleeved mode, and the first driving cylinder can drive the paper roll clamping arm to transversely slide along the matched linear slide rails so as to match and adjust the transverse distance between the two chucks which are transversely symmetrically; the guide subassembly includes a plurality of first guide rollers and screw thread conduction roller, all be equipped with at least one on the position of matching each paper supply device on the crane span structure first guide roller and screw thread conduction roller, the cylinder paper of arranging in on the paper supply device twines on the first guide roller and the screw thread conduction roller of matching and along the paper supply direction draft, crane span structure and subassembly butt joint position department of cutting still are equipped with and are used for carrying out range upon range of device with many cylinder paper along the draft of paper supply direction, range upon range of device is passed through including establishing a plurality of paper of leading of crane span structure upper end and vertical interval setting, and each paper leads to lead to the side and just the lower extreme and all be equipped with a conduction roller and receipts material roller respectively, and many cylinder paper along the draft of paper supply direction are twined in proper order and are passed through and are stretched out and accomplish cylinder paper range upon range of after the conduction roller, the paper leads to.
- 4. The A4 paper double-rotary-knife paper cutting, ream production and carton packaging integrated production line as claimed in claim 3,the slitting component comprises a first slitting knife group and a second slitting knife group arranged at the upper end and/or the lower end of the first slitting knife group; the first slitting knife group comprises a knife shaft, the knife shaft is mounted on the rack through a bearing seat, and a plurality of first slitting knives are separately mounted on the knife shaft through a blocking sleeve; the second slitting knife group comprises a knife holder which extends transversely and is fixedly connected with the rack, a dovetail chute is arranged on the longitudinal side edge of the knife holder, a plurality of mounting blocks matched with the dovetail chute are hung on the knife holder, an air cylinder is fixedly arranged on each mounting block and is in transmission connection with an electric cutter, the electric cutter is matched and right opposite to the first slitting knife in the arrangement position, and the electric cutter can cut a plurality of pieces of laminated roll paper into a plurality of pieces of strip paper by matching with the first slitting knife;the transverse cutting assembly comprises an upper knife roll and a lower knife roll which are transversely arranged and connected with the rack through bearings, one transverse end of the upper knife roll and one transverse end of the lower knife roll are fixedly provided with transmission gears which are meshed with each other, the other transverse end of the upper knife roll and the other transverse end of the lower knife roll are provided with transmission wheels, one of the two transmission wheels is in transmission connection with a guide roll of the traction assembly and a third driving motor through a transmission belt, and the third driving motor drives the upper knife roll and the lower knife roll to reversely rotate through the transmission of the transmission belt and the transmission gears; the cutter mounting grooves are symmetrically arranged in the two axial directions on the side walls of the circular peripheries of the upper cutter roll and the lower cutter roll, a transverse cutter arranged along the radial direction of the upper cutter roll or the lower cutter roll is locked in each cutter mounting groove through a wedge block and a screw, and the transverse cutter is also arranged in a cutter mounting groove matched with the extending edge of the transverse cutter; the third driving motor drives the upper knife roll, the lower knife roll and the transverse cutters arranged on the upper knife roll and the lower knife roll to reversely rotate and be meshed at intervals through the transmission belt and the transmission gear, and a plurality of long-strip papers are transversely cut into a plurality of piles of A4 papers in a matching manner;the high-speed paper feeding device comprises a high-speed paper feeding device, a front-position lower paper feeding device, a high-speed lower paper feeding device and a rear-position lower paper feeding device, wherein the high-speed paper feeding device, the front-position lower paper feeding device and the rear-position lower paper feeding device respectively comprise a paper feeding roller and a tensioning roller which are arranged on a frame through bearings and transversely, the paper feeding roller and the tensioning roller are connected; the high-speed paper feeding device comprises a high-speed upper paper feeding device, a front lower paper feeding device and a high-speed lower paper feeding device, wherein paper feeding rollers of the high-speed upper paper feeding device, the front lower paper feeding device and the high-speed lower paper feeding device are in transmission connection through a first transmission belt, the paper feeding rollers of the front lower paper feeding device are in transmission connection with a third driving motor through a first synchronous transmission wheel, a second transmission belt and a synchronous belt transmission pair, and the diameter sizes of the paper feeding rollers of the high-speed upper paper feeding device and the high-speed lower paper feeding device are the same and are larger; the paper feeding rollers of the upper paper feeding device and the rear lower paper feeding device are also in transmission connection with a second synchronous transmission wheel arranged at the transverse side end of the frame through a fourth transmission belt, the second synchronous transmission wheel is also in transmission connection with a transmission wheel arranged on the upper knife roller through a third transmission belt, the matching enables the paper feeding rollers of the upper paper feeding device and the rear lower paper feeding device to rotate through the transmission of a third driving motor, and the diameter sizes of the paper feeding rollers of the upper paper feeding device and the rear lower paper feeding device are the same.
- 5. The a4 paper double-rotary-knife paper cutting, ream production and box packaging integrated production line of any one of claims 1 to 4, wherein the ream packer comprises:the ream conveying belt is used for receiving reams from the double-rotary-cutter paper cutting mechanism and conveying the reams to the ream conveying mechanism;the ream conveying mechanism is used for receiving reams from the butt joint position of the ream conveying belt and conveying the reams to the ejection assembly;the packaging paper feeding mechanism is used for cutting the conjoined packaging paper into single packaging paper and/or conveying the single packaging paper to a paper feeding station;the liftout assembly is used for vertically jacking the wrapping paper and the A4 ream of paper to a first packaging station after vertically jacking each A4 ream of paper to the lower end of the wrapping paper positioned on the upper paper station one by one and matching with the transverse packaging assembly to finish transverse edge packaging of the ream of paper;the transverse packaging assembly comprises two paper pushing devices, a side paper clamping device, a paper pressing device and a glue spraying device which are transversely and symmetrically arranged, wherein the glue spraying device is used for spraying glue on one transverse side edge of packaging paper, the paper pressing device is used for pressing and buckling the packaging paper at the top end of an A4 ream, the side paper clamping device is used for clamping and fixing an A4 ream of paper in cooperation with the ejecting assembly, the two paper pushing devices can transversely move oppositely to bend and glue the two transverse side edges of the packaging paper and half-wrap the A4 ream of paper in a matching manner, and the two transverse paper pushing devices are also used for supporting the A4 ream of paper in cooperation with the side paper clamping device to enable the ejecting assembly to retract;the longitudinal angle folding assembly comprises a movable angle folding device and a fixed angle folding device which are transversely and symmetrically arranged, the movable angle folding device can transversely move to fold two vertex angles of one transverse side edge of a piece of packaging paper matched with A4 ream, the fixed edge folding device is matched with the ream material stirring assembly to transversely stir the A4 ream of paper, and the fixed edge folding device is matched to fold two vertex angles of the other transverse side edge of the packaging paper matched with A4 ream of paper;the longitudinal edge sealing assembly comprises two lower side edge folding heads which are longitudinally arranged at intervals, two glue spraying heads which are longitudinally symmetrically arranged and two upper side edge sealing heads which are longitudinally arranged at intervals, wherein the two lower side edge folding heads are used for turning up two lower sides of two longitudinal sides of the packaging paper when the A4 reams of paper are transversely stirred by the ream stirring assembly in a matching way, the two glue spraying heads are used for spraying glue on the two turned lower sides, and the two upper side edge sealing heads are used for turning down two upper sides of two longitudinal sides of the packaging paper and pasting the matched lower sides with the glue when the A4 reams of paper are transversely stirred by the ream stirring assembly to complete ream packaging;a ream kick-out assembly for intermittently kicking the A4 ream in the cross direction and delivering the A4 ream to a ream blanking conveyor.
- 6. The a4 paper double-rotary-knife paper cutting, ream production and carton packaging integrated production line as claimed in claim 5, wherein the wrapping paper feeding mechanism is provided with a traction paper feeding device, a static eliminating device, a cutting device and a conveying device on the carton body along the longitudinal direction; wherein,the traction paper supply device comprises a discharging shaft, a drafting shaft, a pressing shaft and a tensioning shaft which are arranged on the box body through bearings, cylindrical conjoined packing paper is placed on the discharging shaft and is wound on the drafting shaft and the tensioning shaft, the drafting shaft is in transmission connection with a fourth driving motor arranged on the box body through a synchronous belt or a transmission chain, the fourth driving motor is used for driving the drafting shaft to rotate and sending the roller packing paper to the conveying device after being drafted through the cutting device, and the pressing shaft is arranged at the vertical upper end of the drafting shaft and can vertically move relative to the drafting shaft to adjust the vertical distance between the pressing shaft and the drafting shaft so as to match and clamp or loosen the packing paper;the static electricity removing device comprises an air blowing nozzle fixedly arranged on the box body, and the air blowing nozzle is connected with an ion fan fixedly arranged in the box body through a pipeline and is used for blowing static electricity of the conjoined packing paper pulled by the traction paper supply device;the cutting device comprises an upper cutter holder fixedly arranged on the box body, a driving cylinder in transmission connection with an upper cutting knife is arranged on the upper cutter holder, a lower cutting knife fixedly arranged on the box body through a lower cutter holder is arranged at the matching position of the lower end of the upper cutting knife, and the upper cutting knife and the lower cutting knife are arranged in a staggered mode in the conveying direction; the driving cylinder can drive the upper cutting knife to move towards or away from the lower cutting knife, and the upper cutting knife is matched with the lower cutting knife to cut the conjoined packing paper into single packing paper with matched size;the conveying device comprises two synchronous belt conveying belts which are arranged at intervals along the transverse direction, the two synchronous belt conveying belts are in transmission connection with a fifth driving motor fixedly arranged on the box body through a rotating shaft matched with a first synchronous belt, the fifth driving motor drives the two synchronous belt conveying belts to move and is matched with a material guide plate arranged at the lower end of the fifth driving motor, and the single packing paper is conveyed to a paper feeding station through synchronous transmission;the ream paper conveying mechanism comprises a first conveying belt which is arranged on the cabinet body through a screw rod, the first conveying belt is transversely arranged, and the first conveying belt is in transmission connection with a sixth driving motor fixedly arranged on the cabinet body through a plurality of synchronous belt transmission pairs; the two circulating material guiding devices are symmetrically arranged on two longitudinal sides of the first conveying belt, the two circulating material guiding devices are in synchronous transmission connection through gears matched with a first rotating shaft, the first rotating shaft is in transmission connection with a seventh driving motor fixedly arranged on the cabinet body through a synchronous belt transmission pair, each circulating material guiding device comprises a rotating main shaft, a supporting shaft, a rotating chain wheel and a transmission chain wheel, the rotating main shaft and the supporting shaft are vertically arranged and are connected with the cabinet body through bearing seats, the rotating main shaft is in meshing transmission connection with the first rotating shaft through the gears, the rotating chain wheel and the transmission chain wheel are respectively arranged on the rotating main shaft and the supporting shaft and are in transmission connection through chains, and a plurality of material correcting plates for correcting A4 paper are further arranged on the chains; the sixth driving motor drives the first conveying belt to transversely convey A4 reams of paper, and a seventh driving motor transmission chain of the two-circulation material guide device is matched to drive the material correcting plate to circularly move, so that reams of paper are accurately conveyed to the material ejecting assembly in a matching manner;the ejection assembly comprises a supporting seat fixedly arranged on the cabinet body, an ejection frame is movably arranged on the supporting seat, a first carrier plate is arranged at the upper end of the ejection frame, the bottom end of the ejection frame is in transmission connection with an eighth driving motor fixedly arranged on the cabinet body through a hinged seat, a crank connecting rod and a swing rod, and the eighth driving motor can drive the ejection frame to drive the first carrier plate and A4 reams of paper placed on the first carrier plate to vertically move; an ejector rod is movably arranged on the supporting seat, the upper end of the ejector rod is connected with a supporting block movably embedded on the first support plate, the bottom end of the ejector rod is in transmission connection with a ninth driving motor fixedly arranged on the cabinet body through a first hinge seat, a first crank connecting rod and a first swing rod, the ninth driving motor drives the ejector rod to drive the supporting block to vertically move, and when the first support plate is vertically retracted by matching with a jacking support A4 ream, the two paper pushing devices can support an A4 ream of paper.
- 7. The A4 paper double-rotary-knife paper cutting, ream production and carton packaging integrated production line as claimed in claim 6,the two paper pushing devices respectively comprise a linear guide rail which is fixedly arranged on the cabinet body and extends transversely, a push plate is fixedly arranged on the linear guide rail, one end of the push plate is provided with an inclined wedge surface or an arc-shaped wedge surface, the other end of the push plate is in transmission connection with a tenth driving motor fixedly arranged on the cabinet body through a second hinge seat, a second crank connecting rod and a second swing rod, the tenth driving motor drives the push plate to slide along the linear guide rail, and the push plates of the two paper pushing devices move oppositely in a matching manner to bend and glue the two transverse sides of the packaging paper and half-wrap A4 reams of paper;the lateral paper clamping device comprises a fixed clamping plate and a movable clamping plate, wherein the fixed clamping plate is fixedly arranged on the cabinet body, the movable clamping plate can move transversely, the movable clamping plate is connected with a first linear guide rail which is obliquely arranged, the first linear guide rail is arranged on a support which is fixedly connected with the cabinet body, the top end of the support is provided with an eleventh driving motor, the eleventh driving motor is connected with the first linear guide rail through a third oscillating bar, a third crank connecting rod and a third hinge seat and can drive a sliding rail of the first linear guide rail to slide relative to the support, and the movable clamping plate is matched with the fixed clamping plate to move transversely and is matched with the fixed clamping plate to clamp and fix A4 reams of;the paper pressing device comprises a first support fixedly arranged on the cabinet body, a second linear guide rail is vertically arranged on the first support, one end of a sliding rail of the second linear guide rail is connected with the pressing plate, the other end of the sliding rail of the second linear guide rail is in transmission connection with a twelfth driving motor fixedly arranged on the cabinet body through a fourth hinge seat, a fourth crank connecting rod and a fourth swing rod, the twelfth driving motor can drive the sliding rail of the second linear guide rail to drive the pressing plate to extend into a space between the fixed clamping plate and the movable clamping plate, and the transverse packaging assembly is matched with the top end of A4 reams of paper to finish transverse side packaging of A4 reams of paper;the movable angle folding device and the fixed angle folding device both comprise two angle folding blocks fixedly installed through an installation plate, the two angle folding blocks are arranged at intervals in the vertical direction, the installation plate of the movable angle folding device is further arranged on a third linear guide rail extending along the transverse direction, the installation plate is further in transmission connection with a second rotating shaft through a fifth crank connecting rod and a fifth swing rod, and the second rotating shaft is in transmission connection with a thirteenth driving motor fixedly arranged on the cabinet body through a synchronous belt transmission pair; the thirteenth driving motor drives the mounting plate to drive the two matched angle folding blocks to prop against two vertex angles of one transverse side edge of the packaging paper or enable two vertex angles of the other transverse side edge of the packaging paper to prop against two angle folding blocks of the fixed angle folding device when the A4 ream of paper is shifted transversely by the ream shifting assembly, and the angle folding of the longitudinal side edge of the packaging paper is completed in a matched manner;the ream paper material shifting assembly comprises two circulating material shifting devices which are longitudinally and symmetrically arranged, the two circulating material shifting devices are connected through a third rotating shaft, the third rotating shaft is also in transmission connection with a fourteenth driving motor arranged in the cabinet body through two synchronous belt transmission pairs and a fourth rotating shaft, and the fourth rotating shaft is also in transmission connection with a side edge conveying belt of a ream paper blanking conveying belt through a gear and a first transmission shaft; each circulating material shifting device comprises a first rotating chain wheel arranged on the third rotating shaft and a first transmission chain wheel arranged on the cabinet body through a bearing, the first rotating chain wheel and the first transmission chain wheel are in transmission connection through a first chain, and the first chain is further provided with eight shifting claws for shifting A4 reams; the fourteenth driving motor drives the first chain to drive the eight material shifting claws to circularly move, and the A4 reams of paper is shifted in a matched mode to transversely move.
- 8. The A4 paper double-rotary-cutter paper cutting, ream production and carton packaging integrated production line as recited in claim 5, wherein the carton mechanism comprises a carton device, a ream feeding assembly arranged at one longitudinal end of the carton device, a blanking mechanism arranged at the other longitudinal end of the carton device and butted with the other longitudinal end of the carton device, a carton feeding assembly arranged at one transverse side of the carton device and a carton cover feeding assembly; the luggage device comprises a frame body, an ejector rod mechanism and a luggage cover packaging mechanism, wherein the frame body is provided with an upper layer feeding frame and a lower layer material receiving frame, the upper layer feeding frame is provided with a feeding hole, the ejector rod mechanism comprises a plurality of ejector rods and a top plate connected with the ejector rods, the top plate is arranged corresponding to the feeding hole, a rear side pressing assembly and a front side baffle are respectively arranged on the lower layer material receiving frame corresponding to two sides of the feeding hole, and the unloading mechanism is provided with two leading-in parts; during packaging, packing box feeding assembly, case lid feeding assembly provide packing box and case lid respectively, on the packing box device will be sent to the ream to ream feeding assembly, ejector pin mechanism first moves ejector pin and roof vertical downstream one section distance, sinks the packing box into the roof after the feed inlet is in order to contact the lapse through the gravity of ream, and ejector pin mechanism drive ejector pin and roof progressively move down, lie in after the packing box fills with the ream of predetermineeing quantity on the lower floor receives the work or material rest, the front and back part of packing box is moved down the in-process and is buckled, thereby back side pressure subassembly, front side baffle and leading-in portion are buckled the week side part of packing box in proper order and are handled the packing of accomplishing the packing box, case lid packagine machine constructs packs the case lid again.
- 9. The a4 paper double-rotary-cutter paper cutting, ream production and carton packaging integrated production line as recited in claim 8, wherein the carton comprises a carrier, a first bending part connected to the front and rear edges of the carrier, a second bending part connected to the left and right edges of the carrier, a third bending part connected to the two side edges of the rear first bending part, and a fourth bending part connected to the two side edges of the front first bending part, the rear lateral pressure assembly comprises a lateral pressure cylinder pivoted to the outside of the frame and a lateral pressure block pivoted to the lateral pressure cylinder, the lateral pressure cylinder drives the lateral pressure block to rotate reciprocally by 90 ° along one end of the lateral pressure block to fold and press the third bending part; a pressing assembly is further arranged between the rear side pressing assembly and the front side baffle and comprises a fifteenth driving motor and a pressing block pivoted to the fifteenth driving motor, and the fifteenth driving motor drives the pressing block to rotate back and forth by 90 degrees to press the second bending part at intervals; the place ahead of preceding side shield is located to the guiding-in portion, the top of guiding-in portion is the arcuation setting from bottom to top from the one end that is close to preceding side shield toward the one end of keeping away from preceding side shield, the top of guiding-in portion still is set up to be by the inboard edge outside edge leaned on to the side by being close to the order paper.
- 10. The a4 paper double-rotary-cutter paper cutting, ream paper production and carton packaging integrated production line as claimed in claim 8, wherein the carton cover packaging mechanism comprises a fixed plate arranged on the frame body, a driving device arranged on the fixed plate, a first mounting plate connected with the driving device, four vertical press blocks respectively arranged on four edges of the first mounting plate, a pressing cylinder arranged on the vertical press blocks and a horizontal press block arranged on the pressing cylinder, the driving device drives the mounting plate to move up and down, and the pressing cylinder pushes the horizontal press block to move inwards; the ream feeding assembly comprises a first feeding assembly, a transport frame in butt joint with the first feeding assembly, a first pushing assembly arranged on the transport frame and far away from the butt joint end with the first feeding assembly, and a second pushing assembly which is arranged perpendicular to the first pushing assembly and in butt joint with the luggage device; the first feeding assembly comprises a first belt and a motor for driving the first belt to feed; the conveying frame comprises a conveying rail, a second belt arranged on the conveying rail and a first motor driving the second belt to transmit; the first material pushing assembly comprises a third belt and a second motor for driving the third belt to feed; the second material pushing assembly comprises two first circulating material shifting devices which are transversely and symmetrically arranged, the two first circulating material shifting devices are connected through two fifth rotating shafts, one of the two fifth rotating shafts is further connected with a sixteenth driving motor arranged on the frame body through a synchronous belt transmission pair, each first circulating material shifting device comprises a second transmission chain wheel arranged on the two fifth rotating shafts, the two second transmission chain wheels of each first circulating material shifting device are in transmission connection through a second chain, and a first shifting eight claw used for shifting A4 reams to move is further arranged on each second chain; the sixteenth driving motor drives the second chain to drive the first material shifting eight claws to circularly move, and the A4 reams of paper are shifted in a matched mode to longitudinally move and push the paper to the luggage device; the packing box feeding assembly and the box cover feeding assembly comprise mounting brackets, stop pieces arranged on two sides of the mounting brackets, a third motor, a connecting rod connected with the third motor, two movable rods arranged on the connecting rod, a suction nozzle arranged on the movable rods, a second driving device and conveyor belts arranged on two sides of the mounting brackets, wherein the third motor drives the connecting rod to rotate, so that one end of each movable rod is lifted or lowered, and the second driving device drives the conveyor belts to rotate; the unloading mechanism comprises a plurality of rollers arranged side by side, and the rollers are driven by a third driving device to rotate so as to continuously unload the luggage.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921073823.1U CN210336188U (en) | 2019-07-10 | 2019-07-10 | A4 paper double-rotary-cutter paper cutting, ream paper production and box packaging integrated production line |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921073823.1U CN210336188U (en) | 2019-07-10 | 2019-07-10 | A4 paper double-rotary-cutter paper cutting, ream paper production and box packaging integrated production line |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210336188U true CN210336188U (en) | 2020-04-17 |
Family
ID=70196920
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921073823.1U Active CN210336188U (en) | 2019-07-10 | 2019-07-10 | A4 paper double-rotary-cutter paper cutting, ream paper production and box packaging integrated production line |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210336188U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110303545A (en) * | 2019-07-10 | 2019-10-08 | 东莞市骏兴机械科技有限公司 | A4 paper double back rotary knife cut paper enables paper production and case packing one production line |
| CN114394279A (en) * | 2022-01-20 | 2022-04-26 | 瑞安市东腾机械有限公司 | Large ream paper packaging machine |
-
2019
- 2019-07-10 CN CN201921073823.1U patent/CN210336188U/en active Active
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN110303545A (en) * | 2019-07-10 | 2019-10-08 | 东莞市骏兴机械科技有限公司 | A4 paper double back rotary knife cut paper enables paper production and case packing one production line |
| CN110303545B (en) * | 2019-07-10 | 2024-02-20 | 东莞市骏兴机械科技有限公司 | A4 paper double-rotary cutter paper cutting, ream paper production and case packaging integrated production line |
| CN114394279A (en) * | 2022-01-20 | 2022-04-26 | 瑞安市东腾机械有限公司 | Large ream paper packaging machine |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN110303545A (en) | A4 paper double back rotary knife cut paper enables paper production and case packing one production line | |
| CN110271894A (en) | A4 paper double back rotary knife cut paper enables paper production line | |
| JP6976702B2 (en) | A device for holding flat elements in sheet form that pass through a processing machine | |
| US6129503A (en) | Combination counter-ejector shingle-output delivery system | |
| KR102773815B1 (en) | Transfer module for converting machine | |
| IT202200026202A1 (en) | PACKAGING MACHINE FOR PACKAGING GROUPS OF PRODUCTS IN PACKAGING BOXES MADE FROM FLATTENED TUBULAR CARDBOARD OR CARDBOARD BLANKS AND INTENDED TO BE INSERTED IN A PACKAGING BOX | |
| CN112758393B (en) | A fully automatic paper stacking equipment | |
| US10618241B2 (en) | Device for storing and removing cardboard for a bridge in a corrugated cardboard production line | |
| CN210339762U (en) | A4 paper double-rotary-cutter ream paper production line | |
| CN212314091U (en) | Automatic processing production line for paper rolls | |
| CN114955080A (en) | Automatic paper stack detection production equipment group | |
| CN217805739U (en) | Ceramic tile packaging production line | |
| CN221874453U (en) | Automatic paper stacking equipment | |
| CN110815931B (en) | Single-page carton stapler | |
| CN211002218U (en) | Instruction placing mechanism of box packing machine | |
| CN210011409U (en) | A nail box machine | |
| CN216267851U (en) | Binding means is used to mistake proofing position carton packing | |
| CN210336187U (en) | A double rotary knife cutter for A4 paper | |
| CN212862058U (en) | Automatic packaging device for cigarette box paperboard finished products | |
| US20020047236A1 (en) | Device for forming a stack of successively arranged printed sheets | |
| CN117550143B (en) | Ceramic tile high-speed packaging machine | |
| US3783753A (en) | Apparatus for feeding flattened, tubular container blanks | |
| CN224045602U (en) | High-efficient automatic paper folding packagine machine | |
| CN216443856U (en) | Split type viscose hem compounding machine | |
| CN111392121A (en) | An automatic packaging device for cigarette case cardboard products |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |