CN210173046U - Positioning tool for machining spline shaft double key grooves - Google Patents
Positioning tool for machining spline shaft double key grooves Download PDFInfo
- Publication number
- CN210173046U CN210173046U CN201921017738.3U CN201921017738U CN210173046U CN 210173046 U CN210173046 U CN 210173046U CN 201921017738 U CN201921017738 U CN 201921017738U CN 210173046 U CN210173046 U CN 210173046U
- Authority
- CN
- China
- Prior art keywords
- inclined plane
- holding ring
- location
- spline shaft
- fixed block
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
- 238000003754 machining Methods 0.000 title claims abstract description 7
- 230000007704 transition Effects 0.000 claims abstract description 4
- 238000000034 method Methods 0.000 description 5
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000003801 milling Methods 0.000 description 1
- 238000003672 processing method Methods 0.000 description 1
Images


Landscapes
- Jigs For Machine Tools (AREA)
Abstract
The utility model discloses a location frock for processing integral key shaft double key groove, its characterized in that includes workstation and holding ring, detachably installs the fixed block that has V type groove on the workstation, detachably is connected with the clamp plate on the fixed block, the interior rampart of holding ring sets up to the internal spline, the outer rampart of holding ring is surrounded in proper order by semi-circular arc face, first location inclined plane, transition cambered surface and second location inclined plane and is linked up and form, first location inclined plane with the mutual symmetry setting in second location inclined plane, radially be provided with the screw hole on the holding ring. The utility model is used for the double key groove of processing integral key shaft, its machining precision is high, the clamping is rectified and the convenient high efficiency of processing.
Description
Technical Field
The utility model relates to a location appurtenance's technical field for processing integral key shaft double key groove, concretely relates to location frock for processing integral key shaft double key groove.
Background
At present, in the field of spline shaft processing, when a double-key-groove part is subjected to key groove milling processing, a fan-shaped part to be processed needs to be fixed on a machine tool, and clamps on the machine tool are all universal clamps, so that a workpiece can only be fixed, but the position of the workpiece cannot be guaranteed, the angle position relation between a spline and the double-key-groove part needs to be guaranteed during the processing of the double-key-groove spline shaft, and the spline is clamped again after being milled during actual processing, and the processing precision is greatly reduced due to repeated clamping and positioning.
Therefore, in the traditional method, the angle positions of the spline and the key groove are corrected by methods such as manual marking and the like, and the angle of the workpiece is adjusted, so that the key groove can be ensured to be in the correct position.
However, the error of manual adjustment is large, and operations such as scribing are required, so that the complexity is high; in addition, the machining error caused by re-clamping cannot be completely eliminated; therefore, the traditional processing method has unsatisfactory efficiency, processing precision and processing simplicity.
SUMMERY OF THE UTILITY MODEL
In view of the not enough of background art, the utility model provides a location frock for processing integral key shaft double key groove has solved how accurate, high-efficient and conveniently process the technical problem of integral key shaft double key groove.
For solving the technical problem, the utility model provides a following technical scheme:
a location frock for processing integral key shaft double key groove, including workstation and holding ring, detachably installs the fixed block that has V type groove on the workstation, detachably is connected with the clamp plate on the fixed block, the inner ring wall of holding ring sets up to the internal spline, the outer ring wall of holding ring is surrounded in proper order by semi-circular arc surface, first location inclined plane, transition cambered surface and second location inclined plane and links up and form, first location inclined plane with the mutual symmetry setting of second location inclined plane, radially be provided with the screw hole on the holding ring.
The workbench is in threaded connection with the fixed block.
The fixed block is in threaded connection with the pressing plate.
Compared with the prior art, the utility model beneficial effect who has is: the spline of the spline shaft and the angle positions of the double key grooves can be accurately positioned through the matching of the first positioning inclined surface and the second positioning inclined surface of the positioning ring, and the double key grooves of the spline shaft can be efficiently and conveniently processed; the spline shaft can be fixed on the workbench through the fixing block and the pressing plate, and the spline groove can be conveniently and stably processed.
Drawings
The utility model discloses there is following figure:
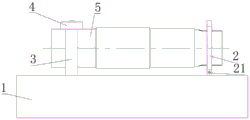
FIG. 1 is a schematic view of the present invention;
fig. 2 is a schematic view of the pressing plate and the fixing block of the present invention clamping the spline shaft therein;
fig. 3 is a schematic view of the positioning ring of the present invention.
Detailed Description
As shown in the figure, a location frock for processing integral key shaft double key groove, including workstation 1 and holding ring 2, holding ring 2 is used for the suit to wait to process the integral key shaft 5 of double key axle, detachably installs fixed block 3 that has V type groove 31 on the workstation 1, and 3 mainly used auxiliary clamping integral key shaft 5 of fixed block prevent that integral key shaft 5 from taking place to remove in the course of working, in this embodiment, workstation 1 with 3 mutual threaded connection of fixed block. The fixed block 3 is detachably connected with a pressing plate 4, in the embodiment, the fixed block 3 is in threaded connection with the pressing plate 4, and the pressing plate 4 and the fixed block 3 are matched with each other to clamp the spline shaft 5. The inner ring wall of the positioning ring 2 is provided with an inner spline 21, and the inner spline 21 is matched with an outer spline of the spline shaft 5; the outer annular wall of the positioning ring 2 is formed by sequentially surrounding and connecting a semi-circular arc surface 22, a first positioning inclined surface 23, a transition arc surface 24 and a second positioning inclined surface 25, wherein the first positioning inclined surface 23 and the second positioning inclined surface 25 are symmetrically arranged, and a threaded hole 26 is radially formed in the positioning ring 2. The first positioning inclined surface 23 and the second positioning inclined surface 25 are used for being attached to the table top of the workbench to position the angle of the positioning ring 2, so that the technical effect of controlling the angle of the spline shaft 5 sleeved by the positioning ring 2 is further achieved, and the angle positions of the spline shaft 5 and the double key grooves are accurately positioned.
During operation, the external spline of the spline shaft 5 is inserted into the internal spline of the positioning ring 2, then a screw is screwed into the threaded hole of the positioning ring 2, the spline shaft 5 is tightly pressed by the screw, the tail end of the spline shaft 5 extends into the V-shaped groove 31 of the fixing block 3, then the positioning ring 2 and the spline shaft 5 therein are rotated to ensure that the first positioning inclined surface 23 of the positioning ring 2 is attached to the table-board of the workbench 1, then the pressing plate 4 is in threaded connection with the fixing block 3 to tightly press the spline shaft 5 in the state between the pressing plate 4 and the fixing block 3, then the fixing block 3 is in threaded connection with the workbench 1, at the moment, the first key groove of the spline shaft 5 can be processed, after the processing is finished, the fixing block 3 and the pressing plate 4 on the fixing block 3 are loosened, the positioning ring 2 is rotated with the spline shaft 5, so that the second positioning, then, the pressing plate 4 and the fixing block 3 are fixed, the fixing block 3 is in threaded connection with the workbench 1, the second key groove of the spline shaft 5 is machined, after machining is finished, the pressing plate 4 on the fixing block 3 is loosened, the positioning ring 2 is detached from the spline shaft 5, and the machined spline shaft can be taken out.
In conclusion, the spline of the spline shaft 5 and the angle positions of the double key grooves can be accurately positioned through the matching of the first positioning inclined surface 23 and the second positioning inclined surface 25 of the positioning ring 2, and the spline shaft double key grooves can be efficiently and conveniently processed; can fix integral key shaft 5 on workstation 1 through fixed block 3 and clamp plate 4, be convenient for stably process the spline groove.
Claims (3)
1. A location frock for processing integral key shaft double key groove, its characterized in that includes workstation and holding ring, detachably installs the fixed block that has V type groove on the workstation, detachably is connected with the clamp plate on the fixed block, the inner ring wall of holding ring sets up to the internal spline, the outer rampart of holding ring is surrounded in proper order by semi-circular arc face, first location inclined plane, transition cambered surface and second location inclined plane and links up and form, first location inclined plane with the mutual symmetry setting of second location inclined plane, radially be provided with the screw hole on the holding ring.
2. The positioning tool for machining the spline shaft double-key groove according to claim 1, wherein the workbench and the fixing block are in threaded connection with each other.
3. The positioning tool for machining the spline shaft double-key groove according to claim 1, wherein the fixing block and the pressing plate are in threaded connection with each other.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921017738.3U CN210173046U (en) | 2019-07-02 | 2019-07-02 | Positioning tool for machining spline shaft double key grooves |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201921017738.3U CN210173046U (en) | 2019-07-02 | 2019-07-02 | Positioning tool for machining spline shaft double key grooves |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210173046U true CN210173046U (en) | 2020-03-24 |
Family
ID=69839815
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201921017738.3U Active CN210173046U (en) | 2019-07-02 | 2019-07-02 | Positioning tool for machining spline shaft double key grooves |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210173046U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116078965A (en) * | 2022-11-29 | 2023-05-09 | 科升挤出机械科技(南京)有限公司 | Involute spline cold rolling structure |
-
2019
- 2019-07-02 CN CN201921017738.3U patent/CN210173046U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116078965A (en) * | 2022-11-29 | 2023-05-09 | 科升挤出机械科技(南京)有限公司 | Involute spline cold rolling structure |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN202985192U (en) | Fixture for turning gear carrier eccentric holes | |
| CN106541290A (en) | A kind of jig of the circumferential registration for thin-wall part processing | |
| CN206588380U (en) | A kind of fixture in processing precise metalwork trigger body tailstock hole | |
| CN210649696U (en) | Floating clamping device for machining outer circle of connecting rod by lathe | |
| CN205630094U (en) | Quick drilling anchor clamps | |
| CN204308646U (en) | The Automatic-clamping centering machine of specific number of teeth gear ring class part | |
| CN204843657U (en) | Car of last hole of plate part and interior annular adds clamping apparatus | |
| CN203918029U (en) | A kind of fix tool of three-jaw self-centering chuck three-jaw | |
| CN104400471B (en) | Pincers tooth box body dovetail groove milling fixture and processing method thereof | |
| CN211102754U (en) | Special-shaped 90-degree joint type portable multifunctional combined clamp | |
| JP2005111598A (en) | Jig plate | |
| CN201179565Y (en) | A three-jaw chuck | |
| CN104162795B (en) | The jig of a kind of circumferential registration and the processing method in the hole, location of location-plate thereof | |
| CN207205939U (en) | The lathe tool of skew T class part | |
| CN206464858U (en) | A kind of jig for the circumferential registration processed for thin-wall part | |
| CN215468583U (en) | Quick self-centering clamping device of gear shaping machine | |
| CN206588621U (en) | A kind of processing precise metalwork end plane special fixture | |
| CN211072627U (en) | Sector gear finish turning tool | |
| CN213257440U (en) | Polygonal inner hole broaching equipment | |
| CN107052831A (en) | Clamping centering fixture for processing the thin wall cylinder axial groove beyond milling machine platform | |
| CN211840281U (en) | Rotary type porous drilling machine fixture for thin-wall sleeve part | |
| CN212145529U (en) | Clutch housing milling flutes auxiliary device | |
| CN203853559U (en) | Piece type plug gage turning tooling fixture | |
| CN202240641U (en) | Chuck positioning device | |
| CN207668537U (en) | A kind of chuck connector and connecting chuck |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| GR01 | Patent grant |