CN210024884U - A super-finishing positioning mandrel device for the inner ring of a railway bearing - Google Patents
A super-finishing positioning mandrel device for the inner ring of a railway bearing Download PDFInfo
- Publication number
- CN210024884U CN210024884U CN201920427036.6U CN201920427036U CN210024884U CN 210024884 U CN210024884 U CN 210024884U CN 201920427036 U CN201920427036 U CN 201920427036U CN 210024884 U CN210024884 U CN 210024884U
- Authority
- CN
- China
- Prior art keywords
- bearing
- mandrel
- workpiece
- positioning sleeve
- inner ring
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Active
Links
Images


Landscapes
- Rolling Contact Bearings (AREA)
- Grinding And Polishing Of Tertiary Curved Surfaces And Surfaces With Complex Shapes (AREA)
Abstract
本实用新型介绍了一种铁路轴承内圈超精加工定位芯轴装置,包括:芯轴、定位套、轴承、弹性挡圈、螺母和垫片;所述的芯轴为阶梯圆柱芯轴,小端设置两排高精度的角接触球轴承;所述的定位套为带台阶的环形套,内孔为两段阶梯孔,中部内孔安装在轴承外径上,装轴承一端端口设置挡圈槽;所述的弹性挡圈安装在定位套的挡圈槽内;所述的垫片通过螺母压紧在轴承的内圈端面上,工件安装到定位套上。将本装置装到超精磨机床上,当工件旋转时,定位套和工件一起同步转动,而工件和芯轴之间没有相对转动,不再对工件的内径产生划伤、磨损,该装置设计科学,结构简单,对工件的内径有良好保护作用,提高了工件的加工质量,进一步提升了工件的使用寿命。
The utility model introduces a positioning mandrel device for super-finishing machining of the inner ring of a railway bearing, which comprises: a mandrel, a positioning sleeve, a bearing, an elastic retaining ring, a nut and a washer; the mandrel is a stepped cylindrical mandrel, and the small Two rows of high-precision angular contact ball bearings are arranged at the ends; the positioning sleeve is an annular sleeve with steps, the inner hole is a two-stage stepped hole, the inner hole in the middle is installed on the outer diameter of the bearing, and the end port of the bearing is provided with a retaining ring groove The elastic retaining ring is installed in the retaining ring groove of the positioning sleeve; the gasket is pressed on the end face of the inner ring of the bearing through the nut, and the workpiece is installed on the positioning sleeve. The device is installed on the ultra-finishing machine tool. When the workpiece rotates, the positioning sleeve and the workpiece rotate synchronously, and there is no relative rotation between the workpiece and the mandrel, and the inner diameter of the workpiece will no longer be scratched and worn. The device is designed It is scientific and simple in structure, and has a good protective effect on the inner diameter of the workpiece, which improves the processing quality of the workpiece and further improves the service life of the workpiece.
Description
技术领域technical field
本实用新型属于铁路轴承的加工技术领域,具体涉及一种铁路车辆轴承内圈超精加工定位芯轴装置。The utility model belongs to the technical field of processing of railway bearings, in particular to a positioning mandrel device for super-finishing machining of an inner ring of a railway vehicle bearing.
背景技术Background technique
目前,在铁路轴承内圈超精加工的磨削工序中,内圈外径的超精加工都是以内径芯轴定位和支撑的,定位和支撑的芯轴都是固定不旋转的,靠芯轴喷出的高压油将工件浮起,工件在旋转的过程中由于压力油的变化使得工件和芯轴之间的间隙发生变化,间隙的变化使工件内径与芯轴接触并产生相对运动,造成轴承内圈的内径划伤、磨损,影响产品的加工质量。At present, in the grinding process of super-finishing of the inner ring of railway bearings, the super-finishing of the outer diameter of the inner ring is all positioned and supported by the inner diameter mandrel, and the positioning and supporting mandrel is fixed and does not rotate. The high-pressure oil sprayed from the shaft floats the workpiece. During the rotation of the workpiece, the gap between the workpiece and the mandrel changes due to the change of the pressure oil. The inner diameter of the inner ring of the bearing is scratched and worn, which affects the processing quality of the product.
实用新型内容Utility model content
本实用新型的目的是提出一种铁路轴承内圈超精加工定位芯轴装置,该装置利用一对高精度轴承安装在定位芯轴上,轴承上安装有一定位套,工件装在定位套上,使得原来的固定芯轴改为可旋转的定位套,使定位套和工件一起同步转动,工件和芯轴没有相对转动,不再对工件的内径产生划伤。The purpose of this utility model is to propose a positioning mandrel device for super-finishing machining of the inner ring of a railway bearing. The device utilizes a pair of high-precision bearings to be mounted on the positioning mandrel. The original fixed mandrel is changed to a rotatable positioning sleeve, so that the positioning sleeve and the workpiece rotate synchronously, the workpiece and the mandrel do not rotate relative to each other, and the inner diameter of the workpiece is no longer scratched.
本实用新型的目的可采用如下技术方案来实现:一种铁路轴承内圈超精加工定位芯轴装置,包括:芯轴、定位套、轴承、弹性挡圈、螺母和垫片,所述的芯轴为阶梯圆柱芯轴,阶梯小端设置两排轴承,端头设置一段螺纹;所述的定位套为带台阶的环形套,内孔为两段阶梯孔,中部内孔安装在轴承外径上,装轴承的一端端口设置挡圈槽;所述的弹性挡圈安装在定位套的挡圈槽内;所述的垫片套在芯轴带螺纹一端,通过螺母压紧在轴承内圈的端面上。The purpose of the utility model can be achieved by the following technical solutions: a super-finishing positioning mandrel device for the inner ring of a railway bearing, comprising: a mandrel, a positioning sleeve, a bearing, an elastic retaining ring, a nut and a gasket, the core The shaft is a stepped cylindrical mandrel, the small end of the step is provided with two rows of bearings, and the end is provided with a thread; the positioning sleeve is an annular sleeve with steps, the inner hole is a two-stage stepped hole, and the inner hole in the middle is installed on the outer diameter of the bearing. , a retaining ring groove is set at one end port of the bearing; the elastic retaining ring is installed in the retaining ring groove of the positioning sleeve; the gasket is sleeved on the threaded end of the mandrel, and is pressed against the end face of the bearing inner ring by a nut superior.
所述的芯轴,其阶梯小端的外径尺寸和轴承内圈的内径尺寸高精度配合。For the mandrel, the outer diameter of the small end of the step and the inner diameter of the inner ring of the bearing are matched with high precision.
所述的定位套台阶小端的孔径尺寸大于心轴阶梯大端的外径尺寸,定位套中部的阶梯孔长度及孔径尺寸和两个轴承的轴向尺寸及外径尺寸相匹配,并和轴承的外径高精度配合。The aperture size of the small stepped end of the positioning sleeve is larger than the outer diameter of the large stepped end of the mandrel, and the length and aperture size of the stepped hole in the middle of the positioning sleeve match the axial size and outer diameter of the two bearings, and match the outer diameter of the bearing. Diameter with high precision.
所述的定位套其大端外径尺寸和工件的内径尺寸高精度配合。The outer diameter of the large end of the positioning sleeve is matched with the inner diameter of the workpiece with high precision.
所述的垫片外径尺寸和轴承内圈的外径尺寸相对应。The outer diameter of the gasket corresponds to the outer diameter of the inner ring of the bearing.
所述的轴承采用高精度的角接触球轴承。The bearing adopts high precision angular contact ball bearing.
本实用新型使用时,先将两排轴承安装在芯轴的阶梯小端,再将定位套套在轴承上,用弹性挡圈将轴承定位,装上垫片,用螺母拧紧,最后将工件装在定位套上。将本装置装到超精磨机床上,当工件旋转时,定位套和工件一起同步转动,而工件和芯轴之间没有相对转动,不再对工件的内径产生划伤、磨损。When the utility model is used, two rows of bearings are firstly installed on the small stepped end of the mandrel, then the positioning sleeve is sleeved on the bearing, the bearing is positioned with an elastic retaining ring, a gasket is installed, tightened with a nut, and finally the workpiece is installed on the Positioning sleeve. When the device is installed on the ultra-fine grinding machine, when the workpiece rotates, the positioning sleeve and the workpiece rotate synchronously, and there is no relative rotation between the workpiece and the mandrel, and the inner diameter of the workpiece is no longer scratched and worn.
本实用新型的有益效果是:该装置设计科学,结构简单,使用轻便,对工件的内径有良好保护作用,提高了工件的加工质量,进一步提升了工件的使用寿命。The beneficial effects of the utility model are as follows: the device is scientifically designed, simple in structure, light in use, has a good protective effect on the inner diameter of the workpiece, improves the processing quality of the workpiece, and further increases the service life of the workpiece.
附图说明Description of drawings
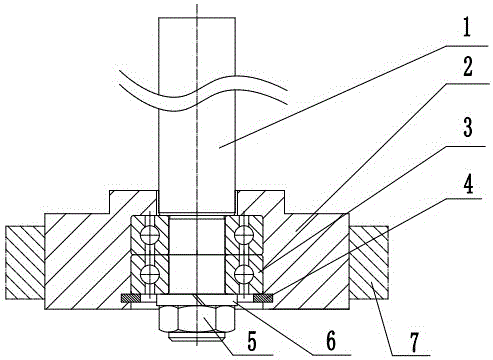
图1为本实用新型的主视图;Fig. 1 is the front view of the utility model;
图2为本实用新型的芯轴主视图;Fig. 2 is the front view of the mandrel of the utility model;
图3为本实用新型的定位套主视图;Fig. 3 is the front view of the positioning sleeve of the utility model;
图中标记:1、芯轴,2、定位套,3、轴承,4、弹性挡圈,5、螺母,6、垫片,7、工件。Marked in the figure: 1. Mandrel, 2. Positioning sleeve, 3. Bearing, 4. Retaining ring, 5. Nut, 6. Washer, 7. Workpiece.
具体实施方式Detailed ways
以下结合附图对本实用新型的具体实施方式做进一步的详细说明。The specific embodiments of the present utility model will be further described in detail below with reference to the accompanying drawings.
如图1、图2、图3所示,一种铁路轴承内圈超精加工定位芯轴装置,包括:芯轴1、定位套2、轴承3、弹性挡圈4、螺母5和垫片6;所述的芯轴1为阶梯圆柱芯轴,阶梯小端设置两排轴承3,小端的外径尺寸和轴承3内圈的内径尺寸高精度配合,端头设置一段螺纹,和螺母5的螺纹相对应;所述的定位套2为带台阶的环形套,内孔为两段阶梯孔,台阶小端的孔径尺寸略大于芯轴1大端的外径尺寸,保证芯轴1大端和定位套2不接触,定位套2中部的阶梯孔安装在轴承3的外径上,阶梯孔的长度及孔径尺寸和两个轴承3的轴向尺寸及外径尺寸相匹配,和轴承3高精度配合,装轴承3的一端端口设置挡圈槽,挡圈槽在定位套2中的位置正好满足两轴承3的轴向尺寸;定位套2的大端外径尺寸和工件7的内径尺寸高精度配合,使工件7在定位套2上固定不动;所述的弹性挡圈4安装在定位套2的挡圈槽内,对轴承3起定位作用;所述的垫片6套在芯轴1带螺纹一端,垫片6的外径尺寸和轴承3内圈的外径尺寸相对应,正好挡在轴承3的内圈上,通过螺母5压紧在内圈端面上;所述的轴承3采用高精度的角接触球轴承,确保了芯轴1的回转精度高,对产品的加工质量有保证。As shown in Figures 1, 2 and 3, a super-finishing positioning mandrel device for the inner ring of a railway bearing includes: a
本实用新型的工艺过程是:先将两排高精度的轴承3安装在芯轴1的阶梯小端,再将定位套2穿过芯轴1大端套在轴承3的外径上,用弹性挡圈4放置到定位套2的挡圈槽内,将轴承3定位,接着装上垫片6,用螺母5拧紧,将垫片6压在轴承3的内圈端面上,最后将工件7装在定位套2上。将本装置安装到超精磨机床上,当工件7旋转时,定位套2和工件7一起同步转动,而工件7和芯轴1之间没有相对转动,不再对工件7的内径产生划伤、磨损,对工件7的内径有良好保护作用,提高了工件7的加工质量,进一步提升了铁路轴承的使用寿命。The technological process of the present utility model is as follows: firstly, two rows of high-
Claims (6)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201920427036.6U CN210024884U (en) | 2019-04-01 | 2019-04-01 | A super-finishing positioning mandrel device for the inner ring of a railway bearing |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201920427036.6U CN210024884U (en) | 2019-04-01 | 2019-04-01 | A super-finishing positioning mandrel device for the inner ring of a railway bearing |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN210024884U true CN210024884U (en) | 2020-02-07 |
Family
ID=69357333
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201920427036.6U Active CN210024884U (en) | 2019-04-01 | 2019-04-01 | A super-finishing positioning mandrel device for the inner ring of a railway bearing |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN210024884U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116818886A (en) * | 2023-06-30 | 2023-09-29 | 天津理工大学 | Pipeline welding seam scanning device |
-
2019
- 2019-04-01 CN CN201920427036.6U patent/CN210024884U/en active Active
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN116818886A (en) * | 2023-06-30 | 2023-09-29 | 天津理工大学 | Pipeline welding seam scanning device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN205765315U (en) | On-line grinding device for pipeline female cone sealing surface | |
| CN207522261U (en) | A kind of self-centering burnishing device of outer round mouth deburring for steel pipe end surface | |
| WO2018103030A1 (en) | Tri-axial ball bearing extrusion jig | |
| CN210938276U (en) | Centering shaft for supporting bearing inner ring during super-finishing | |
| CN103122981B (en) | A kind of support unit supporting different axle head sized balls leading screw | |
| CN201366604Y (en) | Rolling tool for hole | |
| CN204976329U (en) | Deep hole internal grinding head | |
| CN102114588A (en) | Dedicated rolling head for rolling super-long deep hole | |
| CN105114454A (en) | Anti-backlash rolling bearing device for battery pole piece rolling mill | |
| CN204524702U (en) | A kind of excircle surface rolling device | |
| CN107511725B (en) | Precise movable center device | |
| CN105538125B (en) | A kind of Superfinishing machine supporting mechanism | |
| CN111203769A (en) | Tapered roller grinding method and device based on large-end spherical datum plane as datum positioning | |
| CN204545815U (en) | A kind of cylinder mirror processing device | |
| CN201544007U (en) | Rolling cutter | |
| CN201931249U (en) | Rolling-pressing head special for rolling and pressing ultra-long deep hole | |
| CN203125182U (en) | Bearing support processing device | |
| CN109794537B (en) | Tri-rotor Spinning Fixture for Small Diameter Plunger Assembly and Its Operation Technology | |
| CN217966537U (en) | A high-precision support for the spindle of a grinding machine | |
| CN211136542U (en) | Special baffle device for workpiece flush | |
| CN216298767U (en) | Waterproof rotary flat center device | |
| CN112276699A (en) | Bearing Roller Positioning Grinding Support Structure | |
| CN213224972U (en) | A valve stem roller | |
| CN201067821Y (en) | Core shaft clamp for machining disc type gear | |
| CN106002182A (en) | Installation tool special for fixing bearing by means of roller-type ring-shaped rolling bearing seat |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| GR01 | Patent grant | ||
| CP03 | Change of name, title or address | ||
| CP03 | Change of name, title or address |
Address after: 471039 No. 96, Jianxi, Luoyang District, Henan, Jianshe Road Patentee after: Luoyang Bearing Group Co.,Ltd. Country or region after: China Patentee after: Luoyang Bearing Group Railway Bearing Co.,Ltd. Address before: 471039 No. 96, Jianxi, Luoyang District, Henan, Jianshe Road Patentee before: LUOYANG LYC BEARING Co.,Ltd. Country or region before: China Patentee before: Luoyang Bearing Group Railway Bearing Co.,Ltd. |