CN203636194U - Automatic spot welding tongs - Google Patents
Automatic spot welding tongs Download PDFInfo
- Publication number
- CN203636194U CN203636194U CN201320690888.7U CN201320690888U CN203636194U CN 203636194 U CN203636194 U CN 203636194U CN 201320690888 U CN201320690888 U CN 201320690888U CN 203636194 U CN203636194 U CN 203636194U
- Authority
- CN
- China
- Prior art keywords
- copper
- electrode
- automatic spot
- caliper
- cylinder
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003466 welding Methods 0.000 title abstract description 16
- RYGMFSIKBFXOCR-UHFFFAOYSA-N Copper Chemical compound [Cu] RYGMFSIKBFXOCR-UHFFFAOYSA-N 0.000 claims abstract description 31
- 229910052802 copper Inorganic materials 0.000 claims abstract description 31
- 239000010949 copper Substances 0.000 claims abstract description 31
- 210000000080 chela (arthropods) Anatomy 0.000 claims description 12
- 238000001816 cooling Methods 0.000 claims description 3
- 238000009413 insulation Methods 0.000 claims description 3
- 238000009434 installation Methods 0.000 claims description 2
- 229910000975 Carbon steel Inorganic materials 0.000 abstract description 3
- 239000010962 carbon steel Substances 0.000 abstract description 3
- 238000000034 method Methods 0.000 abstract description 3
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 abstract 8
- 229910052742 iron Inorganic materials 0.000 abstract 4
- 239000000498 cooling water Substances 0.000 abstract 1
- 238000005516 engineering process Methods 0.000 description 4
- 239000000463 material Substances 0.000 description 2
- 238000005476 soldering Methods 0.000 description 2
- 238000005266 casting Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
- 238000007634 remodeling Methods 0.000 description 1
Images

Landscapes
- Resistance Welding (AREA)
Abstract
The utility model relates to a pair of automatic spot welding tongs which comprises an iron tong body, wherein a copper electrode base is arranged on the iron tong body; an electrode cap is arranged on the copper electrode base; the other end of the iron tong body is connected with a cylinder; an electrode holder is arranged on the main shaft of the cylinder; an electrode rod is arranged on the electrode holder; the electrode holder is connected with a soft copper bar; the copper electrode base is connected with a copper bar. The copper bar is arranged on the iron tong body. As improvement, an insulating sleeve is arranged between the electrode holder and the main shaft of the cylinder. A cooling water inlet is formed in one side of the copper electrode base. The automatic spot welding tongs provided by the utility model are wide in application, can be held by hand to operate, and can be also arranged on a three-dimensional servo mechanism or an arm of a robot for automatic operation. As the tong body is made of carbon steel to reduce the resistance of a welding loop, the copper bar is additionally arranged beside the tong body, so that a good path is provided for welding current, and the requirements of a welding process are met.
Description
Technical field
The utility model relates to a kind of electric welding equipment, is specifically related to a kind of automatic spot pincers.
Background technology
At present, the soldering turret of spot-welding technology is because the welding current of flowing through is large, electrode operating pressure is large, and therefore caliper forms by copper material casting, its complex manufacturing process, and the cycle is longer, and processing cost is very high.
Utility model content
The technical problems to be solved in the utility model is to provide a kind of pliers spot welding head that can carry out automatic spot.
For solving the problems of the technologies described above, automatic spot pincers of the present utility model, comprise irony caliper, copper electrode seat is installed on irony caliper, installing electrodes cap on copper electrode seat, the irony caliper other end connects cylinder, on cylinder main shaft, installing electrodes is held, electrode is held installing electrodes bar, and electrode is held connection soft copper row, and copper electrode seat connects a copper bar.Adopt this set can reduce the resistance of welding circuit.
Improve as one, described copper installation is on irony caliper.The welding current that is set to like this provides good path, has met welding process requirement.
Improve as one, described electrode is held between the main shaft of cylinder insulation sleeve is installed.
Improve as one, a side of copper electrode seat is provided with cooling nozzle.
Improve as one, described irony caliper is U-shaped.
Adopt after such structure, automatic spot of the present utility model pincers are widely used, can be by artificial hand-held, and also can be placed on the arm of three-dimensional servo control mechanism or robot and realize automatic operation.When manual operation, can in position configure handle, be convenient to grip; Fixture can be set when automatic operation to be fixed on servo control mechanism.Because caliper changes carbon steel into, in order to reduce the resistance of welding circuit, add copper bar on caliper side, for welding current provides good path, meet welding process requirement.
Accompanying drawing explanation
Below in conjunction with the drawings and specific embodiments, the utility model is described in further detail.
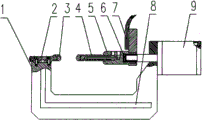
Fig. 1 is the structural representation of automatic spot pincers of the present utility model.
Fig. 2 is the top view of automatic spot pincers of the present utility model.
The specific embodiment
As depicted in figs. 1 and 2, automatic spot pincers of the present utility model comprise U-shaped irony caliper 1, copper electrode seat 2 is installed on irony caliper 1, installing electrodes cap 3 on copper electrode seat 2, irony caliper 1 other end connects cylinder 9, on the main shaft of cylinder 9, installing electrodes holds 5, electrode is held installing electrodes bar 4 on 5, electrode is held and on 5, is connected soft copper row 7, copper electrode seat 2 connects a copper bar 8, copper bar 8 is arranged on irony caliper 1, electrode hold 5 and the main shaft of cylinder 9 between insulation sleeve 6 is installed, one side of copper electrode seat 2 is provided with cooling nozzle 10, soldering turret entirety is carbon steel material and is made, between its each parts, be all welded to connect.
The above, only to preferred embodiment of the present utility model, not the utility model is done to other forms of restriction, any those skilled in the art may utilize the technology contents of above-mentioned announcement to be changed or be modified as the equivalent embodiment of equal variation.Every the utility model scheme content that do not depart from,, all drops in protection domain of the present utility model any simple modification made for any of the above embodiments, equivalent variations and remodeling according to technical spirit of the present utility model.
Claims (5)
1. automatic spot pincers, it is characterized in that: comprise irony caliper, copper electrode seat is installed on irony caliper, installing electrodes cap on copper electrode seat, the irony caliper other end connects cylinder, and on cylinder main shaft, installing electrodes is held, and electrode is held installing electrodes bar, electrode is held connection soft copper row, and copper electrode seat connects a copper bar.
2. according to automatic spot pincers claimed in claim 1, it is characterized in that: described copper installation is on irony caliper.
3. according to automatic spot claimed in claim 1 pincers, it is characterized in that: described electrode is held between the main shaft of cylinder insulation sleeve is installed.
4. according to the automatic spot pincers described in claim 1,2 or 3, it is characterized in that: a side of copper electrode seat is provided with cooling nozzle.
5. according to automatic spot pincers claimed in claim 3, it is characterized in that: described irony caliper is U-shaped.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320690888.7U CN203636194U (en) | 2013-10-30 | 2013-10-30 | Automatic spot welding tongs |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320690888.7U CN203636194U (en) | 2013-10-30 | 2013-10-30 | Automatic spot welding tongs |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203636194U true CN203636194U (en) | 2014-06-11 |
Family
ID=50867474
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201320690888.7U Expired - Fee Related CN203636194U (en) | 2013-10-30 | 2013-10-30 | Automatic spot welding tongs |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203636194U (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108381084A (en) * | 2018-03-17 | 2018-08-10 | 江苏车瑞智能装备有限公司 | Planer-type aluminium caliper |
| CN113351967A (en) * | 2020-03-06 | 2021-09-07 | 广州优尼冲压有限公司 | DCE bolt pressure welding device |
-
2013
- 2013-10-30 CN CN201320690888.7U patent/CN203636194U/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108381084A (en) * | 2018-03-17 | 2018-08-10 | 江苏车瑞智能装备有限公司 | Planer-type aluminium caliper |
| CN113351967A (en) * | 2020-03-06 | 2021-09-07 | 广州优尼冲压有限公司 | DCE bolt pressure welding device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN203712067U (en) | Welding bolt locating device | |
| CN204584527U (en) | A kind of gate-type submerged arc welding machine | |
| CN109483035A (en) | A kind of indirect welding soldering turret and indirect welding device | |
| CN101934436A (en) | Efficient welding rod | |
| CN202219369U (en) | Multi-welding spot electric welder | |
| CN103639634A (en) | Welding tool for outgoing line | |
| CN203541787U (en) | Double-head electric soldering iron | |
| CN202586064U (en) | Automatic tinning device | |
| CN203171125U (en) | Core-sleeving fixing device for electrode holders spring | |
| CN201644970U (en) | Brazing machine | |
| CN201815791U (en) | Hanging spot welding positioning device | |
| CN207289142U (en) | One kind is without dead angle air cooling type argon arc welding gun TIG-150 | |
| CN201970002U (en) | Electrode holder | |
| CN206356720U (en) | It is a kind of to get the fixture of copper bar ready for clamping | |
| CN203390413U (en) | Novel welding equipment for silk-covered flat type copper wire | |
| CN103157943A (en) | Positioning clamp for welding | |
| CN101369482A (en) | Water-cooled transformer and its welding method for line pipe and connection copper bar | |
| CN202447820U (en) | Flexible-electrode and welding fixture for keeping workpiece position | |
| CN202444170U (en) | Welding clamp for coil wires of transformer | |
| CN201592319U (en) | Welding clamp with safe operation | |
| CN103567589A (en) | Double-headed electric soldering iron for welding | |
| CN201192753Y (en) | Copper iron joint type electrode holder core with top joint | |
| CN201744775U (en) | Environmental-protection energy-saving electric welding extension clamp | |
| CN201455521U (en) | Soldering pliers for electric-arc welding device | |
| CN103567616A (en) | Welding gun |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20140611 Termination date: 20191030 |