CN203509608U - Multifunctional clamp - Google Patents
Multifunctional clamp Download PDFInfo
- Publication number
- CN203509608U CN203509608U CN201320559669.5U CN201320559669U CN203509608U CN 203509608 U CN203509608 U CN 203509608U CN 201320559669 U CN201320559669 U CN 201320559669U CN 203509608 U CN203509608 U CN 203509608U
- Authority
- CN
- China
- Prior art keywords
- compression
- screw nut
- positioning
- guide
- clamp body
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 230000007246 mechanism Effects 0.000 claims abstract description 38
- 230000006835 compression Effects 0.000 claims description 36
- 238000007906 compression Methods 0.000 claims description 36
- 238000010586 diagram Methods 0.000 description 7
- 238000003754 machining Methods 0.000 description 7
- 238000005553 drilling Methods 0.000 description 4
- 230000007547 defect Effects 0.000 description 3
- 238000006073 displacement reaction Methods 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- XEEYBQQBJWHFJM-UHFFFAOYSA-N Iron Chemical compound [Fe] XEEYBQQBJWHFJM-UHFFFAOYSA-N 0.000 description 1
- 230000002950 deficient Effects 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
Images







Landscapes
- Jigs For Machine Tools (AREA)
Abstract
本实用新型公开了一种多功能夹具,该夹具专用于加工C6140车床床头箱拨叉,其包括定位机构、夹紧机构以及导向机构。该定位机构的定位钉采用在夹具体上设置孔进行安装,可以随时安装拆卸,因此根据加工阶段可以选用不同规格的定位钉,使一套夹具可以适用不同的加工阶段,减少了夹具体的套数。而夹紧机构采用可调式支撑螺杆螺母,提高了夹紧的稳定性。导向机构的导套在拆卸时,采用螺栓顶出方式,拆卸方便,提高了钻套的使用周期。

The utility model discloses a multifunctional fixture, which is specially used for processing the shift fork of the headstock of a C6140 lathe, and comprises a positioning mechanism, a clamping mechanism and a guiding mechanism. The positioning nails of the positioning mechanism are installed by setting holes on the clamp body, and can be installed and disassembled at any time. Therefore, positioning nails of different specifications can be selected according to the processing stage, so that a set of fixtures can be applied to different processing stages, reducing the number of sets of clamp bodies. . The clamping mechanism adopts an adjustable support screw nut, which improves the stability of clamping. When the guide sleeve of the guide mechanism is disassembled, the bolt is ejected, which is convenient for disassembly and improves the service life of the drill sleeve.
Description
技术领域 technical field
本实用新型涉及机械加工的技术领域,尤指一种专用于加工C6140车床床头箱的拨叉所使用的夹具。 The utility model relates to the technical field of mechanical processing, in particular to a fixture specially used for processing a shift fork of a head box of a C6140 lathe.
背景技术 Background technique
工件的加工都需要夹具以辅助定位,C6140车床床头箱拨叉的加工也不例外,C6140车床床头箱拨叉1的结构如图1所示。但是,C6140车床床头箱拨叉的现有夹具却存在如下缺陷: The processing of the workpiece requires fixtures to assist in positioning, and the processing of the headbox fork of the C6140 lathe is no exception. The structure of the headbox fork 1 of the C6140 lathe is shown in Figure 1. But, the existing fixture of C6140 lathe headstock shift fork has following defectives:
1.定位缺陷:目前在加工C6140车床床头箱拨叉时,所采用夹具的定位元件都是固定在夹具体上的,不能移动调节,也不能进行更换。但是,由于在加工过程中每个阶段(粗加工或者精加工等)的加工余量不同,就会导致被加工零件在夹具体上的定位也不一样的。因此具有一种规格定位元件的夹具只能满足一种加工阶段:要么是粗加工要么是精加工。这就要求每个加工阶段都要有一套夹具设置相对应的定位元件配合使用,这就提高了成本。 1. Positioning defect: At present, when processing the fork of the headstock of the C6140 lathe, the positioning elements of the fixture used are all fixed on the fixture body, and cannot be moved, adjusted, or replaced. However, due to the different machining allowances at each stage (rough machining or finishing machining, etc.) in the machining process, the positioning of the machined parts on the clamp body will also be different. Therefore, a fixture with one specification of positioning elements can only satisfy one processing stage: either roughing or finishing. This requires a set of fixtures to be used in conjunction with positioning elements corresponding to each processing stage, which increases the cost.
2.夹紧机构的缺陷:所述拨叉的现有夹具的夹紧机构4'如图2所示,其主要包括压紧杠杆41'、压紧螺杆螺母组42'、压紧螺母43'、平衡螺杆螺母组44'以及支撑杆45',工件被夹在压紧杠杆41'与支撑杆45'之间。然而现有夹具由于支撑杆45'是固定的,采用固定支撑,不可调节,因此夹紧稳定性不高。 2. Defects of the clamping mechanism: the clamping mechanism 4' of the existing fixture of the shift fork is shown in Figure 2, which mainly includes a compression lever 41', a compression screw nut group 42', a compression nut 43', a balance The screw nut group 44' and the supporting rod 45', the workpiece is clamped between the pressing lever 41' and the supporting rod 45'. However, the existing clamps are not adjustable because the support rod 45' is fixed and supported by a fixed structure, so the clamping stability is not high.
3.导向机构缺陷:在钻拨叉1的孔11时,目前一般都采用普通导套进行刀具的定位,而现有夹具的导套与钻模板是过盈配合,所以在拆卸导套时,一般采用敲打的方式拆卸,很容易对导套造成伤害,缩短了导套的使用周期。
3. Defects of the guide mechanism: When drilling the
实用新型内容 Utility model content
本实用新型所要解决的技术问题在于提供一种可以更换不同规格定位元件的多功能夹具,以使一套夹具可以适用多个加工阶段。 The technical problem to be solved by the utility model is to provide a multifunctional fixture that can replace positioning elements of different specifications, so that a set of fixtures can be applied to multiple processing stages.
本实用新型所要解决的另一技术问题在于提供一种多功能夹具,其夹紧机构的支撑为可调支撑,以提高夹紧稳定性。 Another technical problem to be solved by the utility model is to provide a multifunctional clamp, the support of the clamping mechanism is an adjustable support to improve the clamping stability.
本实用新型所要解决的又一技术问题在于提供一种导套拆卸方便的多功能夹具。 Yet another technical problem to be solved by the utility model is to provide a multi-functional clamp with convenient disassembly of the guide sleeve.
为解决上述技术问题,本实用新型的技术解决方案是: For solving the problems of the technologies described above, the technical solution of the utility model is:
一种多功能夹具,包括夹具体、定位机构、夹紧机构以及导向机构;所述的夹具体由一块底板及垂直且刚性连接在该底板上的两块竖板组成,两块竖板也相互垂直,并定义垂直于底板的方向为Z向,分别垂直于两块竖板的方向为X向及Y向;垂直于X向的竖板上开有一个X向孔,另一块竖板上开有两个Y向孔;所述的定位机构包括一块Z向定位板、一个X向定位钉及两个Y向定位钉,该Z向定位板固定在所述底板上,该X向定位钉插接在所述X向孔上,所述Y向定位钉插接在所述Y向孔上。 A multifunctional fixture, including a clamp body, a positioning mechanism, a clamping mechanism and a guide mechanism; the clamp body is composed of a bottom plate and two vertical plates rigidly connected to the bottom plate, and the two vertical plates are also connected to each other Vertical, and define the direction perpendicular to the bottom plate as the Z direction, and the directions perpendicular to the two vertical plates as the X direction and the Y direction; there is an X-directed hole on the vertical plate perpendicular to the X direction, and a hole on the other vertical plate. There are two Y-direction holes; the positioning mechanism includes a Z-direction positioning plate, an X-direction positioning nail and two Y-direction positioning nails, the Z-direction positioning plate is fixed on the bottom plate, and the X-direction positioning nail is inserted connected to the X-direction hole, and the Y-direction positioning nail is inserted into the Y-direction hole.
所述的夹紧机构包括压紧杠杆、压紧螺杆螺母组、压紧螺母、平衡螺杆螺母组以及可调支撑螺杆螺母组,该可调支撑螺杆螺母组、压紧螺杆螺母组以及平衡螺杆螺母组依次且呈一字形螺旋固定在所述夹具体底板上的相应螺纹孔上,所述压紧杠杆套在所述压紧螺杆螺母组上,所述压紧螺母旋在该压紧螺杆螺母的螺杆上。 The clamping mechanism includes a compression lever, a compression screw nut group, a compression nut, a balance screw nut group and an adjustable support screw nut group, and the adjustable support screw nut group, the compression screw nut group and the balance screw nut group The groups are sequentially and in-line helically fixed on the corresponding threaded holes on the bottom plate of the clamp body, the compression lever is sleeved on the compression screw nut group, and the compression nut is screwed on the compression screw nut. on the screw.
所述压紧螺杆螺母组的螺杆上套有一弹簧,该弹簧位于所述压紧杠杆的下方。 A spring is sheathed on the screw rod of the compression screw nut group, and the spring is located below the compression lever.
所述的导向机构包括钻模板及导套,该钻模板固定在所述夹具体的其中一个竖板顶部,其上设有导孔,该导套套在该导孔内,且两者为过盈配合;所述导套的上边缘设有凸台,该凸台上设有至少两个螺纹孔。 The guide mechanism includes a drill template and a guide sleeve, the drill template is fixed on the top of one of the vertical plates of the clamp body, and a guide hole is provided on it, and the guide sleeve is sleeved in the guide hole, and the two are interference Cooperate; the upper edge of the guide sleeve is provided with a boss, and the boss is provided with at least two threaded holes.
采用上述方案后,本实用新型具有如下优点: After adopting the above scheme, the utility model has the following advantages:
1.由于在夹具体上设计了用以安装定位钉的孔,这样定位钉即可随时安装或者拆卸,因此在加工过程中,可以根据加工余量的不同,选择不同规格的定位钉安装到夹具体上,使一套夹具可以适应于粗加工和精加工两种加工阶段,减少了夹具的套数,降低了成本; 1. Since holes for installing positioning nails are designed on the clamp body, the positioning nails can be installed or disassembled at any time. Therefore, during the processing, positioning nails of different specifications can be selected and installed on the clamp body according to the difference in machining allowance. , so that a set of fixtures can be adapted to two processing stages of rough machining and finishing, reducing the number of sets of fixtures and reducing the cost;
2.所述夹紧机构的支撑端以及平衡端均采用了螺杆螺母组的高度可调结构,而可调支撑提高了夹紧的稳定性,可调平衡端则起到平衡夹紧力及防止工件位移和变形的作用; 2. The support end and the balance end of the clamping mechanism both adopt the height-adjustable structure of the screw nut group, and the adjustable support improves the stability of the clamping, and the adjustable balance end balances the clamping force and prevents the displacement of the workpiece and deformation effects;
3.在所述导向机构的导套上设置了凸台,并在凸台上设置至少两个螺纹孔,这样在拆卸时,可以利用螺栓顶住钻模板,将导套顶出而拆卸;这样拆卸方式方便、快捷、而且不损坏导套,可以延长导套的使用周期。 3. A boss is set on the guide sleeve of the guide mechanism, and at least two threaded holes are set on the boss, so that when dismounting, the bolt can be used to withstand the drilling template, and the guide sleeve can be ejected and disassembled; It is convenient, fast, and does not damage the guide sleeve, and can prolong the service life of the guide sleeve.
附图说明 Description of drawings
图1是C6140车床床头箱拨叉的结构示意图; Fig. 1 is a structural schematic diagram of a C6140 lathe bedside box shift fork;
图2是所述拨叉的现有夹具的夹紧机构的结构示意图; Fig. 2 is a structural schematic diagram of the clamping mechanism of the existing fixture of the shift fork;
图3是本实用新型的总装配三维图; Fig. 3 is a three-dimensional diagram of the general assembly of the utility model;
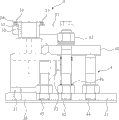
图4是本实用新型的总装配示意图; Fig. 4 is the general assembly schematic diagram of the present utility model;
图5是本实用新型的总装配俯视图; Fig. 5 is a top view of the general assembly of the utility model;
图6是图5的A-A剖视图; Fig. 6 is A-A sectional view of Fig. 5;
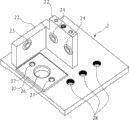
图7是本实用新型所述夹具体的三维视图; Fig. 7 is a three-dimensional view of the clip body described in the present invention;
图8是本实用新型所述定位机构的三维图; Fig. 8 is a three-dimensional diagram of the positioning mechanism described in the present invention;
图9是本实用新型所述定位机构安装在夹具体上的示意图; Fig. 9 is a schematic diagram of the positioning mechanism of the present invention installed on the clamp body;
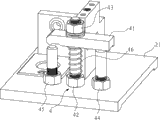
图10是本实用新型所述夹紧机构安装在夹具体上的示意图; Fig. 10 is a schematic diagram of the clamping mechanism of the present invention installed on the clamp body;
图11是本实用新型所述导向机构安装在夹具体上的示意图。 Fig. 11 is a schematic view of the guide mechanism of the present invention installed on the clamp body.
具体实施方式 Detailed ways
下面结合附图和具体实施例对本实用新型作进一步详述。 Below in conjunction with accompanying drawing and specific embodiment the utility model is described in further detail.
本实用新型所揭示的是一种多功能夹具,该夹具专用于C6140车床床头箱拨叉1(如图1所示)的加工,如图3至图6所示,为本实用新型的较佳实施例。所述的夹具包括夹具体2、定位机构3、夹紧机构4以及导向机构5。其中:
What the utility model discloses is a kind of multifunctional fixture, and this fixture is specially used in the processing of C6140 lathe head box shift fork 1 (shown in Fig. 1), as shown in Fig. 3 to Fig. 6, is the utility model comparatively good example. The clamp includes a clamp body 2 , a
同时配合图7所示,所述的夹具体2由一块底板21及垂直且刚性连接在该底板21上的两块竖板22组成,两块竖板22也相互垂直,并定义垂直于底板21的方向为Z向,分别垂直于两块竖板22的方向为X向及Y向。垂直于X向的竖板22上开有一个X向孔23,另一块竖板22上开有两个Y向孔24。该底板21上设有一个凸台25用于放置后述的Z向定位板31,该凸台25上开有排屑孔26及两个沉头螺纹孔27,该沉头螺纹孔27用于Z向定位板31的定位安装,该排屑孔26用于钻孔时排出加工铁屑。所述的底板21上还设有三个螺纹孔28,用于安装后续夹紧机构4的三个螺杆螺母组。
Simultaneously as shown in FIG. 7 , the clamp body 2 is composed of a
同时配合图8及图9所示,所述的定位机构3包括一块Z向定位板31、一个X向定位钉32及两个Y向定位钉33。该Z向定位板31通过螺钉固定在所述夹具体2的底板21的凸台25上。所述X向定位钉32插接在所述夹具体2的X向孔23上,所述Y向定位钉33插接在所述夹具体2的Y向孔24上。所述Z向定位板31限制了拨叉Z向的移动;所述X向定位钉32限制了拨叉X向的移动和绕Y轴的转动;所述两个Y向定位钉33限制了拨叉Y 向的移动、绕X轴的转动和绕Z轴的转动;这样该组定位机构3共限制了拨叉的6个自由度,符合加工时的定位要求。由于所述的定位钉32、33都是以活动插接的方式定位在夹具体2上的,因此可以根据粗精加工等加工阶段的不同,更换不同规格的定位钉,这样只需一套夹具就可以适用不同加工阶段,减少了夹具的数量,降低了成本。
As shown in FIG. 8 and FIG. 9 , the
同时配合图10所示,所述的夹紧机构4包括压紧杠杆41、压紧螺杆螺母组42、压紧螺母43、平衡螺杆螺母组44以及可调支撑螺杆螺母组45,所述的可调支撑螺杆螺母组45、压紧螺杆螺母组42以及平衡螺杆螺母组44依次且呈一字形螺旋固定在所述夹具体2的底板21上相应的螺纹孔28上,且旋转相应的螺母,与之配合的螺杆的高度要以可以相对上下调节。所述压紧杠杆41套在所述压紧螺杆螺母组42上,所述压紧螺母43旋在该压紧螺杆螺母42的螺杆上。使用时,将工件放在夹具上并定位,之后调节可调支撑螺杆螺母组45的螺母,使其螺杆支撑端与工件接触,再调节平衡螺杆螺母组44的螺母,使其螺杆顶端与工件上被压点等高,然后再拧紧中间的压紧螺母43,使工件夹在压紧杠杆41与可调支撑螺母螺母组45之间,这样就可以实现对工件的夹紧。由于该夹紧机构的支撑端采用了高度可调的螺杆螺母组结构,可以根据工件的高度进行调节,因此可以提高夹紧的稳定。而另一端的平衡端,也采用高度可以调节的结构,可以起到平衡夹紧力的作用,可以防止工件位移和变形。此外,在所述压紧螺杆螺母组42的螺杆上还可以套一弹簧46,该弹簧46位于所述压紧杠杆41的下方。该弹簧46的作用时,当拆卸工件时,弹簧可以将压紧杠杆41弹起,以利于工件的拆卸。
Cooperate with shown in Figure 10 simultaneously, described
再同时配合图11所示,所述的导向机构5包括钻模板51及导套52,该钻模板51固定在所述夹具体2的其中一个竖板22顶部,其上设有导孔53,该导孔53位于所述拨叉1的孔11上方,该导套52套在该导孔53内,且两者为过盈配合。所述导套52的上边缘设有凸台54,该凸台54上设有至少两个螺纹孔55。在拆卸导套时,可以使用与该螺纹孔55相匹配的长螺栓拧在两个螺纹孔55内,当螺栓旋到底部时,继续旋紧螺栓,螺栓将顶住钻模板51,从而将导套52顶出。
At the same time, as shown in FIG. 11, the guide mechanism 5 includes a
以上所述,仅是本实用新型的较佳实施例而已,并非对本实用新型的技术范围作任何限制,故但凡依本实用新型的权利要求和说明书所做的变化或修饰,皆应属于本实用新型专利涵盖的范围之内。 The above are only preferred embodiments of the present utility model, and are not intended to limit the technical scope of the present utility model. Therefore, any changes or modifications made according to the claims of the utility model and the specification should belong to the utility model. Within the scope covered by the utility model patent.
Claims (4)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320559669.5U CN203509608U (en) | 2013-09-10 | 2013-09-10 | Multifunctional clamp |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320559669.5U CN203509608U (en) | 2013-09-10 | 2013-09-10 | Multifunctional clamp |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203509608U true CN203509608U (en) | 2014-04-02 |
Family
ID=50368590
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201320559669.5U Expired - Fee Related CN203509608U (en) | 2013-09-10 | 2013-09-10 | Multifunctional clamp |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203509608U (en) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104275617A (en) * | 2014-11-05 | 2015-01-14 | 重庆和剑机械制造有限公司 | Quick clamping device for milling lower plane of first/second-gear shifting fork |
| CN104308620A (en) * | 2014-11-05 | 2015-01-28 | 重庆和剑机械制造有限公司 | Simple positioning tool for milling biplanes of first and second gear shifting forks |
| CN104325331A (en) * | 2014-11-05 | 2015-02-04 | 重庆和剑机械制造有限公司 | Special auxiliary clamping mechanism for milling upper plane of one-and-two-gear shifting yoke |
| CN104353880A (en) * | 2014-11-05 | 2015-02-18 | 重庆和剑机械制造有限公司 | Precision machining equipment for lower plane of 1 and 2-gear shift fork of automobile |
| CN104384987A (en) * | 2014-11-04 | 2015-03-04 | 重庆和剑机械制造有限公司 | Rapid clamping mechanism for milling upper surface of reverse gear shifting fork |
| CN104439421A (en) * | 2014-12-10 | 2015-03-25 | 柳州杰龙汽车零部件制造有限公司 | Drilling equipment for drilling lower bracket for reaction rod in dumper bodies |
| CN104476269A (en) * | 2014-11-04 | 2015-04-01 | 重庆和剑机械制造有限公司 | Clamping mechanism special for milling upper and lower surfaces of reverse gear shifting fork |
| CN104493253A (en) * | 2014-12-09 | 2015-04-08 | 重庆迪科汽车研究有限公司 | Simple shifting fork drilling die |
| CN105372122A (en) * | 2015-11-28 | 2016-03-02 | 沈阳飞机工业(集团)有限公司 | Fixture for resin encapsulation of compression performance test piece and usage method thereof |
| CN109079392A (en) * | 2018-09-06 | 2018-12-25 | 浙江天马停车设备有限公司 | The two-sided dismountable weld holder of H-type pedestal |
-
2013
- 2013-09-10 CN CN201320559669.5U patent/CN203509608U/en not_active Expired - Fee Related
Cited By (13)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104384987A (en) * | 2014-11-04 | 2015-03-04 | 重庆和剑机械制造有限公司 | Rapid clamping mechanism for milling upper surface of reverse gear shifting fork |
| CN104476269A (en) * | 2014-11-04 | 2015-04-01 | 重庆和剑机械制造有限公司 | Clamping mechanism special for milling upper and lower surfaces of reverse gear shifting fork |
| CN104353880A (en) * | 2014-11-05 | 2015-02-18 | 重庆和剑机械制造有限公司 | Precision machining equipment for lower plane of 1 and 2-gear shift fork of automobile |
| CN104275617A (en) * | 2014-11-05 | 2015-01-14 | 重庆和剑机械制造有限公司 | Quick clamping device for milling lower plane of first/second-gear shifting fork |
| CN104325331A (en) * | 2014-11-05 | 2015-02-04 | 重庆和剑机械制造有限公司 | Special auxiliary clamping mechanism for milling upper plane of one-and-two-gear shifting yoke |
| CN104308620A (en) * | 2014-11-05 | 2015-01-28 | 重庆和剑机械制造有限公司 | Simple positioning tool for milling biplanes of first and second gear shifting forks |
| CN104353880B (en) * | 2014-11-05 | 2016-08-24 | 重庆和剑机械制造有限公司 | A kind of automobile one or two keeps off shift fork lower plane finishing equipment |
| CN104493253A (en) * | 2014-12-09 | 2015-04-08 | 重庆迪科汽车研究有限公司 | Simple shifting fork drilling die |
| CN104493253B (en) * | 2014-12-09 | 2017-03-08 | 重庆迪科汽车研究有限公司 | Simple shift fork drilling die |
| CN104439421A (en) * | 2014-12-10 | 2015-03-25 | 柳州杰龙汽车零部件制造有限公司 | Drilling equipment for drilling lower bracket for reaction rod in dumper bodies |
| CN105372122A (en) * | 2015-11-28 | 2016-03-02 | 沈阳飞机工业(集团)有限公司 | Fixture for resin encapsulation of compression performance test piece and usage method thereof |
| CN105372122B (en) * | 2015-11-28 | 2018-12-21 | 沈阳飞机工业(集团)有限公司 | A kind of fixture and application method for compression performance testpieces resin encapsulating |
| CN109079392A (en) * | 2018-09-06 | 2018-12-25 | 浙江天马停车设备有限公司 | The two-sided dismountable weld holder of H-type pedestal |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201399692Y (en) | Special fixture for milling machine | |
| CN204711607U (en) | A kind of automation fixture | |
| CN203019089U (en) | Moving lathe end beam boring mill clamp | |
| CN202479826U (en) | Clamp for machining thread hole of flange by drill | |
| CN103753271B (en) | Air cylinder clamp | |
| CN202317749U (en) | Cylinder bottom drilling fixture for jack | |
| CN101758397B (en) | Positioning and drilling fixture for crank oil hole | |
| CN203124795U (en) | Clamp for drilling | |
| CN105729164A (en) | Milling clamp for plane of sliding saddle | |
| CN105729169A (en) | Saddle boring and milling clamp | |
| CN205270951U (en) | Jig of radial spot facing work of adaptable multiple size vehicle axle | |
| CN103949909A (en) | CNC (computer numerical control) machined spherical piece combined clamp and clamping method | |
| CN106736765A (en) | An angle steel fixture | |
| CN202894837U (en) | Clamp for machining phi-30mm auxiliary hole of rear leaf spring shackle | |
| CN206185259U (en) | Dabber anchor clamps are used in processing | |
| CN110757213A (en) | Multi-station vertical machining center four-axis hydraulic clamp | |
| CN202684581U (en) | Universal clamp for machining ball screw pin hole | |
| CN208034157U (en) | Clamping jig for round piece | |
| CN205415037U (en) | A special fixture for drilling of arc work piece | |
| CN205325285U (en) | Lathe machining is with activity cushion structure | |
| CN204818867U (en) | A foundatin plate for inciting somebody to action frock clamp fixes on lathe | |
| CN201792222U (en) | Jig | |
| CN205074842U (en) | Eccentric orfice anchor clamps | |
| CN223251226U (en) | Tool setting gauge mounting structure for numerical control machine tool | |
| CN206689784U (en) | Frock clamp for milling flat |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20140402 Termination date: 20160910 |
|
| CF01 | Termination of patent right due to non-payment of annual fee |