CN203401113U - Drilling jig of half coupling - Google Patents
Drilling jig of half coupling Download PDFInfo
- Publication number
- CN203401113U CN203401113U CN201320508138.3U CN201320508138U CN203401113U CN 203401113 U CN203401113 U CN 203401113U CN 201320508138 U CN201320508138 U CN 201320508138U CN 203401113 U CN203401113 U CN 203401113U
- Authority
- CN
- China
- Prior art keywords
- coupler
- bushing
- bushing plate
- hole
- drill
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000005553 drilling Methods 0.000 title abstract description 16
- 230000008878 coupling Effects 0.000 title abstract description 7
- 238000010168 coupling process Methods 0.000 title abstract description 7
- 238000005859 coupling reaction Methods 0.000 title abstract description 7
- 238000000034 method Methods 0.000 description 3
- 238000005516 engineering process Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000006243 chemical reaction Methods 0.000 description 1
- 230000007547 defect Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
Images

Landscapes
- Drilling And Boring (AREA)
Abstract
The utility model discloses a drilling jig of a half coupling. The drilling jig comprises a drilling template and a base, wherein the drilling template is arranged on the upper side of the half coupling, the base is arranged on the lower side of the half coupling, a locating structure which is used for making the drilling template located to the half coupling is arranged on the drilling template, a drill bushing hole is formed in the drilling template, a drill bushing is arranged in the drill bushing hole, and a detachable clamping device is arranged between the drilling template and the base. According to the drilling jig, working efficiency is improved, and positional accuracy of the hole is improved.
Description
Technical field
The utility model relates to Machining Technology field, relates in particular to a kind of drill jig.
Background technology
Shaft coupling is a kind of part conventional in plant equipment, and its effect is that the axle of two rotations is linked together.Shaft coupling is generally comprised of two half a couplers, needs to arrange through hole on half a coupler, then a half a coupler is connected with bolt and nut by through hole with another half a coupler.Through hole on half a coupler is generally processed on drilling machine.If small lot batch manufacture, general employing line is rushed sample and is then placed on drilling machine and holes, if produce in enormous quantities, if also adopt this method boring, have following problem, the one, it is very time-consuming that sample is rushed in line, operating efficiency is very low, and the 2nd, it is low that the hole site precision that sample bores is rushed in line.
Utility model content
Problem to be solved in the utility model is, for the defect of prior art, provides a kind of half a coupler drill jig, can increase work efficiency and improve the positional precision in hole.
The purpose of this utility model is achieved through the following technical solutions.A kind of half a coupler drill jig, comprise be arranged on half a coupler upside bushing plate, be arranged on the base of half a coupler downside, bushing plate is provided with for bushing plate being positioned to the location structure on half a coupler, on bushing plate, be also provided with drill bushing hole, drill bushing is provided with drill bushing in hole, is provided with dismountable clamping device between described bushing plate and base.During use, half a coupler is placed on base, and bushing plate is placed on half a coupler, utilizes location structure that bushing plate is accurately located on half a coupler, with clamping device, bushing plate, half a coupler and base are clamped again, then place it on drilling machine and can hole.After a half a coupler drilling part completes, clamping device is unclamped, part takes off, then another half a coupler part is processed by the same method.Adopt this device, need not rule and rush sample, install and dismantle half a coupler conveniently, therefore improved operating efficiency, and because having adopted location structure location, therefore improved positioning precision, thereby improved the positional precision in hole.
As preferably, described bushing plate is circular configuration, and the center of bushing plate is provided with the through hole of a circle, and described location structure comprises the circle bulge loop arranging along the edge of bushing plate circle, and the U-shaped groove arranging on the circumference of through hole.Half a coupler is a circular configuration, and there is a manhole at center, has a U-shaped groove on the circumference of manhole.During use, the bulge loop of bushing plate is enclosed within on half a coupler, the U-shaped groove on bushing plate is alignd with the U-shaped groove on half a coupler, bushing plate can be positioned on half a coupler exactly, accurate positioning, the positional precision of boring is high.This location structure is simple, easy to use.
As preferably, described clamping device comprises C shape pad and stud, and C shape pad is arranged on the upside of bushing plate, and stud is through C shape pad, bushing plate, half a coupler and base, and fastening nuts is used respectively at the two ends of stud.This clamping device is simple in structure, easy to operate.
As preferably, described drill bushing hole is circular configuration, and the circumference in drill bushing hole is provided with some semi-circular recesses.Between drill bushing and drill bushing hole, be interference fit, drill bushing produces wearing and tearing after using a period of time, drill bushing must be taken out from the drill bushing hole of bushing plate, because be interference fit, during taking-up, frictional force is very large, is difficult to take out.Semi-circular recesses is set, has reduced the contact area between drill bushing and bushing plate, thereby reduced frictional force, be easy to operate, improved operating efficiency.
Main beneficial effect of the present utility model is, improved operating efficiency, improved the hole site precision of half a coupler.
Accompanying drawing explanation
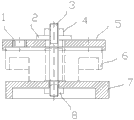
Fig. 1 is a kind of structural representation of the present utility model.
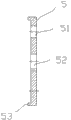
Fig. 2 is the structural representation of bushing plate.
Fig. 3 is the cutaway view of Fig. 2.
The specific embodiment
Below the utility model is described in further detail in conjunction with the accompanying drawings and embodiments:
As shown in Figure 1 to Figure 3, a kind of half a coupler drill jig, comprise the bushing plate 5 that is arranged on half a coupler 6 upsides, be arranged on the base 7 of half a coupler downside, bushing plate is circular configuration, the center of bushing plate is provided with the through hole 52 of a circle, bushing plate is provided with 6 drill bushing holes 51, drill bushing hole is circular configuration, the circumference in drill bushing hole is provided with four uniform semi-circular recesses 511, 6 drill bushing holes are positioned on same circumference, in each drill bushing hole, be provided with drill bushing 1, bushing plate is provided with for bushing plate being positioned to the location structure on half a coupler, location structure comprises the circle bulge loop 53 arranging along the edge of bushing plate circle, and the U-shaped groove arranging on the circumference of through hole 52.Between described bushing plate and base, be provided with dismountable clamping device, clamping device comprises C shape pad 2 and stud 3, C shape pad is arranged on the upside of bushing plate, stud is through C shape pad, bushing plate, half a coupler and base, the two ends of stud use respectively fastening nuts 4 and fastening nuts 8 fastening.
During use, half a coupler is placed on base, bushing plate is placed on half a coupler, bulge loop circle is lived half a coupler, U-shaped groove on bushing plate aligns with the U-shaped groove on half a coupler, C shape pad is arranged on the upside of bushing plate, and stud is through C shape pad, bushing plate, half a coupler and base, the two ends of stud use respectively fastening nuts 4 and fastening nuts 8 fastening.Then place it on drilling machine and can hole.After a half a coupler drilling part completes, clamping device is unclamped, part takes off, then another half a coupler part is processed by the same method.Adopt this device, need not rule and rush sample, install and dismantle half a coupler conveniently, therefore improved operating efficiency, and adopted location structure location, therefore improved positioning precision, thereby also improved the positional precision in hole.
The above is the preferably specific embodiment of the utility model, not with this, limits practical range of the present utility model.The utility model can also have other embodiment, only otherwise deviate from spirit of the present utility model, and within no matter in form what kind of conversion all drops on protection domain of the present utility model.
Claims (4)
1. a half a coupler drill jig, it is characterized in that, comprise be arranged on half a coupler upside bushing plate, be arranged on the base of half a coupler downside, bushing plate is provided with for bushing plate being positioned to the location structure on half a coupler, on bushing plate, be also provided with drill bushing hole, drill bushing is provided with drill bushing in hole, is provided with dismountable clamping device between described bushing plate and base.
2. half a coupler drill jig according to claim 1, it is characterized in that, described bushing plate is circular configuration, and the center of bushing plate is provided with the through hole of a circle, described location structure comprises the circle bulge loop arranging along the edge of bushing plate circle, and the U-shaped groove arranging on the circumference of through hole.
3. half a coupler drill jig according to claim 1, it is characterized in that, described clamping device comprises C shape pad and stud, and C shape pad is arranged on the upside of bushing plate, stud is through C shape pad, bushing plate, half a coupler and base, and fastening nuts is used respectively at the two ends of stud.
4. according to the half a coupler drill jig described in claim 1 or 2 or 3, it is characterized in that, described drill bushing hole is circular configuration, and the circumference in drill bushing hole is provided with some semi-circular recesses.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320508138.3U CN203401113U (en) | 2013-08-20 | 2013-08-20 | Drilling jig of half coupling |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN201320508138.3U CN203401113U (en) | 2013-08-20 | 2013-08-20 | Drilling jig of half coupling |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203401113U true CN203401113U (en) | 2014-01-22 |
Family
ID=49937056
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN201320508138.3U Expired - Fee Related CN203401113U (en) | 2013-08-20 | 2013-08-20 | Drilling jig of half coupling |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203401113U (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108672772A (en) * | 2018-06-07 | 2018-10-19 | 绵竹市科迪机械加工有限公司 | For drilling shaft sleeve fixing device |
| CN108746771A (en) * | 2018-06-07 | 2018-11-06 | 绵竹市科迪机械加工有限公司 | The fixture of axle sleeve process safety can be improved |
| CN112846302A (en) * | 2021-03-05 | 2021-05-28 | 中核核电运行管理有限公司 | Same-drilling reaming tool suitable for machining pin hole of main pump coupler |
-
2013
- 2013-08-20 CN CN201320508138.3U patent/CN203401113U/en not_active Expired - Fee Related
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108672772A (en) * | 2018-06-07 | 2018-10-19 | 绵竹市科迪机械加工有限公司 | For drilling shaft sleeve fixing device |
| CN108746771A (en) * | 2018-06-07 | 2018-11-06 | 绵竹市科迪机械加工有限公司 | The fixture of axle sleeve process safety can be improved |
| CN112846302A (en) * | 2021-03-05 | 2021-05-28 | 中核核电运行管理有限公司 | Same-drilling reaming tool suitable for machining pin hole of main pump coupler |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN201720483U (en) | Drilling equipment for drilling circumference of circular shaft parts | |
| CN203679353U (en) | Valve body drilling jig for marine stop valve | |
| CN202964162U (en) | Tool for guaranteeing coaxiality of flange hole | |
| CN203679354U (en) | Valve body drill jig of butterfly valve | |
| CN202779918U (en) | Porous punching and positioning die for circular plane disk | |
| CN103522276A (en) | Idler wheel gauge | |
| CN203171016U (en) | Drilling clamp of shell part | |
| CN202571915U (en) | Clamp for numerical control drilling of disc-shaped workpieces | |
| CN203817786U (en) | Positioning device for shifting fork drill jig | |
| CN202317767U (en) | Shaft parts drilling fixture | |
| CN203448719U (en) | Drill jig for outer-circle end face of machine base | |
| CN203804615U (en) | Device capable of improving accuracy in perpendicularity of cross-hole drilling | |
| CN203484709U (en) | Special-shaped drill jig tool | |
| CN203245615U (en) | Clamp for machining connecting rod large-end hole and connecting rod small-end hole | |
| CN203765042U (en) | Combined valve cover machining fixture | |
| CN203917519U (en) | Locate fast bending jig group | |
| CN202639419U (en) | Fast clamping device of drill jig | |
| CN201776640U (en) | Fixture for hole drilling of workpieces | |
| CN202498324U (en) | Welding device for tower body standard knot steps | |
| CN203484714U (en) | Pump body drill jig | |
| CN202985177U (en) | Fixture for drilling holes on weighing platform sensor fixing plate | |
| CN202825294U (en) | Punching clamp of flange plate | |
| CN102873554A (en) | Punching clamp for flange plate | |
| CN203804600U (en) | Cylindrical pin drilling device | |
| CN201736134U (en) | Clamping device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20140122 Termination date: 20140820 |
|
| EXPY | Termination of patent right or utility model |