CN203364809U - Flatness and parallelism measuring apparatus - Google Patents
Flatness and parallelism measuring apparatus Download PDFInfo
- Publication number
- CN203364809U CN203364809U CN 201320427331 CN201320427331U CN203364809U CN 203364809 U CN203364809 U CN 203364809U CN 201320427331 CN201320427331 CN 201320427331 CN 201320427331 U CN201320427331 U CN 201320427331U CN 203364809 U CN203364809 U CN 203364809U
- Authority
- CN
- China
- Prior art keywords
- measurement
- hole
- parallelism
- push rod
- flatness
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000005259 measurement Methods 0.000 claims abstract description 121
- 238000006073 displacement reaction Methods 0.000 claims abstract description 89
- NJPPVKZQTLUDBO-UHFFFAOYSA-N novaluron Chemical compound C1=C(Cl)C(OC(F)(F)C(OC(F)(F)F)F)=CC=C1NC(=O)NC(=O)C1=C(F)C=CC=C1F NJPPVKZQTLUDBO-UHFFFAOYSA-N 0.000 claims description 46
- 230000001105 regulatory effect Effects 0.000 claims description 6
- 238000000034 method Methods 0.000 abstract description 13
- 230000007246 mechanism Effects 0.000 description 10
- 238000003825 pressing Methods 0.000 description 10
- 238000013016 damping Methods 0.000 description 5
- 230000000694 effects Effects 0.000 description 5
- 238000004519 manufacturing process Methods 0.000 description 5
- 239000000758 substrate Substances 0.000 description 5
- 239000011148 porous material Substances 0.000 description 3
- 238000004364 calculation method Methods 0.000 description 2
- 238000001514 detection method Methods 0.000 description 2
- 230000006978 adaptation Effects 0.000 description 1
- 230000003044 adaptive effect Effects 0.000 description 1
- 230000003139 buffering effect Effects 0.000 description 1
- 238000007599 discharging Methods 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 239000012467 final product Substances 0.000 description 1
- 238000007667 floating Methods 0.000 description 1
- 238000000691 measurement method Methods 0.000 description 1
Images



Landscapes
- A Measuring Device Byusing Mechanical Method (AREA)
Abstract
The utility model discloses a flatness and parallelism measuring apparatus which comprises a workbench top, a lower measuring seat arranged on the workbench top and vertical slide rails at both sides of the lower measuring seat. An upper measuring seat is arranged above the lower measuring seat to form a vertical sliding connection with the vertical slide rails. The upper and lower measuring seat are respectively provided with a plurality of first displacement sensors and second displacement sensors in annular equilibrium distribution about a same vertical central shaft. During a measurement process, the first displacement sensors and second displacement sensors are set to zero with a standard calibration block at first, and the coordinate figure of measurement points of a workpiece can be measured. A data process system can be fitted to obtain the reference planes of upper and lower measured surfaces, and then calculates the flatness error of the upper and lower measured surfaces, and parallelism error of the upper measured surface with respect to the lower measured surface. The flatness and parallelism measuring apparatus can measure flatness and parallelism at the same time, and is rapid in measuring process, high in measuring precision, and suitable for on-line measurement.
Description
Technical field
The utility model relates to field of measuring technique, especially relates to a kind of measurement mechanism for measurement plane degree and the depth of parallelism, and its oil cooler be applicable to having upper and lower two annular planes carries out the measurement of flatness and the depth of parallelism.
Background technology
Some workpiece higher to shape need have the tolerance of flatness and the depth of parallelism usually; although can be measured flatness and two plane-parallel depth of parallelisms of single plane by three-coordinates measuring machine or relevant special measurement instrument; but because there are the problem expensive, that process of measurement is complicated in the said equipment and instrument; thereby can't in commercial production, obtain general application; especially be not suitable for the quick online detection on production line, and be difficult to measure flatness and the depth of parallelism on two planes simultaneously.Usually, people still utilize some simple survey instruments and measure flatness and the depth of parallelism that frock is measured specific workpiece.For example, on Chinese patent literature disclosed a kind of " measurement mechanism and the measuring method of the cage guide side workplace depth of parallelism ", notification number is CN102661703A, this measurement mechanism comprises and can be fixed on guide rail or the support that can dismantle from guide rail, be fixed on the measurement plate on support, offer at least two spaced sample holes on the surface of measurement plate, when support is fixed on guide rail, the straight line at place, sample hole is parallel with the side workplace of guide rail.While measuring the paired rail-sides workplace depth of parallelism, two measurement mechanisms of mirror image symmetry are fixed on to the same level position of paired guide rail, the side workplace of one of them guide rail of take is reference field, measure the distance of place, the corresponding measurement mechanism loading hole of a guide rail, two sample holes to a straight line on the corresponding measurement mechanism of another guide rail, according to the length of rail-sides workplace horizontal direction, can measure the depth of parallelism of paired rail-sides workplace again.Above-mentioned measurement mechanism is conducive to measure the depth of parallelism between two planes separated by a distance, but still there are the following problems: at first it can't measure the flatness of correlation plane when measuring the depth of parallelism, secondly, when the depth of parallelism of measuring between two planes, it does not consider the flatness error on each plane itself, thereby the accuracy of its measurement result and measuring accuracy are restricted.
The utility model content
The purpose of this utility model is in order to overcome existing measurement plane degree and the depth of parallelism simultaneously of being difficult to of existing measurement mechanism, thereby the process of measurement complexity is not suitable for on-line measurement, and the low problem of precision of measuring the depth of parallelism, a kind of flatness and parallelism measuring apparatus and corresponding measuring method are provided, it is applicable to measure the workpiece that oil cooler and so on has upper and lower two coaxial annular planes, can measure upper and lower two parallel planes flatness separately and the depth of parallelism each other simultaneously, and process of measurement is quick, the measuring accuracy of the depth of parallelism is high, thereby be applicable to on-line measurement.
To achieve these goals, the utility model is by the following technical solutions: a kind of flatness and parallelism measuring apparatus, comprise measurement component and there is the data handling system of display terminal, described measurement component comprises a work top, the upright slide rail that work top is provided with lower measuring seat and is positioned at lower measuring seat both sides, be provided with above lower measuring seat with upright slide rail and form and slide up and down the upper measuring seat be connected, on described, on lower measuring seat, be respectively equipped with some around same vertical around central shaft decile is arranged ringwise the first displacement transducer and second displacement sensor, first, the signal output part of second displacement sensor is connected with the signal input part of data handling system.
The utility model adopts the height coordinate of each measurement point on the measurement face up and down of a plurality of the first displacement transducers and second displacement sensor measuring workpieces, thereby can obtain the volume coordinate of each measurement point, utilize existing Three-dimensional Design Software, above-mentioned discrete point coordinate can be simulated to upper and lower two reference planes, and then can obtain measuring up and down face flatness separately and the depth of parallelism each other.Because the DATA REASONING of each measurement point is disposablely to complete simultaneously, and measurement data can automatically process and be exported by data handling system, thereby can realize the on-line measurement of flatness and the depth of parallelism.Particularly, in the measurement of paralleism, the tested plane of workpiece should be to make comparisons with the depth of parallelism reference field of workpiece, because the depth of parallelism reference field of workpiece itself inevitably has flatness error, thereby we need to be measured and obtain its theoretical principle plane the depth of parallelism reference field of workpiece, then use the measurement of paralleism benchmark of this theoretical principle plane as the tested plane of workpiece.Yet in existing parallelism measurement method, the lower surface of workpiece normally is placed on as depth of parallelism reference field on the reference measurement platform of a level, upper surface by measuring workpieces is that a plurality of measurement points on detection plane obtain its corresponding parallelism error, owing to can't tested plane and the depth of parallelism reference field of workpiece be measured simultaneously, therefore can't obtain the theoretical principle plane of depth of parallelism reference field, and then to be difficult to avoid the lower surface of workpiece be the impact of the flatness error of depth of parallelism reference field on measurement of paralleism accuracy and precision itself.The utility model is distinguished depth of parallelism reference field and the tested plane of measuring workpieces simultaneously with upper and lower two group of first displacement transducer and second displacement sensor, and simulate reference plane separately, the error that both can be used for the Calculation Plane degree, can be used for again calculating the error of the depth of parallelism, thereby effectively improved the utilization ratio of data acquisition, and be conducive to improve the speed that data are processed, make it can be applicable to detecting online fast.
As preferably, described lower measuring seat comprises the lower measurement pedestal be fixed on work top, be arranged on the lower measurement platen on lower measurement pedestal, in the middle of lower measurement pedestal, have with coaxial around central shaft under dodge circular hole, on lower measurement pedestal around under dodge circular hole and be provided with equally spacedly some lower adjusting chutes radially, each time regulated in chute and all is provided with slidably lower adjusting slider, each second displacement sensor is dodged the inner of circular hole under being fixed on correspondingly on each time adjusting slider and being positioned at, on lower measurement platen, the position of corresponding second displacement sensor is provided with adjusting slotted hole radially, the contact of second displacement sensor upper end upwards passes the adjusting slotted hole, work top is provided with and the coaxial and lower push rod moving up and down around central shaft, it is conical that the upper end of lower push rod is, correspondingly, the inner face of lower adjusting slider is the inclined-plane of being close to the lower push rod conical end, also be provided with spring-housing groove longitudinally on lower adjusting slider, the block that laterally is provided with stage clip in spring-housing groove and is fixedly connected with lower measurement pedestal, the outer end of stage clip is against block, the inner of stage clip is against the spring-housing groove side.
Second displacement sensor of the present utility model adopts the adjustable floating structure in position, when moving up lower push rod, the conical upper end of lower push rod can make each time adjusting slider synchronously outwards mobile fast along the lower adjusting chute of level, and the displacement of each time adjusting slider is identical.On the contrary, when moving down lower push rod, each time adjusting slider can rely on the elastic force of stage clip synchronously to move at fast outside center along lower adjusting chute, thereby can adapt to the measurement of the oil cooler of different model, and improves the accuracy of measuring.Because the contact of second displacement sensor upper end upwards passes the adjusting slotted hole on lower measurement platen, thereby can guarantee that workpiece can compress the contact of second displacement sensor upper end while being placed on lower measurement platen reliably.In addition, lower measuring seat adopts fabricated structure, both convenient lower processing and manufacturings of regulating chute, simultaneously can be by reasonably design, make lower adjusting slider in height with lower adjusting chute, form interference fit, like this, under the needs adjustment during position of adjusting slider, can first suitably become flexible the lower platen of measuring, instantly after adjusting slider is adjusted to the right place, can lower measurement platen is fastening, thereby avoid because of lower adjusting slider the loosening slight swing that affects the second displacement sensor be arranged on lower adjusting slider in lower adjusting chute, with accuracy and the consistance of guaranteeing measurement data.
As preferably, be provided with under being positioned at the lower push rod guide holder of dodging circular hole above described work top, the lower push rod guide holder is provided with vertical pilot hole, the side of pilot hole at least comprises a perpendicular, the lower end of lower push rod and pilot hole are suitable and form upper and lower being slidably connected with pilot hole, be provided with support below work top, be articulated with horizontal lower dolly bar on support, the outer end of lower dolly bar arranges the handle with index dial, the inner of lower dolly bar is provided with driving bevel gear, be articulated with vertical lower driving stem below work top, the lower surface of lower push rod is provided with threaded hole, the upper end of lower driving stem is threaded in the threaded hole of lower push rod, the lower end of lower driving stem is provided with the driven bevel pinion with the driving bevel gear engagement.
Because lower push rod is slidably connected on the lower push rod guide holder, therefore, when turning handle, lower dolly bar can pass through driving bevel gear, driven bevel pinion drives lower driving stem and rotates, move up and down along the lower push rod guide holder thereby drive the lower push rod be threaded with lower driving stem, and then realize the position adjustments to lower adjusting slider and second displacement sensor.Be arranged on the control of the convenient position adjustments to lower adjusting slider and second displacement sensor of index dial on lower dolly bar.
As preferably, described lower measurement platen upper surface is provided with three arc brace rod sheets of arranging at circumferencial direction etc. minute centered by around central shaft, is provided with circular elastic press in the middle of the lower surface of upper measuring seat.
Three arc brace rod sheets are supporting workpiece firmly both, can reduce again the contact area of lower measurement platen and workpiece, is conducive to improve the flatness precision of the surface of contact of lower measurement platen and workpiece, facilitates its processing.And be arranged on when elastic press in the middle of measuring seat both had been conducive to measuring seat and moves down, Work-sheet pressing is fixed, can be avoided and the first displacement transducer produces and interferes simultaneously.
As preferably, described upper measuring seat comprises the upper measurement pedestal be slidably connected on upright slide rail, be arranged on the door shape adjustment rack above the measurement pedestal, in the middle of upper measurement pedestal, have with coaxial around central shaft on dodge circular hole, be provided with equally spacedly some adjusted chutes radially around above dodging circular hole on upper measurement pedestal, all be provided with slidably the adjusted slide block in each adjusted chute, each first displacement transducer is fixed on correspondingly on each adjusted slide block and is positioned at the inner of dodging circular hole, the contact of the first displacement transducer lower end passes downwards dodges circular hole, door shape adjustment rack is provided with and the coaxial and upper ejector pin moving up and down around central shaft, it is conical that the bottom of upper ejector pin is, correspondingly, the inner face of adjusted slide block is the inclined-plane of being close to the upper ejector pin conical end, also be provided with spring-housing groove longitudinally on the adjusted slide block, the block that laterally is provided with stage clip in spring-housing groove and is fixedly connected with upper measurement pedestal, the outer end of stage clip is against block, the inner of stage clip is against the spring-housing groove side.
The mount fixing structure of the mount fixing structure of the first displacement transducer of the present utility model and second displacement sensor is basic identical, thereby can adapt to the measurement of the oil cooler of different model, and improves the accuracy of measuring.
As preferably, the centre of described door shape adjustment rack is provided with the upper ejector pin guide holder, the upper ejector pin guide holder is provided with vertical pilot hole, the side of pilot hole at least comprises a perpendicular, the upper end of upper ejector pin and pilot hole are suitable and form upper and lower being slidably connected with pilot hole, be provided with fixed mount above door shape adjustment rack, the lateral part of the clamping back-up block of one T font flatly is fixedly connected on the sidewall of fixed mount, the middle part that clamps the longitudinal component of back-up block level is provided with holes for clamping, be articulated with vertical upper driving stem in holes for clamping, the end face that clamps the back-up block longitudinal component is provided with the adjustment gap that extends to holes for clamping, the clamping back-up block is positioned at the two side portions of adjusting gap and is respectively equipped with locking screw holes and through hole, one lock-screw is connected on locking screw holes through through hole whorl, the upper surface of upper ejector pin is provided with threaded hole, the lower end of upper driving stem is threaded in the threaded hole of upper ejector pin.
When rotating upper driving stem, can drive upper ejector pin along the oscilaltion of upper ejector pin guide holder, and then realize the position adjustments to adjusted slide block and the first displacement transducer.Lock-screw can make to clamp back-up block and clamp and pin driving stem, thereby guarantees that the position of the first displacement transducer fixes.
Therefore, the utility model is applicable to measure the workpiece that oil cooler and so on has upper and lower two coaxial annular planes, can measure upper and lower two parallel planes flatness separately and the depth of parallelism each other simultaneously, and process of measurement is quick, the measuring accuracy of the depth of parallelism is high, thereby is applicable to on-line measurement.
The accompanying drawing explanation
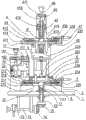
Fig. 1 is a kind of structural representation of the present utility model.
Fig. 2 is a kind of cut-open view of the present utility model.
Fig. 3 is a kind of structural representation of pedestal.
Fig. 4 is a kind of structural representation of lower adjusting slider.
Fig. 5 is a kind of structural representation of bounce cylinder.
In figure: 1, work top 11, lower push rod guide holder 111, pilot hole 12, support 13, lower dolly bar 14, driving bevel gear 15, driven bevel pinion 16, limiting bracket 161, stop screw 162, set nut 17 bounce cylinders 171, buffer head 172, back-moving spring 173, damping pore 18, lower driving stem 2, lower measuring seat 21, lower measurement pedestal 211, pedestal 212, pressing plate 213, under dodge circular hole 214, lower adjusting chute 22, lower measurement platen 221, regulate slotted hole 222, arc brace rod sheet 223, tommy 224, locating piece 23, lower adjusting slider 231, rectangular recess 232, rubber cushion blocks 233, friction disc 234, spring-housing groove 235, block 236, stage clip 24, drive cylinder 3, upright slide rail 4, upper measuring seat 41, upper measurement pedestal 411, substrate 412, cover plate 413, on dodge circular hole 414, adjusted chute 415, upper ejector pin guide holder 416, fixed mount 417, clamp back-up block 418, holes for clamping 419, adjust gap 42, door shape adjustment rack 43, adjusted slide block 44, lock-screw 45, elastic press 46, upper driving stem 5, the first displacement transducer 6, second displacement sensor 7, triple motion sensor 8, lower push rod 9, upper ejector pin.
Embodiment
Below in conjunction with accompanying drawing and embodiment, the utility model is further described.
As Fig. 1, a kind of flatness and parallelism measuring apparatus shown in Fig. 2, it adopts displacement transducer oil cooler one class to be had to being measured of workpiece on upper and lower two coaxial annular planes, specifically comprise measurement component and there is the data handling system of display terminal, described measurement component comprises a work top 1, work top is arranged on a frame, lower measuring seat 2 is set on work top, and the upright slide rail 3 be fixedly connected with work top is set in lower measuring seat both sides, arrange with upright slide rail and form and slide up and down the upper measuring seat 4 be connected above lower measuring seat.The lower measuring seat be arranged on work top comprises a lower measurement pedestal 21 be fixed on work top, is fixedly connected with lower measurement platen 22 on lower measurement pedestal, with for placing the workpiece of measurement.Lower measurement pedestal adopts fabricated structure, comprises the pedestal 211 be fixedly connected with work top and is connected by screw the pressing plate 212 at pedestal upper surface, in the middle of lower measurement pedestal, arrange connect pedestal and pressing plate under dodge circular hole 213.In addition, the pedestal upper surface of lower measurement pedestal around under dodge circular hole and be provided with equally spacedly some lower adjusting chutes 214 radially, the U-shaped groove that lower adjusting chute is upper opening, and dodge circular hole under connecting, so that its processing and manufacturing, cover pressing plate on pedestal after, lower adjusting chute forms the rectangular channel of opening closure.Each time regulated in chute lower adjusting slider 23 all is set slidably, the inner of lower adjusting slider is stretched out lower adjusting chute and is dodged circular hole under being positioned at, the inner of dodging circular hole under each time adjusting slider is positioned at is fixedly installed second displacement sensor 6, the signal output part of second displacement sensor is connected with the signal input part of data handling system, thereby make the second displacement sensor do movement radially along with lower adjusting slider, to adapt to the measurement needs of different size workpiece.
In order to improve measuring accuracy, lower adjusting slider and lower adjusting chute can form interference fit in short transverse, like this, when needs are adjusted the position of second displacement sensor, can first unclamp the pressing plate on pedestal, so that the movement of lower adjusting slider, after the second displacement sensor is adjusted to the right place, tightening up pressing plate can be fixed lower adjusting slider, thereby can avoid lower adjusting slider to swing at the trace of vertical direction, is conducive to improve measuring accuracy.Perhaps, as shown in Figure 4, also two rectangular recess 231 can be set in the upper surface rear and front end of lower adjusting slider, rubber cushion blocks 232 is set in rectangular recess, and on the surface of rubber cushion blocks, the friction disc 233 that exceeds lower adjusting slider upper surface is set, like this, when adjusting slider is installed in lower adjusting chute instantly, rubber cushion blocks can make fit the tightly end face of lower adjusting chute of friction disc, avoids the loosening of lower adjusting slider, simultaneously the convenient lower movement of adjusting slider when not unclamping pressing plate.The second displacement sensor can adopt the spring linear displacement transducer, like this, after the workpiece of measuring is removed, the second displacement sensor can automatically reset, in order to next workpiece is measured, certainly, the contact of second displacement sensor should arrange upward, thereby can be measured the lower measurement face of workpiece.The position that is fixed on corresponding second displacement sensor on the lower measurement platen on pressing plate need arrange regulates slotted hole 221, so that the contact of second displacement sensor upper end upwards passes the adjusting slotted hole, guarantee that the lower measurement face of workpiece contacts with the contact of second displacement sensor.Certainly, regulating slotted hole need to radially arrange, so that the second displacement sensor is done movement radially.
With the similar ground of lower measuring seat, also need to arrange corresponding displacement transducer on upper measuring seat, in order to the upper measurement face of workpiece is measured.Particularly, upper measuring seat comprises and is slidably connected at the upper measurement pedestal 41 on upright slide rail and is arranged on the door shape adjustment rack 42 above the measurement pedestal, upper measurement pedestal adopts fabricated structure equally, it comprises the substrate 411 be slidably connected with upright slide rail and is connected by screw the cover plate 412 at upper surface of base plate, in the middle of upper measurement pedestal, arrange with under dodge circular hole coaxial and perforation substrate and cover plate on dodge circular hole 413.In addition, the upper surface of base plate of upper measurement pedestal around on dodge circular hole some adjusted chutes 414 radially be set equally spacedly, the U-shaped groove that the adjusted chute is upper opening, and dodge circular hole on connecting, so that its processing and manufacturing, cover cover plate on substrate after, the adjusted chute forms the rectangular channel of opening closure.All be provided with slidably adjusted slide block 43 in each adjusted chute, the inner of adjusted slide block is stretched out the adjusted chute and is positioned at and dodges circular hole, be positioned at the inner of dodging circular hole at each adjusted slide block and be fixedly installed the first displacement transducer 5, the signal output part of the first displacement transducer is connected with the signal input part of data handling system, thereby make the first displacement transducer and second displacement sensor around same vertical around central shaft ringwise decile arrange, and the first displacement transducer can be done movement radially along with the adjusted slide block, to adapt to the measurement needs of different size workpiece.
Be understandable that, with the similar ground of lower adjusting slider, adjusted slide block and adjusted chute also can form interference fit in short transverse, to avoid the adjusted slide block, at the trace of vertical direction, swing.Perhaps, also can be embedded in the lower surface rear and front end of adjusted slide block two rubber cushion blocks, and on the surface of rubber cushion blocks, the friction disc that exceeds lower adjusting slider lower surface is set.And the first displacement transducer adopts the spring linear displacement transducer equally, and the contact of the first displacement transducer should arrange down, and the contact of the first displacement transducer lower end should pass downwards and dodge circular hole, in order to the upper measurement face of workpiece is measured.
In order to adjust the position of second displacement sensor, as shown in Figure 2, under being positioned at, the top setting of work top dodges the lower push rod guide holder 11 of circular hole, the lower push rod guide holder is provided with vertical pilot hole 111, certainly, pilot hole should with under to dodge circular hole coaxial, the side of pilot hole comprises a perpendicular, thereby make pilot hole become the major arc hole, perhaps pilot hole also can arrange two parallel perpendiculars, certainly, pilot hole also can adopt the regular polygon hole, the lower end of one lower push rod 8 and pilot hole are suitable and form upper and lower being slidably connected with pilot hole, thereby make lower push rod with coaxial around central shaft, and can avoid the rotation of lower push rod.It is conical that the upper end of lower push rod is, and correspondingly, the inner face of lower adjusting slider is the inclined-plane of being close to the lower push rod conical end, and like this, when lower push rod rises, can promote lower adjusting slider and outwards move, thus the position of adjustment second displacement sensor.In addition, we also need arrange spring-housing groove 234 longitudinally on lower adjusting slider, and place, corresponding spring-housing groove outer end is fixedly connected with a block 235 on the pedestal of lower measurement pedestal, a stage clip 236 of laterally placing is set in spring-housing groove, the outer end of stage clip is against block, the inner of stage clip is against the spring-housing groove side, thereby makes the inner of lower adjusting slider be close to the upper end of lower push rod.When lower push rod moves down, lower adjusting slider moves in can be under the effect of stage clip.
In order to drive the lower push rod lifting, we can arrange support 12 below work top, horizontal lower dolly bar 13 of pivot joint on support, the outer end of lower dolly bar is provided with the handle of index dial, the inner of lower dolly bar arranges driving bevel gear 14, vertical lower driving stem 18 of the following pivot joint of work top, the driven bevel pinion 15 that the lower end of lower driving stem arranges and driving bevel gear meshes.In addition, on the lower surface of lower push rod, threaded hole is set, the upper end of lower driving stem is threaded in the threaded hole of lower push rod.Like this, when by handle, rotating lower dolly bar, can pass through driving bevel gear, the lower driving stem rotation of driven bevel pinion driving, because can't rotating, lower push rod can only move up and down along the pilot hole of lower push rod guide holder, therefore lower driving stem can drive the lower push rod oscilaltion by the effect of screw thread, and then drive second displacement sensor is done movement radially.Index dial can show the corresponding displacement of second displacement sensor, certainly, we also can on lower measurement pedestal, be positioned at one of them lower adjusting slider side place be provided for measuring under adjusting slider move radially the triple motion sensor 7 of distance, thereby the displacement of lower adjusting slider can be sent to data handling system, be convenient to data handling system and determine rapidly and accurately the planimetric coordinates value after second displacement sensor position is adjusted.
Further, in order to adjust the position of the first displacement transducer, we need to arrange upper ejector pin guide holder 415 in the centre of door shape adjustment rack, the upper ejector pin guide holder is provided with vertical pilot hole, the upper end of one upper ejector pin 9 and pilot hole are suitable and form upper and lower being slidably connected with pilot hole, thereby make upper ejector pin with coaxial around central shaft, and can avoid the rotation of upper ejector pin.It is conical that the bottom of upper ejector pin is, and correspondingly, the inner face of adjusted slide block is the inclined-plane of being close to the upper ejector pin conical end, like this, when upper ejector pin descends, can promote the adjusted slide block and outwards move, thereby adjust the position of the first displacement transducer.In addition, with the similar ground of lower adjusting slider, also need to arrange spring-housing groove 234 longitudinally on the adjusted slide block, and place, corresponding spring-housing groove outer end is fixedly connected with a block 235 on the substrate of upper measuring seat, the stage clip 236 of horizontal placement is set in spring-housing groove, the outer end of stage clip is against block, and the inner of stage clip is against the spring-housing groove side.Thereby the lower end of upper ejector pin is close in the inner that makes the adjusted slide block.When upper ejector pin moves up, the adjusted slide block moves in can be under the effect of stage clip.
In order to drive the upper ejector pin lifting, as Fig. 1, shown in Fig. 2, we can set firmly a fixed mount 416 on door shape adjustment rack, the lateral part of the clamping back-up block 417 of a T font flatly is fixedly connected on the sidewall of fixed mount, the middle part that clamps the longitudinal component of back-up block level arranges holes for clamping 418, be articulated with vertical upper driving stem 46 in holes for clamping, the end face that clamps the back-up block longitudinal component is provided with the adjustment gap 419 that extends to holes for clamping, the clamping back-up block is positioned at a side of adjusting gap a locking screw holes is set, be positioned at the clamping back-up block opposite side of adjusting gap simultaneously coaxial through hole is set, one lock-screw 44 is connected on locking screw holes through the through hole rear thread, on the upper surface of upper ejector pin, threaded hole is set, the lower end of upper driving stem is threaded in the threaded hole of upper ejector pin.Like this, when we need to adjust the position of the first displacement transducer, rotatably go up driving stem and move up and down to drive upper ejector pin, and then the adjusted slide block is moved radially.When the first displacement transducer is adjusted to the right place, tighten lock-screw and can make the holes for clamping that clamps back-up block clamp upper driving stem, thereby avoid the rotation of driving stem.Certainly, we can arrange at the afterbody of lock-screw a handle, to facilitate the rotation of lock-screw, and upper driving stem passes the upper end of holes for clamping, a handle with index dial also can be set, with the rotation that facilitates upper driving stem and the control of adjustment amount.
Further, we also can arrange at the upper surface of lower measurement platen three arc brace rod sheets 222 of arranging at circumferencial direction etc. minute centered by around central shaft, arc brace rod sheet should be lower than the contact of second displacement sensor, so that workpiece can compress the contact of second displacement sensor when supporting workpiece, and, also can arrange at the center of lower measurement platen adaptive with the center pit of workpiece lower surface and with the tommy 223 coaxial around central shaft, a side at lower measurement platen arranges locating piece 224 simultaneously, in order to workpiece is positioned, guarantee the consistance of measuring.Meanwhile, in the middle of the lower surface of upper measuring seat, circular elastic press 45 is set, when upper measuring seat moves down, but the elastic press workpiece pressing is avoided the mobile measuring error that produces because of workpiece.
Be understandable that, we also can be positioned at lower measuring seat two side positions a driving cylinder 24 is set respectively on work top, drive the piston rod of cylinder to be connected with the upper measurement pedestal of upper measuring seat, so that control the lifting of upper measuring seat.And also need to arrange corresponding position-limit mechanism on work top, so that the descending stroke of measuring seat in control, position-limit mechanism comprises the limiting bracket 16 be fixed on work top, a vertical stop screw 161 is threaded on limiting bracket, set nut 162 also has been threaded on stop screw, a vertical bounce cylinder 17 also is set on limiting bracket, the piston rod end that bounce cylinder makes progress is provided with the buffer head 171 that rubber is made, and the height of buffer head will be higher than the screw head above stop screw.As shown in Figure 5, the cavity that is positioned at the piston bottom in the cylinder body of bounce cylinder is provided with back-moving spring 172, and in the bottom surface of cylinder body, damping pore 173 is set.Like this, when upper measuring seat moves down under the promotion of driving cylinder, at first upper measurement pedestal on upper measuring seat contacts the buffer head on bounce cylinder, now, back-moving spring in bounce cylinder plays the buffer damping effect on the one hand, on the other hand, because the aperture of the damping pore on cylinder body is very little, therefore, air in the inferior part of the cylinder block cavity is compressed because not discharging fast, thereby further play the effect of buffering and damping, until upper measurement pedestal touches the head of screw above stop screw.When upper measuring seat rises, back-moving spring can promote to move on the piston of bounce cylinder, thereby makes buffer head be up to original position.Be screwed into the descending stroke that the degree of depth is measuring seat on capable of regulating by adjusting stop screw on limiting bracket, set nut can be locked limitation locking, avoids it to rotate voluntarily.
The utility model also needs to make in addition a standard check block when measurement plane degree and the depth of parallelism, this standard check block is cylindrical, its size that highly reaches upper and lower two calibration plane is identical with tested workpiece, pilot hole with the tommy adaptation of lower measurement platen center is set on lower calibration plane simultaneously, certainly, two calibration plane up and down of standard check block should have high flatness and the depth of parallelism, the error of its flatness and the depth of parallelism should be less than the flatness of workpiece and 0.2 times of parallelism tolerance, and concrete measuring process is as follows:
1. first the standard check block is placed on lower measuring seat, then start and drive cylinder, the upper measuring seat of lower measuring seat top is moved down, now, be arranged on, on lower measuring seat first, the contact of second displacement sensor compresses two calibration plane up and down of standard check block, data handling system can receive each first, first group of displacement signal value in short transverse that the second displacement sensor is sent, upper measuring seat then moves up, by the standard check block around rotate the angle of a setting around central shaft, and then move down measuring seat, thereby obtain the displacement signal value of second group of short transverse, by that analogy, when the standard check block after around central shaft, rotating N time, data handling system obtains the displacement signal value of N+1 group short transverse altogether, finally, data handling system by each first, the mean value of the N+1 of second displacement sensor displacement signal value is set as the null value of height coordinate, thereby unified first, the measuring basis of second displacement sensor.It should be noted that, the standard check block at every turn around the angle of rotating around central shaft preferably should and adjacent first, second displacement transducer between corresponding central angle equate, that is to say, the number of first, second displacement transducer should be N+1, like this, the standard check block is at every turn around the angle A of rotating around central shaft=360 °/(N+1).In the utility model, the quantity of first, second displacement transducer is preferably 6 or 8, and like this, number of revolutions N is 5 or 7, and the standard check block equals 60 degree or 45 degree around the angle A of rotating around central shaft at every turn;
2. workpiece is lain on lower measuring seat, the center pit of workpiece lower surface is positioned on the tommy of lower measuring seat, locating piece on lower measuring seat limits workpiece and avoids its rotation, then drive measuring seat on air cylinder driven to move down, now, first, second displacement transducer can measure that on the upper and lower measurement plane of workpiece, each measurement point is at the coordinate figure of short transverse, and data handling system can obtain the spatial value of each measurement point according to each first, second displacement transducer position coordinates in surface level of input in advance;
3. data handling system, according to the spatial value of each measurement point on the upper and lower measurement face of workpiece, gets final product the reference plane that matching obtains upper and lower measurement face.It should be noted that, by the discrete point in space, by least square fitting, must belong to prior art to plane, all there is this calculation procedure in existing 3D sculpting software, be not described in detail at this;
4. first calculate respectively each measurement point on the upper and lower measurement face of workpiece and arrive the offset distance between its corresponding reference plane, can obtain upper and lower measurement face flatness error value separately, calculate again the reference point of corresponding each first displacement transducer horizontal level on the upper corresponding reference plane of measurement face to the distance between the corresponding reference plane of lower measurement face, the maximal value of this distance is deducted to minimum value and can obtain the parallelism error value that upper measurement face descends measurement face relatively.
Claims (6)
1. a flatness and parallelism measuring apparatus, comprise measurement component and there is the data handling system of display terminal, it is characterized in that, described measurement component comprises a work top, the upright slide rail that work top is provided with lower measuring seat and is positioned at lower measuring seat both sides, be provided with above lower measuring seat with upright slide rail and form and slide up and down the upper measuring seat be connected, on described, on lower measuring seat, be respectively equipped with some around same vertical around central shaft decile is arranged ringwise the first displacement transducer and second displacement sensor, first, the signal output part of second displacement sensor is connected with the signal input part of data handling system.
2. a kind of flatness according to claim 1 and parallelism measuring apparatus, it is characterized in that, described lower measuring seat comprises the lower measurement pedestal be fixed on work top, be arranged on the lower measurement platen on lower measurement pedestal, in the middle of lower measurement pedestal, have with coaxial around central shaft under dodge circular hole, on lower measurement pedestal around under dodge circular hole and be provided with equally spacedly some lower adjusting chutes radially, each time regulated in chute and all is provided with slidably lower adjusting slider, each second displacement sensor is dodged the inner of circular hole under being fixed on correspondingly on each time adjusting slider and being positioned at, on lower measurement platen, the position of corresponding second displacement sensor is provided with adjusting slotted hole radially, the contact of second displacement sensor upper end upwards passes the adjusting slotted hole, work top is provided with and the coaxial and lower push rod moving up and down around central shaft, it is conical that the upper end of lower push rod is, correspondingly, the inner face of lower adjusting slider is the inclined-plane of being close to the lower push rod conical end, also be provided with spring-housing groove longitudinally on lower adjusting slider, the block that laterally is provided with stage clip in spring-housing groove and is fixedly connected with lower measurement pedestal, the outer end of stage clip is against block, the inner of stage clip is against the spring-housing groove side.
3. a kind of flatness according to claim 2 and parallelism measuring apparatus, it is characterized in that, be provided with under being positioned at the lower push rod guide holder of dodging circular hole above described work top, the lower push rod guide holder is provided with vertical pilot hole, the side of pilot hole at least comprises a perpendicular, the lower end of lower push rod and pilot hole are suitable and form upper and lower being slidably connected with pilot hole, be provided with support below work top, be articulated with horizontal lower dolly bar on support, the outer end of lower dolly bar arranges the handle with index dial, the inner of lower dolly bar is provided with driving bevel gear, be articulated with vertical lower driving stem below work top, the lower surface of lower push rod is provided with threaded hole, the upper end of lower driving stem is threaded in the threaded hole of lower push rod, the lower end of lower driving stem is provided with the driven bevel pinion with the driving bevel gear engagement.
4. a kind of flatness according to claim 2 and parallelism measuring apparatus, it is characterized in that, described lower measurement platen upper surface is provided with three arc brace rod sheets of arranging at circumferencial direction etc. minute centered by around central shaft, is provided with circular elastic press in the middle of the lower surface of upper measuring seat.
5. according to claim 1 or 2 or 3 or 4 described a kind of flatness and parallelism measuring apparatus, it is characterized in that, described upper measuring seat comprises the upper measurement pedestal be slidably connected on upright slide rail, be arranged on the door shape adjustment rack above the measurement pedestal, in the middle of upper measurement pedestal, have with coaxial around central shaft on dodge circular hole, be provided with equally spacedly some adjusted chutes radially around above dodging circular hole on upper measurement pedestal, all be provided with slidably the adjusted slide block in each adjusted chute, each first displacement transducer is fixed on correspondingly on each adjusted slide block and is positioned at the inner of dodging circular hole, the contact of the first displacement transducer lower end passes downwards dodges circular hole, door shape adjustment rack is provided with and the coaxial and upper ejector pin moving up and down around central shaft, it is conical that the bottom of upper ejector pin is, correspondingly, the inner face of adjusted slide block is the inclined-plane of being close to the upper ejector pin conical end, also be provided with spring-housing groove longitudinally on the adjusted slide block, the block that laterally is provided with stage clip in spring-housing groove and is fixedly connected with upper measurement pedestal, the outer end of stage clip is against block, the inner of stage clip is against the spring-housing groove side.
6. a kind of flatness according to claim 5 and parallelism measuring apparatus, it is characterized in that, the centre of described door shape adjustment rack is provided with the upper ejector pin guide holder, the upper ejector pin guide holder is provided with vertical pilot hole, the side of pilot hole at least comprises a perpendicular, the upper end of upper ejector pin and pilot hole are suitable and form upper and lower being slidably connected with pilot hole, be provided with fixed mount above door shape adjustment rack, the lateral part of the clamping back-up block of one T font flatly is fixedly connected on the sidewall of fixed mount, the middle part that clamps the longitudinal component of back-up block level is provided with holes for clamping, be articulated with vertical upper driving stem in holes for clamping, the end face that clamps the back-up block longitudinal component is provided with the adjustment gap that extends to holes for clamping, the clamping back-up block is positioned at the two side portions of adjusting gap and is respectively equipped with locking screw holes and through hole, one lock-screw is connected on locking screw holes through through hole whorl, the upper surface of upper ejector pin is provided with threaded hole, the lower end of upper driving stem is threaded in the threaded hole of upper ejector pin.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320427331 CN203364809U (en) | 2013-07-16 | 2013-07-16 | Flatness and parallelism measuring apparatus |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320427331 CN203364809U (en) | 2013-07-16 | 2013-07-16 | Flatness and parallelism measuring apparatus |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203364809U true CN203364809U (en) | 2013-12-25 |
Family
ID=49812557
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201320427331 Expired - Fee Related CN203364809U (en) | 2013-07-16 | 2013-07-16 | Flatness and parallelism measuring apparatus |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203364809U (en) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103411577A (en) * | 2013-07-16 | 2013-11-27 | 宁波北仑宁润机械有限公司 | Flatness and parallelism measurement device and flatness and parallelism measurement method |
| CN104344803A (en) * | 2014-10-11 | 2015-02-11 | 成都道成设备工程有限责任公司 | Flatness detecting device with variable detecting position |
| CN104807417A (en) * | 2015-03-26 | 2015-07-29 | 北京工业大学 | Rapid measurement method for parallelism error of linear guide rails |
| CN104990523A (en) * | 2015-08-03 | 2015-10-21 | 昆山康斯特精密机械有限公司 | Mold floating mechanism in wheel bearing outer ring groove measurement equipment |
| CN107131850A (en) * | 2017-06-26 | 2017-09-05 | 中广核达胜加速器技术有限公司 | A kind of accelerating tube magnet ring parallelism detecting device |
| CN107560587A (en) * | 2017-08-29 | 2018-01-09 | 广州文冲船厂有限责任公司 | A kind of flatness detection method |
| CN110514153A (en) * | 2019-10-14 | 2019-11-29 | 重庆机电智能制造有限公司 | A large-scale part plane detection device |
| CN112091670A (en) * | 2020-09-15 | 2020-12-18 | 苏州市华宏精密铸造有限公司 | Novel machining positioning device |
| CN114593697A (en) * | 2020-12-03 | 2022-06-07 | 汉达精密电子(昆山)有限公司 | A device for detecting product gap and flatness |
| CN120306977A (en) * | 2025-06-12 | 2025-07-15 | 格拉默汽车内饰部件(北京)有限公司 | A kind of automatic assembly device of damper |
-
2013
- 2013-07-16 CN CN 201320427331 patent/CN203364809U/en not_active Expired - Fee Related
Cited By (16)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103411577A (en) * | 2013-07-16 | 2013-11-27 | 宁波北仑宁润机械有限公司 | Flatness and parallelism measurement device and flatness and parallelism measurement method |
| CN103411577B (en) * | 2013-07-16 | 2016-03-09 | 宁波北仑宁润机械有限公司 | A kind of flatness and parallelism measuring apparatus and measuring method |
| CN104344803B (en) * | 2014-10-11 | 2017-12-19 | 成都道成设备工程有限责任公司 | A kind of flatness checking device of variable test position |
| CN104344803A (en) * | 2014-10-11 | 2015-02-11 | 成都道成设备工程有限责任公司 | Flatness detecting device with variable detecting position |
| CN104807417A (en) * | 2015-03-26 | 2015-07-29 | 北京工业大学 | Rapid measurement method for parallelism error of linear guide rails |
| CN104990523B (en) * | 2015-08-03 | 2018-04-27 | 昆山康斯特精密机械有限公司 | Mo(u)ld top half relocation mechanism in hub bearing outer ring channel level measurement device |
| CN104990523A (en) * | 2015-08-03 | 2015-10-21 | 昆山康斯特精密机械有限公司 | Mold floating mechanism in wheel bearing outer ring groove measurement equipment |
| CN107131850A (en) * | 2017-06-26 | 2017-09-05 | 中广核达胜加速器技术有限公司 | A kind of accelerating tube magnet ring parallelism detecting device |
| CN107560587A (en) * | 2017-08-29 | 2018-01-09 | 广州文冲船厂有限责任公司 | A kind of flatness detection method |
| CN107560587B (en) * | 2017-08-29 | 2020-09-01 | 广州文冲船厂有限责任公司 | Flatness detection method |
| CN110514153A (en) * | 2019-10-14 | 2019-11-29 | 重庆机电智能制造有限公司 | A large-scale part plane detection device |
| CN112091670A (en) * | 2020-09-15 | 2020-12-18 | 苏州市华宏精密铸造有限公司 | Novel machining positioning device |
| CN114593697A (en) * | 2020-12-03 | 2022-06-07 | 汉达精密电子(昆山)有限公司 | A device for detecting product gap and flatness |
| CN114593697B (en) * | 2020-12-03 | 2023-07-11 | 汉达精密电子(昆山)有限公司 | Device for detecting gap and flatness of product |
| CN120306977A (en) * | 2025-06-12 | 2025-07-15 | 格拉默汽车内饰部件(北京)有限公司 | A kind of automatic assembly device of damper |
| CN120306977B (en) * | 2025-06-12 | 2025-09-19 | 格拉默汽车内饰部件(北京)有限公司 | Automatic assembly device for damper |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103411577B (en) | A kind of flatness and parallelism measuring apparatus and measuring method | |
| CN107063167B (en) | Fine cutting block-shaped product detection device | |
| CN203772257U (en) | Semi-automatic planeness detection device | |
| CN204228179U (en) | Multi-faceted detection apparatus for adjusting position | |
| CN108592851B (en) | Workpiece symmetry detection tool and detection method | |
| CN110617753A (en) | Novel aperture detection jig, aperture measurement height gauge and detection method thereof | |
| CN205245950U (en) | Height gage | |
| CN104792361A (en) | Cone-cylinder shaped part centroid and centroidal deviation measuring device | |
| CN201463872U (en) | Comprehensive test instrument of parallel and torsion of refrigerator compressor crankshaft | |
| CN208952936U (en) | Flatness detection machine | |
| CN103743328B (en) | Steering nut guide hole position degree detection apparatus | |
| CN201757636U (en) | Workpiece symmetry detection device | |
| CN206095816U (en) | Static side's board method testing arrangement of timber shear modulus | |
| CN214289472U (en) | A equipment for detecting plate warpage | |
| CN212179829U (en) | Device for measuring groove depth by laser | |
| CN203837647U (en) | Improved device for detecting surface of workpiece | |
| CN207751444U (en) | A kind of glass screen height and flatness checking device | |
| CN209416261U (en) | A kind of face recognizing mechanism | |
| CN115847487A (en) | Bionic touch finger friction experiment device | |
| CN202522200U (en) | Rapid high-precision height detector | |
| CN221925068U (en) | A transmission shaft yoke detection tool | |
| CN108405359B (en) | Automatic detector for radial clearance of deep groove ball bearing | |
| CN220062922U (en) | Wire drawing machine roll surface flatness detection device | |
| CN220729118U (en) | Height gauge device capable of being precisely adjusted | |
| CN219977310U (en) | Stamping workpiece roughness check out test set |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CX01 | Expiry of patent term | ||
| CX01 | Expiry of patent term |
Granted publication date: 20131225 |
|
| CU01 | Correction of utility model | ||
| CU01 | Correction of utility model |
Correction item: Termination upon expiration of patent Correct: Revocation of Patent Expiration and Termination False: Expiration and Termination of 39 Volume 3101 Patent on August 1, 2023 Number: 31-01 Volume: 39 |
|
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20131225 |