CN203357689U - Special horizontal double-sided digital-controlled driller with multiple main shafts - Google Patents
Special horizontal double-sided digital-controlled driller with multiple main shafts Download PDFInfo
- Publication number
- CN203357689U CN203357689U CN 201320442102 CN201320442102U CN203357689U CN 203357689 U CN203357689 U CN 203357689U CN 201320442102 CN201320442102 CN 201320442102 CN 201320442102 U CN201320442102 U CN 201320442102U CN 203357689 U CN203357689 U CN 203357689U
- Authority
- CN
- China
- Prior art keywords
- main shafts
- multiaxis
- workpiece
- numerical control
- special horizontal
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000005553 drilling Methods 0.000 claims abstract description 32
- 239000000463 material Substances 0.000 claims abstract description 22
- 238000003825 pressing Methods 0.000 claims abstract description 18
- OKTJSMMVPCPJKN-UHFFFAOYSA-N Carbon Chemical compound [C] OKTJSMMVPCPJKN-UHFFFAOYSA-N 0.000 claims description 11
- 229910002804 graphite Inorganic materials 0.000 claims description 11
- 239000010439 graphite Substances 0.000 claims description 11
- 230000033001 locomotion Effects 0.000 abstract description 3
- 238000010586 diagram Methods 0.000 description 8
- 238000000034 method Methods 0.000 description 6
- 238000005516 engineering process Methods 0.000 description 4
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 4
- 230000008859 change Effects 0.000 description 3
- 238000003754 machining Methods 0.000 description 3
- 230000008569 process Effects 0.000 description 3
- 230000005540 biological transmission Effects 0.000 description 2
- 230000000694 effects Effects 0.000 description 2
- 230000035515 penetration Effects 0.000 description 2
- 239000000126 substance Substances 0.000 description 2
- 230000009471 action Effects 0.000 description 1
- 230000003796 beauty Effects 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 239000000428 dust Substances 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 230000001681 protective effect Effects 0.000 description 1
- 239000002689 soil Substances 0.000 description 1
- 229910001220 stainless steel Inorganic materials 0.000 description 1
- 239000010935 stainless steel Substances 0.000 description 1
- 238000003860 storage Methods 0.000 description 1
- 230000001360 synchronised effect Effects 0.000 description 1
- 230000009466 transformation Effects 0.000 description 1
Images


Landscapes
- Drilling And Boring (AREA)
Abstract
The utility model discloses a special horizontal double-sided digital-controlled driller with multiple main shafts. The driller comprises upright posts, a driller body, a movable working table and an electric system, wherein the upright posts are respectively arranged at the left side and the right side of the driller body; the movable working table which can move in the X direction is arranged between the two upright posts; a rotatable working table with a workpiece positioning tool is arranged on the movable working table; an automatic material pressing device is arranged above the rotatable working table; multi-shaft drilling power heads which can move upwards and downwards along a shaft Z are respectively arranged on the two upright posts; the main shafts of the two multi-shaft drilling power heads move on the same vertical face; the multi-shaft drilling power heads relatively do the motions of feeding and withdrawal in the Y direction and comprise at least two drilling main shafts which are driven by a motor output shaft; a drill bit is arranged on each drilling main shaft. According to the special horizontal double-sided digital-controlled driller, the two multi-shaft drilling power heads work simultaneously and the working efficiency is high, and the rotatable working table can be used for rotating the workpiece at 90 degrees, so that the automation degree is high, the chip removal is smooth, and the working condition environment is improved.
Description
Technical field
The utility model relates to a kind of special purpose machine tool of manufacturing chemical anticorrosion apparatus, particularly a kind of two-sided numerical control drilling machine of horizontal many main shafts that is mainly used in the graphite block boring of heat transmission equipment.
Background technology
Mainly containing of existing chemical machinery industry application used the vertical direction that swing arm is bored to hole, hole by the drilling machine horizontal direction of soil system or transformation.The problems such as these the two kinds of processing modes at first position of workpiece hole are to guarantee by line and two kinds of forms of template, and boring is manual-alignment, artificial feeding, and machining accuracy is low.These years along with the rise of Numeric Control Technology, new technology more and more is employed recently.The utility model patent that the denomination of invention completed in 2012 by the patentee is " three dimensional deep hole numerical control drilling machine ", be that horizontal direction and vertical direction are combined, and workpiece processed simultaneously.Adopt four unit heads processing works simultaneously, improved operating efficiency, cut not freely but this equipment also exists vertical direction boring row, affect working (machining) efficiency, the poor problem of work condition environment.
Summary of the invention
Technical problem to be solved in the utility model is the problem existed for prior art, provides a kind of high efficiency, labor intensity is little, automaticity is high, improve the two-sided numerical control drilling machine of Horizontal multi-shaft of work condition environment.
For solving this technical problem, the utility model provides the many main shafts of a kind of graphite block special horizontal two-sided numerical control drilling machine, comprise column, lathe bed, travelling table and electrical system, the left and right sides of described lathe bed is respectively equipped with column, be provided with the travelling table that can move along directions X between two columns, described travelling table is provided with a rotary table with the workpiece positioning tool, the top of described rotary table is provided with the automatic pressing material device, on described two columns, a set of multiaxis drill unit respectively is installed, described multiaxis drill unit can move up and down along Z axis, the main shaft of two multiaxis drill units moves on same facade, the multiaxis drill unit along the relative feeding of Y-direction with exit.
Described multiaxis drill unit comprises at least 2 drilling main shafts that driven by a motor output shaft, and each drilling main shaft is provided with a drill bit.
Described multiaxis drill unit comprises 2,3 or 3 above drilling main shafts that driven by a motor output shaft.
Described automatic pressing material device is supported by portal frame, is hydraulic pressure material pressing device or Pneumatic material pressing device.
Described workpiece positioning tool refers to as circular, square or rectangular workpiece location.
Two multiaxis drill units are equipped with cutter guide device, described cutter guide device is provided with the pilot hole that the drill bit for the multiaxis drill unit passes through, cutter guide device and multiaxis drill unit are arranged on same slide plate, described cutter guide device is provided with drive unit V, and this drive unit V drives cutter guide device to move up and down and the Y-axis horizontal feed along Z axis together with the multiaxis drill unit on slide plate.
Described electrical system comprises PLC and host computer, and PLC controls each drive unit and multiaxis drill unit, and PLC is connected with host computer.
Beneficial effect: the utility model compared with prior art, adopt seven numerical control axles, two multiaxis drill units and rotary table, two multiaxis drill units are worked simultaneously, and can be to 90 ° of rotations of workpiece, automaticity is high, and row cuts smooth and easy, high efficiency, labor strength is little, is convenient to dust-proof dust-removing, improves work condition environment.
The accompanying drawing explanation
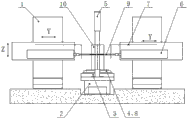
Fig. 1 is structural representation front view of the present utility model;
Fig. 2 is structural representation left view of the present utility model;
Schematic diagram when Fig. 3 a is the utility model processing round piece;
The schematic diagram of workpiece half-twist when Fig. 3 b is the utility model processing round piece;
Schematic diagram when Fig. 4 is the utility model processing box-shaped workpiece;
Schematic diagram when Fig. 5 is the utility model processing pane shape workpiece.
In figure: 1 column, 2 lathe beds, 3 travelling tables, 4 rotary tables, 5 automatic pressing material devices, 6 multiaxis drill units, 7 cutter guide devices, 8 workpiece positioning tools, 9 drill bits, 10 workpiece.
The specific embodiment
Below in conjunction with drawings and Examples, the utility model is done to specific descriptions.
Figure 1 shows that structural representation front view of the present utility model.
Figure 2 shows that structural representation left view of the present utility model.
The utility model column 1, lathe bed 2, travelling table 3, rotary table 4, automatic pressing material device 5, multiaxis drill unit 6, cutter guide device 7, workpiece positioning tool 8, electrical system and pneumatic system.
The left and right sides of described lathe bed 2 is respectively equipped with column 1, is provided with travelling table 3 between two columns 1, and travelling table 3 is arranged on lathe bed 2, and travelling table 3 can move horizontally along X-direction by the drive unit I.
Described drive unit I comprises line slideway, ball screw assembly, and servomotor, line slideway and servomotor are arranged on lathe bed 2, the screw of ball screw assembly, and travelling table 3 fix, the leading screw of ball screw assembly, is connected with the output shaft of servomotor, the driven by servomotor leading screw rotates, thereby drive travelling table 3, on lathe bed 2, moves horizontally.
Described travelling table 3 is provided with the rotary table 4 with workpiece positioning tool 8, for place work piece 10.
Described workpiece positioning tool 8 refers to as circle is square or the rectangular workpiece location.
The top of described rotary table 4 is provided with automatic pressing material device 5 by portal frame, workpiece 10 is carried out to the clamping location and can carry out 90 ° of rotations to workpiece 10, thereby realize the material hole of graphite workpiece 10 and the Drilling operation in water hole.
Described automatic pressing material device 5 is supported by portal frame, is hydraulic pressure material pressing device or Pneumatic material pressing device.
The two ends of described travelling table 3 are equipped with telescopic stainless steel protective cover, can play protection and beauty function.
On described two columns 1, a set of multiaxis drill unit 6 respectively is installed, multiaxis drill unit 6 drives it to move up and down along Z axis by drive unit II,
Described multiaxis drill unit 6 comprises at least 2 drilling main shafts that driven by a motor output shaft, and each drill unit is provided with a drill bit 9, and working (machining) efficiency improves greatly.
Described multiaxis drill unit 6 comprises 2,3 or 3 above drilling main shafts that driven by a motor output shaft, can bore four holes, six holes or eight holes simultaneously, be 1,1.5 or 2 times of four unit heads of prior art numerical control drilling machine, greatly improved operating efficiency.
Described two multiaxis drill unit 6 main shafts move on same facade, but and Y-direction left and right feeding and exiting, drill bit 9 is respectively from the left and right of workpiece 10 towards middle feeding, will expect that hole or water hole bore thoroughly.
Drill bit 9 vis-a-vis, but a plurality of drill bit 9 can transversely arranged also longitudinal arrangement, during work about the drill bit of face simultaneously to the center line feeding, on one side subdrilling cross center line, another side gets into center line again, should thoroughly not make hole drill again drill bit interfere.
For the ease of the processing to cylindrical work 10, two multiaxis drill units 6 that are arranged on column 1 are equipped with cutter guide device 7, for the auxiliary guide effect of rimmer knife tool process.
Described cutter guide device 7 is provided with the pilot hole that the drill bit 9 for multiaxis drill unit 6 passes through, cutter guide device 7 is arranged on same slide plate with multiaxis drill unit 6, be connected with the drive unit V between cutter guide device 7 and multiaxis drill unit 6, this drive unit V drives cutter guide device 7 to move horizontally, cutter guide device 7 can move up and down along Z axis together with multiaxis drill unit 6 on slide plate, but Y-axis horizontal feed again.
The drive unit V is identical with drive unit I structure and mounting means, can accomplish to change according to bore position, automated movement is to position location, to adapt to the variation of diametric(al) position, when workpiece to be machined 10 is circle, cutter guide device 7 will be according to variation and the drilling spindle synchronous automatic adjusting position of workpiece circumference, the validity led with assurance to reach near as far as possible close workpiece.
In order to control conveniently, described electrical system comprises PLC and host computer, adopts the PLC+ host computer to be controlled, PLC controls each drive unit and multiaxis drill unit 6, PLC is connected with host computer, and host computer facilitates storage and the input of workpiece procedure, easy and simple to handle.The software work platform is WINXP, the operation interface close friend, and resource management is clear effectively, has powerful programing function; Workpiece size can manual keyboard be inputted, and also can input by the USB flash disk interface, and can carry out CAD/CAM and directly change, and removes the loaded down with trivial details of manual programming from.CAD domain paper according to the user, the host computer procedure of system can be converted to procedure by workpiece figure automatically, and sends the data to PLC, according to fixed datum mark, PLC is sent to each performance element by instruction, and detects the action situation of each performance element constantly.
Schematic diagram when Fig. 3 a is depicted as the utility model processing round piece.
The schematic diagram of half-twist when Fig. 3 b is depicted as the utility model processing round piece.
Schematic diagram while Figure 4 shows that the utility model processing box-shaped workpiece.
Schematic diagram while Figure 5 shows that the utility model processing pane shape workpiece.
After box-shaped or pane workpiece 10 clampings location are processed to the hole of a face, workpiece 10 is rotated to 90 °, again to workpiece 10 vertical direction hole processing, after the material hole of workpiece planarization machines, half-twist can be realized the water hole processing to the workpiece vertical direction, and the clamping of workpiece 10 is realized by the automatic pressing material device 5 that is positioned at workpiece 10 tops.
The utility model compared with prior art, has the following advantages:
1) high efficiency: two multiaxis drill units are worked simultaneously, and each drill unit is provided with two above drill bits, as each unit head fills three drill bits, can bore six holes simultaneously, 1.5 times of four unit heads of prior art numerical control drilling machine, therefore, high efficiency;
2) penetration rate is fast: two multiaxis drill unit horizontal direction feeding drillings of the present utility model, due to vertical direction boring, row cuts not smooth, therefore two levels and two Vertical Dynamic head boring rows than prior art cut smooth and easy, the rotating speed of drill bit and feed speed are 1-2 times of vertical direction boring, therefore, row cuts smooth and easy, and penetration rate is fast;
3) the clamping workpiece automaticity is high: twice clamping of workpiece one-time positioning just can complete whole processing, workpiece is placed on the workpiece positioning tool of rotary table, automatic pressing material device clamping work pieces is arranged, clamping for the first time behind workpiece location, after completing the processing of workpiece material hole, to clamping after the workpiece half-twist, can complete the water hole processing on workpiece circular arc face or vertical plane, can on an equipment, machine hole vertical, horizontal both direction; The utility model clamping workpiece is automatically to complete by pneumatic, only needs just can complete clamping workpiece several seconds.Be by completing manually than present technology, complete that clamped one time is minimum to be wanted about 20 minutes, clamping efficiency can improve several tens times;
4) product cost is low: the utility model is provided with two multiaxis drill units and seven numerical control axles; Than four unit heads of prior art, 11 numerical control axles, separately have gantry beam cost 1/3;
5) labour intensity is little: a people can operate two above equipment simultaneously, does not need artificial manual operations, by computer instruction, carries out workpiece processing, and the workman can reduce dust suction away from workpiece, and work condition environment is convenient to administer;
6) automaticity is high: the utility model adopts seven numerical control axles, two multiaxis drill units, rotary table, workpiece positioning tool and automatic pressing material devices, and adopt special electrical control, workpiece figure is inputed to computer, lathe positions processing automatically, make mistakes less, precision is high, automaticity is high.
The above-mentioned embodiment of the utility model, just illustrate, and is not only, all in the utility model scope or the change be equal in scope of the present utility model all by the utility model, surrounded.
Claims (7)
1. the two-sided numerical control drilling machine of the many main shafts of graphite block special horizontal, comprise column (1), lathe bed (2), travelling table (3) and electrical system, the left and right sides of described lathe bed (2) is respectively equipped with column (1), be provided with the travelling table (3) that can move along directions X between two columns (1), it is characterized in that: described travelling table (3) is provided with a rotary table with workpiece positioning tool (8) (4), the top of described rotary table (4) is provided with automatic pressing material device (5), a set of multiaxis drill unit (6) respectively is installed on described two columns (1), described multiaxis drill unit (6) can move up and down along Z axis, the main shaft of two multiaxis drill units (6) moves on same facade, multiaxis drill unit (6) along the relative feeding of Y-direction with exit.
2. the two-sided numerical control drilling machine of the many main shafts of graphite block special horizontal according to claim 1, it is characterized in that: described multiaxis drill unit (6) comprises at least 2 drilling main shafts that driven by a motor output shaft, and each drilling main shaft is provided with a drill bit (9).
3. the two-sided numerical control drilling machine of the many main shafts of graphite block special horizontal according to claim 2 is characterized in that: described multiaxis drill unit (6) comprises 2,3 or 3 above drilling main shafts that driven by a motor output shaft.
4. the two-sided numerical control drilling machine of the many main shafts of graphite block special horizontal according to claim 1 is characterized in that: described automatic pressing material device (5) is supported by portal frame, is hydraulic pressure material pressing device or Pneumatic material pressing device.
5. the two-sided numerical control drilling machine of the many main shafts of graphite block special horizontal according to claim 1 is characterized in that: described workpiece positioning tool (8) refers to as circular, square length or square cross location.
6. the two-sided numerical control drilling machine of the many main shafts of graphite block special horizontal according to claim 1, it is characterized in that: two multiaxis drill units (6) are equipped with cutter guide device (7), described cutter guide device (7) is provided with the pilot hole that passes through of drill bit (9) for multiaxis drill unit (6), cutter guide device (7) is arranged on same slide plate with multiaxis drill unit (6), described cutter guide device (7) is provided with drive unit V, this drive unit V drives cutter guide device (7) to move up and down and the Y-axis horizontal feed along Z axis together with multiaxis drill unit (6) on slide plate.
7. according to the two-sided numerical control drilling machine of the claim 1~6 any one many main shafts of described graphite block special horizontal, it is characterized in that: described electrical system comprises PLC and host computer, PLC controls each drive unit and multiaxis drill unit (6), and PLC is connected with host computer.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320442102 CN203357689U (en) | 2013-07-23 | 2013-07-23 | Special horizontal double-sided digital-controlled driller with multiple main shafts |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320442102 CN203357689U (en) | 2013-07-23 | 2013-07-23 | Special horizontal double-sided digital-controlled driller with multiple main shafts |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203357689U true CN203357689U (en) | 2013-12-25 |
Family
ID=49805506
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201320442102 Expired - Fee Related CN203357689U (en) | 2013-07-23 | 2013-07-23 | Special horizontal double-sided digital-controlled driller with multiple main shafts |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203357689U (en) |
Cited By (10)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103341916A (en) * | 2013-07-23 | 2013-10-09 | 济南志力数控机械有限公司 | Horizontal type multi-spindle two-sided numerical control drilling machine for graphite block |
| CN105312610A (en) * | 2015-12-05 | 2016-02-10 | 天津鼎天斯凯特机械有限公司 | Transverse push type drilling machine |
| CN106042050A (en) * | 2016-06-03 | 2016-10-26 | 中国工程物理研究院激光聚变研究中心 | Perforating device |
| CN107649702A (en) * | 2017-11-09 | 2018-02-02 | 南昌工程学院 | A kind of workpiece rotates clipping Drilling operation machinery |
| CN107931651A (en) * | 2017-12-21 | 2018-04-20 | 广州市正坚包装材料科技有限公司南沙分公司 | Plate metallic channel cutting device |
| CN108297290A (en) * | 2018-02-08 | 2018-07-20 | 张治国 | The processing method of П type graphite electric heaters |
| CN110695393A (en) * | 2019-10-08 | 2020-01-17 | 温州职业技术学院 | Submerged reducer punching device |
| CN111300053A (en) * | 2020-03-26 | 2020-06-19 | 浙江海帝克机床有限公司 | Double-turret combined machining machine tool |
| CN111823009A (en) * | 2020-08-05 | 2020-10-27 | 常州机电职业技术学院 | A synchronous drilling and milling tool for ultra-distant coaxial holes |
| CN117464057A (en) * | 2023-12-11 | 2024-01-30 | 荆门创升机械工业有限公司 | A butterfly valve flange end face drilling die tooling |
-
2013
- 2013-07-23 CN CN 201320442102 patent/CN203357689U/en not_active Expired - Fee Related
Cited By (11)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103341916A (en) * | 2013-07-23 | 2013-10-09 | 济南志力数控机械有限公司 | Horizontal type multi-spindle two-sided numerical control drilling machine for graphite block |
| CN105312610A (en) * | 2015-12-05 | 2016-02-10 | 天津鼎天斯凯特机械有限公司 | Transverse push type drilling machine |
| CN106042050A (en) * | 2016-06-03 | 2016-10-26 | 中国工程物理研究院激光聚变研究中心 | Perforating device |
| CN107649702A (en) * | 2017-11-09 | 2018-02-02 | 南昌工程学院 | A kind of workpiece rotates clipping Drilling operation machinery |
| CN107931651A (en) * | 2017-12-21 | 2018-04-20 | 广州市正坚包装材料科技有限公司南沙分公司 | Plate metallic channel cutting device |
| CN107931651B (en) * | 2017-12-21 | 2024-05-31 | 广州市正坚包装材料科技有限公司南沙分公司 | Plate wire groove cutting device |
| CN108297290A (en) * | 2018-02-08 | 2018-07-20 | 张治国 | The processing method of П type graphite electric heaters |
| CN110695393A (en) * | 2019-10-08 | 2020-01-17 | 温州职业技术学院 | Submerged reducer punching device |
| CN111300053A (en) * | 2020-03-26 | 2020-06-19 | 浙江海帝克机床有限公司 | Double-turret combined machining machine tool |
| CN111823009A (en) * | 2020-08-05 | 2020-10-27 | 常州机电职业技术学院 | A synchronous drilling and milling tool for ultra-distant coaxial holes |
| CN117464057A (en) * | 2023-12-11 | 2024-01-30 | 荆门创升机械工业有限公司 | A butterfly valve flange end face drilling die tooling |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN103341916A (en) | Horizontal type multi-spindle two-sided numerical control drilling machine for graphite block | |
| CN201760630U (en) | Three dimensional deep hole numerical control drilling machine | |
| CN104209756B (en) | A kind of six-shaft multifunctional numerical control drilling milling machine | |
| CN104259860B (en) | Five-axle linkage turning drilling-tapping is integrally machined machine | |
| CN202845837U (en) | Drilling machine | |
| CN203610970U (en) | Numerical-control turning, milling and drilling multifunctional compound machine tool | |
| CN208178927U (en) | A Composite CNC Machine Tool with Multi-Axis Turning and Milling Function | |
| CN203266102U (en) | Six axis drilling and milling CNC machine tool | |
| CN105522618A (en) | Full-automatic wood processing machine | |
| CN103008712A (en) | Intelligent single action and joint action type adjustable numerical control drilling and boring system with multiple main shafts and working method | |
| CN104414040B (en) | ornament processing device | |
| CN203245400U (en) | Intelligent three-dimensional multiple-spindle single action and joint action adjustable numerical-control drilling and boring system | |
| CN202921954U (en) | Multi-spindle drilling machine | |
| RU98350U1 (en) | MULTI-PURPOSE MACHINE WITH NUMERIC SOFTWARE CONTROL AND AUTOMATIC TOOL CHANGE | |
| CN104043853A (en) | Numerical control drilling machine tool | |
| CN203779102U (en) | Crossed sliding rail numerical control milling and drilling machine | |
| CN203505764U (en) | Ornament processing device | |
| CN203076628U (en) | Horizontal double-end automatic feeding multiple-shaft drilling machine | |
| CN103551861A (en) | Numerical control machining center machine tool | |
| CN205466586U (en) | Full -automatic wood working machine | |
| CN204018775U (en) | Numerical control rocker arm drilling machine | |
| CN204135781U (en) | A kind of drilling and milling machine servo feeding apparatus | |
| CN204195232U (en) | Five-axle linkage turning drilling-tapping one processing machine | |
| CN203509592U (en) | A CNC machining center | |
| CN206550759U (en) | Gantry machining center |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20131225 Termination date: 20200723 |