CN203343781U - Eccentric hole machining clamp used for lathe - Google Patents
Eccentric hole machining clamp used for lathe Download PDFInfo
- Publication number
- CN203343781U CN203343781U CN 201320297559 CN201320297559U CN203343781U CN 203343781 U CN203343781 U CN 203343781U CN 201320297559 CN201320297559 CN 201320297559 CN 201320297559 U CN201320297559 U CN 201320297559U CN 203343781 U CN203343781 U CN 203343781U
- Authority
- CN
- China
- Prior art keywords
- lathe
- ring
- semi
- eccentric hole
- positioning disc
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003754 machining Methods 0.000 title description 2
- 238000004519 manufacturing process Methods 0.000 abstract description 6
- 238000000034 method Methods 0.000 description 6
- 230000009286 beneficial effect Effects 0.000 description 1
- 238000005520 cutting process Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000005482 strain hardening Methods 0.000 description 1
Images

Landscapes
- Gripping On Spindles (AREA)
Abstract
本实用新型属于一种车床用加工夹具,公开一种车床用偏心孔加工夹具。其主要特点是由定位轴、定位圆盘、工件夹紧装置组成;所述定位轴与定位圆盘一端面同轴连接固定,所述工件夹紧装置设置在定位圆盘的另一侧,该工件夹紧装置由半环、固定螺栓组成,半环的其中一个连接部采用铰接方式相连接,半环的另一连接部采用可拆卸连接件固定,在半环上、沿半环的中心对称设置至少两个固定螺栓,固定螺栓的端头指向半环的中心,并在固定螺栓的端头连接防脱件,半环通过连接板与该侧定位圆盘端面连接固定。该新型夹具可适合一定尺寸的不同直径的圆柱体工件装夹,定位效率高,定位精准,装卸工件方便,特别适用于大批量生产。
The utility model belongs to a processing jig for a lathe, and discloses an eccentric hole processing jig for a lathe. Its main features are composed of a positioning shaft, a positioning disc, and a workpiece clamping device; the positioning shaft is connected and fixed coaxially with one end of the positioning disc, and the workpiece clamping device is arranged on the other side of the positioning disc. The workpiece clamping device is composed of a half ring and a fixing bolt. One of the connecting parts of the half ring is connected by a hinge, and the other connecting part of the half ring is fixed by a detachable connecting piece. It is symmetrical on the half ring and along the center of the half ring. Set at least two fixing bolts, the ends of the fixing bolts point to the center of the half ring, and the ends of the fixing bolts are connected with anti-off parts, and the half ring is connected and fixed with the end face of the side positioning disc through the connecting plate. The new fixture is suitable for clamping cylindrical workpieces of different diameters of a certain size, has high positioning efficiency, accurate positioning, and convenient loading and unloading of workpieces, and is especially suitable for mass production.
Description
技术领域 technical field
本实用新型属于一种车床用加工夹具,尤其是一种车床用偏心孔加工夹具。 The utility model belongs to a processing jig for a lathe, in particular to an eccentric hole processing jig for a lathe.
背景技术 Background technique
在机械冷加工过程中,我们常会遇到一些棘手问题。例如有些具有斜面、斜孔、偏心、曲面等,通常普通机床根本无法完成,即使完成了,也很难保证质量。这时生产上就用到夹具了。夹具在整个切削加工行业中起到极为重要的作用,生产工人通过利用合适的夹具就能在普通机床上完成对特殊形状零件的的加工。 In the process of mechanical cold working, we often encounter some difficult problems. For example, some have inclined surfaces, inclined holes, eccentricities, curved surfaces, etc., which are usually impossible to complete with ordinary machine tools. Even if they are completed, it is difficult to guarantee the quality. At this time, fixtures are used in production. Fixtures play an extremely important role in the entire cutting processing industry. Production workers can complete the processing of special-shaped parts on ordinary machine tools by using suitable fixtures.
目前,针对车削偏心孔。传统的方法先由钳工根据图样画出偏心孔的位置,然后由车工根据所划的孔线上四爪单支卡盘或弯板、花盘等通用夹具,经找正后车好偏心孔。传统方法可以加工偏心孔,但操作过程困难,调整偏心距的难度大,对操作工经验要求高,尤其是在大批量生产中,不易保证产品质量,不能满足大批量生产的要求。 Currently, for turning eccentric holes. In the traditional method, the fitter first draws the position of the eccentric hole according to the drawing, and then the turner turns the eccentric hole after alignment with a four-jaw single chuck or a common fixture such as a bent plate or a face plate on the drawn hole line. The traditional method can process eccentric holes, but the operation process is difficult, the difficulty of adjusting the eccentric distance is high, and the operator experience is high, especially in mass production, it is difficult to guarantee product quality and cannot meet the requirements of mass production.
实用新型内容 Utility model content
本实用新型为解决其技术问题所采取的技术方案是,设计一种车床用偏心孔加工夹具,由定位轴、定位圆盘、工件夹紧装置组成;所述定位轴与定位圆盘一端面同轴连接固定,所述工件夹紧装置设置在定位圆盘的另一侧,该工件夹紧装置由半环、固定螺栓组成,半环的其中一个连接部采用铰接方式相连接,半环的另一连接部采用可拆卸连接件固定,在半环上、沿半环的中心对称设置至少两个固定螺栓,固定螺栓的端头指向半环的中心,并在固定螺栓的端头连接防脱件,半环通过连接板与该侧定位圆盘端面连接固定。 The technical solution adopted by the utility model for solving the technical problems is to design a fixture for processing eccentric holes for a lathe, which is composed of a positioning shaft, a positioning disc, and a workpiece clamping device; The shaft is connected and fixed, and the workpiece clamping device is arranged on the other side of the positioning disc. The workpiece clamping device is composed of a half ring and a fixing bolt. One of the connecting parts of the half ring is connected in a hinged manner, and the other half ring The first connecting part is fixed by a detachable connecting piece, and at least two fixing bolts are symmetrically arranged on the half ring and along the center of the half ring. , the half ring is connected and fixed with the end face of the side positioning disc through the connecting plate.
进一步地,所述半环与定位圆盘同轴设置。 Further, the half ring is arranged coaxially with the positioning disc.
进一步地,所述防脱件是V形块。 Further, the anti-off piece is a V-shaped block.
进一步地,所述铰接方式具体是采用第一销轴铰接,所述可拆卸连接件具体是活节螺栓,活节螺栓与半环通过第二销轴铰接。 Further, the hinged way is specifically to use a first pin to hinge, the detachable connecting member is specifically a swing bolt, and the swing bolt and the half ring are hinged through a second pin.
进一步地,所述定位轴端部呈圆锥形。 Further, the end of the positioning shaft is conical.
进一步地,所述固定螺栓的个数为两个。 Further, the number of the fixing bolts is two.
进一步地,所述定位圆盘朝向夹紧装置一侧的端面上设有偏心距刻度值。 Further, an eccentricity scale value is provided on the end face of the positioning disc facing the side of the clamping device.
进一步地,所述V形块与固定螺栓的端头连接成一体。 Further, the V-shaped block is integrally connected with the end of the fixing bolt.
本实用新型的有益效果是:该新型夹具可适合一定尺寸的不同直径的圆柱体工件装夹,偏心定位效率高,定位精准,装卸工件方便,特别适用于大批量生产。 The beneficial effects of the utility model are: the new fixture can be suitable for clamping cylindrical workpieces of different diameters of a certain size, has high eccentric positioning efficiency, accurate positioning, convenient loading and unloading of workpieces, and is especially suitable for mass production.
附图说明 Description of drawings
图1为本实用新型一种车床用偏心孔加工夹具的结构示意图; Fig. 1 is the structure schematic diagram of a kind of eccentric hole processing jig of lathe of the present invention;
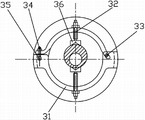
图2为图1的左视图。 Fig. 2 is a left side view of Fig. 1 .
具体实施方式 Detailed ways
参看图1、2,一种车床用偏心孔加工夹具,由定位轴1、定位圆盘2、工件夹紧装置3组成;所述定位轴1与定位圆盘2一端面同轴连接固定,定位轴1端部呈圆锥形,所述工件夹紧装置3设置在定位圆盘2的另一侧,该工件夹紧装置3由半环31、固定螺栓32组成,半环31的其中一个连接部采用铰接方式相连接,该铰接方式具体是采用第一销轴33铰接,半环31的另一连接部采用可拆卸连接件固定,该可拆卸连接件具体是活节螺栓34,活节螺栓34与半环31通过第二销轴35铰接,在半环31上、沿半环31的中心对称设置至少两个固定螺栓32,该固定螺栓32的个数具体可以是两个,固定螺栓32的端头指向半环31的中心,并在固定螺栓32的端头连接防脱件,该防脱件是V形块36,V形块36与固定螺栓32的端头连接成一体,半环31通过连接板4与该侧定位圆盘2端面连接固定,所述半环31与定位圆盘2同轴设置,定位圆盘2朝向夹紧装置3一侧的端面上设有偏心距刻度值。
Referring to Figures 1 and 2, an eccentric hole machining fixture for a lathe is composed of a
使用时,把定位轴1装配于车床主轴内,松开活节螺栓34上的螺母,活节螺栓34可绕第二销轴35转动,半环31可绕第一销轴33转动,放入工件后旋紧活节螺栓34的螺母,工件可划线,配合定位圆盘2找正工件的方位和偏心点,松开固定螺栓32,调整好工件位置,再旋紧,用V形块36夹紧工件,完工后,旋开活节螺栓34和固定螺栓32,可拆掉工件。
During use, the
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320297559 CN203343781U (en) | 2013-05-28 | 2013-05-28 | Eccentric hole machining clamp used for lathe |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320297559 CN203343781U (en) | 2013-05-28 | 2013-05-28 | Eccentric hole machining clamp used for lathe |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203343781U true CN203343781U (en) | 2013-12-18 |
Family
ID=49743714
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201320297559 Expired - Fee Related CN203343781U (en) | 2013-05-28 | 2013-05-28 | Eccentric hole machining clamp used for lathe |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203343781U (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104440756A (en) * | 2014-12-09 | 2015-03-25 | 国家电网公司 | Lifting mounting device |
| CN105108513A (en) * | 2015-08-31 | 2015-12-02 | 重庆帅昌机械制造有限公司 | Angle iron type lathe fixture for air valve |
| CN109332753A (en) * | 2018-12-05 | 2019-02-15 | 哈电集团(秦皇岛)重型装备有限公司 | A kind of BTA drill bit Counterboring apparatus and expanding method |
-
2013
- 2013-05-28 CN CN 201320297559 patent/CN203343781U/en not_active Expired - Fee Related
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104440756A (en) * | 2014-12-09 | 2015-03-25 | 国家电网公司 | Lifting mounting device |
| CN105108513A (en) * | 2015-08-31 | 2015-12-02 | 重庆帅昌机械制造有限公司 | Angle iron type lathe fixture for air valve |
| CN109332753A (en) * | 2018-12-05 | 2019-02-15 | 哈电集团(秦皇岛)重型装备有限公司 | A kind of BTA drill bit Counterboring apparatus and expanding method |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN106312633B (en) | A kind of machining clamping multi-functional clamp | |
| CN205254276U (en) | Gapless positioning fixture of awl in hollow shaft class work piece | |
| CN207013741U (en) | A kind of frock for turning eccentric shaft parts | |
| CN105014421A (en) | Self-adaptive flat tongs | |
| CN205630066U (en) | Press crankshaft machining complete set anchor clamps | |
| CN202292184U (en) | Automatic centering flat tongs for machine | |
| CN203765504U (en) | Combined clamp for machining semi-annular workpiece | |
| CN103624282A (en) | Automatic aligning and clamping mechanism for three-jaw chuck | |
| CN202062304U (en) | Cylindrical grinder clamp for sleeve type component | |
| CN202556081U (en) | Eccentric clamp | |
| CN203944861U (en) | Special Tooling for Bearing Ring Turning | |
| CN107139000A (en) | The fixture of Step Shaft cylindrical turning plane and radial bore | |
| CN203918498U (en) | A kind of milling and grinding positioning tool of cylindrical component | |
| CN203635973U (en) | Automatic aligning clamp mechanism for three-jaw chucks | |
| CN203266213U (en) | Lathe manual spindle clamp | |
| CN207344227U (en) | Split type V-type angle block gauge | |
| CN207043761U (en) | A kind of fixture for being used to process thin-walled ring external diameter | |
| CN202639924U (en) | Turning fixture for wheel groove milling cutter | |
| CN105252325A (en) | Double-centre outer circle machining tool | |
| CN205465495U (en) | Multi -disc clamping device of circle shear blade | |
| CN205085696U (en) | A frock clamp that is used for processing hexagonal on axle class part | |
| CN219665530U (en) | Automatic centering clamping device of welding robot | |
| CN204413698U (en) | A kind of fixture | |
| CN205571490U (en) | A drilling jig for drilling the center hole at the end of a shaft | |
| CN204997456U (en) | Special four -axis anchor clamps |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20131218 Termination date: 20140528 |