CN203143757U - Full-automatic film winding machine - Google Patents
Full-automatic film winding machine Download PDFInfo
- Publication number
- CN203143757U CN203143757U CN 201320061475 CN201320061475U CN203143757U CN 203143757 U CN203143757 U CN 203143757U CN 201320061475 CN201320061475 CN 201320061475 CN 201320061475 U CN201320061475 U CN 201320061475U CN 203143757 U CN203143757 U CN 203143757U
- Authority
- CN
- China
- Prior art keywords
- cylinder
- film
- piston rod
- frame
- mandrel
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000004804 winding Methods 0.000 title abstract description 11
- 239000012528 membrane Substances 0.000 claims description 28
- 238000010438 heat treatment Methods 0.000 claims description 4
- 239000004033 plastic Substances 0.000 abstract description 4
- 238000004519 manufacturing process Methods 0.000 abstract description 3
- 239000010408 film Substances 0.000 abstract 7
- 230000005540 biological transmission Effects 0.000 abstract 1
- 239000010409 thin film Substances 0.000 abstract 1
- 238000000034 method Methods 0.000 description 4
- 239000012785 packaging film Substances 0.000 description 2
- 229920006280 packaging film Polymers 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 1
- 239000002985 plastic film Substances 0.000 description 1
- 229920006255 plastic film Polymers 0.000 description 1
- 230000007115 recruitment Effects 0.000 description 1
Images

Landscapes
- Winding Of Webs (AREA)
Abstract
The utility model relates to a full-automatic film winding machine. The full-automatic film winding machine is characterized by comprising a film supplying mechanism, a film winding mechanism and a controller. The film winding mechanism comprises guide tracks, a rack is arranged on the guide tracks, and a main shaft is arranged on the rack. One end of the main shaft is provided with a wheel disc, and mandrels are uniformly distributed on the periphery of the inner surface of the wheel disc. An electric motor is arranged below the wheel disk, belt pulleys are arranged on the main shaft and an output shaft of the electric motor, and a transmission belt is connected between the two belt pulleys. A jacking cylinder is arranged on the rack, and a piston rod of the jacking cylinder abuts against one of the mandrels. A tube delivery platform is arranged on one side of the rack, one side of the tube delivery platform, which is adjacent to the rack, is provided with a first guide rod and a tube groove which is used for holding a core tube, one end of the first guide rod is provided with a tube installing cylinder, a first shifting fork is fixed at the outer end of a piston rod of the tube installing cylinder and extends into the tube groove, and the core tube inside the tube groove is shifted and sleeved on the mandrel by the first shifting fork through retraction of the piston rod. By the aid of the full-automatic film winding machine, the labor quantity is small, the labor intensity is low, the working efficiency is high, and the production cost is low. The full-automatic film winding machine is applicable to winding, cutting-off and unwinding of plastic thin films.
Description
Technical field
The utility model relates to a kind of membrane coiler structure.Specifically, be the full automaticity membrane coiler that food fresh keeping film, packaging film and so on plastic sheeting is twined and cuts off automatically, unloads volume.
Background technology
At present, in the plastic sheeting processing industry of food fresh keeping film, packaging film and so on, being used for the equipment of winding plastic film all is that tradition is around film device.Adopt tradition around film device during around film, no matter be tubulature, unload pipe, still cut off plastic sheeting, all be to adopt manual operations, namely rely on workman's craft to carry out tubulature respectively fully, unload pipe or film rupturing operation, the workman who not only needs is many, labour intensity is big, and inefficiency, productive costs height.
The utility model content
Problem to be solved in the utility model provides a kind of full automaticity membrane coiler.Adopt full automaticity membrane coiler of the present utility model to come coiling film volume, not only can reduce the recruitment number, reduce working strength of workers, and can increase work efficiency, reduce production costs.
For addressing the above problem, the utility model is taked following technical scheme:
Full automaticity membrane coiler characteristics of the present utility model are to comprise film supplying unit, membrane coiler structure and controller.Described membrane coiler structure contains guide rail, and organic frame on the guide rail has main shaft and the two to be rotatable shape and cooperates on the frame.Described main shaft is vertical with described guide rail, and main shaft one end has wheel disc, is evenly equipped with the mandrel of plug-in mounting core pipe around the inside face of wheel disc, mandrel axially vertical with the card of wheel disc, and mandrel one end and wheel disc are fixed together; Have near switch on the frame in the wheel disc outside.Main shaft one end of contiguous wheel disc stretches out outside wheel disc, and there is motor the wheel disc below, on the external part of main shaft and the output shaft of motor belt wheel is arranged all, is connected with driving band between two belt wheels.Hold out against cylinder on the frame of contiguous mandrel front of motor, this holds out against cylinder and is on the frame of contiguous film supplying unit one side.Hold out against vertically paralleling with main shaft of cylinder, it is can be when taking turns disc spins relative with the front of motor of all mandrels and withstand the front of motor of mandrel to hold out against the piston rod of cylinder.Described frame one side is sent the pipe platform, and this send the pipe platform to be in frame one side of described guide rail rear end.The pipe platform that send of contiguous frame has to place the tube seat of core pipe on one side, there is first guide rod that parallels with tube seat the tube seat inboard, first guide rod, one end of contiguous frame is provided with the tubulature cylinder, the piston rod of tubulature cylinder is in when stretching out fully under described first guide rod, fixedly there is first shift fork piston rod outer end, the bar hole is arranged on first shift fork, described guide rod penetrates in the bar hole, described first shift fork stretches in the described tube seat, by the withdrawal of piston rod, can the core pipe in the tube seat be dialled to and be enclosed within on the mandrel by first shift fork.
In the frame of main shaft below second guide rod is arranged, contiguous frame one side that holds out against cylinder is unloaded the pipe cylinder, unloads when the piston rod of managing cylinder stretches out fully to be on second guide rod.Fixedly there is second shift fork piston rod outer end of unloading the pipe cylinder, and the bar hole is arranged on second shift fork, and described second guide rod penetrates in the bar hole.Described second shift fork extends the front of motor of mandrel, by the withdrawal of piston rod, can will be unloaded from mandrel around the core pipe of full film by second shift fork.
Described film supplying unit is in contiguous guide rail one end that holds out against cylinder one side, is connected with reset cylinder between the bottom of film supplying unit and membrane coiler structure, between the top of film supplying unit and membrane coiler structure the film cutting-off mechanism is arranged.
Describedly hold out against cylinder, tubulature cylinder, unload the pipe cylinder, reset cylinder all links to each other with controller by lead with motor.
Take such scheme, have the following advantages;
By such scheme as can be seen, by last process, the core pipe is rolled in the tube seat of managing on the platform automatically, then, control the tubulature cylinder by controller, make the action of withdrawing of the piston rod of tubulature cylinder, and by first shift fork that is installed in the piston rod outer end core pipe is contained on the mandrel.Afterwards, under the control of motor, pass through the belt wheel of its mouth, the belt wheel of main shaft one end, driving band and the main shaft driven wheel disc spins between two belt wheels by motor, make another mandrel corresponding with tube seat, repeat above-mentioned course of action again, core pipe in the tube seat is contained on another mandrel, until making the core pipe is housed all on each mandrel.Afterwards, when driving core pipe rotation on the mandrel by the rotation of the live roll in the film supplying unit and intermediate calender rolls, the winding film that film supplying unit is sent here is on a core pipe.When a core pipe behind full film, describedly can give signal of controller near switch, given by controller again and cut the film cylinder, unload the pipe cylinder, hold out against cylinder and motor is assigned instruction simultaneously, stretch under the film cylinder piston rod and cut off film by cutting, the piston rod withdrawal that holds out against cylinder is broken away from around that full core pipe.Meanwhile, corresponding with the intermediate calender rolls of film supplying unit to the core pipe that makes a sky by driven by motor wheel disc spins, by the piston rod withdrawal of unloading the pipe cylinder, will unload around the full core pipe of film, and make film that film supplying unit sends here on the core pipe of a sky.Afterwards, repeat said process repeatedly, do not need manual operations, just can realize automatic tubulature, automatically unload pipe, automatically around actions such as films.The workman who not only needs is few, and labour intensity is little, also can increase work efficiency, and reduces production costs.
Description of drawings
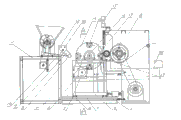
Fig. 1 is full automaticity membrane coiler structural representation of the present utility model;
Fig. 2 is the schematic top plan view of Fig. 1;
Fig. 3 is the A-A cross-sectional schematic of Fig. 1.
The specific embodiment
As Fig. 1, Fig. 2 and shown in Figure 3, full automaticity membrane coiler of the present utility model comprises film supplying unit, membrane coiler structure and controller 24.Described membrane coiler structure contains two guide rails that are parallel to each other 3, and this guide rail fixes on the ground under installing condition.Guide rail 3 is provided with frame 2, and frame 2 two bottom sides respectively are equipped with two rollers 4, and two rollers 4 of the same side place on that guide rail 3 of homonymy, and described frame 2 can seesaw along guide rail 3 by this roller.Described frame 2 is the cuboid framework, and two long margin frames at its top are provided with main shaft 16, and main shaft 16 two ends all are rotatable shape and cooperate respectively with between two long margin frames of frame 2 by bearing, makes described main shaft 16 perpendicular with described guide rail 3.Main shaft 16 1 ends are provided with wheel disc 13, and wheel disc 13 centers are processed with axis hole, and described main shaft 16 penetrates in the axis hole at wheel disc 13 centers and the two is fixed together.Described wheel disc 13 is fixed on a long margin frame inboard on frame 2 tops, is evenly equipped with four mandrels 14 that are used for plug-in mounting core pipe around the inside face of wheel disc 13, and these four mandrels all equate with the spacing of described main shaft 16.Mandrel 14 axially vertical with the card of wheel disc 13,13 employings of mandrel 14 1 ends and wheel disc bolt is fixed together.Being equipped with near switch 19 on the frame 2 in wheel disc 13 outsides, is whether controller 24 provides core pipe on the mandrel 14 around the signal of full film to be used for, described near switch 19 contiguous wheel discs 13.Main shaft 16 1 ends of contiguous wheel disc 13 stretch out outside wheel disc 13, on the frame 2 of wheel disc 13 belows motor 6 are installed, and this motor is stepping motor.All fixedly there are 5 of belt wheel 5, two belt wheels to be connected with driving band 7 on the output shaft of the external part of main shaft 16 and motor 6, by the output shaft rotation of motor 6, can pass through belt wheel 5,13 rotations of driving band 7 drive wheel discs.Fixedly hold out against cylinder 21 on the frame 2 of contiguous mandrel 14 front of motors, this holds out against cylinder and is on the frame 2 of contiguous film supplying unit 18 1 sides.Hold out against vertically paralleling with main shaft 16 of cylinder 21, it is can be when wheel disc 13 rotates relative with the front of motor of all mandrels 14 and withstand the front of motor of mandrel 14 to hold out against the piston rod of cylinder 21.Described frame 2 one sides are provided with send pipe platform 11, and this send the pipe platform to be in frame 2 one sides of described guide rail 3 rear ends.The pipe platform 11 that send of contiguous frame 2 is processed with to place the tube seat 8 of core pipe on one side, tube seat 8 inboards are provided with two first guide rods 121 that parallel with tube seat 8, and the two ends of described two first guide rods 121 all are separately fixed at sending on the pipe platform 11 of tube seat 8 two ends by permanent seat 12.Those permanent seat 12 arranged outside of contiguous frame 2 one sides have tubulature cylinder 10, tubulature cylinder 10 1 ends of adjacent piston bar outer end are fixed on the described respective fixation seat 12, be under described first guide rod 121 when making the piston rod of tubulature cylinder 10 stretch out fully, fixedly there is first shift fork 9 outer end of piston rod, be processed with the bar hole on first shift fork 9, described first guide rod 121 penetrates in the bar hole and the two is bearing fit.The outer end of described first shift fork 9 is stretched in the described tube seat 8, by the withdrawal of piston rod, can the core pipe in the tube seat 8 be dialled to and be enclosed within on the corresponding mandrel 14 by first shift fork 9.
Be provided with two second guide rods 22 in the frame 2 of main shaft 16 belows, the two ends of these two second guide rods are fixed on the frame 2 by nut respectively.Contiguous frame 2 one sides that hold out against cylinder 21 are provided with unloads pipe cylinder 20, and pipe cylinder 20 1 ends that unload of adjacent piston bar outer end are fixed on the frame 2, make the piston rod that unloads pipe cylinder 20 be on second guide rod 22 when stretching out fully.The piston rod outer end of unloading pipe cylinder 20 fixedly has on second shift fork, 23, the second shift forks 23 and is processed with two bar holes, and described second guide rod 22 penetrates respectively in the respective rods hole and the two is bearing fit.Described second shift fork 23 extends the front of motor of mandrel 14, by the withdrawal of piston rod, can will be unloaded from mandrel 14 around the core pipe of full film by second shift fork 23.
Described film supplying unit 18 is in contiguous guide rail 3 front ends that hold out against cylinder 21 1 sides, be connected with reset cylinder 1 between the bottom of film supplying unit 18 and membrane coiler structure, by stretching of reset cylinder 1 piston rod, can realize that frame 2 seesaws along guide rail 3, the mandrel 14 of realizing treating the cored pipe with send pipe platform 11 near and the contact of the mandrel 14 that separates and have the core pipe and film supplying unit 18 or separate.
Core pipe on close that mandrel 14 of film supplying unit 18 1 sides is after expiring film, for realizing automatically film being cut off.Between the top between film supplying unit 18 and membrane coiler structure, be provided with the film cutting-off mechanism.Described film cutting-off mechanism contains cuts film cylinder 15 and cutter 17.Describedly cut film supplying unit 18 tops that film cylinder 15 is fixed on contiguous membrane coiler structure one side.Cut the piston rod of film cylinder 15 down, described cutter 17 is heating wire, and this heating wire is fixed on the piston rod outer end of cutting film cylinder 15 by means of support, and cutter 17 is towards the below.Cutting film cylinder 15 links to each other with controller 24 by lead.
Describedly hold out against cylinder 21, tubulature cylinder 10, unload pipe cylinder 20, reset cylinder 1 all links to each other with controller 24 by lead with motor 6.For simplicity, all omitted the lead that is connected that holds out against cylinder 21, tubulature cylinder 10, unloads pipe cylinder 20, reset cylinder 1 and 24 of motor 6 and controllers among Fig. 1, Fig. 2 and Fig. 3.
For ease of sending the core pipe on the pipe platform 11 can roll into automatically in the described tube seat 8, one side the described table top of pipe platform 11 that send is close to being inclined upwardly of frame 2 around it, make the core pipe to roll into automatically in the tube seat 8.
During work, by last process, the core pipe is rolled into automatically send in the tube seat 8 of managing on the platform 11.Then, control tubulature cylinder 10 by controller 24, make the action of withdrawing of the piston rod of tubulature cylinder 10, and by first shift fork 9 that is installed in the piston rod outer end core pipe is contained on the mandrel 14.Afterwards, under the control of motor 2, driving band 7 and main shaft 16 by 5 of motor 2 belt wheel 5, the belt wheel 5 of main shaft 16 1 ends, two belt wheels by its mouth drive wheel discs 13 rotations, make another mandrel 14 corresponding with tube seat 8, repeat above-mentioned course of action again, core pipe in the tube seat 8 is contained on another mandrel 14, until making on each mandrel 14 the core pipe is housed all.Afterwards, when driving core pipe rotation on the mandrel 14 by the rotation of the live roll in the film supplying unit 18 and intermediate calender rolls, the winding film that film supplying unit 18 is sent here is on a core pipe.When a core pipe behind full film, describedly can give 24 1 signals of controller near switch 19, cut film cylinder 15, unloaded pipe cylinder 20, held out against cylinder 21 and motor 6 is assigned instruction simultaneously by controller 24 again, stretch under film cylinder 15 piston rods and cut off film by cutting, the piston rod withdrawal that holds out against cylinder 21 is broken away from around that full core pipe.Meanwhile, it is corresponding with the intermediate calender rolls of film supplying unit 18 to the core pipe that makes a sky to drive wheel disc 13 rotations by motor 6, by the piston rod withdrawal of unloading pipe cylinder 20, will unload around the core pipe of full film, and make film that film supplying unit 18 sends here on the core pipe of a sky.Afterwards, repeat said process repeatedly, realize automatic tubulature, twine, unload automatically pipe automatically.
Claims (6)
1. the full automaticity membrane coiler is characterized in that comprising film supplying unit (18), membrane coiler structure and controller (24); Described membrane coiler structure contains guide rail (3), and guide rail (3) is gone up organic frame (2), has main shaft (16) and the two to be rotatable shape on the frame (2) and cooperates; Described main shaft (16) is vertical with described guide rail (3), main shaft (16) one ends have wheel disc (13), be evenly equipped with the mandrel (14) of plug-in mounting core pipe around the inside face of wheel disc (13), mandrel (14) axially vertical with the card of wheel disc (13), mandrel (14) one ends and wheel disc (13) are fixed together; Have near switch (19) on the frame (2) in wheel disc (13) outside; Main shaft (16) one ends of contiguous wheel disc (13) stretch out outside wheel disc (13), there is motor (6) wheel disc (13) below, belt wheel (5) is all arranged on the output shaft of the external part of main shaft (16) and motor (6), be connected with driving band (7) between two belt wheels (5); Hold out against cylinder (21) on the frame (2) of contiguous mandrel (14) front of motor, this holds out against cylinder and is on the frame (2) of contiguous film supplying unit (18) one sides; Hold out against vertically paralleling with main shaft (16) of cylinder (21), it is can be when wheel disc (13) rotates relative with the front of motor of all mandrels (14) and withstand the front of motor of mandrel (14) to hold out against the piston rod of cylinder (21); Described frame (2) one sides are sent pipe platform (11), and this send the pipe platform to be in frame (2) one sides of described guide rail (3) rear end; The tube seat (8) that has to place the core pipe on platform (11) one side is managed in sending of contiguous frame (2), there is first guide rod (121) that parallels with tube seat (8) tube seat (8) inboard, first guide rod (121) one ends of contiguous frame (2) are provided with tubulature cylinder (10), the piston rod of tubulature cylinder (10) is under described first guide rod (121) when stretching out fully, fixedly there is first shift fork (9) the piston rod outer end, first shift fork has the bar hole on (9), described first guide rod (121) penetrates in the bar hole, described first shift fork (9) stretches in the described tube seat (8), by the withdrawal of piston rod, can the core pipe in the tube seat (8) be dialled to and be enclosed within on the mandrel (14) by first shift fork (9);
In the frame (2) of main shaft (16) below second guide rod (22) is arranged, contiguous frame (2) one sides that hold out against cylinder (21) are unloaded pipe cylinder (20), unload when the piston rod of managing cylinder (20) stretches out fully to be on second guide rod (22); Fixedly there is second shift fork (23) the piston rod outer end of unloading pipe cylinder (20), and second shift fork has the bar hole on (23), and described second guide rod (22) penetrates in the bar hole; Described second shift fork (23) extends the front of motor of mandrel (14), by the withdrawal of piston rod, can will be unloaded from mandrel (14) around the core pipe of full film by second shift fork (23);
Described film supplying unit (18) is in contiguous guide rail (3) one ends that hold out against cylinder (21) one sides, is connected with reset cylinder (1) between the bottom of film supplying unit (18) and membrane coiler structure, between the top of film supplying unit (18) and membrane coiler structure the film cutting-off mechanism is arranged;
Describedly hold out against cylinder (21), tubulature cylinder (10), unload pipe cylinder (20), reset cylinder (1) all links to each other with controller (24) by lead with motor (6).
2. full automaticity membrane coiler according to claim 1 is characterized in that described motor (6) is stepping motor.
3. full automaticity membrane coiler according to claim 1 is characterized in that described mandrel (14) has four, and these four mandrels all equate with the spacing of described main shaft (16).
4. full automaticity membrane coiler according to claim 1, it is characterized in that the described table top that send pipe platform (11) around its contiguous frame (2) one side be inclined upwardly, make the core pipe can roll into automatically in the tube seat (8).
5. full automaticity membrane coiler according to claim 1, it is characterized in that described film cutting-off mechanism contains cuts film cylinder (15) and cutter, cut film cylinder (15) and link to each other with controller (24) by lead, describedly cut film supplying unit (18) top that film cylinder (15) is fixed on contiguous membrane coiler structure one side; Cut the piston rod of film cylinder (15) down, described cutter is fixed on the piston rod outer end of cutting film cylinder (15).
6. full automaticity membrane coiler according to claim 5 is characterized in that described cutter (17) is heating wire, and this heating wire is fixed on the piston rod outer end of cutting film cylinder (15) by means of support, and cutter (17) is towards the below.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320061475 CN203143757U (en) | 2013-02-04 | 2013-02-04 | Full-automatic film winding machine |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320061475 CN203143757U (en) | 2013-02-04 | 2013-02-04 | Full-automatic film winding machine |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203143757U true CN203143757U (en) | 2013-08-21 |
Family
ID=48971301
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201320061475 Expired - Fee Related CN203143757U (en) | 2013-02-04 | 2013-02-04 | Full-automatic film winding machine |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203143757U (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN107857151A (en) * | 2017-11-22 | 2018-03-30 | 江门新时代包装材料有限公司 | A kind of tape roll material-changing device of adhesive tape cutting machine |
| CN108100720A (en) * | 2016-11-25 | 2018-06-01 | 常州百利菲特防水设备有限公司 | Full-automatic volume felt intubation machine |
| CN108861746A (en) * | 2018-07-23 | 2018-11-23 | 李朋飞 | A kind of magnetic suspension electricity drive type automatic rewinding device of roll paper |
| CN112829982A (en) * | 2021-02-22 | 2021-05-25 | 三明学院 | A kind of packaging equipment and its packaging process |
-
2013
- 2013-02-04 CN CN 201320061475 patent/CN203143757U/en not_active Expired - Fee Related
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN108100720A (en) * | 2016-11-25 | 2018-06-01 | 常州百利菲特防水设备有限公司 | Full-automatic volume felt intubation machine |
| CN107857151A (en) * | 2017-11-22 | 2018-03-30 | 江门新时代包装材料有限公司 | A kind of tape roll material-changing device of adhesive tape cutting machine |
| CN108861746A (en) * | 2018-07-23 | 2018-11-23 | 李朋飞 | A kind of magnetic suspension electricity drive type automatic rewinding device of roll paper |
| CN112829982A (en) * | 2021-02-22 | 2021-05-25 | 三明学院 | A kind of packaging equipment and its packaging process |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN105035812B (en) | Multi-station full-automatic central surface coiling machine | |
| CN204873177U (en) | Asbest rope spindle winder | |
| CN104925558A (en) | Full-automatic filter element winding machine | |
| CN201220868Y (en) | Reel cotton pulp production facility | |
| CN204383855U (en) | A kind of thin film winding machine with pressure jacking mechanism | |
| CN110444348B (en) | Hydraulic bottom automatic disc feeding and discharging device | |
| CN211309048U (en) | Automatic film winding machine for medicine packaging | |
| CN102583112B (en) | Wheel changing device | |
| CN108178017A (en) | A kind of bobbin winder device of electric wire | |
| CN102795499A (en) | Automatic reeling device of compound machine | |
| CN207293800U (en) | A kind of elastic webbing automatic reeling machine | |
| CN209998127U (en) | Upper and lower disc device of copper wire drawing machine | |
| CN108820970A (en) | One kind being packed for bubble film winder | |
| CN105024501A (en) | Automatic stator coil winding machine | |
| CN108328397A (en) | A kind of automatic rolling device of woven bag | |
| CN103337359B (en) | High-power transformer coil manufactures the pneumatic conducting wire tensioning device of walking | |
| CN112278416A (en) | Automatic non-woven fabric packaging device and working method thereof | |
| CN208199912U (en) | A kind of automatic rolling device of woven bag | |
| CN105356691A (en) | Winding machine for automobile engine stator foldable coils | |
| CN201808956U (en) | Cloth pulling device for cloth storage rack | |
| CN206763631U (en) | A kind of copper wire take-up device being switched fast | |
| CN215207773U (en) | Automatic winding equipment for frying basket | |
| CN104787611A (en) | Film splitting machine | |
| CN210456973U (en) | Round wire collecting device | |
| CN217788101U (en) | Cable wrapping device |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20130821 Termination date: 20210204 |