CN203091448U - Ultra-thin two-sided buckle aluminium profile extrusion die - Google Patents
Ultra-thin two-sided buckle aluminium profile extrusion die Download PDFInfo
- Publication number
- CN203091448U CN203091448U CN 201320015035 CN201320015035U CN203091448U CN 203091448 U CN203091448 U CN 203091448U CN 201320015035 CN201320015035 CN 201320015035 CN 201320015035 U CN201320015035 U CN 201320015035U CN 203091448 U CN203091448 U CN 203091448U
- Authority
- CN
- China
- Prior art keywords
- die
- ultra
- thin
- utility
- model
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- XAGFODPZIPBFFR-UHFFFAOYSA-N aluminium Chemical compound [Al] XAGFODPZIPBFFR-UHFFFAOYSA-N 0.000 title claims abstract description 12
- 229910052782 aluminium Inorganic materials 0.000 title claims abstract description 12
- 239000004411 aluminium Substances 0.000 title abstract description 4
- 238000001125 extrusion Methods 0.000 title abstract 2
- 239000000463 material Substances 0.000 claims description 8
- 238000003466 welding Methods 0.000 abstract 1
- 238000007599 discharging Methods 0.000 description 6
- 238000000465 moulding Methods 0.000 description 4
- 238000010586 diagram Methods 0.000 description 2
- 238000007493 shaping process Methods 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 1
- 239000007787 solid Substances 0.000 description 1
Images


Landscapes
- Moulds, Cores, Or Mandrels (AREA)
Abstract
The utility model discloses an ultra-thin two-sided buckle aluminium profile extrusion die which comprises an upper die and a lower die, wherein the upper die is composed of diversion holes and a working head; two diversion holes are distributed on the upper die, the two diversion holes are distributed in an up-and-down symmetrical mode, and the working head is supported by using a smooth circular arc structure design; the lower die is composed of a welding chamber, a forming hole and a discharge outlet; the discharge outlet is formed below the forming hole; and the upper and lower dies are ultra-short parallel working strips with a length of 1.0 millimeter. According to the utility model, the forming degree and the service life of the die can be effectively improved.
Description
Technical field
The utility model relates to a kind of extruding die for aluminum shaped material, is specifically related to a kind of extruding die for aluminum shaped material of producing the ultrathin double-face buckle, belongs to the aluminium section die technical field.
Background technology
The ultrathin double-face buckle is aluminium section bar a kind of section bar commonly used.Before the utility model was made, traditional ultrathin double-face buckle extruding die for aluminum shaped material was difficult for being shaped, and service life is short.
Summary of the invention
The purpose of this utility model just provides a kind of easy shaping, the ultrathin double-face buckle extruding die for aluminum shaped material of long service life.
This ultrathin double-face buckle extruding die for aluminum shaped material comprises two parts of upper die and lower die; Patrix is made of tap hole, foreman; Be distributed with 2 tap holes on it, described tap hole is symmetrically distributed up and down, and described foreman supports and adopts smooth arc structure design; Counterdie is made of seam chamber, moulding hole, discharging opening; Described discharging opening is below the moulding hole; Described upper and lower mould adopts ultrashort 1.0 millimeters multiple operation bands.
The utility model compared with prior art, its characteristics are: the patrix foreman supports and adopts smooth arc structure design, and upper and lower mould adopts ultrashort 1.0 millimeters multiple operation bands, the shaping degree and the service life of having improved mould effectively.
Description of drawings
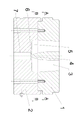
Fig. 1 is a normal cross-section structural representation of the present utility model.
Fig. 2 be among Fig. 1 A-A to the sectional structure schematic diagram.
Fig. 3 be among Fig. 1 B-B to the sectional structure schematic diagram.
Fig. 4 is a ultrathin double-face buckle section material section shape.
The specific embodiment
The specific embodiment of the present utility model: referring to Fig. 1, Fig. 2, Fig. 3, the utility model comprises patrix 1 and 2 two parts of counterdie; Patrix 1 is made of tap hole 3, foreman 4; Be distributed with 2 tap holes on it, described tap hole is symmetrically distributed up and down, and described foreman supports and adopts smooth arc structure design; Counterdie 2 is made of seam chamber 5, moulding hole 6, discharging opening 7; Described discharging opening 7 is below moulding hole 6.Soft solid aluminum enters counterdie seam chamber 5 via two tap holes 3 up and down, cooperates the profile shapes that with following mold forming hole 6 through the patrix foreman 4 who adopts smooth arc structure design again, passes through discharging opening 7 dischargings at last.Described upper and lower mould is fixed into one by four pins 8 and two screws 9.
Claims (1)
1. ultrathin double-face buckle extruding die for aluminum shaped material comprises two parts of upper die and lower die; Its characteristics are: the patrix foreman supports and adopts smooth arc structure design, and upper and lower mould adopts ultrashort 1.0 millimeters multiple operation bands.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320015035 CN203091448U (en) | 2013-01-12 | 2013-01-12 | Ultra-thin two-sided buckle aluminium profile extrusion die |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201320015035 CN203091448U (en) | 2013-01-12 | 2013-01-12 | Ultra-thin two-sided buckle aluminium profile extrusion die |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN203091448U true CN203091448U (en) | 2013-07-31 |
Family
ID=48842892
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201320015035 Expired - Fee Related CN203091448U (en) | 2013-01-12 | 2013-01-12 | Ultra-thin two-sided buckle aluminium profile extrusion die |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN203091448U (en) |
Cited By (1)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114505362A (en) * | 2022-01-20 | 2022-05-17 | 佛山市三水凤铝铝业有限公司 | Hot extrusion die |
-
2013
- 2013-01-12 CN CN 201320015035 patent/CN203091448U/en not_active Expired - Fee Related
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN114505362A (en) * | 2022-01-20 | 2022-05-17 | 佛山市三水凤铝铝业有限公司 | Hot extrusion die |
| CN114505362B (en) * | 2022-01-20 | 2023-11-21 | 佛山市三水凤铝铝业有限公司 | Hot extrusion die |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN203400953U (en) | High-yield hot extrusion die for thin-wall small round tube type aluminum section bars | |
| CN204093928U (en) | One-time formed circle_curling die tool | |
| CN107824627B (en) | Adjustable support aluminium section hot-extrusion die | |
| CN202316623U (en) | Extrusion mold | |
| CN204934229U (en) | A kind of 7075 aluminium alloy extrusion moulds | |
| CN204486494U (en) | Heavy in section Thin-walled Aluminum profile extrusion die | |
| CN205008411U (en) | Hot extrusion die of cantilever frame | |
| CN104942033A (en) | Large thin-wall square tube extrusion mold | |
| CN104001749A (en) | Continuous extrusion mold for C-shaped slot row | |
| CN203695637U (en) | Extrusion mold for compartment door profile | |
| CN203018546U (en) | Rapid small-hole punch pin improvement structure | |
| CN204122505U (en) | A kind of C type groove row die for continuously extruding | |
| CN204220660U (en) | Two-chip type structure hot-extrusion mold | |
| CN204074771U (en) | A kind of Cold Extrusion Punch of freewheel hub | |
| CN204620665U (en) | Square sunflower radiating rib the Aluminum-Extruding Die | |
| CN203994822U (en) | A kind of low degree of eccentricity propellant spiral shell molding die | |
| CN208772183U (en) | A kind of reverse extrusion mold | |
| CN203221079U (en) | Composite heat extrusion mould structure of aluminum alloy pull rod | |
| CN203018478U (en) | Dragon plate aluminum section extrusion die | |
| CN203109171U (en) | Mold core | |
| CN206215687U (en) | A kind of hot extrusion monoblock type aluminium sheet mould | |
| CN207668416U (en) | A kind of external screw thread double bond slot forging piece molding die | |
| CN206215684U (en) | The series hard metal of hot extrusion 7 shunts mould | |
| CN203018480U (en) | Single tube door sheet aluminum section extrusion die | |
| CN203018479U (en) | Aluminum section extrusion die for frame of LED (light-emitting diode) display screen |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20130731 Termination date: 20150112 |
|
| EXPY | Termination of patent right or utility model |