The residual neat recovering system of phase-change heat-exchanger and low-pressure coal saver associating
Technical field
The utility model relates to a kind of residual neat recovering system, especially relates to the residual neat recovering system of a kind of phase-change heat-exchanger and low-pressure coal saver associating, is mainly used in reclaiming the waste heat in the flue gases such as thermal power plant, metallurgy, petrochemical industry.
Background technology
China is in the world one of maximum greenhouse gas emission state at present; " energy-saving and emission-reduction " are important core of Chinese society economic development during " 12 ", are energy savings, the essential measure that reduces carbon emission, protection of the environment and improve energy utilization rate, strengthen heat recovery.
As everyone knows, contain sulfur trioxide (SO in the flue gas of coal-burning power plant, metallurgy, petrochemical industry discharging
3), the too low meeting of exhaust gas temperature causes the wall of heat exchanger heating surface that acid occurs and reveals corrosion and stifled ash, so the flue-gas temperature of discharging should not be too low, general way is to adopt to improve exhaust gas temperature or improve EAT to alleviate the problem of heat exchanger heating surface cold end corrosion, but can make like this efficient of using energy source lower, cause certain energy waste.
How to greatest extent Mist heat recovering, can avoid again heat exchanger heat exchange wall generation dewing corrosion and stifled ash simultaneously, becomes the focal issue that this art engineering staff pays close attention to.the device of Mist heat recovering is to greatest extent now also arranged, it was on 09 12nd, 2012 as open day, publication number is in the Chinese patent of CN202432505U, a kind of fire coal boiler fume waste heat recycling system is disclosed, this fire coal boiler fume waste heat recycling system economizer is set to be arranged in parallel main economizer and the bypass economizer between exhanst gas outlet and deduster, the air preheater that is connected with the fan outlet place of Secondary Air is arranged on main economizer, arrange in turn to water-to-water heat exchanger along the flue gas circulating direction on the bypass economizer, the condensate water heat exchanger, be arranged in parallel for water-to-water heat exchanger and arbitrary high-pressure heater, condensate water heat exchanger and arbitrary low-pressure heater are arranged in parallel, the cold wind heat exchanger at the fan outlet place that is connected to Secondary Air of closed cycle is set between air-introduced machine and desulfuration absorbing tower, according to the cascaded utilization of energy principle, be used with different approaches respectively for heat and the more inferior heat of higher quality, improved heat recovery rate in flue gas, but be difficult to prevent that flue gas from revealing corrosion to the acid of equipment.
Now also have and to prevent that flue gas is to the waste-heat recovery device of equipment dewing corrosion, it was on 05 04th, 2011 as open day, publication number is in the Chinese patent of CN201819198U, a kind of high-low pressure combined-type economizer is disclosed, this high-low pressure combined-type economizer comprises by smoke gas flow is located at the first high-pressure economizer, air preheater and low-pressure coal saver in flue successively through direction, also comprise second high-pressure economizer of connecting with the first high-pressure economizer, the second high-pressure economizer is connected with the feed water system of boiler; Low-pressure coal saver is connected with a heat exchanger, and the boiler supply air system is connected with air preheater by heat exchanger; Although although this high-low pressure combined-type economizer can prevent flue gas, corrosion is revealed in the acid of equipment,, employing be all economizer, the raising of heat exchange efficiency and intensity is remarkable not, the size of heat exchanger is larger, manufacturing cost is higher.
In sum, also there is no at present a kind of reasonable in design, dependable performance, Mist heat recovering to greatest extent can be avoided again the residual neat recovering system of heat exchanger heat exchange wall generation cold end corrosion.
The utility model content
The purpose of this utility model is to overcome above shortcomings in prior art, and provide a kind of reasonable in design, dependable performance, Mist heat recovering, can avoid again the phase-change heat-exchanger of heat exchanger heat exchange wall generation cold end corrosion and the residual neat recovering system of low-pressure coal saver associating to greatest extent.
the technical scheme in the invention for solving the above technical problem is: the residual neat recovering system of this phase-change heat-exchanger and low-pressure coal saver associating comprises the flue gas flue, terminal control unit, down-comer, tedge, be provided with the low-pressure coal saver of heat-exchange working medium import and high temperature heat-exchange working medium outlet, be provided with the phase-change heat-exchanger of saturated vapor outlet and condensing water inlet, and the phase-change heat-exchange drum that is provided with saturated vapor entrance, condensation-water drain, the import of low-temperature heat exchange working medium and heat-exchange working medium outlet, its design feature is: also comprise phase-change heat-exchanger tail flue gas temperature measurer, tedge medium temperature measurer, down-comer medium temperature measurer, low-temperature heat exchange working medium control valve, economizer heat exchange drum tube connector, the economizer tube connector, heat exchange drum tube connector, the heat-exchange working medium temperature measurer, the heat-exchange working medium control valve, high temperature heat-exchange working medium temperature measurer, high temperature heat-exchange working medium control valve and low-temperature heat exchange working medium temperature measurer, described low-pressure coal saver and phase-change heat-exchanger are installed in the flue gas flue, described phase-change heat-exchanger tail flue gas temperature measurer is arranged on the flue gas flue, described low-pressure coal saver, phase-change heat-exchanger and phase-change heat-exchanger tail flue gas temperature measurer are arranged in order along the flow of flue gas direction, described phase-change heat-exchange drum is positioned at above the flue gas flue, the upper end of described down-comer is connected on the condensation-water drain of phase-change heat-exchange drum, the lower end of this down-comer is connected on the condensing water inlet of phase-change heat-exchanger, and described down-comer medium temperature measurer is arranged on down-comer, the upper end of described tedge is connected on the saturated vapor entrance of phase-change heat-exchange drum, and the lower end of this tedge is connected in the saturated vapor outlet of phase-change heat-exchanger, and described tedge medium temperature measurer is arranged on tedge, the upper end of described economizer heat exchange drum tube connector is connected in the heat-exchange working medium outlet of phase-change heat-exchange drum, the lower end of this economizer heat exchange drum tube connector is connected in the heat-exchange working medium import of low-pressure coal saver, and described heat-exchange working medium temperature measurer and heat-exchange working medium control valve are installed on economizer heat exchange drum tube connector, one end of described heat exchange drum tube connector is connected in the low-temperature heat exchange working medium import of phase-change heat-exchange drum, described low-temperature heat exchange working medium control valve and low-temperature heat exchange working medium temperature measurer are installed on heat exchange drum tube connector, one end of described economizer tube connector is connected in the high temperature heat-exchange working medium outlet of low-pressure coal saver, and described high temperature heat-exchange working medium temperature measurer and high temperature heat-exchange working medium control valve are installed on the economizer tube connector, described terminal control unit is wired on phase-change heat-exchanger tail flue gas temperature measurer, tedge medium temperature measurer, down-comer medium temperature measurer and low-temperature heat exchange working medium control valve.
As preferably, heat-exchange working medium outlet described in the utility model, heat-exchange working medium temperature measurer, heat-exchange working medium control valve and heat-exchange working medium import are arranged in order.
As preferably, low-temperature heat exchange working medium control valve described in the utility model, low-temperature heat exchange working medium temperature measurer and the import of low-temperature heat exchange working medium are arranged in order.
As preferably, high temperature heat-exchange working medium control valve described in the utility model, high temperature heat-exchange working medium temperature measurer and the outlet of high temperature heat-exchange working medium are arranged in order.
As preferably, heat-exchange working medium control valve described in the utility model is the hand-operated valve structure.
As preferably, high temperature heat-exchange working medium control valve described in the utility model is the hand-operated valve structure.
As preferably, phase-change heat-exchange drum described in the utility model be positioned at phase-change heat-exchanger directly over.
The utility model compared with prior art, have the following advantages and effect: 1, adopt the phase-change heat-exchange technology, heat exchange efficiency and intensity have obtained significant raising with respect to traditional heat exchangers, can greatly dwindle size of heat exchanger, save heat exchanger materials, save the heat exchanger cost.
2, adopt phase-change heat-exchanger and low-pressure coal saver combined technology, can be that restrictive condition is regulated the heat-exchange working medium amount that enters the phase-change heat-exchange drum according to the phase-change heat-exchanger wall temperature, make phase-change heat-exchanger heat exchange wall surface temperature all the time higher than flue gas acid dew point, thereby avoid the cold end corrosion of phase-change heat-exchanger heat exchange wall, heat-exchange working medium through the heating of phase-change heat-exchange drum passes into low-pressure coal saver again, can make low-pressure coal saver heat exchange wall surface temperature also all the time higher than flue gas acid dew point, also can avoid the cold end corrosion of low-pressure coal saver heat exchange wall.
3, the technology that combines with low-pressure coal saver by phase-change heat-exchanger, lifting heat-exchange working medium temperature that can be larger, Mist heat recovering to greatest extent, the better economy of recovery.
4, can regulate according to the thermal source working conditions change, adaptability is good.
5, realize the waste gas residual heat recycling, had the good economic value of environmental protection.
As from the foregoing, reasonable in design of the present utility model, by pipeline, valve and temperature measurer, phase-change heat-exchanger and low-pressure coal saver are combined, make the utility model Mist heat recovering to greatest extent, can avoid again heat exchanger heat exchange wall generation cold end corrosion, greatly promote the overall performance of residual neat recovering system.The utility model is on structure, be not only single phase-change heat-exchanger and single low-pressure coal saver simple combination, the utility model is on function, be not only also the function of single phase-change heat-exchanger and the function sum of single low-pressure coal saver, but will be far longer than the function of single phase-change heat-exchanger and the function sum of single low-pressure coal saver.
Description of drawings
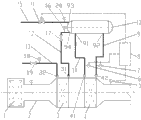
Fig. 1 is the structural representation of the residual neat recovering system of phase-change heat-exchanger and low-pressure coal saver associating in the utility model embodiment.
Fig. 2 is that the residual neat recovering system in Fig. 1 is marked with the structural representation that working medium flows to.
in figure: the 1-air preheater, 2-flue gas flue, the 3-low-pressure coal saver, the 4-phase-change heat-exchanger, 5-phase-change heat-exchanger tail flue gas temperature measurer, 6-tedge medium temperature measurer, 7-down-comer medium temperature measurer, the 8-terminal control unit, the 9-down-comer, 10-phase-change heat-exchange drum, 11-low-temperature heat exchange working medium control valve, 12-economizer heat exchange drum tube connector, 13-economizer tube connector, the 14-tedge, 15-heat exchange drum tube connector, 16-heat-exchange working medium temperature measurer, 17-heat-exchange working medium control valve, 18-high temperature heat-exchange working medium temperature measurer, 19-high temperature heat-exchange working medium control valve, 20-low-temperature heat exchange working medium temperature measurer, the import of 31-heat-exchange working medium, the outlet of 32-high temperature heat-exchange working medium, the outlet of 41-saturated vapor, the 42-condensing water inlet, 91-saturated vapor entrance, the 92-condensation-water drain, the import of 93-low-temperature heat exchange working medium, the outlet of 94-heat-exchange working medium.
The specific embodiment
The utility model is described in further detail below in conjunction with accompanying drawing and by embodiment, and following examples are to explanation of the present utility model and the utility model is not limited to following examples.
Embodiment.
referring to Fig. 1 to Fig. 2, the residual neat recovering system of the phase-change heat-exchanger in the present embodiment and low-pressure coal saver associating comprises air preheater 1, flue gas flue 2, low-pressure coal saver 3, phase-change heat-exchanger 4, phase-change heat-exchanger tail flue gas temperature measurer 5, tedge medium temperature measurer 6, down-comer medium temperature measurer 7, terminal control unit 8, down-comer 9, phase-change heat-exchange drum 10, low-temperature heat exchange working medium control valve 11, economizer heat exchange drum tube connector 12, economizer tube connector 13, tedge 14, heat exchange drum tube connector 15, heat-exchange working medium temperature measurer 16, heat-exchange working medium control valve 17, high temperature heat-exchange working medium temperature measurer 18, high temperature heat-exchange working medium control valve 19 and low-temperature heat exchange working medium temperature measurer 20.
Be provided with heat-exchange working medium import 31 and high temperature heat-exchange working medium outlet 32 in low-pressure coal saver 3 in the present embodiment, be provided with saturated vapor outlet 41 and condensing water inlet 42 in phase-change heat-exchanger 4, be provided with saturated vapor entrance 91, condensation-water drain 92, the import 93 of low-temperature heat exchange working medium and heat-exchange working medium outlet 94 in phase-change heat-exchange drum 10.
Low-pressure coal saver 3 in the present embodiment and phase-change heat-exchanger 4 are installed in flue gas flue 2, phase-change heat-exchanger tail flue gas temperature measurer 5 is arranged on flue gas flue 2, and low-pressure coal saver 3, phase-change heat-exchanger 4 and phase-change heat-exchanger tail flue gas temperature measurer 5 are arranged in order along the flow of flue gas direction.
Phase-change heat-exchange drum 10 in the present embodiment is positioned at flue gas flue 2 tops, generally, this phase-change heat-exchange drum 10 be positioned at phase-change heat-exchanger 4 directly over.The upper end of down-comer 9 is connected on the condensation-water drain 92 of phase-change heat-exchange drum 10, and the lower end of this down-comer 9 is connected on the condensing water inlet 42 of phase-change heat-exchanger 4, and down-comer medium temperature measurer 7 is arranged on down-comer 9.
The upper end of the tedge 14 in the present embodiment is connected on the saturated vapor entrance 91 of phase-change heat-exchange drum 10, and the lower end of this tedge 14 is connected in the saturated vapor outlet 41 of phase-change heat-exchanger 4, and tedge medium temperature measurer 6 is arranged on tedge 14.
The upper end of the economizer heat exchange drum tube connector 12 in the present embodiment is connected in the heat-exchange working medium outlet 94 of phase-change heat-exchange drum 10, the lower end of this economizer heat exchange drum tube connector 12 is connected in the heat-exchange working medium import 31 of low-pressure coal saver 3, heat-exchange working medium temperature measurer 16 and heat-exchange working medium control valve 17 are installed on economizer heat exchange drum tube connector 12, and heat-exchange working medium outlet 94, heat-exchange working medium temperature measurer 16, heat-exchange working medium control valve 17 and heat-exchange working medium import 31 are arranged in order.Heat-exchange working medium control valve 17 in the present embodiment is the hand-operated valve structure.
One end of the heat exchange drum tube connector 15 in the present embodiment is connected in the low-temperature heat exchange working medium import 93 of phase-change heat-exchange drum 10, low-temperature heat exchange working medium control valve 11 and low-temperature heat exchange working medium temperature measurer 20 are installed on heat exchange drum tube connector 15, and low-temperature heat exchange working medium control valve 11, low-temperature heat exchange working medium temperature measurer 20 and low-temperature heat exchange working medium import 93 are arranged in order.
One end of the economizer tube connector 13 in the present embodiment is connected in the high temperature heat-exchange working medium outlet 32 of low-pressure coal saver 3, high temperature heat-exchange working medium temperature measurer 18 and high temperature heat-exchange working medium control valve 19 are installed on economizer tube connector 13, and high temperature heat-exchange working medium control valve 19, high temperature heat-exchange working medium temperature measurer 18 and high temperature heat-exchange working medium outlet 32 are arranged in order.High temperature heat-exchange working medium control valve 19 in the present embodiment is the hand-operated valve structure.
Terminal control unit 8 in the present embodiment is wired on phase-change heat-exchanger tail flue gas temperature measurer 5, tedge medium temperature measurer 6, down-comer medium temperature measurer 7 and low-temperature heat exchange working medium control valve 11.
Residual neat recovering system in the present embodiment in use, air preheater 1 is installed on flue gas flue 2, low-pressure coal saver 3 and phase-change heat-exchanger 4 are placed in flue gas flue 2, on the flow of flue gas direction, before low-pressure coal saver 3 is placed in phase-change heat-exchanger 4, phase-change heat-exchanger 4 back-end ductworks are equipped with phase-change heat-exchanger tail flue gas temperature measurer 5, and namely air preheater 1, low-pressure coal saver 3, phase-change heat-exchanger 4 and phase-change heat-exchanger tail flue gas temperature measurer 5 are arranged in order along the flow of flue gas direction.Phase-change heat-exchange drum 10 is placed in outside flue gas flue 2, and be positioned at the top of phase-change heat-exchanger 4, phase-change heat-exchange drum 10 forms certain difference in height with phase-change heat-exchanger 4, are connected with down-comer by tedge 14 and are connected with phase-change heat-exchanger 4, form a closed loop, on tedge 14 and down-comer 9, temperature measurer is housed all.the heat-exchange working medium import 31 of low-pressure coal saver 3 is connected with the heat-exchange working medium outlet 94 of phase-change heat-exchange drum 10 by economizer heat exchange drum tube connector 12, external heat-exchanging working medium enters phase-change heat-exchange drum 10 by heat exchange drum tube connector 15, pick out by the high temperature heat-exchange working medium outlet 32 of economizer tube connector 13 from low-pressure coal saver 3 again, on the heat exchange drum tube connector 15 of external heat-exchanging working medium access phase-change heat-exchange drum 10, low-temperature heat exchange working medium control valve 11 is housed, low-temperature heat exchange working medium control valve 11 is by terminal control unit 8 control connections, terminal control unit 8 is by wire and the tedge medium temperature measurer 6 that is arranged on tedge 14, down-comer medium temperature measurer 7 on down-comer 9, and the phase-change heat-exchanger tail flue gas temperature measurer 5 on flue gas flue 2 is connected.Residual neat recovering system in the present embodiment makes phase-change heat-exchanger 4 wall surface temperatures higher than flue gas acid dew point in flue gas low-temperature zone employing phase-change heat-exchange technology, avoids heat exchanger cold end corrosion problem; Promote to greatest extent at fume high-temperature zone employing low-pressure coal saver 3 and be heated Temperature of Working, residual neat recovering system by phase-change heat-exchanger 4 and low-pressure coal saver 3 associatings can fully carry out flue gas heat recovery, for flue gas waste heat recovery and energy-saving and emission-reduction provide a kind of reliable, economic method.
Low-pressure coal saver 3 and phase-change heat-exchanger 4 in the present embodiment are placed in flue gas flue 2, before on the flow of flue gas direction, low-pressure coal saver 3 is arranged in phase-change heat-exchanger 4, phase-change heat-exchanger tail flue gas temperature measurer 5 is housed on the flue gas flue 2 of phase-change heat-exchanger 4 afterbodys, flue gas in flue gas flue 2 flow through successively low-pressure coal saver 3 and phase-change heat-exchanger 4, carry out heat exchange with the heat-exchange working medium of the low-pressure coal saver 3 of flowing through, with the heat-exchange working medium heat temperature raising; Carry out heat exchange with the heat-exchange working medium in phase-change heat-exchanger 4, the heat-exchange working medium heating is produced saturated vapor; After the two-stage heat exchange, flue-gas temperature reduces, and the phase-change heat-exchanger tail flue gas temperature measurer 5 on the flue gas flue 2 of phase-change heat-exchanger 4 afterbodys is used for the flue-gas temperature of monitoring after the residual heat system cooling.
Phase-change heat-exchange drum 10 in the present embodiment is placed in outside flue gas flue 2, and phase-change heat-exchanger 4 top positions places make it that to form certain altitudes poor with phase-change heat-exchanger 4, are connected with down-comer by tedge 14 to be connected with phase-change heat-exchanger 4, and the closed circuit of a closure of formation.The saturated vapor that phase-change heat-exchanger 4 produces is pooled in phase-change heat-exchange drum 10 by tedge 14; Outside heat-exchange working medium after carrying out heat exchange with saturated vapor, accesses low-pressure coal saver 3 by heat exchange drum tube connector 15 access phase-change heat-exchange drums 10; The saturated vapor heat exchange is cooled to heat-exchange working medium, under action of gravitation, be back to phase-change heat-exchanger 4 by down-comer 9, the tedge medium temperature measurer 6 on tedge 14 and the down-comer medium temperature measurer 7 on down-comer 9 are respectively used to monitor medium temperature and the interior medium temperature of down-comer 9 in tedge 14.
The present embodiment picks out by economizer tube connector 13 through the heat-exchange working medium of low-pressure coal saver 3 heat temperature raisings, and high temperature heat-exchange working medium temperature measurer 18 is housed on economizer tube connector 13, monitors by 18 pairs of Temperature of Workings of high temperature heat-exchange working medium temperature measurer.
on the heat exchange drum tube connector 15 of the external heat-exchanging working medium access phase-change heat-exchange drum 10 of the present embodiment, low-temperature heat exchange working medium control valve 11 is housed, low-temperature heat exchange working medium control valve 11 is connected with terminal control unit 8 by wire, terminal control unit 8 is by wire and the tedge medium temperature measurer 6 that is arranged on tedge 14, be arranged on the down-comer medium temperature measurer 7 on down-comer 9, and the phase-change heat-exchanger tail flue gas temperature measurer 5 that is arranged on flue gas flue 2 is connected, terminal control unit 8 is regulated the aperture of low-temperature heat exchange working medium control valve 11 according to the feedback information of these three temperature measurers, enter the heat-exchange working medium amount of phase-change heat-exchange drum 10 with control.
Residual neat recovering system in the present embodiment is when operation, external heat-exchanging working medium passes into phase-change heat-exchange drum 10, carry out heat exchange 10 li of phase-change heat-exchange drums with the saturated vapor that produces from phase-change heat-exchanger 4, after saturated vapor is cooled into condensation working medium, get back to phase-change heat-exchanger 4 under action of gravitation, then carry out heat exchange and absorb flue gas heat with flue gas in flue gas flue 2, further reduce the temperature of flue gas, make condensation working medium be heated the formation saturated vapor and enter phase-change heat-exchange drum 10, so circulation.Heat-exchange working medium is heated 10 li of phase-change heat-exchange drums, enter low-pressure coal saver 3 by economizer heat exchange drum tube connector 12, carry out heat exchange at 3 li of low-pressure coal savers and flue gas in flue gas flue 2, reduce flue-gas temperature, heat-exchange working medium is further heated intensification, picks out outside system afterwards.After the heat exchange of two-stage heat exchanger, heat-exchange working medium can be heated to higher temperature, and significantly Mist heat recovering, can avoid again this two-stage heat exchanger heat exchange wall generation cold end corrosion simultaneously.
the utility model is arranged in the temperature of the heat-exchange working medium of heat exchange drum tube connector 15, be arranged in the temperature of the heat-exchange working medium of economizer heat exchange drum tube connector 12, and the temperature that is arranged in the heat-exchange working medium of economizer tube connector 13 raises successively, namely enter the temperature of heat-exchange working medium of phase-change heat-exchange drum 10 from low-temperature heat exchange working medium import 93 relatively low, and it is relatively high from the temperature of the heat-exchange working mediums of high temperature heat-exchange working medium outlet 32 outputs, that is to say that herein high temperature and low temperature are comparatively speaking, therefore the utility model is at low-temperature heat exchange working medium control valve 11, in the title of low-temperature heat exchange working medium temperature measurer 20 and low-temperature heat exchange working medium import 93 titled with " low temperature " two words, and at high temperature heat-exchange working medium temperature measurer 18, in the title of high temperature heat-exchange working medium control valve 19 and high temperature heat-exchange working medium outlet 32 titled with " high temperature " two words.
In addition, need to prove, the specific embodiment described in this specification, the shape of its parts and components, institute's title of being named etc. can be different, and the above content described in this specification is only to the explanation of the utility model structure example.All equivalence variation or simple change of doing according to the described structure of the utility model patent design, feature and principle are included in the protection domain of the utility model patent.The utility model person of ordinary skill in the field can make various modifications or replenishes or adopt similar mode to substitute described specific embodiment; only otherwise depart from structure of the present utility model or surmount this scope as defined in the claims, all should belong to protection domain of the present utility model.