CN202917252U - Tin mechanism - Google Patents

Tin mechanism Download PDF

Info

Publication number
CN202917252U
CN202917252U CN 201220546821 CN201220546821U CN202917252U CN 202917252 U CN202917252 U CN 202917252U CN 201220546821 CN201220546821 CN 201220546821 CN 201220546821 U CN201220546821 U CN 201220546821U CN 202917252 U CN202917252 U CN 202917252U
Authority
CN
China
Prior art keywords
furnace
wire pressing
tinning
crimping
tin
Prior art date
Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
Expired - Lifetime
Application number
CN 201220546821
Other languages
Chinese (zh)
Inventor
甘宝连
Current Assignee (The listed assignees may be inaccurate. Google has not performed a legal analysis and makes no representation or warranty as to the accuracy of the list.)
Dongguan Senjia Machinery Co ltd
Original Assignee
Dongguan Senjia Machinery Co ltd
Priority date (The priority date is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the date listed.)
Filing date
Publication date
Application filed by Dongguan Senjia Machinery Co ltd filed Critical Dongguan Senjia Machinery Co ltd
Priority to CN 201220546821 priority Critical patent/CN202917252U/en
Application granted granted Critical
Publication of CN202917252U publication Critical patent/CN202917252U/en
Anticipated expiration legal-status Critical
Expired - Lifetime legal-status Critical Current

Links

Images

Landscapes

  • Wire Processing (AREA)

Abstract

本实用新型公开了上锡机构,属于电线加工生产领域。它包括第一气缸、压线连杆、压线平台、助焊剂炉和上锡炉;压线连杆平行设置压线平台上端,压线连杆下端设有压线头,压线头相对于压线平台内侧面突出,使压线头下压时会将电线折弯上助焊剂或上锡;压线连杆通过第一气缸驱动垂直移动,带动压线头下压上助焊剂或上锡;助焊剂炉和上锡炉设在压线平台下方。该上锡机构,能够自动上助焊剂,再自动上锡操作。

Figure 201220546821

The utility model discloses a tinning mechanism, which belongs to the field of wire processing and production. It comprises a first cylinder, a wire pressing connecting rod, a wire pressing platform, a flux furnace and a tinning furnace; the wire pressing connecting rod is arranged parallel to the upper end of the wire pressing platform, and a wire pressing head is arranged at the lower end of the wire pressing connecting rod, and the wire pressing head protrudes relative to the inner side of the wire pressing platform, so that when the wire pressing head is pressed down, the wire will be bent and fluxed or tinned; the wire pressing connecting rod is driven by the first cylinder to move vertically, driving the wire pressing head to press down and apply flux or tin; the flux furnace and the tinning furnace are arranged below the wire pressing platform. The tinning mechanism can automatically apply flux and then automatically perform tinning operations.

Figure 201220546821

Description

Upper tin mechanism
Technical field
The utility model relates to electric wire processing field, particularly relates to tin mechanism.
Background technology
After electric wire being turned round the line processing, need to carry out upper tin to electric wire and process, tin not only can be protected electric wire, also is easy to welding.Traditional technique first with upper scaling powder, goes up tin again, but traditional technique can only manual operation, causes tin efficient low, the labor intensive material resources.
The utility model content
For addressing the above problem, the utility model provides upper tin mechanism, can automatically go up scaling powder, again automatic tin operation.
Technical solution adopted in the utility model is: upper tin mechanism comprises the first cylinder, line pressing connecting rod, line ball platform, scaling powder stove and upper tin stove; Line pressing connecting rod arranges line ball platform upper end, and the line pressing connecting rod lower end is provided with the line ball head, and the line ball head is outstanding with respect to line ball platform medial surface, can be with scaling powder in the electric wire bending or upper tin when the line ball head is pressed down; Line pressing connecting rod is vertically mobile by the first air cylinder driven, drives and presses scaling powder or upper tin under the line ball head; Scaling powder stove and upper tin stove are located at line ball platform below.
In technique scheme, line pressing connecting rod be arranged in parallel on the line ball platform.
In technique scheme, upper tin mechanism also comprises the second cylinder; The second air cylinder driven scaling powder stove is vertical with upper tin stove mobile, makes scaling powder stove and upper tin stove can not stop mobile electric wire.
In technique scheme, upper tin mechanism also comprises vertical guide rail and slide block; Scaling powder stove and upper tin stove are fixed on the slide block, and slide block is connected on the vertical guide rail, and the second air cylinder driven slide block is mobile in vertical guide rail, and it is vertical with upper tin stove mobile to drive the scaling powder stove.
The beneficial effects of the utility model are: the upper tin mechanism of above-mentioned structure, and by the mode bending electric wire of line ball, contact scaling powder stove and upper tin stove are gone up scaling powder, again automatic tin automatically; The scaling powder stove can vertically move with upper tin stove, does not stop loading and unloading to be beneficial to automation; Can go up respectively scaling powder and upper tin to two electric wires, working (machining) efficiency is high.
Description of drawings
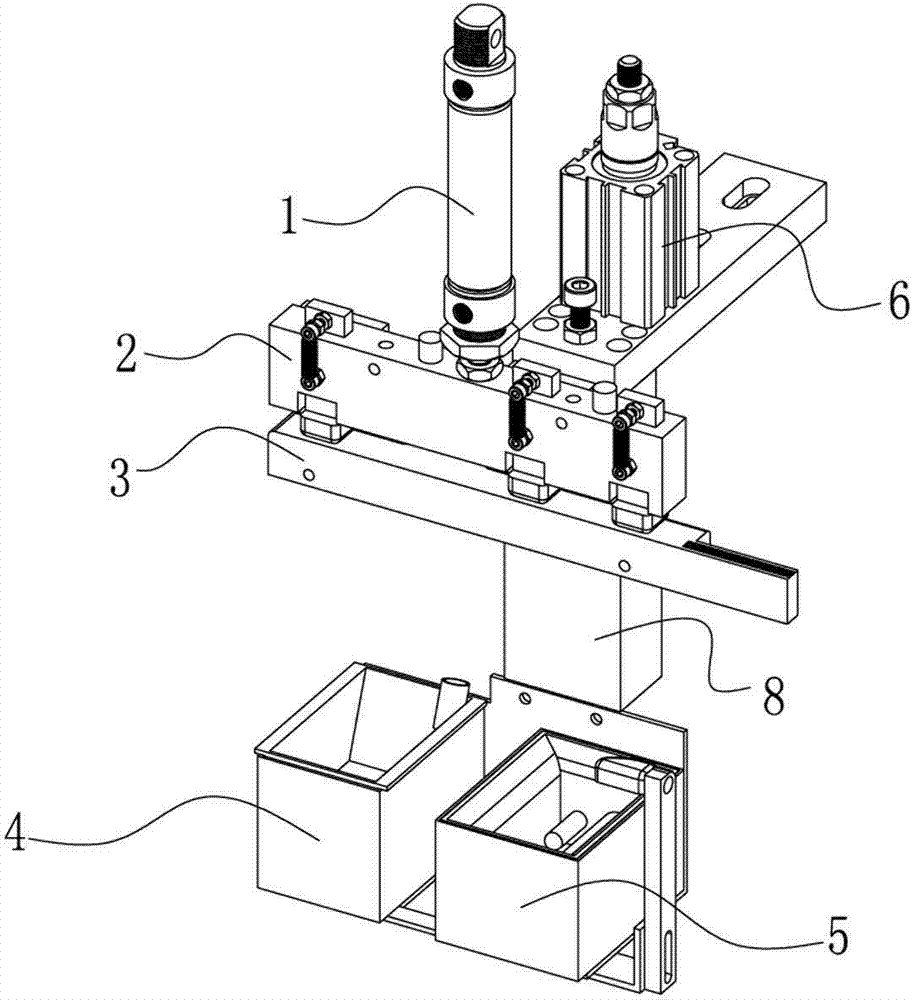
Fig. 1 is overall structure figure of the present utility model;
Fig. 2 is exploded view of the present utility model;
Fig. 3 is line ball head front view of the present utility model.
Among the figure, the 1, first cylinder; 2, line pressing connecting rod; 21, line ball head; 3, line ball platform; 4, scaling powder stove; 5, upper tin stove; 6, the second cylinder; 7, vertical guide rail; 8, slide block.
Embodiment
Below in conjunction with accompanying drawing the utility model is described in further detail.
Fig. 1 to Fig. 3 has schematically shown the upper tin mechanism according to a kind of execution mode of the present utility model.
Upward tin mechanism comprises the first cylinder 1, line pressing connecting rod 2, line ball platform 3, scaling powder stove 4, upper tin stove 5, the second cylinder 6, vertical guide rail 7 and slide block 8; Line pressing connecting rod 2 line ball platform 3 upper ends that be arranged in parallel, line pressing connecting rod 2 lower ends are provided with line ball head 21, line ball head 21 is outstanding with respect to line ball platform 3 medial surfaces, can be with scaling powder in the electric wire bending or upper tin when line ball head 21 is pressed down, and line ball head 21 front ends are a draw-in groove, line ball does not better allow electric wire walks when pressing down electric wire; Line pressing connecting rod 2 drives vertical mobile by the first cylinder 1, drive the line ball head and press scaling powder or upper tin for 21 times; Scaling powder stove 4 and upper tin stove 5 are located at line ball platform 3 belows; Scaling powder stove 4 and upper tin stove 5 are fixed on the slide block 8, scaling powder stove 4 is in upper tin stove 5 left sides, slide block 8 is connected on the vertical guide rail 7, the second cylinder 6 drives slide block 8 in vertical guide rail 7 interior movements and drives scaling powder stove 4 and upper tin stove 5 vertical moving, and makes scaling powder stove 4 and upper tin stove 5 can not stop mobile electric wire.
Above-mentioned, upper tin mechanism is by the blanking of stepper motor conveyer belt material loading.
When using the utility model, electric wire is by stepper motor conveyer belt material loading; First electric wire is sent to line ball platform 3 positions of scaling powder stove 4 tops, and relative line ball platform 3 medial surfaces of electric wire front end are outstanding; Line ball head 21 presses down electric wire, with the electric wire bending down; Scaling powder stove 4 rises, with scaling powder on the end in contact before the electric wire; After finishing scaling powder, scaling powder stove 4 descends; The electric wire of upper scaling powder is sent to line ball platform 3 positions of upper tin stove 5 tops, upper tin stove 5 rises again, tin on the end in contact before upper tin stove 5 and the electric wire; After finishing tin, electric wire is by the blanking of stepper motor conveyer belt.The utility model can be to the electric wire of not going up scaling powder and upper scaling powder but the electric wire of not going up tin operate simultaneously, working (machining) efficiency is high.
Above embodiment just is explanation rather than restriction the utility model, so all equivalences of doing according to the described method of the utility model patent claim change or modify, is included in the utility model patent claim.

Claims (4)

1.上锡机构,其特征在于,包括第一气缸、压线连杆、压线平台、助焊剂炉和上锡炉;所述压线连杆设置所述压线平台上端,所述压线连杆下端设有压线头,所述压线头相对于所述压线平台内侧面突出;所述压线连杆通过所述第一气缸驱动垂直移动,带动所述压线头下压上助焊剂或上锡;所述助焊剂炉和所述上锡炉设在所述压线平台下方。 1. The tinning mechanism is characterized in that it comprises a first cylinder, a crimping rod, a crimping platform, a flux furnace and a tinning furnace; the crimping rod is provided with the upper end of the crimping platform, and the crimping rod A crimping head is provided at the lower end of the connecting rod, and the crimping head protrudes relative to the inner surface of the crimping platform; the crimping connecting rod is driven to move vertically by the first cylinder, driving the crimping head to press down the flux or Tinning; the flux furnace and the tinning furnace are arranged under the crimping platform. 2.根据权利要求1所述的上锡机构,其特征在于:所述压线连杆平行设置所述压线平台上端。 2 . The tinning mechanism according to claim 1 , wherein the crimping rod is arranged parallel to the upper end of the crimping platform. 3 . 3.根据权利要求1所述的上锡机构,其特征在于:所述上锡机构还包括第二气缸;所述第二气缸驱动所述助焊剂炉和所述上锡炉垂直移动。 3. The tin loading mechanism according to claim 1, characterized in that: the tin loading mechanism further comprises a second air cylinder; the second air cylinder drives the flux furnace and the tin loading furnace to move vertically. 4.根据权利要求3所述的上锡机构,其特征在于:上锡机构还包括垂直导轨和滑块;所述助焊剂炉和所述上锡炉固定在所述滑块上,所述滑块连接在所述垂直导轨上,所述第二气缸驱动所述滑块在所述垂直导轨内移动,带动所述助焊剂炉和所述上锡炉垂直移动。 4. The tinning mechanism according to claim 3, characterized in that: the tinning mechanism also includes a vertical guide rail and a slider; the flux furnace and the tin furnace are fixed on the slider, and the slider The block is connected on the vertical guide rail, and the second cylinder drives the slider to move in the vertical guide rail, driving the flux furnace and the upper tin furnace to move vertically.
CN 201220546821 2012-10-24 2012-10-24 Tin mechanism Expired - Lifetime CN202917252U (en)

Priority Applications (1)

Application Number Priority Date Filing Date Title
CN 201220546821 CN202917252U (en) 2012-10-24 2012-10-24 Tin mechanism

Applications Claiming Priority (1)

Application Number Priority Date Filing Date Title
CN 201220546821 CN202917252U (en) 2012-10-24 2012-10-24 Tin mechanism

Publications (1)

Publication Number Publication Date
CN202917252U true CN202917252U (en) 2013-05-01

Family

ID=48165541

Family Applications (1)

Application Number Title Priority Date Filing Date
CN 201220546821 Expired - Lifetime CN202917252U (en) 2012-10-24 2012-10-24 Tin mechanism

Country Status (1)

Country Link
CN (1) CN202917252U (en)

Cited By (2)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN103551700A (en) * 2013-11-04 2014-02-05 昆山美连德电子科技有限公司 Wire harness weaving tin adhering machine
CN105935825A (en) * 2016-07-10 2016-09-14 霍丁格包尔文(苏州)电子测量技术有限公司 Automatic tin applying machine of strain gauge lead

Cited By (3)

* Cited by examiner, † Cited by third party
Publication number Priority date Publication date Assignee Title
CN103551700A (en) * 2013-11-04 2014-02-05 昆山美连德电子科技有限公司 Wire harness weaving tin adhering machine
CN103551700B (en) * 2013-11-04 2015-12-02 昆山美连德电子科技有限公司 A kind of wire harness braiding solder machine
CN105935825A (en) * 2016-07-10 2016-09-14 霍丁格包尔文(苏州)电子测量技术有限公司 Automatic tin applying machine of strain gauge lead

Similar Documents

Publication Publication Date Title
CN107262563B (en) Bending machine
CN201702776U (en) Manipulator for full-automatic sheet discharging machine
CN202278296U (en) Automatic spot welder
CN201446703U (en) Bender for plastic sheets
CN202917794U (en) European standard plug frame riveting mechanism
CN104741846A (en) A purely manual welding machine for shoemaking
CN204847370U (en) A loading attachment for producing window decoration lens
CN201353896Y (en) Full automatic creasing and cutting machine
CN204584527U (en) A kind of gate-type submerged arc welding machine
CN204320854U (en) Electronic transformer iron core shaping device
CN204075029U (en) Brush handle forming machine
CN205764701U (en) A kind of door of elevator production line
CN202384626U (en) Working pieces transmission mechanism on automatic processing equipment for DC plug
CN210703244U (en) Automatic change water-cooling wall and close welding set of shielding
CN205203522U (en) Automatic aluminium nail machine seals
CN203426560U (en) Automatic welding device for capacitor core
CN203185955U (en) OGS fine-carving machine
CN207282881U (en) A kind of line device of LED light strip automatic welding machine
CN202279525U (en) Automatic feeding device for paint spraying machine
CN202186743U (en) Chip mounting machine for manufacturing piezoresistor
CN207447172U (en) A kind of turnover clamping jaw to pre-bend for cell polar ear
CN201863389U (en) Hot-melt jig
CN204673144U (en) A kind of platform floor automatic welding line and robot welding system thereof
CN202917801U (en) twisted wire assembly
CN202150626U (en) Tin immersion structure of full-automatic fast pressing machine

Legal Events

Date Code Title Description
C14 Grant of patent or utility model
GR01 Patent grant
CX01 Expiry of patent term

Granted publication date: 20130501