CN202861747U - Bearing press fitting clamping fixture device - Google Patents
Bearing press fitting clamping fixture device Download PDFInfo
- Publication number
- CN202861747U CN202861747U CN 201220521868 CN201220521868U CN202861747U CN 202861747 U CN202861747 U CN 202861747U CN 201220521868 CN201220521868 CN 201220521868 CN 201220521868 U CN201220521868 U CN 201220521868U CN 202861747 U CN202861747 U CN 202861747U
- Authority
- CN
- China
- Prior art keywords
- bearing press
- bearing
- counterdie
- patrix
- hole
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
Images


Landscapes
- Mounting, Exchange, And Manufacturing Of Dies (AREA)
Abstract
本实用新型公开了一种轴承压装胎具装置,旨在提供一种能够适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装的轴承压装胎具装置。它包括上压模装置和下压模装置,所述的上压模装置和下压模装置呈上下对称分布,所述的上压模装置包括上固定板和上模,所述的下压模装置包括下固定板和下模,所述的上模和下模中间均设有通孔,所述的通孔内设有导正销,所述的导正销通过弹簧与下固定板连接。本实用新型的有益效果是:能够适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装,不但对装置中性好,而且装配精度高,极大地提高了生产效率,特别适合中批、大批量生产,操作方便。
The utility model discloses a bearing press-fitting mold device, aiming to provide a bearing press-fitting mold device suitable for the bearing press-fitting produced by the car power assembly, the transmission assembly and the bearing press-fitting assembly line of the manufacturing company . It includes an upper die device and a lower die device, the upper die device and the lower die device are symmetrically distributed up and down, the upper die device includes an upper fixing plate and an upper die, and the lower die device The device includes a lower fixing plate and a lower die, and a through hole is arranged between the upper die and the lower die, and a guiding pin is arranged in the through hole, and the guiding pin is connected with the lower fixing plate through a spring. The beneficial effect of the utility model is: it can be applied to the bearing press assembly produced by the car power assembly, the transmission assembly and the bearing press assembly line of the manufacturing company, which not only has good neutrality to the device, but also has high assembly precision, greatly improving the production High efficiency, especially suitable for medium batch and large batch production, easy to operate.
Description
技术领域 technical field
本实用新型涉及一种机械制造工艺装备器具,尤其是指一种轴承压装胎具装置。 The utility model relates to a mechanical manufacturing process equipment appliance, in particular to a bearing press-fitting tire device.
背景技术 Background technique
一般情况下,工人师傅们在压装轴承时,都是用榔头(木榔头、铁榔头以及橡胶榔头),这样在压装轴承时不但费时费力,而且容易伤坏轴承和轴,同时生产效率不高。所以只适合单件小批量生产,当中批生产或大批量生产时,无法满足生产需求。 Under normal circumstances, workers and masters use hammers (wooden hammers, iron hammers and rubber hammers) when pressing bearings. This is not only time-consuming and laborious when pressing bearings, but also easily damages bearings and shafts. At the same time, production efficiency is low. high. Therefore, it is only suitable for single-piece small-batch production, and it cannot meet production needs during medium-batch or large-batch production.
中国专利授权公告号:CN 201783804U,授权公告日2011年4月6日,公开了一种齿轮泵滑动轴承压装胎具,包括胎具体,胎具体的台肩下平面上设有胎具限位面,胎具限位面里侧设有限位间隙槽,胎具体下端设有轴承工程塑料层压装保护弧面,齿轮泵滑动轴承压装胎具可以保证压装精度,尺寸控制准确。本实用新型的不足之处在于,该压装胎具只适用于对齿轮泵滑动轴承的压装,不适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装。 Chinese patent authorization announcement number: CN 201783804U, authorized announcement date April 6, 2011, discloses a gear pump sliding bearing press-fit tire, including a tire body, the tire body is provided with a mold limiter on the lower plane of the shoulder On the surface, there is a limit gap groove on the inner side of the tire limit surface, and the lower end of the tire body is provided with a bearing engineering plastic laminated protective arc surface. The gear pump sliding bearing press-fit tire can ensure the press-fit accuracy and accurate size control. The disadvantage of the utility model is that the press-fit tire tool is only suitable for the press-fit of the sliding bearing of the gear pump, and is not suitable for the press-fit of the powertrain of the car, the transmission assembly and the bearing press-fit line produced by the bearing press-fit assembly line of the manufacturing company. .
实用新型内容 Utility model content
本实用新型是为了克服现有技术中轴承压装胎具不适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装的不足,提供了一种能够适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装的轴承压装胎具装置。 The utility model aims at overcoming the deficiency that the bearing press-fitting mold in the prior art is not suitable for the car power assembly, the transmission assembly and the bearing press-fit produced by the bearing press-fit assembly line of the manufacturing company, and provides a kind of bearing press-fit suitable for the car. The bearing press-fit tire device for powertrain, transmission assembly and bearing press-fit production line of the manufacturing company.
为了实现上述目的,本实用新型采用以下技术方案: In order to achieve the above object, the utility model adopts the following technical solutions:
一种轴承压装胎具装置,包括上压模装置和下压模装置,所述的上压模装置和下压模装置呈上下对称分布,所述的上压模装置包括上固定板和上模,所述的上模与上固定板连接,所述的上模中间设有通孔,所述的通孔内设有导正销,所述的导正销通过弹簧与上固定板连接,所述的下压模装置包括下固定板和下模,所述的下模与下固定板连接,所述的下模中间设有通孔,所述的通孔内设有导正销,所述的导正销通过弹簧与下固定板连接。 A bearing press-fitting mold device, comprising an upper die device and a lower die device, the upper die device and the lower die device are distributed symmetrically up and down, and the upper die device includes an upper fixing plate and an upper die, the upper die is connected with the upper fixing plate, a through hole is provided in the middle of the upper die, and a pilot pin is arranged in the through hole, and the guide pin is connected with the upper fixing plate through a spring, The lower die device includes a lower fixing plate and a lower die, the lower die is connected to the lower fixing plate, a through hole is provided in the middle of the lower die, and a guide pin is arranged in the through hole, so that The above-mentioned guide pin is connected with the lower fixing plate through a spring.
所述的上压模装置包括上固定板和上模,所述的上模与上固定板连接,所述的上模中间设有通孔,所述的通孔内设有导正销,所述的导正销通过弹簧与上固定板连接,弹簧的一端连接导正销,弹簧的另一端固定在上固定板上,通过导正销和弹簧的配合使用进行轴承压装,所述的下压模装置包括下固定板和下模,所述的下模与下固定板连接,所述的下模中间设有通孔,所述的通孔内设有导正销,所述的导正销通过弹簧与下固定板连接,弹簧的一端连接导正销,弹簧的另一端固定在下固定板上,通过导正销和弹簧的配合使用进行轴承压装,上压模装置与下压模装置呈上下对称分布,且上压模装置、下压模装置分别与气源连接。这样设计满足了能够适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装的目的。 The upper die device includes an upper fixing plate and an upper die, the upper die is connected to the upper fixing plate, a through hole is provided in the middle of the upper die, and a pilot pin is arranged in the through hole, so that The above-mentioned pilot pin is connected to the upper fixed plate through a spring, one end of the spring is connected to the pilot pin, and the other end of the spring is fixed on the upper fixed plate, and the bearing is pressed through the cooperation of the pilot pin and the spring. The compression molding device includes a lower fixing plate and a lower mold, the lower mold is connected with the lower fixing plate, a through hole is arranged in the middle of the lower mold, and a guiding pin is arranged in the described through hole, and the guiding pin is arranged in the described through hole. The pin is connected to the lower fixing plate through a spring, one end of the spring is connected to the guide pin, and the other end of the spring is fixed on the lower fixing plate, and the bearing is pressed through the cooperation of the guide pin and the spring, and the upper die device and the lower die device It is distributed symmetrically up and down, and the upper die device and the lower die device are respectively connected with the air source. This design satisfies the purpose of being applicable to the bearing press assembly produced by the car power assembly, the transmission assembly and the bearing press assembly line of the manufacturing company.
作为优选,所述的导正销形状为带台阶状的圆柱形,所述的导正销包括定位块、活动块、限位块和连接块,所述弹簧的一端套接在连接块上,所述的导正销中的活动块分别与上模和下模连接,其中定位块是用于固定轴承的位置,活动块分别与上模和下模滑动连接,限位块使得导正销限位在上模和下模中滑动,连接块通过弹簧分别与上固定板和下固定板连接,这样设计提高了装配精度,对称性较高。 Preferably, the shape of the pilot pin is a stepped cylinder, the pilot pin includes a positioning block, a movable block, a limit block and a connecting block, one end of the spring is sleeved on the connecting block, The movable blocks in the pilot pin are respectively connected with the upper die and the lower die, wherein the positioning block is used to fix the position of the bearing, the movable block is respectively slidably connected with the upper die and the lower die, and the limit block makes the guide pin limit The bit slides in the upper mold and the lower mold, and the connecting block is respectively connected with the upper fixing plate and the lower fixing plate through springs. This design improves the assembly accuracy and has high symmetry.
作为优选,所述的上模形状和下模形状均为圆柱形,所述的上模上设有轴承安装槽和锁紧块,所述的锁紧块置于轴承安装槽的一侧,所述的下模上设有轴承安装槽,轴承安装在轴承安装槽内,由于上模在安装过程中轴承安装槽方向朝下,故而通过锁紧块将轴承固定在上模中,防止轴承安装槽中的轴承的掉落。 As a preference, the shape of the upper mold and the lower mold are both cylindrical, and the upper mold is provided with a bearing installation groove and a locking block, and the locking block is placed on one side of the bearing installation groove. The above-mentioned lower mold is provided with a bearing installation groove, and the bearing is installed in the bearing installation groove. Since the direction of the bearing installation groove of the upper mold is facing downward during the installation process, the bearing is fixed in the upper mold by a locking block to prevent the bearing installation groove from drop of bearings in the
作为优选,所述弹簧与连接块的连接方式为过渡配合,提高了该轴承压装胎具装置的制作精度,以便于提高装配的精度,同时提高了工作效率。 Preferably, the connection between the spring and the connecting block is a transition fit, which improves the manufacturing precision of the bearing press-fitting mold device, facilitates the improvement of the assembly precision, and improves the work efficiency at the same time.
作为优选,所述的活动块与上模和下模的连接方式为间隙配合或者过渡配合,提高了该轴承压装胎具装置的制作精度,以便于提高装配的精度,同时提高了工作效率。 Preferably, the connection between the movable block and the upper mold and the lower mold is clearance fit or transition fit, which improves the manufacturing accuracy of the bearing press-fitting mold device, so as to improve the assembly accuracy and improve the work efficiency at the same time.
作为优选,所述的上模和下模上设有若干螺纹孔,所述的上固定板和下固定板上也设有与螺纹孔相对应的安装孔,所述的上固定板与上模螺钉连接,所述的下固定板与下模螺钉连接,采用螺钉连接便于该轴承压装胎具装置的拆卸与安装。 As a preference, the upper mold and the lower mold are provided with several threaded holes, the upper fixing plate and the lower fixing plate are also provided with mounting holes corresponding to the threaded holes, and the upper fixing plate and the upper mold Screw connection, the lower fixing plate is connected with the lower mold by screws, and the screw connection is used to facilitate the disassembly and installation of the bearing press-fitting mold device.
作为另一种优选,所述的上固定板与上模焊接,所述的下固定板与下模焊接,提高该轴承压装胎具装置的强度。 As another preference, the upper fixing plate is welded to the upper mold, and the lower fixing plate is welded to the lower mold, so as to improve the strength of the bearing press-fit tire device.
作为优选,所述的上固定板和下固定板上均设有若干光孔,通过光孔便于固定上固定板和下固定板。 As a preference, several light holes are provided on the upper and lower fixing plates, through which the upper and lower fixing plates can be easily fixed.
本实用新型的有益效果是:能够适用于轿车类动力总成、变速器总成以及制造公司轴承压装流水线生产的轴承压装,不但装置对中性好,而且装配精度高,极大地提高了生产效率,特别适合中批、大批量生产,操作方便。 The beneficial effect of the utility model is: it can be applied to the bearing press assembly produced by the car power assembly, the transmission assembly, and the bearing press assembly line of the manufacturing company. High efficiency, especially suitable for medium batch and large batch production, easy to operate.
附图说明 Description of drawings
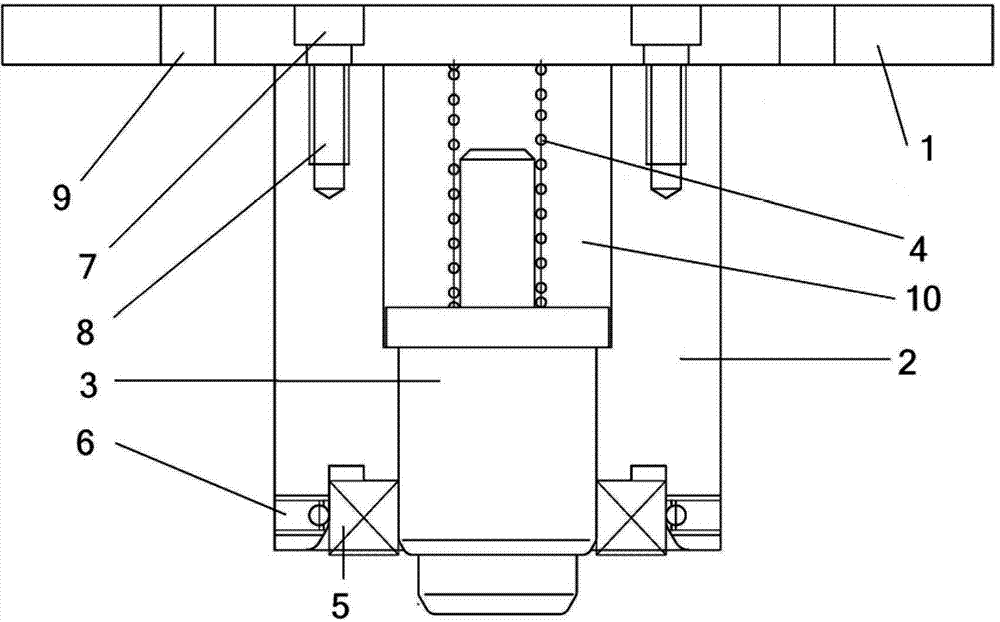
图1是上压模装置的结构示意图; Fig. 1 is the structural representation of upper die device;
图2是下压模装置的结构示意图。 Fig. 2 is a structural schematic diagram of the lower die device.
图中:1.上固定板,2.上模,3.导正销,4.弹簧,5.轴承,6.锁紧块,7.安装孔,8.螺纹孔,9.光孔,10. 通孔,11.定位块,12.活动块,13.限位块,14.连接块,15.下模,16.下固定板。 In the figure: 1. Upper fixing plate, 2. Upper mold, 3. Guide pin, 4. Spring, 5. Bearing, 6. Locking block, 7. Mounting hole, 8. Threaded hole, 9. Light hole, 10 . Through hole, 11. Positioning block, 12. Movable block, 13. Limiting block, 14. Connection block, 15. Lower mold, 16. Lower fixed plate.
具体实施方式 Detailed ways
下面结合附图和具体实施方式对本实用新型做进一步的描述。 Below in conjunction with accompanying drawing and specific embodiment, the utility model is further described.
实施例一:如图1、图2所述的实施例中,一种轴承压装胎具装置,包括上压模装置和下压模装置,上压模装置和下压模装置呈上下对称分布,上压模装置包括上固定板1和上模2,上模2与上固定板1连接,上模2中间设有通孔10,通孔10内设有导正销3,导正销3通过弹簧4与上固定板1连接,下压模装置包括下固定板16和下模15,下模15与下固定板16连接,下模15中间设有通孔10,通孔10内设有导正销3,导正销3通过弹簧4与下固定板16连接。导正销3形状为带台阶状的圆柱形,导正销3包括定位块11、活动块12、限位块13和连接块14,弹簧4的一端套接在连接块14上,其中弹簧4的另一端分别与上固定板1和下固定板16固定连接,导正销3中的活动块12分别与上模2和下模15连接。上模2形状和下模15形状均为圆柱形,上模2上设有轴承安装槽和锁紧块6,锁紧块6置于轴承安装槽的一侧,下模15上设有轴承安装槽。弹簧4与连接块14的连接方式为过渡配合。活动块12与上模2和下模15的连接方式为间隙配合或者过渡配合。上模2和下模15上设有四个螺纹孔8,上固定板1和下固定板16上也设有与螺纹孔8相对应的安装孔7,上固定板1与上模2螺钉连接,下固定板16与下模15螺钉连接。上固定板1和下固定板16上均设有四个光孔9。该轴承压装胎具装置与气源连接。
Embodiment 1: In the embodiment as shown in Fig. 1 and Fig. 2, a bearing press-fitting mold device includes an upper die device and a lower die device, and the upper die device and the lower die device are symmetrically distributed up and down , the upper die device includes an upper fixed plate 1 and an
实施例二:该实施例中的轴承压装胎具装置结构基本与实施例一相同,其不同之处在于,上固定板1与上模2焊接,下固定板16与下模15焊接。
Embodiment 2: The structure of the bearing press fitting device in this embodiment is basically the same as that of Embodiment 1, the difference is that the upper fixing plate 1 is welded to the
其使用方法如下:在使用时,先将轴承5分别放入下模15与上模2的轴承安装槽中,并通过锁紧块6将放入上模2轴承安装槽中的轴承5固定,将待装组件放入下模15与上模2之间。然后,打开气源,上模2下行开始进行轴承压装。压装完毕后,关闭气源,上模2上行结束工序。如此重复,整个过程6秒左右即可完成。此轴承压装胎具装置不但对中性好,装配精度高,极大地提高了生产效率。特别适合中批、大批量生产的流水线作业。
Its use method is as follows: when in use, first put the
Claims (8)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201220521868 CN202861747U (en) | 2012-10-11 | 2012-10-11 | Bearing press fitting clamping fixture device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN 201220521868 CN202861747U (en) | 2012-10-11 | 2012-10-11 | Bearing press fitting clamping fixture device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN202861747U true CN202861747U (en) | 2013-04-10 |
Family
ID=48028503
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN 201220521868 Expired - Fee Related CN202861747U (en) | 2012-10-11 | 2012-10-11 | Bearing press fitting clamping fixture device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN202861747U (en) |
Cited By (14)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104589024A (en) * | 2015-01-16 | 2015-05-06 | 无锡市创能机械制造有限公司 | Bearing press mounting tool for plate rammer vibration box |
| CN105081738A (en) * | 2015-08-07 | 2015-11-25 | 安阳工学院 | Installation device for bilateral bearings of rear axle differential of electric tricycle |
| CN105773518A (en) * | 2016-04-19 | 2016-07-20 | 江西江铃底盘股份有限公司 | Press-fitting system and method for main speed reducer shell and flange head |
| CN106246744A (en) * | 2015-11-03 | 2016-12-21 | 无锡市三立轴承有限公司 | Double installing type bearing assembly heads |
| CN106312441A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Preheating mounting head for bearing |
| CN106321660A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Preheating type bearing mounting head structure |
| CN106312913A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Hydraulic bearing mounting head |
| CN106312912A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Bearing installing head |
| CN106312919A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Preheating type manual assembly head for bearing |
| CN108406270A (en) * | 2018-04-23 | 2018-08-17 | 温州职业技术学院 | A kind of bearing Mounting device |
| CN108673095A (en) * | 2018-06-27 | 2018-10-19 | 河源职业技术学院 | A kind of decompressor for finger tip gyro |
| CN109088520A (en) * | 2017-06-14 | 2018-12-25 | 石伟 | A kind of pressure rotor fixed position mould |
| CN110153687A (en) * | 2019-06-03 | 2019-08-23 | 安阳工学院 | Self-centering differential bearing installation device and installation method for double-sided bearings |
| CN114473954A (en) * | 2022-03-09 | 2022-05-13 | 广西玉柴机器股份有限公司 | Press mounting tool for new structure idle gear bearing |
-
2012
- 2012-10-11 CN CN 201220521868 patent/CN202861747U/en not_active Expired - Fee Related
Cited By (18)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN104589024A (en) * | 2015-01-16 | 2015-05-06 | 无锡市创能机械制造有限公司 | Bearing press mounting tool for plate rammer vibration box |
| CN105081738A (en) * | 2015-08-07 | 2015-11-25 | 安阳工学院 | Installation device for bilateral bearings of rear axle differential of electric tricycle |
| CN105081738B (en) * | 2015-08-07 | 2017-11-07 | 安阳工学院 | A kind of electric tricycle rearmost axle differential mechanism double-sided bearings erecting device |
| CN106312919A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Preheating type manual assembly head for bearing |
| CN106312441A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Preheating mounting head for bearing |
| CN106321660A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Preheating type bearing mounting head structure |
| CN106312913A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Hydraulic bearing mounting head |
| CN106312912A (en) * | 2015-11-03 | 2017-01-11 | 无锡市三立轴承有限公司 | Bearing installing head |
| CN106246744A (en) * | 2015-11-03 | 2016-12-21 | 无锡市三立轴承有限公司 | Double installing type bearing assembly heads |
| CN105773518A (en) * | 2016-04-19 | 2016-07-20 | 江西江铃底盘股份有限公司 | Press-fitting system and method for main speed reducer shell and flange head |
| CN105773518B (en) * | 2016-04-19 | 2017-10-03 | 江西江铃底盘股份有限公司 | A kind of press mounting system and its pressing method of final drive casing and collar head |
| CN109088520A (en) * | 2017-06-14 | 2018-12-25 | 石伟 | A kind of pressure rotor fixed position mould |
| CN108406270A (en) * | 2018-04-23 | 2018-08-17 | 温州职业技术学院 | A kind of bearing Mounting device |
| CN108673095A (en) * | 2018-06-27 | 2018-10-19 | 河源职业技术学院 | A kind of decompressor for finger tip gyro |
| CN108673095B (en) * | 2018-06-27 | 2023-12-26 | 河源职业技术学院 | Stamping device for fingertip gyroscope |
| CN110153687A (en) * | 2019-06-03 | 2019-08-23 | 安阳工学院 | Self-centering differential bearing installation device and installation method for double-sided bearings |
| CN110153687B (en) * | 2019-06-03 | 2021-01-22 | 安阳工学院 | A differential bearing installation device and installation method for self-centering double-sided bearings |
| CN114473954A (en) * | 2022-03-09 | 2022-05-13 | 广西玉柴机器股份有限公司 | Press mounting tool for new structure idle gear bearing |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN203003796U (en) | Pin bush tool | |
| CN202964162U (en) | Tool for guaranteeing coaxiality of flange hole | |
| CN203470972U (en) | Drill jig tool for mounting holes of automobile panel | |
| CN203044672U (en) | Combined male die of punching die | |
| CN205111750U (en) | Bush pressfitting mounting tool | |
| CN203045236U (en) | Welding fixture of oil cylinder supporting seat assembly | |
| CN204123132U (en) | A kind of electric machine stand vertical lathing tooling | |
| CN104707911A (en) | Punching and blanking mold for small bracket | |
| CN202240375U (en) | Press liner fixture equipment with center pressure heads and floating mandrels for guiding and centering | |
| CN103084489A (en) | Guide structure for fine blanking die sets | |
| CN102784869A (en) | Structure of novel die set | |
| CN203526900U (en) | Disc spring press-fit tool | |
| CN203712236U (en) | Assembly fixture of armrest box shaft pin of automobile | |
| CN204149111U (en) | A kind of car door adhesive tape pressing jig | |
| CN204052790U (en) | The internal segment assembling mould of the flat sleeve of milling | |
| CN102019339A (en) | Electromagnetic die punching frame | |
| CN201913178U (en) | Electric upsetting mold frame for valve blank capable of facilitating mold alignment | |
| CN204748474U (en) | Car base bearing automatic assembly frock | |
| CN201913177U (en) | Electric upsetting mold frame for high-precision valve blank | |
| CN204171173U (en) | The shaping lower mould assembly of a kind of centre frame | |
| CN203266084U (en) | Screw positioning device of automatic screw twisting machine | |
| CN204565694U (en) | Blank hole location processing tool | |
| CN203509500U (en) | Sliding bearing press-fitting fixture | |
| CN204013109U (en) | A kind of automobile window motor casing inner bearing press-loading apparatus | |
| CN203171483U (en) | Collecting pipe assembly mold positioning structure for heat exchanger assembly machine |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20130410 Termination date: 20131011 |