The multistation drying room of top turnover workpiece
Technical field
The utility model relates to a kind of drying room, relates in particular to a kind of multistation drying room of top turnover workpiece.
Background technology
In the paint line of the conveying workpieces of driving a vehicle automatically, the drying room of supporting top turnover workpiece generally all is the single station slot type drying room that supplies a suspension bracket turnover, and a workpiece that a suspension bracket is hung carries out heat drying.In order to ensure drying time, production line need dispose the requirement that a plurality of oven dry grooves could satisfy productive temp sometimes, has increased equipment investment, energy consumption and floor space, has also influenced the raising of production capacity.
Summary of the invention
The utility model technical problem to be solved is that the multistation drying room of the top turnover workpiece that a kind of cost of investment is little, production efficiency is high is provided.
In order to solve the problems of the technologies described above, the utility model is realized through following technical scheme: a kind of multistation drying room of top turnover workpiece, form by drying room chamber body, inlet/outlet mechanism, door moving machine structure, elevating mechanism, travel mechanism and hot air circulating system; Said inlet/outlet mechanism is arranged at body top, drying room chamber; Said door moving machine structure is arranged on drying room chamber external; And said door moving machine structure is connected with said inlet/outlet mechanism driving; The said valency mechanism that rises is arranged on the external sidewall paneling in drying room chamber, and its top is positioned at drying room chamber body, and said travel mechanism is arranged on the inner both sides of drying room.
Preferably, said inlet/outlet mechanism is by going into the part door and going out the part door and form; Go into the part door and go out part door bottom to be provided with roller, said roller cooperates with the guide rail that is arranged on body top, drying room chamber, moves flexibly through the traction of door moving machine structure.
Preferably, said travel mechanism is made up of mobile carrier chain, carrier chain guide rail, carrier chain tensioning apparatus, drive sprocket and drive unit; Mobile carrier chain is arranged on the carrier chain guide rail, and the carrier chain tensioning apparatus is arranged on and moves carrier chain one end, and drive unit is arranged at outside the body wall plate of drying room chamber, is connected with the carrier chain tensioning apparatus through drive sprocket.
Preferably, said hot air circulating system is made up of burner, heat exchanger, connection airduct, circulating fan, ajutage and backwind tube; Heat exchanger is arranged on burner and is connected between the airduct, connects the airduct other end and is connected with circulating fan and ajutage in turn, and backwind tube is connected with heat exchanger.
Preferably, said drive unit is provided with the torquer of crossing that is used for mechanism's overload protection.
Compared with prior art, the usefulness of the utility model is: the multistation drying room of this top turnover workpiece adopts hoisting mechanism and travel mechanism, make workpiece outside stove, accept to withdraw in the stove after;, implements beat the oven dry operation in carrying; Both guarantee the process time of oven dry, also satisfied the requirement of productive temp, be equivalent to the work of many oven dry grooves; Improved production efficiency, energy efficient and cost of investment.
Description of drawings:
Below in conjunction with accompanying drawing the utility model is further specified.
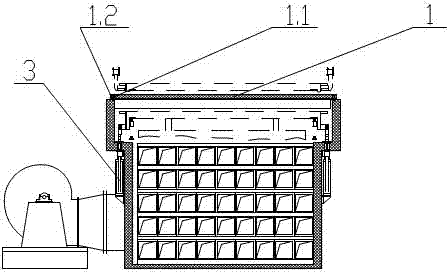
Fig. 1 is the multistation drying room inlet/outlet mechanism structure sketch map of the utility model top turnover workpiece;
Fig. 2 is suspension bracket lift cylinder, riser guide and V-arrangement support board structure enlarged drawing;
Fig. 3 is a suspension bracket travel mechanism structural representation;
Fig. 4 is the hot air circulating system structural representation.
Among the figure: 1, inlet/outlet mechanism; 1.1, roller; 1.2, rolling wheel guide rails; 2, door moving machine structure; 3, elevating mechanism; 3.1, lift cylinder; 3.2, the guiding of going up and down; 3.3, the V-arrangement supporting plate; 4, travel mechanism; 4.1, move carrier chain; 4.2, the carrier chain guide rail; 4.3, mobile drive deivce; 5, hot air circulating system; 5.1, burner; 5.2, heat exchanger; 5.3, connect airduct; 5.4, circulating fan; 5.5, ajutage.
The specific embodiment:
Below in conjunction with the accompanying drawing and the specific embodiment the utility model is described in detail:
A kind of multistation drying room of top turnover workpiece is made up of drying room chamber body, inlet/outlet mechanism 1, door moving machine structure 2, elevating mechanism 3, travel mechanism 4 and hot air circulating system 5; Said inlet/outlet mechanism 1 is arranged at body top, drying room chamber; Said door moving machine structure 2 is arranged on drying room chamber external; And said door moving machine structure 2 is in transmission connection with said inlet/outlet mechanism 1; The said valency mechanism 3 that rises is arranged on the external sidewall paneling in drying room chamber, and its top is positioned at drying room chamber body, and said travel mechanism 4 is arranged on the inner both sides of drying room.
As shown in Figure 1, said inlet/outlet mechanism 1 is by going into the part door and going out the part door and form; Go into the part door and go out part door bottom to be provided with roller 1.1, said roller 1.1 cooperates with the guide rail 1.2 that is arranged on body top, drying room chamber, moves flexibly through the traction of door moving machine structure 2.
As shown in Figure 2, said elevating mechanism 3 is made up of lift cylinder 3.1, the guiding 3.2 of going up and down and V-arrangement supporting plate 3.3; Lift cylinder 3.1 is arranged on guiding 3.2 inboards, and V-arrangement supporting plate 3.3 is arranged on guiding 3.2 tops; This elevating mechanism 3 is arranged on workpiece inlet/outlet mechanism 1 below; Be used to accept and submit to suspension bracket from the planer-type driving; For avoiding the influence of drying room chamber temperature, lift cylinder 3.1 is arranged in outside the body wall plate of drying room chamber, and should there be good provision for thermal insulation at guiding 3.2 places of going up and down.
As shown in Figure 3, said travel mechanism 4 is made up of mobile carrier chain 4.1, carrier chain guide rail 4.2, carrier chain tensioning apparatus, drive sprocket and drive unit 4.3; Move carrier chain 4.1 and be arranged on the carrier chain guide rail 4.2, the carrier chain tensioning apparatus is arranged on and moves carrier chain 4.1 1 ends, and drive unit 4.3 is arranged at outside the body wall plate of drying room chamber, is connected with the carrier chain tensioning apparatus through drive sprocket; This suspension bracket travel mechanism 4 is installed in the inner both sides of drying room chamber body; Be used for moving the suspension bracket that hangs full workpiece; Moving of suspension bracket is beat-type; Displacement is according to the requirement of productive temp, for preventing that moving middle workpiece accident blocks conveying, also is equipped with the torquer of crossing that is used for mechanism's overload protection on the drive unit 4.3.
As shown in Figure 4, said hot air circulating system 5 is made up of burner 5.1, heat exchanger 5.2, connection airduct 5.3, circulating fan 5.4, ajutage 5.5 and backwind tube 5.6; Heat exchanger 5.2 is arranged on burner 5.1 and is connected between the airduct 5.3, connects airduct 5.3 other ends and is connected with circulating fan 5.4 and ajutage 5.5 in turn, and backwind tube 5.6 is connected with heat exchanger 5.2; Hot air circulating system 5 is removed ajutage 5.5 and is arranged in the body of drying room chamber with backwind tube 5.6, and its burner 5.1, heat exchanger 5.2 are arranged on drying room chamber external; The effect of this hot air circulating system 5 is to produce hot blast and implement the heating to workpiece; Temperature control in the stove is to measure the return air temperature signal by temperature sensor; Control burner through digital display temperature controller and the relatively back output instruction signal of set temperature value, thereby realize furnace temperature automatic control and demonstration; Air outlet and return air inlet are the shutter form, are convenient to regulate air output, make to blow in the baker evenly; The layout of ajutage 5.5 and backwind tube 5.6 makes the unimpeded and circulation of hot blast according to the shape and size of hanging after the combination of the workpiece on the suspension bracket, guarantees the workpiece thermally equivalent.
Said drying room chamber body adopts the steel structure frame structure; Be assembly unit insulation wallboard around framework is outer; Wallboard is certain thickness typing warming plate; The thickness of wallboard and insulation material should be confirmed according to the operating temperature of drying room; The inside and outside wall material can be selected according to customer requirement; The length of chamber body mainly is dependent on the entering door opening of workpiece and goes out the layout size in distance and drying room blast pipe 5.5 and backwind tube 5.6 and air port thereof between the part door opening, goes into the part door opening and the distance (station number) that goes out between the part door opening should be confirmed according to drying time and productive temp and suspension bracket spacing, the width of drying room chamber body and the layout that highly all depends on drying room airduct and air port thereof and the combination size of the relevant workpiece that hangs with productivity ratio.
Its concrete working method is following, and the first step is gone into part: the planer-type driving drives the suspension bracket motion arrival drying room chamber body workpiece that hangs with workpiece and goes into the top of part door, the travel switch sender; Then, drying room is gone into the part door and is opened, and sender puts in place; Then, suspension bracket elevating mechanism 3 promotes, and holds up planer-type driving over sling, sender; Sender is left in the planer-type driving; Then, in the suspension bracket elevating mechanism 3 decline retraction drying room chamber bodies, place suspension bracket on the mobile carrier chain 4.1 of suspension bracket travel mechanism 4; Elevating mechanism 3 continues to descend, and sender puts in place; In second step, move: suspension bracket travel mechanism 4 starts, and moves carrier chain 4.1 drive suspension brackets and moves a beat distance, puts in place, is positioned at outer mobile drive deivce 4.3 senders of drying room chamber body wall plate; In the 3rd step, go out part: drying room chamber body goes out the part door to be opened, and sender puts in place; Suspension bracket elevating mechanism 3 promotes, and holds up suspension bracket, and sender puts in place; Planer-type driving puts in place, promotes, and holds up suspension bracket, and sender and leaving puts in place; In the suspension bracket elevating mechanism 3 decline retraction drying room chamber bodies, sender puts in place.More than action also comprises the control of hot air circulating system etc. by PLC control, and the travel switch of all senders all outside drying room, as implementing device in stove, is then drawn by lever.
The multistation drying room of this top turnover workpiece adopts hoisting mechanism and travel mechanism; After making workpiece outside stove, accept to withdraw in the stove, in beat is carried, implement the oven dry operation, both guaranteed the process time of oven dry; Also satisfied the requirement of productive temp; Be equivalent to the work of many oven dry grooves, improved production efficiency, energy efficient and cost of investment.
It is emphasized that: above only is the preferred embodiment of the utility model; Be not that the utility model is done any pro forma restriction; Every technical spirit according to the utility model all still belongs in the scope of the utility model technical scheme any simple modification, equivalent variations and modification that above embodiment did.