A kind of Drawing Die
Technical field
The utility model relates to a kind of Drawing Die, relates in particular to the adjustable rotation of a kind of pressure-pad-force and draws in the formula Drawing Die, belongs to mould applications.
Background technology
Pull and stretch is one of sheet metal forming technology commonly used; The potential that how to reduce drawing coefficient, performance plate is the emphasis of research of drawing performance and stamping Die Design always; And present die industry is in design technology and drawing Die Design process; The mode that usually adopts plate to be drawn into die obtains needed drawing part, and general pull and stretch die is fixed, flexible member effect blank holder compresses plate, the punch motion, pulls out needed product.The problem that this type mould exists is: the mode form that (1) plate is drawn into is single, causes frictional force big, and pull and stretch is wrinkling to be increased with the possibility of breaking; (2) a kind of plate of thickness is fixed and can only be adapted to the pressure-pad-force curve of pull and stretch; Pressure-pad-force will be difficult to adjustment when sheet thickness changes; To same thickness plate, the pressure-pad-force curve can't be coordinated with the curve that material forming requires mutually, is difficult to bring into play the shaping potentiality of plate.
The utility model content
The purpose of the utility model is to design the mould structure that a kind of pressure-pad-force can be regulated at any time, plate is drawn in rotation complex method gets into the die hole, for pull and stretch provides a kind of new method.Therefore, the utility model is designed to punch and die rotary to change the state that plate flows into, promptly by traditional formula of drawing in become draw at present rotative combined.
The technical scheme of the utility model is:
A kind of Drawing Die comprises the die structure, blank holder and punch structure;
The die structure comprises: upper clamping plate, and last rotation supporting structure is fixed under the upper clamping plate, and it is inner that the top rotary table structure is nested in rotation supporting structure, and it is inboard that die is fixed on the top rotary table structure, and recess is downward;
Blank holder comprises: the turning down supporting construction; It is inner that the lower rotary table structure is nested in the turning down supporting construction; And flexibly connect over against the ball in the half slot that forms through turning down supporting construction inboard and the lower rotary table structure outside; Blank holder centre bore aperture equals the die bore, is positioned under the die structure;
Punch structure comprises: the punch axle; Punch axle external diameter is positioned at the blank holder below over against the blank holder centre bore, and passes through bearing fixing on cylinder bodily form hollow base less than die bore and blank holder centre bore aperture; The Drawing Die lower bolster is fastenedly connected with its top backing plate and forms the lower bolster structure; Hollow base is fastened on the lower bolster superstructure, and a circular hole is laterally opened in the hollow base side, passes through bevel gear shaft that connects external power supply of bearing fixing in the circular hole; The bevel gear shaft head connects the bevel-gear sett group, and bevel gear set is connected with the punch axle through the key on the punch axle.
The said rotation supporting structure of going up comprises: on turn round base for supporting, on turn round the base for supporting cover, it is nested and be fixed on revolution base for supporting cover inboard wherein to go up the revolution base for supporting; Said top rotary table structure comprises the revolution supporting wheel, on turn round the supporting wheel cover, it is nested and be fixed on revolution supporting wheel cover inboard wherein to go up the revolution supporting wheel; Said turning down supporting construction comprises the turning down base for supporting, turning down support base cover for seat, and wherein the turning down base for supporting overlaps nested and is fixed on turning down base for supporting inboard; Said lower rotary table structure comprises: the turning down supporting wheel, and turning down supporting wheel cover, wherein the turning down supporting wheel is nested and to be fixed on turning down supporting wheel cover inboard.
Said Drawing Die top also comprises die shank, spline pin; Wherein the die shank outer radial has half slot A; Radially also there is half slot B upper clamping plate centre bore inboard, and die shank 1 is nested in the centre bore of upper clamping plate, half slot A and half slot B over against; The spline pin inserts in the slot of half slot A and half slot B formation, and start-stop transfers to usefulness to die shank.
Also comprise ball, the said ball of going up is installed in the circular trough that forms between the rotation supporting structure inboard and the top rotary table structure outside.
The punch axle bottom of said punch structure is fitted bearing also, and bearing fixing is on bearing (setting) plate, and said bearing (setting) plate embeds and be fixed on the hollow base inboard.
Also comprise one group for the blank holder structure provides the hydraulic cylinder of hydraulic pressure, hydraulic cylinder head cover, wherein, hydraulic cylinder head cover is fixed on the turning down supporting construction, is fastenedly connected between hydraulic cylinder and the hydraulic cylinder head cover.
Said hydraulic cylinder has pressure-regulating valve.
Said die structure division also comprises: spring; Said spring upper end is fastenedly connected and is nested in the spring bracing with spring bracing; Be fastenedly connected under said spring bracing and the spring bracing fixed head; Be fastenedly connected under spring bracing fixed head and the upper clamping plate center, push pedal is fixed on spring lower end, activity, and to be nested in the die structure inboard and over against the punch shaft head.
The drawing and forming method of described Drawing Die, in this Drawing Die when work,, the punch axle drives with key through bevel-gear sett and rotates, die decline, the blank holder structure is in not duty, and when die during near the blank holder structure, the hydraulic coupling of blank holder makes
Plate and lower rotary table structure and die are adjacent to; Descend together then, when plate touched the punch axle, the punch axle drove plate and rotates; Die, top rotary table structure, lower rotary table structure are driven together by plate and rotate, and die and lower rotary table structure continue to descend until drawing and forming simultaneously.
The beneficial effect of the utility model is: after adopting the technical scheme of the utility model; Can reduce the Limit Drawing coefficient of plate, give full play to the potential of material, reduce the material forming performance demands; The sheet material of great conserve expensive, particularly advanced high-strength panel.In addition, adopt hydraulic pressure pressure-pad-force control strategy to give full play to the forming limit of material, reduce requirement, greatly practice thrift cost high performance material according to controlling the pressure-pad-force size at any time.
Description of drawings
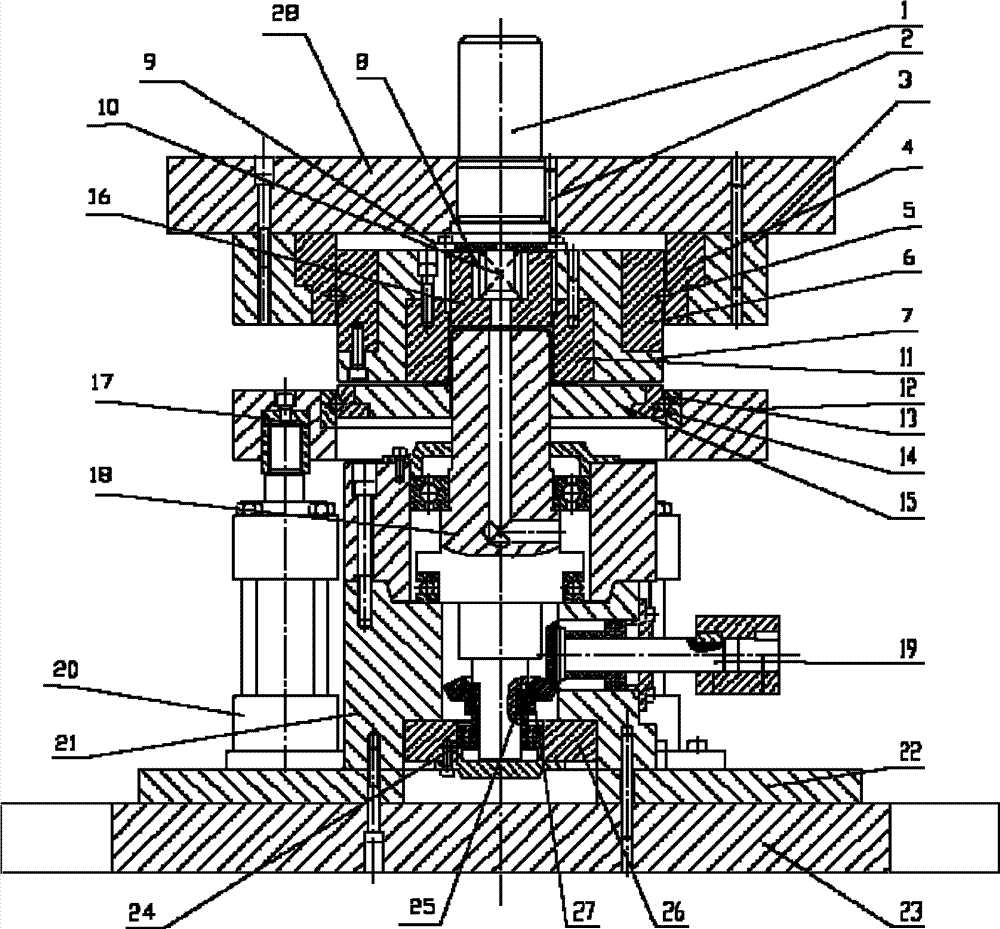
Fig. 1 is the structural representation that the formula Drawing Die is drawn in the adjustable rotation of the pressure-pad-force of the utility model.
Wherein: 1 die shank, 2 spline pins turn round base for supporting on 3, revolution base for supporting cover on 4, ball on 5, revolution supporting wheel cover on 6; Turn round supporting wheel on 7,8 spring bracings, 9 spring bracing fixed heads, 10 springs, 11 dies, 12 turning down base for supporting; 13 turning down support base cover for seat, 14 turning down supporting wheel covers, 15 turning down supporting wheels, 16 push pedals, 17 hydraulic cylinder head covers, 18 punch axles; 19 bevel gear shafts, 20 hydraulic cylinders, 21 hollow bases, 22 backing plates, 23 counterdie seat boards; 24 bearings, 25 keys, 26 bearing (setting) plates, 27 bevel gear set, 28 upper clamping plates.
The specific embodiment
Referring to Fig. 1, during the work of this Drawing Die, punch axle 18 drives with key 25 through bevel-gear sett 27 and rotates; Die 11 descends, and the blank holder structure is in not duty, when die during near the blank holder structure; The hydraulic coupling of blank holder is adjacent to plate and lower rotary table structure and die 11; Descend together then, when plate touched punch axle 18, punch axle 18 drove plate and rotates; Die 11, top rotary table structure, lower rotary table structure are driven together by plate and rotate, and die 11 continues to descend until drawing and forming with the lower rotary table structure simultaneously.Describe in the face of the concrete structure of this Drawing Die down:
The Drawing Die that the utility model relates to comprises the die structure, blank holder and punch structure.
The die structure comprises: upper clamping plate 28, last rotation supporting structure are fixed under the upper clamping plate 28, and it is inner that the top rotary table structure is nested in rotation supporting structure, and it is inboard that die 11 is fixed on the top rotary table structure, and recess is downward;
Blank holder comprises: the turning down supporting construction; It is inner that the lower rotary table structure is nested in the turning down supporting construction; And flexibly connect over against the ball in the half slot that forms through turning down supporting construction inboard and the lower rotary table structure outside; Blank holder centre bore aperture equals the die bore, is positioned under the die structure;
Punch structure comprises: punch axle 18; Punch axle 18 external diameters are positioned at the blank holder below over against the blank holder centre bore, and pass through bearing fixing on cylinder bodily form hollow base less than die bore and blank holder centre bore aperture; Drawing Die lower bolster 23 is fastenedly connected with its top backing plate 22 and forms the lower bolster structure; Hollow base is fastened on the lower bolster superstructure, and a circular hole is laterally opened in the hollow base side, passes through bevel gear shaft 19 that connects external power supply of bearing fixing in the circular hole; Bevel gear shaft 19 heads connect bevel-gear sett group 27, and bevel gear set 27 is connected with the punch axle through the key 25 on the punch axle.
The said rotation supporting structure of going up comprises: on turn round base for supporting 3, on turn round base for supporting cover 4, it is nested and be fixed on and turn round base for supporting and overlap 4 inboards wherein to go up revolution base for supporting 3; Said top rotary table structure comprises revolution supporting wheel 15, on turn round supporting wheel cover 14, it is nested and be fixed on and turn round supporting wheel and overlap 14 inboards wherein to go up revolution supporting wheel 15; Said turning down supporting construction comprises turning down base for supporting 12, turning down support base cover for seat 13, and wherein turning down support base cover for seat 13 is nested and be fixed on turning down support base cover for seat 13 inboards; Said lower rotary table structure comprises: turning down supporting wheel 15, and turning down supporting wheel cover 14, wherein turning down supporting wheel 15 is nested and be fixed on the turning down supporting wheel and overlap 14 inboards.
Said Drawing Die top also comprises die shank 1, spline pin 2; Wherein die shank 1 outer radial has half slot A; Radially also there is half slot B die holder plate centre bore inboard, and die shank 1 is nested in the centre bore of die holder plate 28, half slot A and half slot B over against; Spline pin 2 inserts in the slot of half slot A and half slot B formation, and 1 start-stop transfers to usefulness to die shank.
In order to strengthen going up the rotary stability of turning down rotating disk, said Drawing Die can also increase installs ball 5, and last ball diameter is Φ 10mm, and the said ball 5 of going up is installed in the circular trough that forms between the rotation supporting structure inboard and the top rotary table structure outside.
In order to increase the running steadiness of described Drawing Die punch axle, the punch axle bottom of said punch structure is fitted bearing 24 also, and bearing 24 is fixed on the bearing (setting) plate 26, and said bearing (setting) plate 26 embeds and be fixed on the hollow base inboard.
Said Drawing Die; Also comprise one group for the blank holder structure provides the hydraulic cylinder 20 of hydraulic pressure, hydraulic cylinder head cover 17, wherein; Hydraulic cylinder head cover 17 is fixed on the turning down supporting construction; Be fastenedly connected between hydraulic cylinder 35 and the hydraulic cylinder head cover 17, the pressure that hydraulic cylinder provides can be regulated control at any time through pressure valve, thereby the pressure of blank holder also can be regulated at any time.
After the plate pull and stretch is accomplished; For plate is fallen from die automatically; Said die structure division also comprises: spring 10, and said spring 10 upper ends and spring bracing are fastenedly connected and are nested in the spring bracing 8, are fastenedly connected under said spring bracing 8 and the spring bracing fixed head 9; Be fastenedly connected under spring bracing fixed head 9 and upper clamping plate 28 centers, push pedal 16 is fixed on spring 10 lower ends, activity, and to be nested in the die structure inboard and over against the punch shaft head.When plate during by pull and stretch, this moment, spring 10 was gradually reduced, and push pedal 16 is risen with respect to die 11, and after plate drew high moulding, the die structure rose, and punch leaves die, and push pedal 16 is pushed product under spring 10 elastic force effects in die 11.