CN201979593U - Four-shaft vacuum ceramic plate extruder - Google Patents
Four-shaft vacuum ceramic plate extruder Download PDFInfo
- Publication number
- CN201979593U CN201979593U CN2011200114752U CN201120011475U CN201979593U CN 201979593 U CN201979593 U CN 201979593U CN 2011200114752 U CN2011200114752 U CN 2011200114752U CN 201120011475 U CN201120011475 U CN 201120011475U CN 201979593 U CN201979593 U CN 201979593U
- Authority
- CN
- China
- Prior art keywords
- vacuum
- pug
- ceramic plate
- extruded
- extruding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 239000000919 ceramic Substances 0.000 title claims abstract description 25
- 238000001125 extrusion Methods 0.000 claims abstract description 22
- 230000005540 biological transmission Effects 0.000 claims abstract description 18
- 238000004519 manufacturing process Methods 0.000 claims abstract description 16
- 238000001816 cooling Methods 0.000 claims abstract description 13
- 239000004576 sand Substances 0.000 claims description 20
- 238000000605 extraction Methods 0.000 claims description 14
- 239000002994 raw material Substances 0.000 abstract description 5
- 238000000034 method Methods 0.000 abstract description 3
- 238000005086 pumping Methods 0.000 abstract 3
- 239000002699 waste material Substances 0.000 abstract 1
- 230000008878 coupling Effects 0.000 description 7
- 238000010168 coupling process Methods 0.000 description 7
- 238000005859 coupling reaction Methods 0.000 description 7
- XLYOFNOQVPJJNP-UHFFFAOYSA-N water Substances O XLYOFNOQVPJJNP-UHFFFAOYSA-N 0.000 description 5
- 238000005253 cladding Methods 0.000 description 4
- 239000011324 bead Substances 0.000 description 3
- 239000003638 chemical reducing agent Substances 0.000 description 3
- 229940095676 wafer product Drugs 0.000 description 3
- 241001062009 Indigofera Species 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 230000008676 import Effects 0.000 description 2
- 238000012423 maintenance Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 241001408630 Chloroclystis Species 0.000 description 1
- 241001236644 Lavinia Species 0.000 description 1
- 230000009286 beneficial effect Effects 0.000 description 1
- 239000000498 cooling water Substances 0.000 description 1
- 230000002950 deficient Effects 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000013467 fragmentation Methods 0.000 description 1
- 238000006062 fragmentation reaction Methods 0.000 description 1
- 238000010438 heat treatment Methods 0.000 description 1
- 238000009434 installation Methods 0.000 description 1
- 238000002156 mixing Methods 0.000 description 1
- 238000000275 quality assurance Methods 0.000 description 1
- 230000009183 running Effects 0.000 description 1
- 238000003756 stirring Methods 0.000 description 1
Images



Landscapes
- Press-Shaping Or Shaping Using Conveyers (AREA)
- Preparation Of Clay, And Manufacture Of Mixtures Containing Clay Or Cement (AREA)
Abstract
A four-shaft vacuum ceramic plate extruder comprises an upper transmission chain and a lower transmission chain which are arranged on a machine seat and a machine frame, wherein the upper transmission chain comprises an upper power device, an upper speed-reducing device, an upper gear transmission device, an upper pug conveying device and a vacuum-pumping device which are all arranged on the machine frame. The lower transmission chain comprises a lower power device, a lower speed-reducing device, a lower gear transmission device, a lower pug conveying device and a vacuum-pumping device which are all arranged on the machine seat. The two transmission chains are in busbar connection with a pug extruding device and a cooling device which are arranged on the machine seat through the vacuum-pumping devices. The pug is extruded into products through the pug extruding device. The technical scheme is that when a system runs, an electrical control device is started, and the pug extrusion is performed through online production control. The four-shaft vacuum ceramic plate extruder overcomes the shortcomings that during the process of the pug extrusion, an existing extruder overheats, the quality of products can not be guaranteed, the production efficiency and the rate of finished products are lower, the waste of raw materials is serious, the investment on new equipment is high, and the like. The four-shaft vacuum ceramic plate extruder can be applied to the extrusion of various ceramic products, in particular to dry hanging curtain wall ceramic plate products.
Description
Technical field
The utility model relates to a kind of four vacuum ceramic plate extruders.
Background technology
Extruder, the crowded sand pump of the cladding curtain wall ceramic wafer of existing production all are single cylinders, only establish in the cylinder one extrude the axle and one group extrude spiral, and crowded sand pump does not have cooling device outward, such extruder generates heat in the pug extrusion seriously, product quality can't guarantee, production efficiency of products and yield rate are all lower, and wastage of material is big; As use the import extruder, its price is up to millions of RMB, and the maintenance management of equipment is extremely inconvenient, in case be beset by technical hitches then have a strong impact on production.
Summary of the invention
At above-mentioned situation, the utility model provides a kind of four vacuum ceramic plate extruders, and its existing higher production efficiency has the better products quality assurance again, but and the equipment investment of conserve expensive.
For achieving the above object, a kind of four vacuum ceramic plate extruders, it comprise be arranged at support and frame on, following two road driving-chains, last driving-chain is by the last power set that are arranged at frame, last deceleration device, transmission device cogs, last pug conveying device and vacuum extractor are formed, the underdrive chain is by the following power set that are arranged on the support, following deceleration device, the lower gear transmission device, following pug conveying device and vacuum extractor are formed, this two road driving-chain confluxes and connects with mud extraction extrusion device and cooling device on being arranged on support, when system moves, start electrical control gear, pug is extruded carried out online production control.
In order to realize result optimizing, improve, improve combination property of the present utility model, further step is.
The mud extraction extrusion device is a diplopore waist type sand pump, establishes two axle and two spirals of extruding extruded in the tube.
Twoly extrude that axle is extruded spool for a left side and axle is extruded on the right side.
Two spirals of extruding are that spiral is extruded on a left side and spiral is extruded on the right side.
Two axle and two spirals of extruding extruded are set in the following pug conveying device.
Vacuum extractor is provided with the vacuum chamber upper box.
Vacuum extractor is provided with the vacuum chamber lower box.
The vacuum chamber upper box is provided with several forms.
The utility model adopts and comprises upper and lower two road driving-chains that are arranged at support and frame, these upper and lower two road driving-chains are respectively by the motor drives of last power set and following power set, drive each device and components and parts operation in the driving-chain, this two road driving-chain confluxes and connects with mud extraction extrusion device and cooling device on being arranged on support through vacuum extractor, pug is extruded into product through the mud extraction extrusion device, when system moves, start electrical control gear, pug is extruded the technical scheme of carrying out online production control; Overcome existing extruder and generated heat in the pug extrusion seriously, product quality can't guarantee that production efficiency and yield rate are all lower, and wastage of material is big, and new equipment drops into defectives such as costliness.
The beneficial effect that the utility model is produced compared to existing technology:
1, the utility model adopts two road driving-chain structures, and is simple and compact for structure, and production range enlarges, and production efficiency and product quality all improve greatly;
2, the utility model adopts diplopore waist type sand pump structure, and it is big to have the power of extruding, and its power of extruding of extruding force rate single-screw extruder is big 2~3 times, reaches 50~70kgf/em
2
3, the utility model adopts two axles of extruding to promote pug with two spirals of extruding, when pug is advanced to mould, raw material cross section density everywhere is better than the raw material that single-screw promotes, and the extruding force of the inner each point of raw material is more even, and the product quality of extruding is better than the single-screw extruder;
4, the utility model adopts two axles of extruding to promote pug with two spirals of extruding, and the pug cross section of its promotion is much wideer than the extruder that single-screw promotes pug, more helps the bigger ceramic wafer product of extrusion molding width;
5, the utility model adopts two road driving-chains, in conjunction with diplopore waist type sand pump and two axle, two helical structure of extruding extruded, and adopt and squeeze the inside and outside cooling device of establishing of sand pump, preferably resolve the heating difficult problem of raw material in extrusion, guarantee product quality, improved production efficiency.
The utility model is applicable to and extrudes various ceramic products, particularly cladding curtain wall ceramic wafer product.
Below in conjunction with the drawings and specific embodiments the utility model is described in further detail.
Description of drawings
Fig. 1 is a front view of the present utility model.
Fig. 2 is the side view of Fig. 1.
Fig. 3 is the front view of diplopore waist type sand pump.
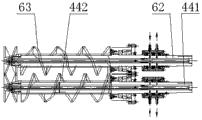
Fig. 4 is for extruding axle and extruding the spiral horizontal view.
Fig. 5 is the cooling device front view.
Fig. 6 is the cooling device sectional view.
Among the figure: 1, support, 2, frame, 3, last driving-chain, 31, last power set, 311, pneumatic clutch, 32, last deceleration device, 321, yielding coupling, 33, the transmission device that cogs, 34, last pug conveying device, 341, last mud box, 342, spiral propeller, 4, the underdrive chain, 41, following power set, 411, pneumatic clutch, 42, following deceleration device, 421, yielding coupling, 43, the lower gear transmission device, 431, positive coupling, 44, following pug conveying device, 441, about extrude axle, 442, about extrude spiral, 5, vacuum extractor, 51, the vacuum chamber upper box, 52, the vacuum chamber lower box, 53, form, 6, the mud extraction extrusion device, 61, diplopore waist type sand pump, 62, two axles of extruding, 63, two spirals of extruding, 7, electrical control gear, 8, cooling device, 81, ring-shaped water jacket, 82, water nozzle, 83, rib, 84, connection method indigo plant.
The specific embodiment
Shown in accompanying drawing, a kind of four vacuum ceramic plate extruders, it comprise be arranged at support 1 and frame 2 on, following two road driving-chains, last driving-chain 3 is by the last power set 31 that are arranged at frame 2, last deceleration device 32, transmission device 33 cogs, last pug conveying device 34 and vacuum extractor 5 are formed, underdrive chain 4 is by the following power set 41 that are arranged on the support 1, following deceleration device 42, lower gear transmission device 43, following pug conveying device 44 and vacuum extractor 5 are formed, this two road driving-chain confluxes with mud extraction extrusion device 6 on being arranged on support 1 and connects, and by electrical control gear 7,8 pairs of pugs of cooling device are processed; For improve production efficiency and product quality, wherein, mud extraction extrusion device 6 adopts diplopore waist type sand pumps 61, and two spirals 63 of extruding that spiral, the right side are extruded spiral are extruded on two axle 62 and the left sides of extruding of establishing in the tube that a left side extrudes that axle, the right side extrude axle; Equally, establish two axle and two spirals of extruding extruded in the following pug conveying device 44; Vacuum extractor 5 is established vacuum chamber upper box 51, vacuum chamber lower box 52; In order to realize automation control, handled easily, care and maintenance, the box body wall of vacuum chamber upper box 51 each side is provided with at least three forms 53, during the system operation, starts electrical control gear 7, pug is extruded carried out online production control.
Referring to accompanying drawing, work of the present utility model is: upper and lower two road driving-chains are formed power source by upper and lower power set respectively, motor in the last power set 31, drive by bead apex, through pneumatic clutch 311, hard flank of tooth cylindrical gear reducer in the driving in the deceleration device 32, the output shaft of reductor is through yielding coupling 321, power is passed to output gear in the transmission device 33 that cogs, pass to last mud box 341 in the pug conveying device 34 and the spiral propeller 342 vacuum chamber upper box 51 to the vacuum extractor 5 again; Motor in the following power set 41, drive by bead apex, through pneumatic clutch 411, hard flank of tooth cylindrical gear reducer under driving in the deceleration device 42, the output shaft of reductor is through yielding coupling 421, power is passed to output gear in the lower gear transmission device 43, pass to down again in the pug conveying device 44 about extrude axle 441 and about extrude the vacuum chamber lower box 52 of spiral 442 to the vacuum extractor 5; Two road power of last driving-chain 3 and underdrive chain 4 all conflux through vacuum extractor 5 and are attached to mud extraction extrusion device 6, driving in the mud extraction extrusion device 6 two in the diplopore waist type sand pump 61 extrudes axle 62 and twoly extrudes spirals 63 runnings, under the control of electrical control gear 7, go up spiral propeller 342 rotations in the mud box 341 in the last pug conveying device 34, with the pug that adds in the feed box, stir through fragmentation, after the mixing, extrude from sieve plate by the spiral propeller in the last mud box 341 34, import the vacuum chamber upper box 51 in the vacuum extractor 5 then, and be cut into thin slice in vacuum chamber upper box 51, pug obtains vacuum outgas effectively and handles in the vacuum chamber upper box 51 of vacuum extractor 5, vacuum extractor 5 comprises vacuum chamber upper box 51 and vacuum chamber lower box 52, vavuum pump-install in addition, aspirating chamber, components and parts such as vacuum meter and vacuum line, its effect is to form vacuum, so that remove the gas that mixes folder in the pug effectively, reach the plasticity that improves pug to greatest extent, to optimize the plasticity extrusion modling performance of pug, thin slice after treatment falls into vacuum chamber lower box 52 from vacuum chamber upper box 51.
Equally, motor in the following power set 41, drive by bead apex, through pneumatic clutch 411, hard flank of tooth cylindrical gear reducer under driving in the deceleration device 42, the output shaft of reductor is through yielding coupling 421, power is passed to lower gear transmission device 43, again through two positive couplings 431, with power and motion pass to down pug conveying device 44 two extrude axle and be contained in two extruding pair extrude spiral on the axle, will together be extruded into mud extraction extrusion device 6 with the pug that falls into vacuum chamber lower box 52 from vacuum extractor 5.
When system moves, start electrical control gear 7, upper and lower two road driving-chains are respectively by the motor drives of last power set 31 and following power set 41, drive each device and components and parts operation in the driving-chain, confluxing is attached to vacuum extractor 5, and pug is after the diplopore waist type sand pump 61 of mud extraction extrusion device 6 is extruded cladding curtain wall ceramic wafer product; Two axle 62 and two spirals 63 of extruding extruded are installed in the diplopore waist type sand pump 61, establish cooling device 8 on the diplopore waist type sand pump 61, this cooling device 8 comprises the ring-shaped water jacket 81 of diplopore waist type sand pump 61 outsides, be installed in the water nozzle 82 of ring-shaped water jacket 81, be arranged on the rib 83 in the diplopore waist type sand pump 61, supporting installation for the ease of diplopore waist type sand pump 61 and cooling device 8, diplopore waist type sand pump 61 two ends are provided with connection method indigo plant 84, when two in the mud extraction extrusion device 6 diplopore waist type sand pumps 61 extrude axle 62 and two when extruding spiral 63 rotations, cooling water is promptly arranged inside and outside the diplopore waist type sand pump 61, and processing is lubricated and cools off to pug simultaneously, and grasp driving-chains operation and pug is extruded state by each form 53 of vacuum chamber upper box 51 each side in the vacuum extractor 5, realize the full-automatic high-quality and efficient production of cladding curtain wall ceramic wafer On-line Product.
Claims (8)
1. one kind four vacuum ceramic plate extruders, it is characterized in that it comprise be arranged at support (1) and frame (2) on, following two road driving-chains, last driving-chain (3) is by the last power set (31) that are arranged at frame (2), last deceleration device (32), transmission device (33) cogs, last pug conveying device (34) and vacuum extractor (5) are formed, underdrive chain (4) is by the following power set (41) that are arranged on the support (1), following deceleration device (42), lower gear transmission device (43), following pug conveying device (44) and vacuum extractor (5) are formed, this two road driving-chain confluxes and connects with mud extraction extrusion device (6) and cooling device (8) on being arranged on support (1), when system moves, start electrical control gear (7), pug is extruded carried out online production control.
2. four vacuum ceramic plate extruders according to claim 1 is characterized in that mud extraction extrusion device (6) is a diplopore waist type sand pump (61), establish two axle (62) and two spirals (63) of extruding extruded in the tube.
3. four vacuum ceramic plate extruders according to claim 2 is characterized in that two extruding that axle (62) is extruded spool for a left side and axle is extruded on the right side.
4. four vacuum ceramic plate extruders according to claim 2 is characterized in that two extruding that spiral (63) is extruded spiral for a left side and spiral is extruded on the right side.
5. four vacuum ceramic plate extruders according to claim 1 is characterized in that in the pug conveying device (44) two axle and two spirals of extruding extruded being set down.
6. four vacuum ceramic plate extruders according to claim 1 is characterized in that vacuum extractor (5) is provided with vacuum chamber upper box (51).
7. four vacuum ceramic plate extruders according to claim 1 is characterized in that vacuum extractor (5) is provided with vacuum chamber lower box (52).
8. four vacuum ceramic plate extruders according to claim 6 is characterized in that vacuum chamber upper box (51) is provided with several forms (53).
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011200114752U CN201979593U (en) | 2011-01-15 | 2011-01-15 | Four-shaft vacuum ceramic plate extruder |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2011200114752U CN201979593U (en) | 2011-01-15 | 2011-01-15 | Four-shaft vacuum ceramic plate extruder |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN201979593U true CN201979593U (en) | 2011-09-21 |
Family
ID=44607061
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2011200114752U Expired - Fee Related CN201979593U (en) | 2011-01-15 | 2011-01-15 | Four-shaft vacuum ceramic plate extruder |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN201979593U (en) |
Cited By (3)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103171031A (en) * | 2013-03-28 | 2013-06-26 | 南京益生宜居建筑材料科技有限公司 | Continuous production method for concrete hollow slab |
| CN103386704A (en) * | 2012-05-08 | 2013-11-13 | 湖南省醴陵市五里牌机械厂 | Triaxial vacuum pug mill |
| CN104908147A (en) * | 2015-07-01 | 2015-09-16 | 中国建材检验认证集团西安有限公司 | Vacuum wallboard extruding machine used for manufacture of light wall boards |
-
2011
- 2011-01-15 CN CN2011200114752U patent/CN201979593U/en not_active Expired - Fee Related
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN103386704A (en) * | 2012-05-08 | 2013-11-13 | 湖南省醴陵市五里牌机械厂 | Triaxial vacuum pug mill |
| CN103171031A (en) * | 2013-03-28 | 2013-06-26 | 南京益生宜居建筑材料科技有限公司 | Continuous production method for concrete hollow slab |
| CN103171031B (en) * | 2013-03-28 | 2015-06-24 | 南京益生宜居建筑材料科技有限公司 | Continuous production method for concrete hollow slab |
| CN104908147A (en) * | 2015-07-01 | 2015-09-16 | 中国建材检验认证集团西安有限公司 | Vacuum wallboard extruding machine used for manufacture of light wall boards |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN206170388U (en) | A low temperature initial refining banbury mixer for rubber reclaiming | |
| CN204222201U (en) | Degraded sheet material two rank extrusion calendaring is molded into complete equipment | |
| CN110802847A (en) | Processing device for PE solid-wall pipe | |
| CN102248587A (en) | Bar extruding machine | |
| CN109535477B (en) | A kind of low-temperature recycling equipment for waste rubber | |
| CN105235187A (en) | Plastic screw extruder | |
| CN105176623B (en) | A kind of greasy filth extrusion shaping machine | |
| CN201979592U (en) | Four-axle vacuum ceramic plate clay extruding cylinder cooling device | |
| CN1094518C (en) | Process for manufacture of soap bars and apparatus therefor | |
| CN203370518U (en) | Novel double-roller-type granulating device | |
| CN108145943B (en) | Net type material kneading plasticization machine | |
| CN203622609U (en) | Strong extruder extrusion mechanism | |
| CN216550340U (en) | Continuous soap forming equipment | |
| CN211616566U (en) | Double-screw extruder for slipping agent | |
| CN212764183U (en) | Double-screw extruder is used in resin production | |
| CN103878968A (en) | Plastic production line | |
| CN212579184U (en) | Extrusion device of wood-plastic extruder | |
| CN210233925U (en) | Plastic extruding machine | |
| CN204874441U (en) | Fatlute extrusion moulding machine | |
| CN221249776U (en) | Plastic extruder with good processing quality | |
| CN116021745B (en) | High-efficient extruder is used in plastics processing | |
| CN215550739U (en) | High-efficient extrusion device of plastic conduit | |
| CN105729618B (en) | Vertical double helix vacuum forming extruder | |
| CN213704445U (en) | Speed-adjustable plastic pipe extrusion traction device | |
| CN216860549U (en) | Continuous blending extruder for various high polymer materials |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CF01 | Termination of patent right due to non-payment of annual fee | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20110921 Termination date: 20190115 |