CN201876211U - Cross rule for detecting size of large cylindrical forging - Google Patents
Cross rule for detecting size of large cylindrical forging Download PDFInfo
- Publication number
- CN201876211U CN201876211U CN2010206109931U CN201020610993U CN201876211U CN 201876211 U CN201876211 U CN 201876211U CN 2010206109931 U CN2010206109931 U CN 2010206109931U CN 201020610993 U CN201020610993 U CN 201020610993U CN 201876211 U CN201876211 U CN 201876211U
- Authority
- CN
- China
- Prior art keywords
- gage
- sleeve
- measuring rule
- movable
- forging
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Lifetime
Links
- 238000005242 forging Methods 0.000 title claims abstract description 25
- 238000007689 inspection Methods 0.000 abstract description 2
- 238000003754 machining Methods 0.000 abstract 1
- 238000010586 diagram Methods 0.000 description 3
- 238000005259 measurement Methods 0.000 description 3
- 238000000034 method Methods 0.000 description 2
- 238000000465 moulding Methods 0.000 description 2
- 230000009286 beneficial effect Effects 0.000 description 1
- 230000002950 deficient Effects 0.000 description 1
- 238000005516 engineering process Methods 0.000 description 1
- 238000004519 manufacturing process Methods 0.000 description 1
- 231100000241 scar Toxicity 0.000 description 1
Images


Landscapes
- A Measuring Device Byusing Mechanical Method (AREA)
Abstract
The utility model discloses a cross rule for detecting the size of a large cylindrical forging, which comprises a fixed measuring rule and a movable measuring rule, wherein a mounting hole is arranged at a middle section of the fixed measuring rule, and a sleeve is upwards arranged in the mounting hole; a sleeve hole is arranged at a middle section of the movable measuring rule, and the upper end of the sleeve is connected with a middle pin; the movable measuring rule is sleeved on the sleeve through the sleeve hole, and sliding grooves are arranged on the movable measuring rule outside the sleeve hole towards the two ends along the length direction; and a suspended hammer assembly is arranged in the sliding grooves and comprises a tally and a suspended hammer which is connected with the tally through a plumb line, and the tally can slide along the sliding grooves on the movable measuring rule. The device has a simple structure and simple steps, and the problem that the sizes of internal and external circles of the cylindrical forging can be accurately measured is solved, the situation that the size is insufficient after machining is effectively prevented, more lining working hours are shortened, and the inspection efficiency is improved.
Description
Technical field
The utility model belongs to technical field of measuring equipment, relates to a kind of cross gage that is used to detect large-scale bobbin forging size.
Background technology
According to the existing equipment of forging industry, the blank of the large-scale bobbin class of heavy wall part adopts flat-die forging mostly.Because the various factors in equipment and the production run, the process gap of the forging ' s block dimension of flat-die forging and requirement is bigger, so must just can carry out machine work later on by each size of check measurement after the forging moulding.Especially the large-scale bobbin forging of flat-die forging moulding, clear scar mark, phenomenon such as uneven appear in unavoidable surface in forging process.Can only use ordinary measring tools such as existing slide calliper rule, tape measure to measure at present, can't measure inner and outer round surface size and concentricity in this case accurately, can very difficult judgement satisfy the workpiece processing dimensional requirement.Therefore, press for a kind of test measuring device that can accurately measure inside and outside circle size and concentricity.
The utility model content
The purpose of this utility model provides a kind of cross gage that is used to detect large-scale bobbin forging size, has solved to rely on the artificial ordinary measring tool that uses to measure the problem of poor accuracy in the prior art.
The technical scheme that the utility model adopted is, a kind of cross gage that is used to detect large-scale bobbin forging size, comprise fixedly gage and movable gage, fixedly the interlude of gage has mounting hole, sleeve upwards is installed in the mounting hole, the interlude of movable gage has sleeve hole, and the upper end of sleeve is connected with intermediate pin, and movable gage is sleeved on the sleeve by sleeve hole; Have chute along its length to two ends outside the sleeve hole of movable gage, be provided with the sash weight assembly in the chute, the sash weight assembly comprises notice plate and the sash weight that is connected by vertical line with notice plate, and notice plate can slide along chute on movable gage.
The beneficial effects of the utility model, simple in structure, step is succinct, has solved the problem of accurate measurement cylinder forging inside and outside circle size, has prevented that effectively the not enough situation of finished size from taking place, and when having shortened more router, has improved and has handed over inspection efficient.
Description of drawings
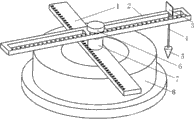
Fig. 1 is the structural representation of the utility model cross gage when being used to detect;
Fig. 2 is fixing gage 1 synoptic diagram;
Fig. 3 is movable gage 2 synoptic diagram;
Fig. 4 is to use the cross gage to detect the enforcement synoptic diagram of bobbin forging inside and outside circle size.
Among the figure, 1. fixing gage, 2. movable gage, 3. notice plate, 4. vertical line, 5. sash weight, 6. intermediate pin, 7. sleeve, 8. flange, 9. sleeve hole, 10. mounting hole, 11. chutes.
Embodiment
Below in conjunction with the drawings and specific embodiments the utility model is elaborated.
With reference to Fig. 1, Fig. 2, Fig. 3, the structure of the utility model cross gage is, comprise fixedly gage 1 and movable gage 2, fixedly the interlude of gage 1 has mounting hole 10, sleeve 7 upwards is installed in the mounting hole 10, the interlude of movable gage 2 has sleeve hole 9, and the upper end of sleeve 7 is connected with intermediate pin 6, and movable gage 2 is sleeved on the sleeve 7 by sleeve hole 9; Have chute 11 along its length to two ends outside the sleeve hole 9 of movable gage 2, be provided with the sash weight assembly in the chute 11, the sash weight assembly comprises notice plate 3 and the sash weight 5 that is connected by vertical line 4 with notice plate 3, and notice plate 3 can slide along chute 11 on movable gage 2.
With reference to Fig. 2, Fig. 3, fixedly gage 1 is the wooden ruler that scale mark is arranged, and fixedly the length of gage 1 is greater than the diameter length of measuring body; Movable gage 2 also is the wooden ruler that scale mark is arranged, and the length of movable gage 2 is with fixedly gage 1 is consistent; Movable gage 2 by sleeve 7 be assembled to fixing gage 1 above; Fixedly gage 1 and movable gage 2 is around intermediate pin 6 rotatable 360 °; Sash weight 5 is connected the datum line that the back forms vertical direction by vertical line 4 with notice plate 3.
With reference to Fig. 1, Fig. 4, the principle of work of the utility model device is, rotary moveable gage 1 and fixedly gage 2 adjust the cylinder center of bobbin forging (flange 8), the positioning and fixing gage 2 then, again movable gage 1 is moved to the radial direction at the defective A of bobbin forging position, then notice plate 3 is moved on to bobbin forging maximum radius position in addition, record notice plate 3 this moment is apart from the distance L of cylinder center
1, the maximum linear distance L at the end of measuring vertical line 4 then to the pit A
2, the nest of measuring is used following formula: R=L
1– L
2, can obtain the minimum exradius R of bobbin of flange 8.
By that analogy, the radius on any point of inside and outside circle of measurement bobbin forging (flange 8) just can determine whether this bobbin forging (flange 8) is to satisfy the qualified forging that part processing requires.
Claims (2)
1. cross gage that is used to detect large-scale bobbin forging size, it is characterized in that: comprise fixedly gage (1) and movable gage (2), fixedly the interlude of gage (1) has mounting hole (10), sleeve (7) upwards is installed in the mounting hole (10), the interlude of movable gage (2) has sleeve hole (9), the upper end of sleeve (7) is connected with intermediate pin (6), and movable gage (2) is sleeved on the sleeve (7) by sleeve hole (9); Have chute (11) along its length to two ends outside the sleeve hole (9) of movable gage (2), chute is provided with the sash weight assembly in (11), the sash weight assembly comprises notice plate (3) and the sash weight (5) that is connected by vertical line (4) with notice plate (3), and notice plate (3) can slide along chute (11) on movable gage (2).
2. the cross gage that is used to detect large-scale bobbin forging size according to claim 1 is characterized in that: the length of described fixedly gage (1) is greater than the diameter length of measuring body.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2010206109931U CN201876211U (en) | 2010-11-17 | 2010-11-17 | Cross rule for detecting size of large cylindrical forging |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CN2010206109931U CN201876211U (en) | 2010-11-17 | 2010-11-17 | Cross rule for detecting size of large cylindrical forging |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN201876211U true CN201876211U (en) | 2011-06-22 |
Family
ID=44164128
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CN2010206109931U Expired - Lifetime CN201876211U (en) | 2010-11-17 | 2010-11-17 | Cross rule for detecting size of large cylindrical forging |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN201876211U (en) |
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102706248A (en) * | 2012-05-18 | 2012-10-03 | 河海大学 | Two-dimensional displacement measurement device and method |
| CN103063100A (en) * | 2012-10-25 | 2013-04-24 | 南京梅山冶金发展有限公司 | Downside dumping type unloading point multifunctional verifying device |
| CN105091706A (en) * | 2015-05-23 | 2015-11-25 | 贵州大学 | Tobacco plant spread angle measuring instrument |
| CN108332629A (en) * | 2018-01-16 | 2018-07-27 | 知新思明科技(北京)有限公司 | Gun barrel nozzle centralized positioning ruler |
| CN108645317A (en) * | 2018-05-03 | 2018-10-12 | 孙佳骏 | A kind of high school mathematics cylinder device for measuring circumference |
| CN115597472A (en) * | 2022-09-27 | 2023-01-13 | 国网江苏省电力有限公司南通供电分公司(Cn) | Iron tower foundation eccentricity measuring device for preventing tower collapse based on center distance |
-
2010
- 2010-11-17 CN CN2010206109931U patent/CN201876211U/en not_active Expired - Lifetime
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102706248A (en) * | 2012-05-18 | 2012-10-03 | 河海大学 | Two-dimensional displacement measurement device and method |
| CN103063100A (en) * | 2012-10-25 | 2013-04-24 | 南京梅山冶金发展有限公司 | Downside dumping type unloading point multifunctional verifying device |
| CN103063100B (en) * | 2012-10-25 | 2016-03-02 | 南京梅山冶金发展有限公司 | Side dump discharge point Multifunctional checking device of a kind of end |
| CN105091706A (en) * | 2015-05-23 | 2015-11-25 | 贵州大学 | Tobacco plant spread angle measuring instrument |
| CN108332629A (en) * | 2018-01-16 | 2018-07-27 | 知新思明科技(北京)有限公司 | Gun barrel nozzle centralized positioning ruler |
| CN108645317A (en) * | 2018-05-03 | 2018-10-12 | 孙佳骏 | A kind of high school mathematics cylinder device for measuring circumference |
| CN115597472A (en) * | 2022-09-27 | 2023-01-13 | 国网江苏省电力有限公司南通供电分公司(Cn) | Iron tower foundation eccentricity measuring device for preventing tower collapse based on center distance |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN204944447U (en) | A kind of can the pick-up unit of continuous coverage deep hole internal diameter | |
| CN201072325Y (en) | Measuring tool especially for hole groove | |
| CN111829479B (en) | A device and method for measuring the shape error of the inner surface of a deep hole of a part | |
| CN202209924U (en) | Oil hole measuring tool for engine connecting rod big end | |
| CN105067046B (en) | A kind of automatic drill riveter calibration method | |
| CN203037195U (en) | Outer cone inclination steel ball measuring gauge | |
| CN204575008U (en) | A kind of tooth pitch measures cubing | |
| CN203163669U (en) | Test tool of gear keyway symmetry degree | |
| CN210664302U (en) | Internal spline coaxiality inspection device and inspection mandrel thereof | |
| CN204555886U (en) | A kind of Wall-Thickness Difference measuring instrument | |
| CN211317140U (en) | Deep hole step height measuring device | |
| CN208998749U (en) | Gear radial clearance and flank of tooth jitter detection apparatus | |
| CN200968846Y (en) | Stepped hole depth measuring instrument | |
| CN209069144U (en) | Internal combustion engine cylinder body main bearing hole circle detection tool that beats | |
| CN219757289U (en) | Spool roundness measurement tool | |
| CN118463823A (en) | Wall thickness measuring device and wall thickness measuring method for thin-wall barrel parts with different conicities | |
| CN211346649U (en) | Tool for detecting span length of inner gear ring of slewing bearing | |
| CN201373726Y (en) | Symmetry degree detection device of parts of complicated shape | |
| CN209355863U (en) | Hole size measuring device | |
| CN213179810U (en) | Measuring device for accurately measuring depth of deep inner hole groove and width of notch | |
| CN112665490B (en) | Eccentric inner curve profile gauge | |
| CN203672279U (en) | Testing tool for detecting gear inner bore diameter | |
| CN204154297U (en) | A kind of on-machine measurement device of large slewing parts Form and position error | |
| CN210070824U (en) | Measuring device for profile milling cutter | |
| CN102706254B (en) | Measuring method for sealing groove in small deep hole |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| CX01 | Expiry of patent term | ||
| CX01 | Expiry of patent term |
Granted publication date: 20110622 |