CN201207017Y - Running-in machine for multi-sleeve bearing - Google Patents
Running-in machine for multi-sleeve bearing Download PDFInfo
- Publication number
- CN201207017Y CN201207017Y CNU2008200291295U CN200820029129U CN201207017Y CN 201207017 Y CN201207017 Y CN 201207017Y CN U2008200291295 U CNU2008200291295 U CN U2008200291295U CN 200820029129 U CN200820029129 U CN 200820029129U CN 201207017 Y CN201207017 Y CN 201207017Y
- Authority
- CN
- China
- Prior art keywords
- running
- head
- bearing
- belt wheel
- machine
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 230000001360 synchronised effect Effects 0.000 claims abstract description 8
- 239000010687 lubricating oil Substances 0.000 claims description 17
- 239000003921 oil Substances 0.000 claims description 12
- 239000003305 oil spill Substances 0.000 claims 1
- 210000004722 stifle Anatomy 0.000 claims 1
- 230000005540 biological transmission Effects 0.000 abstract description 7
- 238000004140 cleaning Methods 0.000 description 8
- 238000004519 manufacturing process Methods 0.000 description 5
- 238000012545 processing Methods 0.000 description 5
- 239000003638 chemical reducing agent Substances 0.000 description 2
- 238000013461 design Methods 0.000 description 2
- 238000005516 engineering process Methods 0.000 description 2
- 239000000463 material Substances 0.000 description 2
- 238000011160 research Methods 0.000 description 2
- 238000001514 detection method Methods 0.000 description 1
- 238000011161 development Methods 0.000 description 1
- 238000010586 diagram Methods 0.000 description 1
- 238000001914 filtration Methods 0.000 description 1
- 230000008676 import Effects 0.000 description 1
- 230000003137 locomotive effect Effects 0.000 description 1
- 238000003754 machining Methods 0.000 description 1
- 238000000034 method Methods 0.000 description 1
- 239000004753 textile Substances 0.000 description 1
Images


Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02P—CLIMATE CHANGE MITIGATION TECHNOLOGIES IN THE PRODUCTION OR PROCESSING OF GOODS
- Y02P70/00—Climate change mitigation technologies in the production process for final industrial or consumer products
- Y02P70/10—Greenhouse gas [GHG] capture, material saving, heat recovery or other energy efficient measures, e.g. motor control, characterised by manufacturing processes, e.g. for rolling metal or metal working
Landscapes
- Sliding-Contact Bearings (AREA)
Abstract
Description
技术领域 technical field
本实用新型属于轴承加工设备技术领域,具体涉及到对轴承进行跑合的装置或设备。The utility model belongs to the technical field of bearing processing equipment, and in particular relates to a device or equipment for running-in a bearing.
技术背景technical background
轴承是一种标准件,在航天、汽车、机床、铁路、能源、家电、纺织等机械设备中得到广泛地应用,随着新材料、新设备、新工艺的开发和应用,轴承的质量以及精度逐步得到了提高。不同的机械设备对轴承的精度要求不相同,汽车、机床、铁路、能源、家电等设备对轴承的精度要求一般不高,普通级轴承就可以满足使用要求,然而,飞机的陀螺仪表、数控机床、火车机车和车厢上使用的轴承,要求精度高、摩擦力矩要小,目前这种高精度的轴承主要依靠进口。Bearing is a standard part, which is widely used in aerospace, automobile, machine tool, railway, energy, household appliances, textile and other mechanical equipment. With the development and application of new materials, new equipment and new processes, the quality and precision of bearings gradually improved. Different mechanical equipment has different precision requirements for bearings. Automobiles, machine tools, railways, energy sources, household appliances and other equipment generally do not have high precision requirements for bearings. Ordinary grade bearings can meet the requirements for use. However, aircraft gyro instruments, CNC machine tools, etc. , The bearings used on train locomotives and carriages require high precision and small frictional torque. At present, such high-precision bearings mainly rely on imports.
确定轴承精度的因素很多,有材料的问题,也有加工工艺的问题,其中轴承的表面的几何精确度以及表面光洁度是确定轴承精度的主要因素,如何提高轴承的精度,目前国内不少的机械加工企业和研究机构开展了研究试验。There are many factors to determine the accuracy of bearings, including material problems and processing technology problems. Among them, the geometric accuracy and surface finish of the bearing surface are the main factors to determine the bearing accuracy. How to improve the accuracy of bearings is currently a lot of domestic machining. Businesses and research institutions conduct research trials.
专利号为02238435.9、发明名称为《轴承跑合机》的中国专利,在主轴尾部安装有以用于装卡的压力缸,压力缸通过安装在空心主轴中的拉杆控制安装在主轴前端的装卡装置,在主轴箱上部的床身上固定有施压装置,施压装置由压力缸和压力缸活塞杆端部安装的施压头组成,施压头上安装有温度检测装置,施压装置的压力缸和装卡装置的压力缸均安装有压力表和压力控制装置,主轴前端安装有一支承座,支承座固定在主轴下部的工作台上。这种结构的轴承跑合机,结构复杂,产品生产成本高,一次只能安装一个轴承,加工效率太低,不能满足生产实践中需要大批量高精度轴承的需要。另外,电动机减速采用机械结构的减速器,机械结构的减速器由于齿轮传动之间的配合误差大,附加震动大,减速器输出轴的转速不是恒定转速,使得被跑合轴承的精度较低。此外,电动机通过皮带传动机构与安装被跑合轴承的主轴相联,皮带传动机构为普通皮带,同样使得被跑合轴承的精度较低。这种轴承跑合机跑合后的轴承,不能满足航天、航空飞行器以及精密仪器仪表所需轴承精度的要求。因此,当前轴承加工技术领域迫切需要解决的一个技术问题是研制一种效率高、精度高的轴承加工跑合设备。The patent number is 02238435.9, and the invention name is "Bearing Running-in Machine". A pressure cylinder for clamping is installed at the end of the main shaft. The pressure cylinder controls the clamping installed at the front end of the main shaft through the pull rod installed in the hollow main shaft. device, a pressure device is fixed on the bed above the headstock, the pressure device is composed of a pressure cylinder and a pressure head installed at the end of the piston rod of the pressure cylinder, a temperature detection device is installed on the pressure head, the pressure of the pressure device The cylinder and the pressure cylinder of the clamping device are all equipped with a pressure gauge and a pressure control device, and a support seat is installed at the front end of the main shaft, and the support seat is fixed on the workbench at the lower part of the main shaft. The bearing running-in machine with this structure has a complex structure, high production cost, and only one bearing can be installed at a time, and the processing efficiency is too low to meet the needs of large quantities of high-precision bearings in production practice. In addition, the motor deceleration adopts a mechanical structure reducer. Due to the large coordination error between the gear transmissions and the additional vibration, the speed of the output shaft of the reducer is not constant, which makes the precision of the running-in bearing low. In addition, the motor is connected with the main shaft on which the running-in bearing is installed through a belt transmission mechanism, and the belt transmission mechanism is an ordinary belt, which also makes the precision of the running-in bearing low. The bearings after running-in of this kind of bearing running-in machine cannot meet the requirements of bearing accuracy required by aerospace, aerospace vehicles and precision instruments. Therefore, a technical problem that urgently needs to be solved in the current field of bearing processing technology is to develop a bearing processing running-in equipment with high efficiency and high precision.
发明内容 Contents of the invention
本实用新型所要解决的技术问题在于克服上述轴承跑合机的缺点,提供一种设计合理、结构简单、定位充分、产品成本低、生产效率高、所加工的轴承精度高的多套轴承跑合机。The technical problem to be solved by the utility model is to overcome the shortcomings of the above-mentioned bearing running-in machine, and provide a multi-set bearing running-in machine with reasonable design, simple structure, sufficient positioning, low product cost, high production efficiency, and high precision of the processed bearings. machine.
解决上述技术问题所采用的技术方案是:在机架上设置有电动机和跑合头固定架,跑合头固定架上设置有跑合头,跑合头上设置有从动齿形带轮,电动机的输出轴上设置有主动齿形带轮,主动齿形带轮通过同步齿形带与从动齿形带轮相联,机架的左侧设置有通过管道与跑合头相联通的过滤器、右侧设置有通过导线与电动机相连接的变频器。The technical solution adopted to solve the above-mentioned technical problems is: a motor and a running-in head fixing frame are arranged on the frame, a running-in head is arranged on the running-in head fixing frame, a driven toothed belt wheel is arranged on the running-in head, The output shaft of the motor is provided with a driving toothed pulley, the driving toothed pulley is connected with the driven toothed pulley through a synchronous belt, and the left side of the frame is provided with a filter connected with the running head through a pipe. The inverter and the right side are provided with a frequency converter connected to the motor through wires.
本实用新型的跑合头为:轴承座的前端设置有前盖、后端设置有闷盖,轴承座上加工有润滑油进油孔、润滑油回油孔、清洗油进油孔、清洗油回油孔,润滑油进油孔和润滑油回油孔通过导管与过滤器相联通,轴承座内设置有用于安装被跑合轴承的主轴,主轴的外端与从动齿形带轮相联。The running-in head of the utility model is as follows: the front end of the bearing seat is provided with a front cover, and the rear end is provided with a stuffy cover, and the bearing seat is processed with lubricating oil inlet holes, lubricating oil return holes, cleaning oil inlet holes, cleaning oil The oil return hole, the lubricating oil inlet hole and the lubricating oil return hole are connected to the filter through the conduit, and the main shaft for installing the running-in bearing is arranged in the bearing seat, and the outer end of the main shaft is connected with the driven toothed pulley .
本实用新型采用了变频器控制电动机的转速,同时采用主动齿形带轮、同步齿形带、从动齿形带轮构成的传动机构将电动机输出的扭转力矩传送到装有被跑合轴承的主轴上,大大提高了被跑合轴承的精度,主轴上可安装10套轴承,可同时对10套轴承进行跑合,跑合头活动联接在跑合头固定架上,与现有的轴承跑合机相比,功效提高10倍,经本实用新型跑合后轴承的迴转精度由跑合前的D级提升到B级。本实用新型具有设计合理、结构简单、产品成本低、生产效率高、所加工的轴承精度高等优点,可作为制造高精度轴承的专用设备。The utility model adopts a frequency converter to control the speed of the motor, and at the same time adopts a transmission mechanism composed of a driving toothed belt wheel, a synchronous toothed belt and a driven toothed belt wheel to transmit the torsional torque output by the motor to the running-in bearing. On the main shaft, the precision of the running-in bearing is greatly improved. 10 sets of bearings can be installed on the main shaft, and 10 sets of bearings can be run-in at the same time. Compared with the integrated machine, the efficacy is increased by 10 times, and the rotation accuracy of the bearing after the running-in of the utility model is improved from the D level before the running-in to the B level. The utility model has the advantages of reasonable design, simple structure, low product cost, high production efficiency, high precision of processed bearings, etc., and can be used as special equipment for manufacturing high-precision bearings.
附图说明 Description of drawings
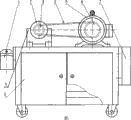
图1是本实用新型一个实施例的结构示意图。Fig. 1 is a schematic structural view of an embodiment of the utility model.
图2是图1的俯视图。FIG. 2 is a top view of FIG. 1 .
图3是图1中跑合头2的结构示意图。FIG. 3 is a structural schematic diagram of the running-in
具体实施方式 Detailed ways
下面结合附图和实施例对本实用新型进一步详细说明,但本实用新型不限于这些实施例。The utility model is described in further detail below in conjunction with accompanying drawing and embodiment, but the utility model is not limited to these embodiments.
实施例1Example 1
在图1、2中,本实施例的多轴承跑合机由过滤器1、跑合头2、从动齿形带轮3、同步齿形带4、主动齿形带轮6、电动机5、变频器7、机架8、跑合头固定架9联接构成。In Figures 1 and 2, the multi-bearing running-in machine of this embodiment consists of a
在机架8上用螺纹紧固联接件固定联接有电动机5和两个跑合头固定架9,两个跑合头固定架9上用螺栓活动联接安装有跑合头2,这种跑合头固定架9,安装跑合头2很方便,提高了工作效率,被跑合的轴承安装在跑合头2内,跑合头2用于对轴承进行跑合,提高轴承的精度,电动机5为本实用新型提供动力,跑合头2上用联接件固定安装有从动齿形带轮3,电动机5的输出轴上用联接件固定安装有主动齿形带轮6,主动齿形带轮6通过同步齿形带4与从动齿形带轮3相联,主动齿形带轮6、同步齿形带4、从动齿形带轮3构成本实用新型的传动机构,这种结构的传动机构,提高了被跑合轴承的精度。机架8的左侧用螺纹紧固联接件固定联接有过滤器1,过滤器1通过管道与跑合头2相联通,过滤器1用于对跑合轴承时所用的润滑油进行过滤。机架8的右侧用螺纹紧固联接件固定联接有变频器7,变频器7通过导线与电动机5相连接,通过变频器7控制电动机5的输入频率,改变电动机5的转速,实现对跑合头2转速的控制,用变频器7控制电动机5的转速,提高了被跑合轴承的精度。On the
图3给出了跑合头2的结构示意图。在图3中,本实施例的跑合头2由闷盖2-1、轴承座2-2、前盖2-4、主轴2-4联接构成。FIG. 3 shows a schematic structural view of the running-in
轴承座2-2的上部径向加工有润滑油进油孔a和润滑油回油孔c,润滑油进油孔a和润滑油回油孔c通过导管与过滤器1相联通,由过滤器1流出的润滑油从润滑油进油孔a进入到轴承座2-2内对被跑合的轴承进行润滑,轴承座2-2内的润滑油从润滑油回油孔c流回到过滤器1进行过滤,轴承座2-2的上部加工有清洗油进油孔b、下部加工有清洗油回油孔d,清洗油进油孔b用于对轴承座2-2内进行清洗时清洗油由清洗油进油孔b流入、从清洗油回油孔d流出。在轴承座2-2的前端用螺栓紧固联接件固定联接有前盖2-4,轴承座2-2的后端用螺栓紧固联接件固定联接有闷盖2-1,轴承座2-2内安装有主轴2-4,从动齿形带轮3用螺纹紧固联接件固定联接在主轴2-4的外端,被跑合的轴承安装在轴承座2-2内的主轴2-4上,主轴2-4上可安装10套被跑合的轴承。The upper part of the bearing seat 2-2 is radially processed with a lubricating oil inlet hole a and a lubricating oil return hole c, and the lubricating oil inlet hole a and the lubricating oil return hole c communicate with the
本实用新型的跑合头2设计为半开式,安装十分方便。主轴2-4上可安装10套轴承,可同时对10套轴承进行跑合,本实用新型与专利号为02238435.9的《轴承跑合机》相比,功效提高10倍,被跑合轴承的精度大大提高,经本实用新型跑合后轴承的迴转精度由跑合前的D级提升到B级。The running-in
Claims (2)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2008200291295U CN201207017Y (en) | 2008-05-16 | 2008-05-16 | Running-in machine for multi-sleeve bearing |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2008200291295U CN201207017Y (en) | 2008-05-16 | 2008-05-16 | Running-in machine for multi-sleeve bearing |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN201207017Y true CN201207017Y (en) | 2009-03-11 |
Family
ID=40466078
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CNU2008200291295U Expired - Fee Related CN201207017Y (en) | 2008-05-16 | 2008-05-16 | Running-in machine for multi-sleeve bearing |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN201207017Y (en) |
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102141474A (en) * | 2011-01-06 | 2011-08-03 | 无锡市第二轴承有限公司 | Bearing running-in testing machine |
| CN102183381A (en) * | 2011-04-26 | 2011-09-14 | 王夏生 | Cleaning running-in machine of sewing machine |
| CN104198019A (en) * | 2014-08-11 | 2014-12-10 | 东本电气科技(苏州)有限公司 | Detection run-in station |
| CN113686575A (en) * | 2021-08-16 | 2021-11-23 | 江苏威玛斯精密机械有限公司 | A full-function dynamic running-in machine control system and control method thereof |
-
2008
- 2008-05-16 CN CNU2008200291295U patent/CN201207017Y/en not_active Expired - Fee Related
Cited By (7)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN102141474A (en) * | 2011-01-06 | 2011-08-03 | 无锡市第二轴承有限公司 | Bearing running-in testing machine |
| CN102141474B (en) * | 2011-01-06 | 2012-11-14 | 无锡市第二轴承有限公司 | Bearing running-in testing machine |
| CN102183381A (en) * | 2011-04-26 | 2011-09-14 | 王夏生 | Cleaning running-in machine of sewing machine |
| CN102183381B (en) * | 2011-04-26 | 2013-11-13 | 王夏生 | Cleaning running-in machine of sewing machine |
| CN104198019A (en) * | 2014-08-11 | 2014-12-10 | 东本电气科技(苏州)有限公司 | Detection run-in station |
| CN113686575A (en) * | 2021-08-16 | 2021-11-23 | 江苏威玛斯精密机械有限公司 | A full-function dynamic running-in machine control system and control method thereof |
| CN113686575B (en) * | 2021-08-16 | 2024-05-10 | 江苏威玛斯精密机械有限公司 | Full-function dynamic running-in machine control system and control method thereof |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN202270998U (en) | Automatic horizontal milling and boring machine | |
| CN202684226U (en) | Numerically-controlled gulleting machine for large cylindrical gear | |
| CN105382281B (en) | Console mode digital-control boring-milling machine ram apparatus | |
| CN108115413B (en) | A kind of process equipment of gear shaft cutting deburring in automobile gearbox | |
| CN101254552A (en) | A Deep Hole Broaching and Boring Machine Tool | |
| CN206690767U (en) | Five-axis engraving machine with mechanical variable speed spindle | |
| CN104308540B (en) | Integral type tooth/spiral case making device and the integral type processing method of tooth/worm gear | |
| CN205362699U (en) | Console mode numerical control boring and milling machine ram device | |
| CN107081483A (en) | Joint of robot RV Key Part of Cycloid Cam Planetary Speed Reducer precision grinders | |
| CN203765231U (en) | Flange welding positioner | |
| CN214920541U (en) | Integrated numerical control machine tool spindle unit | |
| CN103028622B (en) | High-speed aluminum wire drawing machine | |
| CN206794943U (en) | Joint of robot RV Key Part of Cycloid Cam Planetary Speed Reducer precision grinders | |
| CN203236072U (en) | Automatic synchronization tapping machine | |
| CN214869214U (en) | Hybrid bearing main shaft unit mechanism for heavy crankshaft grinding machine | |
| CN208831629U (en) | The dedicated reducer with hardened tooth surface of wire drawing machine | |
| CN213017627U (en) | Self-lubricating gear box for machine tool | |
| CN205685006U (en) | Dual-purpose lathe attacked by a kind of brill | |
| CN203344128U (en) | Wood lathe | |
| CN209632644U (en) | A kind of associated mode Indexing Clamping composite structure | |
| CN209664935U (en) | A kind of internal toothing processing unit (plant) | |
| CN202861869U (en) | Friction wheel traction transmission cycloid machining device | |
| CN209379932U (en) | Gantry machining center main shaft driving structure | |
| CN217914683U (en) | Multi-axis linkage polishing mechanism for precision machining machine tool | |
| CN208826296U (en) | Surface derusting device is used in a kind of production of auto parts and components |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20090311 Termination date: 20110516 |