CN201154427Y - Lithium-ion battery spot welding welding spot positioning device - Google Patents
Lithium-ion battery spot welding welding spot positioning device Download PDFInfo
- Publication number
- CN201154427Y CN201154427Y CNU2007200983107U CN200720098310U CN201154427Y CN 201154427 Y CN201154427 Y CN 201154427Y CN U2007200983107 U CNU2007200983107 U CN U2007200983107U CN 200720098310 U CN200720098310 U CN 200720098310U CN 201154427 Y CN201154427 Y CN 201154427Y
- Authority
- CN
- China
- Prior art keywords
- spot welding
- positioning
- spot
- lithium
- welding
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003466 welding Methods 0.000 title claims abstract description 56
- 229910001416 lithium ion Inorganic materials 0.000 title claims abstract description 15
- HBBGRARXTFLTSG-UHFFFAOYSA-N Lithium ion Chemical compound [Li+] HBBGRARXTFLTSG-UHFFFAOYSA-N 0.000 title claims abstract description 14
- 238000004519 manufacturing process Methods 0.000 abstract description 6
- 239000007788 liquid Substances 0.000 abstract description 3
- 229920000642 polymer Polymers 0.000 abstract description 3
- 230000009286 beneficial effect Effects 0.000 abstract description 2
- 230000001681 protective effect Effects 0.000 description 6
- 238000000034 method Methods 0.000 description 5
- PXHVJJICTQNCMI-UHFFFAOYSA-N Nickel Chemical compound [Ni] PXHVJJICTQNCMI-UHFFFAOYSA-N 0.000 description 4
- 229910000679 solder Inorganic materials 0.000 description 3
- 229910052759 nickel Inorganic materials 0.000 description 2
- 230000007812 deficiency Effects 0.000 description 1
- 238000012986 modification Methods 0.000 description 1
- 230000004048 modification Effects 0.000 description 1
Images

Classifications
-
- Y—GENERAL TAGGING OF NEW TECHNOLOGICAL DEVELOPMENTS; GENERAL TAGGING OF CROSS-SECTIONAL TECHNOLOGIES SPANNING OVER SEVERAL SECTIONS OF THE IPC; TECHNICAL SUBJECTS COVERED BY FORMER USPC CROSS-REFERENCE ART COLLECTIONS [XRACs] AND DIGESTS
- Y02—TECHNOLOGIES OR APPLICATIONS FOR MITIGATION OR ADAPTATION AGAINST CLIMATE CHANGE
- Y02E—REDUCTION OF GREENHOUSE GAS [GHG] EMISSIONS, RELATED TO ENERGY GENERATION, TRANSMISSION OR DISTRIBUTION
- Y02E60/00—Enabling technologies; Technologies with a potential or indirect contribution to GHG emissions mitigation
- Y02E60/10—Energy storage using batteries
Landscapes
- Connection Of Batteries Or Terminals (AREA)
- Secondary Cells (AREA)
Abstract
本实用新型公开了锂离子电池点焊焊点定位装置,它包括点焊底座、连接在所述的点焊底座上的其上连接有定位销的直线导轨、定位座连接在所述的直线导轨上并与之相滑动配合,在所述的定位座上连接有点焊夹具,在位于所述的点焊夹具两侧的定位座上分别连接有通过连接结构与之相横向移动配合的定位块。本实用新型的有益效果是结构简单、使用方便,可以用于各种液态方型锂离子电池以及聚合物电池的生产制造过程中,有效的保证产品质量和提高生产效率。

The utility model discloses a lithium-ion battery spot welding spot positioning device, which comprises a spot welding base, a linear guide rail connected to the spot welding base and a positioning pin connected thereon, and a positioning seat connected to the linear guide rail The spot welding fixture is connected to the positioning seat, and the positioning blocks located on both sides of the spot welding fixture are respectively connected with positioning blocks that move laterally with it through the connecting structure. The utility model has the beneficial effects of simple structure and convenient use, and can be used in the manufacturing process of various liquid square lithium-ion batteries and polymer batteries, effectively ensuring product quality and improving production efficiency.
Description
技术领域 technical field
本实用新型涉及点焊焊点定位装置,特别涉及锂离子电池点焊焊点定位装置。The utility model relates to a spot welding welding point positioning device, in particular to a lithium ion battery spot welding welding point positioning device.
背景技术 Background technique
目前,在通常情况下,为了确保锂离子电池使用的安全性,必须将锂离子电芯与保护线路板装配在一起,通过保护线路板来确保成品电池使用的安全性,但是他们之间的连接方式一般通过点焊的工艺来完成。在实际生产过程中两者之间的焊接一般采用手工定位操作,手工操作会由于无法保证两者之间的平行度和两个焊点的位置而造成焊接强度的不良。有的会造成电芯极耳和保护线路板镍片的损坏,而不得不进行报废;有的会影响产品的使用寿命,造成使用者的抱怨;严重的会影响产品的安全性。At present, in general, in order to ensure the safety of lithium-ion batteries, lithium-ion cells must be assembled with protective circuit boards to ensure the safety of finished batteries by protecting the circuit boards, but the connection between them The method is generally completed by the process of spot welding. In the actual production process, the welding between the two generally adopts manual positioning operation, and manual operation will cause poor welding strength due to the inability to ensure the parallelism between the two and the positions of the two solder joints. Some will cause damage to the tabs of the battery cell and the nickel sheet of the protective circuit board, and have to be scrapped; some will affect the service life of the product and cause complaints from users; seriously affect the safety of the product.
发明内容 Contents of the invention
本实用新型的目的在于克服现有技术不足之处,提供一种结构简单、使用简便、准确可靠的锂离子电池点焊焊点定位装置。The purpose of the utility model is to overcome the deficiencies of the prior art, and provide a lithium-ion battery spot welding welding spot positioning device with simple structure, easy to use, accurate and reliable.
为实现上述目的本实用新型所采用的技术方案是:The technical scheme that the utility model adopts for realizing the above object is:
锂离子电池点焊焊点定位装置,它包括点焊底座、连接在所述的点焊底座上的其上连接有定位销的直线导轨、定位座连接在所述的直线导轨上并与之相滑动配合,在所述的定位座上连接有点焊夹具,在位于所述的点焊夹具两侧的定位座上分别连接有通过连接结构与之相横向移动配合的定位块。Lithium-ion battery spot welding spot positioning device, which includes a spot welding base, a linear guide rail connected to the spot welding base on which a positioning pin is connected, and a positioning seat connected to the linear guide rail and corresponding to it Sliding fit, the spot welding fixture is connected on the positioning seat, and the positioning blocks located on both sides of the spot welding fixture are respectively connected with positioning blocks that move laterally with it through the connecting structure.
本实用新型的有益效果是:The beneficial effects of the utility model are:
1、操作简单,效率高。在开始工作前,只要让技术员通过标准样件调整好此装置后,作业员只要简单的将电池和保护线路板放入点焊夹具中进行焊接即可,免去了不同人员手法的差异,焊点位置不稳定的顾虑以及焊接质量无法有效保证的风险,从而更加准确,可信的制造出好的产品。1. Simple operation and high efficiency. Before starting work, after the technician has adjusted the device through the standard sample, the operator only needs to simply put the battery and protective circuit board into the spot welding fixture for welding, which eliminates the differences in the techniques of different personnel. The concern of unstable point position and the risk that the welding quality cannot be effectively guaranteed, so as to manufacture good products more accurately and credibly.
2、应用范围非常广泛,各种方型,聚合物,液态电池均能够适用。2. The application range is very wide, all kinds of square, polymer and liquid batteries are applicable.
3、成本低,更换方便快捷。采用该装置,效率高、成本低廉。3. Low cost, easy and fast replacement. By adopting the device, the efficiency is high and the cost is low.
总之,本实用新型结构简单、使用方便,可以用于各种液态方型锂离子电池以及聚合物电池的生产制造过程中,有效的保证产品质量和提高生产效率。In a word, the utility model is simple in structure and easy to use, and can be used in the manufacturing process of various liquid prismatic lithium-ion batteries and polymer batteries, effectively ensuring product quality and improving production efficiency.
附图说明 Description of drawings
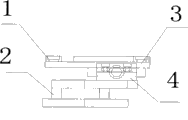
图1为本实用新型的锂离子电池点焊焊点定位装置主视图;Fig. 1 is the front view of the lithium-ion battery spot welding welding spot positioning device of the present utility model;
图2为图1所示装置的俯视图;Fig. 2 is the top view of device shown in Fig. 1;
图3为图1所示装置的点焊夹具视图。Fig. 3 is a view of the spot welding fixture of the device shown in Fig. 1 .
具体实施方式 Detailed ways
下面结合附图和具体实施例对本发明作以详细描述。The present invention will be described in detail below in conjunction with the accompanying drawings and specific embodiments.
如附图所示的锂离子电池点焊焊点定位装置,它包括点焊底座2、连接在所述的点焊底座2上的其上连接有定位销5的直线导轨4、定位座3连接在所述的直线导轨4上并与之相滑动配合,在所述的定位座3上连接有点焊夹具8,在位于所述的点焊夹具两侧的定位座上分别连接有通过连接结构与之相横向移动配合的定位块1。所述的连接结构包括开在定位块上的U形凹槽,在所述的凹槽内设置有螺栓与所述的定位座相连接。As shown in the accompanying drawings, the lithium ion battery spot welding spot positioning device includes a
锂离子电池点焊焊点定位装置其特征在于通过X,Y,Z方向的位置控制可以使得电池正负极耳和保护线路板B+、B-的两个镍触片焊点位置得到有效的保证,由于Y方向上的可移动性,通过点焊底座上定位销的调整,可以控制前焊点和后焊点以及它们之间的最佳距离。Lithium-ion battery spot welding spot positioning device is characterized in that the positions of the positive and negative tabs of the battery and the two nickel contact pieces of the protection circuit board B+ and B- can be effectively guaranteed by position control in the X, Y, and Z directions. , due to the movability in the Y direction, through the adjustment of the positioning pins on the spot welding base, the front and rear welding points and the optimal distance between them can be controlled.
具体使用方法:Specific usage method:
1)将点焊底座首先固定在点焊机的工作台面上,并用螺丝紧固好;1) Fix the spot welding base on the working table of the spot welding machine first, and fasten it with screws;
2)将电芯7和保护线路板6放入点焊夹具中,按要求放置好;2) Put the battery cell 7 and the protective circuit board 6 into the spot welding fixture, and place them as required;
3)此时将点焊夹具再放入定位座中,通过点焊底座的定位销将焊点的Y方向调整到需要的位置;通过定位座的定位块将焊点的X方向调整到需要的位置;调整点焊机的上下电极与电芯极耳和保护线路板触片到需要的位置。3) At this time, put the spot welding fixture into the positioning seat again, adjust the Y direction of the welding point to the required position through the positioning pin of the spot welding base; adjust the X direction of the welding point to the required position through the positioning block of the positioning seat position; adjust the upper and lower electrodes of the spot welding machine, the battery tabs and the contacts of the protective circuit board to the required positions.
4)将定位座往前推动,到极限位置时即可进行第一个焊点的焊接;然后往后推动,到极限位置时即可进行第二个焊点的焊接。4) Push the positioning seat forward, and the welding of the first solder spot can be performed when it reaches the limit position; then push it backward, and the second solder spot can be welded when it reaches the limit position.
5)后续的工作只需将放有电芯和保护线路板的点焊夹具放入到定位座中重复4)的动作即可。5) Subsequent work only needs to put the spot welding fixture with the battery cell and the protective circuit board into the positioning seat and repeat the action of 4).
上述参照实施例对该锂离子电池点焊焊点定位装置进行的详细描述,是说明性的而不是限定性的,因此在不脱离本实用新型总体构思下的变化和修改,应属本实用新型的保护范围之内。The above-mentioned detailed description of the lithium-ion battery spot welding spot welding spot positioning device with reference to the embodiment is illustrative rather than restrictive, so changes and modifications without departing from the general concept of the present utility model should belong to the utility model within the scope of protection.
Claims (2)
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2007200983107U CN201154427Y (en) | 2007-12-04 | 2007-12-04 | Lithium-ion battery spot welding welding spot positioning device |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2007200983107U CN201154427Y (en) | 2007-12-04 | 2007-12-04 | Lithium-ion battery spot welding welding spot positioning device |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN201154427Y true CN201154427Y (en) | 2008-11-26 |
Family
ID=40102216
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CNU2007200983107U Expired - Fee Related CN201154427Y (en) | 2007-12-04 | 2007-12-04 | Lithium-ion battery spot welding welding spot positioning device |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN201154427Y (en) |
Cited By (5)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2012068882A1 (en) * | 2010-11-24 | 2012-05-31 | 长春轨道客车股份有限公司 | Pairing seat for disk brake hanging brackets |
| CN103659068A (en) * | 2012-09-26 | 2014-03-26 | 天宇通讯科技(昆山)有限公司 | Battery pack automatic spot welding locating device |
| CN103682453A (en) * | 2013-11-06 | 2014-03-26 | 朱云 | Battery assembling method and clamp |
| CN103962758A (en) * | 2013-01-28 | 2014-08-06 | 上海新朋联众汽车零部件有限公司 | Movable welding guide device |
| CN109623119A (en) * | 2019-01-09 | 2019-04-16 | 湖南福德电气有限公司 | Resistance band spot welding auxiliary device |
-
2007
- 2007-12-04 CN CNU2007200983107U patent/CN201154427Y/en not_active Expired - Fee Related
Cited By (6)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| WO2012068882A1 (en) * | 2010-11-24 | 2012-05-31 | 长春轨道客车股份有限公司 | Pairing seat for disk brake hanging brackets |
| CN103659068A (en) * | 2012-09-26 | 2014-03-26 | 天宇通讯科技(昆山)有限公司 | Battery pack automatic spot welding locating device |
| CN103962758A (en) * | 2013-01-28 | 2014-08-06 | 上海新朋联众汽车零部件有限公司 | Movable welding guide device |
| CN103682453A (en) * | 2013-11-06 | 2014-03-26 | 朱云 | Battery assembling method and clamp |
| CN103682453B (en) * | 2013-11-06 | 2016-05-04 | 朱云 | Battery assembly method and fixture |
| CN109623119A (en) * | 2019-01-09 | 2019-04-16 | 湖南福德电气有限公司 | Resistance band spot welding auxiliary device |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN205200849U (en) | Power battery module welding set | |
| CN203679540U (en) | Compressing mechanism applied to laser welding | |
| CN202479680U (en) | Secondary battery spot welding machine | |
| CN208246136U (en) | An ultrasonic welding jig for a square cell | |
| CN202661489U (en) | A battery size and insulation performance testing jig | |
| CN204053252U (en) | A laser welding jig for lithium ion battery assembly | |
| CN203751540U (en) | Double-station square lithium battery case laser welding jig | |
| CN206764202U (en) | A kind of photovoltaic module welding of battery film auxiliary positioning tool | |
| CN216117938U (en) | A lithium battery cell short circuit test device | |
| CN202177643U (en) | Lithium ion battery internal resistance voltage detection clamp | |
| CN218396682U (en) | Frock clamp is used in welding of lithium cell multilayer foil utmost point ear | |
| CN204504458U (en) | The welding clamp of tape guide groove | |
| CN208358018U (en) | A kind of Soft Roll laminated type lithium ion battery supersonic welding transfer electrode lug frock clamp | |
| CN201146208Y (en) | A lithium-ion battery pole tab tab welding fixture | |
| CN212705236U (en) | Battery module location buffering pressfitting frock | |
| CN211614728U (en) | A jig tooling for the welding of lithium ion battery module shells | |
| CN204538113U (en) | A kind of soft pack cell tab welding clamp | |
| CN109396598B (en) | Welding strip positioning device and welding strip moving and placing equipment | |
| CN202494764U (en) | Testing tool of small battery | |
| CN106041290A (en) | Continuous ultrasonic electric welding device | |
| CN209919199U (en) | Soldering tool for PIN pin of car switch | |
| CN201856043U (en) | Medium-density series battery pole group welding device | |
| CN201128058Y (en) | Lithium-ion battery spot welding rotary device | |
| CN202905892U (en) | Lithium-ion battery testing and battery tab shaping and cutting integrated device | |
| CN203031146U (en) | Adjustable clamp device for laser welding of aluminum case cell |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20081126 Termination date: 20111204 |