CN201120490Y - HPC groove shaped butt mill - Google Patents
HPC groove shaped butt mill Download PDFInfo
- Publication number
- CN201120490Y CN201120490Y CNU2007203057401U CN200720305740U CN201120490Y CN 201120490 Y CN201120490 Y CN 201120490Y CN U2007203057401 U CNU2007203057401 U CN U2007203057401U CN 200720305740 U CN200720305740 U CN 200720305740U CN 201120490 Y CN201120490 Y CN 201120490Y
- Authority
- CN
- China
- Prior art keywords
- cutting
- cutter
- hpc
- milling cutter
- cutting tool
- Prior art date
- Legal status (The legal status is an assumption and is not a legal conclusion. Google has not performed a legal analysis and makes no representation as to the accuracy of the status listed.)
- Expired - Fee Related
Links
- 238000003801 milling Methods 0.000 claims abstract description 13
- 238000005520 cutting process Methods 0.000 abstract description 24
- 238000003754 machining Methods 0.000 abstract description 5
- 238000007599 discharging Methods 0.000 abstract 1
- 239000002184 metal Substances 0.000 description 5
- 238000000034 method Methods 0.000 description 4
- 238000005516 engineering process Methods 0.000 description 2
- 238000010586 diagram Methods 0.000 description 1
- 230000000694 effects Effects 0.000 description 1
- 238000009499 grossing Methods 0.000 description 1
- 230000013011 mating Effects 0.000 description 1
- 238000005728 strengthening Methods 0.000 description 1
- 230000007704 transition Effects 0.000 description 1
- 238000005303 weighing Methods 0.000 description 1
Images

Landscapes
- Milling Processes (AREA)
Abstract
The utility model relates to an HPC sulciform end milling cutter, and the milling cutter has a pole structure and an edge flute is a spiral groove with equal helical angle. The radius value of curvature of curve of the groove bottom is 0.2-0.5 time of the diameter of a cutting tool. The end milling cutter has advantages of small deformation of chipping and low cutting heat; smooth discharging of chipping; big strength of cutter teeth and being adapted to large feed amount cutting process; and good rigidity of the edge part of the cutting tool, small vibration when cutting and improved surface quality. The service life of the cutting tool can be extended by 35 percent due to the advantages, therefore the end milling cutter is more suitable for the HPC machining mode, and can reduce the use cost of the cutting tool.
Description
Affiliated field: the utility model relates to a kind of HPC slotting cutter.
Background technology:
Along with the CNC process technology is increasingly mature, working (machining) efficiency more and more is much accounted of, and it directly determines the height of processing cost, the length of delivery cycle.At this present situation, exigence improves the working (machining) efficiency of conventional tool.Several key factors of weighing working (machining) efficiency have: cutting speed, cutting width, cutting depth and feed speed.According to the curve of cutting speed and cutter life, under common processing mode (middle low speed processing is in the majority), the simple raising cutting speed that relies on improves working (machining) efficiency, and the height that cost can be suitable mainly is that the cost of lathe is very high.Therefore improve feed speed, reasonably mating cutting depth and cutting width becomes a kind of more economic and practical, reasonable plan more.Common flute profile slotting cutter bottom land radius of curvature is little, and chip space is little, if increasing cutting width or increasing under the condition of feed speed, very easily cause chip removal not smooth, can not carry out normal process.Therefore increase the sectional area of chip pocket, could guarantee normally carrying out of processing.This slotting cutter has designed the flute profile of larger radius of curvature at HPC (High Performance Cutting) high efficiency processing mode.
Summary of the invention:
The purpose of this utility model provides a kind of slotting cutter of suitable high efficiency processing.The purpose of this utility model is to realize by following structure: the utility model is a spiral flute profile slotting cutter, and milling cutter is a bar type structure, and flute is the helicla flute of equal helix angle, strengthens the radius of curvature of flute profile bottom land.Characteristics of the present utility model: 1, the bottom land radius of curvature is big.Bottom land radius of curvature value is 0.2~0.5 times of tool diameter, and this flute profile radius of curvature increases the chip curling radius, has reduced the distortion of smear metal, reduces the generation of cutting edge heat in metal cutting, thereby improves cutter life.2, the chip space of flute is big.The problem that smear metal is difficult to discharge when solving roughing feed amount, big cutting width makes smear metal quick and smoothly by bottom land curved surface and curling, and the centrifugal force during by cutting is dished out, and guarantees carrying out smoothly of processing.3, cutter tooth intensity is big.This special curved grooves also has the effect of strengthening the back of tooth, make the intensity of single cutter tooth more traditional want high, more can be competent at the processing mode of big cutting data.4, cutter good rigidly.Because the flute profile of this structure has been made the curve with larger radius of curvature, so it is thick to increase the core of cutter, make the rigidity of cutter better, the vibration in reducing to process, thus improve machined surface quality.This structure can prolong cutter life 35%.
Description of drawings:
Fig. 1 is the utility model HPC flute profile slotting cutter overall structure schematic diagram.
Fig. 2 is that cross section, A-A perpendicular to the milling cutter axis is to projection view.
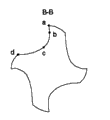
Fig. 3 is that cutting plane B-B perpendicular to the milling cutter helix is to projection view.
The specific embodiment:
As shown in Figure 1, the utility model is a kind of HPC flute profile slotting cutter, and this milling cutter is a bar type structure.Among Fig. 1,1 is shank, and 2 is blade.This milling cutter is that helical angle is the flute profile slotting cutter of L.
Fig. 2 for HPC flute profile slotting cutter perpendicular to the cross section, A-A (marking among Fig. 1) of axis to projection view.R is in the cross section, A-A projection view, the chip curling groove radius of curvature of Zhou Ren, and its value is 0.2~0.5 times of tool diameter.In the cross section, A-A projection view shown in Figure 2, F represents the rib bandwidth of milling cutter.
Fig. 3 for the HPC slotting cutter perpendicular to a certain cutting plane B-B (marking among Fig. 1) of milling cutter helix to projection view.Constitute the cutter slot cross-section contour curve of a tooth of milling cutter by an a, b, c, d.From point of a knife a point, ab is one section inner concave curve, and bc was b point and the one section inner concave curve tangent with curve ab, cd be the c point and with one section inner concave curve of bc contact of a curve.The transition of each section line smoothing connects.
Version key of the present utility model is the flute bottom land radius of curvature by the redesign helical end mills, strengthen bottom land radius of curvature to the 0.2~0.5 times tool diameter of flute profile, increase the chip space of flute, made the smooth more discharge of smear metal, can satisfy the requirement of high efficiency cutting.This in addition structure has increased the intensity of cutter tooth and the rigidity of cutter itself, avoids tipping, can reduce the vibration that cutter produces in process, thereby improves suface processing quality and prolong cutter life.
Claims (1)
1. the flute profile slotting cutter of a suitable HPC processing, it is characterized in that: milling cutter is a bar type structure, spiral flute profile bottom land radius of curvature is 0.2~0.5 times of tool diameter.
Priority Applications (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2007203057401U CN201120490Y (en) | 2007-11-16 | 2007-11-16 | HPC groove shaped butt mill |
Applications Claiming Priority (1)
| Application Number | Priority Date | Filing Date | Title |
|---|---|---|---|
| CNU2007203057401U CN201120490Y (en) | 2007-11-16 | 2007-11-16 | HPC groove shaped butt mill |
Publications (1)
| Publication Number | Publication Date |
|---|---|
| CN201120490Y true CN201120490Y (en) | 2008-09-24 |
Family
ID=40007710
Family Applications (1)
| Application Number | Title | Priority Date | Filing Date |
|---|---|---|---|
| CNU2007203057401U Expired - Fee Related CN201120490Y (en) | 2007-11-16 | 2007-11-16 | HPC groove shaped butt mill |
Country Status (1)
| Country | Link |
|---|---|
| CN (1) | CN201120490Y (en) |
Cited By (2)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101844244A (en) * | 2009-03-23 | 2010-09-29 | 三菱综合材料株式会社 | Slotting cutter |
| CN108746793A (en) * | 2018-07-19 | 2018-11-06 | 苏州阿诺精密切削技术有限公司 | Human body knee joint tibial plate processing milling cutter |
-
2007
- 2007-11-16 CN CNU2007203057401U patent/CN201120490Y/en not_active Expired - Fee Related
Cited By (4)
| Publication number | Priority date | Publication date | Assignee | Title |
|---|---|---|---|---|
| CN101844244A (en) * | 2009-03-23 | 2010-09-29 | 三菱综合材料株式会社 | Slotting cutter |
| CN101844244B (en) * | 2009-03-23 | 2013-08-14 | 三菱综合材料株式会社 | End mill |
| CN108746793A (en) * | 2018-07-19 | 2018-11-06 | 苏州阿诺精密切削技术有限公司 | Human body knee joint tibial plate processing milling cutter |
| CN108746793B (en) * | 2018-07-19 | 2024-05-03 | 苏州阿诺精密切削技术有限公司 | Precision milling cutter for machining tibia plate of human knee joint |
Similar Documents
| Publication | Publication Date | Title |
|---|---|---|
| CN206253710U (en) | A kind of four sword radius end mills | |
| CN201455380U (en) | Groove semi-finishing milling cutter with arc wavy edge | |
| CN210848523U (en) | Gradual change helical angle milling cutter | |
| CN203725860U (en) | High-efficiency inner-cooling end milling cutter for processing titanium alloy slot/cavity | |
| CN217727374U (en) | Unequal rough and fine integrated reamer | |
| CN220782372U (en) | Four-edge ball end milling cutter | |
| CN216828695U (en) | Hole machining tool | |
| CN215090915U (en) | Large spiral angle type coating finish milling cutter | |
| CN217343747U (en) | Large arc taper spherical milling cutter | |
| CN209664392U (en) | Cylinder cap fuel injector aperture knife tool | |
| CN210996740U (en) | Straight milling cutter for processing aluminum profile | |
| CN210359463U (en) | Novel machining tool without regrinding | |
| CN208146983U (en) | A kind of thin plate drilling integration tool of the chip breaking reducing vibration | |
| CN210789370U (en) | Multifunctional stepped drill bit | |
| CN211966071U (en) | Detachable multi-section corn milling cutter | |
| CN208528168U (en) | A kind of milling cutter for processing aero titanium alloy | |
| CN213002838U (en) | Improved cutter for machining aperture of lower cylinder iron casting | |
| CN206383254U (en) | A kind of cemented carbide spiral mill | |
| CN217889630U (en) | Four-edge end mill | |
| CN206952240U (en) | A kind of pump housing semicircle aperture cutter of improved structure | |
| CN219852309U (en) | Milling cutter with lengthened cutting edge | |
| CN221560951U (en) | PCD mills whetstone suitable for carborundum rough milling | |
| CN222931877U (en) | Ball end milling cutter with serrated cutting edge | |
| CN222818012U (en) | Spiral blade MCD milling cutter | |
| CN217433959U (en) | Double-edge upper chip removal T-shaped cutter |
Legal Events
| Date | Code | Title | Description |
|---|---|---|---|
| C14 | Grant of patent or utility model | ||
| GR01 | Patent grant | ||
| C17 | Cessation of patent right | ||
| CF01 | Termination of patent right due to non-payment of annual fee |
Granted publication date: 20080924 Termination date: 20091216 |